Sundance
Sundance was our internal code name for the shared program behind Kaleidescape’s Strato and Alto products. The commercial names were settled late, close to release. In Kaleidescape’s October 2015 Encore announcement, Strato and Alto were the movie players and Terra was the movie server. This case study follows my mechanical work on the program’s four-drive, two-rack-unit server and its front-drive mechanism.
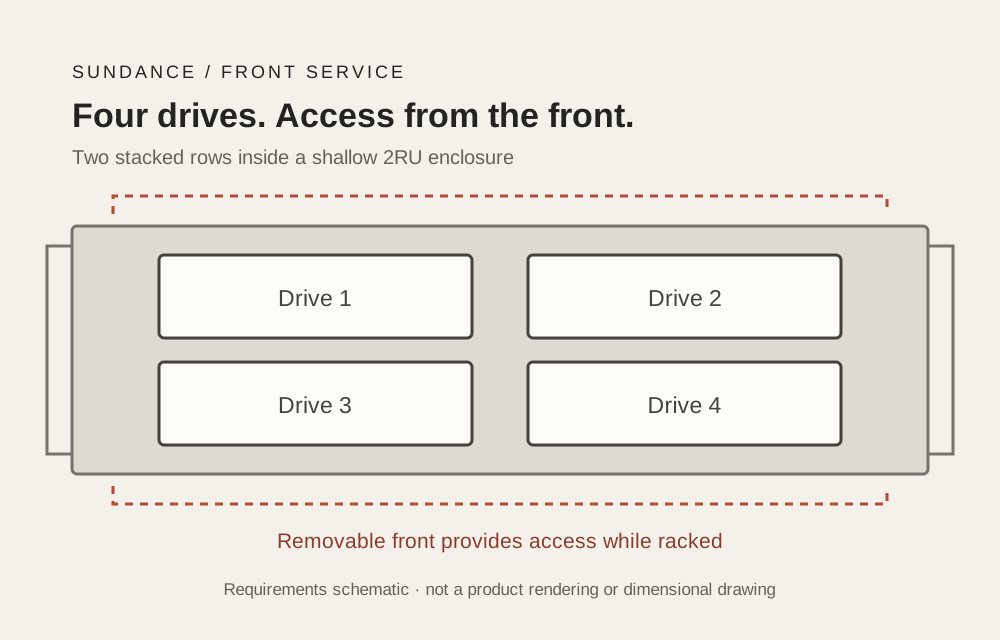
The server brought four front-access hard drives into a shallow enclosure. The user needed to remove a drive while the server stayed in the rack. Inside, that same drive had to remain isolated from the enclosure, locate against its connector and latch securely behind a removable cosmetic front.
My contribution was senior mechanical design engineering for the enclosure and front-drive mechanism. I worked across the chassis, bezel, drive rails and supplier interfaces with Kaleidescape’s hardware team and Function Engineering. Industrial design, electrical design, system testing and manufacturing remained shared responsibilities. The work developed through 2014 and early 2015, from the service-access concept into tooling, prototype fit and validated production corrections.
A front that had to open
The requirements proposal called for four 3.5-inch drives in two stacked rows, accessible without rack removal or enclosure disassembly. The proposed package was 17 inches wide, 3.438 inches high and 10 inches deep. It also needed room for a custom main board and two 60 mm fans. The 15 CFM airflow figure was a design target.
The June system concept put the drive connectors on a mounting plate and considered both internal and external power supplies. A June 18 packaging study also tested the shallower Cinema One height. It exposed crowded drive spacing and interference around the button assembly, while comparing formed-metal guides, plastic guides and a complete sled as different ways to locate the drives. By the July industrial-design review, the team had narrowed several front-access ideas, including hinged doors, to two preferred treatments with a detachable face. Finger scoops also served as air vents. The front was therefore part of the cooling path as well as the user’s route to a failed drive.
Those relationships persisted into the detailed work. January tasks assigned me changes to the bezel’s drive openings and perimeter air inlets, along with matching changes to the blanking plate and HDD frame. Function Engineering carried lead-in and retention-feature tasks. A useful front opening required the cosmetic surface, internal frame and drive mechanism to agree on where the drive could move.
Front-service arrangement
An explanatory schematic drawn from the requirements: four drives in two stacked rows, accessible while the server stays in the rack. It is not final industrial design or a dimensional drawing.
Fitting the board to the enclosure
The main-board review made the electrical components part of the enclosure problem. In August, the review compared supplied connector models with their drawings and checked connector overhang, reset-switch reach, SATA orientation and mounting-hole clearance. Some reference models represented a different connector variant, so their geometry could not simply be accepted as the mechanical definition. The review also considered moving the board mounts to preserve usable space in front of the board. These were coordination questions for the hardware team, not a record that every proposed adjustment was adopted.
Isolation changed the drive constraint
The HDD rail had several jobs: guide insertion, retain the drive, permit removal and limit the hard contact paths carrying vibration into the enclosure. Resolving one of those jobs could disturb another. A stiffer guide could improve location while undermining isolation; a looser interface could improve freedom of movement while reducing control at the latch and connector.
The January task record assigned me two explicit changes: fully enclose the drive in elastomer with no plastic contact points, and return to shoulder screws. The assembly definition records eight rails and sixteen shoulder screws across four drives. The screw’s shoulder provides a defined locating geometry instead of relying only on how far a threaded fastener is tightened.
This was a specific contact-and-constraint design, with the rail coordinated against the bezel opening, blanking plate and formed HDD frame. The record supports that mechanical account. It does not establish a measured acoustic improvement attributable to the rail change alone.
Retention and connection shared a tolerance loop
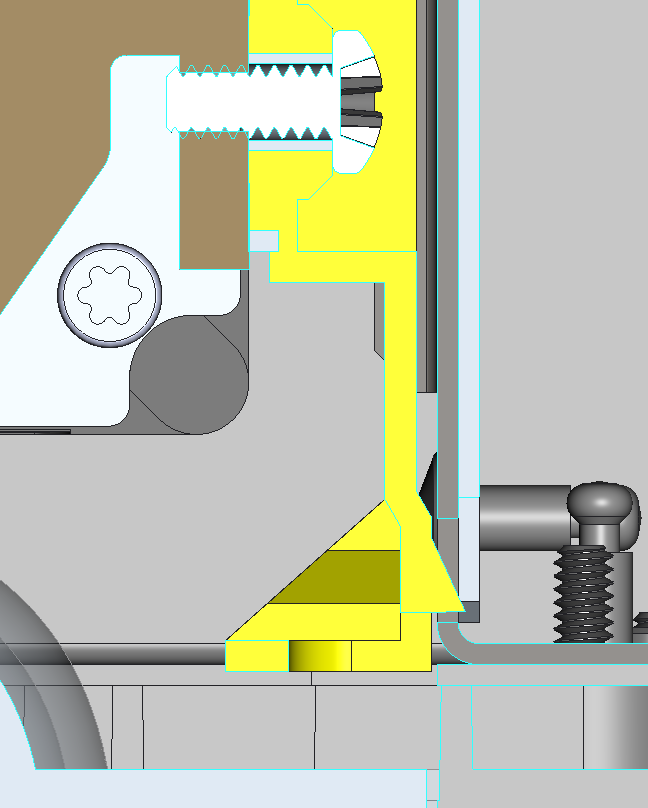
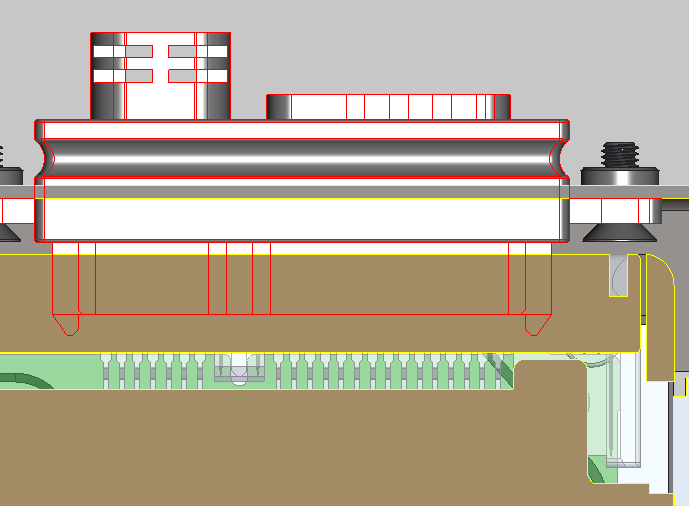
The January 15 tolerance review made the relationship between the front latch and the rear connector explicit. T. DeArk’s analysis, checked by C. Davis, followed the stack from the interior bezel catch through the chassis and HDD cage to the SATA connector hard stop, then back through the drive screw location and the rail’s snap feature.
The nominal gap was positive, but the combined limits allowed interference:
| January review condition | Calculated minimum gap |
|---|---|
| Nominal geometry | 0.50 mm |
| Worst-case stack | -0.36 mm |
| Root-sum-square stack | 0.12 mm |
These are different calculations of the same review configuration. The positive RSS result was not a later fix. The workbook’s conclusion called for a larger snap-to-bezel gap and a check of SATA wipe length to maintain connector continuity.
That distinction shaped the engineering work. Moving a latch until it could engage was only useful if the drive still reached its electrical connection. The corrective geometry had to satisfy both ends of the stack. The section views below show those interfaces in the configuration under review; they do not depict a verified final clearance.
The subsequent snap/SATA correction was taken through tolerance analysis and validation into production. The worksheet above captures the earlier risk.
The two ends of the retention loop
Original embedded section views from the January 15, 2015 tolerance workbook. Analysis by T. DeArk, checked by C. Davis. These show the configuration under review, before the later validated production corrections.
Toolability and assembled fit
The removable front also changed how the cosmetic face was supported. October reviews with Nissha distinguished Sundance’s threaded-insert bosses and metal backing plate from the heat-staked construction of an earlier front. The supplier’s proposed boss and parting-line details had to preserve the visible surface as well as the fastening arrangement. Nissha’s response warned that the current boss geometry would leave visible sink marks and proposed thinner sections; the exchange records that manufacturing tradeoff, not a verified final cosmetic result.
The rail also had to survive the molding process. The October plastics quote gave its tool a 45-day lead, compared with 30 or 35 days for the other listed tools. November supplier DFM comments addressed thin walls, ribs, draft and the junction between the two shots. February comments continued to address fill, deformation and warping. Those were consequential geometry and process decisions inside the functional part.
The February supplier reviews connected those concerns to the geometry of the whole removable front. Yomura proposed wider openings around the carrier faceplate’s four end features so the mold would not depend on thin, fragile steel. Its bezel proposal used angled tooling to release eight hooks. On the two-shot drive rail, the supplier flagged a thin first-shot wall that could deform during overmolding, a notch vulnerable to warping, and a hook whose molded shape had to preserve a functional tolerance. The review tied mold filling, tool release and local stiffness to the same interfaces that made the front serviceable. These were supplier proposals for review, not a record that every proposed change reached production.
The sheet-metal prototypes exposed a different part of the same interface problem. The February AFT inspection record described an inward-bent front flange preventing bezel hooks from engaging. It also reported drive insertion binding where formed shelves scraped the rail, even though the rail’s checked width was within tolerance. Our observations did not agree on every sample condition, which made the actual mating features more useful than a blanket judgment that the chassis was good or bad.
The follow-up sent to AFT separated specific forming, alignment and flange-relief changes from options still being discussed, including rivets, spot welds and fixture features. The part had to fit after forming and assembly, at the location where the drive actually traveled. Passing a nominal dimension elsewhere on the bend was insufficient.
The flange/rail-fit correction, like the snap/SATA correction, was carried through tolerance analysis and validation into production. That result does not turn every supplier proposal in the review packet into an adopted change.
Making the prototype build assemble
The February 6 change notice, ECO-001466, released mechanical files and updated the related BOMs. It distinguished prototype rack ears and other prototype metal assemblies from the broader set of hardware and board changes. MASS Precision then asked which parts it should quote and build. The release organized the next build; it did not, by itself, certify an assembled server.
Cosmetic finish added another assembly variable. In February, Nathan Forster reported that assembling painted cast-plastic prototypes required more filing and scraping than Hunter could reasonably perform. He proposed proceeding with unpainted parts for the engineering build.
I agreed, called Stratasys Direct and instructed Jason Prior to omit paint and graphics from the cast parts. Mark McKenzie supported the decision. On February 26, Jason confirmed that he had instructed his team to ship the available parts unpainted and without graphics.
This selected a prototype build configuration focused on assembly and engineering evaluation. It was separate from the production forming and interface corrections. The correspondence records the supplier instruction and a planned build; it does not establish a measured yield or prove that every planned unit assembled successfully.
From detailed design into production
The engineering result connected the front-service mechanism to the physical behavior of its mating parts. Both the snap/SATA and AFT flange/rail-fit corrections reached production following tolerance analysis and validation. Function Engineering’s analysis and Kaleidescape’s hardware and supplier work were part of that result, alongside my mechanical design contribution.
By early March 2015, my work was moving into handoff. March 5 correspondence arranged the return of an external drive with CAD data on March 9. That is the documented handoff plan; it does not establish a complete transferred database or the date of final product shipment.
Source notes
The architecture and mechanical assignments come from the requirements proposal, June and July design presentations, January task records and the assembly BOM. The retention calculation comes from the original January 15 workbook, authored by T. DeArk and checked by C. Davis. Supplier DFM and AFT review records establish the manufacturing iterations. Retained February and March correspondence records the prototype-finishing decision and scheduled handoff. My September 2026 recollection confirms that both interface corrections entered production after tolerance analysis and validation.
My September 2026 recollection also identifies Sundance as the shared program code name and places the commercial naming late in development. The October 2015 product announcement establishes the public family names and roles.
The hero is the product-family photograph I selected from the project archive. The gallery schematic explains the front-service requirements. The two original workbook diagrams show the earlier analysis configuration, with their authorship and limits preserved.
The product family
Kaleidescape product-family photograph selected from the project archive. Sundance was the shared program code name; this account focuses on the four-drive server mechanics within that program.
