DV700 Disc Vault
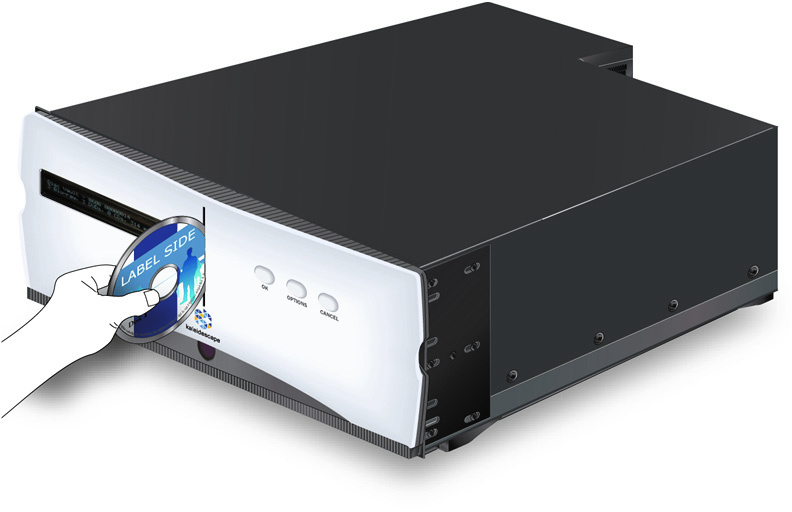
The DV700 Disc Vault made a physical disc collection accessible through a Kaleidescape system. It stored up to 320 discs and handled loading, identification and retrieval through a single front slot. Unlike the M700, it did not include an integrated M-Class player. The DV700 had its own installation guide by January 2012; the work described here concerns its later sustaining investigation in 2014.
I worked with the hardware and service teams to investigate returned vaults, test suspect roller assemblies, and develop changes to the common disc-handling mechanism. The DV700 and M700 shared this mechanical work, but their return histories remained separate. My part of the effort connected observed failures to controlled tests, component definitions, inspection criteria and assembly instructions.
Separate the complaint from the failure
A report that a disc was stuck did not identify which interface had failed. In one DV700 return, three Blu-ray test discs were recognized while three DVDs and three CDs were not. The inspection notes record replacement of the optical drive, recognition of all nine test discs, roller cleaning and a passed run-in. Other DV700 returns did not reproduce their original complaint at all. These were different investigation states, even when the customer symptoms sounded similar.
Another DV700 return contained a cardboard disc with no center hole trapped inside the optical drive. The service worksheet records that I removed it, the optical drive was replaced, and the unit subsequently passed its run-in. Keeping that case separate from roller slippage mattered: similar symptoms could lead to different repairs.
Reproduction also depended on the condition in which the unit was tested. When a new DV700 repeatedly failed run-in in March, I recorded the reported error and separate assembly observations. Richard Lane and Nathan Forster joined the investigation; after the carousel was moved by hand, Richard called for another run because that intervention might have changed the evidence. A mechanism that turned freely during inspection could still have failed in the assembled, powered system.
DV700 loading interface
Make the test earn its conclusion
The shared roller investigation used a known-good vault as a baseline. I installed suspect assemblies from returns, ran front-slot and optical-drive transfers, and kept the test discs for comparison. Some returned rollers ran without reproducing the original timeout. Disc scratching could still appear, so I proposed changing one contact surface at a time and comparing it with the baseline disc.
One apparent result had to be withdrawn. I initially thought installation of the disc-retention cover was causing the rear roller assembly to bind. The cause in that test was a longer screw I had installed in the lower circuit-board mounting hole, forcing the optical drive out of alignment. Replacing it with the correct shorter screw restored normal injection and ejection. Recording that correction kept a test-setup error from becoming a product-design conclusion.
More grip changed the alignment problem
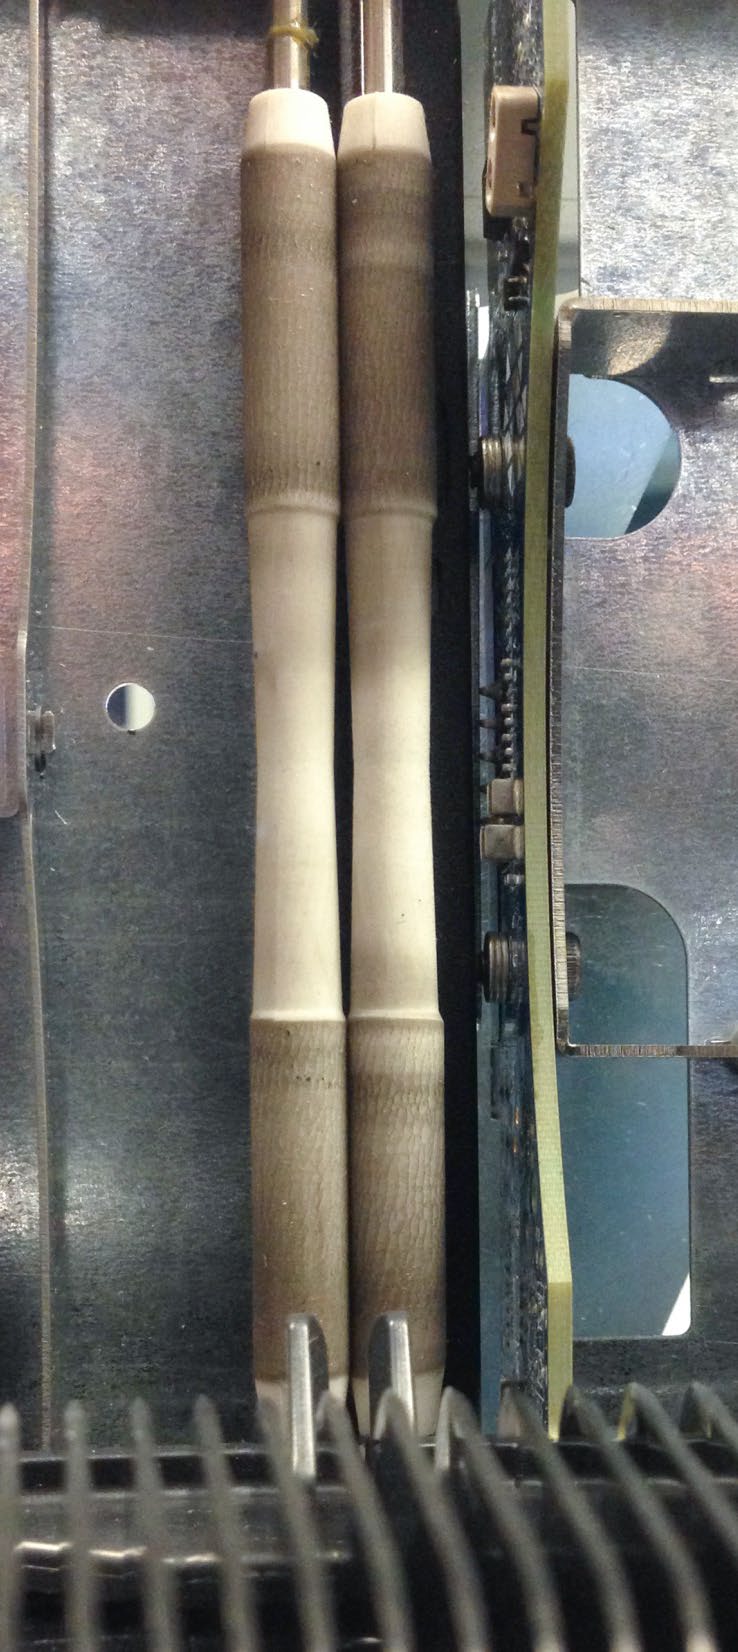
Contamination exposed a mechanical tradeoff. The April roller study recorded slippage at the optical drive and, in some cases, the front slot. Increasing spring force improved tolerance to a dirty roller surface, but the higher load also bent the roller shafts. More traction could therefore move the disc path out of alignment with the next opening.
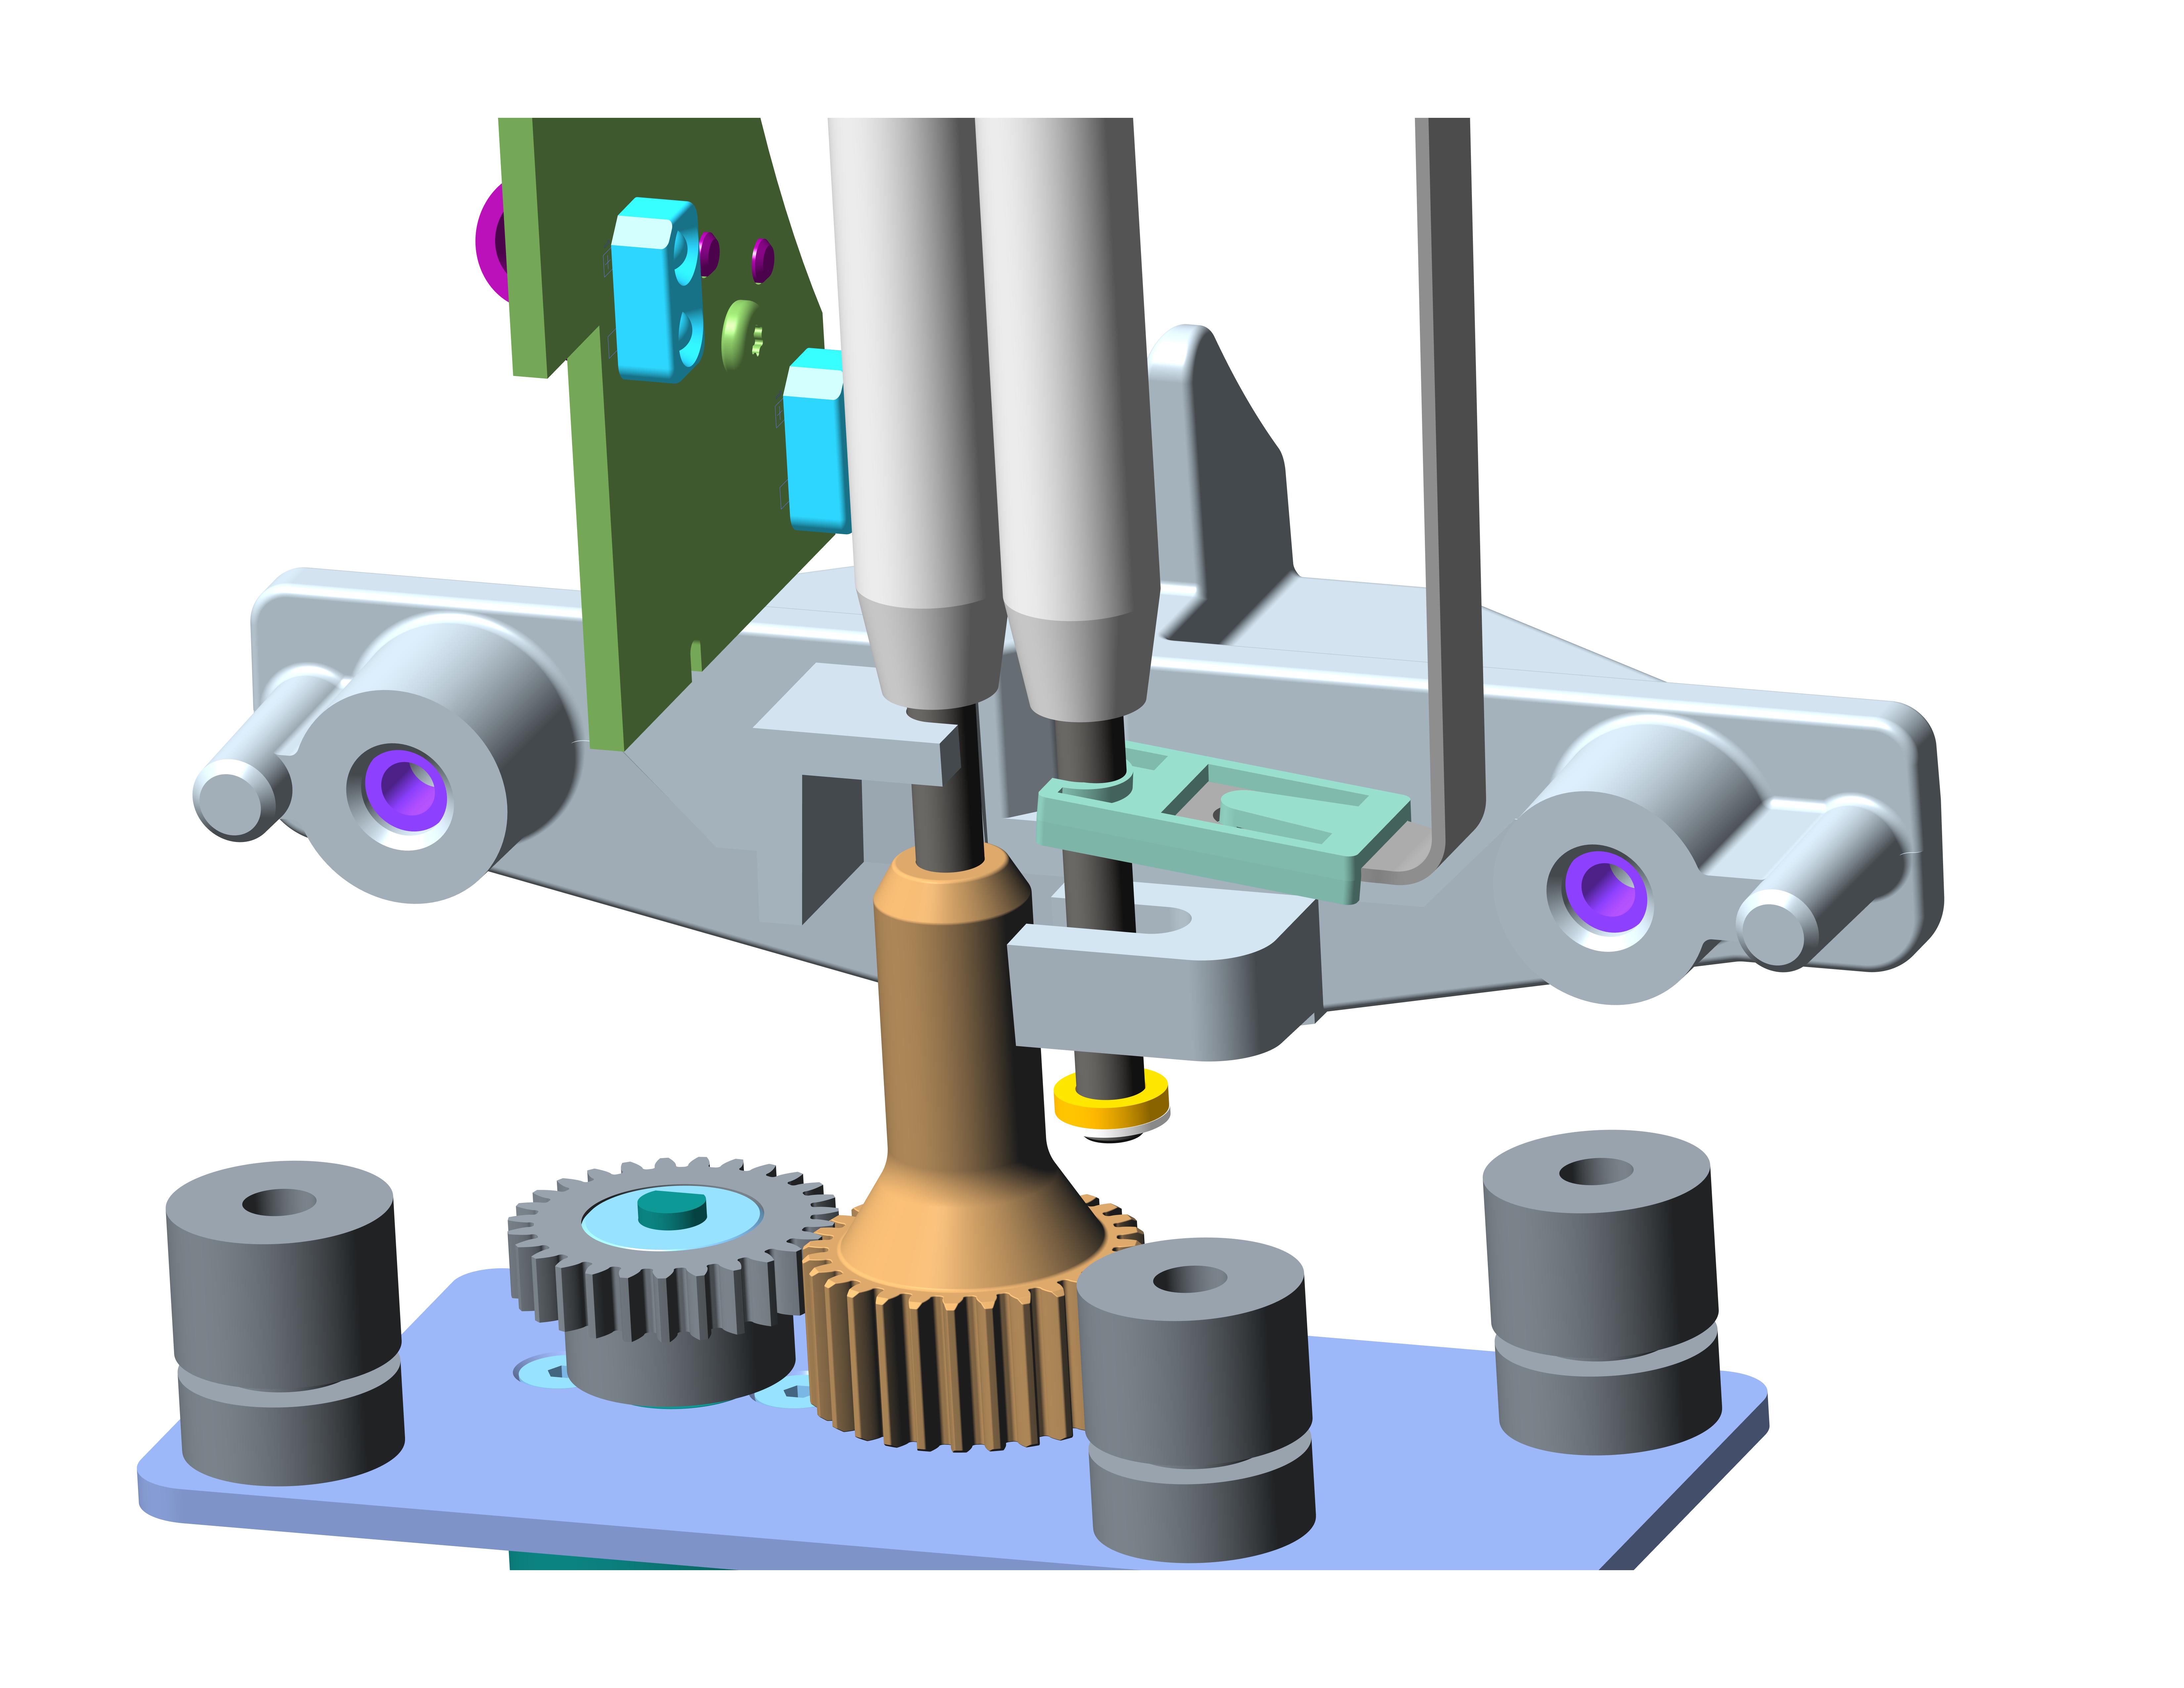
My corrective design work included solid motor-plate mounts, an extended-neck gear, alternative inner guides, and a bearing-block extension to support the roller shaft farther down. The team also considered stiffer shafts, different roller materials and surface treatments. Those alternatives addressed grip and stiffness together; a coating that felt grippier initially was not enough if its performance deteriorated with use.
By the end of May, my status report recorded that coated-roller testing had ended. The coating did not provide a significant improvement and tended to migrate onto the disc surface. New springs, disc guides and bearings had arrived for assembly and further tests. That was a decision about a tested alternative, not a declaration that the remaining mechanism changes were qualified.
The guide geometry had a second job: resisting double-disc grabs caused by discs clinging together. Nathan experimented with moving the guide closer to the disc. I questioned the remaining clearance, and the team assigned me to make prototype variants for testing. Spring load, guide clearance and shaft support had to be evaluated as an assembly.
Contaminated roller surfaces
Roller support study
Keep assembly from moving the disc path
The disc-retention cover could affect alignment without being visibly damaged. May service instructions for both vault models specified larger mounting holes and washers to avoid interference and distortion. They directed assembly staff to leave the roller brackets in place, align the cover without loading the outer screws, then tighten the center and perimeter fasteners in sequence. This turned a geometric concern into a repeatable assembly procedure.
A separate assembly investigation traced a poorly seated roller-assembly tab and excess grease to a specific DV700 through its sensor-board number. Sanmina returned the unit’s manufacturing history and reported that it had passed production tests. The supplier also said the assembly instructions did not specify how much grease to apply. That left the assembly-process question open despite the recorded test passes.
Sanmina sent a work-instruction sheet in April that specified grease application through pneumatic pressure and time. I proposed detailed photographs of each surface showing the intended amount, and asked for the needle-tip applicator used at the factory. John Lio supported the photographs and followed up with Sanmina; the supplier later promised to send an applicator. The record establishes the process clarification and those requests, but does not confirm delivery of the applicator or completion of a new photographic standard.
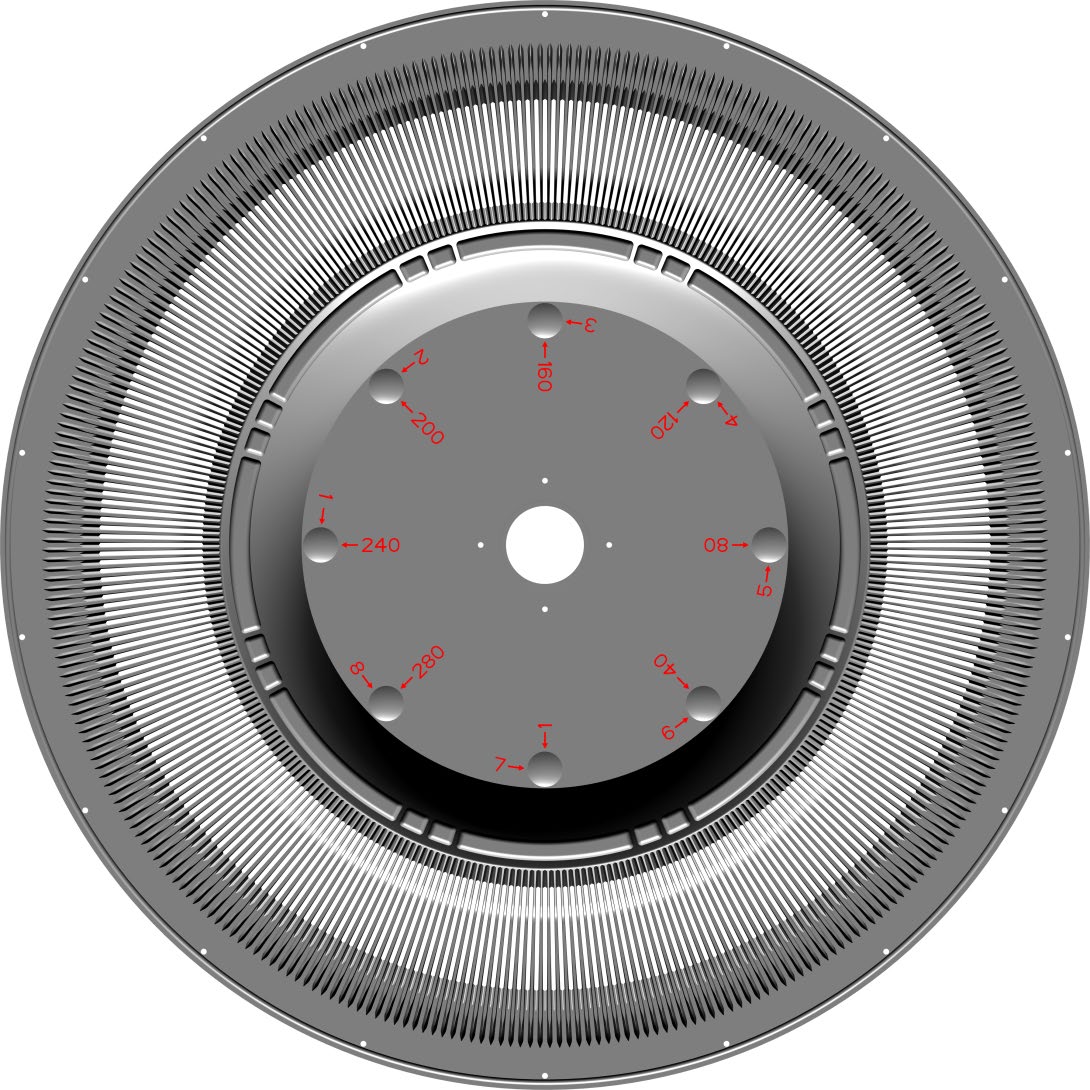
The carousel required its own inspection boundary. The April 10 procedure called for locating high points on a flat surface, measuring vertical deflection, and rejecting and quarantining parts above two millimeters. John Lio sent the updated criteria to Sanmina for immediate use. The team treated warpage as a possible contributor to failures, not as a proven explanation for every returned unit.
That inspection led to a written scrap instruction. On August 14, John identified me as the engineer responsible for the carousel part and its disposition. On August 19, I instructed Sanmina to scrap the failed parts. The supplier acknowledged the instruction the next day; the selected record does not confirm completion of the physical scrapping.
Carousel inspection reference
Carry the correction into production work
Packaging was another mechanical interface. In June, John and I discussed protecting the foam where the vault rack ears could cut into it during handling. I proposed a flexible, die-cut plastic liner that could conform without special forming, with the packaging supplier selecting material based on price and availability. The correspondence records an option under development, with alternatives that included added foam and shipping without the rack ears.
The spring and guide changes progressed in stages. In April, I loaded the guide and bearing files into a working revision, ordered spring prototypes, and proposed testing them before loading the spring definition. By July, I had loaded the spring file and said it could be released with the guide and bearing. My next status report recorded the files prepared for engineering-change release and spring tooling approved for purchase. Assembly-instruction updates and further evaluation remained on the work list.
What the work established
The DV700 service cases and shared mechanism work joined service evidence with mechanical definition. Together, they produced documented unit-level repairs and test dispositions, repeatable inspection and assembly guidance, corrective component revisions, and supplier decisions. Somboun Thavy and John Lio carried the service and manufacturing work; Nathan Forster, Richard Lane, Rob Wudrick and the wider hardware team contributed testing, investigation and release coordination alongside my mechanical work.
The account ends with those supported engineering results. The selected records do not establish a final DV700 fleet failure rate or a completed fleet-wide retrofit. They do show why reliable disc handling required attention to the whole transfer path: the disc surface, spring force, shaft support, guide, optical drive, cover, carousel and the procedure used to assemble and test them.