Cinema One
From Digidesign to Kaleidescape
I joined Kaleidescape in May 2008 after leaving Digidesign. The office shared a parking lot with the building where I had worked at EP Technologies in the late 1980s. I liked that connection.
Cinema One came later. Its development record begins in 2012, with system planning and industrial design, and continues through the 2013 product introduction and manufacturing support in 2014.
Development at a glance
- 2012: Architecture and prototypes, alongside lighting and decorated-film studies.
- Spring 2013: Coordinating the front interfaces, bonding the enclosure and building the units and assembly process.
- Summer-autumn 2013: Production introduction and continuing part refinement.
- 2014: Load checks, assembly and slot follow-through, then the finish and inspection standard.
Designing the complete mechanical product
2012: industrial design and mechanical architecture develop together.
Whipsaw developed the industrial design for Cinema One, a combination movie server and disc player. As Kaleidescape's sole mechanical engineer, I developed the mechanical layout, enclosure structure and mechanical BOM, and carried every item on that BOM through design, specification, testing, validation, part bring-up and production bring-up.
To reproduce Whipsaw's design language of a machined block of aluminum, I used plastic exterior parts around a sheet-metal chassis.
For a product of this size and production volume, a machined billet enclosure was a nonstarter. Cost, manufacturing complexity, grounding and surface temperature all mattered.
The broad silver body and curved white front gave the product a quiet exterior. Behind that front, I had to accommodate the disc opening, buttons, illuminated graphics and infrared receiver, then bring them together with the optical drive, hard drive, fan, electronics and chassis. Each visible interface depended on geometry elsewhere in the assembly.
The finished enclosure
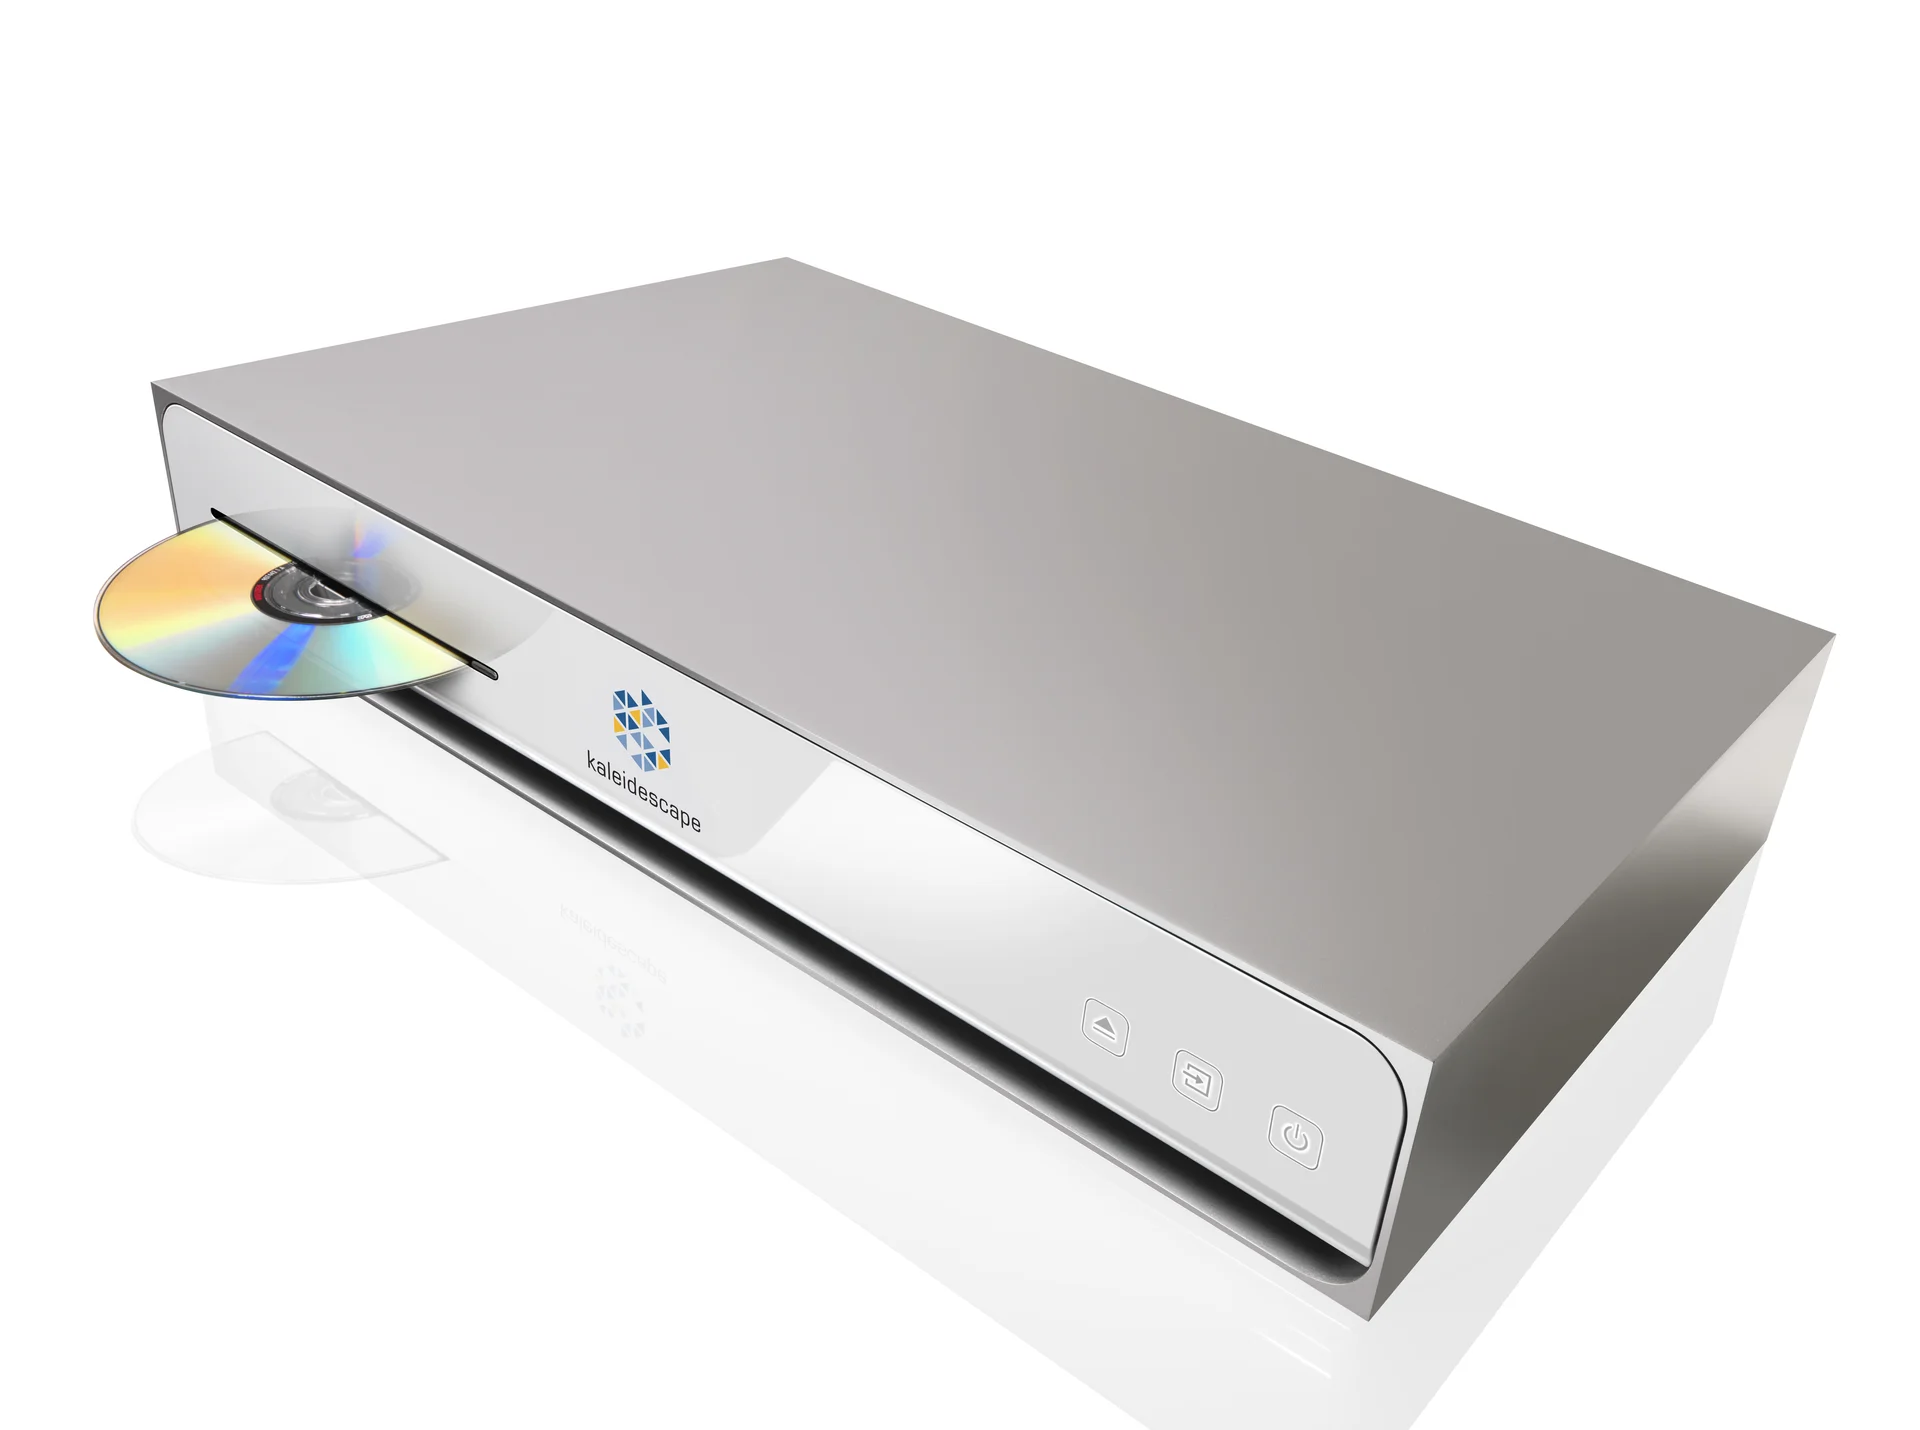
The industrial design and mechanical layout developed together. Whipsaw's May 2012 concepts explored the exterior alongside component placement and cooling. Their finalist update revised dimensions to fit a new mechanical layout, and the July concepts compared several ways to construct the enclosure. My responsibility was to resolve that exterior into parts, interfaces and an assembly that could be manufactured.
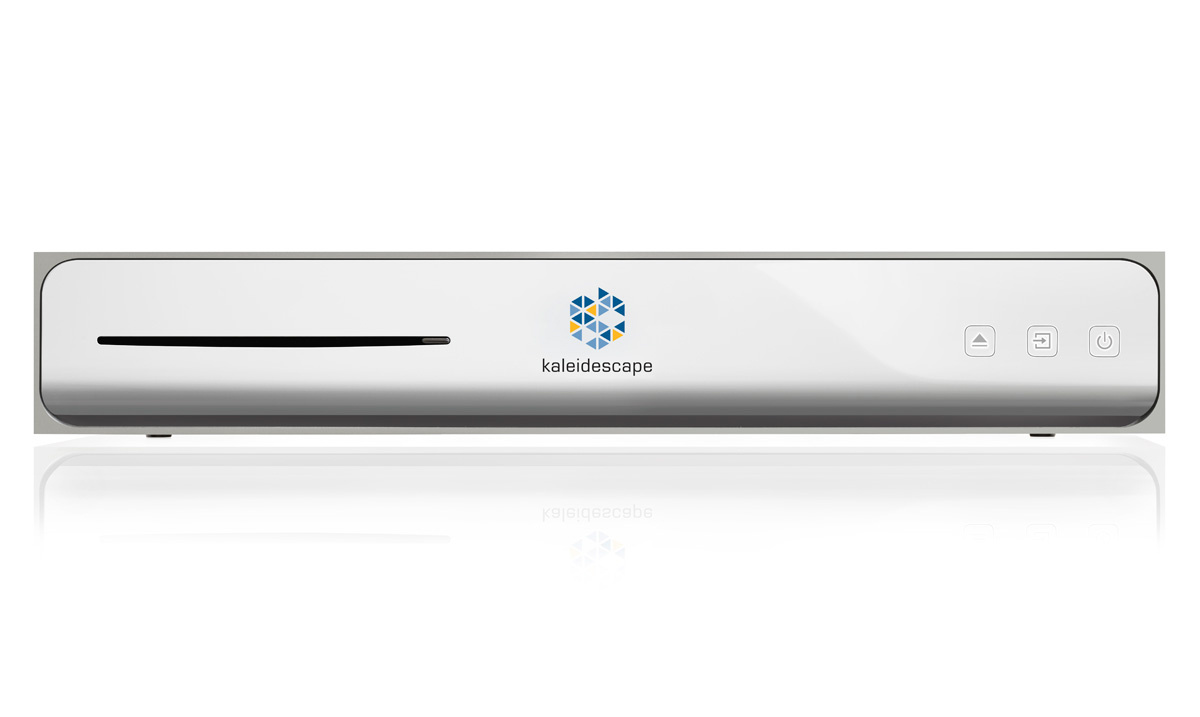
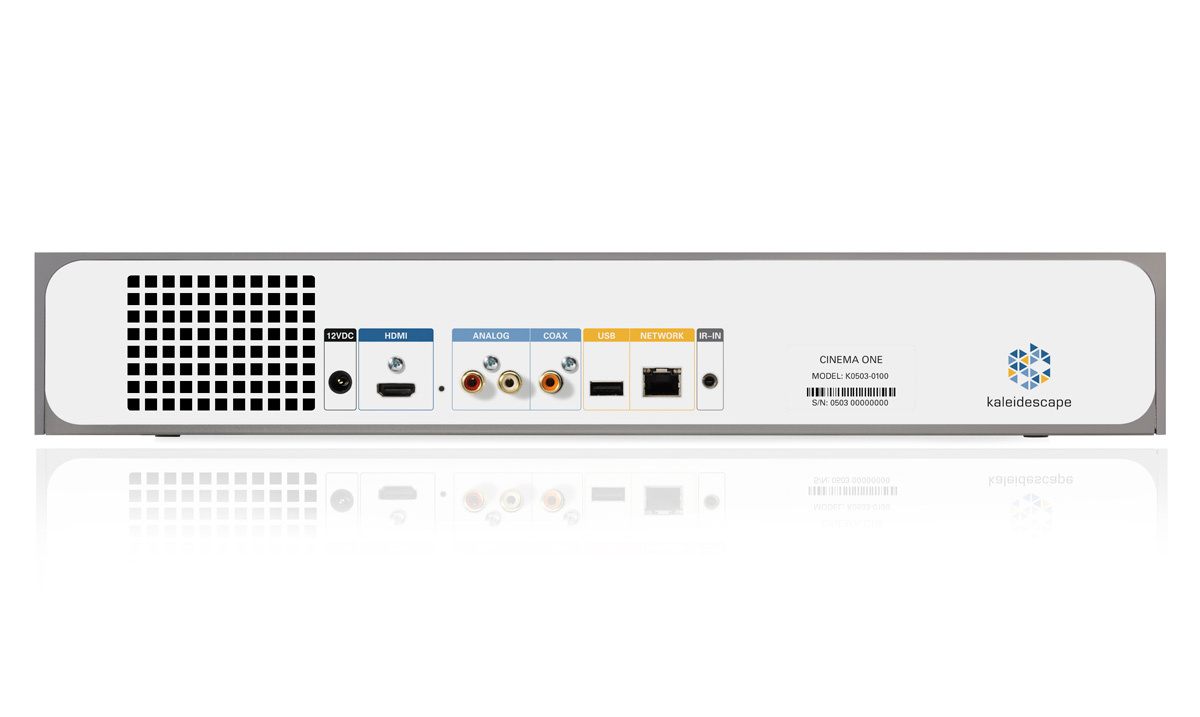
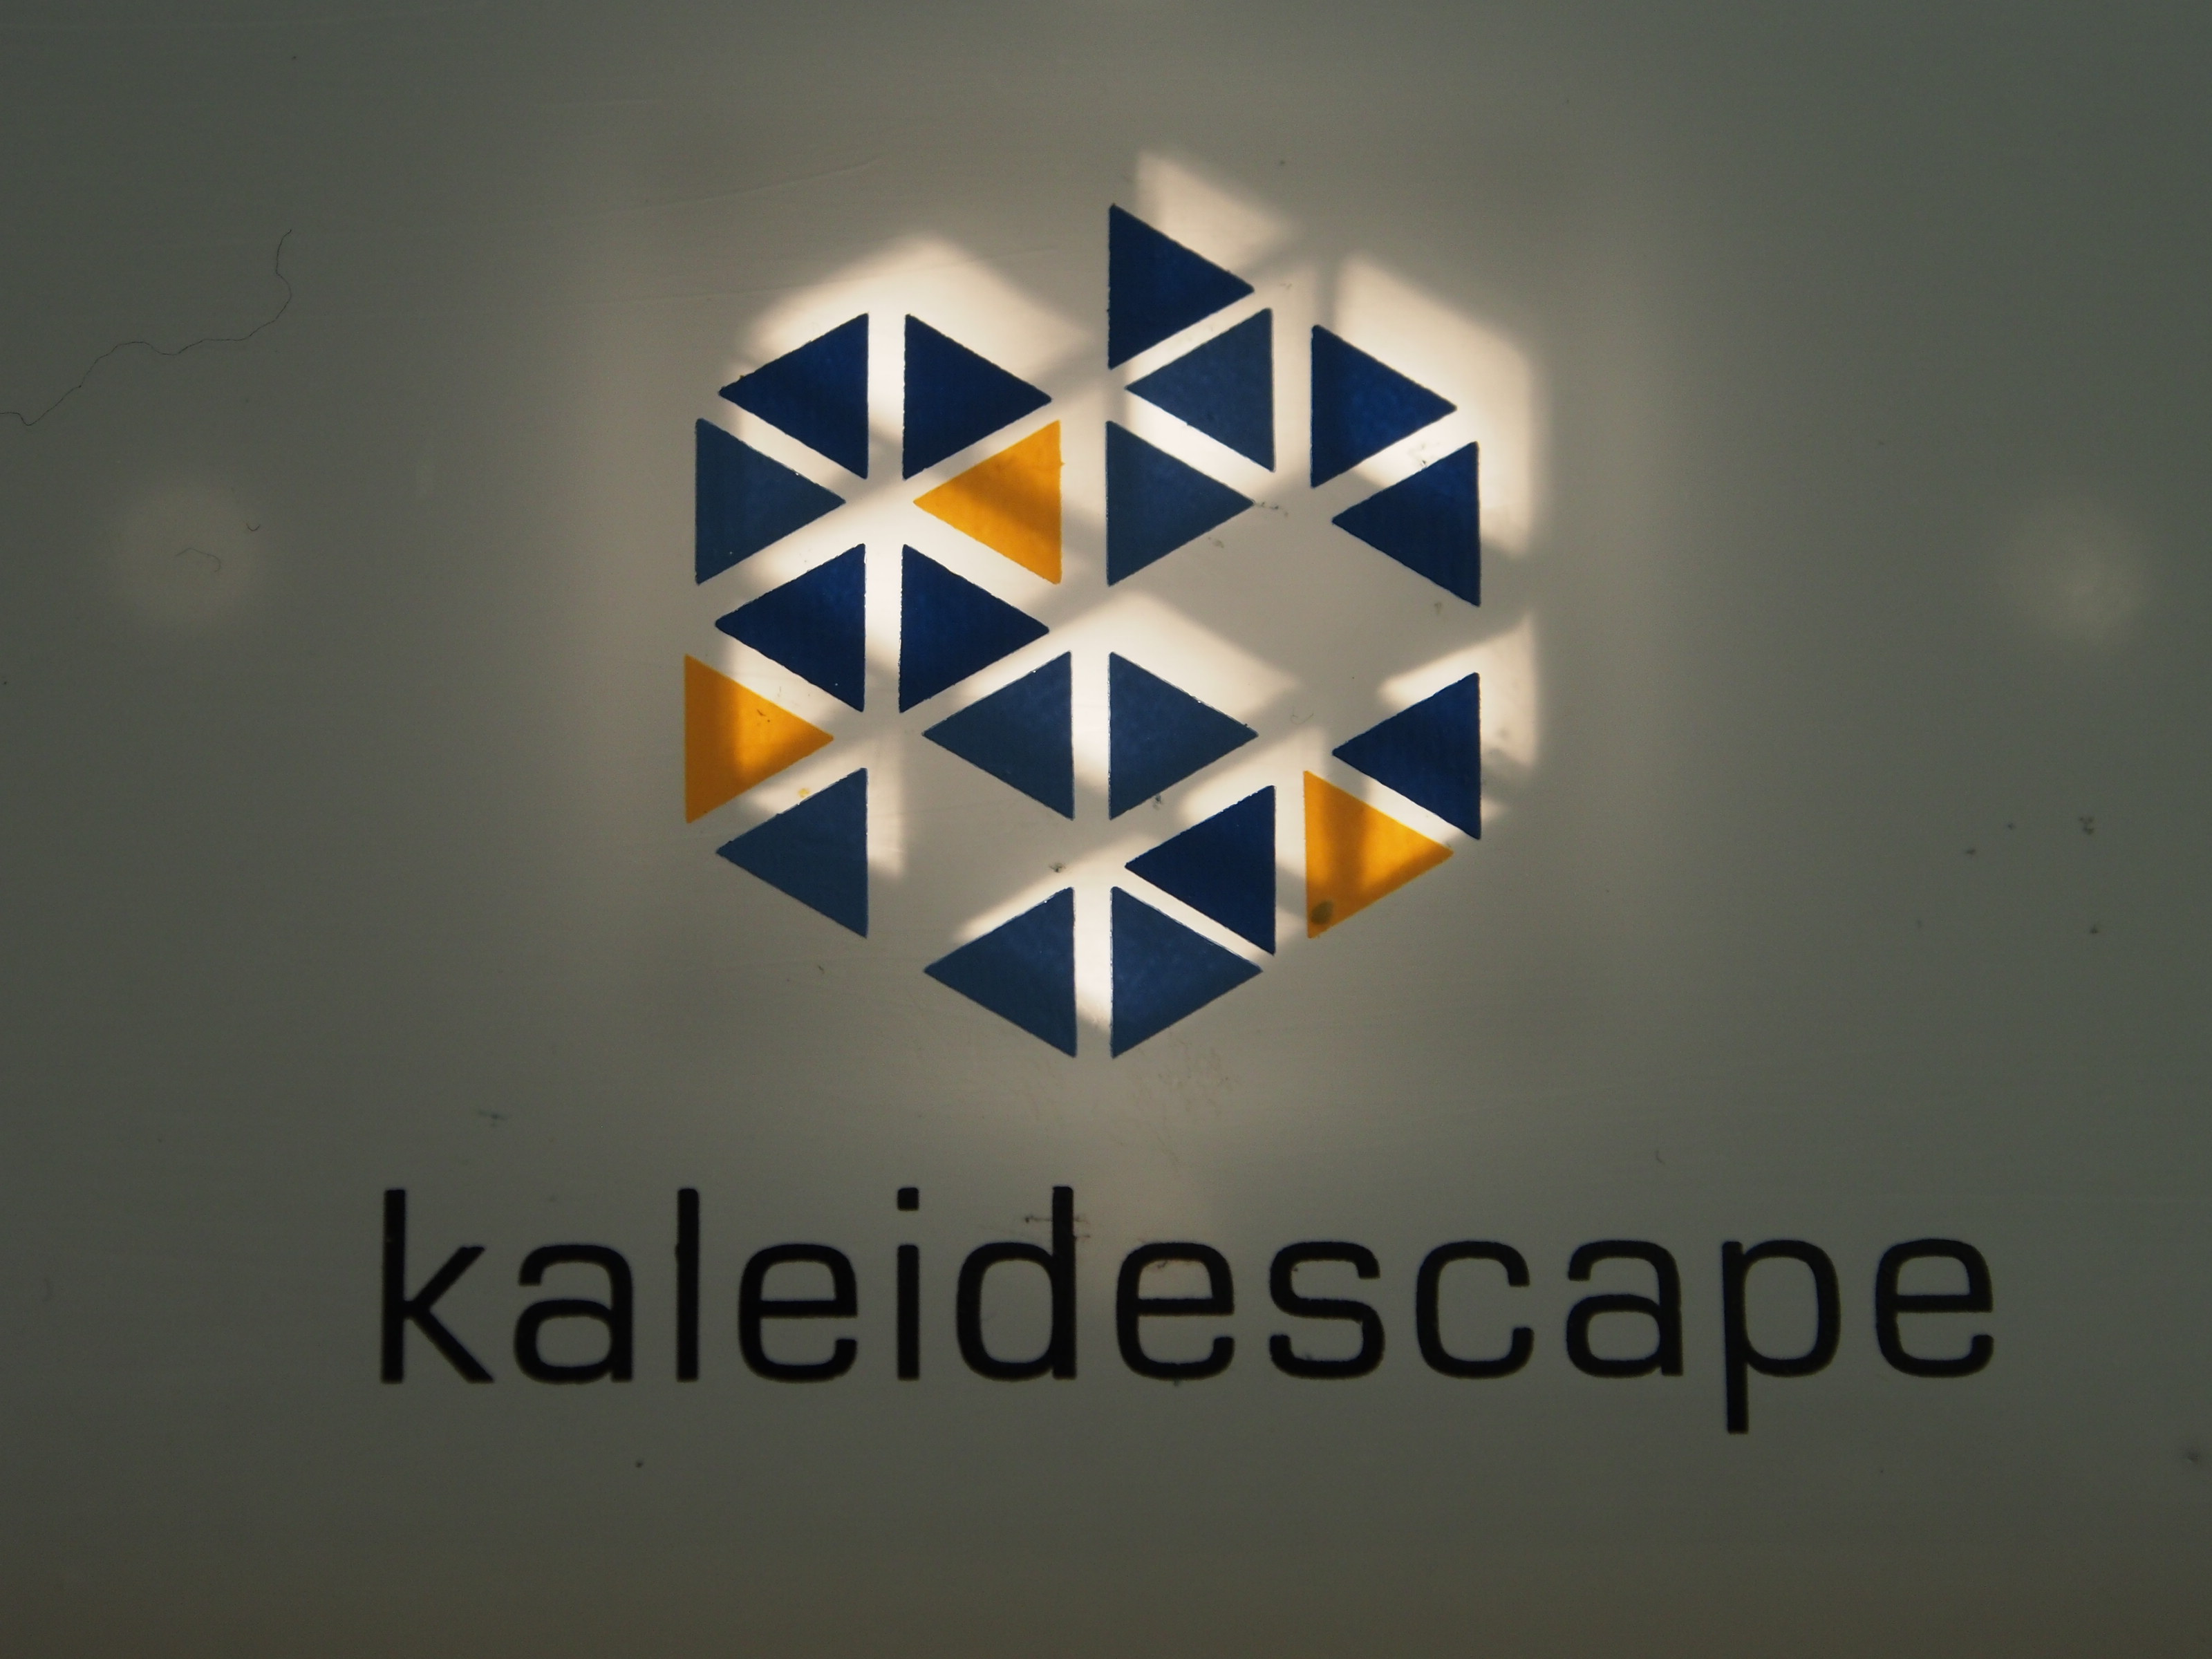
The same idea carried around to the back. The rear label used the same outline as the front bezel, so the surrounding plastic continued the illusion of an extruded aluminum body.
Carrying the outline around the enclosure
The front bezel and rear label repeat the same outline.
Finding room for the parts
2012: packaging and prototypes, alongside the exterior and lighting work.
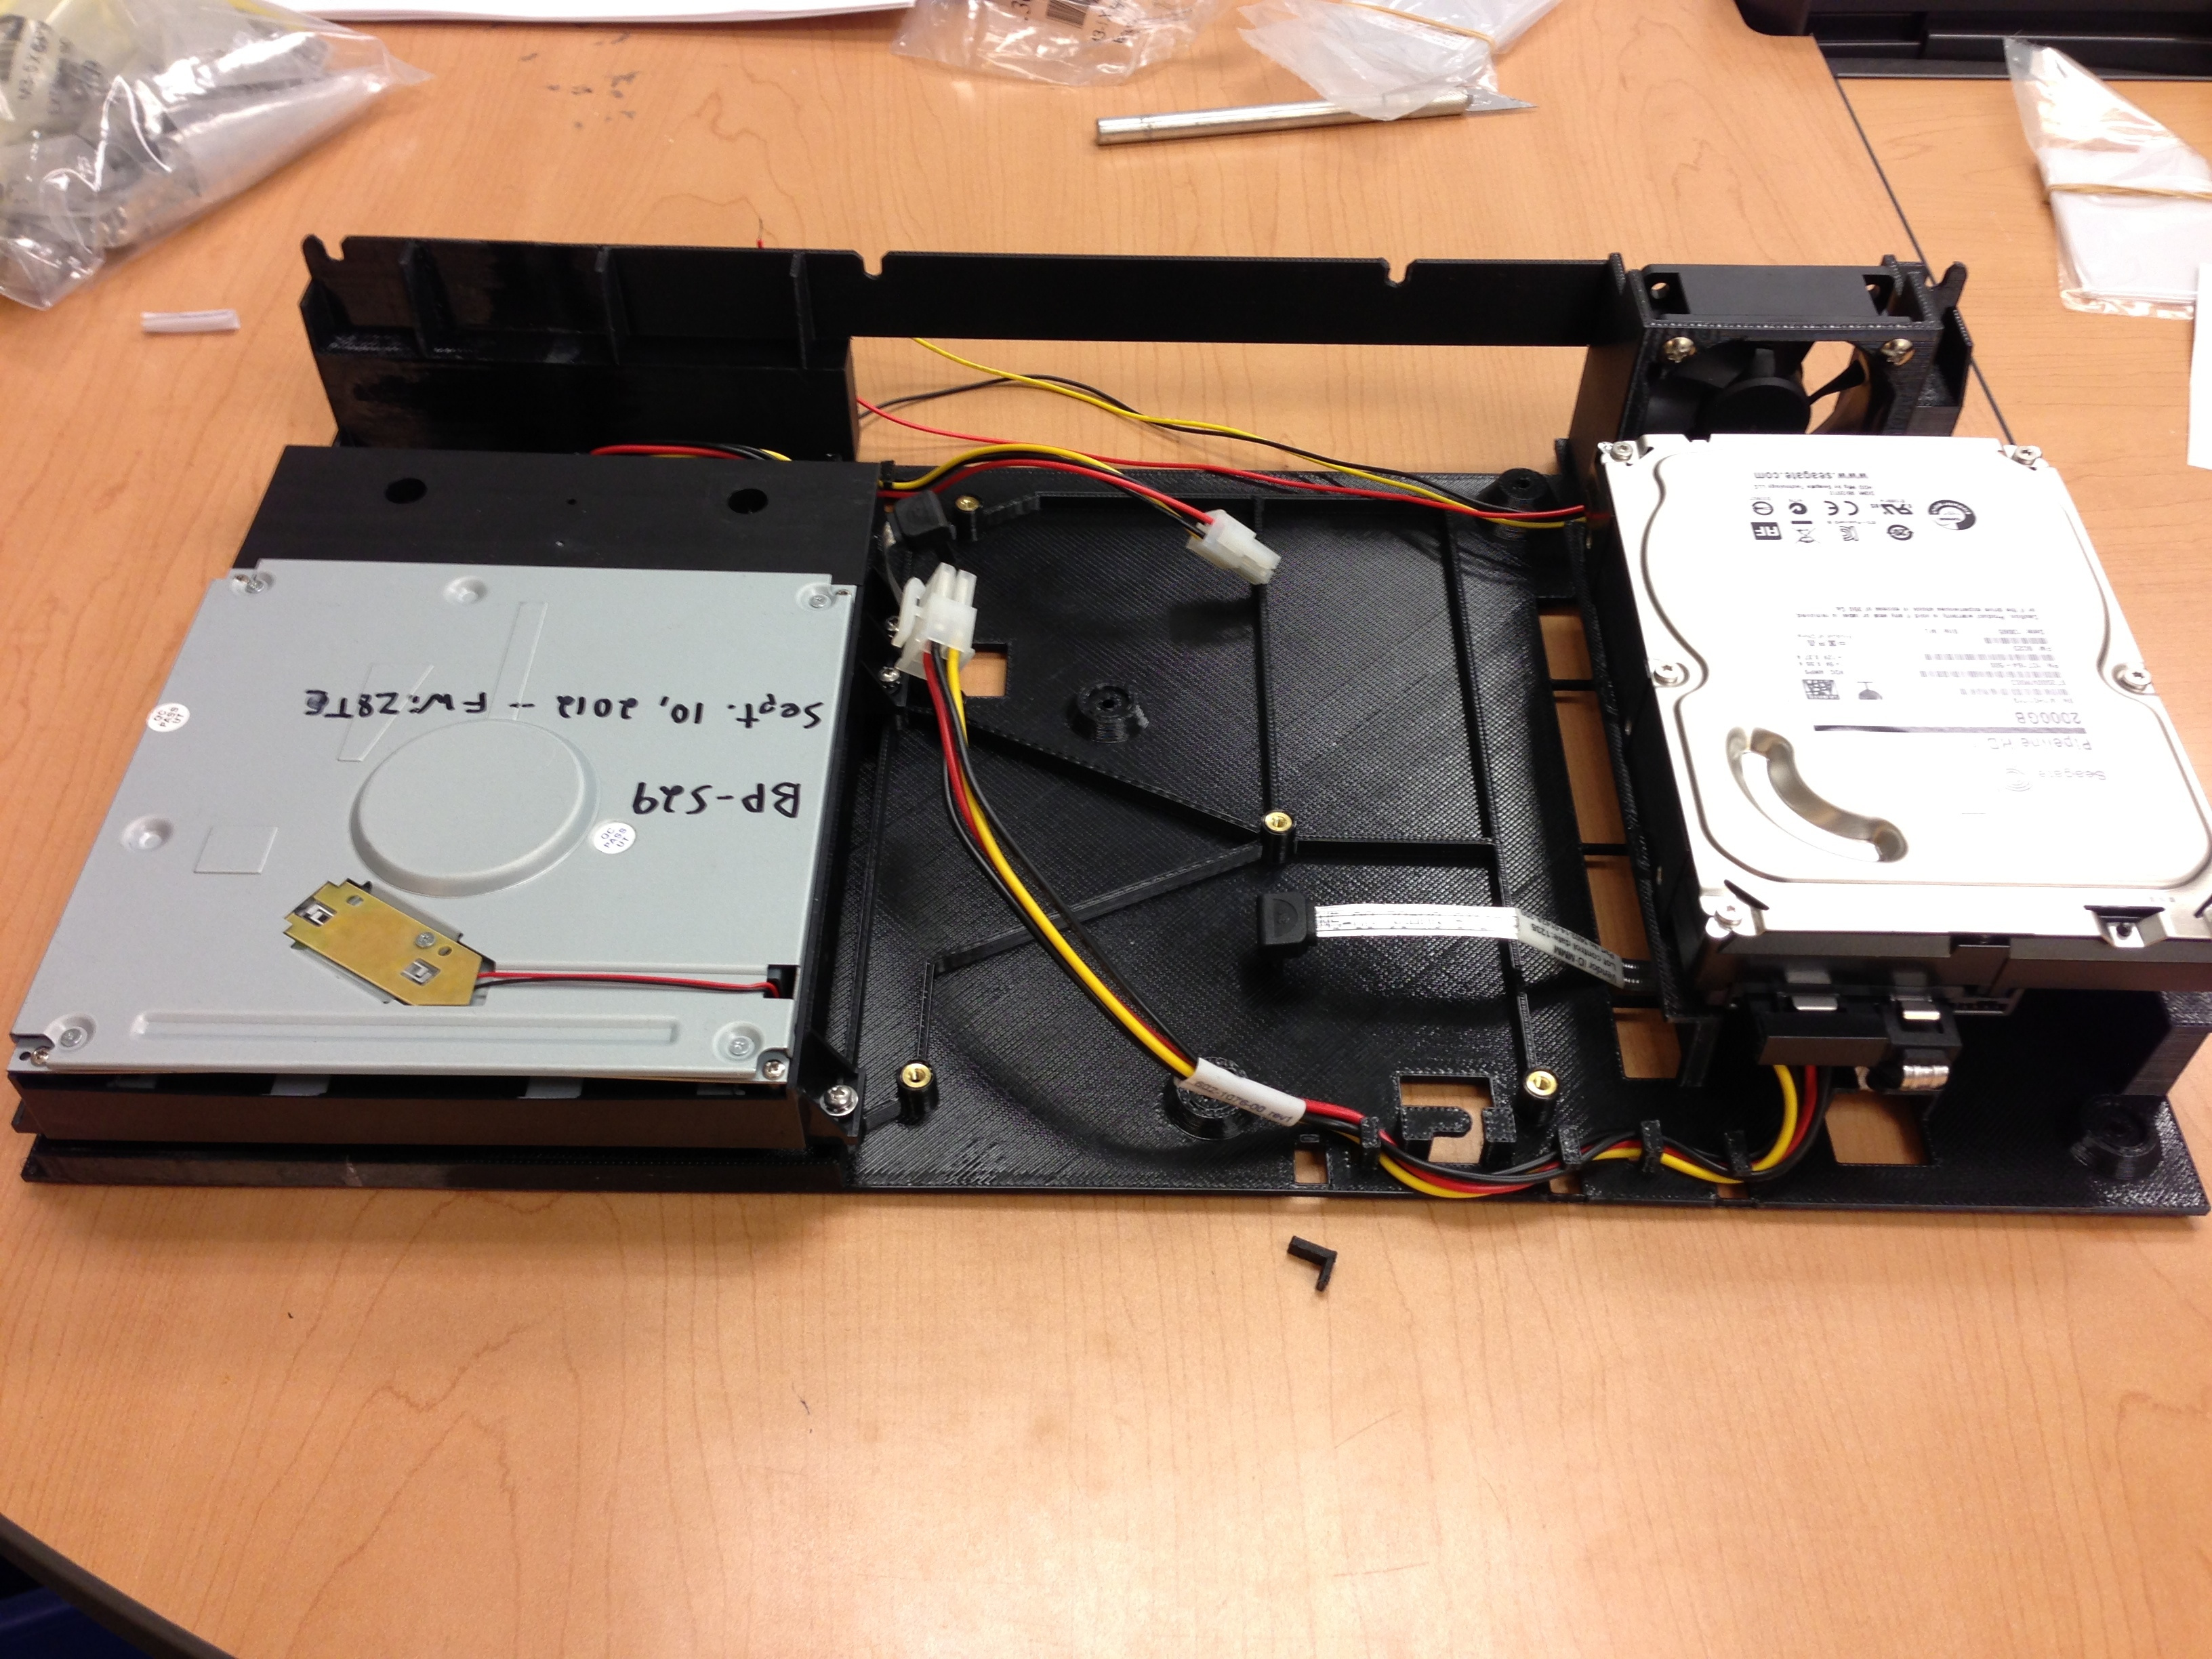
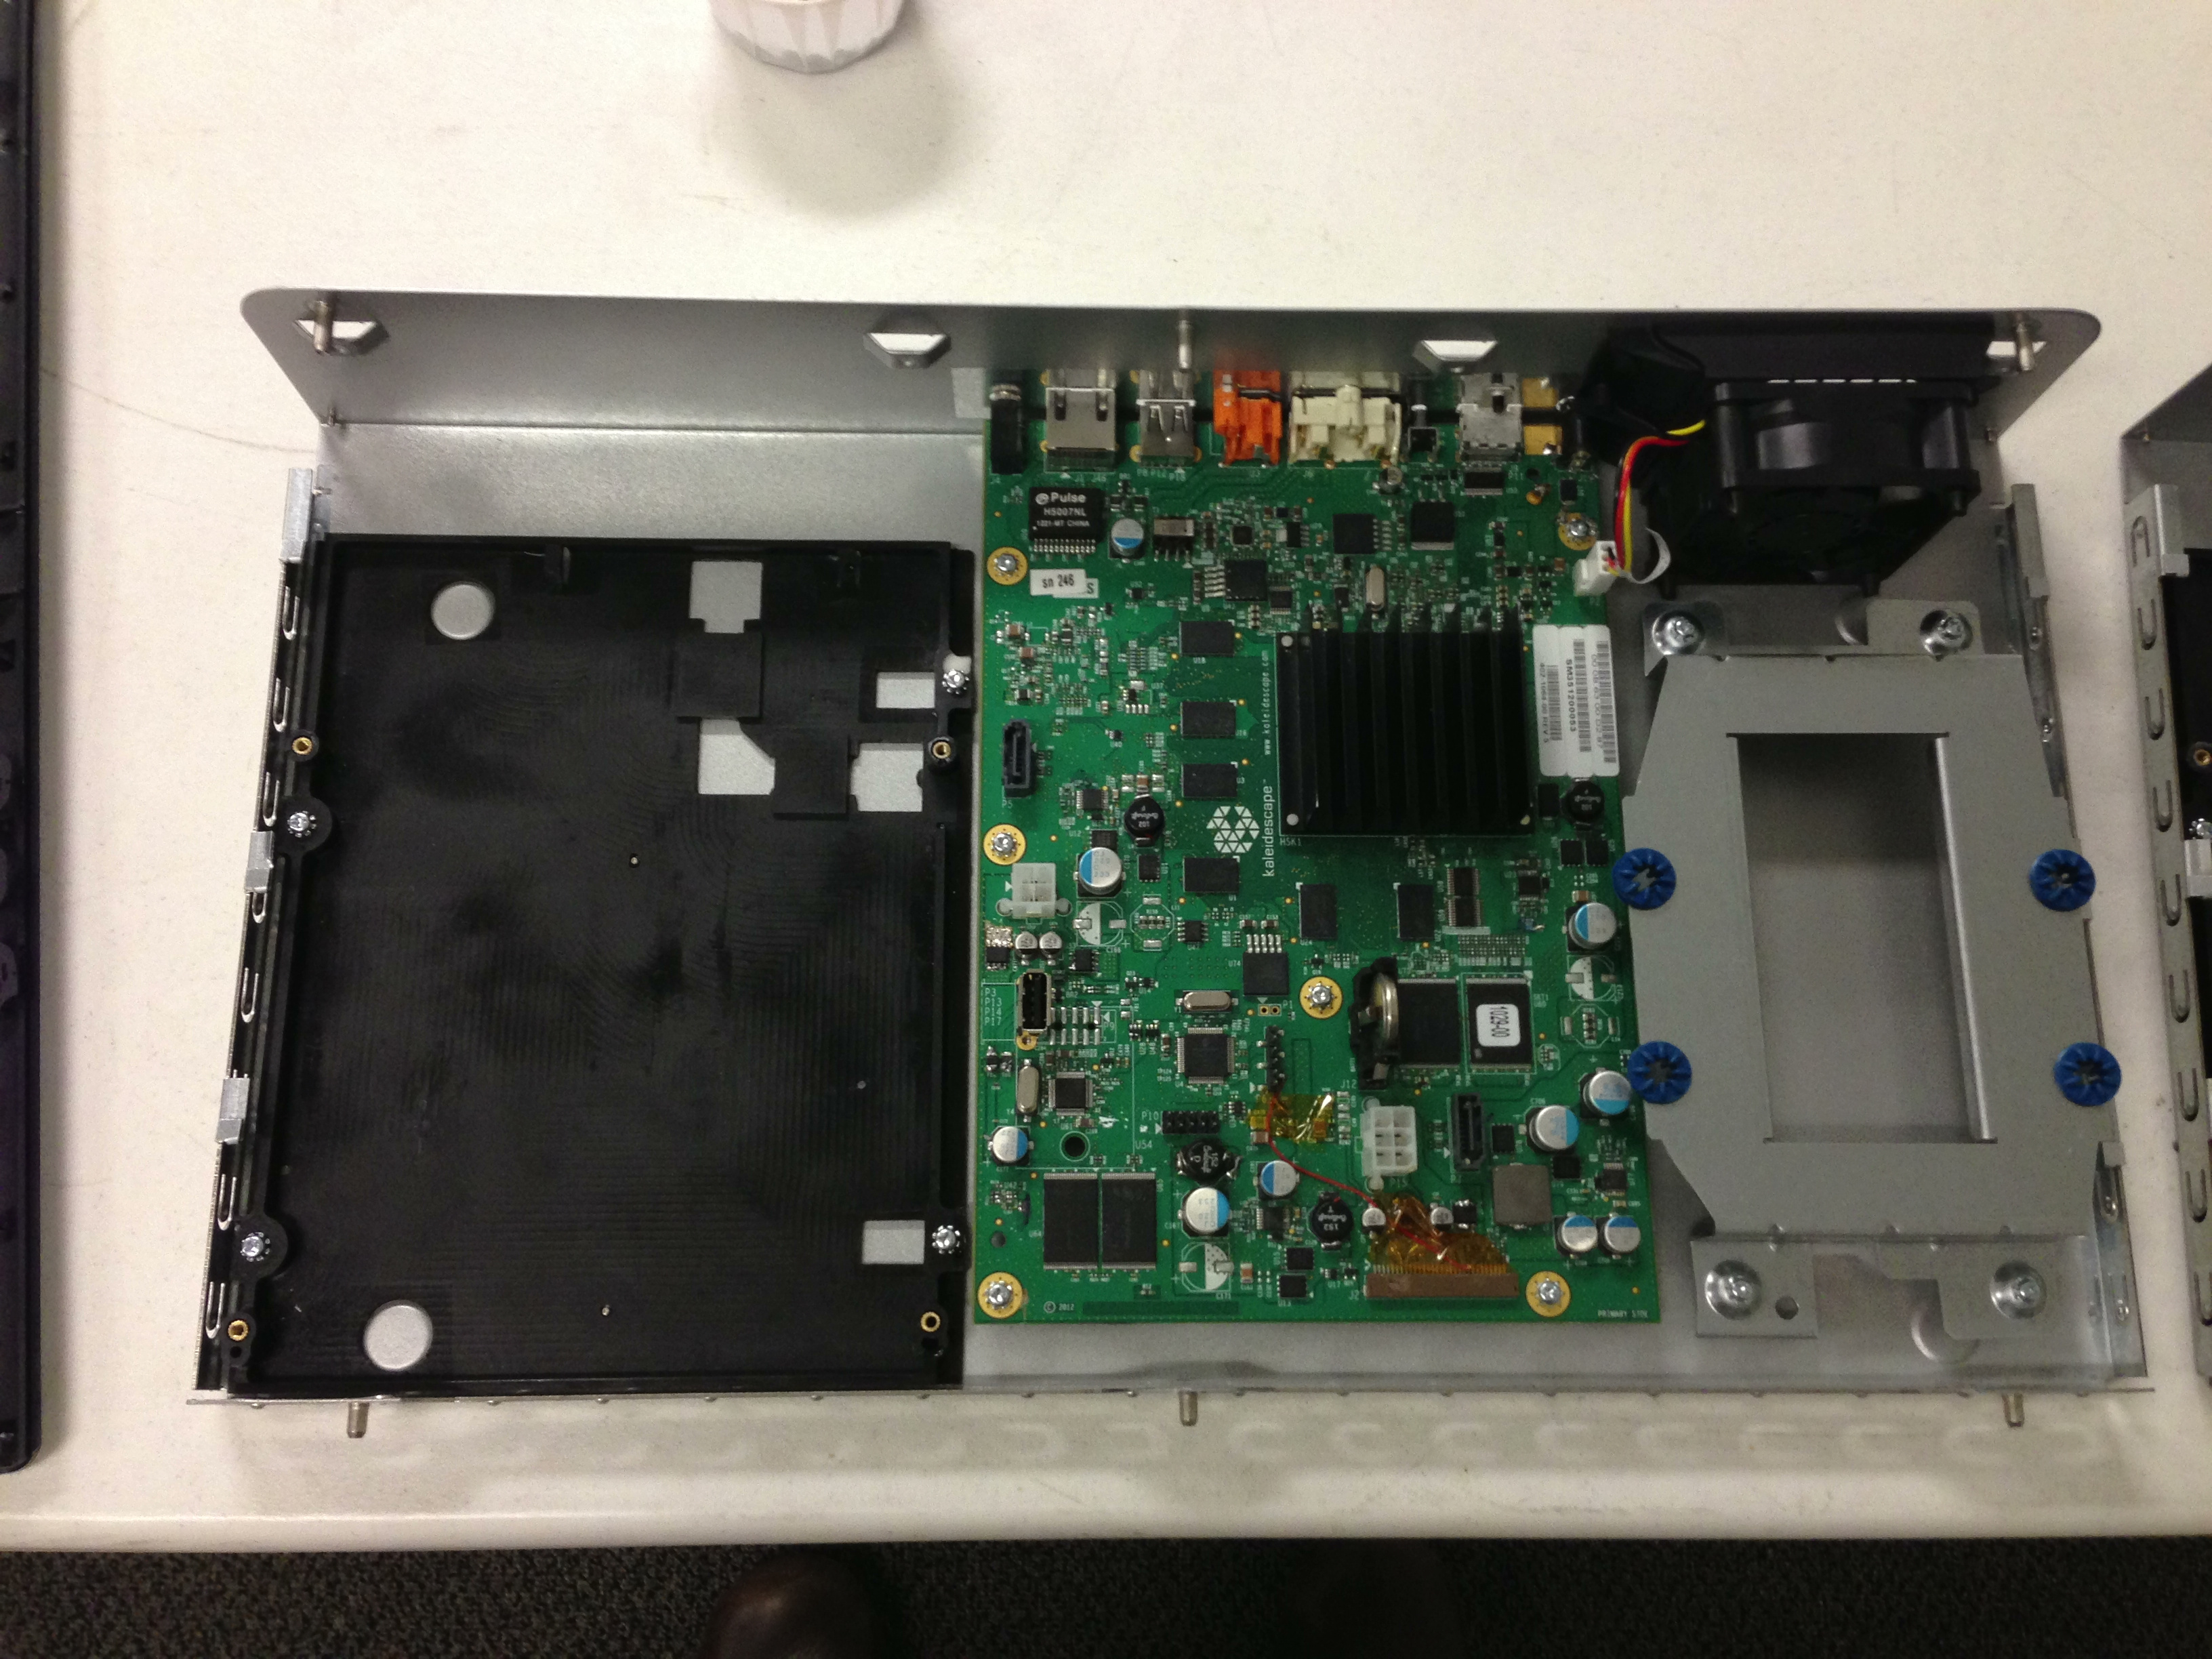
The early layout called for a single fan and an external power supply. Keeping the power supply outside was intended to ease service, cooling and enclosure packaging. The preferred arrangement put the optical drive on the user's left, the mainboard in the center and the hard drive on the right, with the exhaust fan behind it. This brought power distribution, mounting and airflow into the same layout decision. Putting the optical drive in the center would have complicated the mounting because the board could not shrink enough.
Prototype planning had to account for the different processes within the assembly. The October 2012 comparison listed plastic shells, frames, button components and the lens alongside sheet-metal and die-cut or printed parts. Some plastic quotes included paint but excluded graphics; others were for unfinished parts. A representative prototype needed more than the right geometry. Surface finish and graphics had to be considered separately when comparing the options.
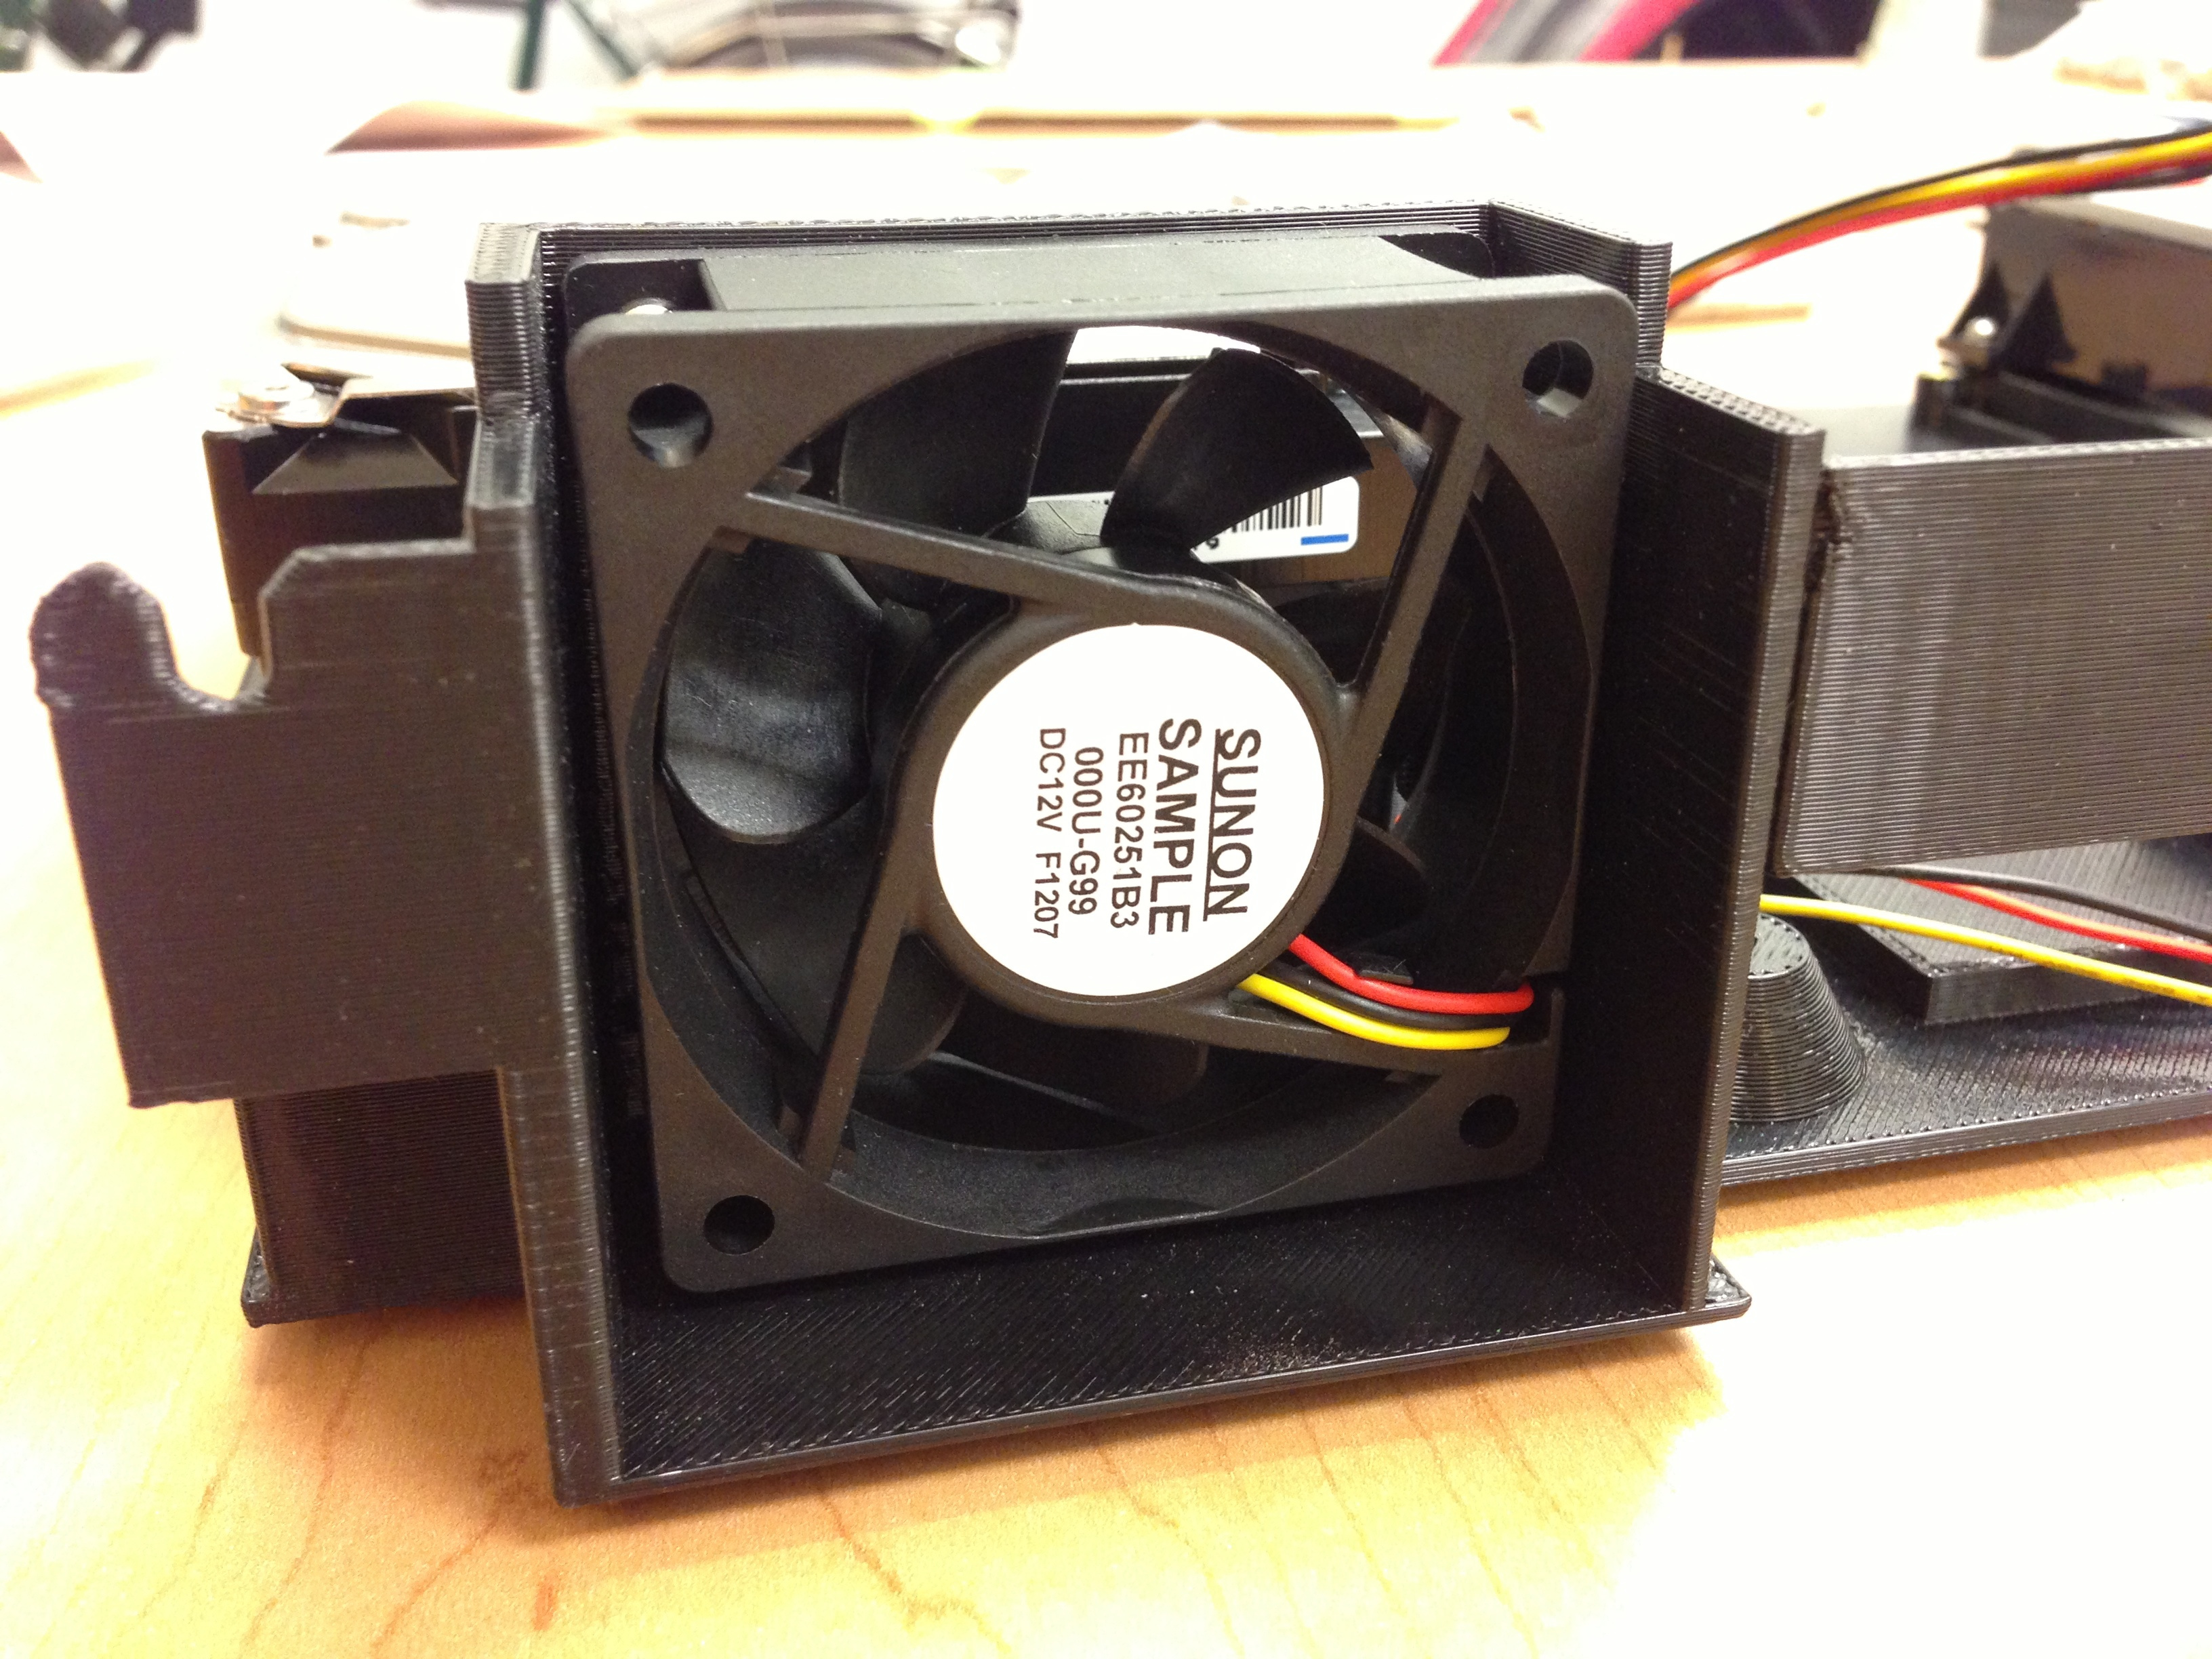
Early prototypes used a 3D-printed plastic subchassis module. The photographs show the drives and fan fitted into that structure, with the central board area still open.
An early printed subchassis
November 2012 prototype photographs.
Building the dead-front bezel
June 2012 into early 2013: lighting studies, decorated films and molded samples.
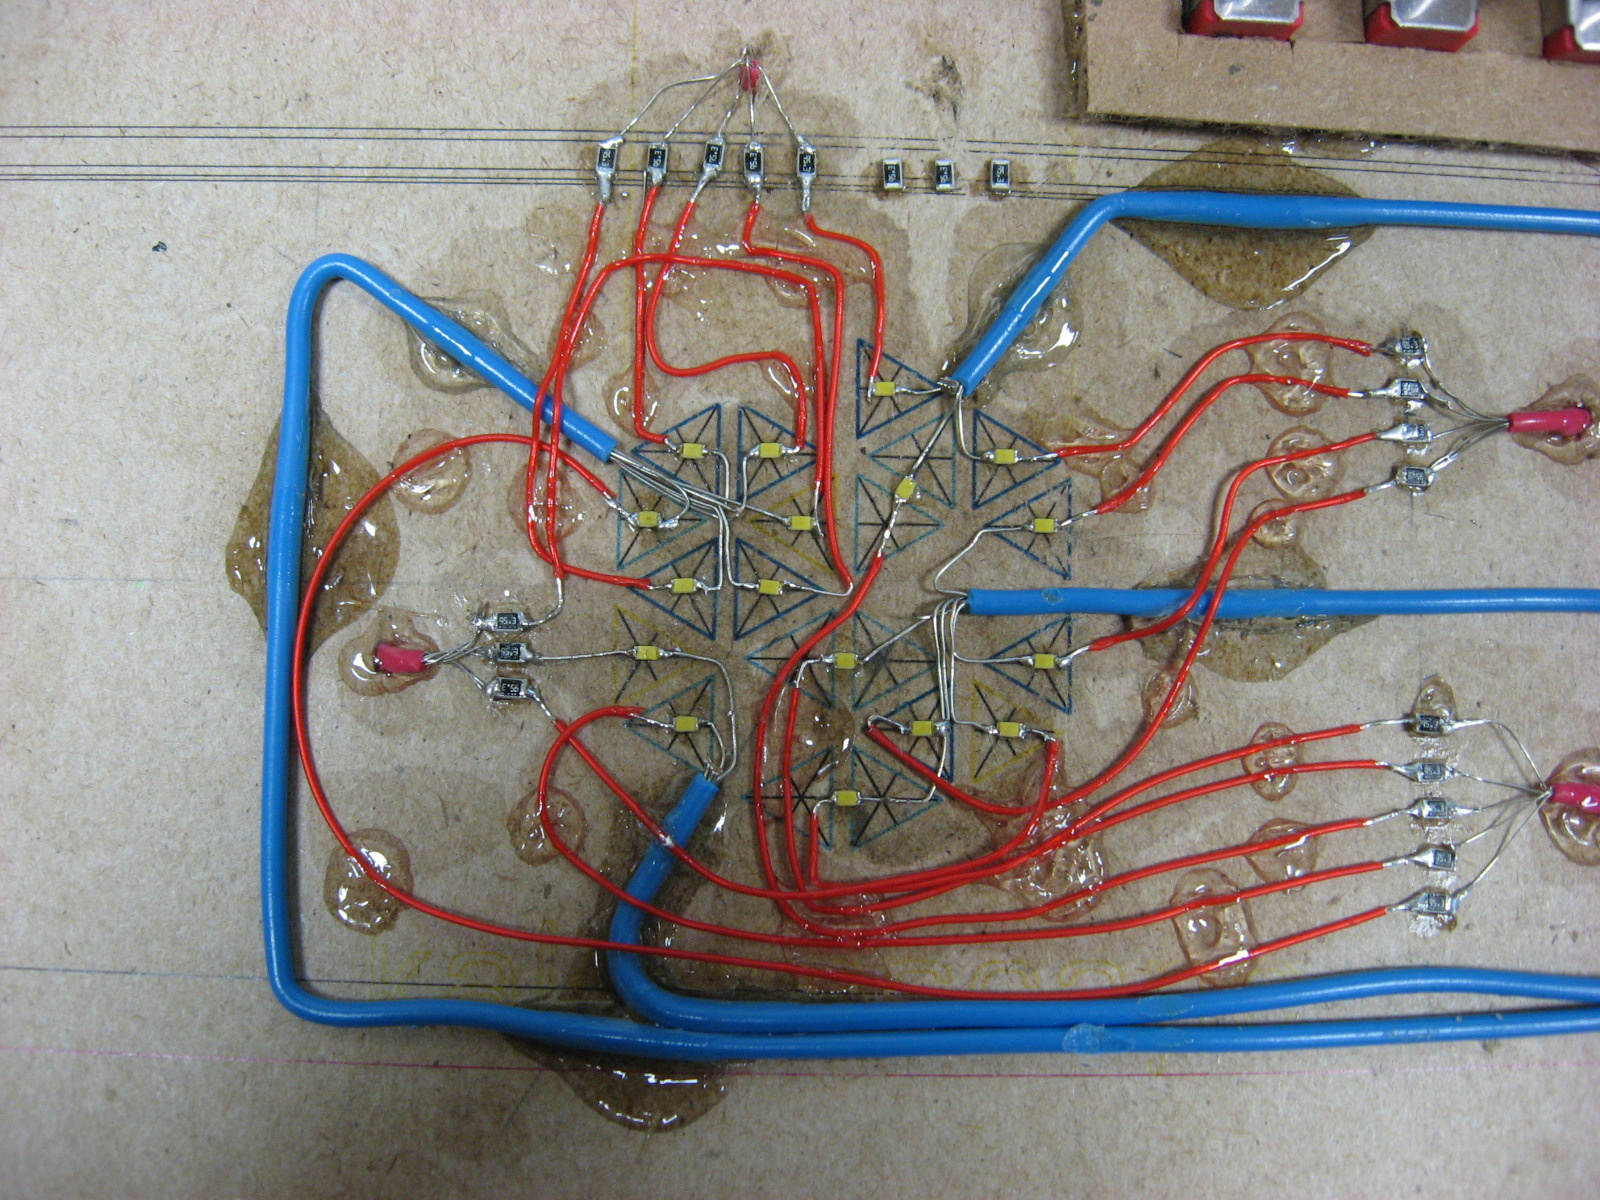
The dead front was powerful to me at the time: a white face that concealed its indicators until they were illuminated. The jewel added another possibility. I could address its facets individually and explore how it might animate. That combination felt cinematic to me, and it drove my early experiments with individually wired LEDs, their timing and intensity, and their distance behind the plastic.
Making that effect work in a production part meant coordinating molded plastic, four or more printing passes, print registration, mechanical tolerance loops and light isolation. I carried that work through supplier qualification, part and process development, and production ramp. I made that combination work in the manufactured bezel.
Animating the jewel was an early exploration, partly for the visual effect and potentially to indicate operating states. Keeping light from bleeding between the facets became one of the biggest challenges.
Testing the jewel facet by facet
An early study of individually addressable facets and LED spacing behind the plastic. Photographed June 29, 2012.
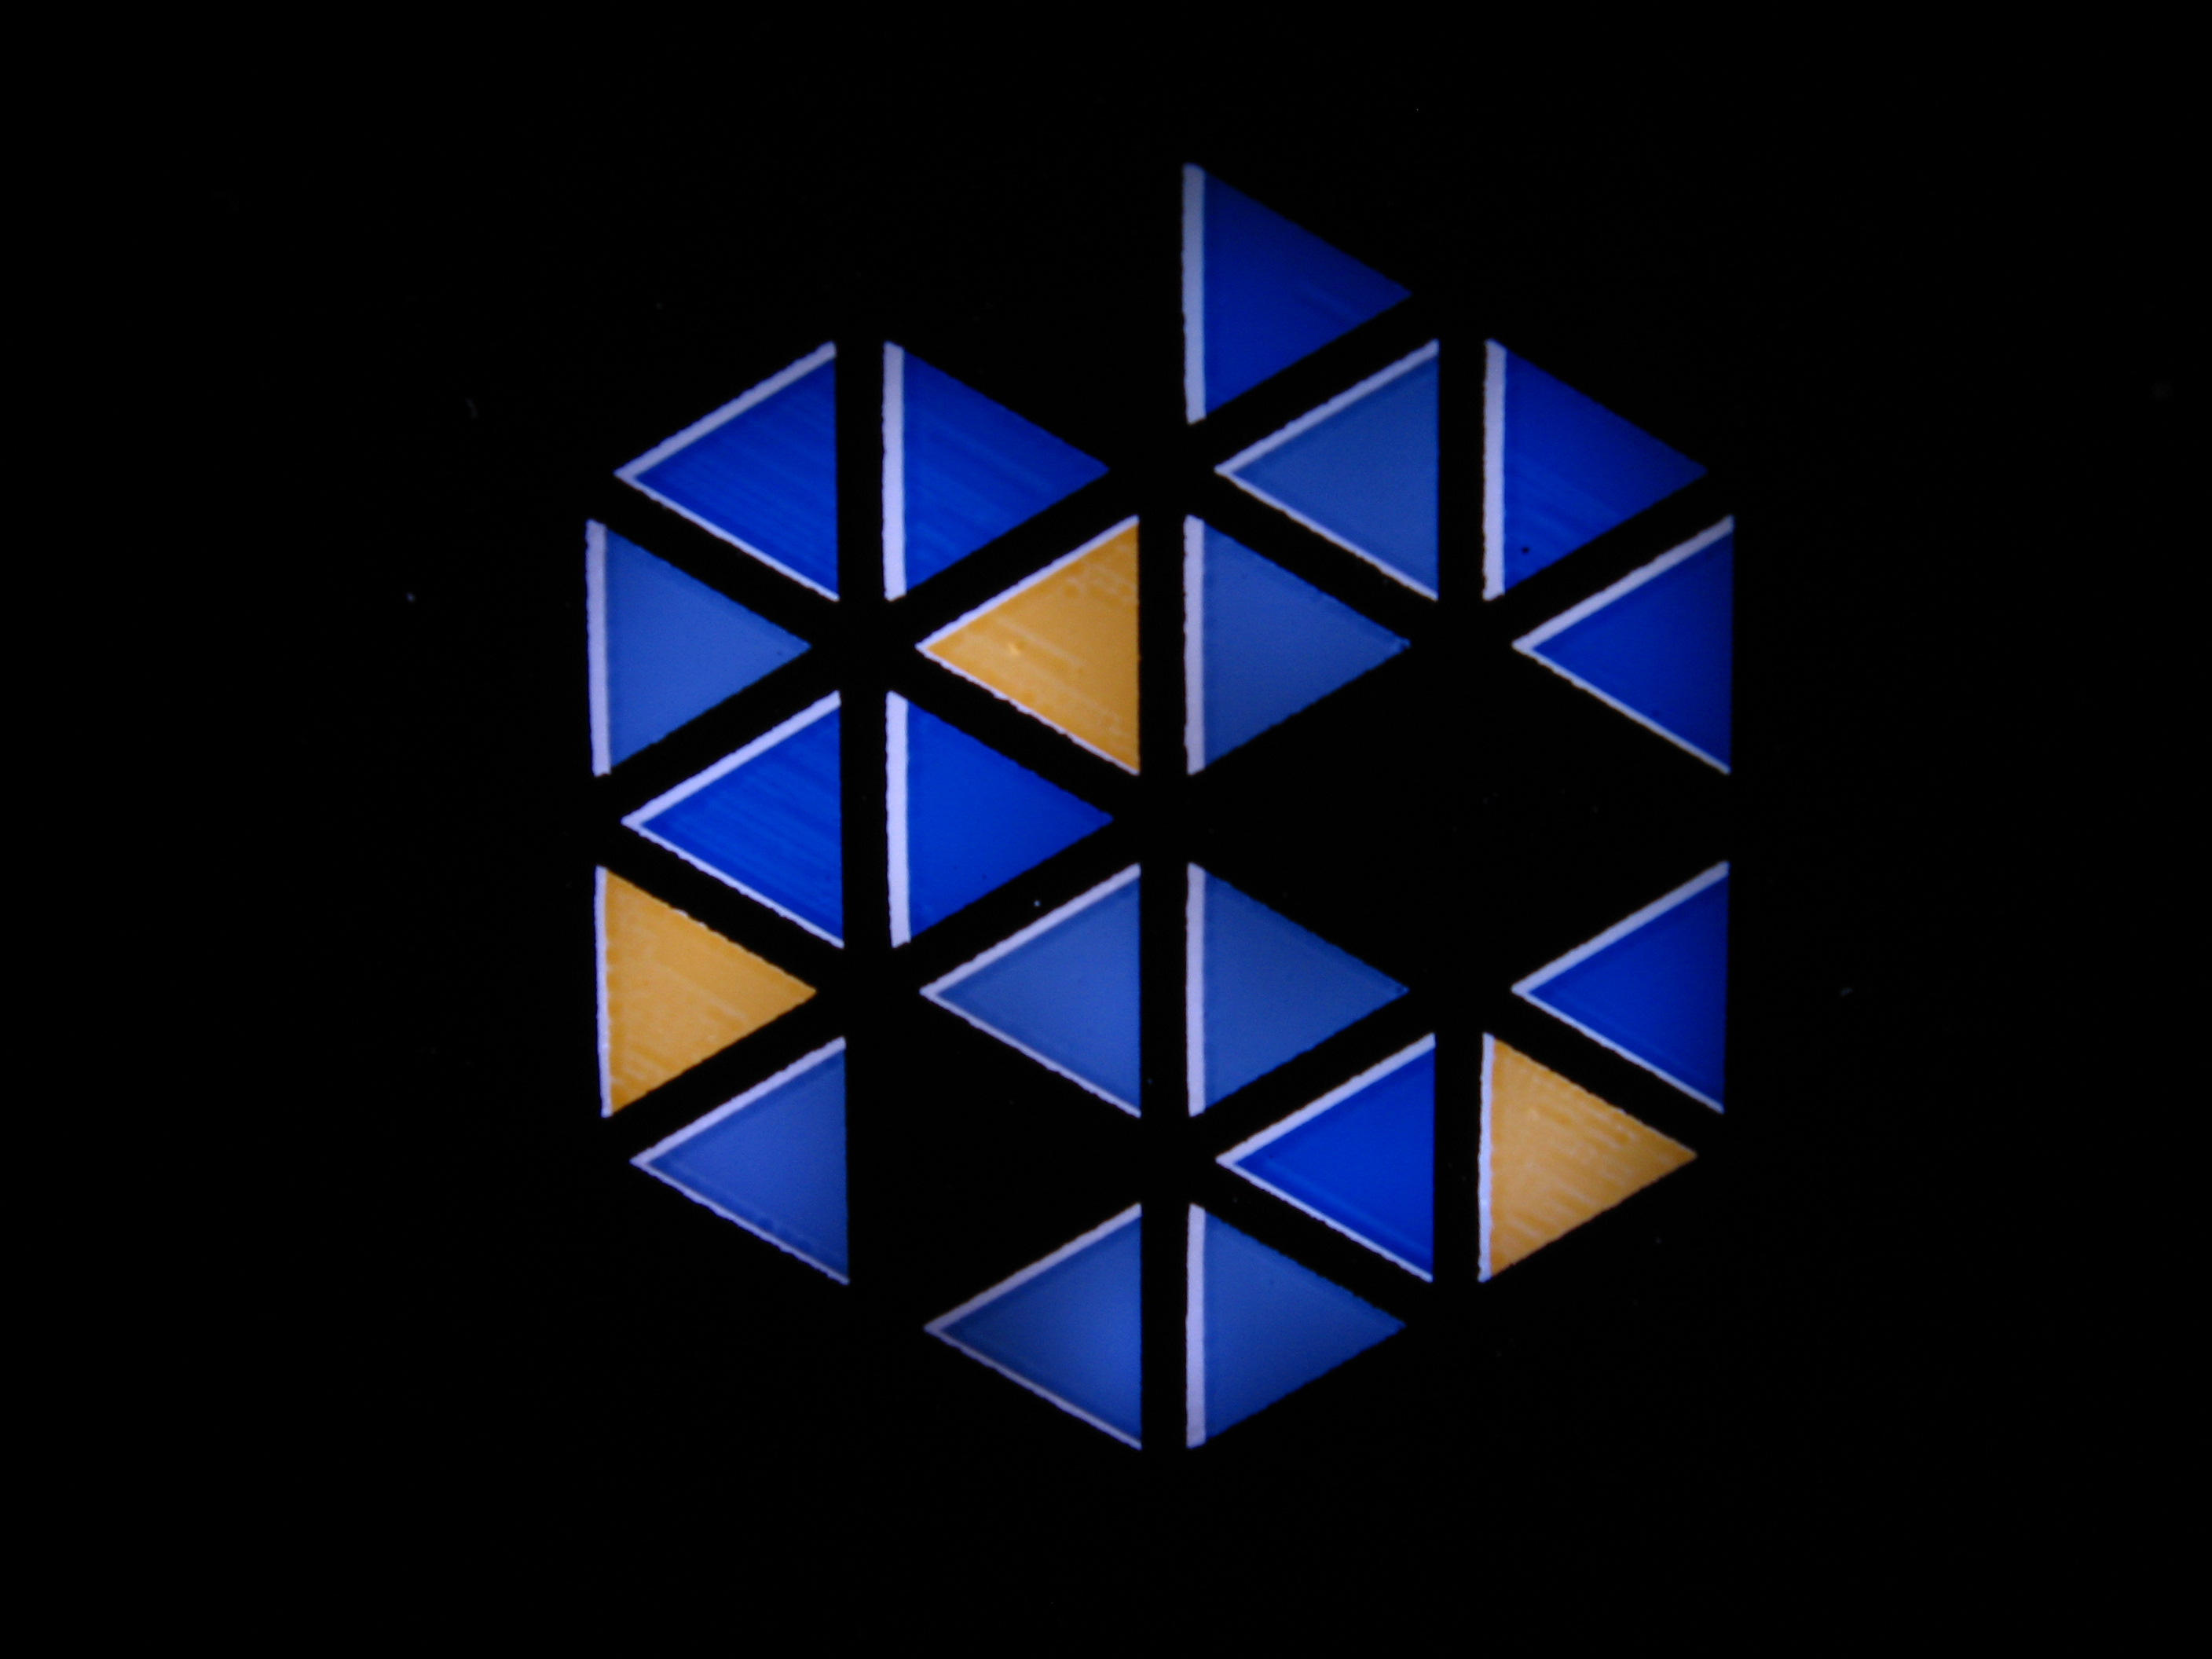
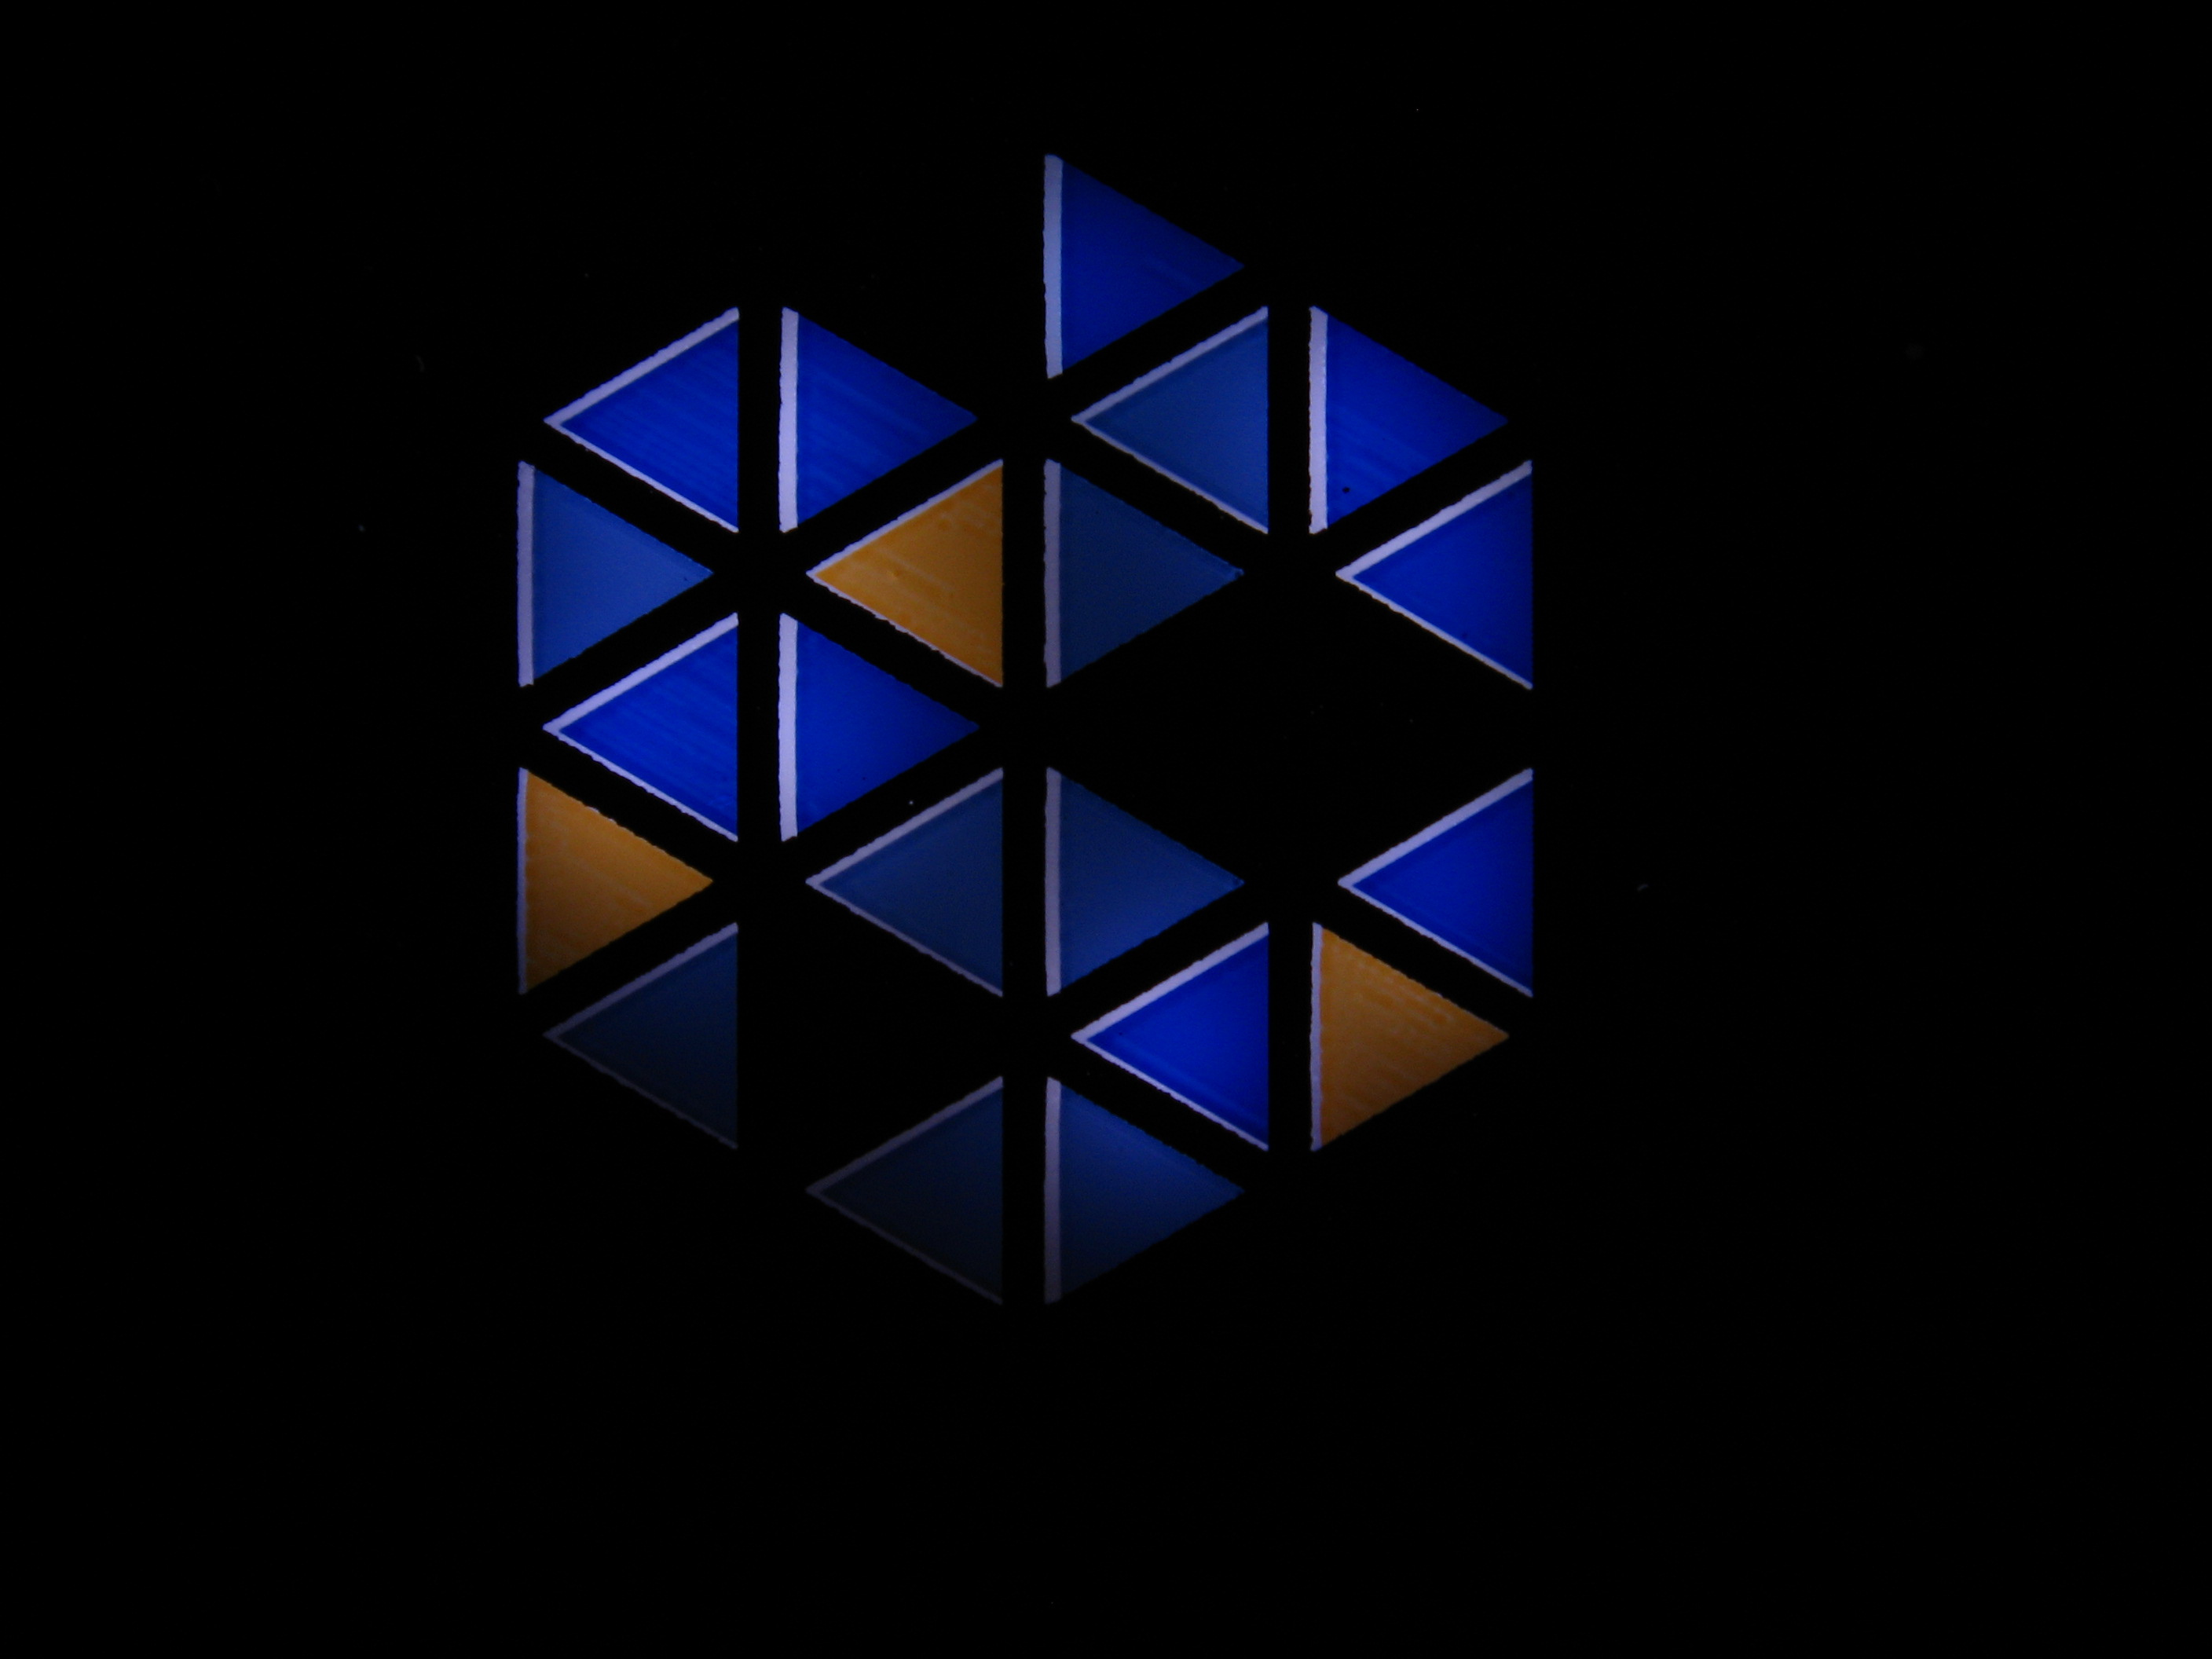
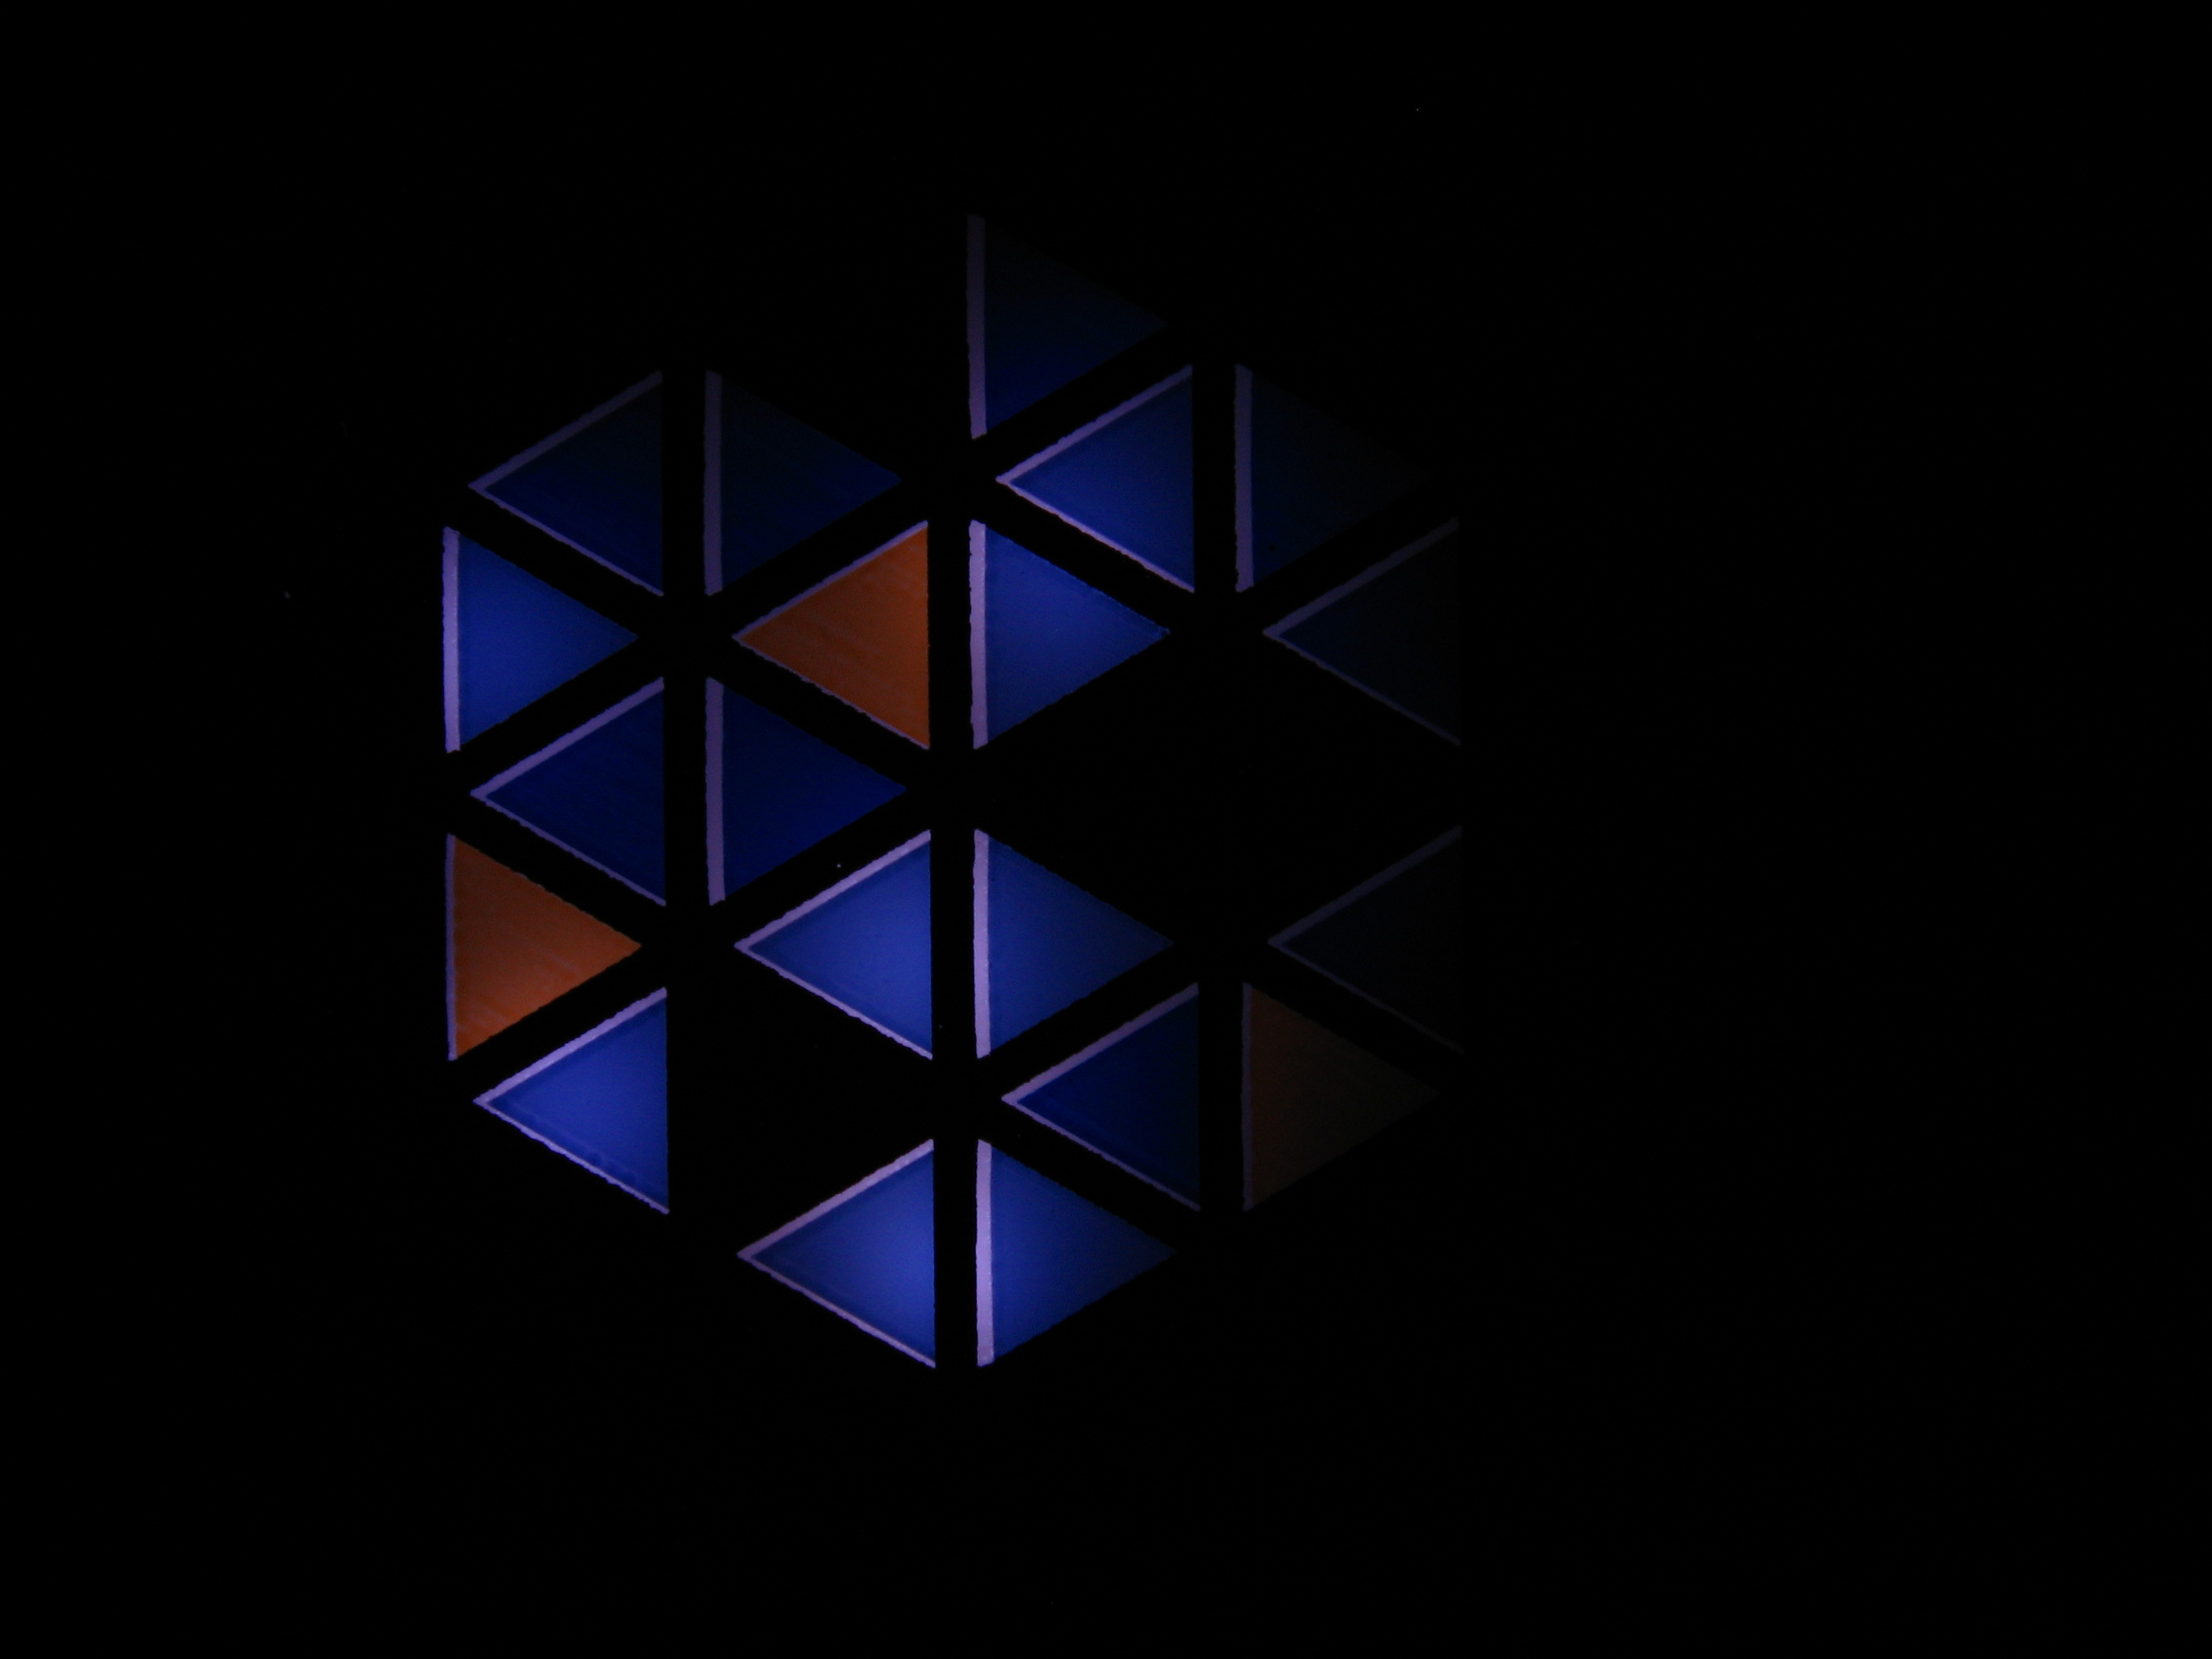
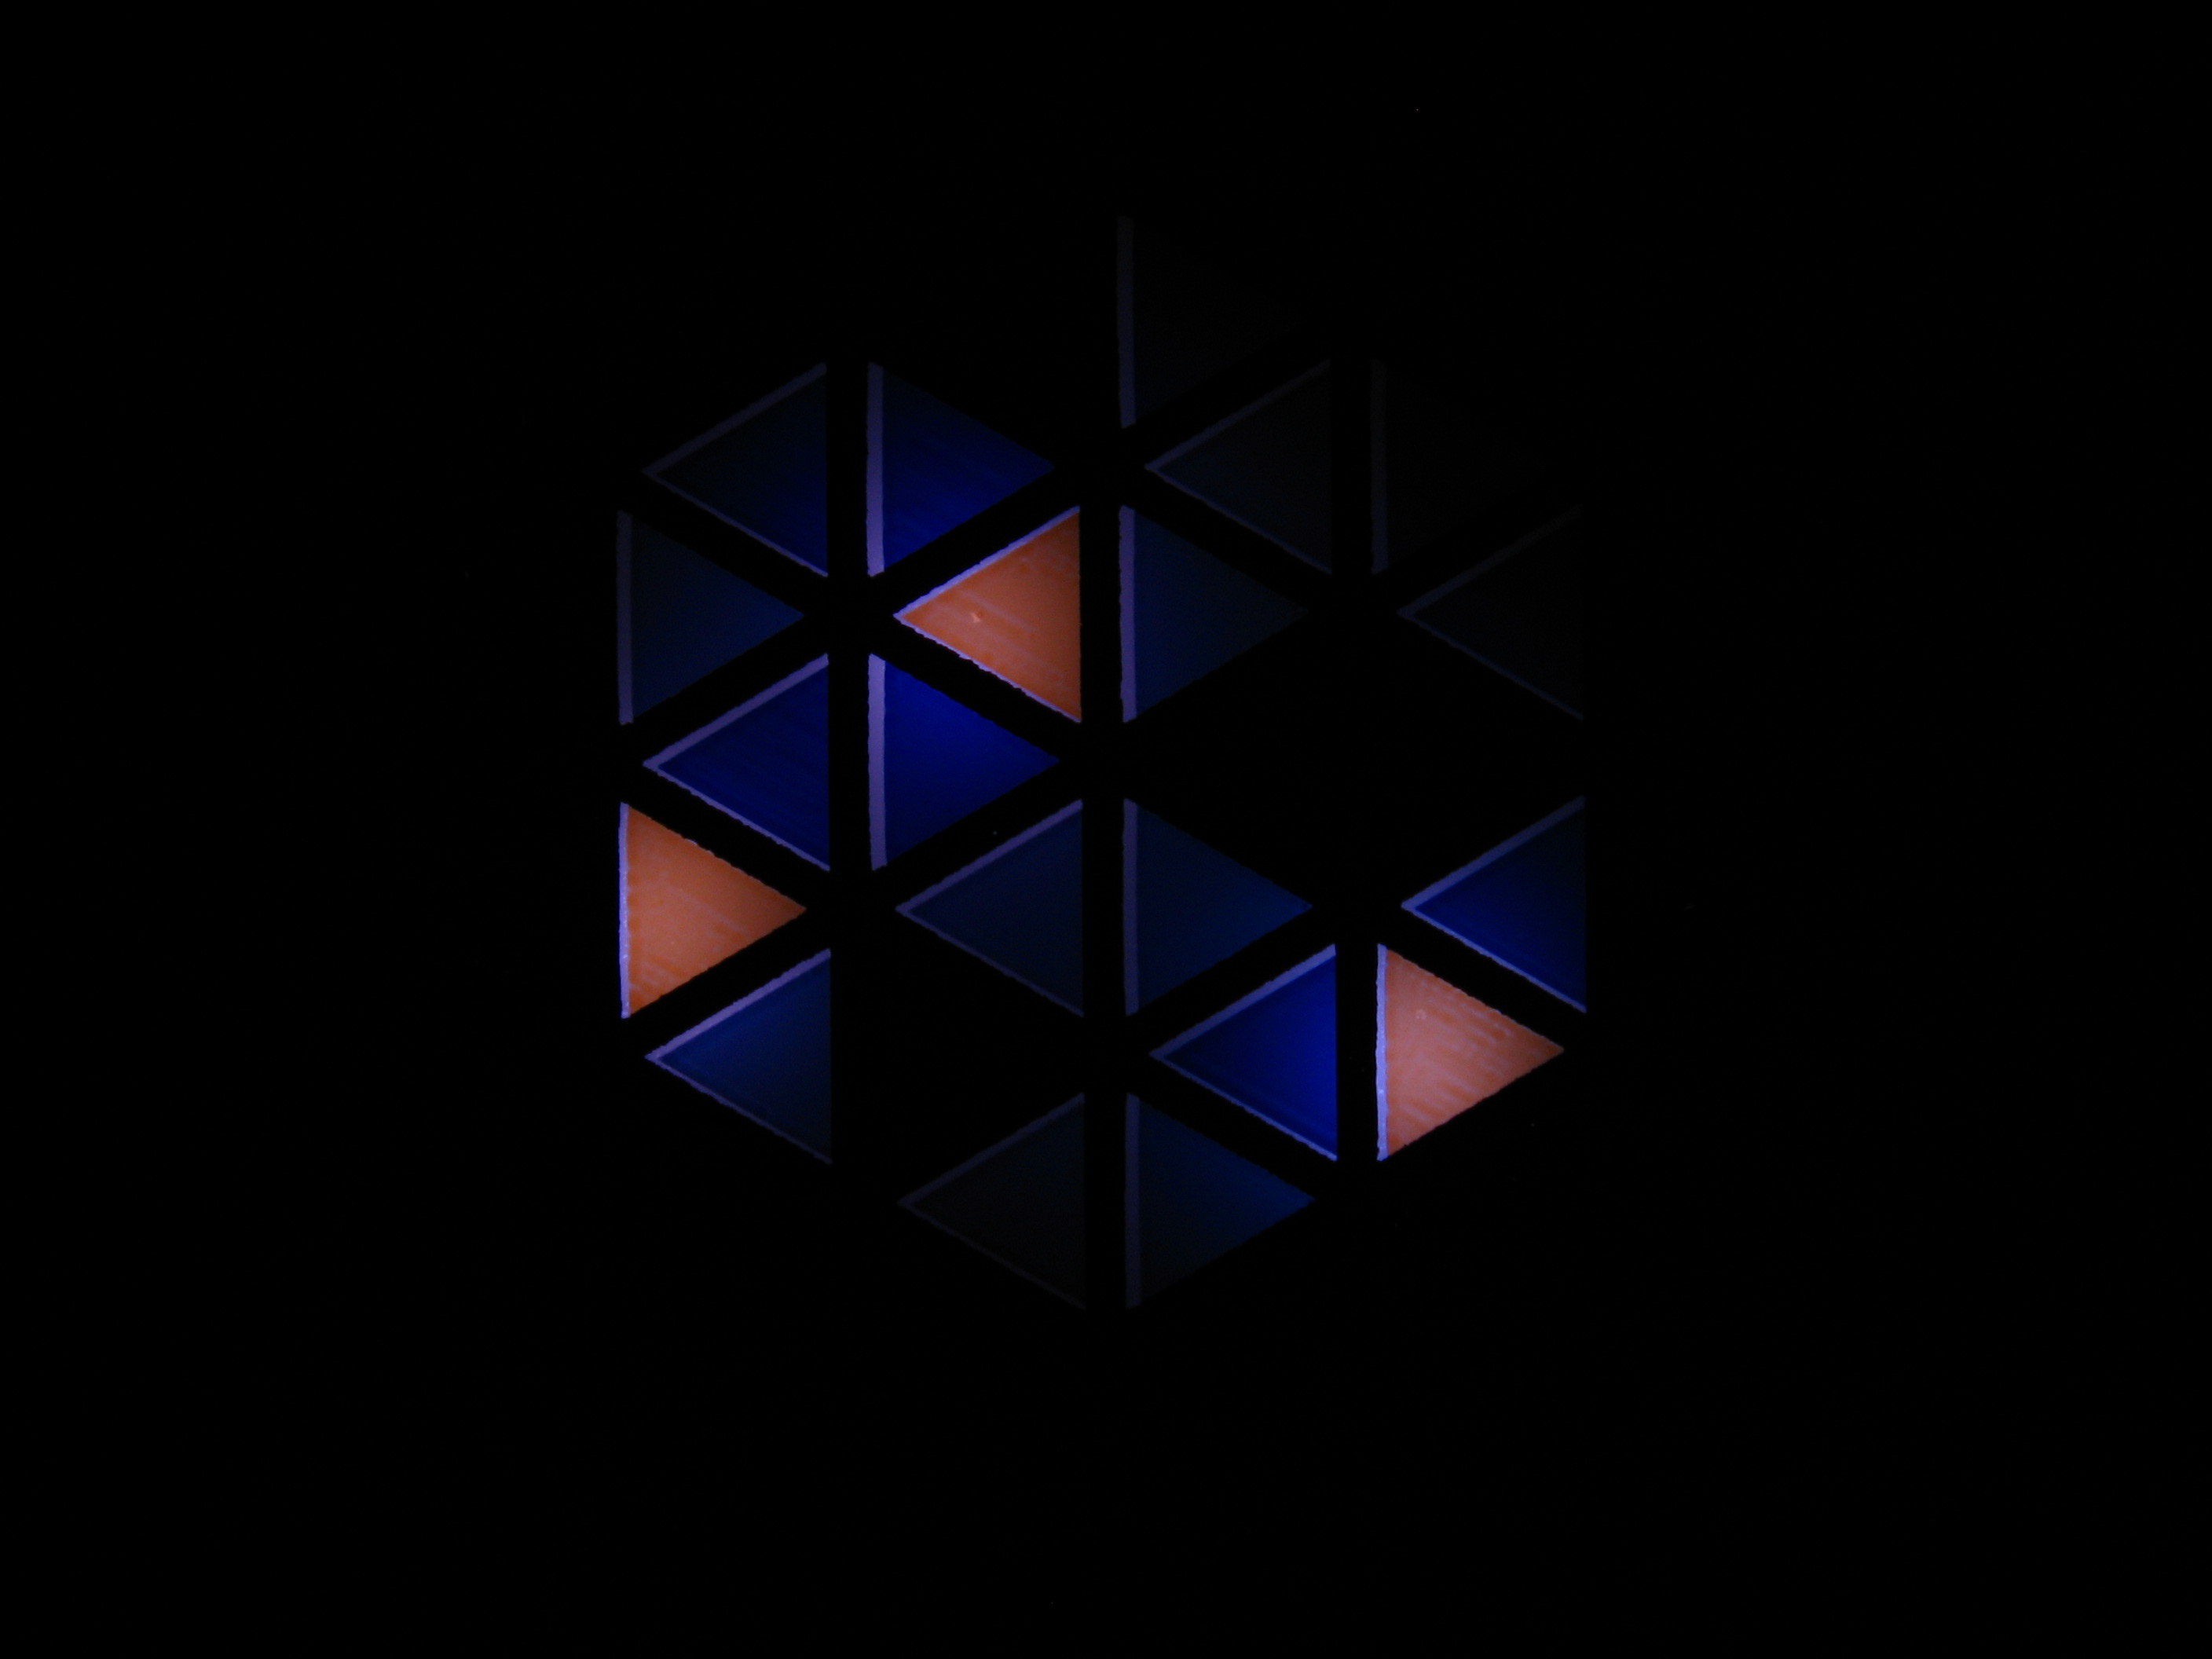
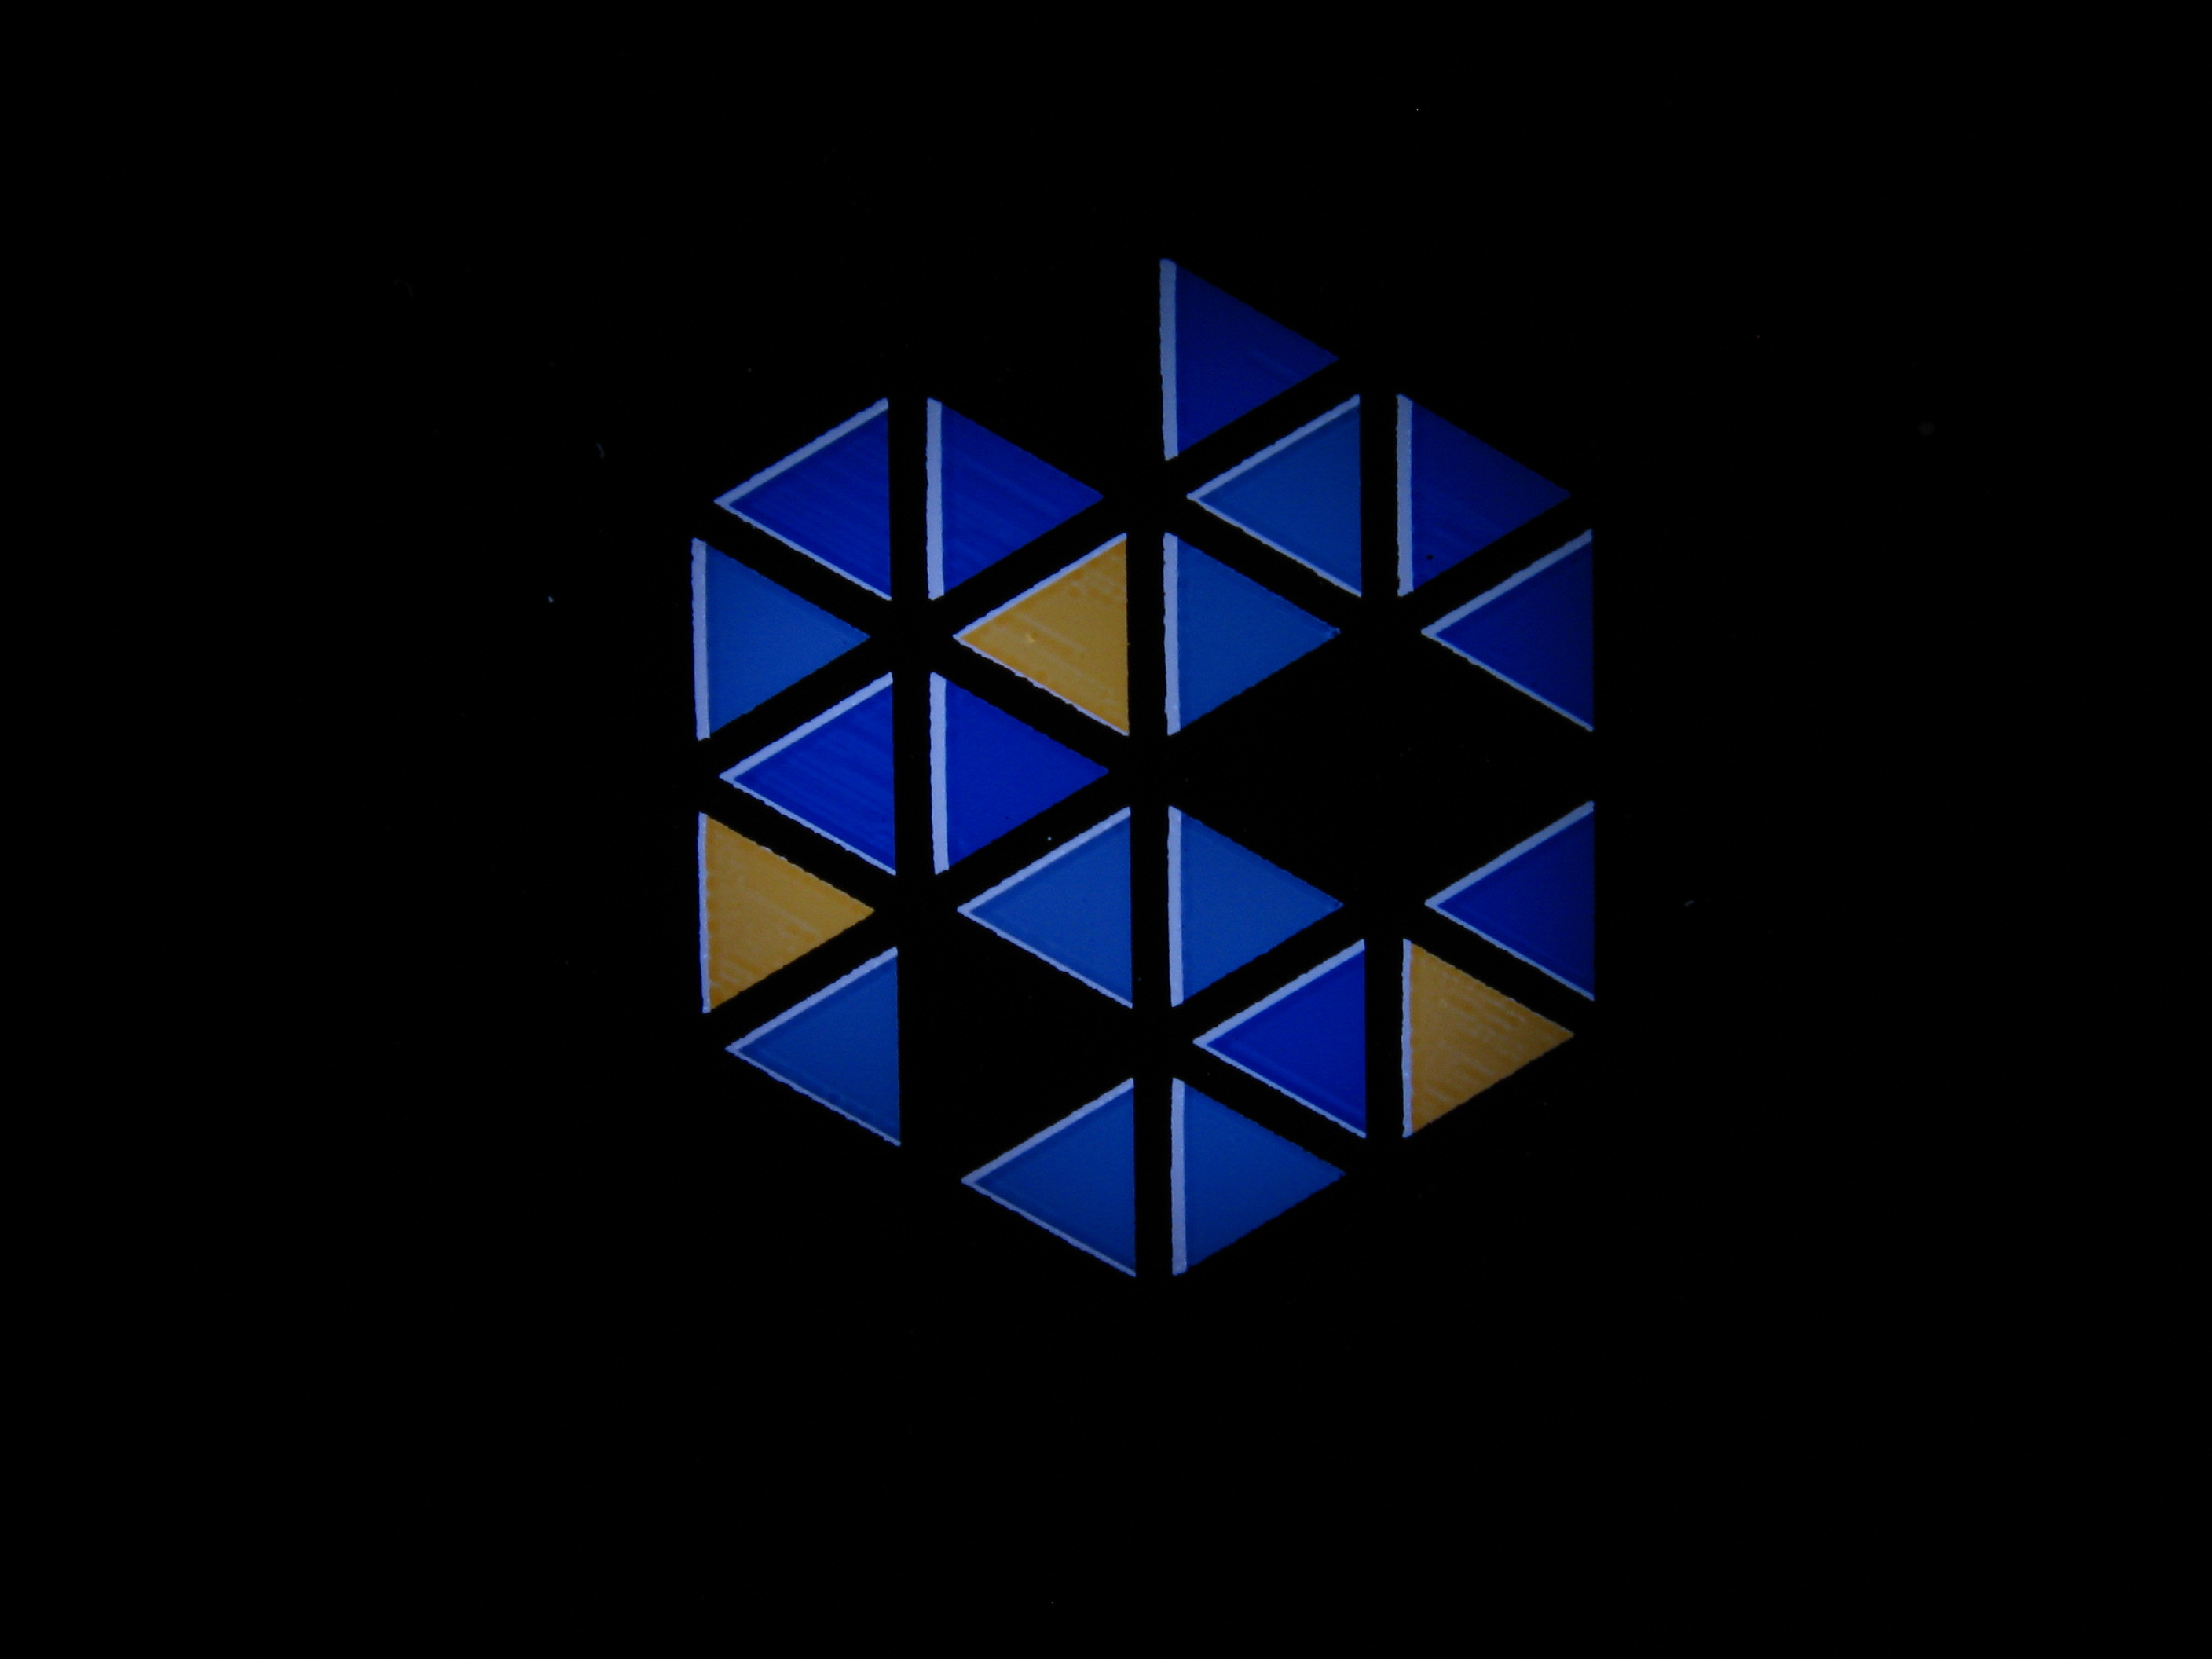
I found and qualified Nissha for its expertise in in-mold decoration (IMD). Few suppliers could produce the films at the level we needed, and Nissha was our single source for them. Nissha recommended Yomura as a supplier.
Nissha's gravure-printed films carried the layered decoration into the molding process. The artwork brought together the white background, colored jewel graphics, masking and separate pad-print operations. The decorated clear faceplate then joined the molded frame, button components and IR lens in the front assembly.
Early film samples made the optical tradeoff explicit. Nissha's October 2012 comparison kept a metallic layer across the indicator windows in one version and opened it in another. Covering the windows hid the unlit icons better, but reduced their brightness when lit. The November experiments proposed varying the black mask around the jewel while keeping the other printed layers fixed.
The printed graphics and mechanical features also had to agree about where light should appear. A November 2012 markup proposed clearance between the colored triangles and the black masking.
Registration and light isolation were separate parts of the problem. The light had to land on the correct printed facet, and it had to stay out of the neighboring facets and indicators.
In one early version, the printed jewel was offset from the LED locations. The resulting light pattern visibly missed the colored facets. I fixed that registration for production through tolerance and positional-control specifications.
When the print and LEDs did not line up
An early bezel photographed December 10, 2012.
Molded samples had to be inspected under room light and with the jewel illuminated. A February 2013 photographic review showed missing print that became hot spots when lit, along with jagged, peeling ink at the disc slot. Nissha proposed changes to printing and foil-flash cleaning, while noting that some printing defects involved competing process tradeoffs.
The light-isolation solution
The later assembly shows how the optical and mechanical work came together. The decorated faceplate joined a molded frame, with the controls and illuminated features arranged across it and the Glow Board behind. Behind the decorated face, I also had to control the light before it reached the plastic. The Glow Board carried the controls and LEDs, located on molded frame pins that aligned its switches with the button actuators. I designed a light-blocking foam gasket that compressed between the inside of the translucent dead-front bezel and the top of the board. Together with plastic ribs, it isolated the illuminated features from light inside the enclosure and from adjacent features. That combination gave us very effective light control.
The light-isolation stack
The Glow Board lifted away from the back of the bezel.
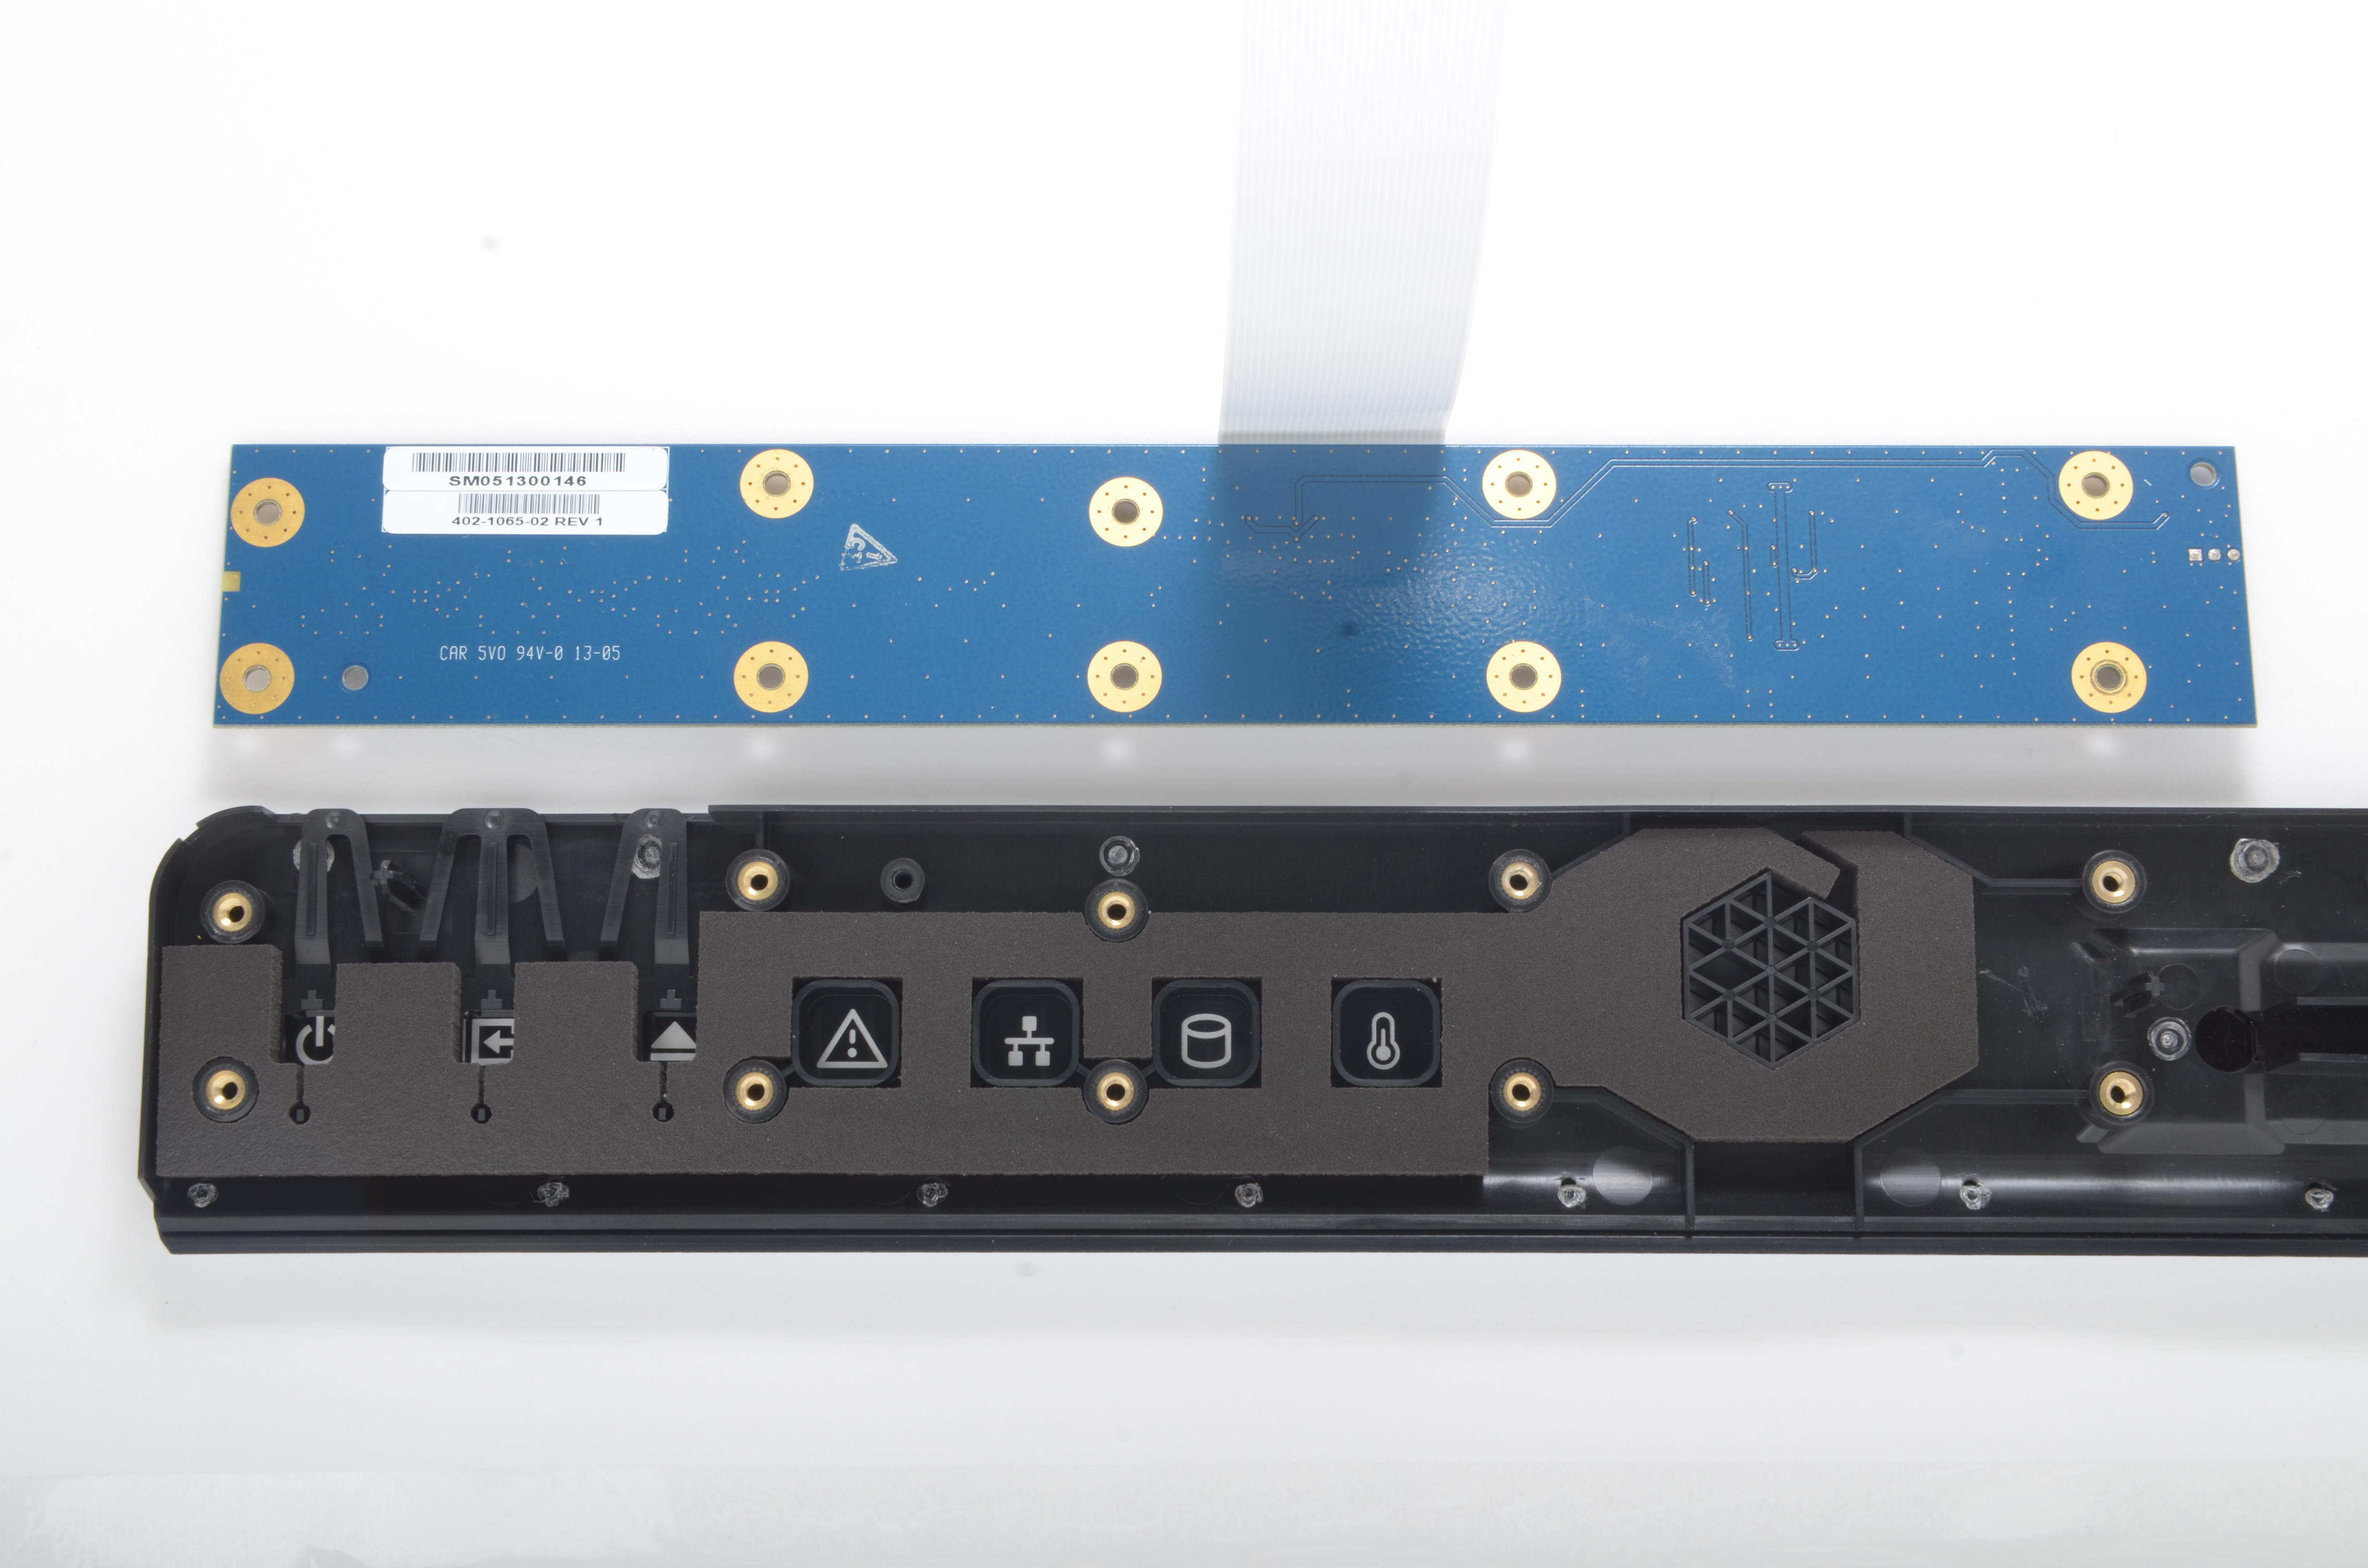
The earlier design used separate button and jewel gaskets; a July 2013 assembly-instruction revision replaced them with one gasket spanning the buttons and logo array.
Board location, button feel and light isolation depended on assembling that stack correctly. The instructions called for fully seating the buttons, installing the gasket, seating the ribbon cable in the Glow Board connector, then locating the board and tightening its mounting screw to the specified torque. During final assembly, the bezel was held at 90 degrees to the chassis to connect the cable.
Making the front fit
March-May 2013: resolving the front interfaces.
The front was a coupled system: the bezel's reveal within the cover, the disc slot's position around the drive, the buttons' travel to the switches, and the Glow Board's location behind the decorated face all had to work together. I coordinated those interfaces across the plastic parts, sheet metal, electronics and assembly method.
I brought Function Engineering in for the tolerance analysis I could not cover myself, drawing on our earlier work together. I secured their agreement to engage and pushed to get the purchase order approved. Their analysis helped make the interactions explicit; I remained responsible for integrating the mating parts and the assembly method.
Function's March 2013 review examined the loops between the bezel, cover, disc slot, sheet metal, alignment features and switches. One example compared the nominal 0.5 mm bezel-to-cover gap with a calculated root-sum-square variation of ±0.92 mm under the initial assumptions. The intended reveal required control of the whole assembly.
The options included increasing the gap, tightening molded-part tolerances and changing how the parts were located during assembly. A companion calculation with tighter tolerances reduced the statistical estimate, although its worst-case variation still exceeded the nominal gap. Vendor confirmation of the process tolerances remained part of the work.
The disc opening and cover installation exposed other constraints. The disc had unequal clearance above and below it. Alignment pins had limited lead-in, and the feet could change the relationship between parts during assembly. Function's review considered centering the opening, changing lead-ins and using assembly spacers.
The front-fit work extended into both the molded features and the assembly method. The April and May change lists called for extending the cover's bezel shroud, moving the slot rib from the cover to the front frame, and revising the alignment slots and screw holes. These were coordinated changes across the cover, frame and decorated faceplate.
Carrying changes through the parts
Spring 2013: connecting the molded controls to the board.
At each control, the molded actuator had to meet the switch on the Glow Board. I had to account for both the clearance along the press direction and the alignment across the switch face, while locating the board within the same front assembly.
The buttons brought a second tolerance problem into the front assembly. Function's March analysis calculated ±0.49 mm worst-case variation and about ±0.22 mm root-sum-square variation along the actuation axis. Their recommendation was an initial 0.4 mm gap, leaving the tool metal safe so the contact geometry could be tuned for feel after the first molding trial. The vertical analysis separately checked whether the actuator would stay centered on the switch.
The front at close range
The controls and slot within the floating bezel.
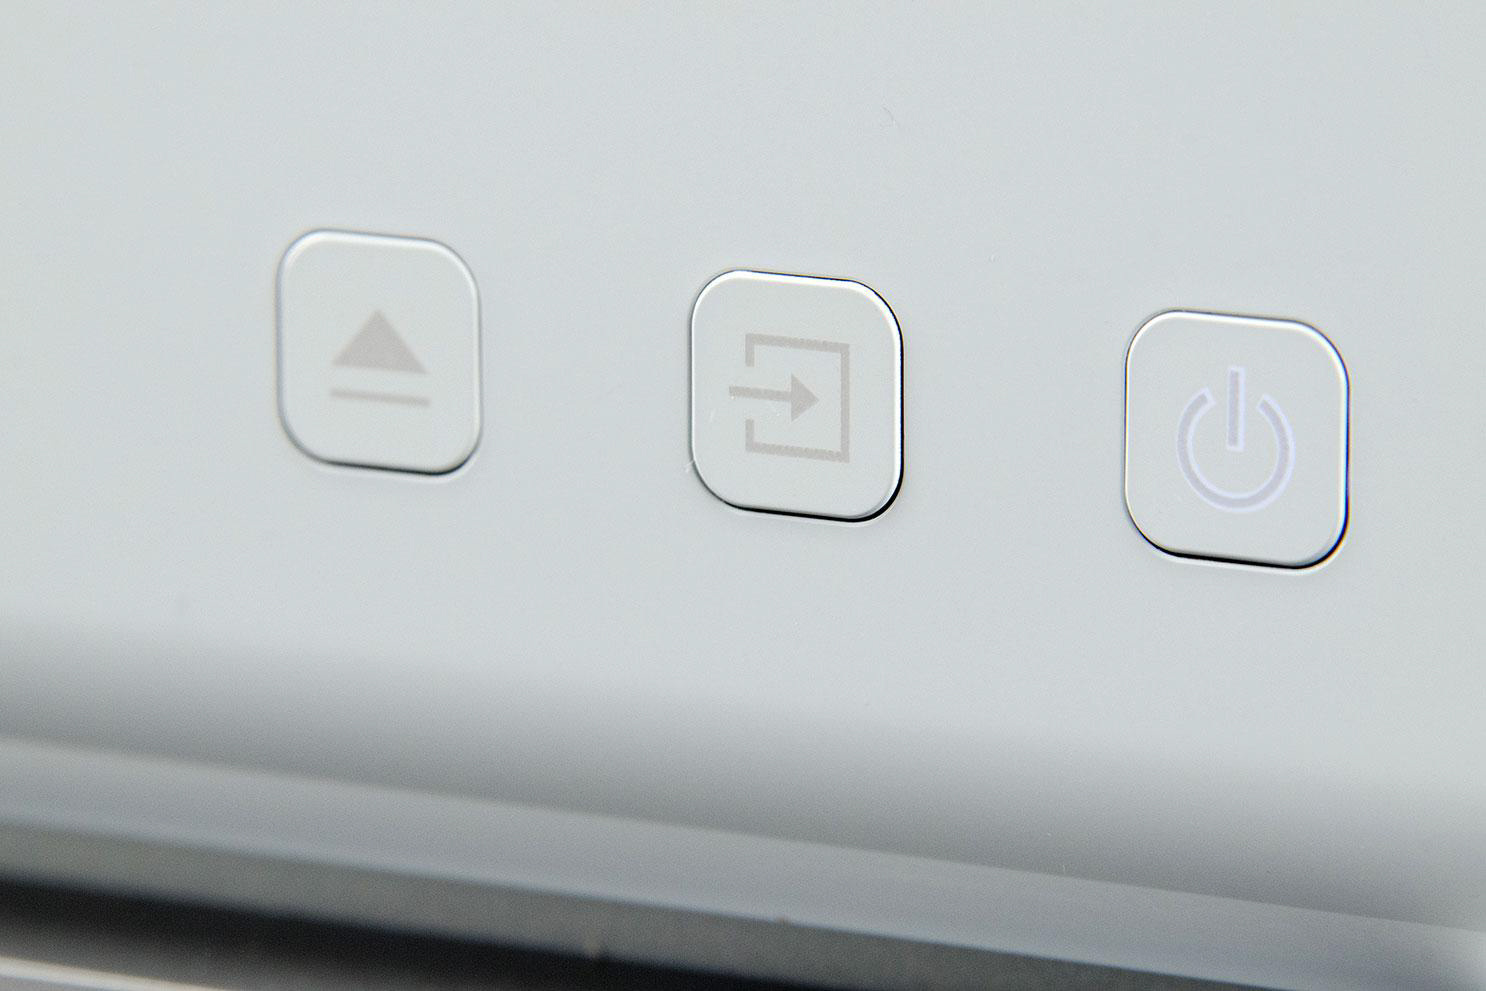
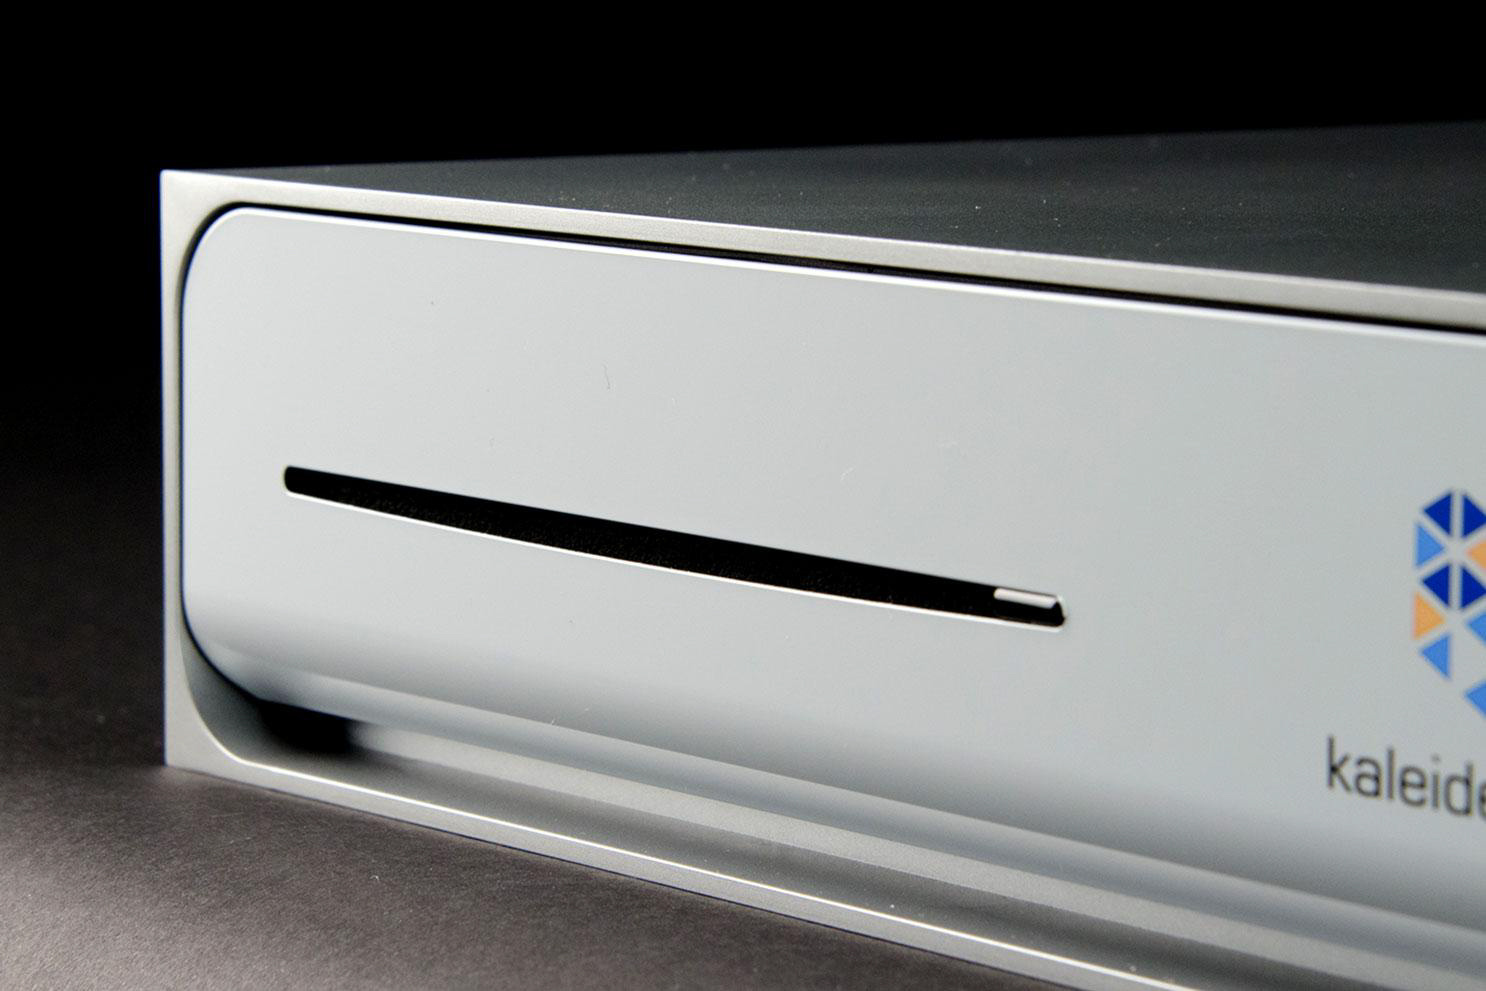
The April and May change lists called for adding 0.3 mm to the button contactors and revising pivot, rib and heat-stake features. The four-corner recesses for gate vestige and ejector mismatch were specified on the button tree, part 502-1194-00. These small details connected the molded controls to the switch positions and the assembled front.
Building the enclosure from the inside out
April 2013: turning the reinforced shell into an assembly.
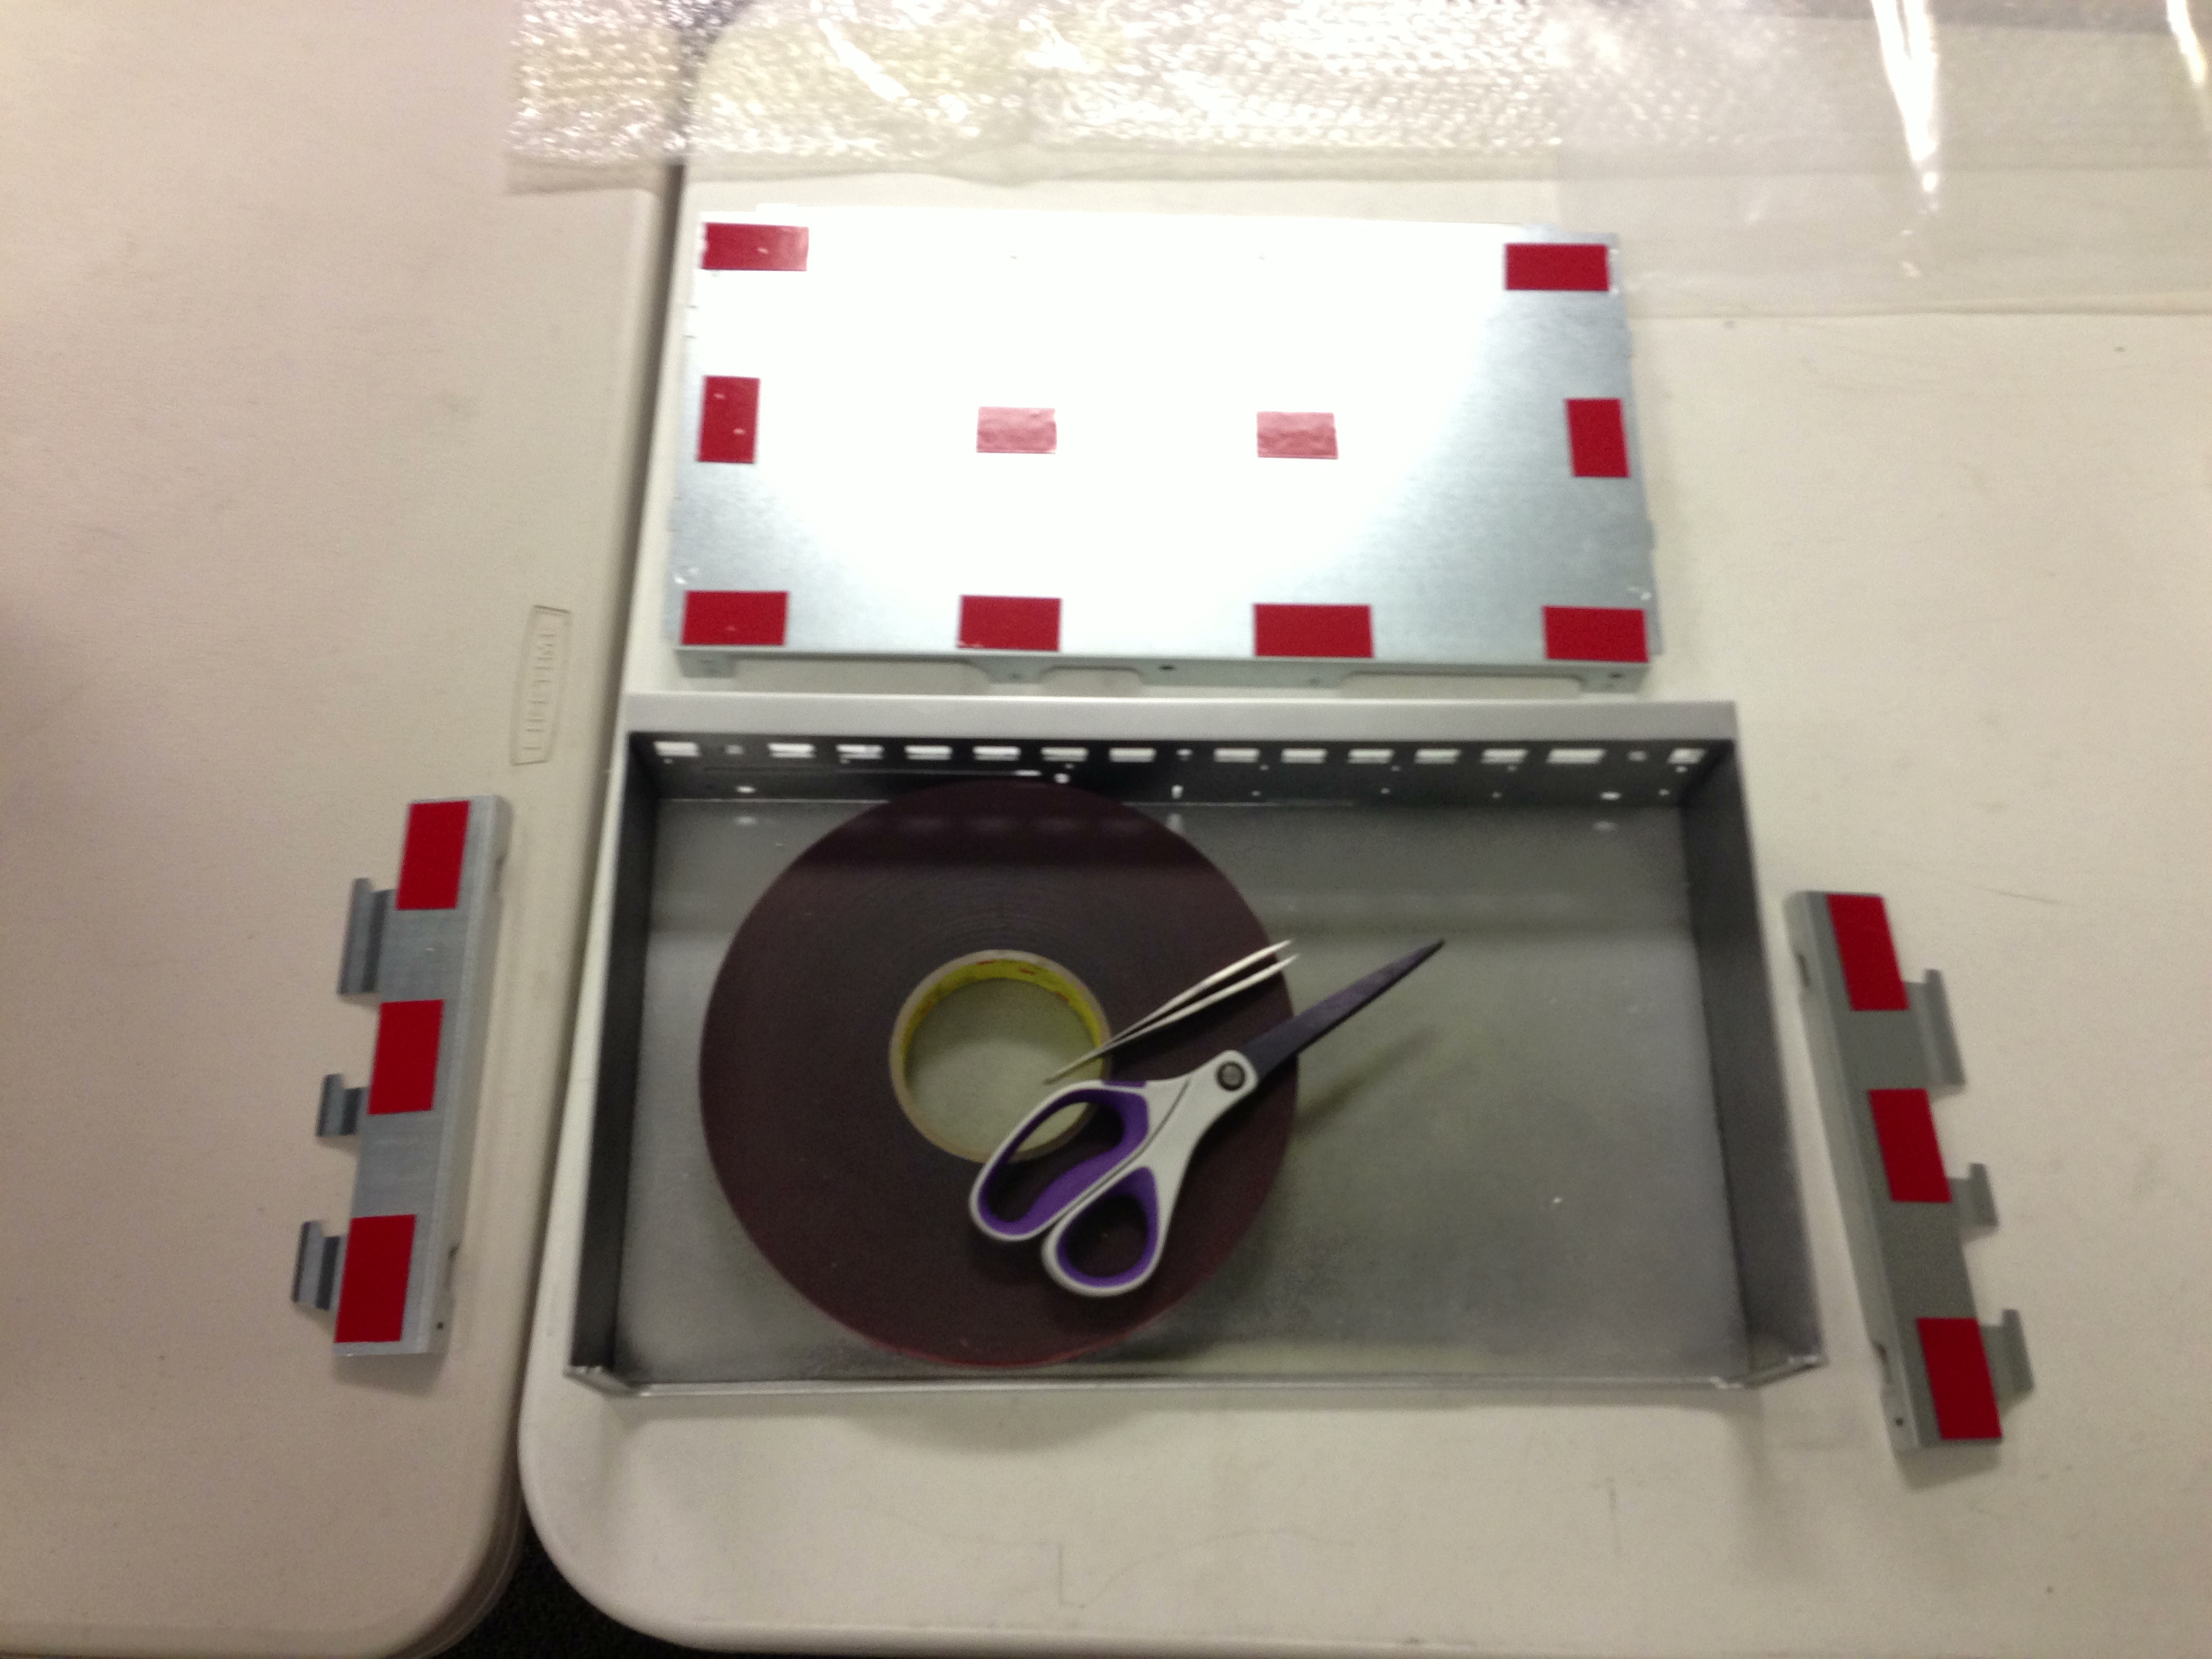
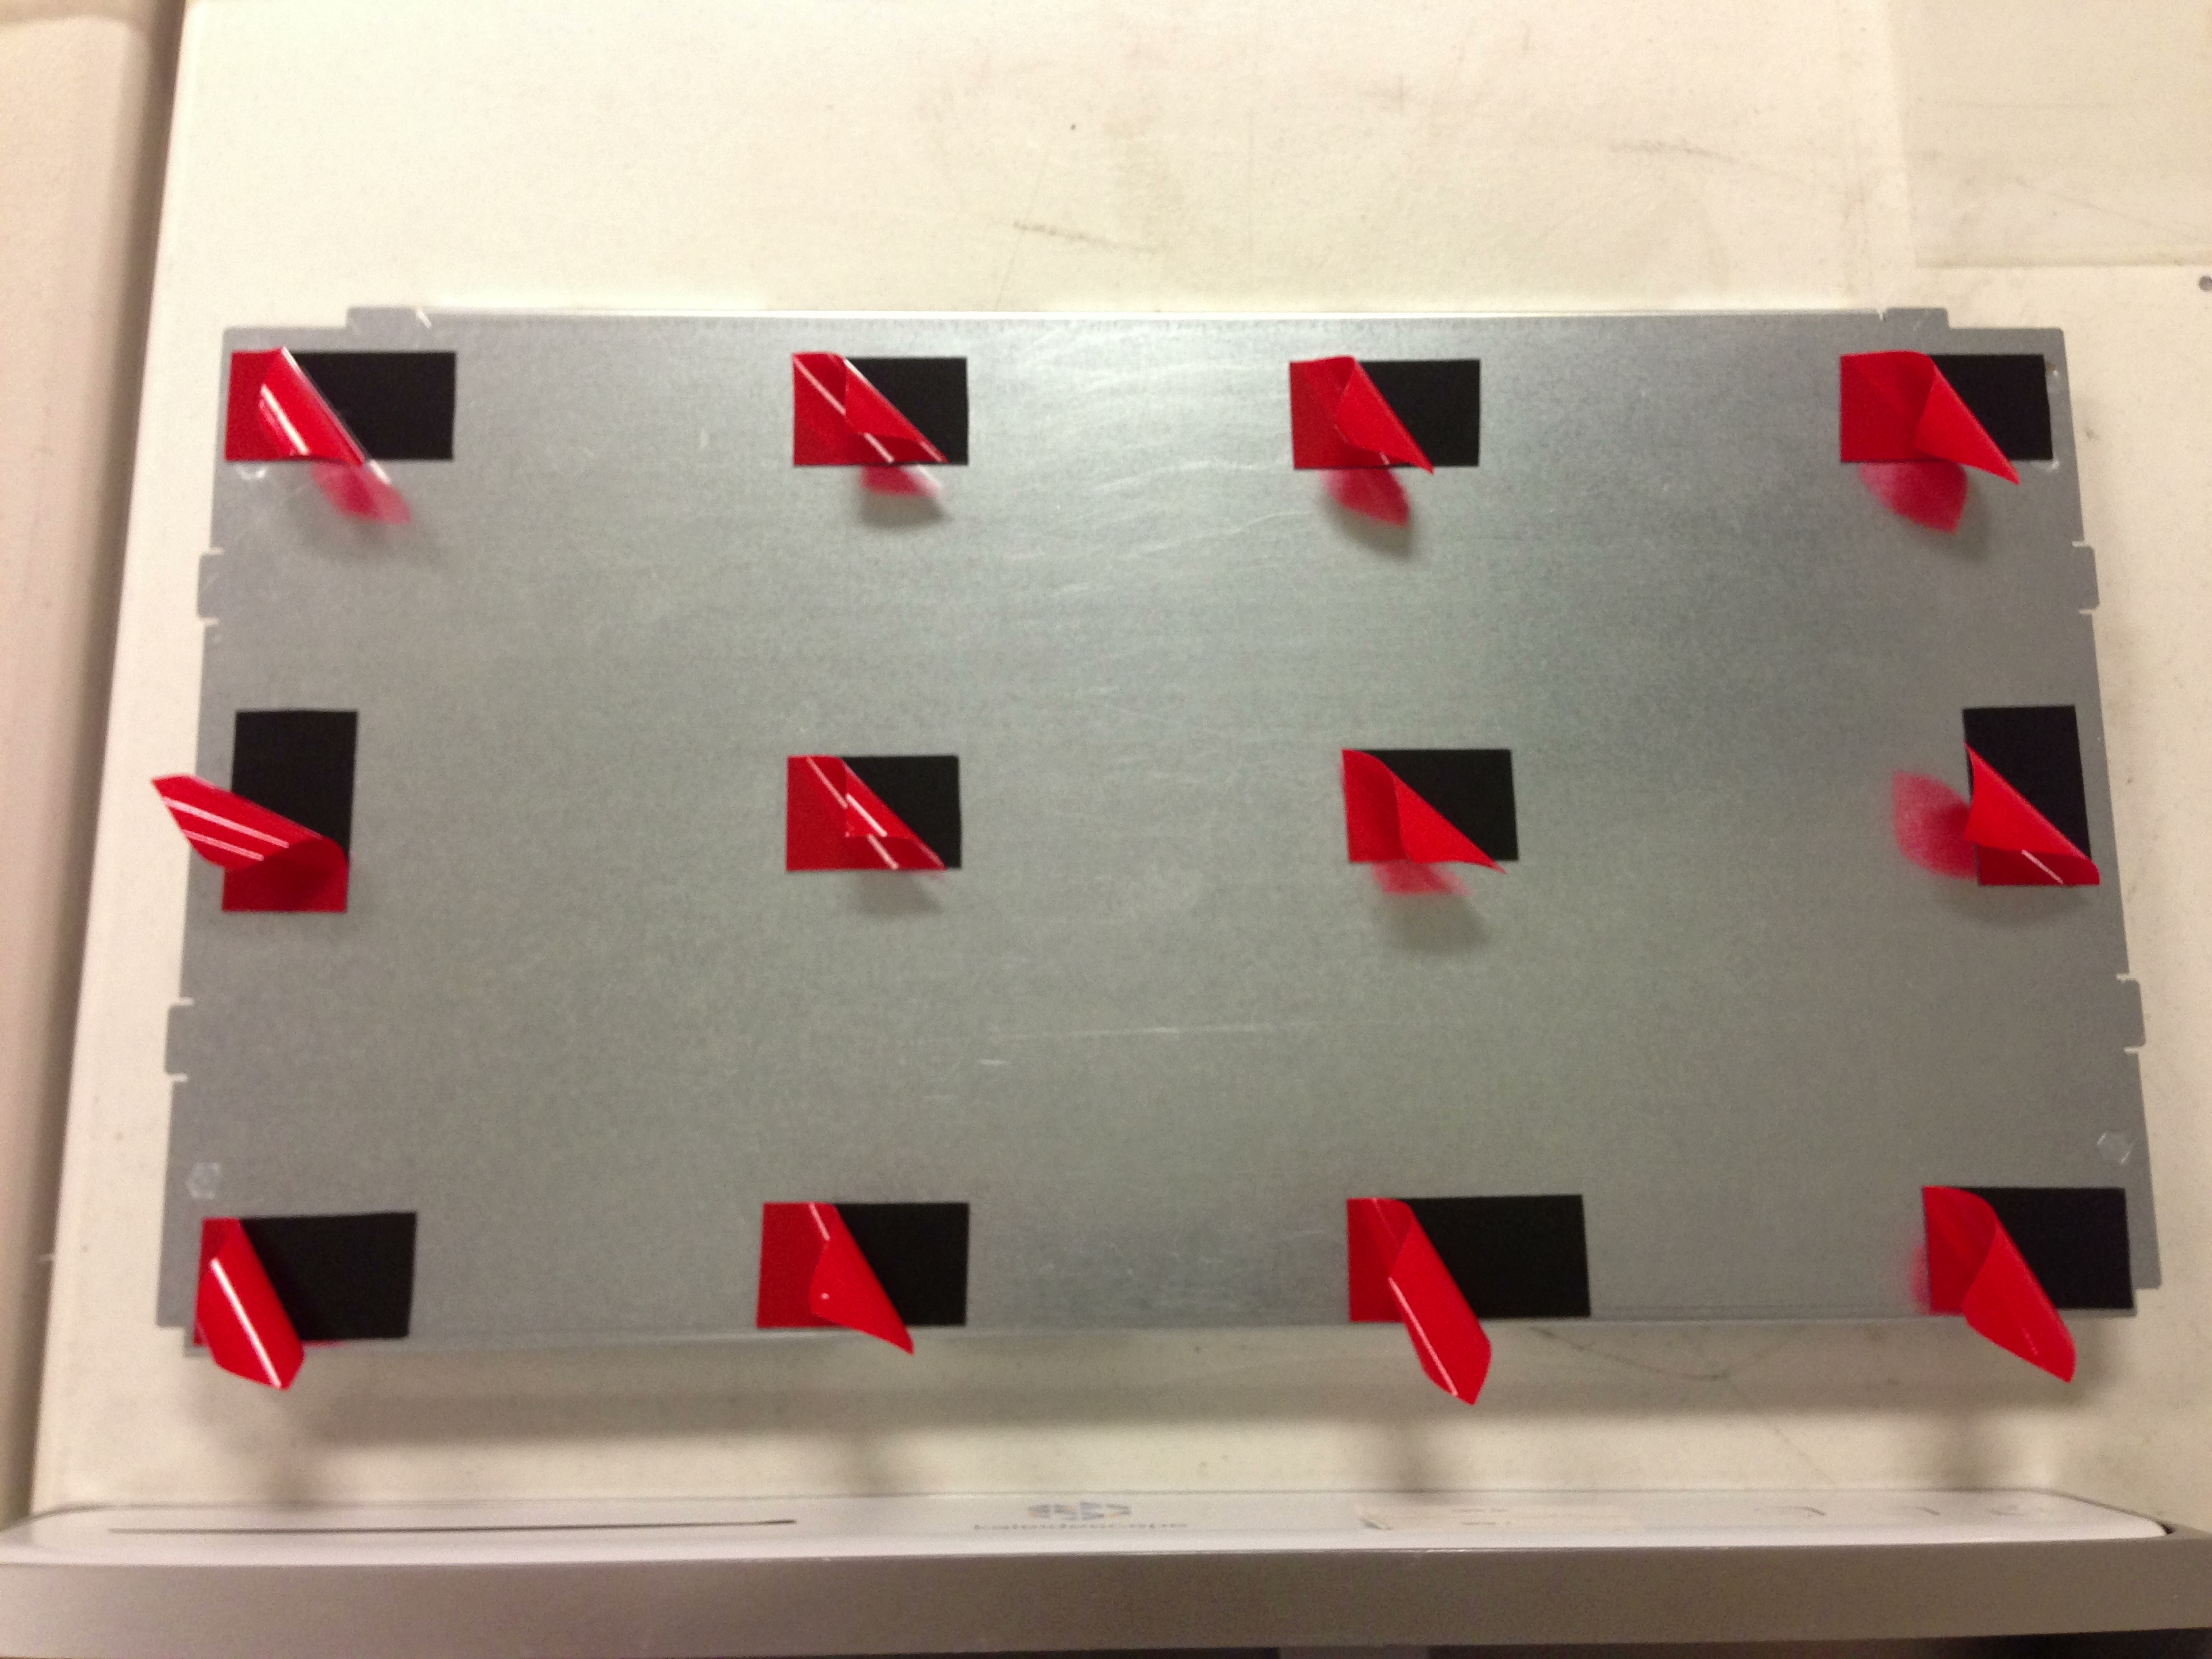
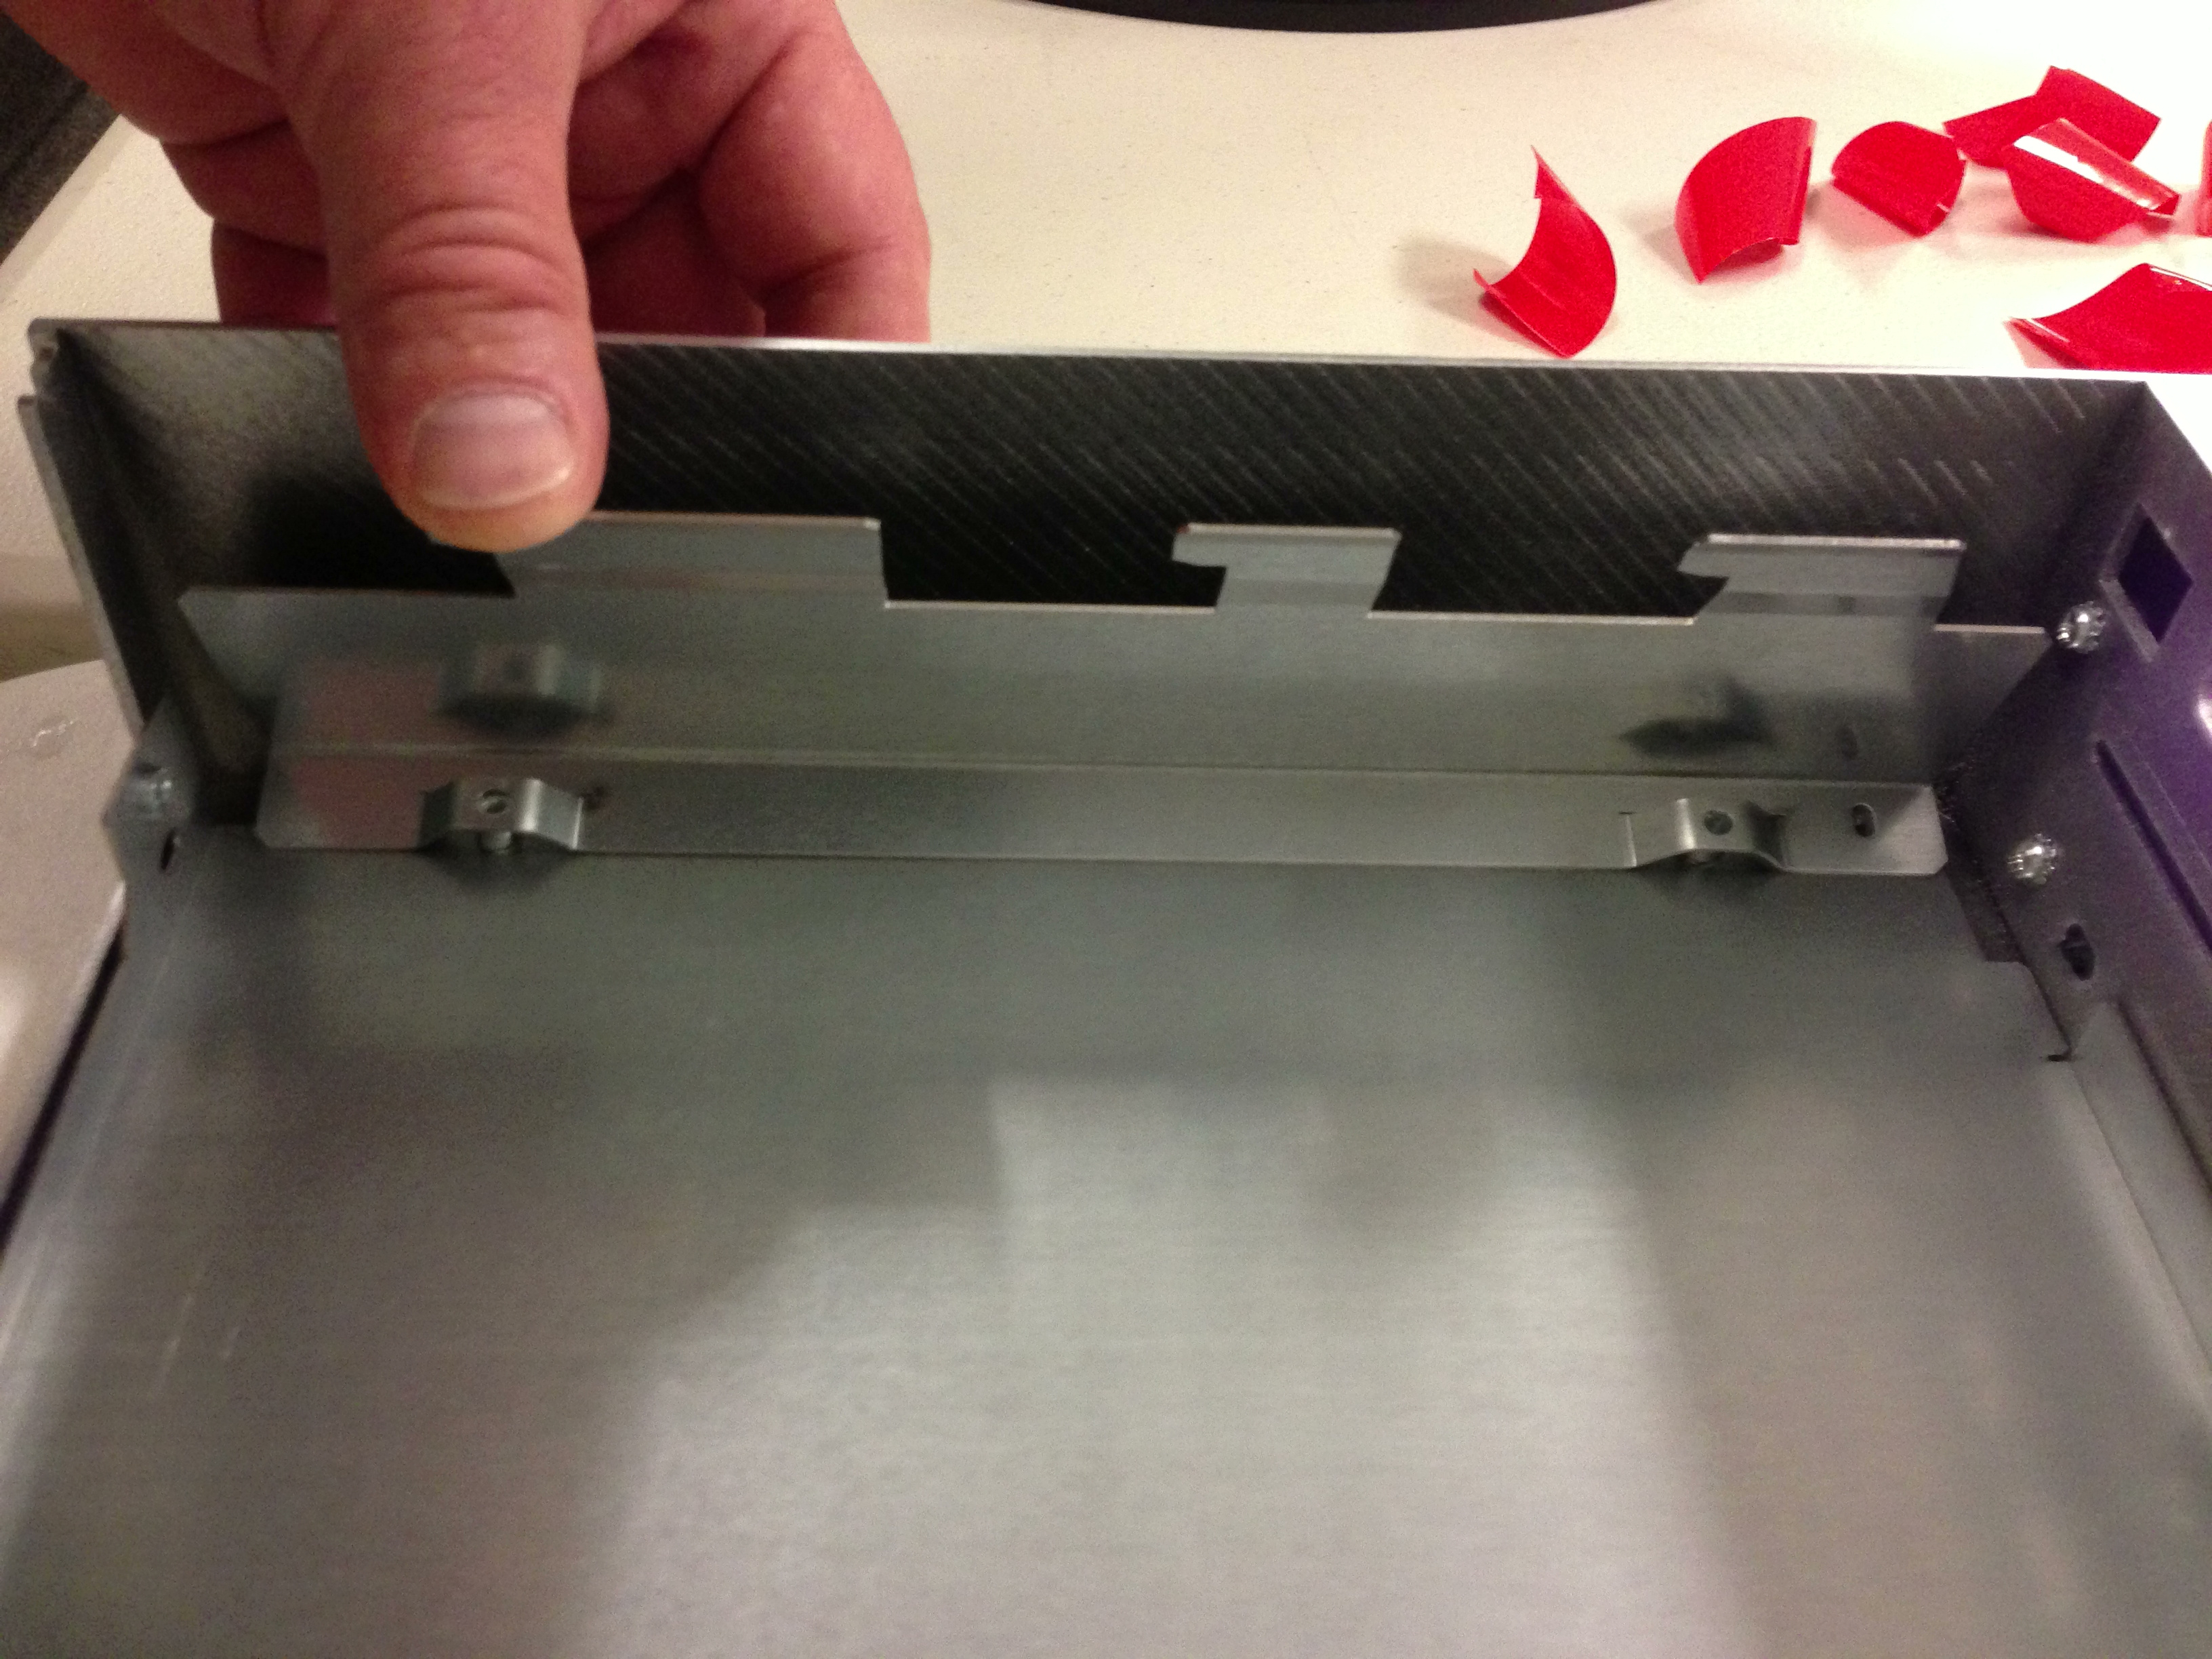
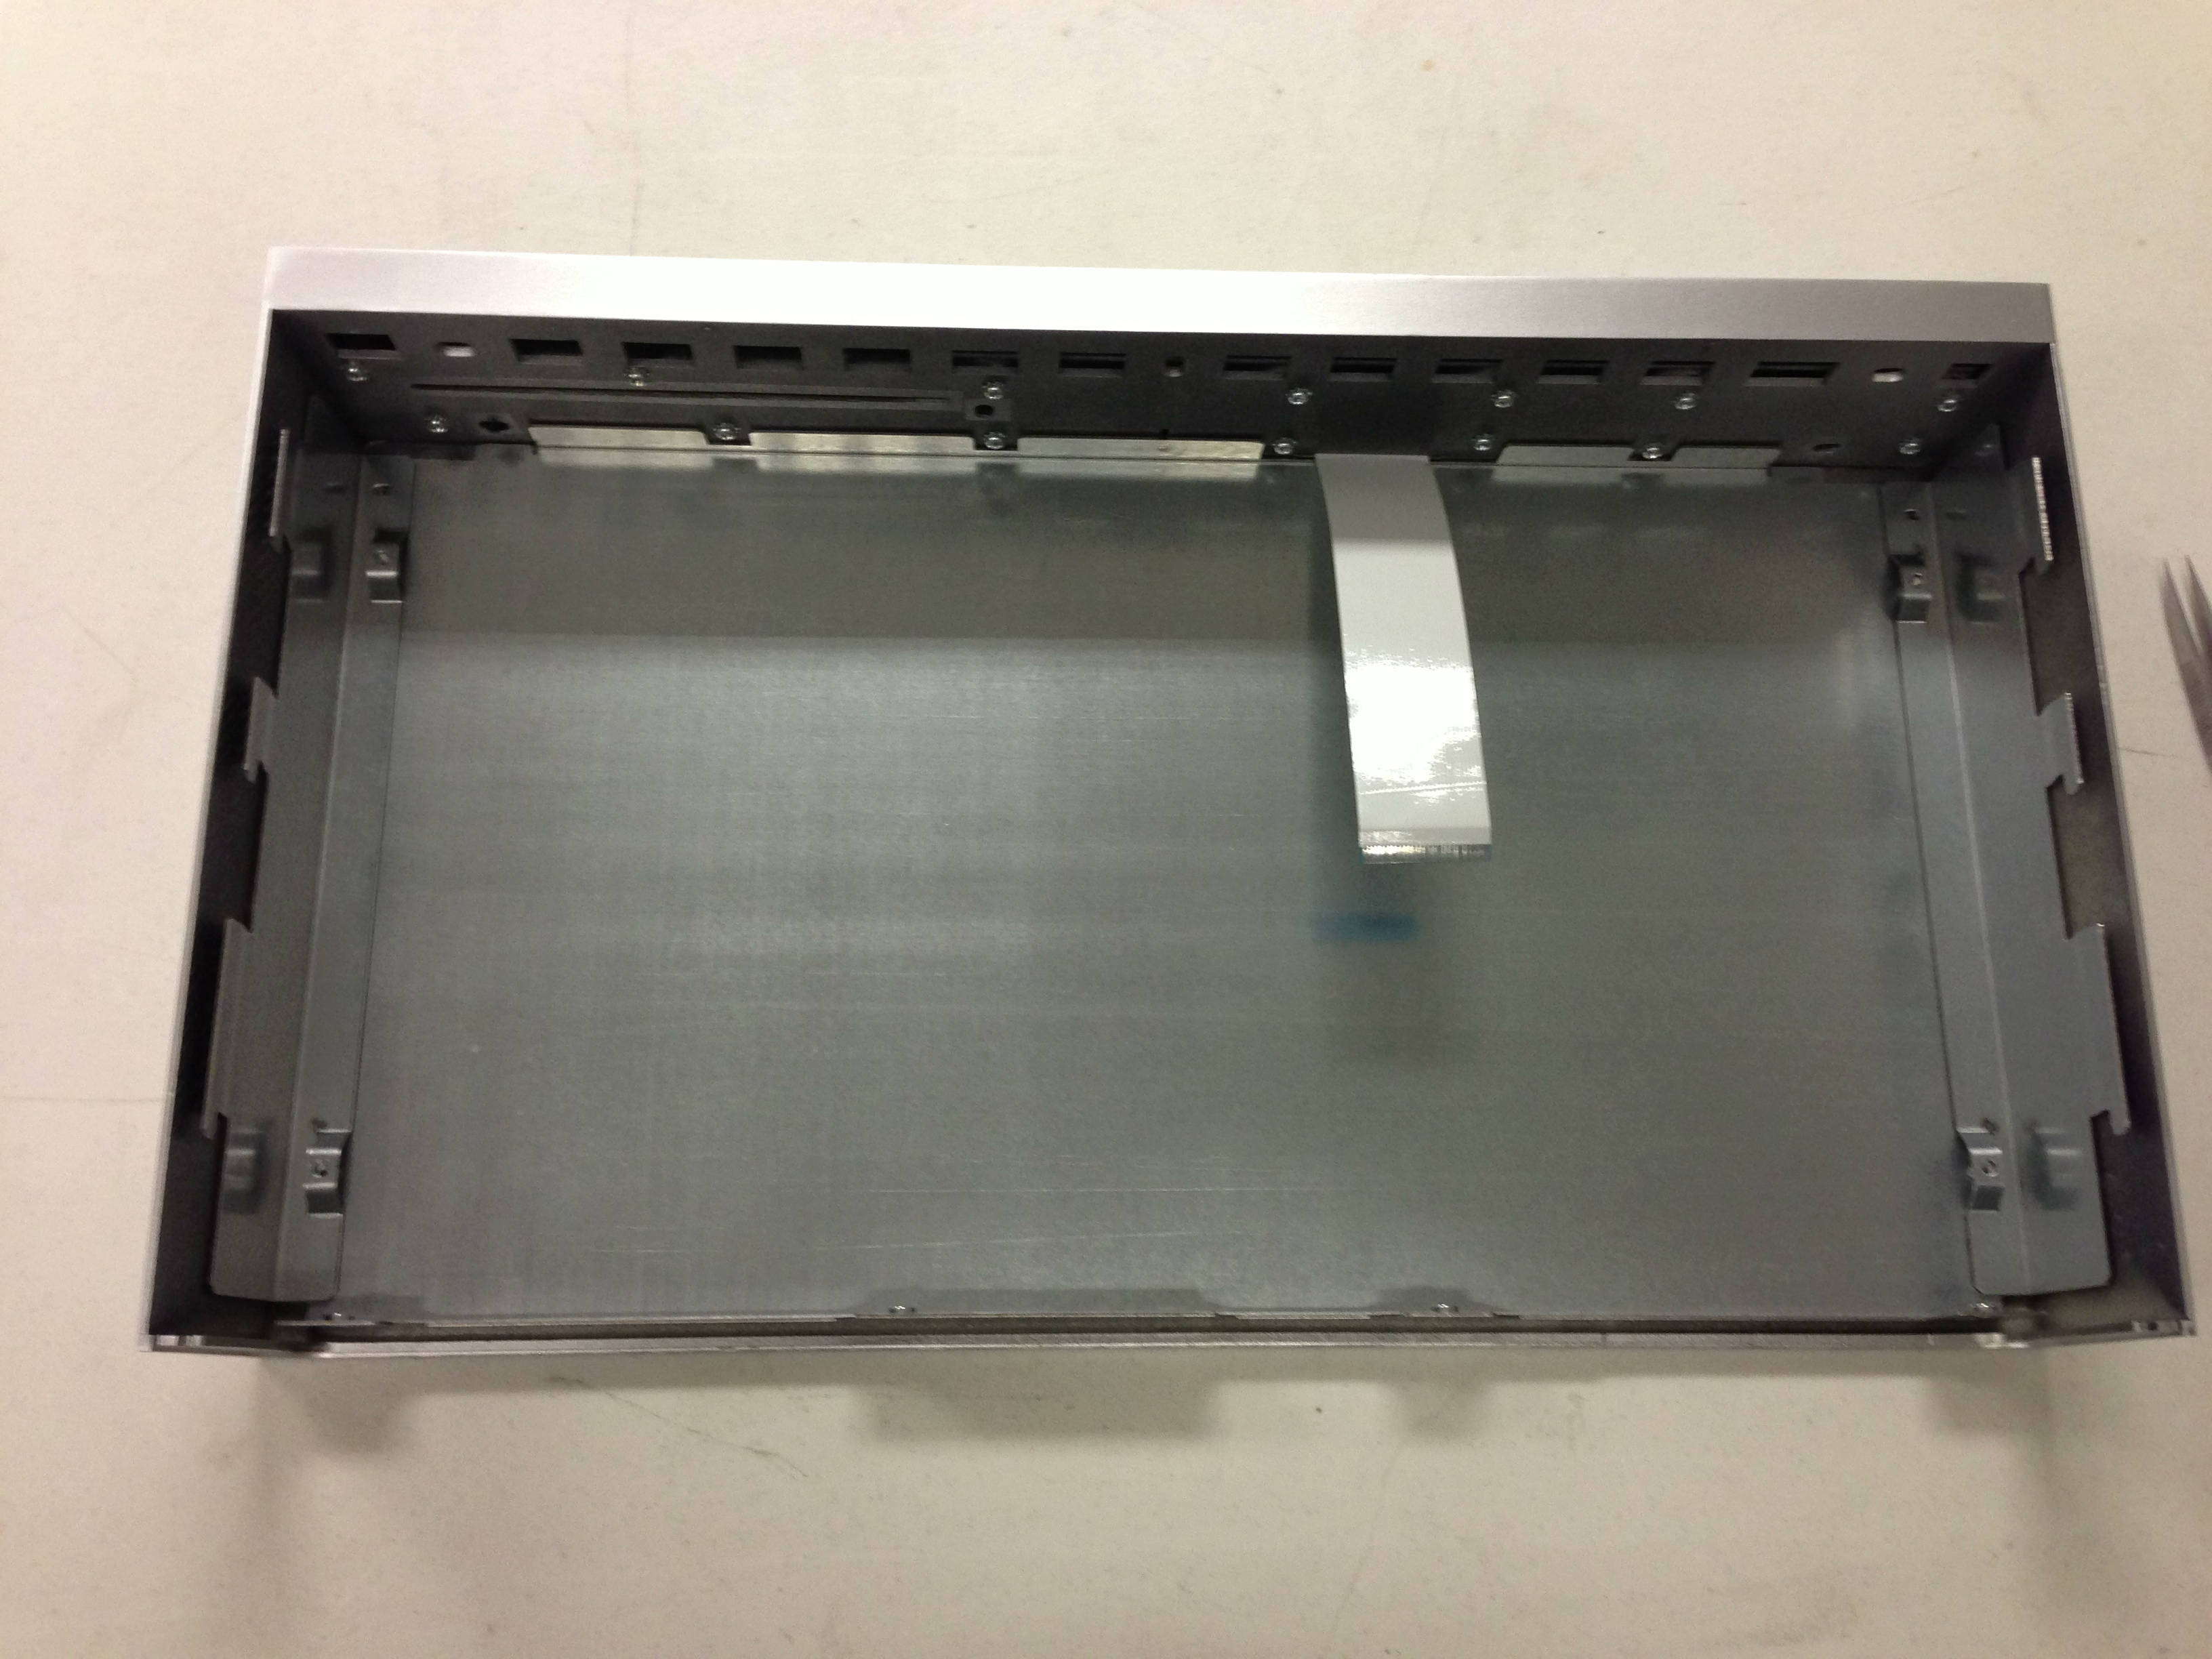
I designed the drop-and-slide plastic cover with bonded sheet-metal panels inside it for stiffening and EMI integrity. Yomura supplied the molded cover and Mass Precision the metalwork. The early assembly combined a top stiffener, left and right stiffeners, and a rear shield; later top-stiffener revisions incorporated the side pieces.
Inside the cover
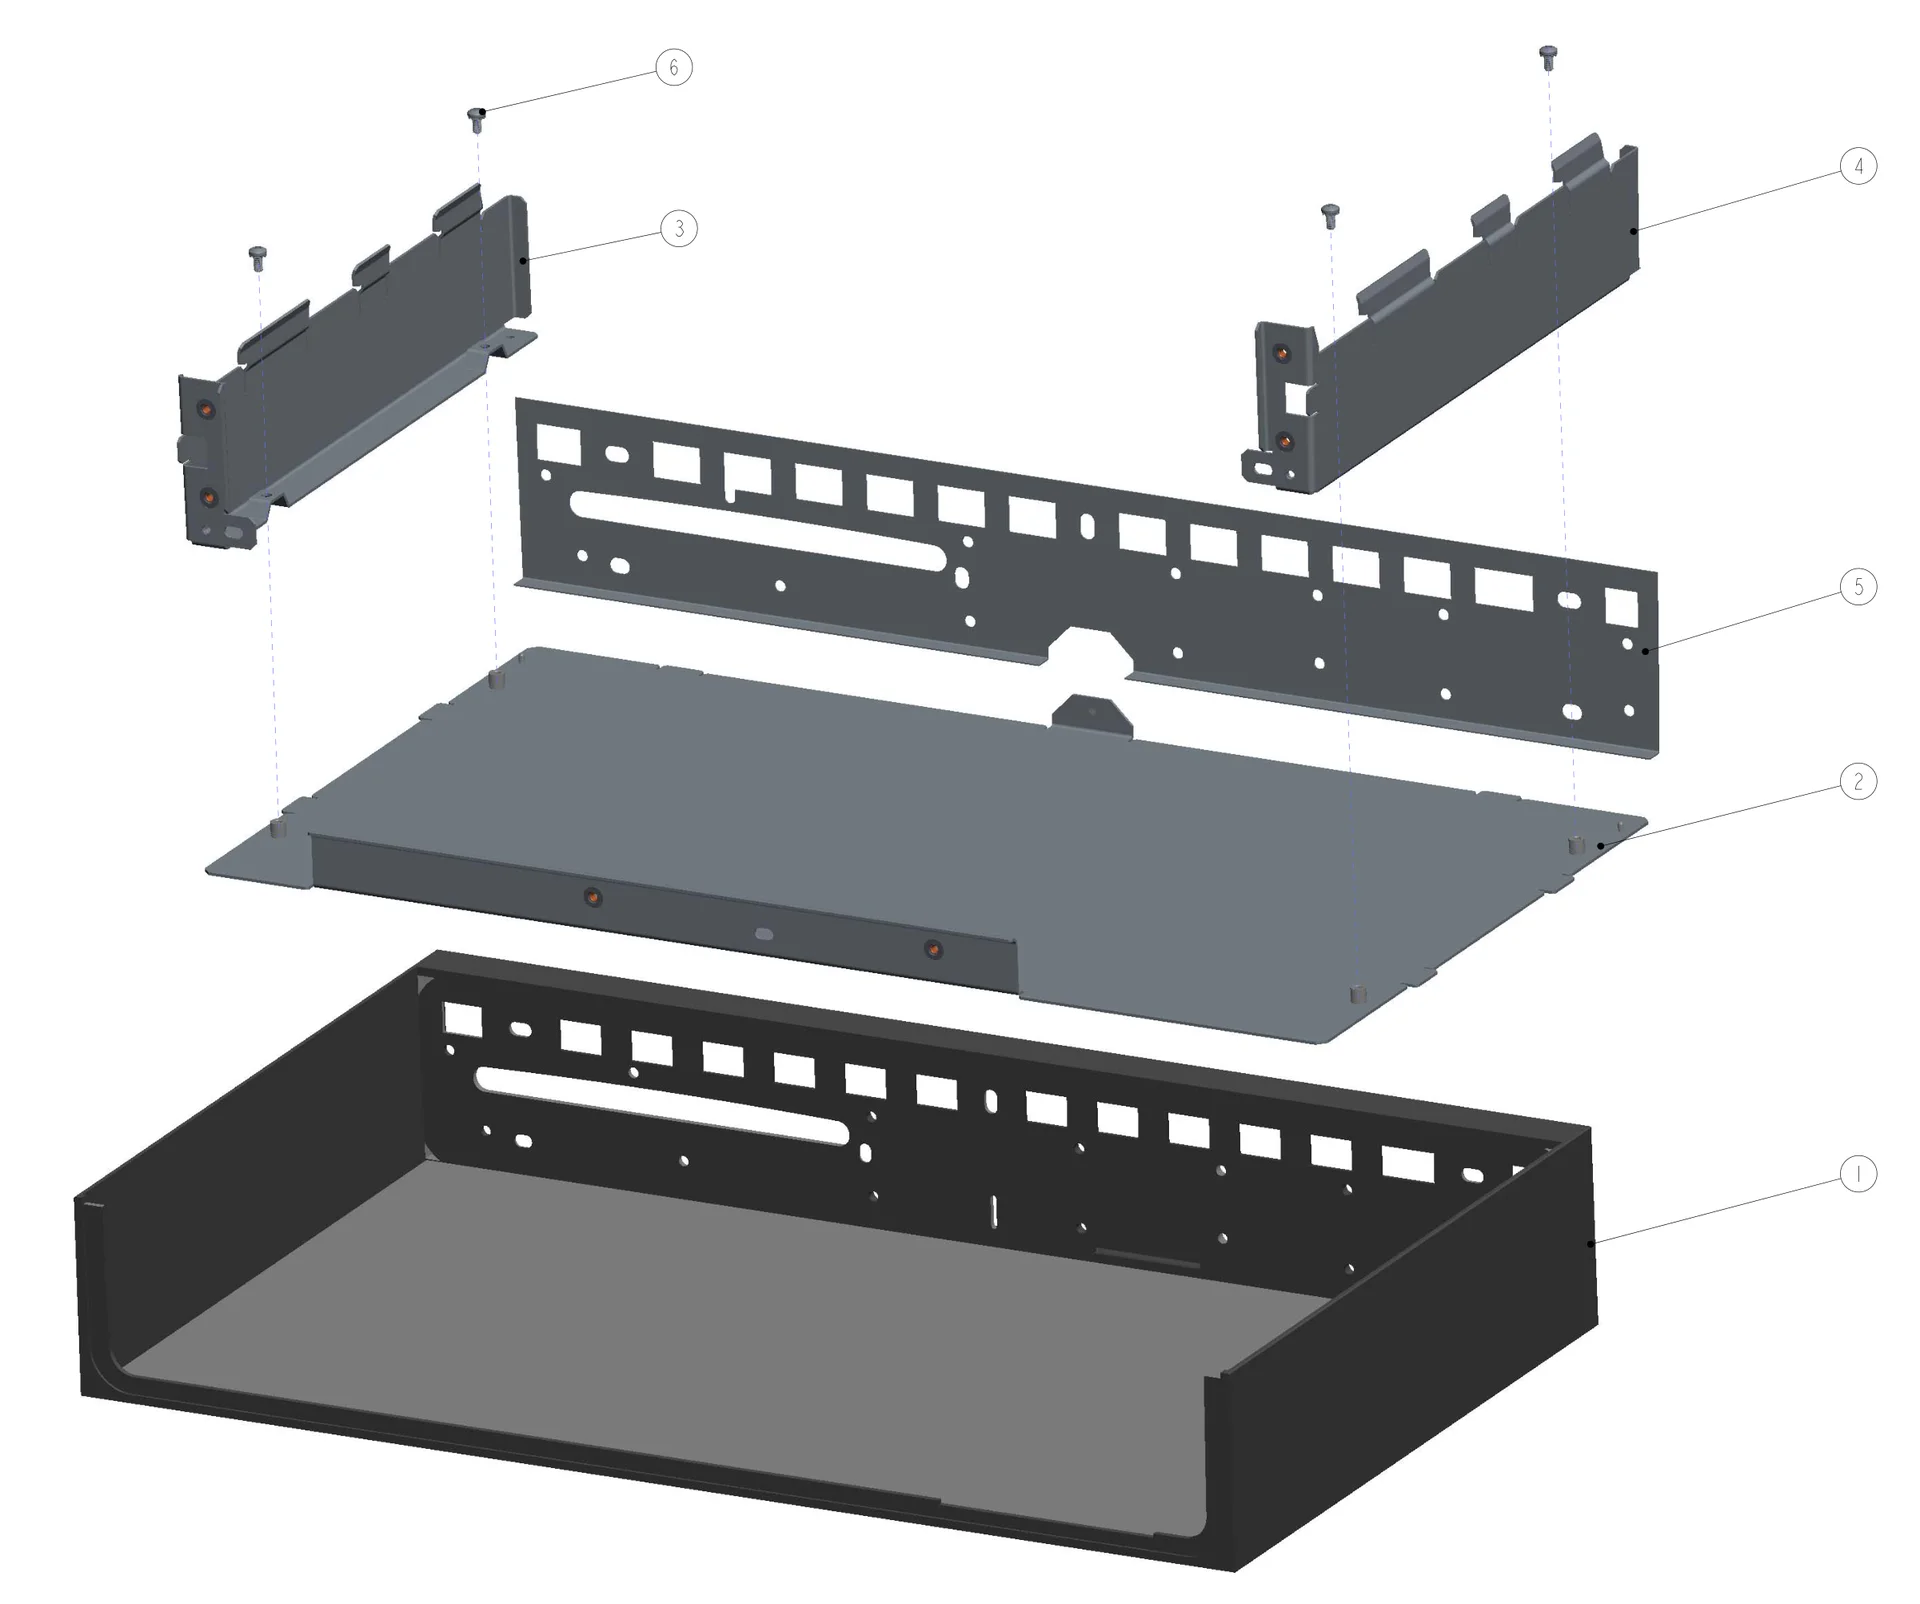
These photographs from my April 2013 build show the preparation and fitting of the reinforcement, from tape placement to the metal installed inside the shell.
Bonding the metal into the plastic
April 22, 2013 photographs of the assembly preparation.
Building the units and the assembly process
April 2013: building units and documenting the process together.
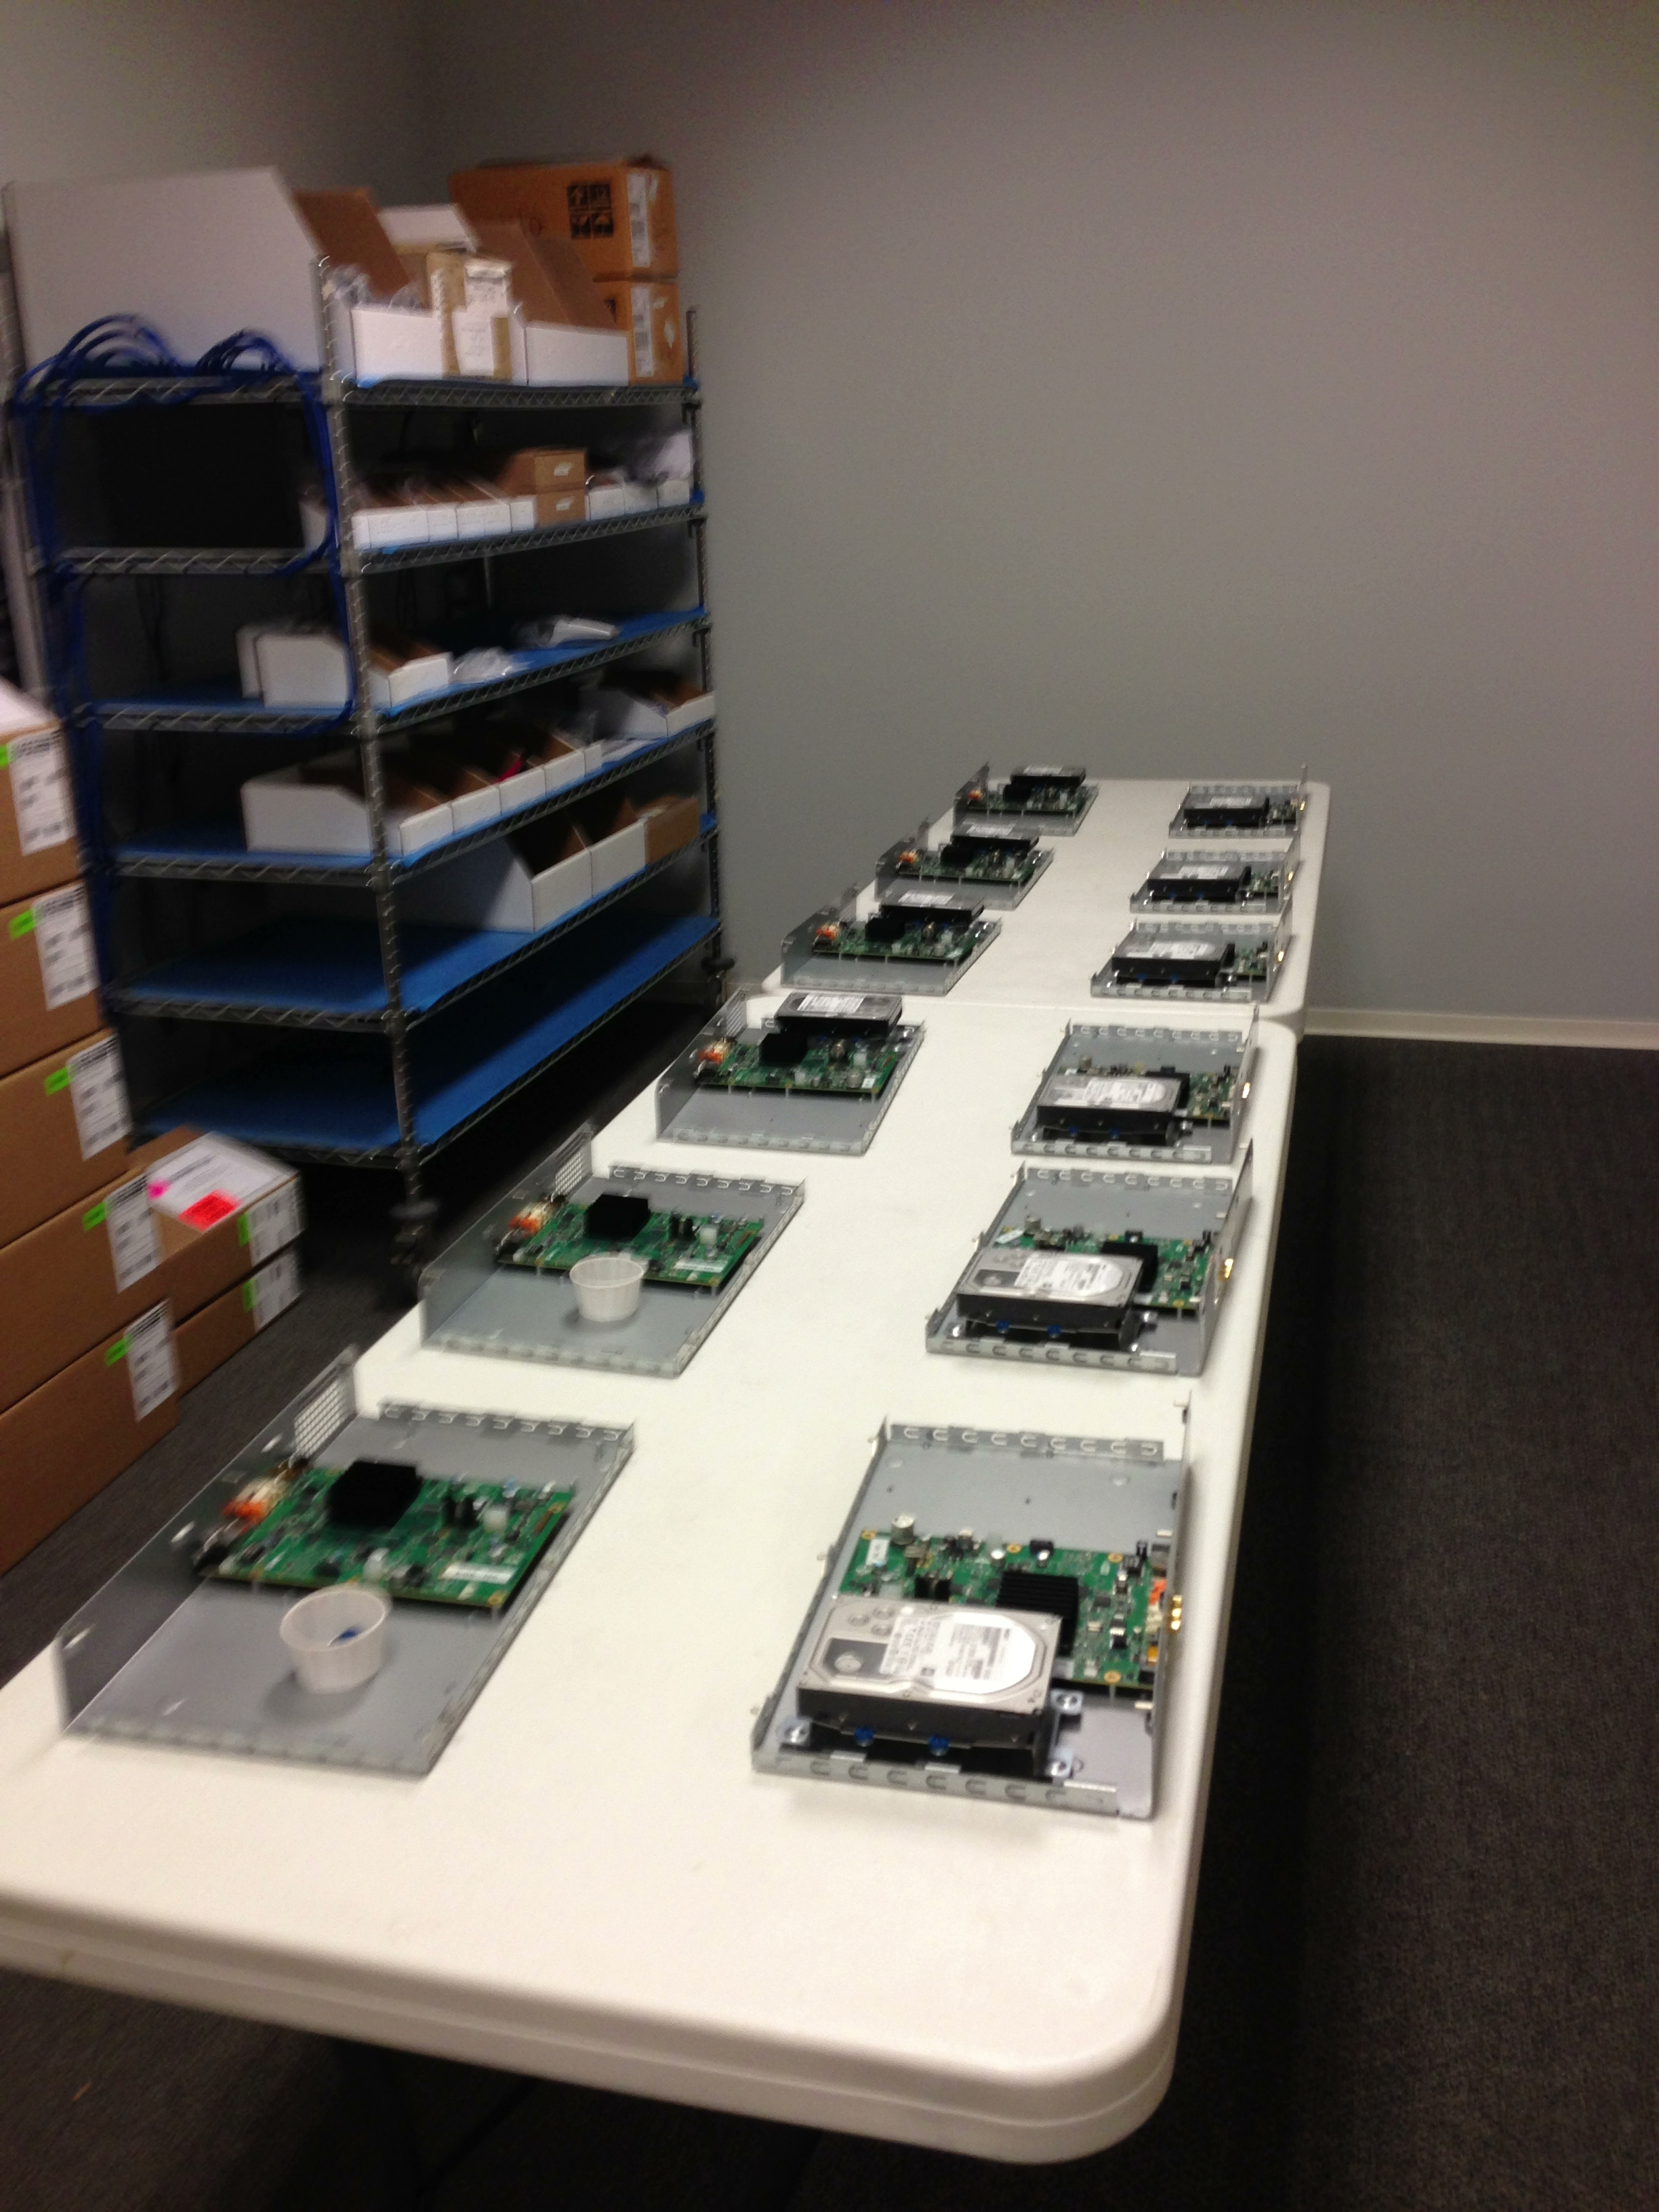
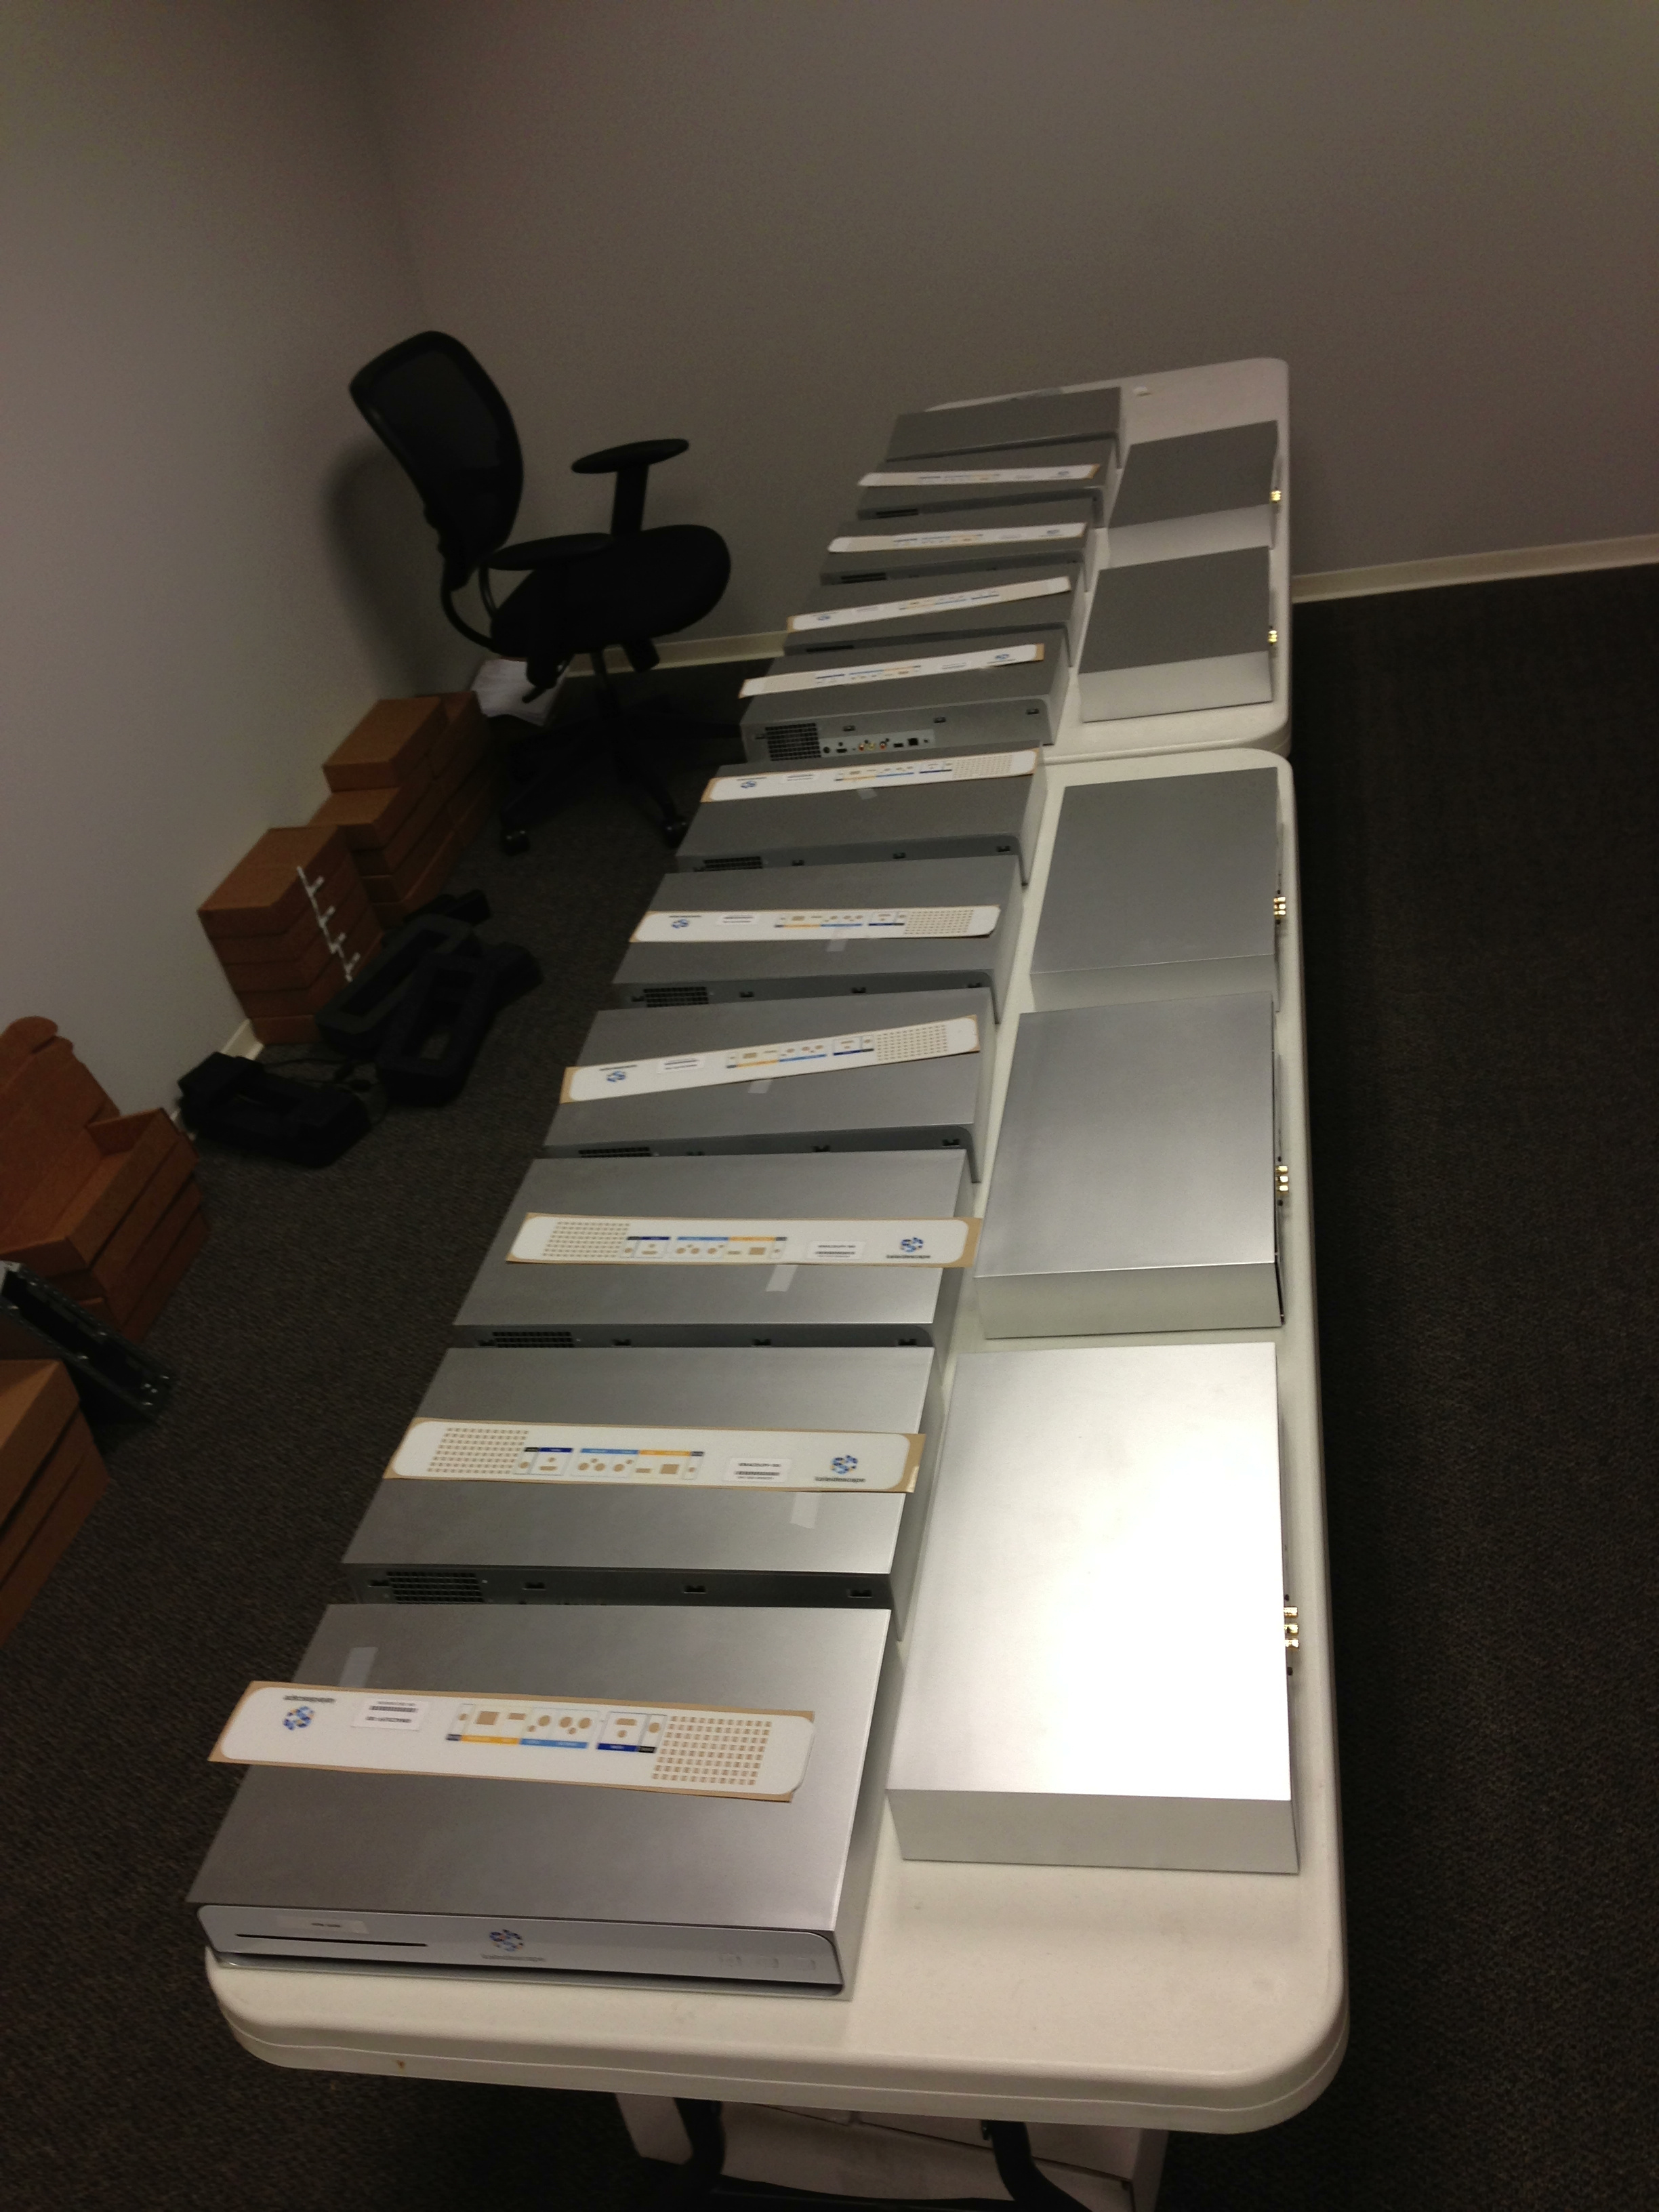
Building the units was also how I developed the assembly process. I carried out my personal pilot build at HQ while the contract manufacturer was not yet online. As I built, I documented the assembly, produced the assembly procedure and workmanship documents, and set up inline QC checks and inspection criteria.
Handling the build at HQ let me do that work together and avoid the logistics and time of bringing up a line at that stage. The photographs below show stages of the build in April 2013.
My personal pilot build
April 2013: units at several stages of assembly.
Refining the production parts
Summer-autumn 2013: sample feedback, production introduction and continuing refinement.
Prototype drawing releases began in October 2012, followed by production drawing releases and Cinema One's July 2013 introduction. Assembly-document revisions continued through the year, covering fasteners, torque instructions and EMI-gasket placement. My responsibility extended through this work of getting the mechanical product built.
Physical samples exposed details that the nominal geometry did not settle. In June 2013, the bezel review showed heat stakes interfering with the button tree, lower stakes failing to clamp the faceplate tightly, and inadequate retention of the IR lens. The feedback called for gate vestiges and inserts to sit below the mating surface so the decorated face could seat against its frame.
The IR lens was one small part of that refinement. I added an internal bounce rib in the June 9, 2013 drawing revision and relocated it in the August 7 revision. The detail changed within the existing lens and front assembly.
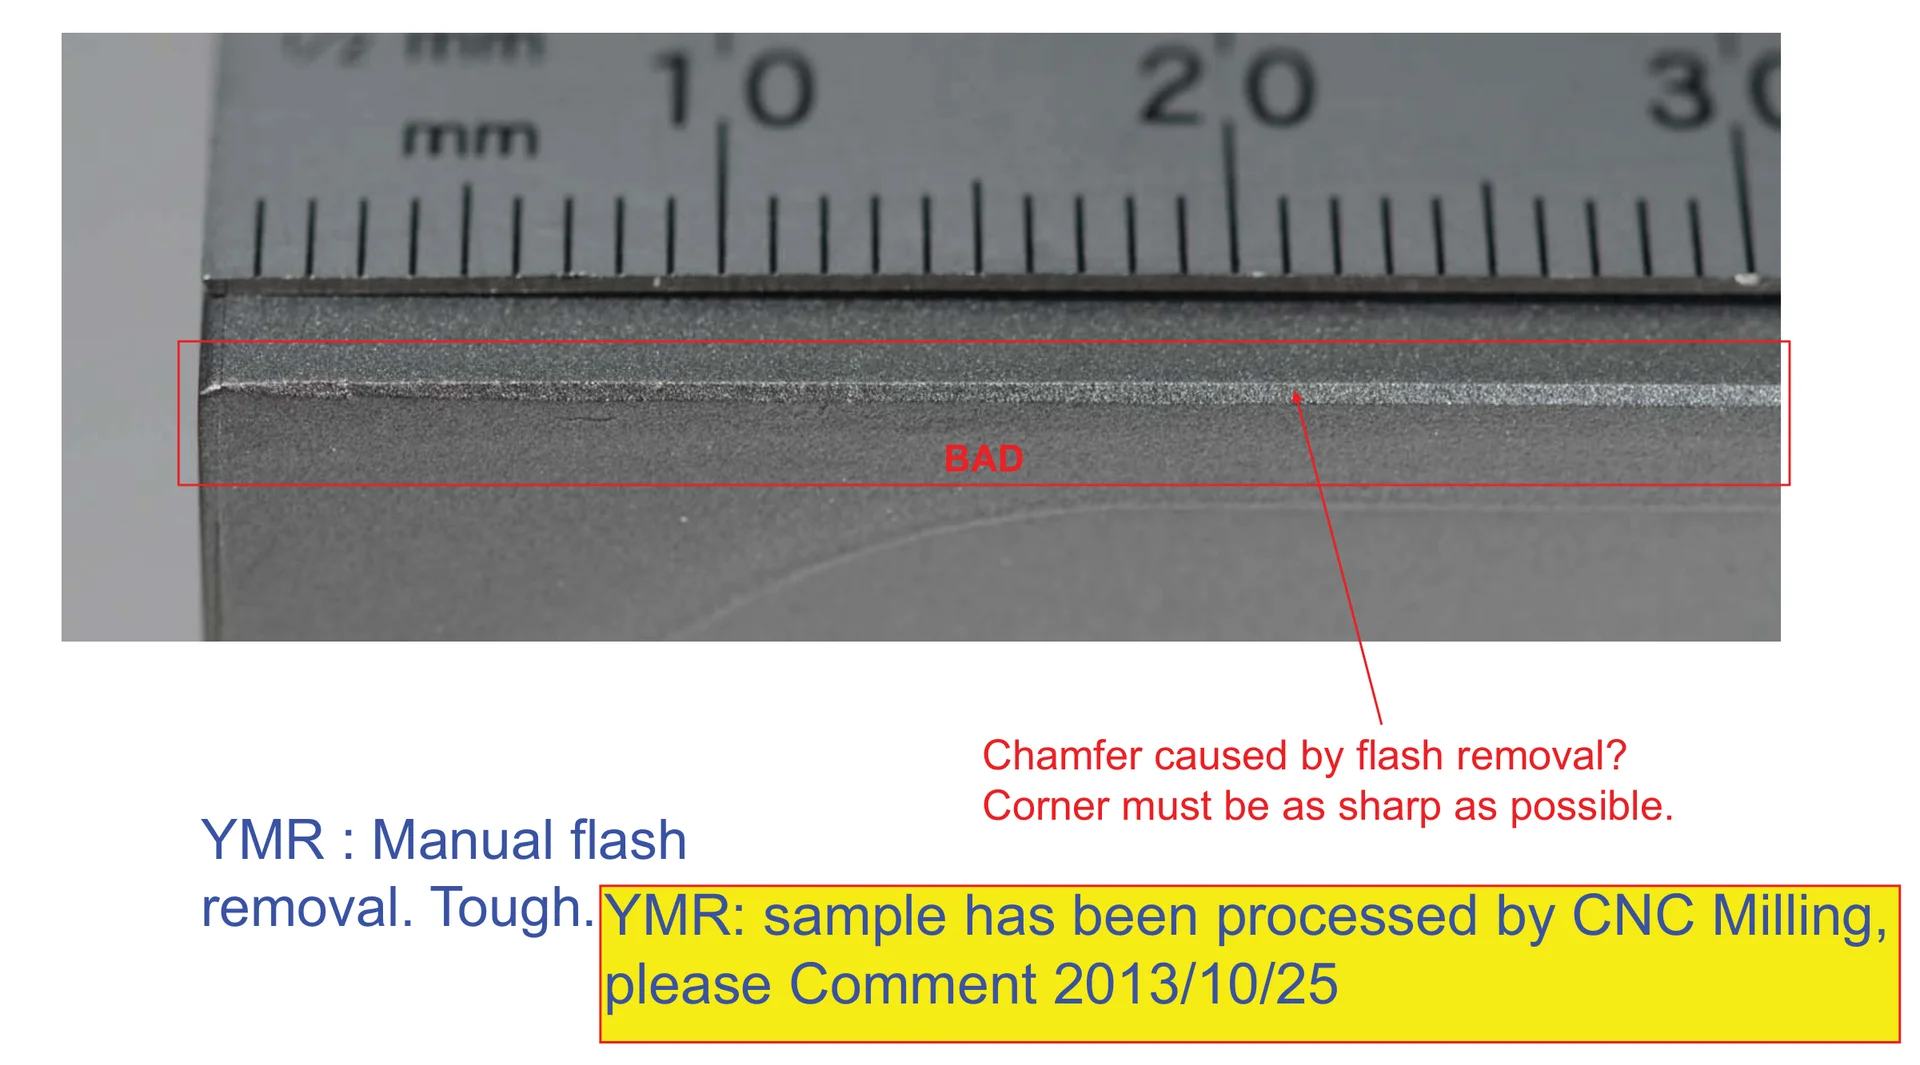
The cover also needed attention after molding. A 2013 sample-feedback photograph questions whether flash removal had chamfered an edge that needed to remain sharp. Yomura's annotations describe difficult manual trimming and report a CNC-milled sample on October 25. Photographs made the edge condition and the supplier's proposed process work concrete enough to review together.
Reviewing the trimmed edge, 2013
Following the assembly into 2014
2014: practical checks, assembly instructions and disc-slot follow-through.
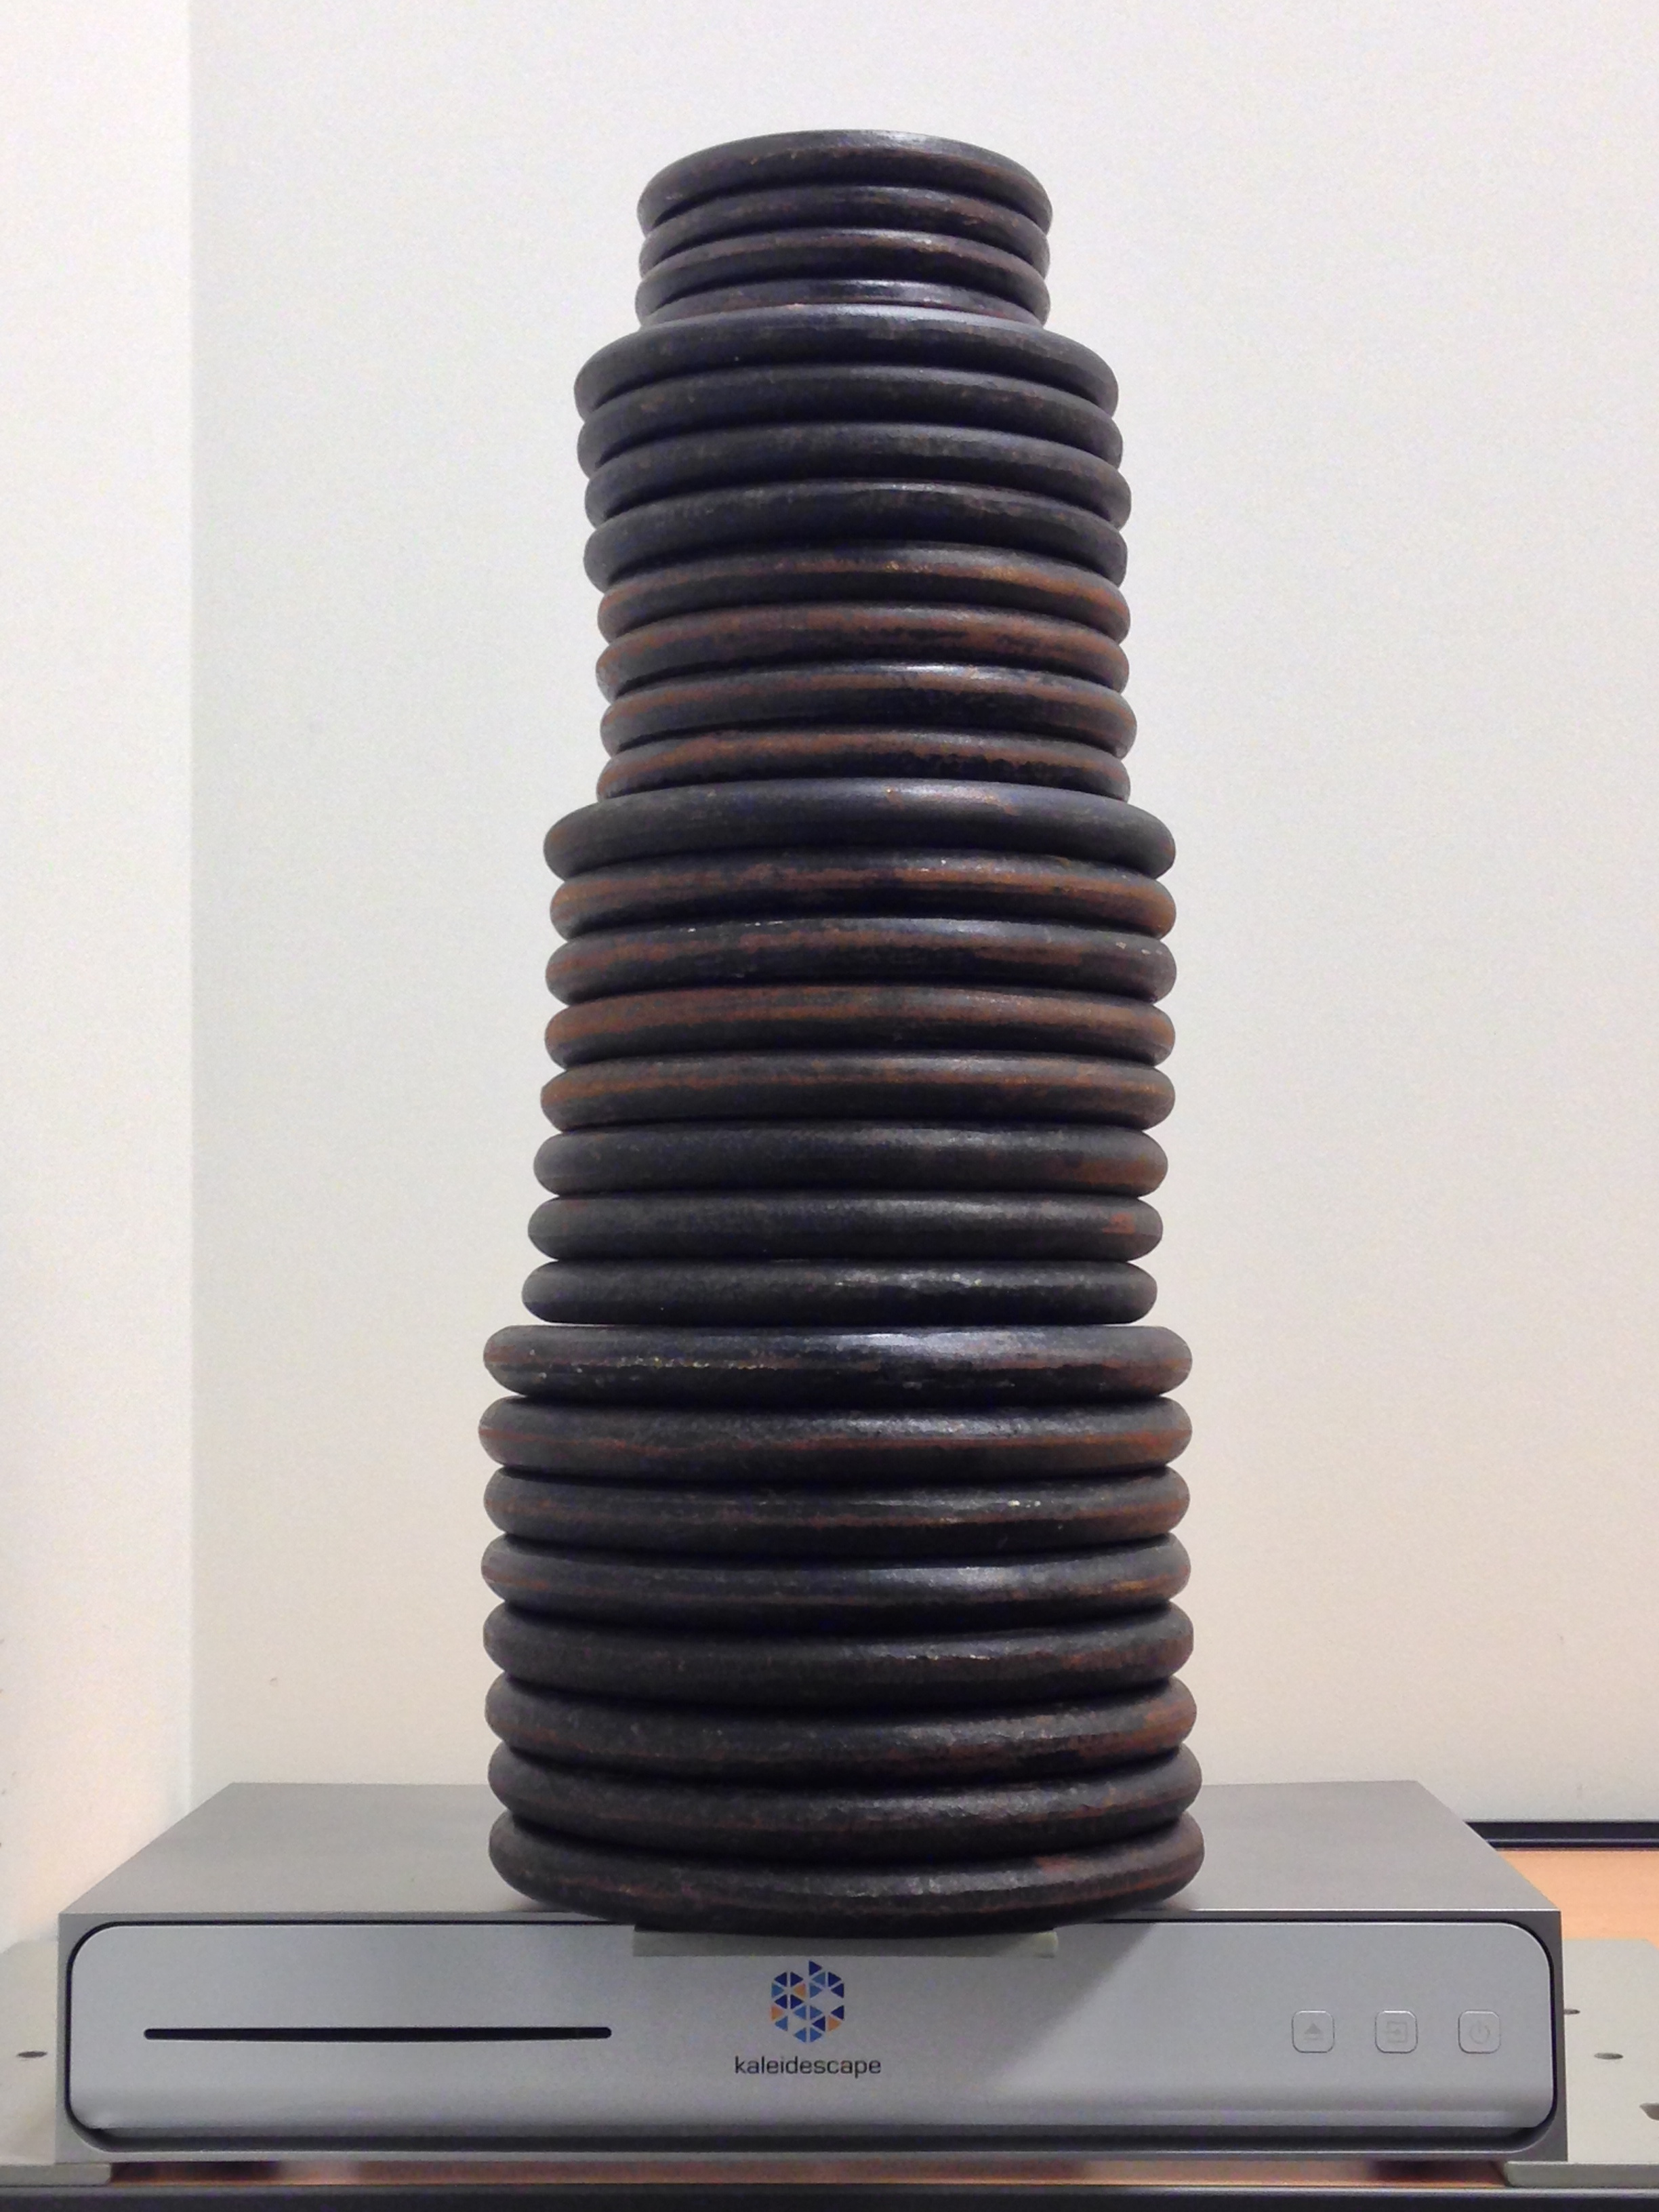
For one practical load check, I broke down my dumbbells at home and brought in 190 lb of plates. The idea was a rough stand-in for something like a technician or installer standing on the unit. I stacked the plates on the enclosure and left it loaded overnight for about ten hours, with no visible deflection. This was an informal practical experiment.
An overnight load check
An informal practical test with weights from home.
The reinforcement depended on a repeatable bond between the metal and plastic. The later assembly instructions, at Revision 9, specified cleaning and different adhesion treatments for the two surfaces, followed by controlled tape placement and pressure. Rollers and a fixture pressed the bonded surfaces together; the side stiffeners had their own clamp arrangement.
By June 2014, Revision 9 brought the assembly method into the same documented record as the part changes.
The assembly instructions addressed the molded cover's natural bow. They specified shims to set the gaps between the cover and faceplate, and a fixture to straighten the cover and locate the bezel while its mounting screws were tightened in sequence. The instructions left the mounting screws loose while the bezel was positioned with shims, then held the cover in a fixture while the screws were tightened in sequence. The procedure controlled how the parts were held together, as well as where they sat relative to one another.
The disc slot also remained an active interface. The April 2014 frame drawing recorded a slot-bump addition. In June, Nathan Forster reported successful tests of modified samples with DVDs, Blu-rays, CDs and Dual Discs, with and without felt; tooling review and scheduling remained next. In July, I loaded a slot-bump modification for the frame assembly into Arena. The sample tests and file update record steps in the work, rather than a confirmed tooling-completion date.
Developing the finish
2014: carrying the appearance standard into factory inspection.
The decoration work continued after launch. In September 2014, Nathan Forster reviewed new-ink front-panel and button foils and reported appearance defects. His review used photographs to make the defects explicit and requested Nissha's own yield data.
The machined-aluminum appearance depended on the coating as well as the enclosure geometry. I evaluated processes and coating types, and created a workmanship guide that the supplier used to make acceptable product.
The pigment should have been distributed evenly through the coating across the whole surface. Instead, it built up and swirled, leaving all sorts of variation and "patina."
I wanted the factory to have a common visual reference for judging the finish. In October 2014, I cut ten top covers so I could photograph the bend surface straight on. The depth of field was narrow, so keeping that surface parallel to the camera sensor mattered.
Photographing the defect, 2014
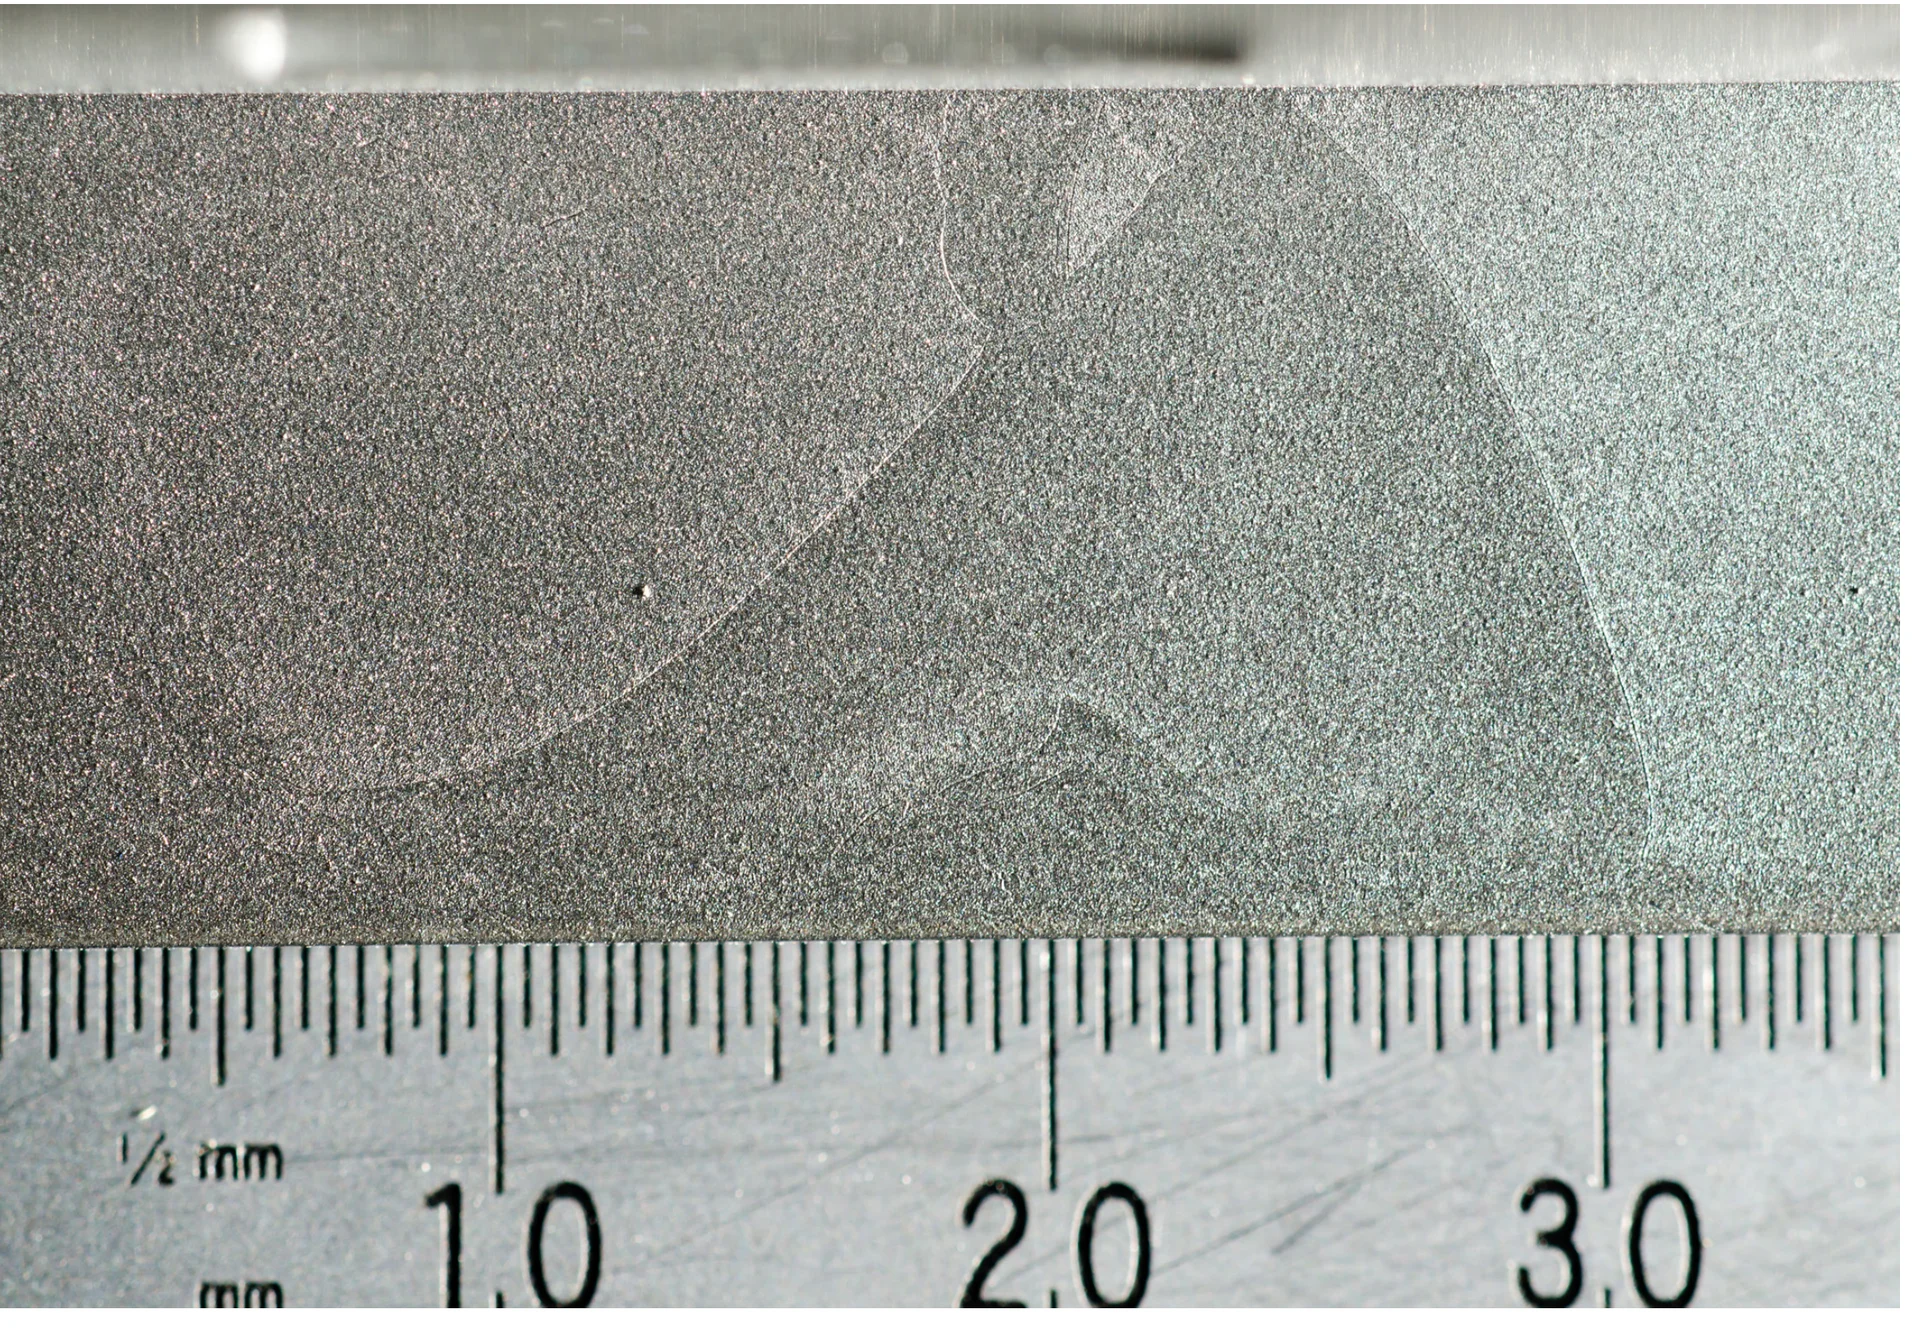
I photographed a range of defects and asked colleagues to vote on numbered pass/fail examples. Mark McKenzie, Nathan Forster and Rob Wudrick participated in the review. I reordered and renumbered the examples, then asked whether I could release the document to Sanmina. Mark approved the release; subsequent factory correspondence called for further inspection against the updated deviation.
I loved the way it turned out: the aluminum-like rectangular mass and the floating front bezel.