Glyph
Getting it into production
Glyph put a personal display inside a pair of headphones. Lower the headband to watch; raise it to listen.
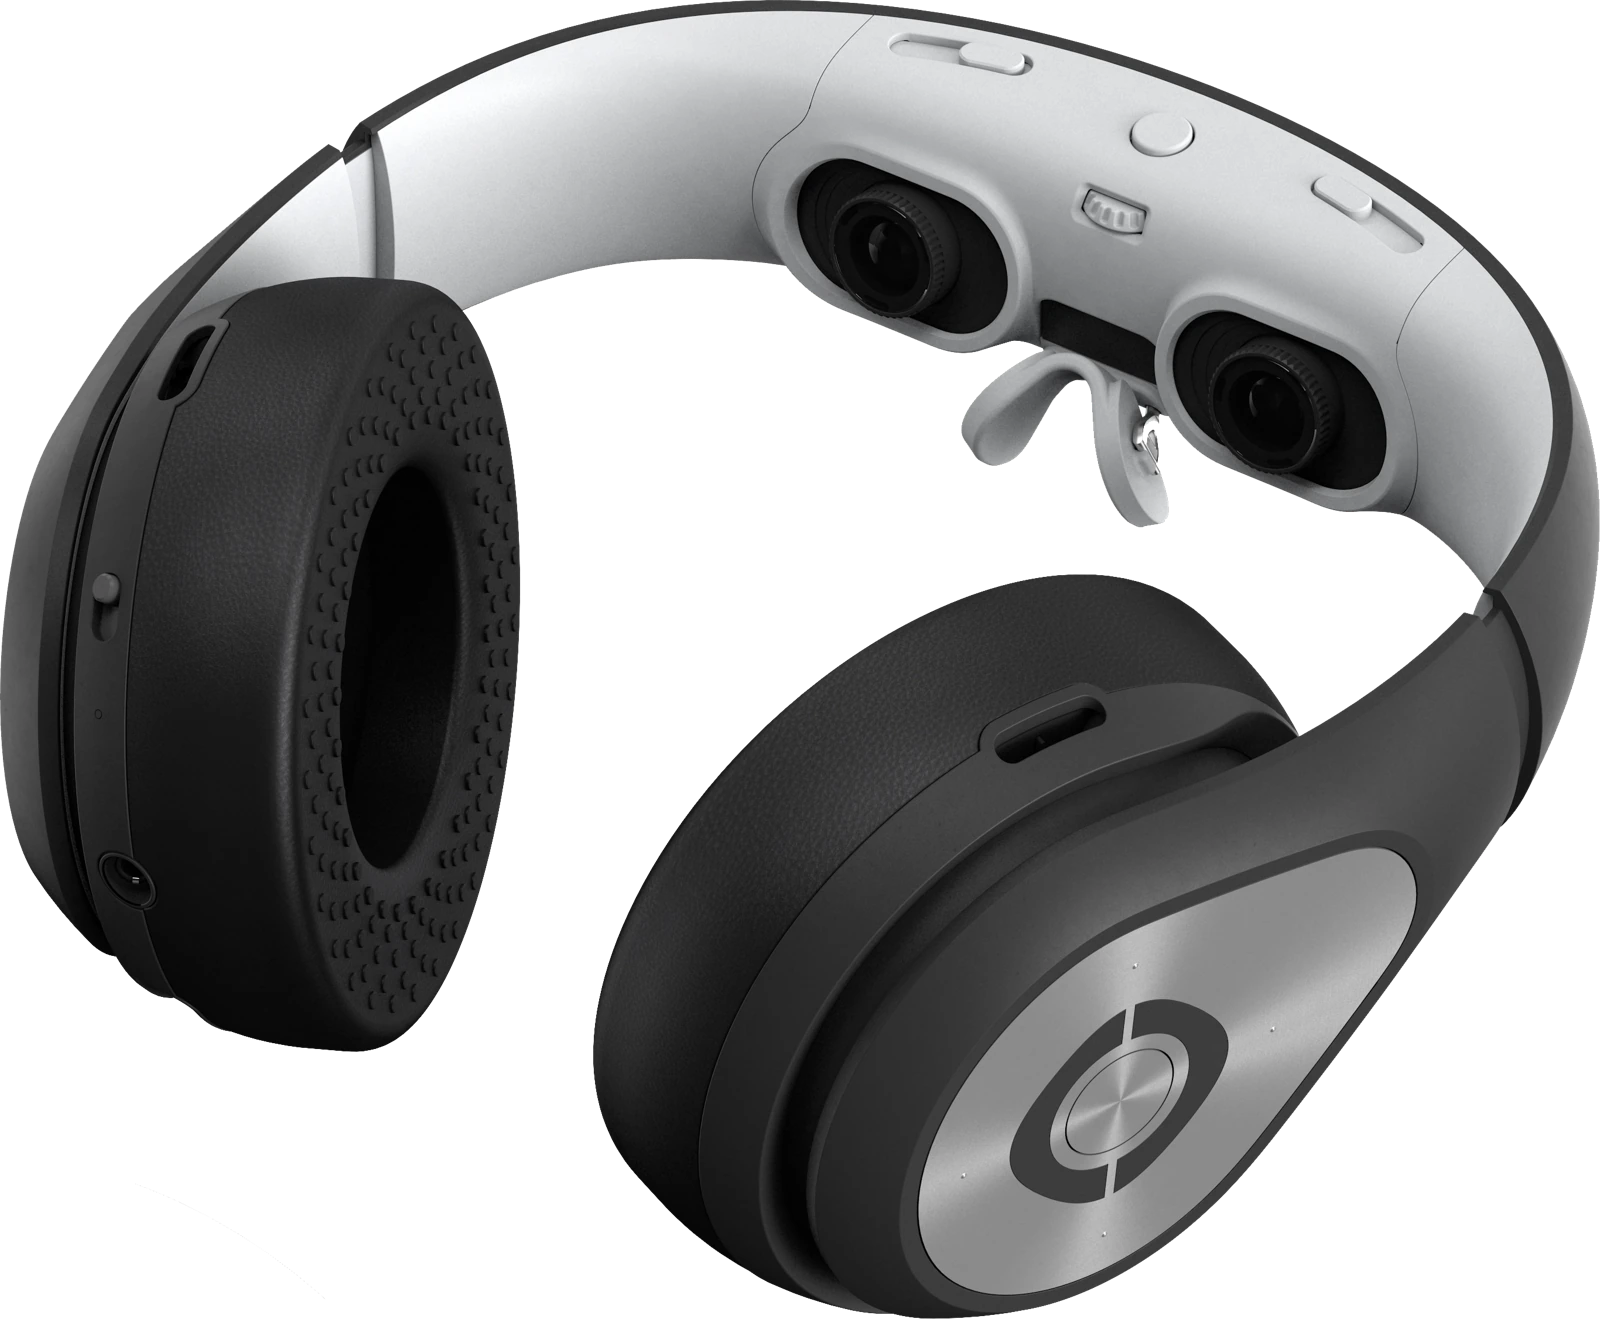
I joined with Kickstarter deliveries already overdue and took responsibility for the whole mechanical bill of materials through tooling, validation and production ramp, including roughly 40 tools.
Across the assembly, I worked through cable binding and abrasion, dust contamination, fit and field failures. I recovered the difficult outer-headband molding process through a hot-runner conversion and process tuning around as-molded part weight.
I developed the headstrap and earpads to improve comfort. I designed the assembly fixtures, created the master color, gap and graphics plans, wrote critical-part inspection and acceptance criteria, and designed and managed the product’s reliability testing program.
Glyph shipped, and Avegant reported Kickstarter fulfillment complete in June 2016. My work continued through the ramp as testing, production builds and customer returns exposed the next problems to solve.
Joining Avegant
Richard Lane, my former boss at Kaleidescape, recommended me to Joerg Tewes, Avegant's CEO. I joined on July 20, 2015, as a Senior Mechanical Engineer to help get Glyph into production and get its overdue Kickstarter deliveries moving. Glyph was the main reason I was hired and became the bulk of my work there.
Glyph combined headphones and a personal display in a 434 g (15.3 oz) headset. Lower the band across your eyes and it became a display; raise it and it returned to headphone use. I took responsibility for the whole mechanical bill of materials: getting the plastic and metal parts, springs, cables, pads and their interfaces through tooling validation and production ramp. Color, material, finish, print and graphics were part of that responsibility too.
An overdue Kickstarter commitment
Before I joined, I looked into the overdue Kickstarter deliveries and the growing backer frustration. The product design was established, but there was still a lot of work between that design and reliable production. I was coming in to help close that gap.
The campaign had raised $1,509,506 from 3,331 backers. The original hardware reward was a beta headset, estimated for December 2014; Avegant subsequently committed to delivering a consumer product instead. When I arrived, that original delivery estimate was already seven months past.
I worked on as many fronts as I could at once. Assembly and fit, cable binding, dust contamination, liner behavior and comfort could all hold up shipment. Pilots and production builds exposed some problems; testing, people wearing the product and customer feedback exposed others. A change to one part had to work within the rest of the assembly, be practical for the supplier to make, and go through the validation it needed. That work continued as production ramped and deliveries began.
It was pandemonium. Testing, supplier questions, tooling changes and production problems were all moving at once. I had a lot of plates spinning, moving between the immediate build problems and the changes needed for the next round.
Fitting two optical engines into the headband
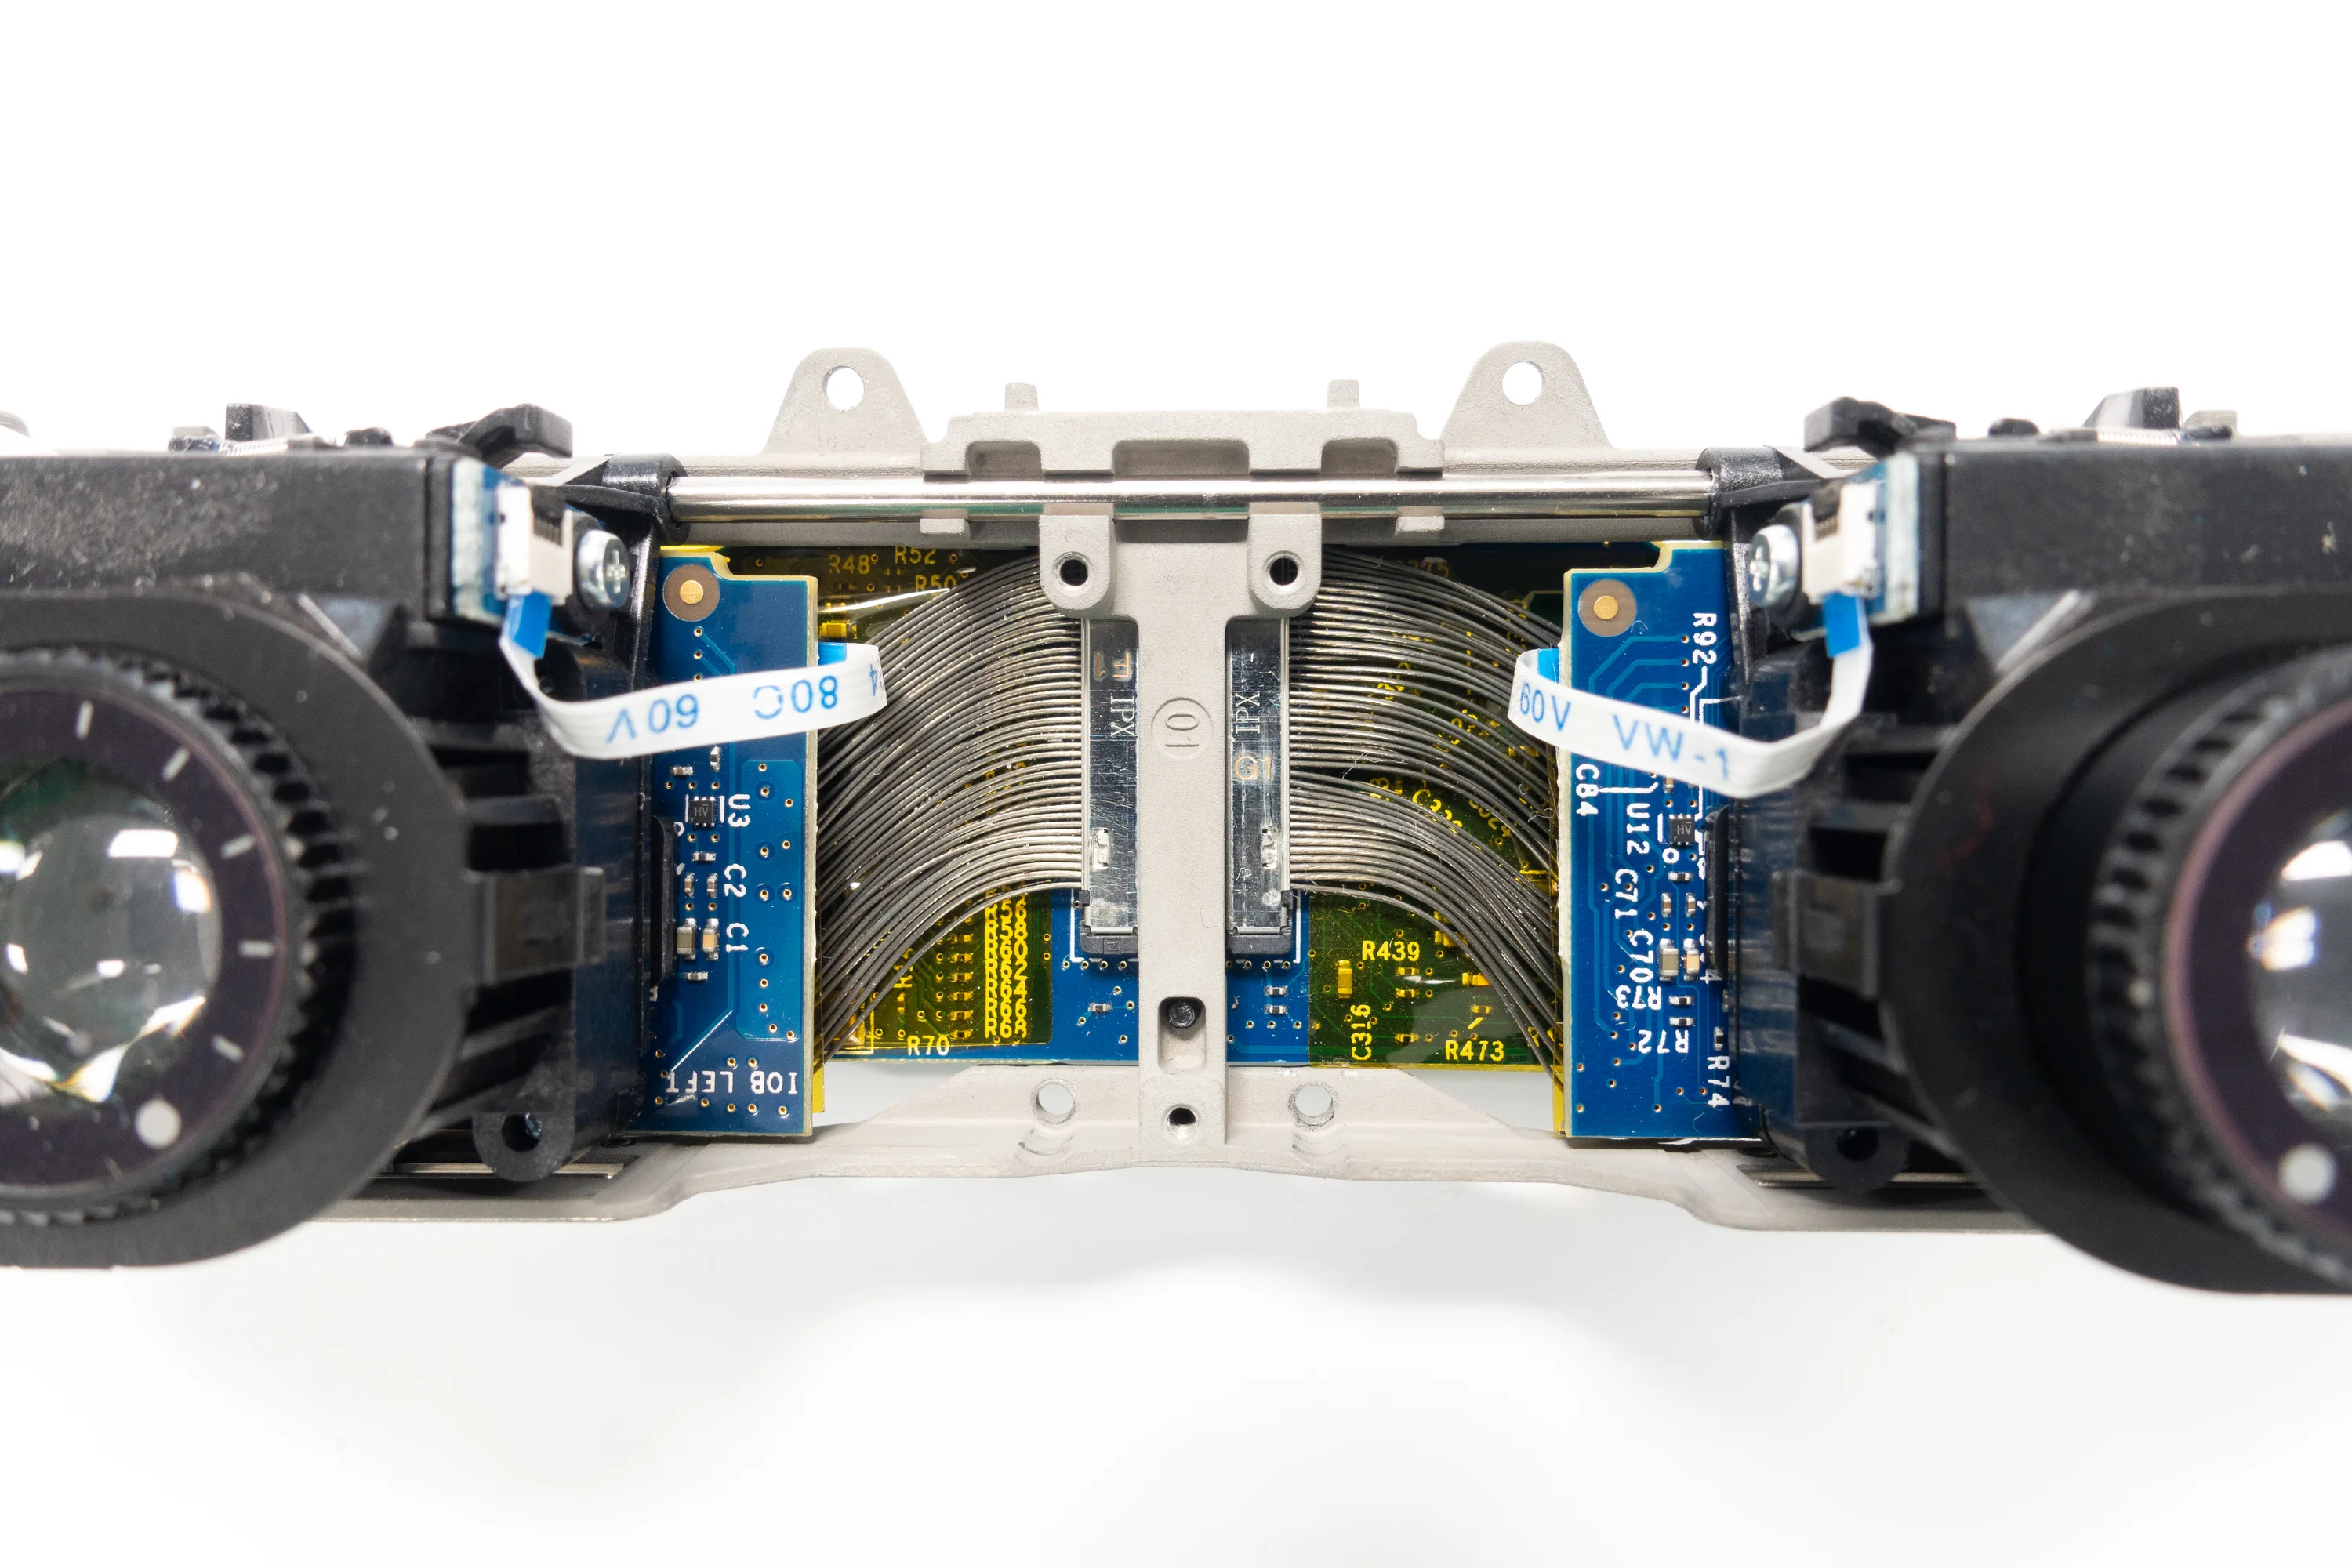
For my mechanical work, the challenge extended from the optical assemblies to the person wearing them. Within each engine, the DMD, illumination optics and eyepiece had to maintain their geometry. The two engines also had to stay aligned with each other as the wearer adjusted their spacing, or interpupillary distance (IPD). The chassis supported those relationships inside a headset that flexed, telescoped and moved between headphone and display positions.
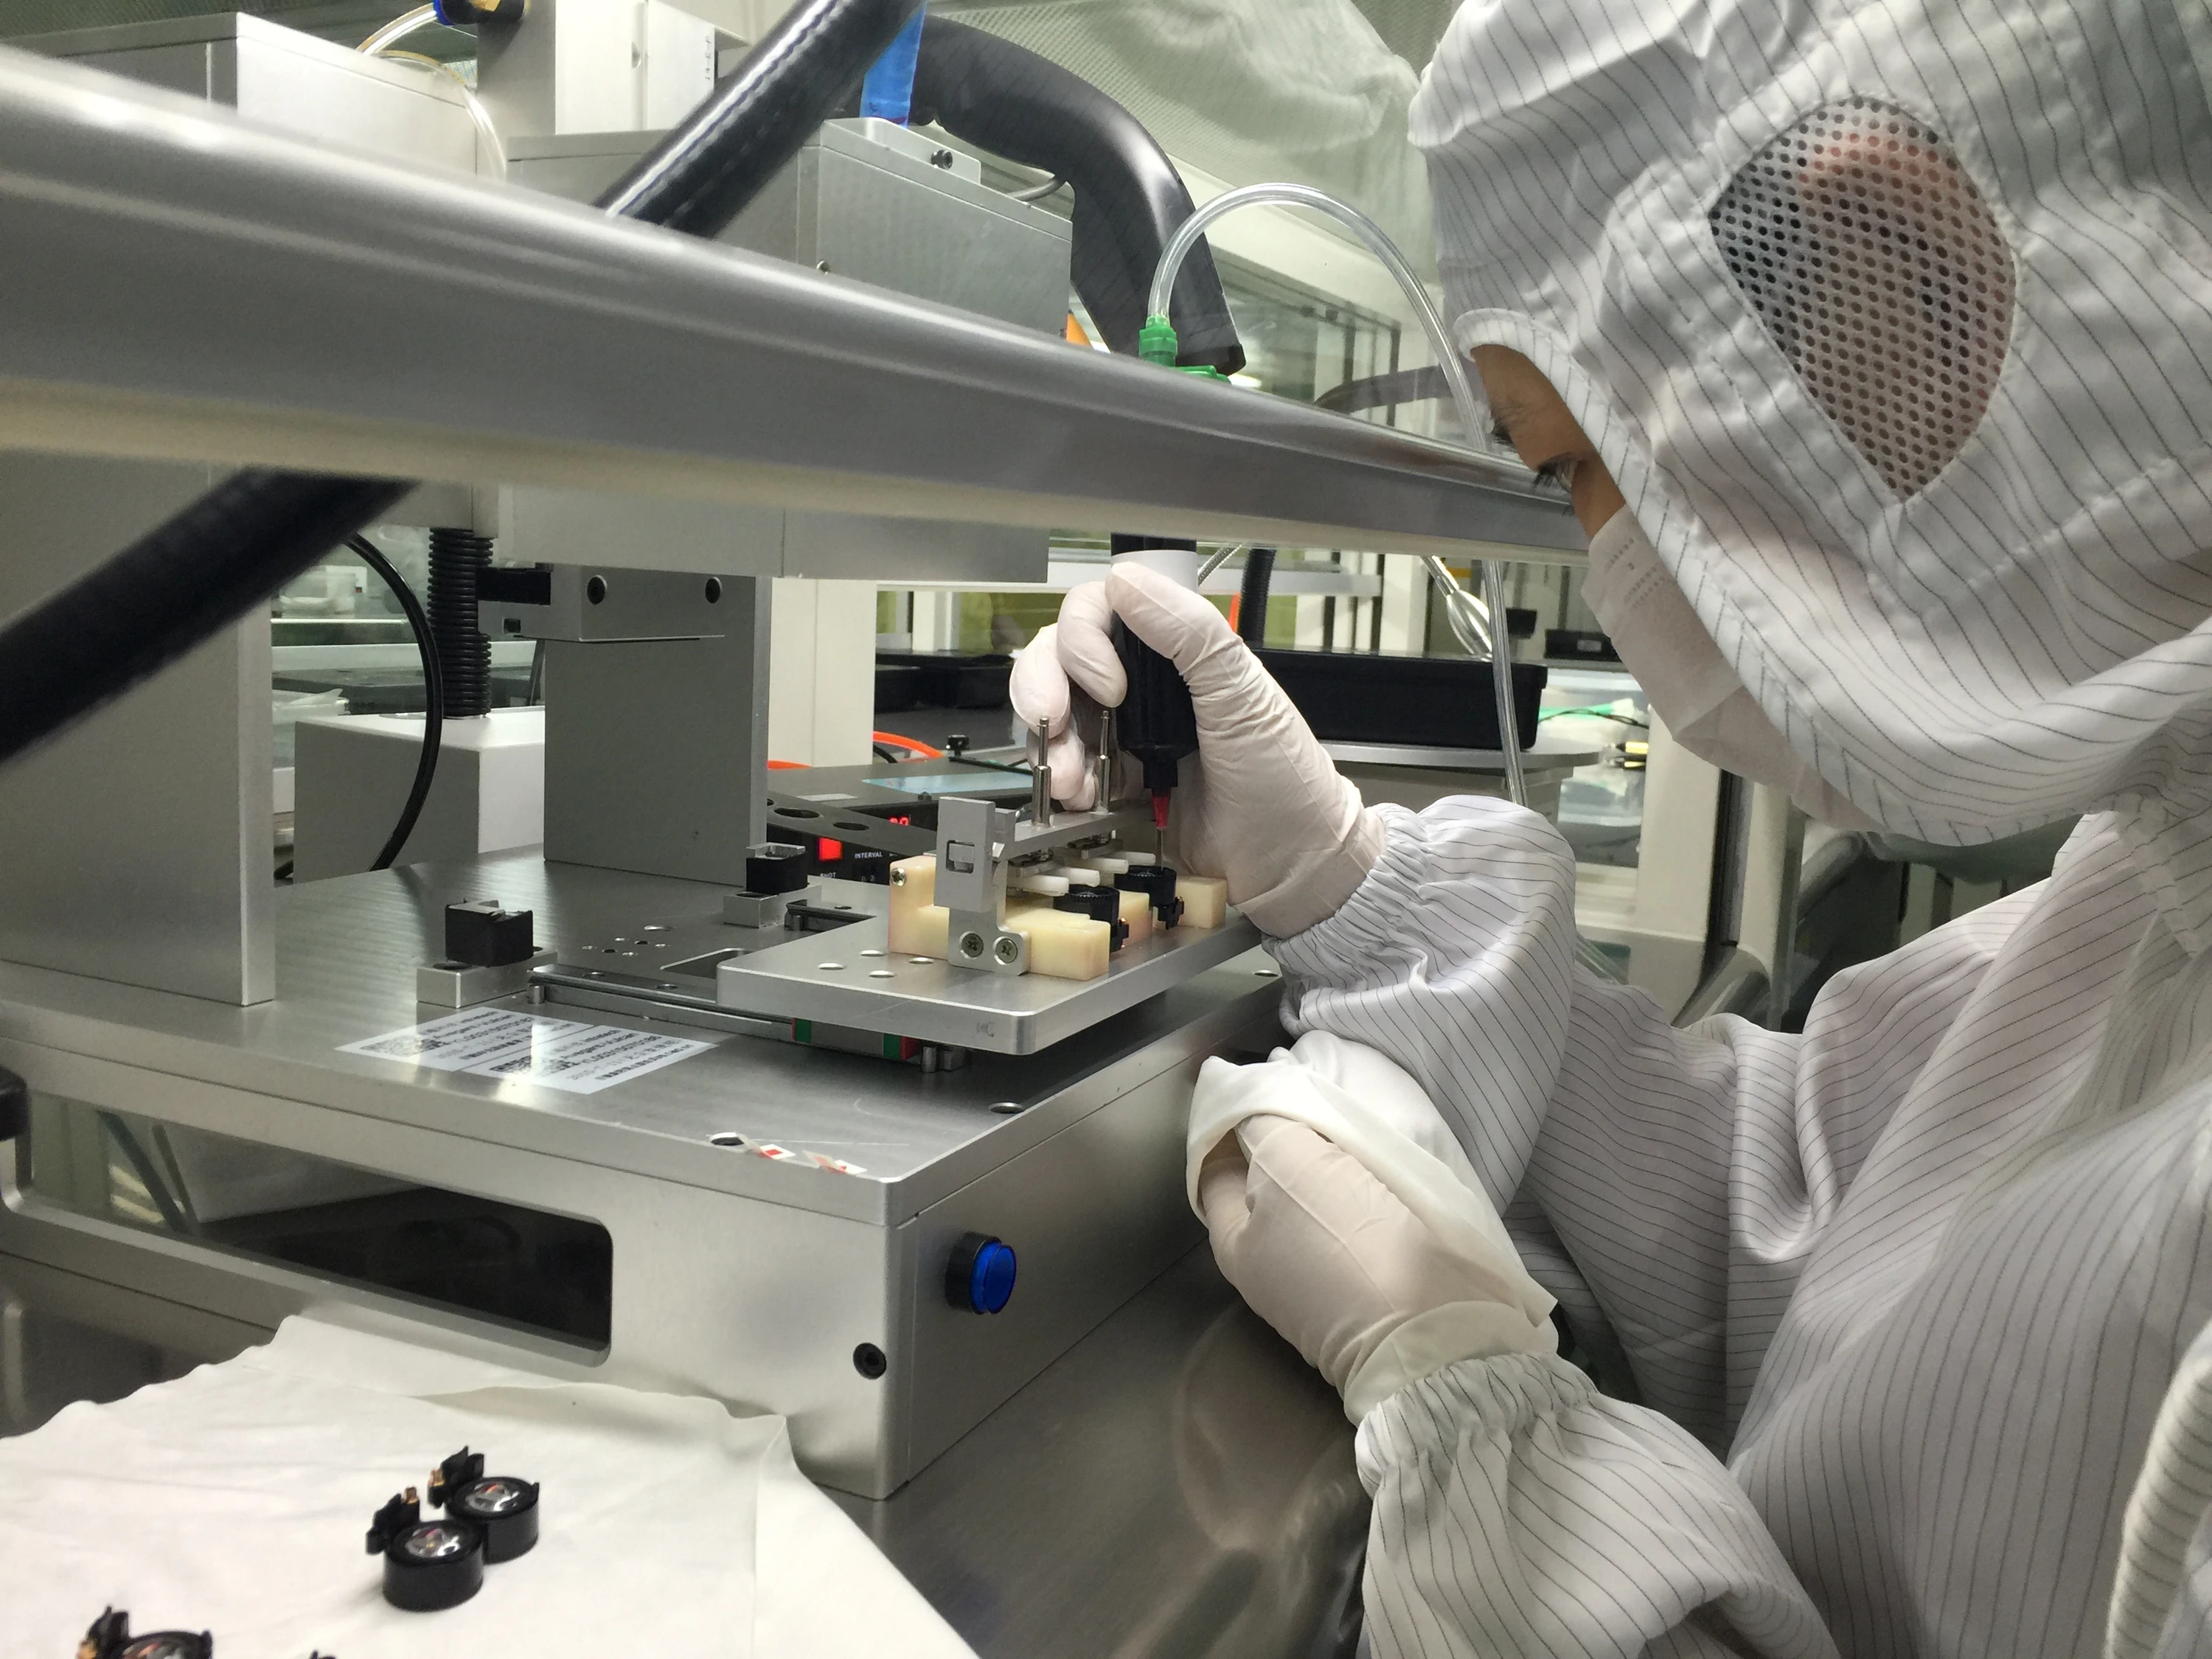
I supported the triplet-lens bonding process early in the program. Chris Westra was taking point on the optical work. I came in to fix problems in both bonding and optical inspection and alignment.
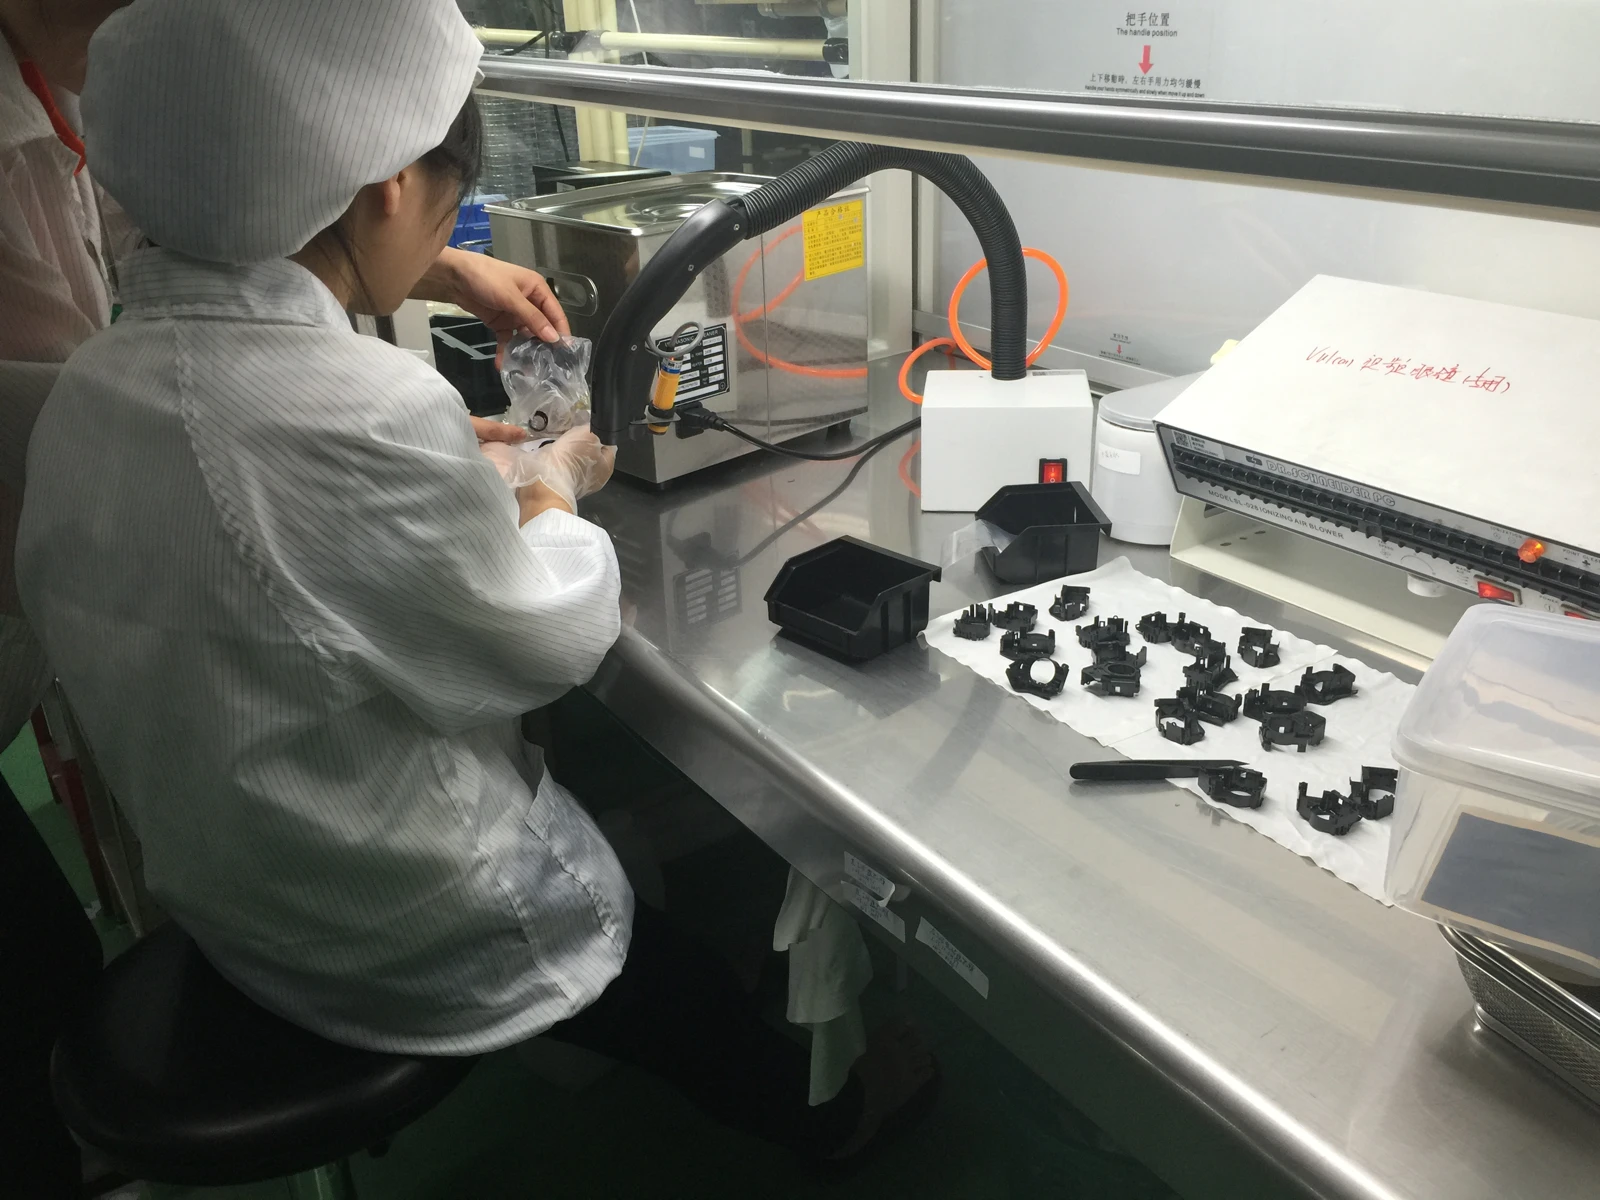 From the workbench
Lens assembly and bonding
Follow the production stations, lens work and fixtures, then look inside the optical engine.
Explore investigation +Close investigation −
Lens assembly and bonding
Follow the production stations, lens work and fixtures, then look inside the optical engine.
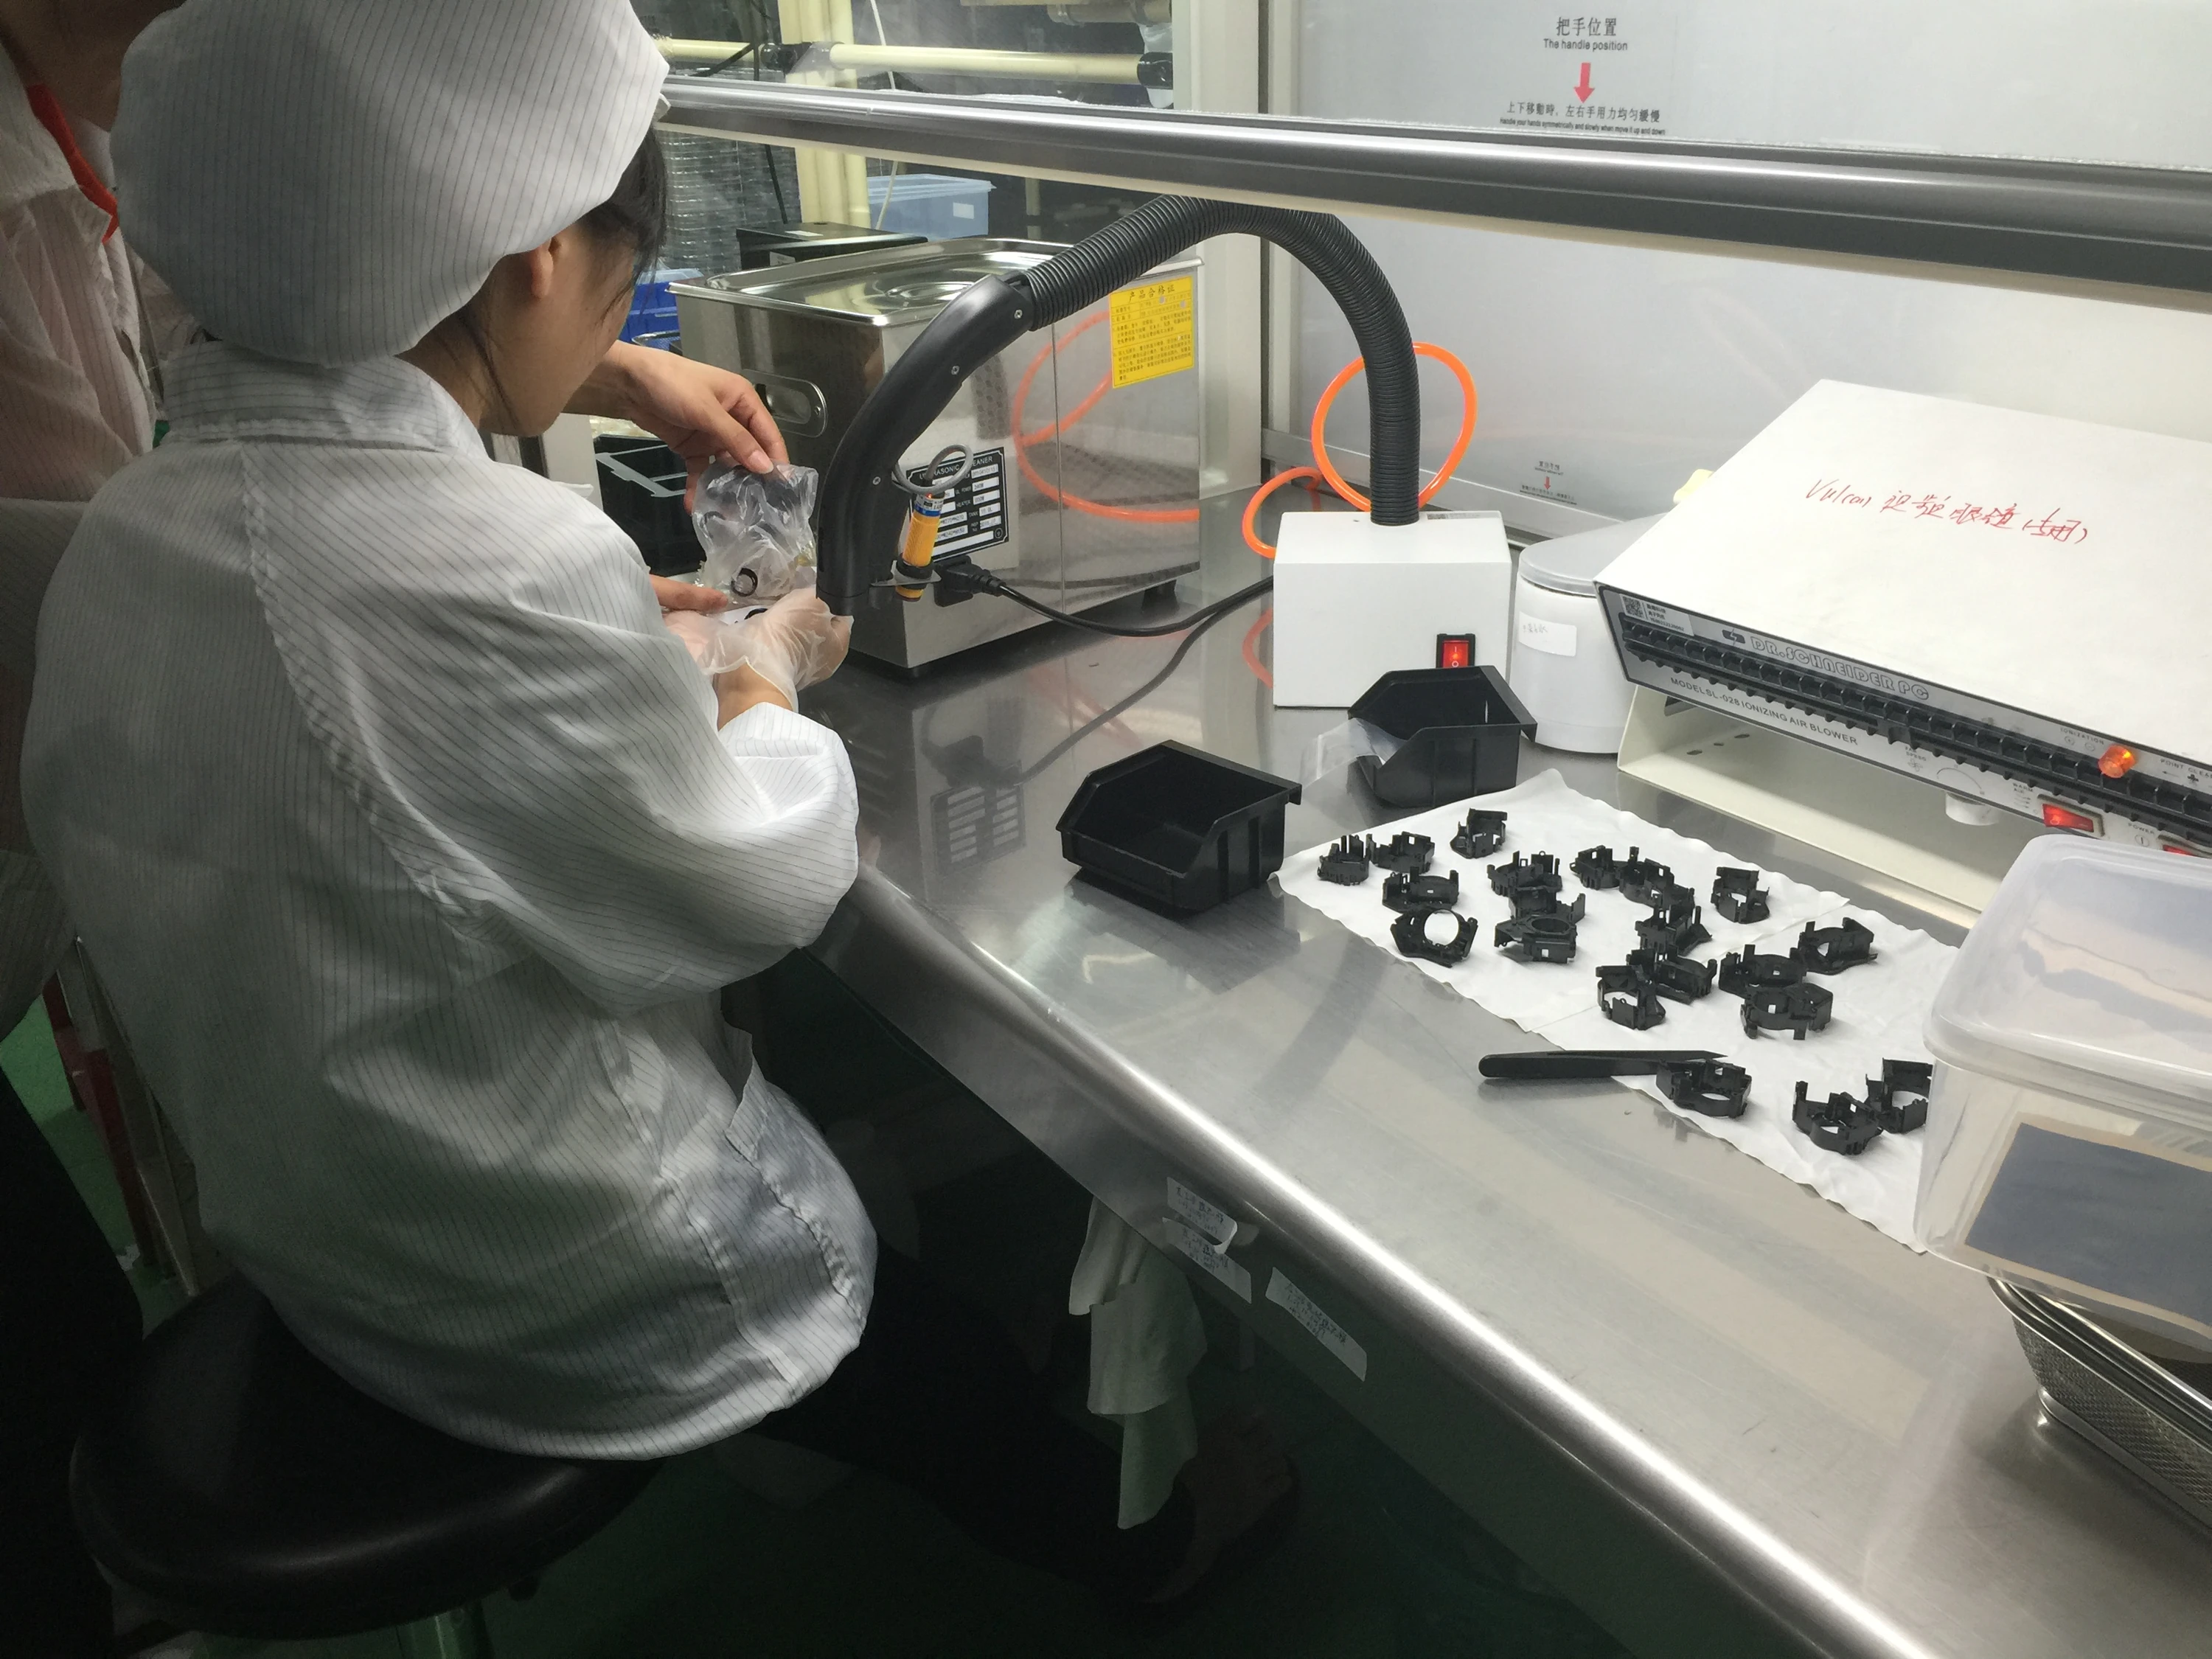
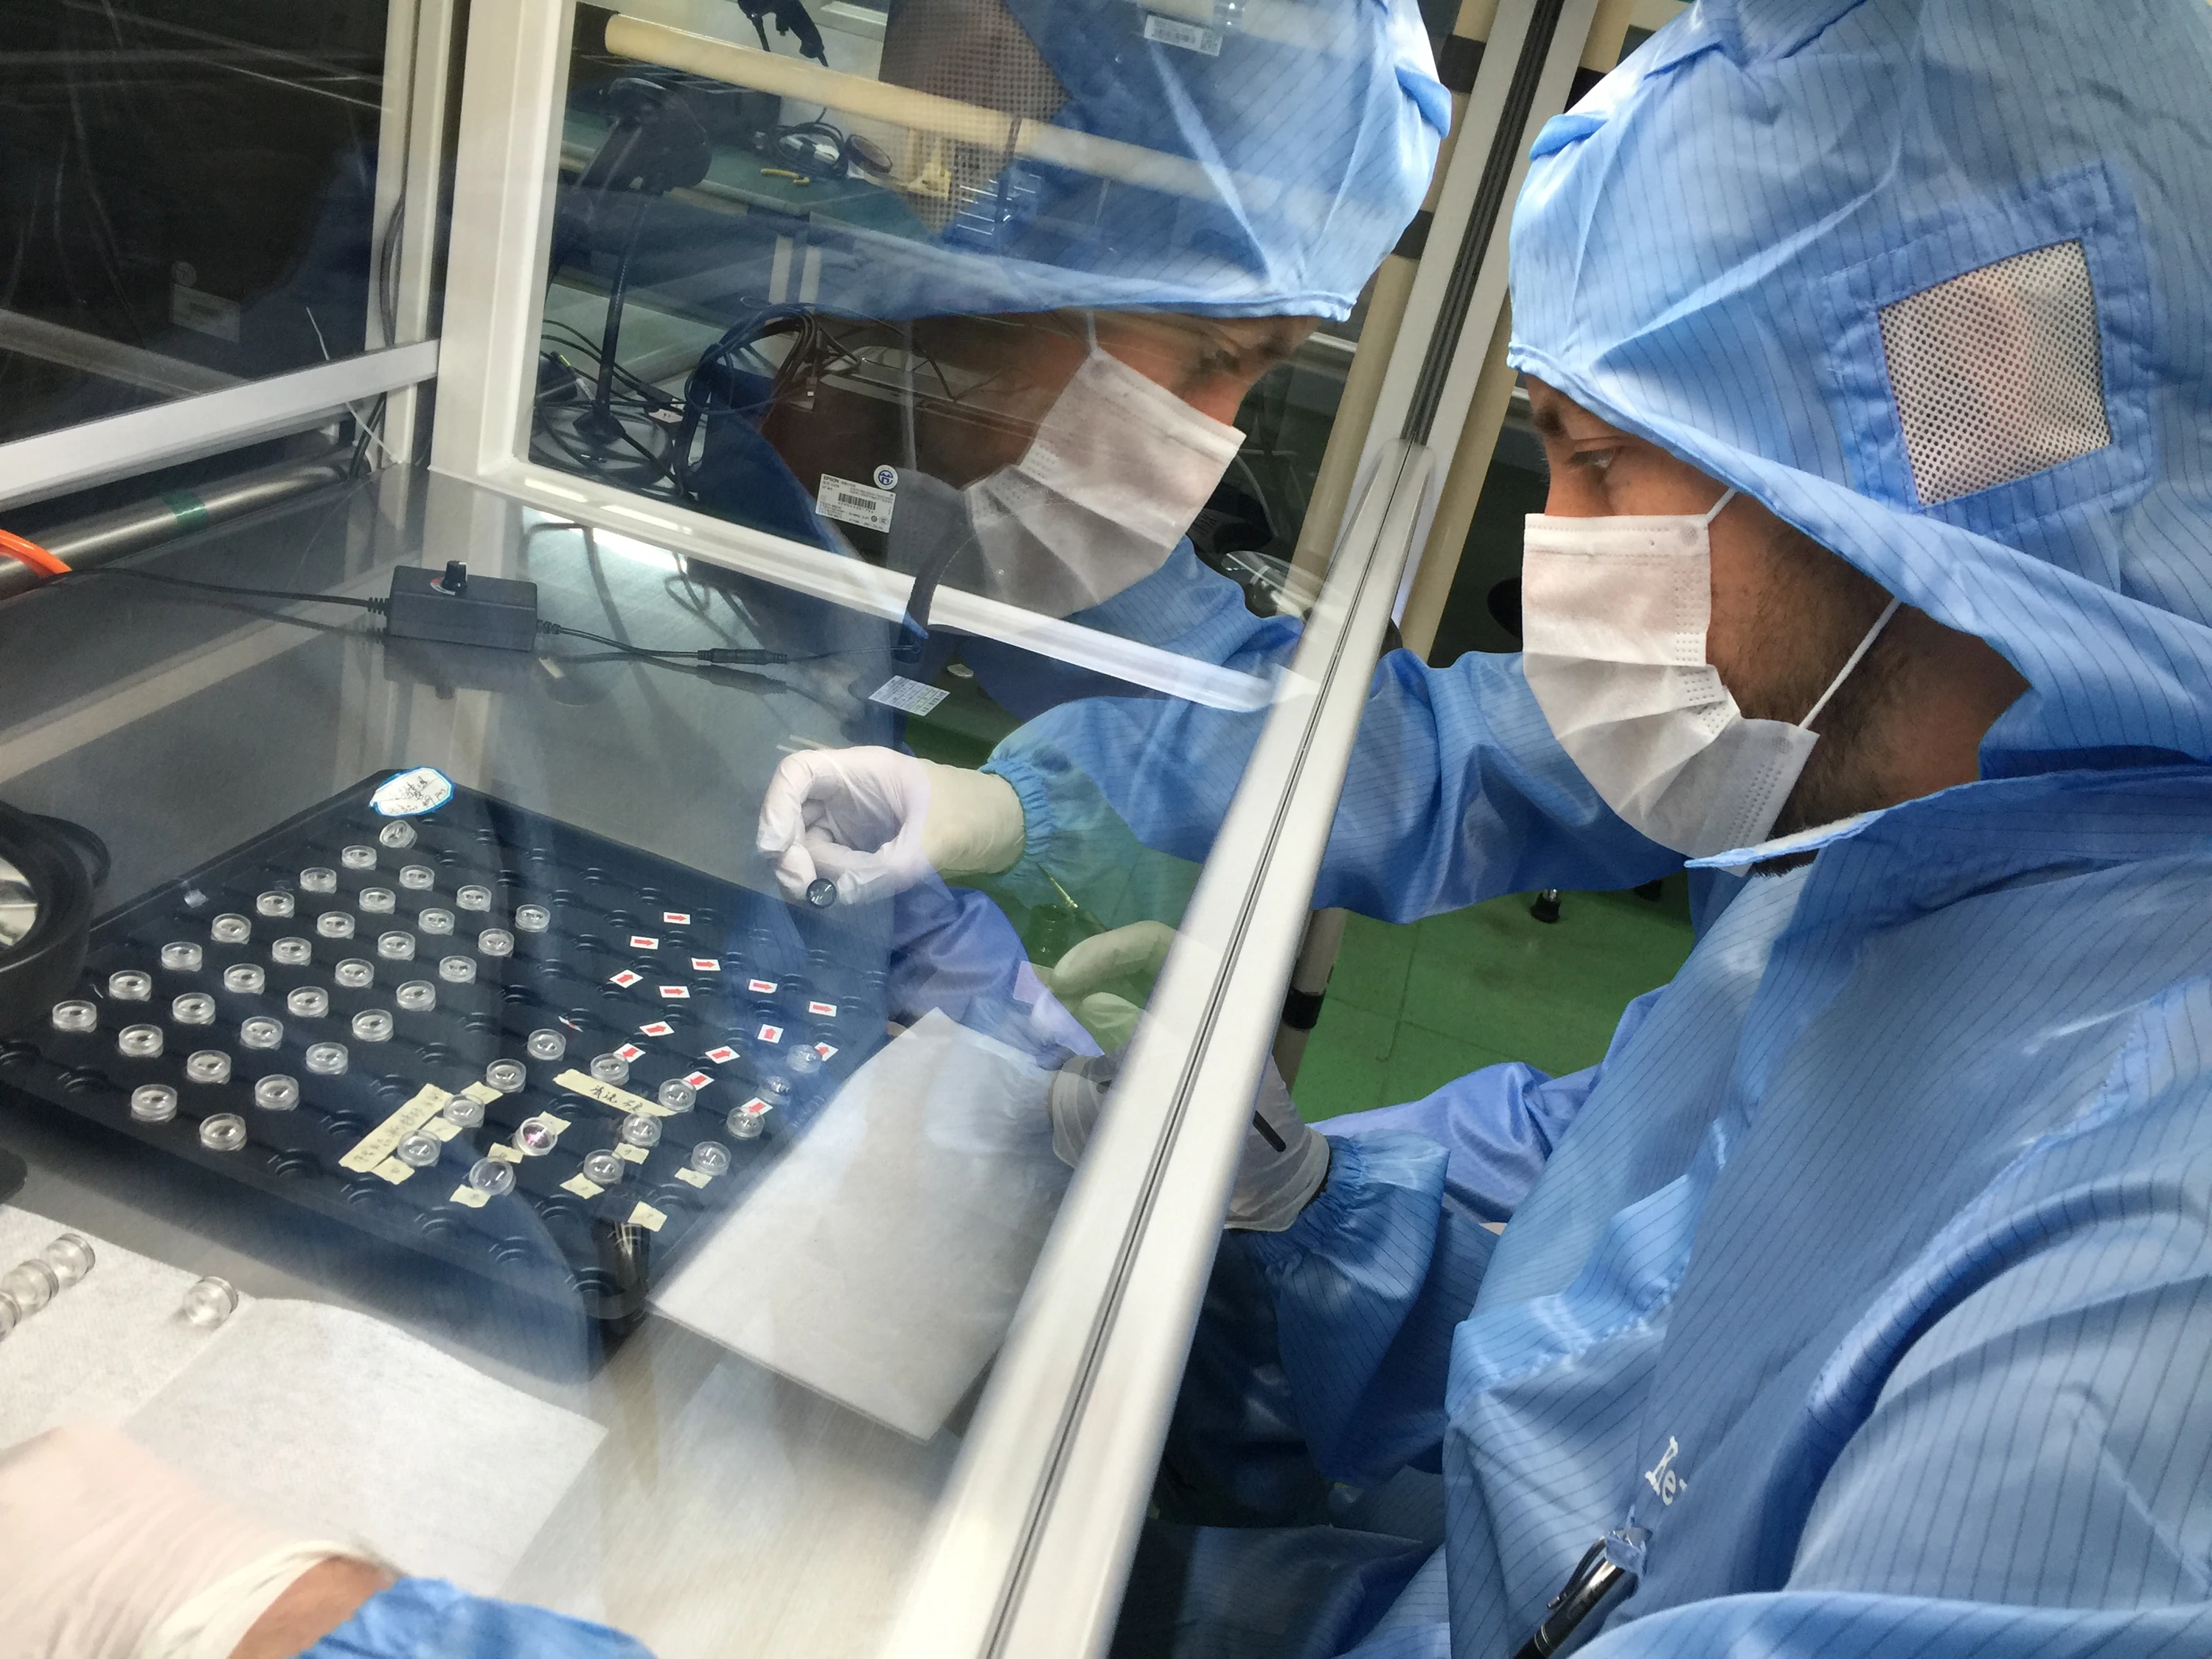
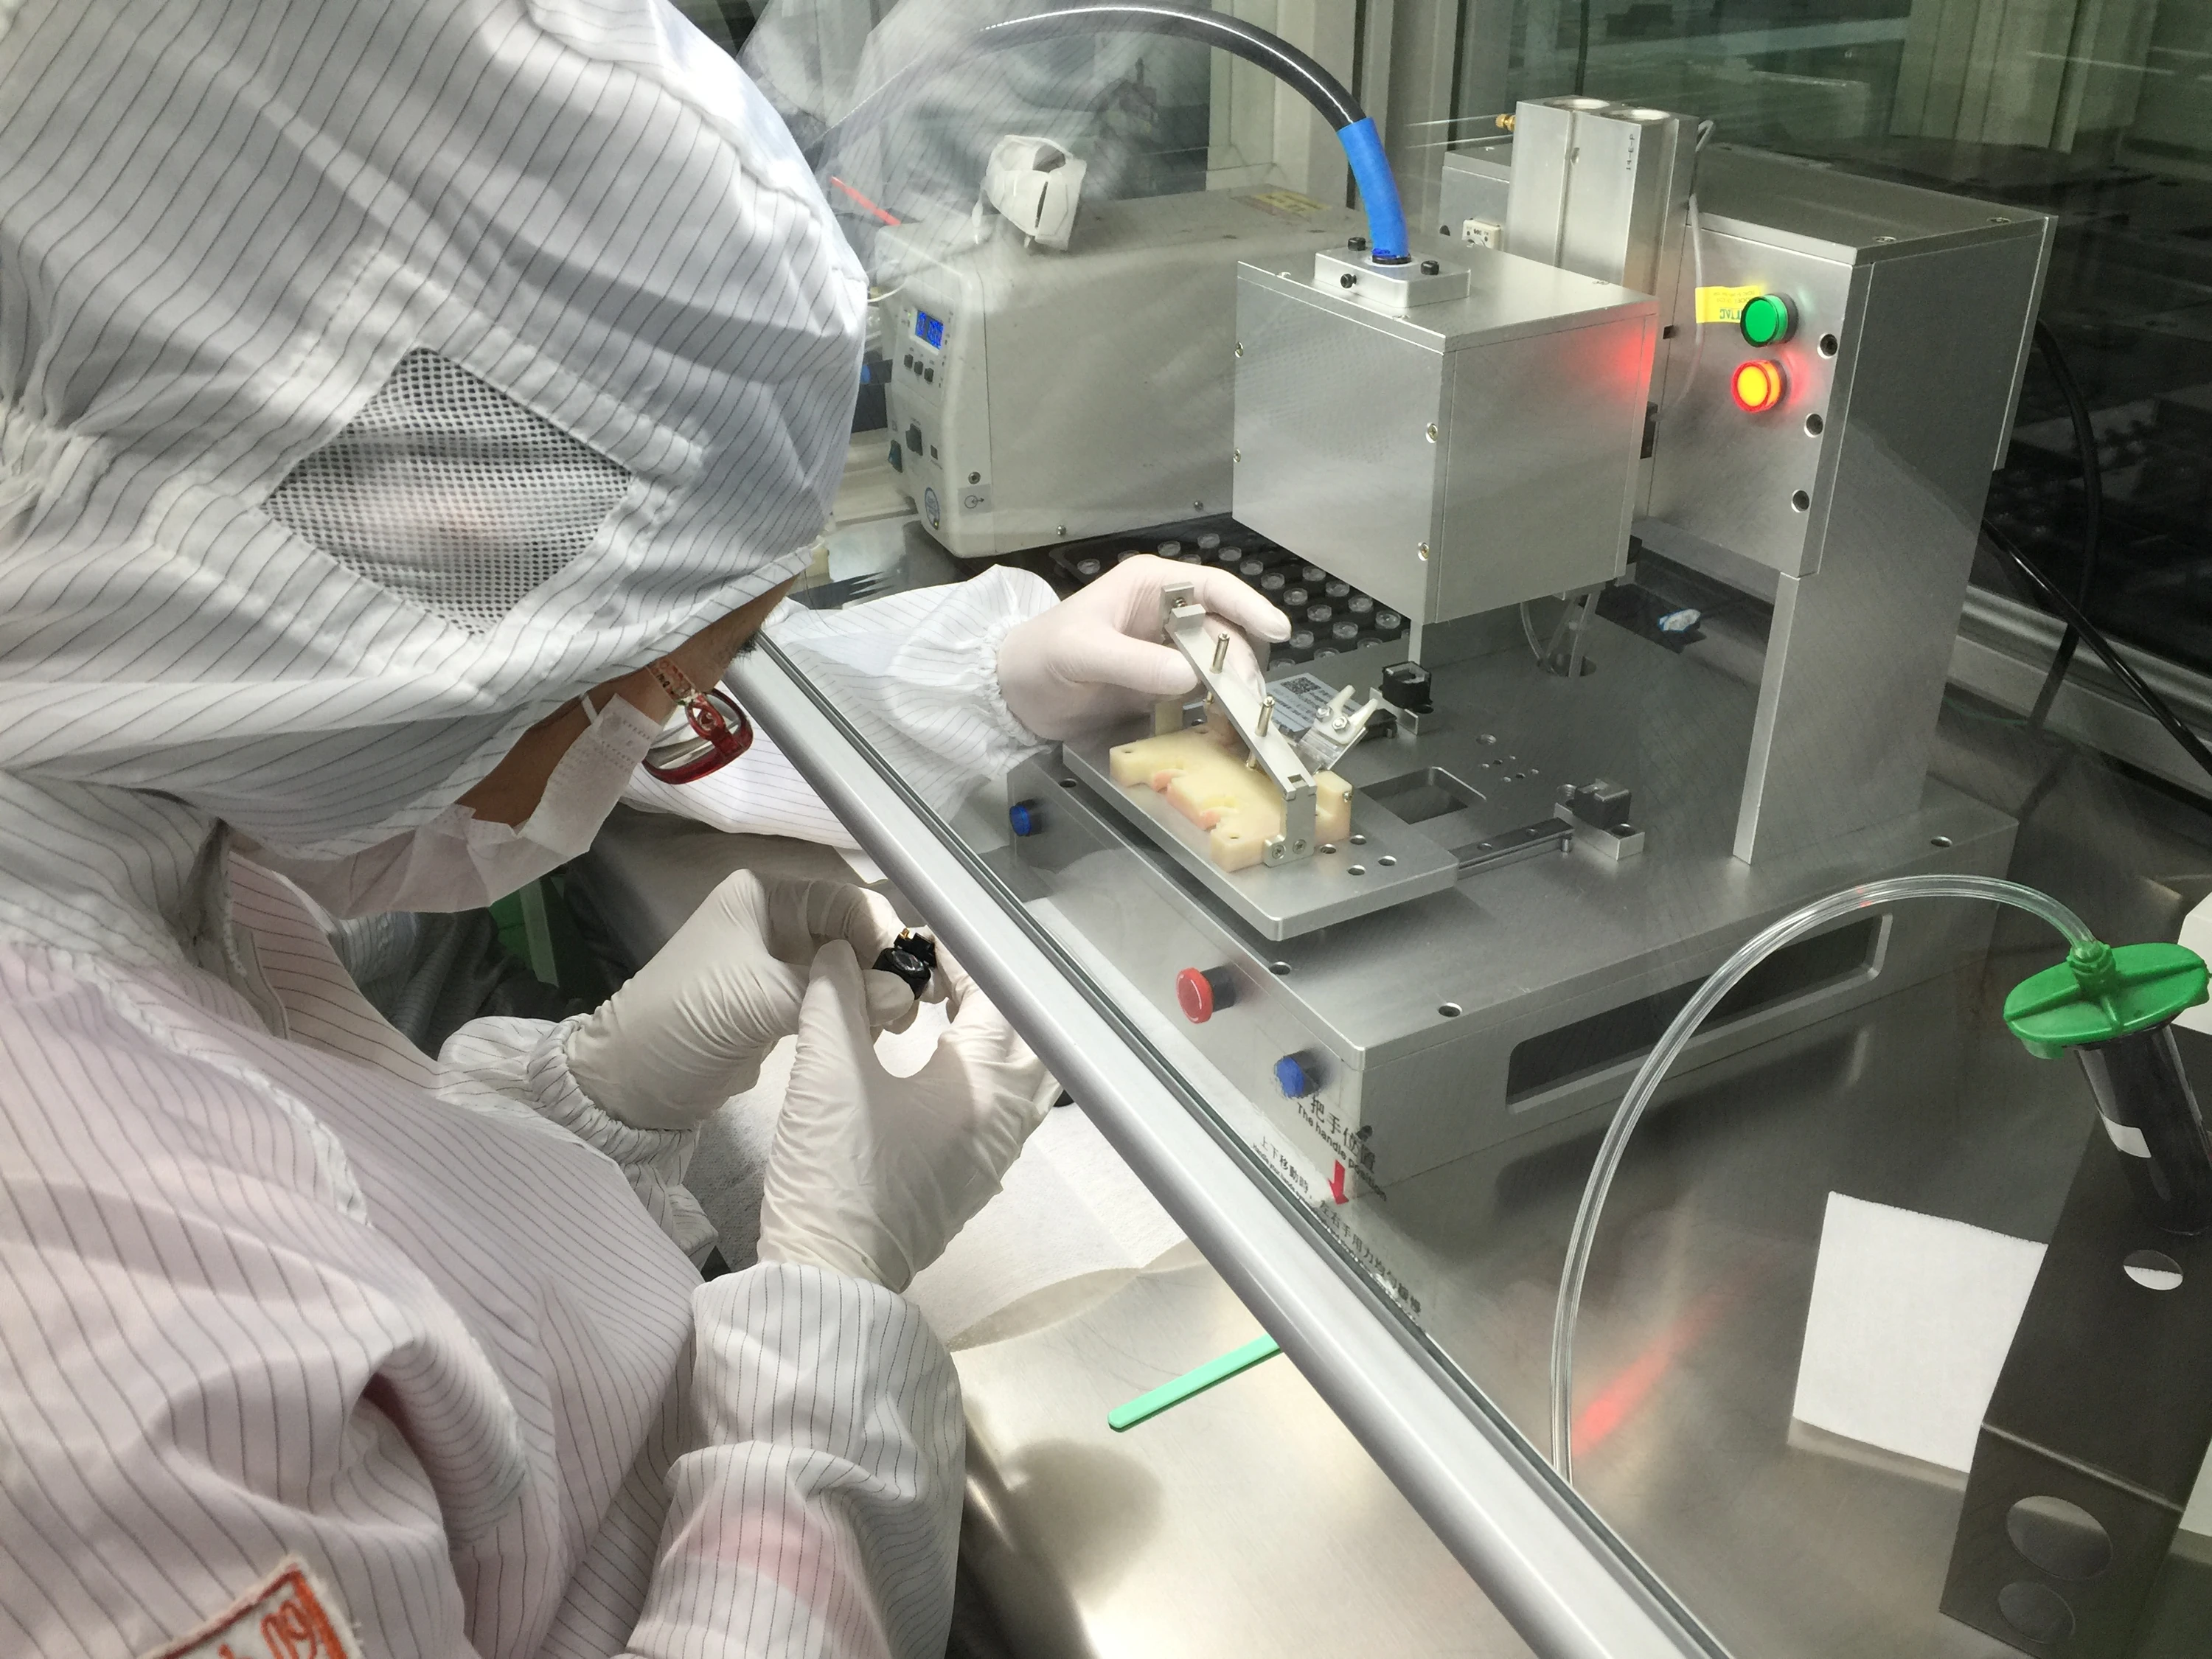
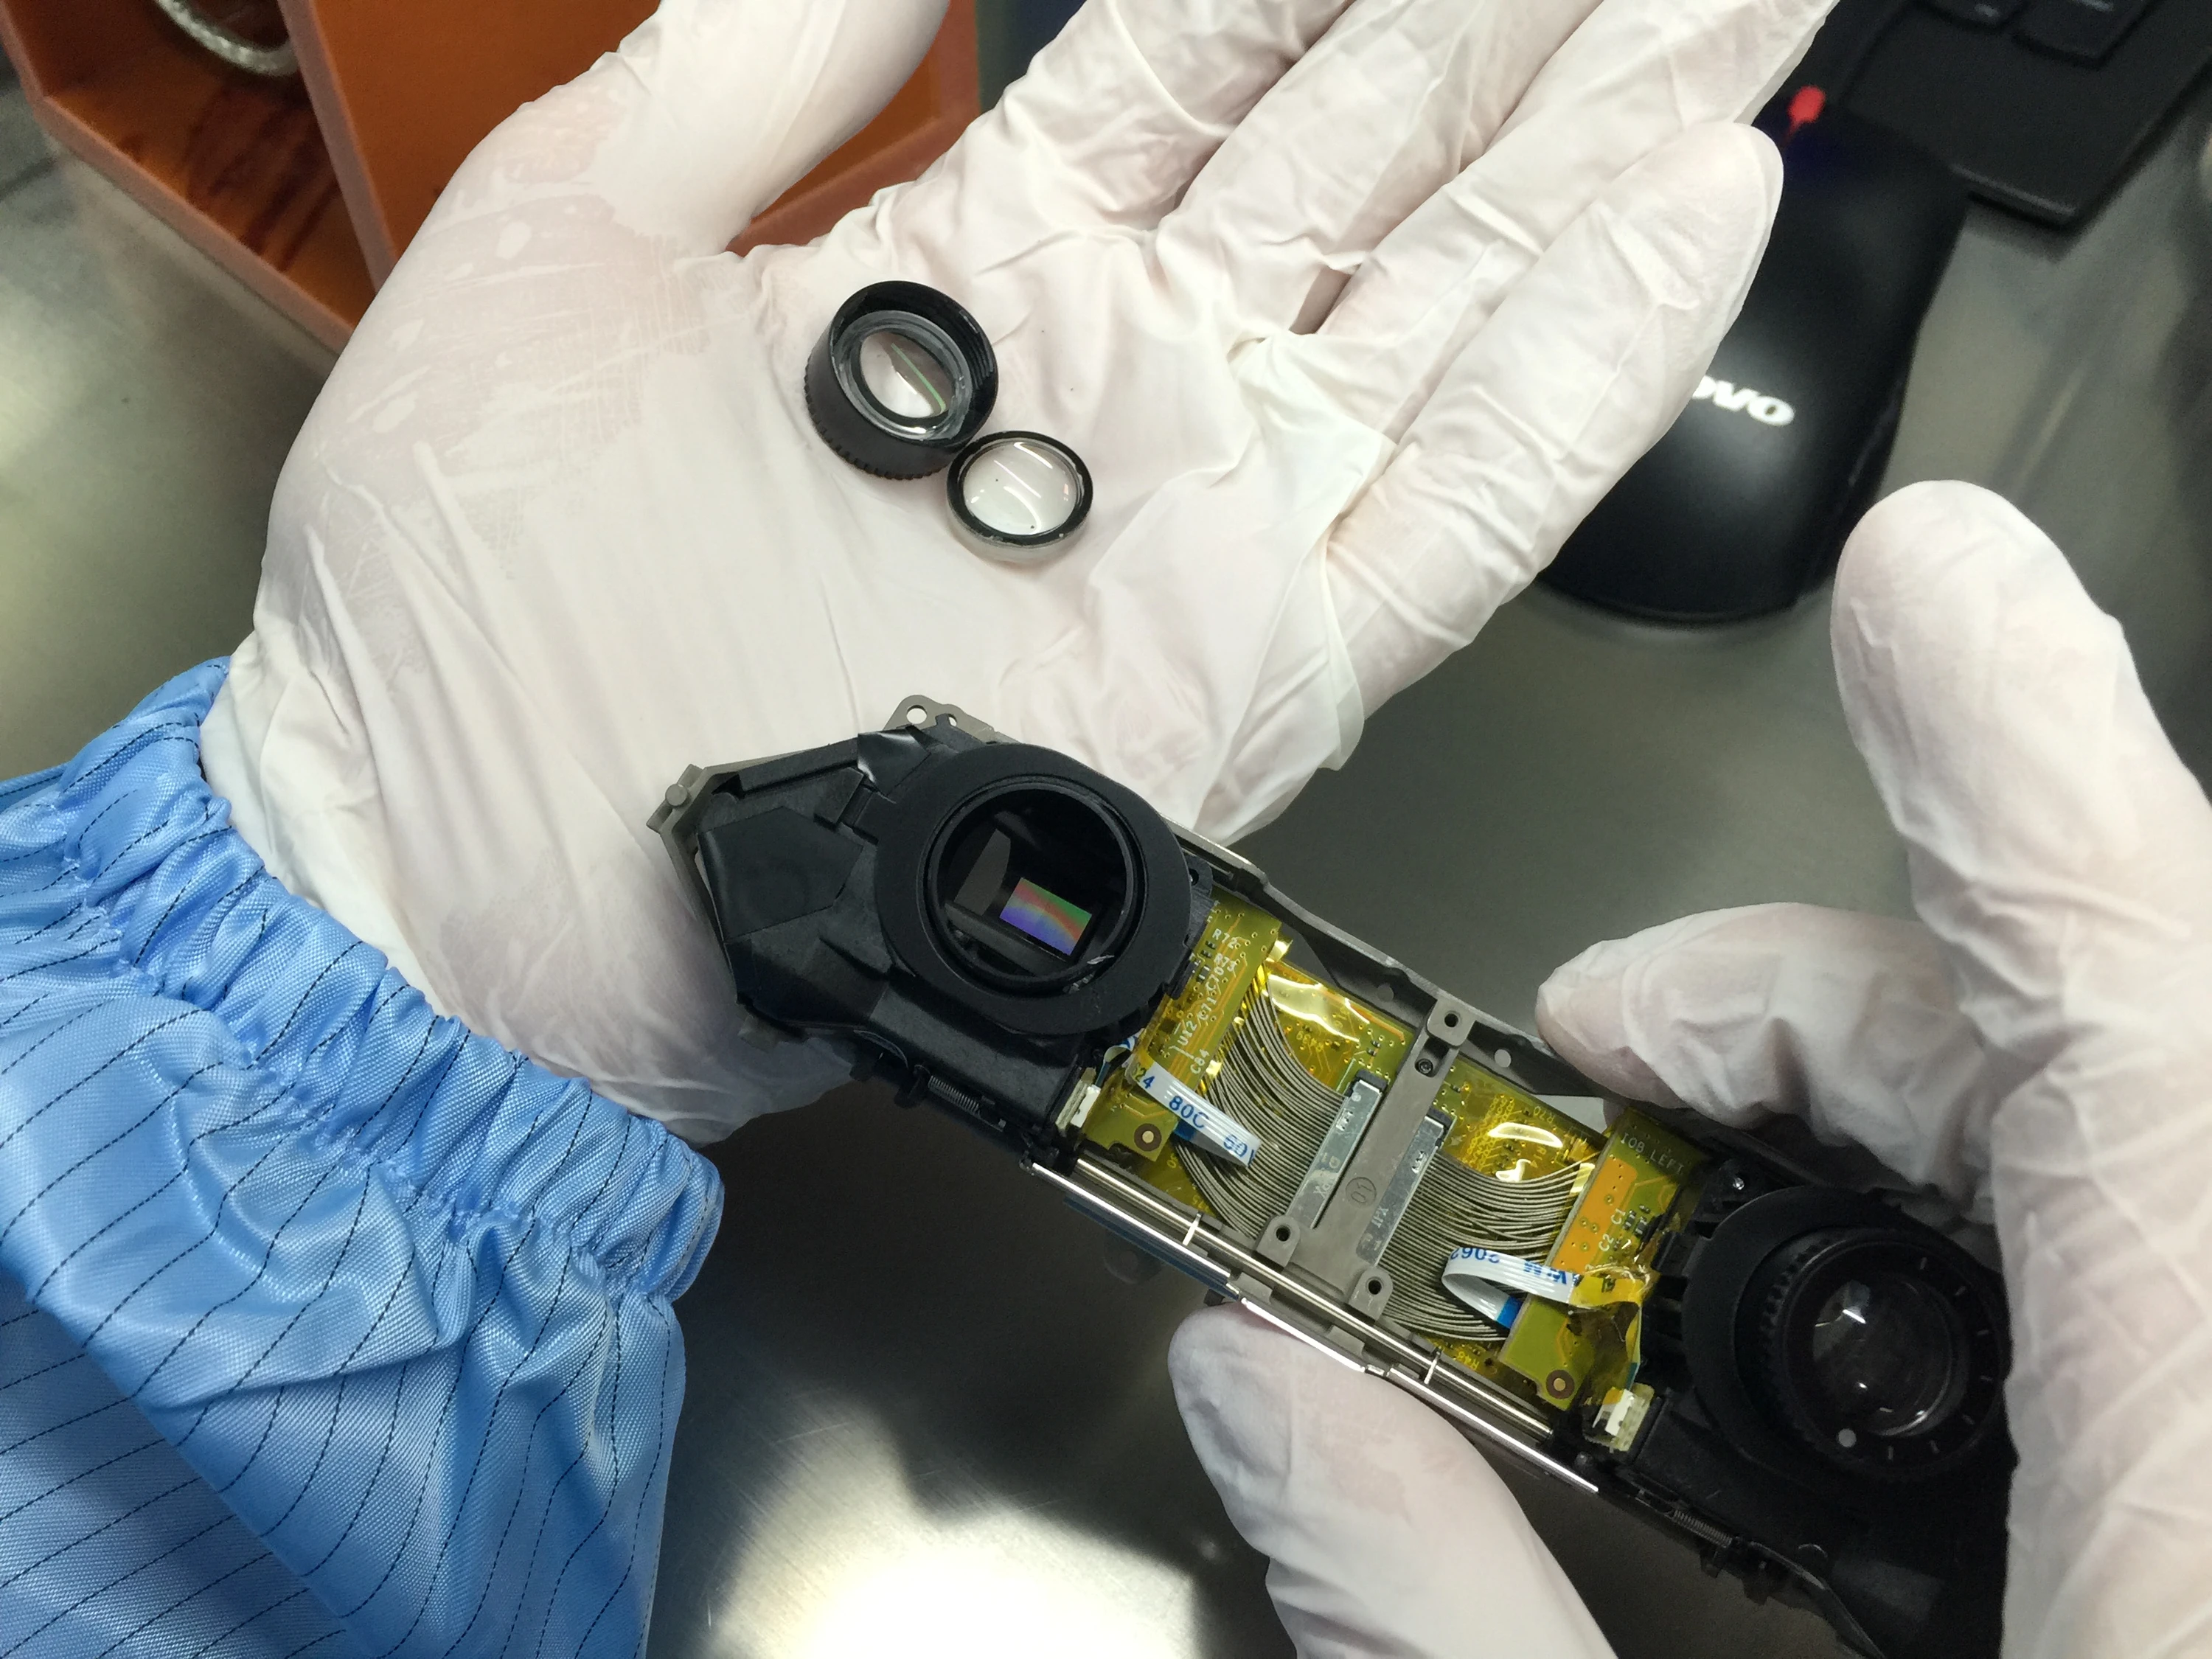
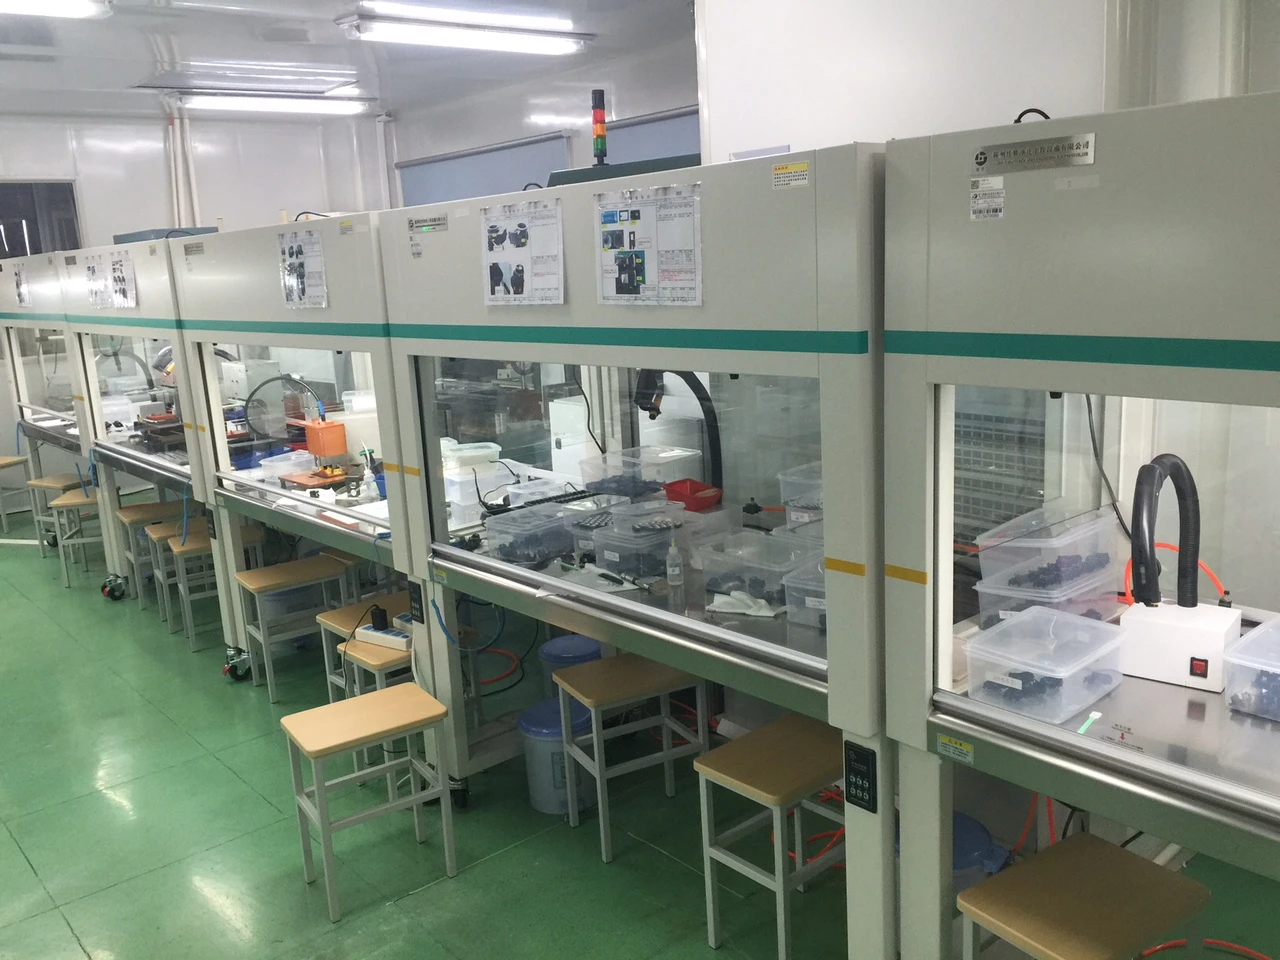
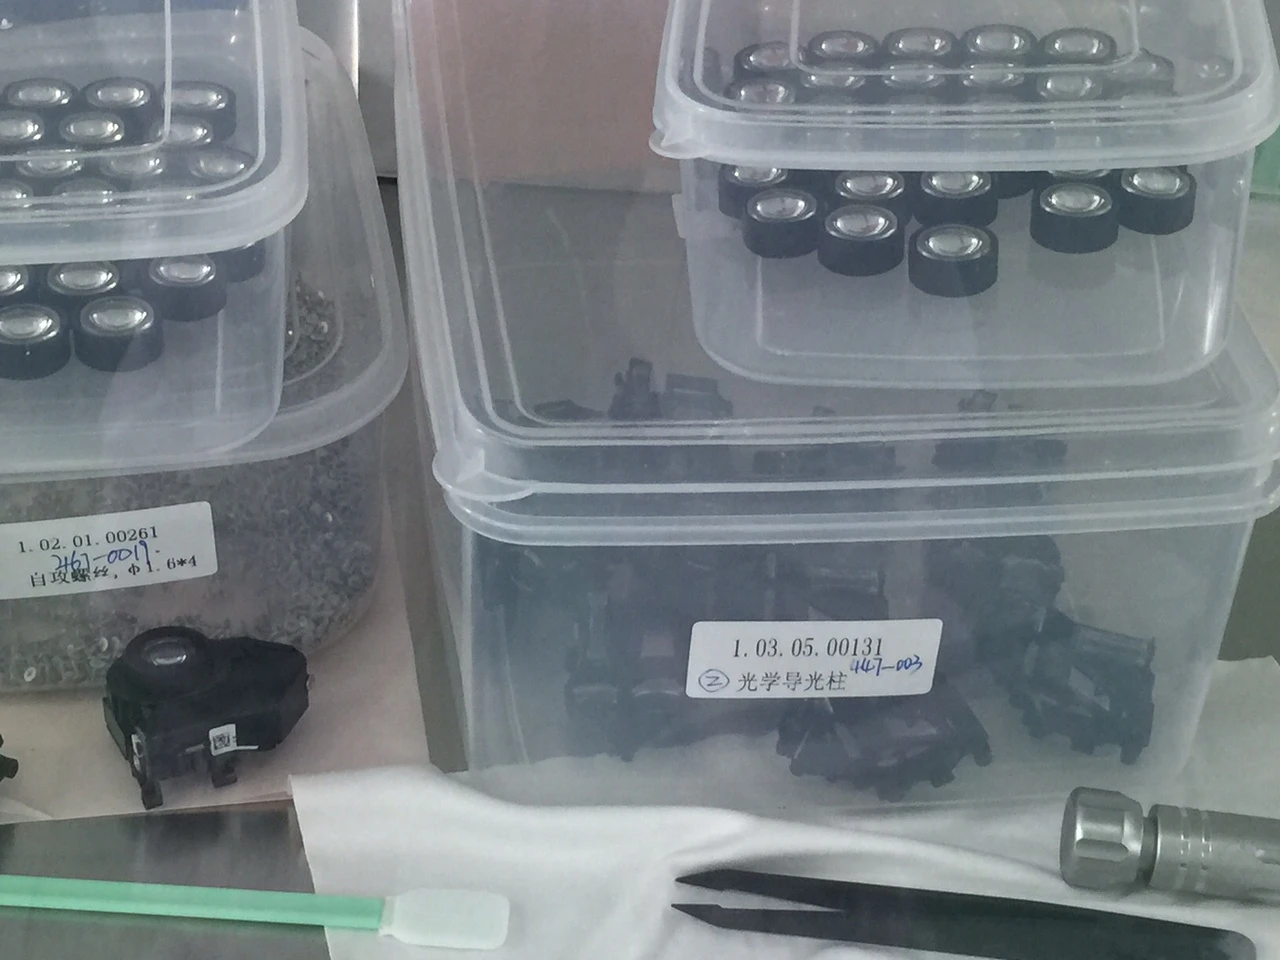
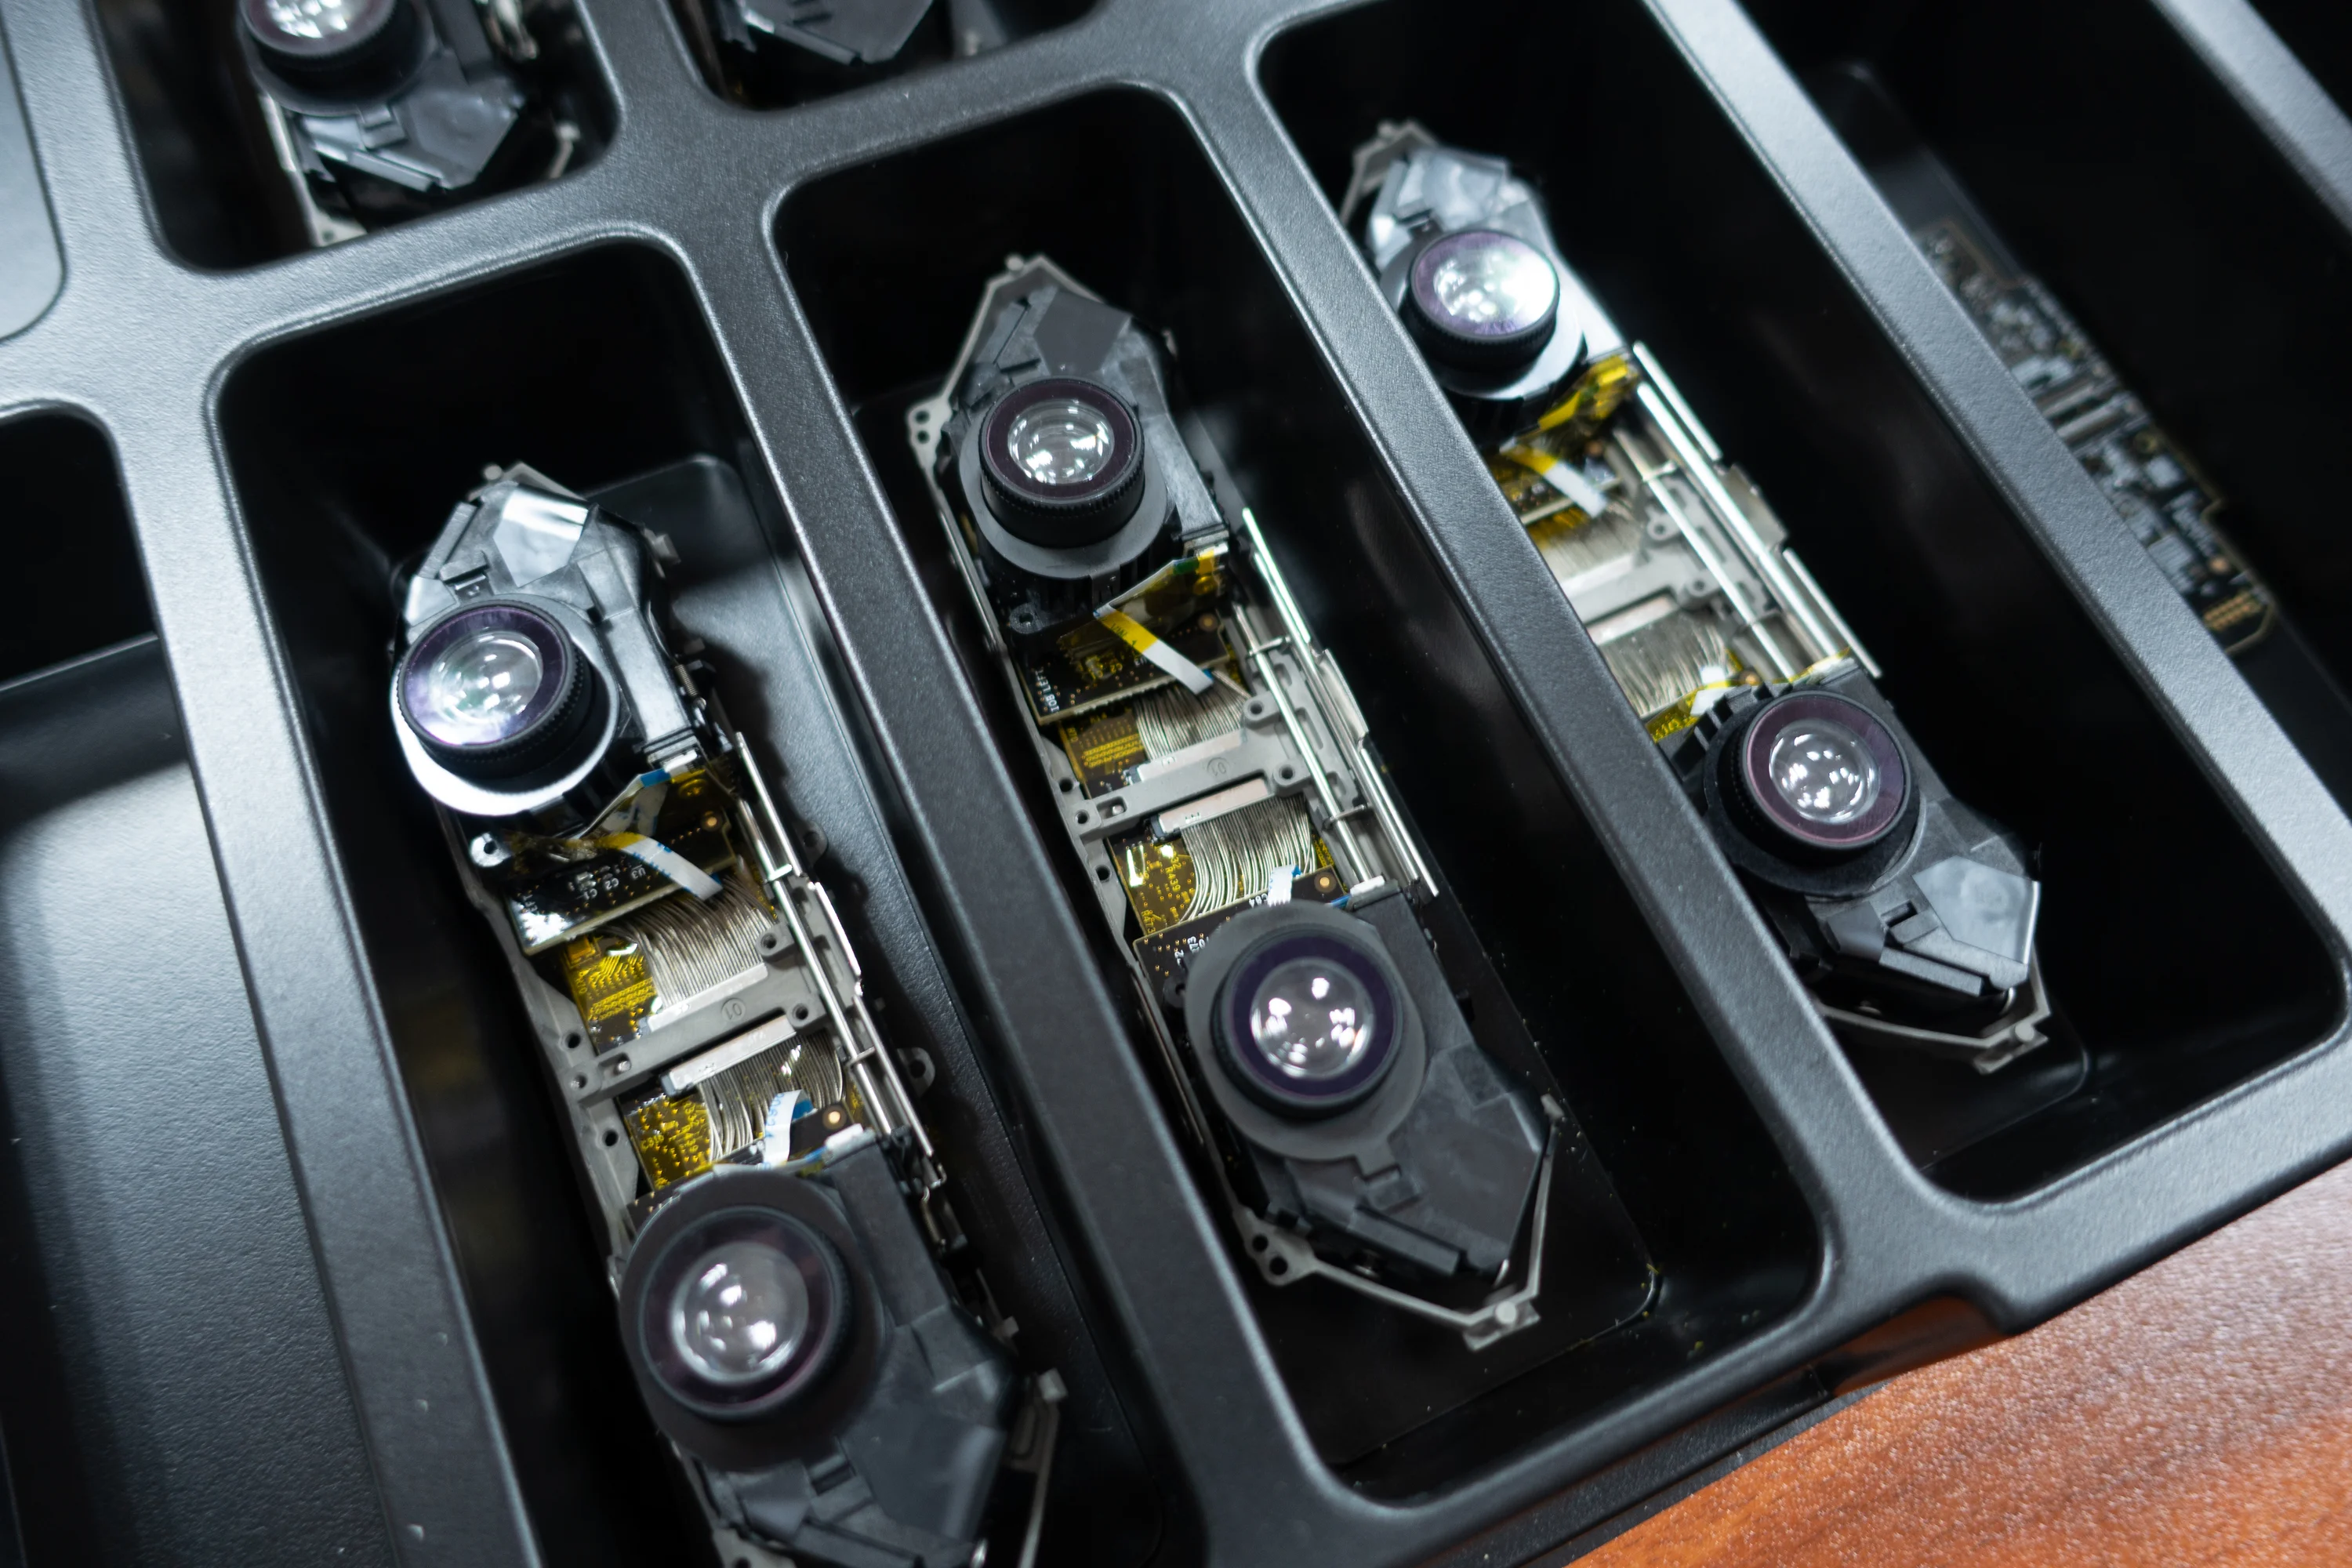
Explore investigation +Close investigation −Lens assembly, bonding and production fixtures
Assembly stations, lens elements and the fixtures used to hold the optical subassemblies during production.
Keeping the optical geometry
Even measuring the assembly required care. The alignment-fixture specification called for three mounting locations that would not force the chassis flat, and checks at both minimum and maximum IPD. Clamping a chassis into a different shape could conceal the geometry we needed to measure. Nose height, headband position and the separate focus controls then let the wearer bring both images into view. Mechanical fit and optical performance met at those interfaces.
Checking alignment, calibration and cleanliness
Alignment, calibration and cleanliness needed different checks. The optical test requirements covered the position of the eyepiece and folding mirror, focus and illumination, color balance, and contamination in the optical path. Some stations combined several of those checks; passing one did not answer all the others.
Inspection coverage mattered, too. A Week 35 factory report recorded scratches, blue dots and folding-mirror dust that the O7 test missed. Its corrective action called for the program to be improved and confirmed before removing eye inspection at O7 and O4.
Inside the optical engine
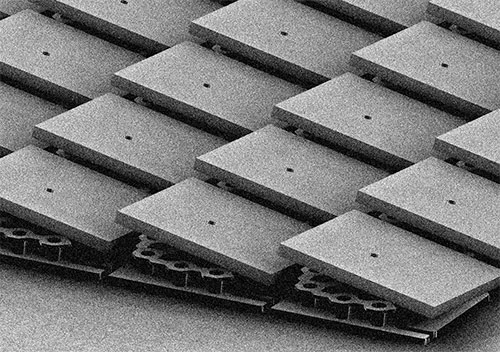
Inside the band were two miniature DLP optical engines, one for each eye. Each used LEDs to illuminate a Texas Instruments digital micromirror device: a 1280 × 720 array of tilting mirrors on a 0.3-inch diagonal. With a mirror pitch of 5.4 µm, the active array occupied just 6.912 × 3.888 mm. Together, the two eyes had about 1.84 million mirrors forming their images.
The mirrors switched light into or away from the viewing path. Custom optics delivered that light through the eyepiece and into the pupil, where the eye's own lens focused it onto the retina. Avegant called this Retinal Imaging Technology. The wearer viewed the illuminated micromirror image through the optics, with an individual focus adjustment for each eye.
How the DLP optical engine works
Getting the mechanical BOM ready to build
My tooling work ran from design through ramp. I worked with Chris Westra, Misha Young, our contract manufacturer Intretech and the component suppliers to turn tooling samples into parts we could build with. That involved inspecting dimensions and appearance, checking how the parts fitted together, getting tool changes made and deciding what could proceed into a build.
Keeping a build moving meant knowing which parts were ready and what still stood between us and a complete set. In late August 2015, we were working toward material readiness for 10 sets before August 26 and 135 sets before September 3. The headband BOM tied those quantities to responsible people, first article inspections, review status, whether a part was usable for engineering validation, and the actions needed from the supplier. A part could be usable for that build while still needing a tooling correction for production.
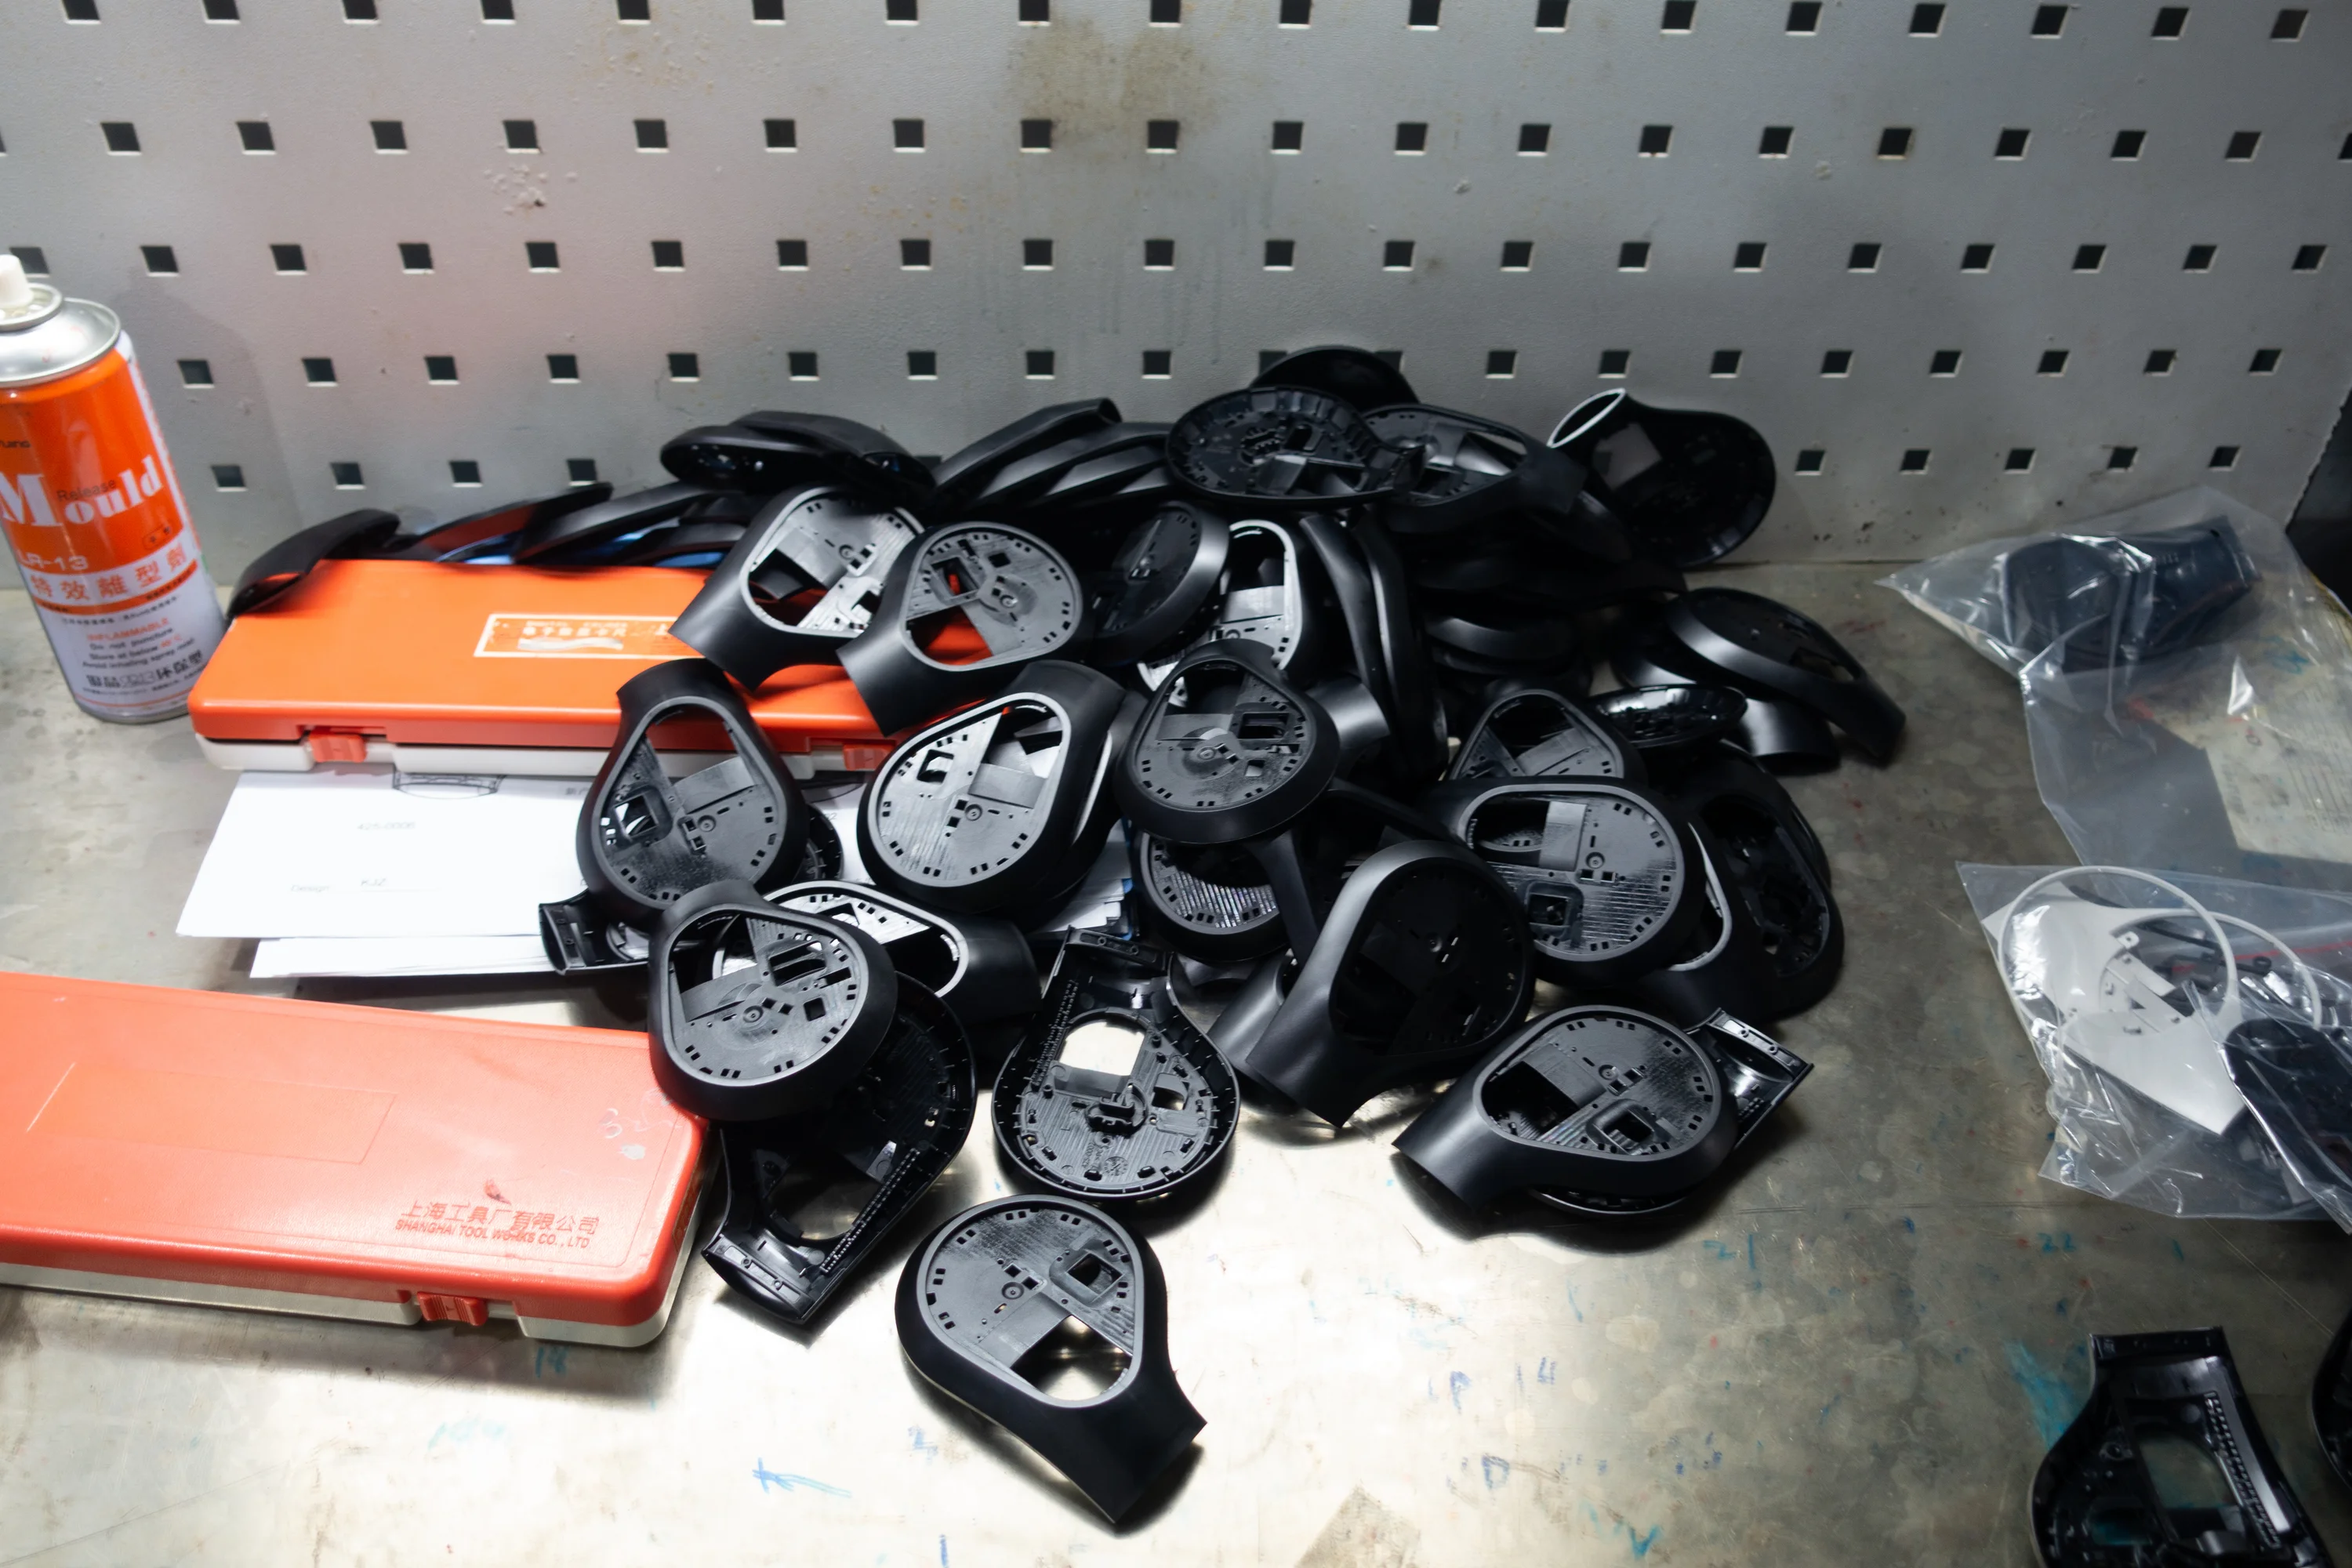
At the molding press
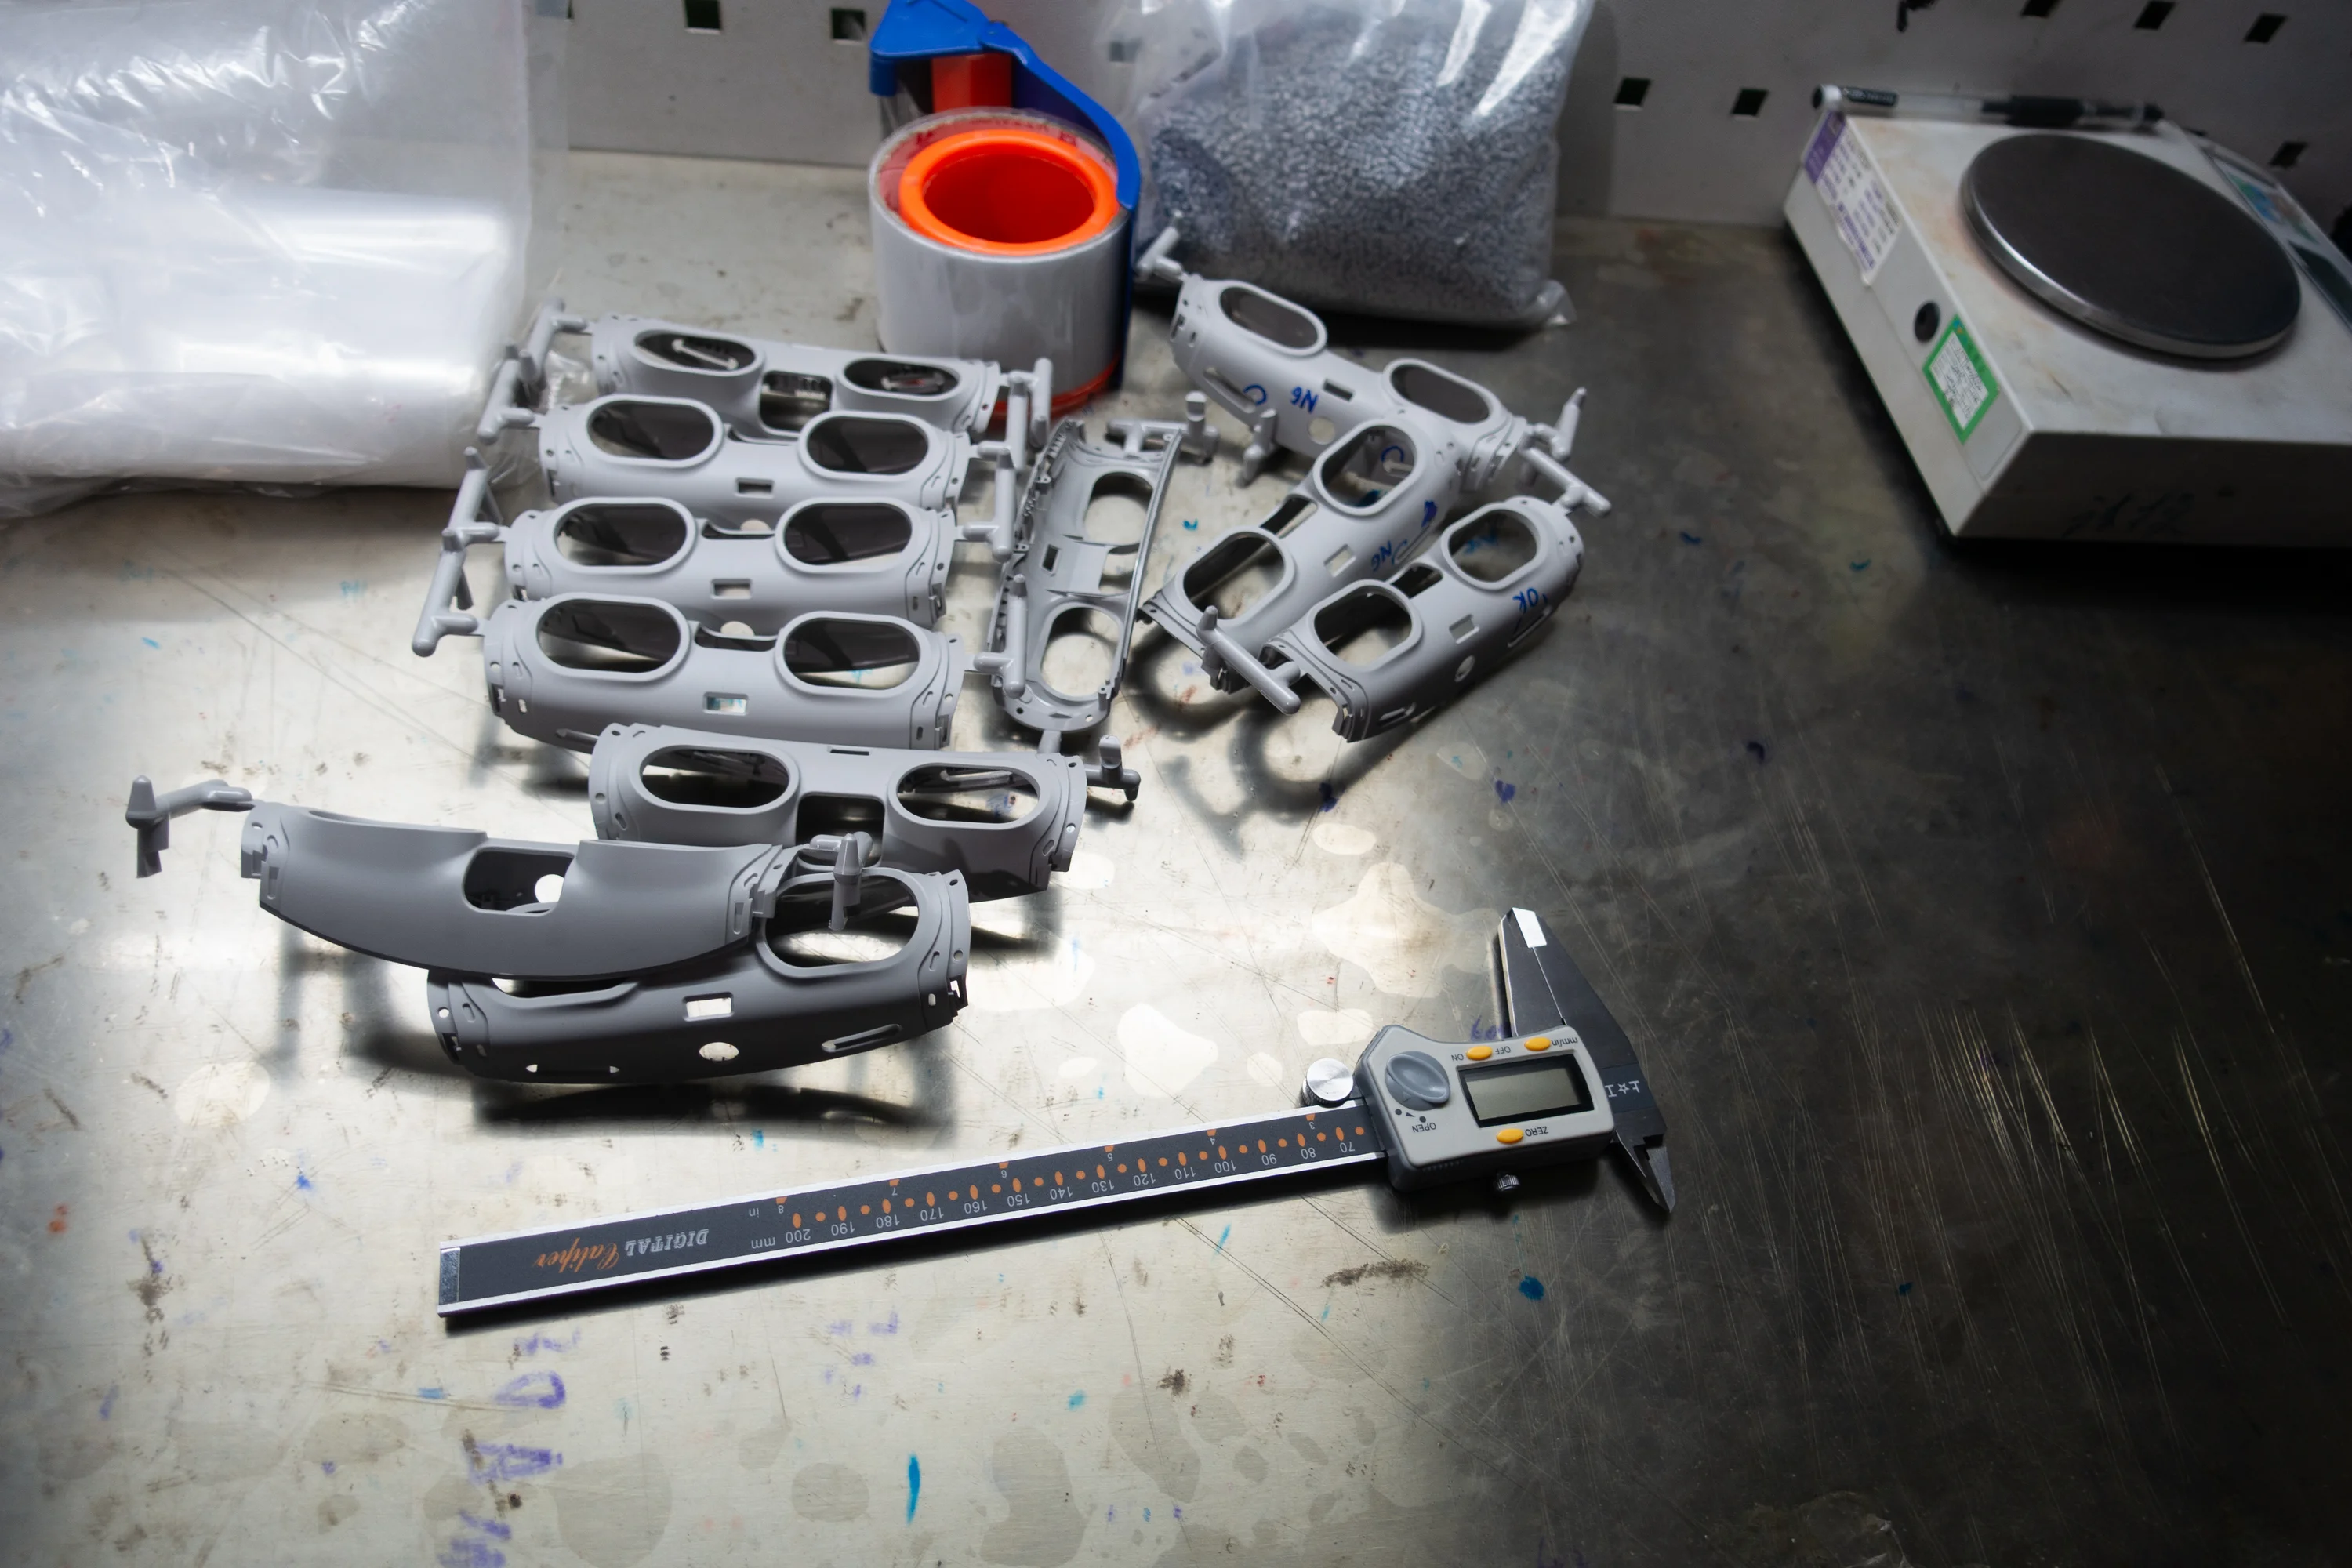
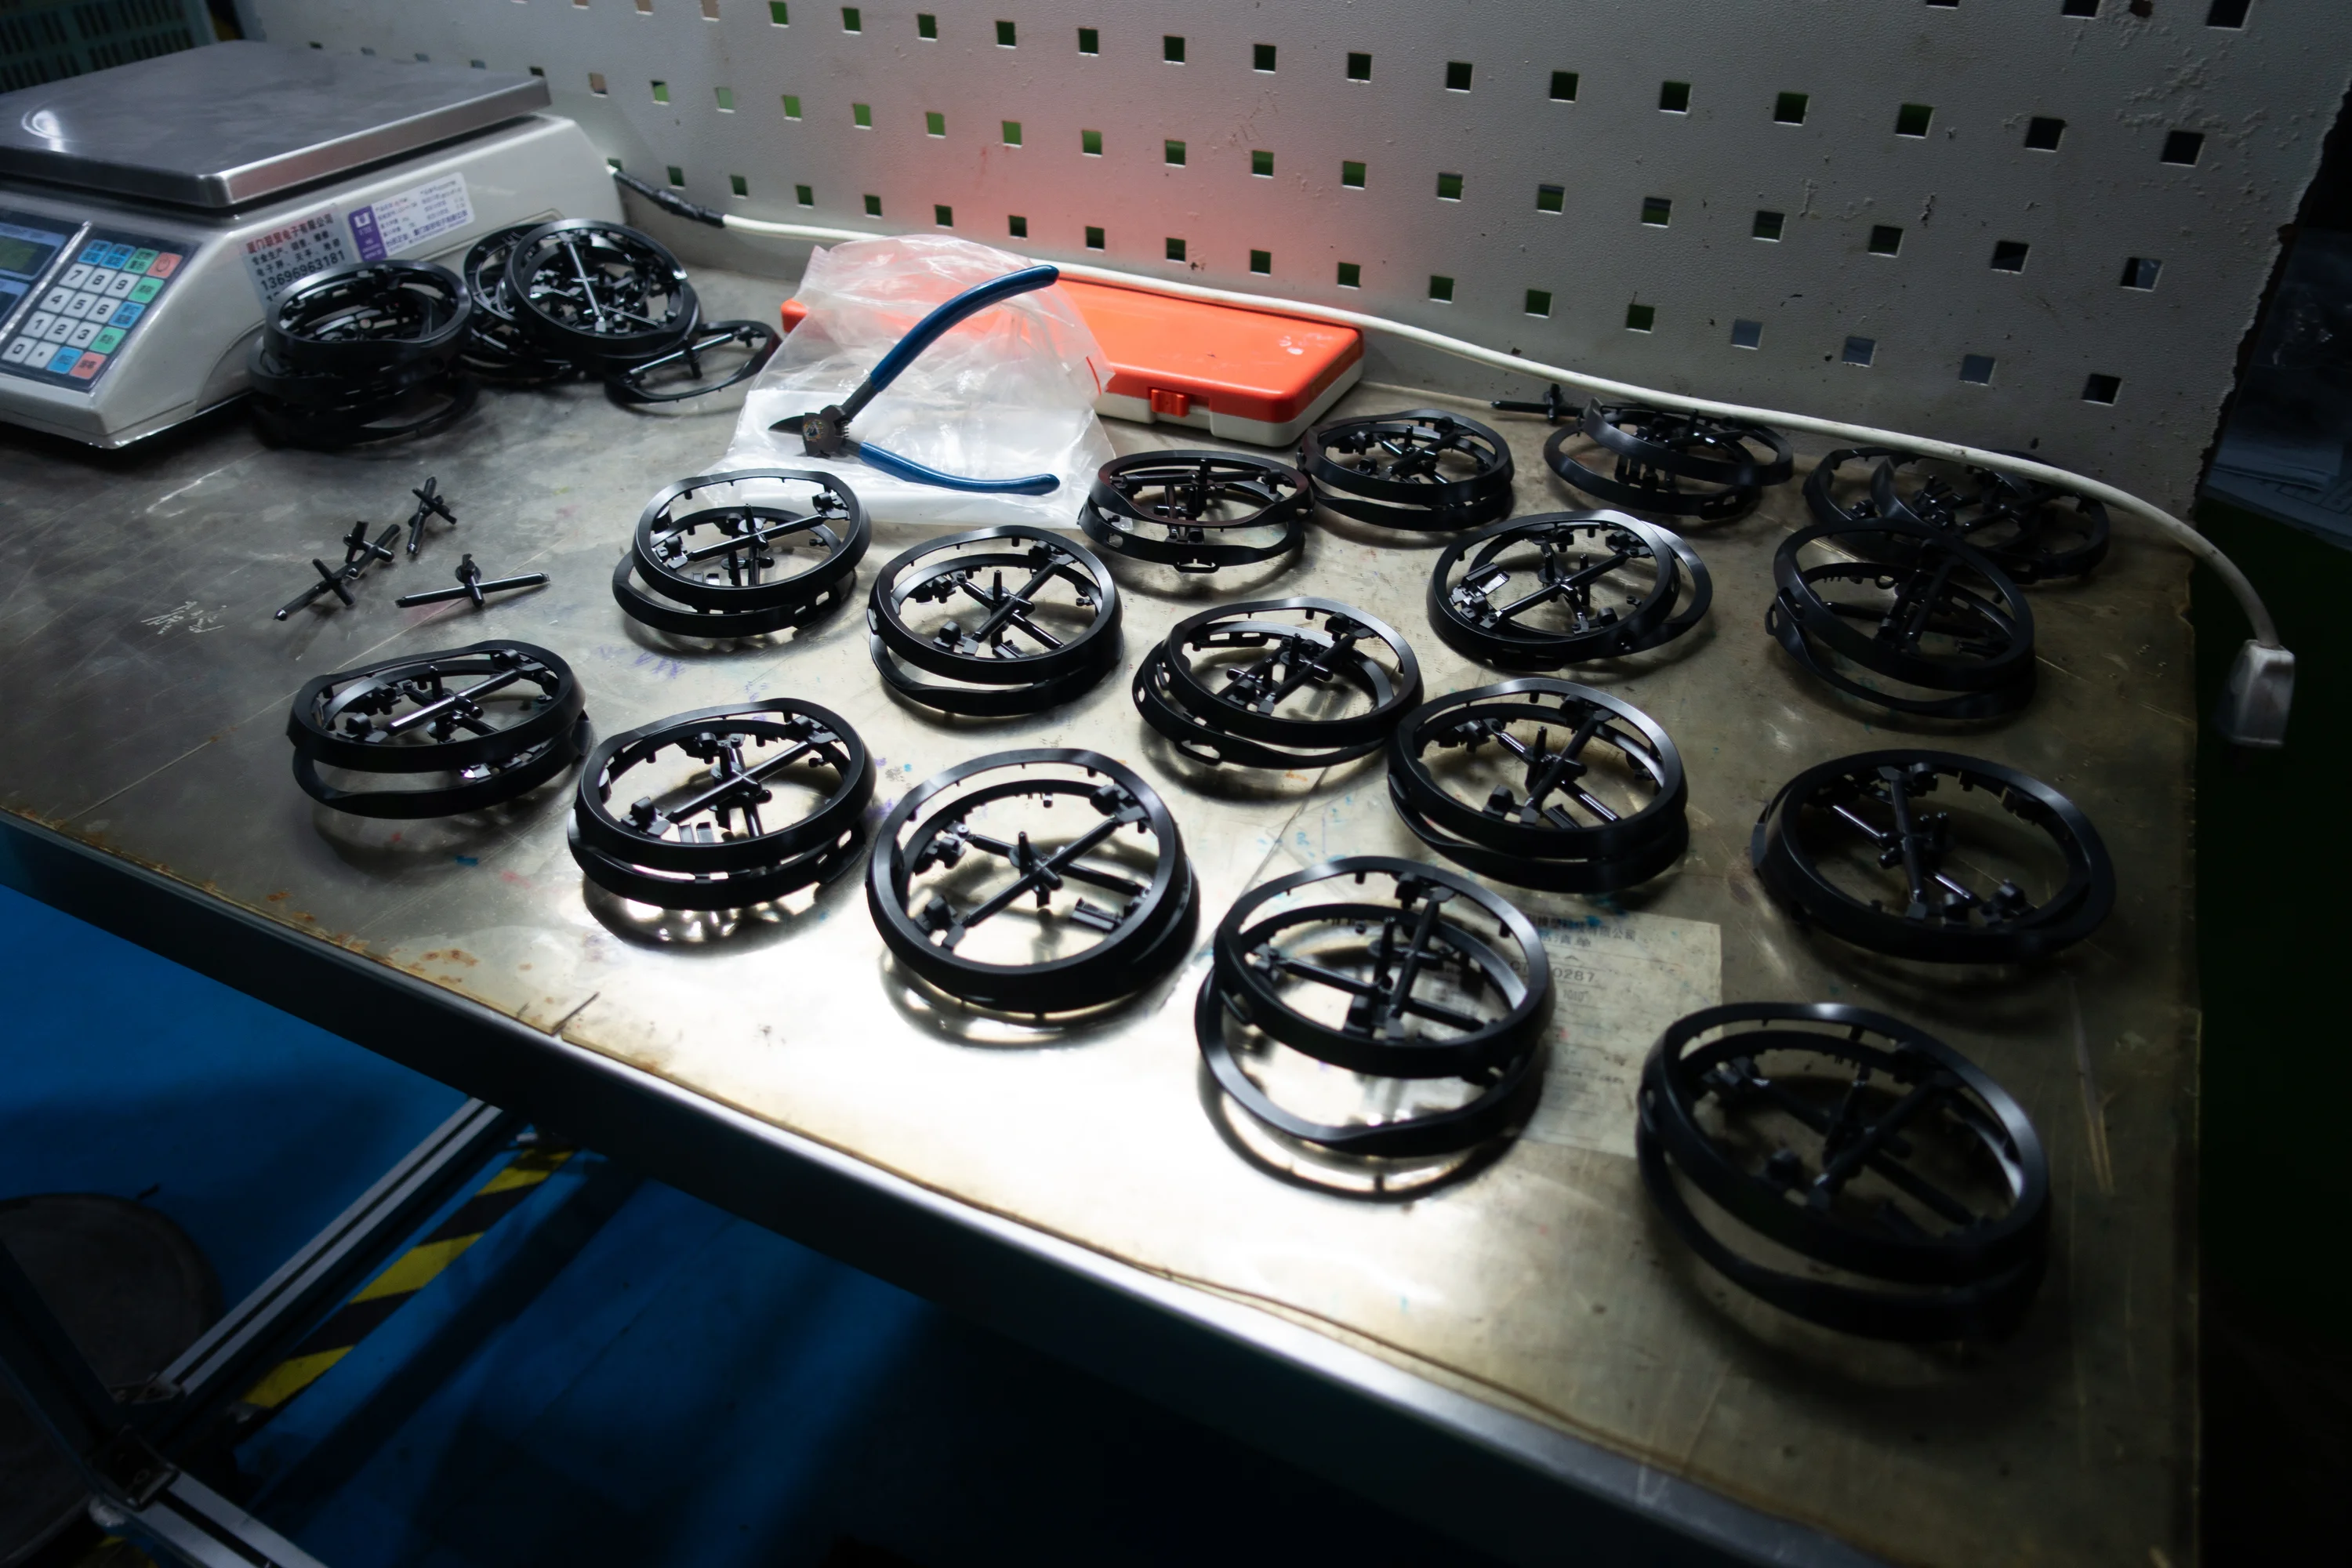
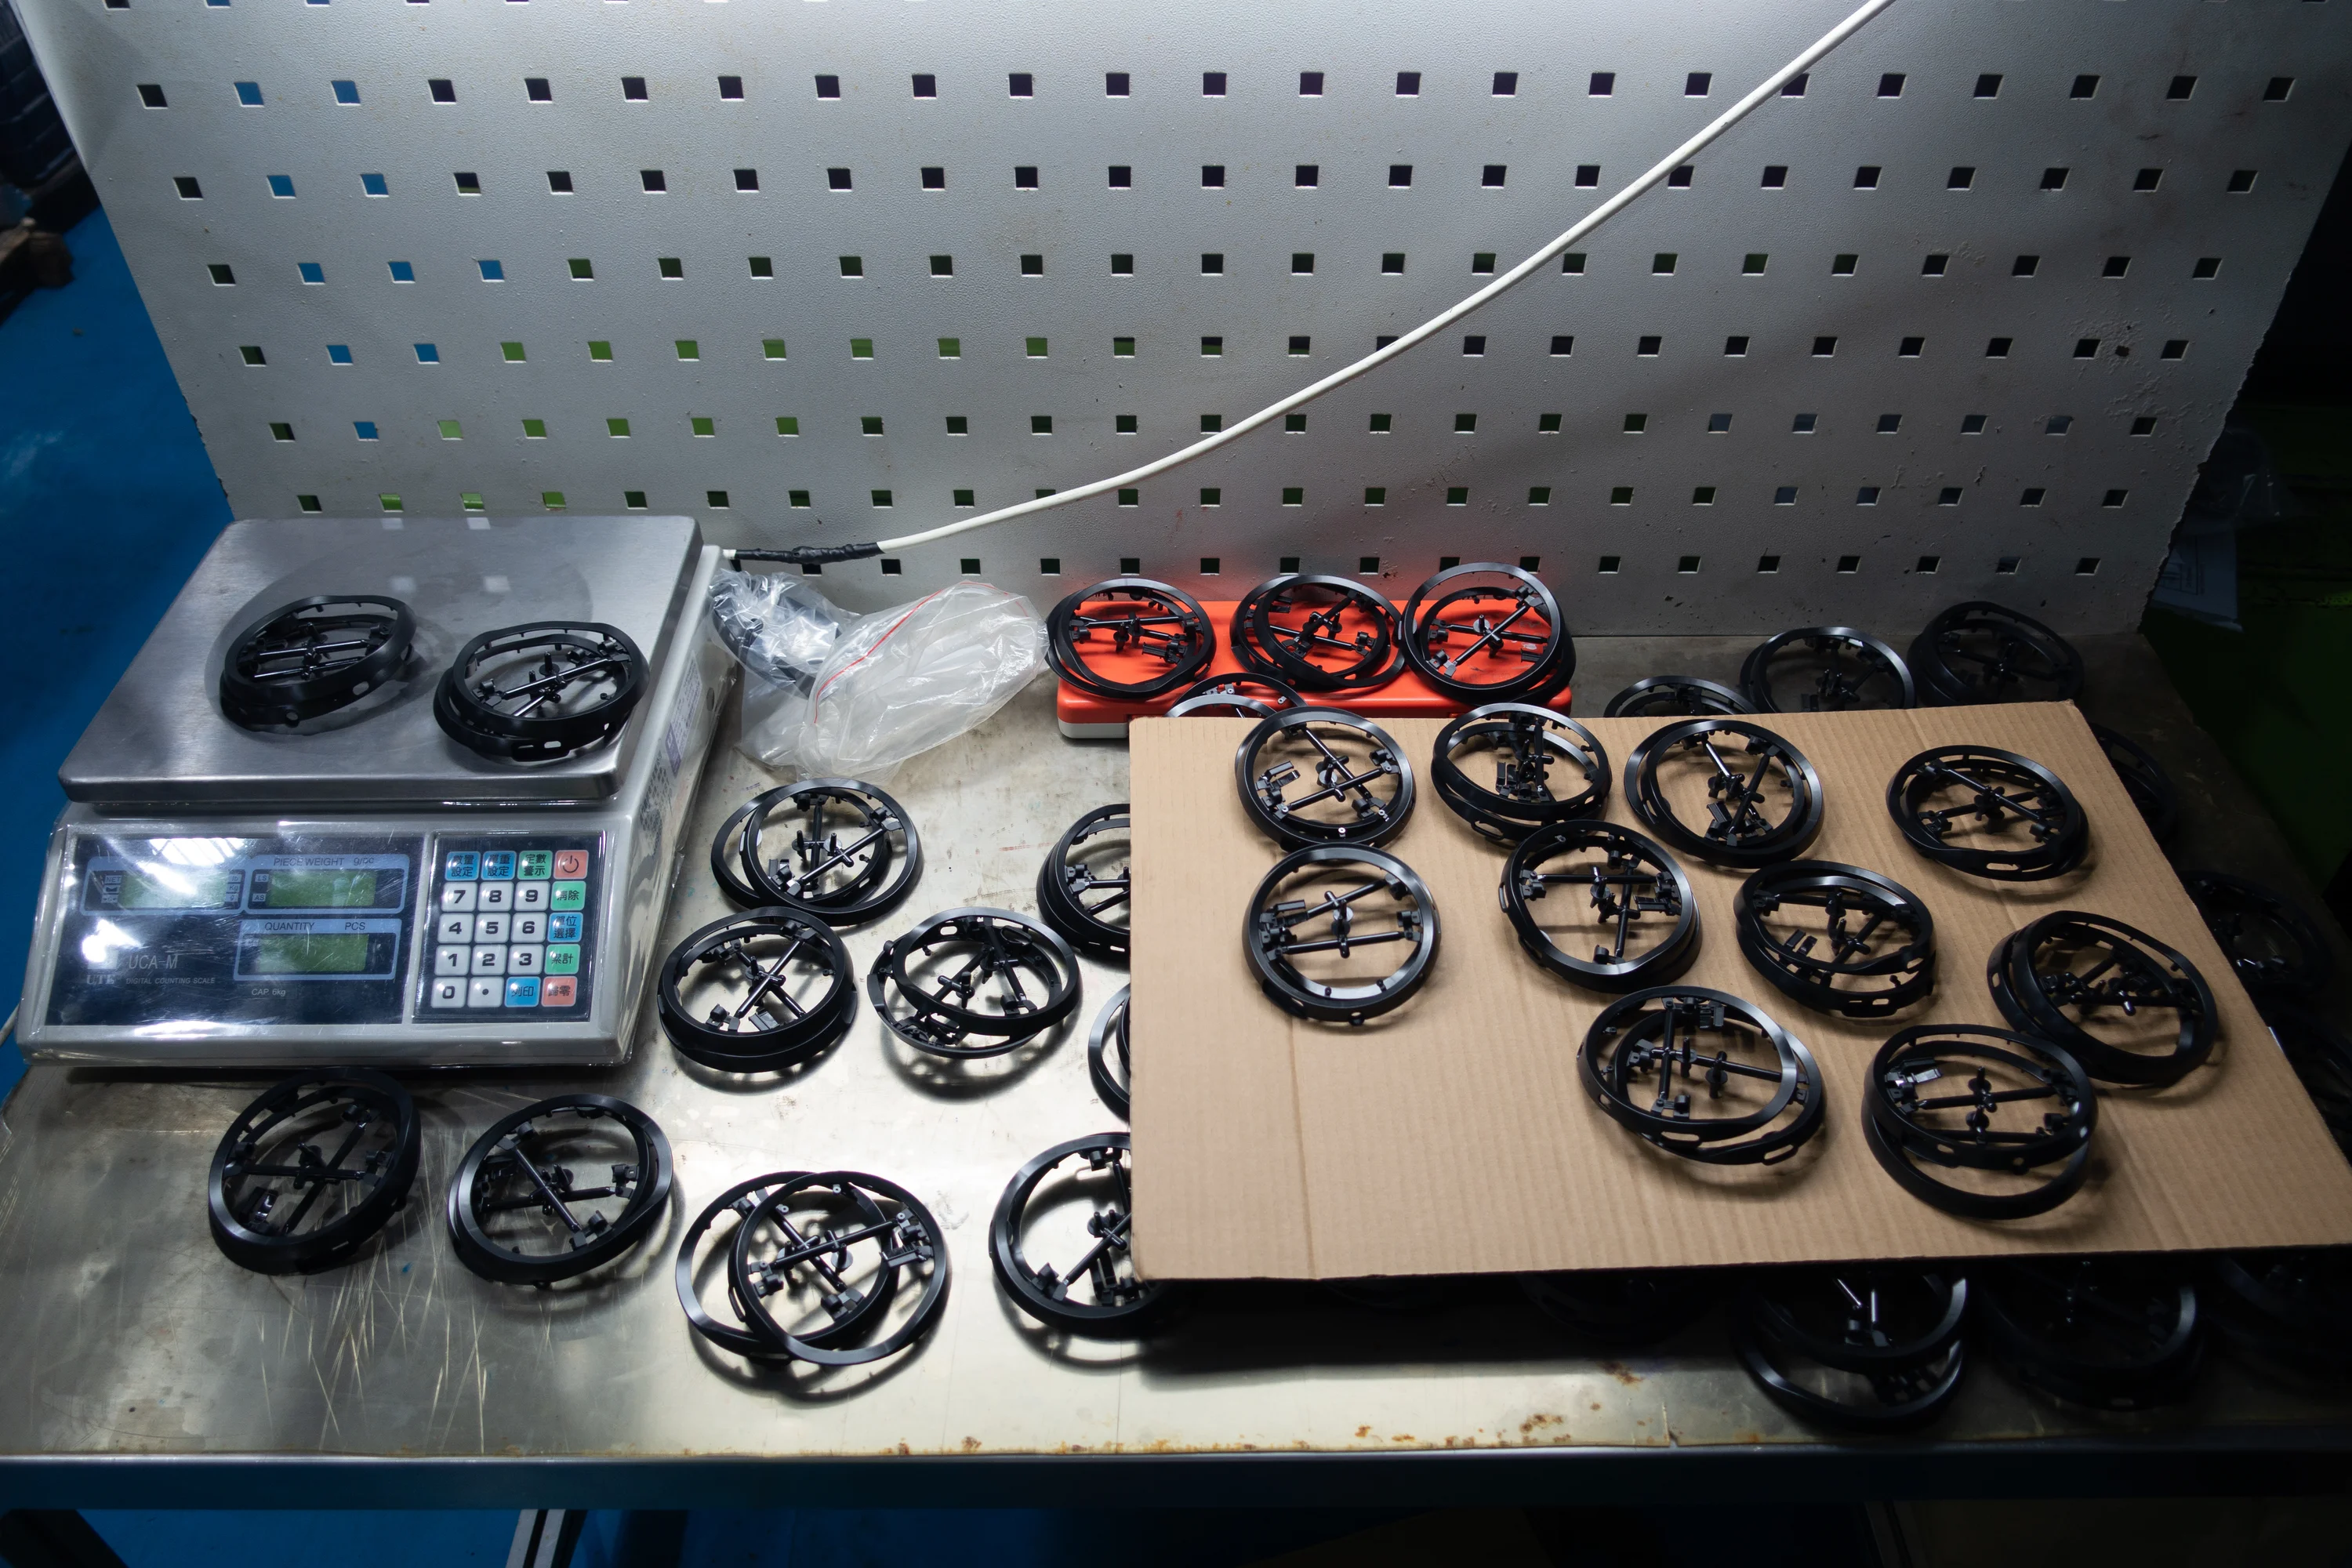
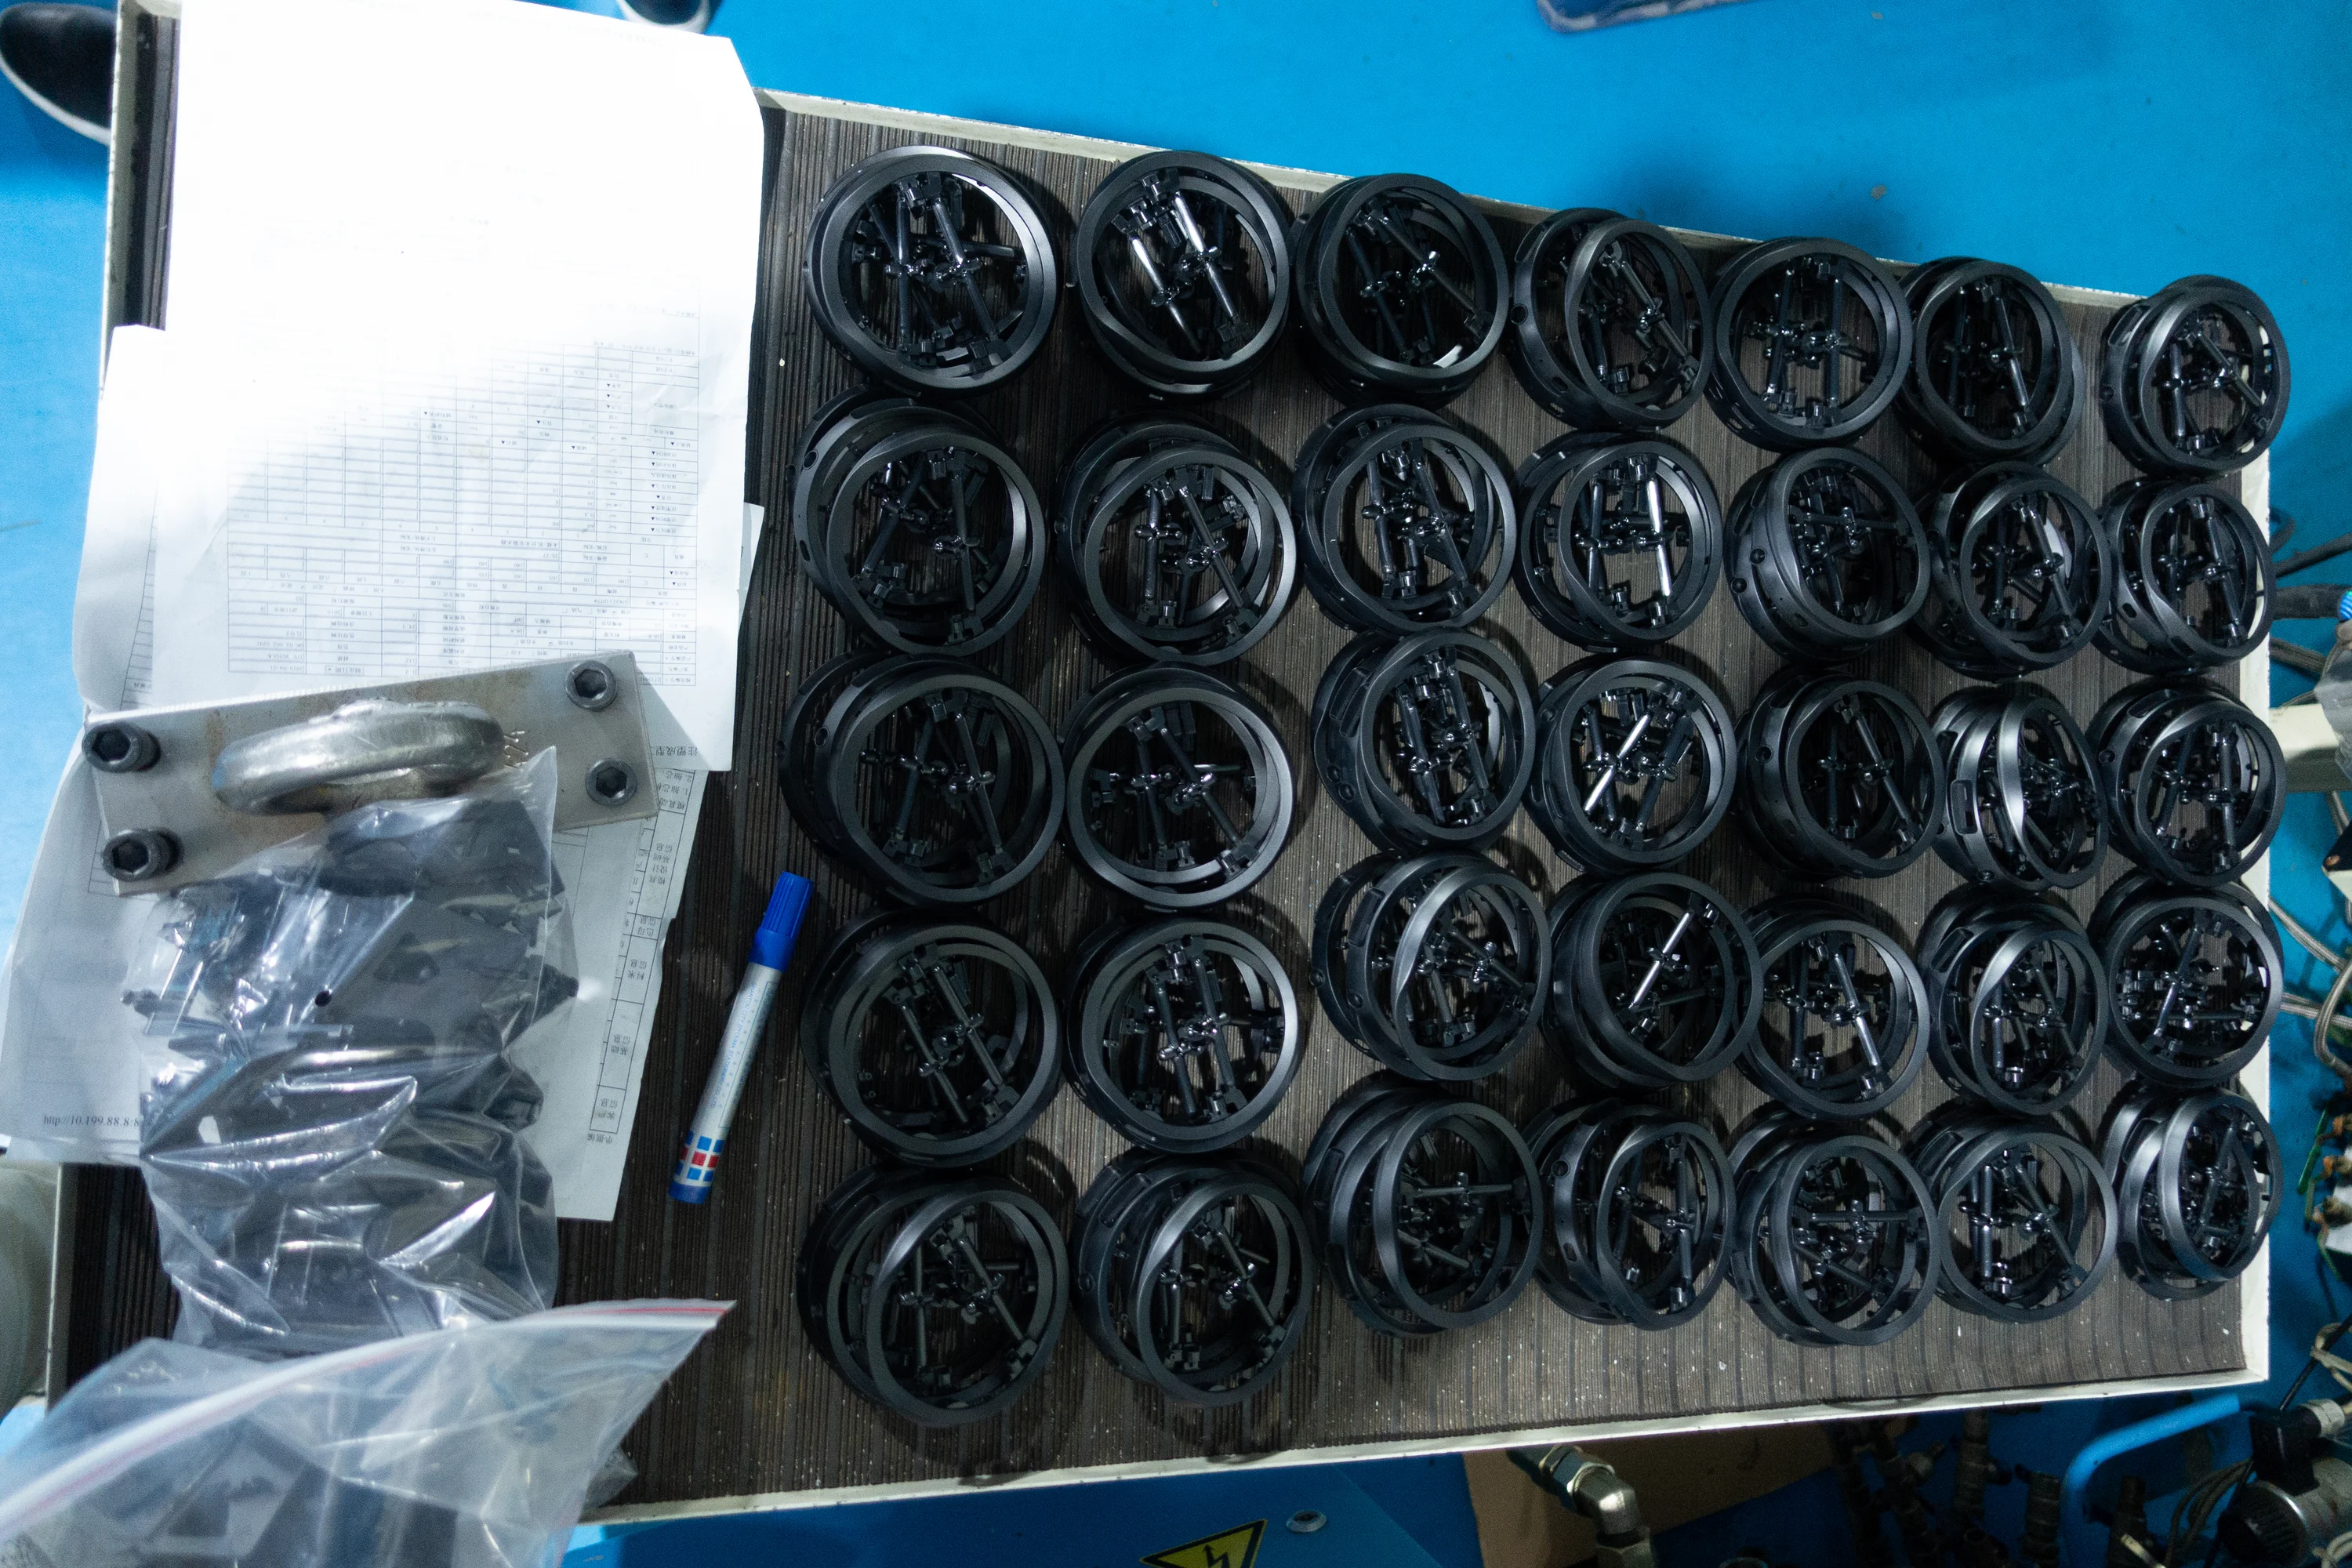
Tool trials and press-side inspection across the mechanical BOM.
The outer-headband tool
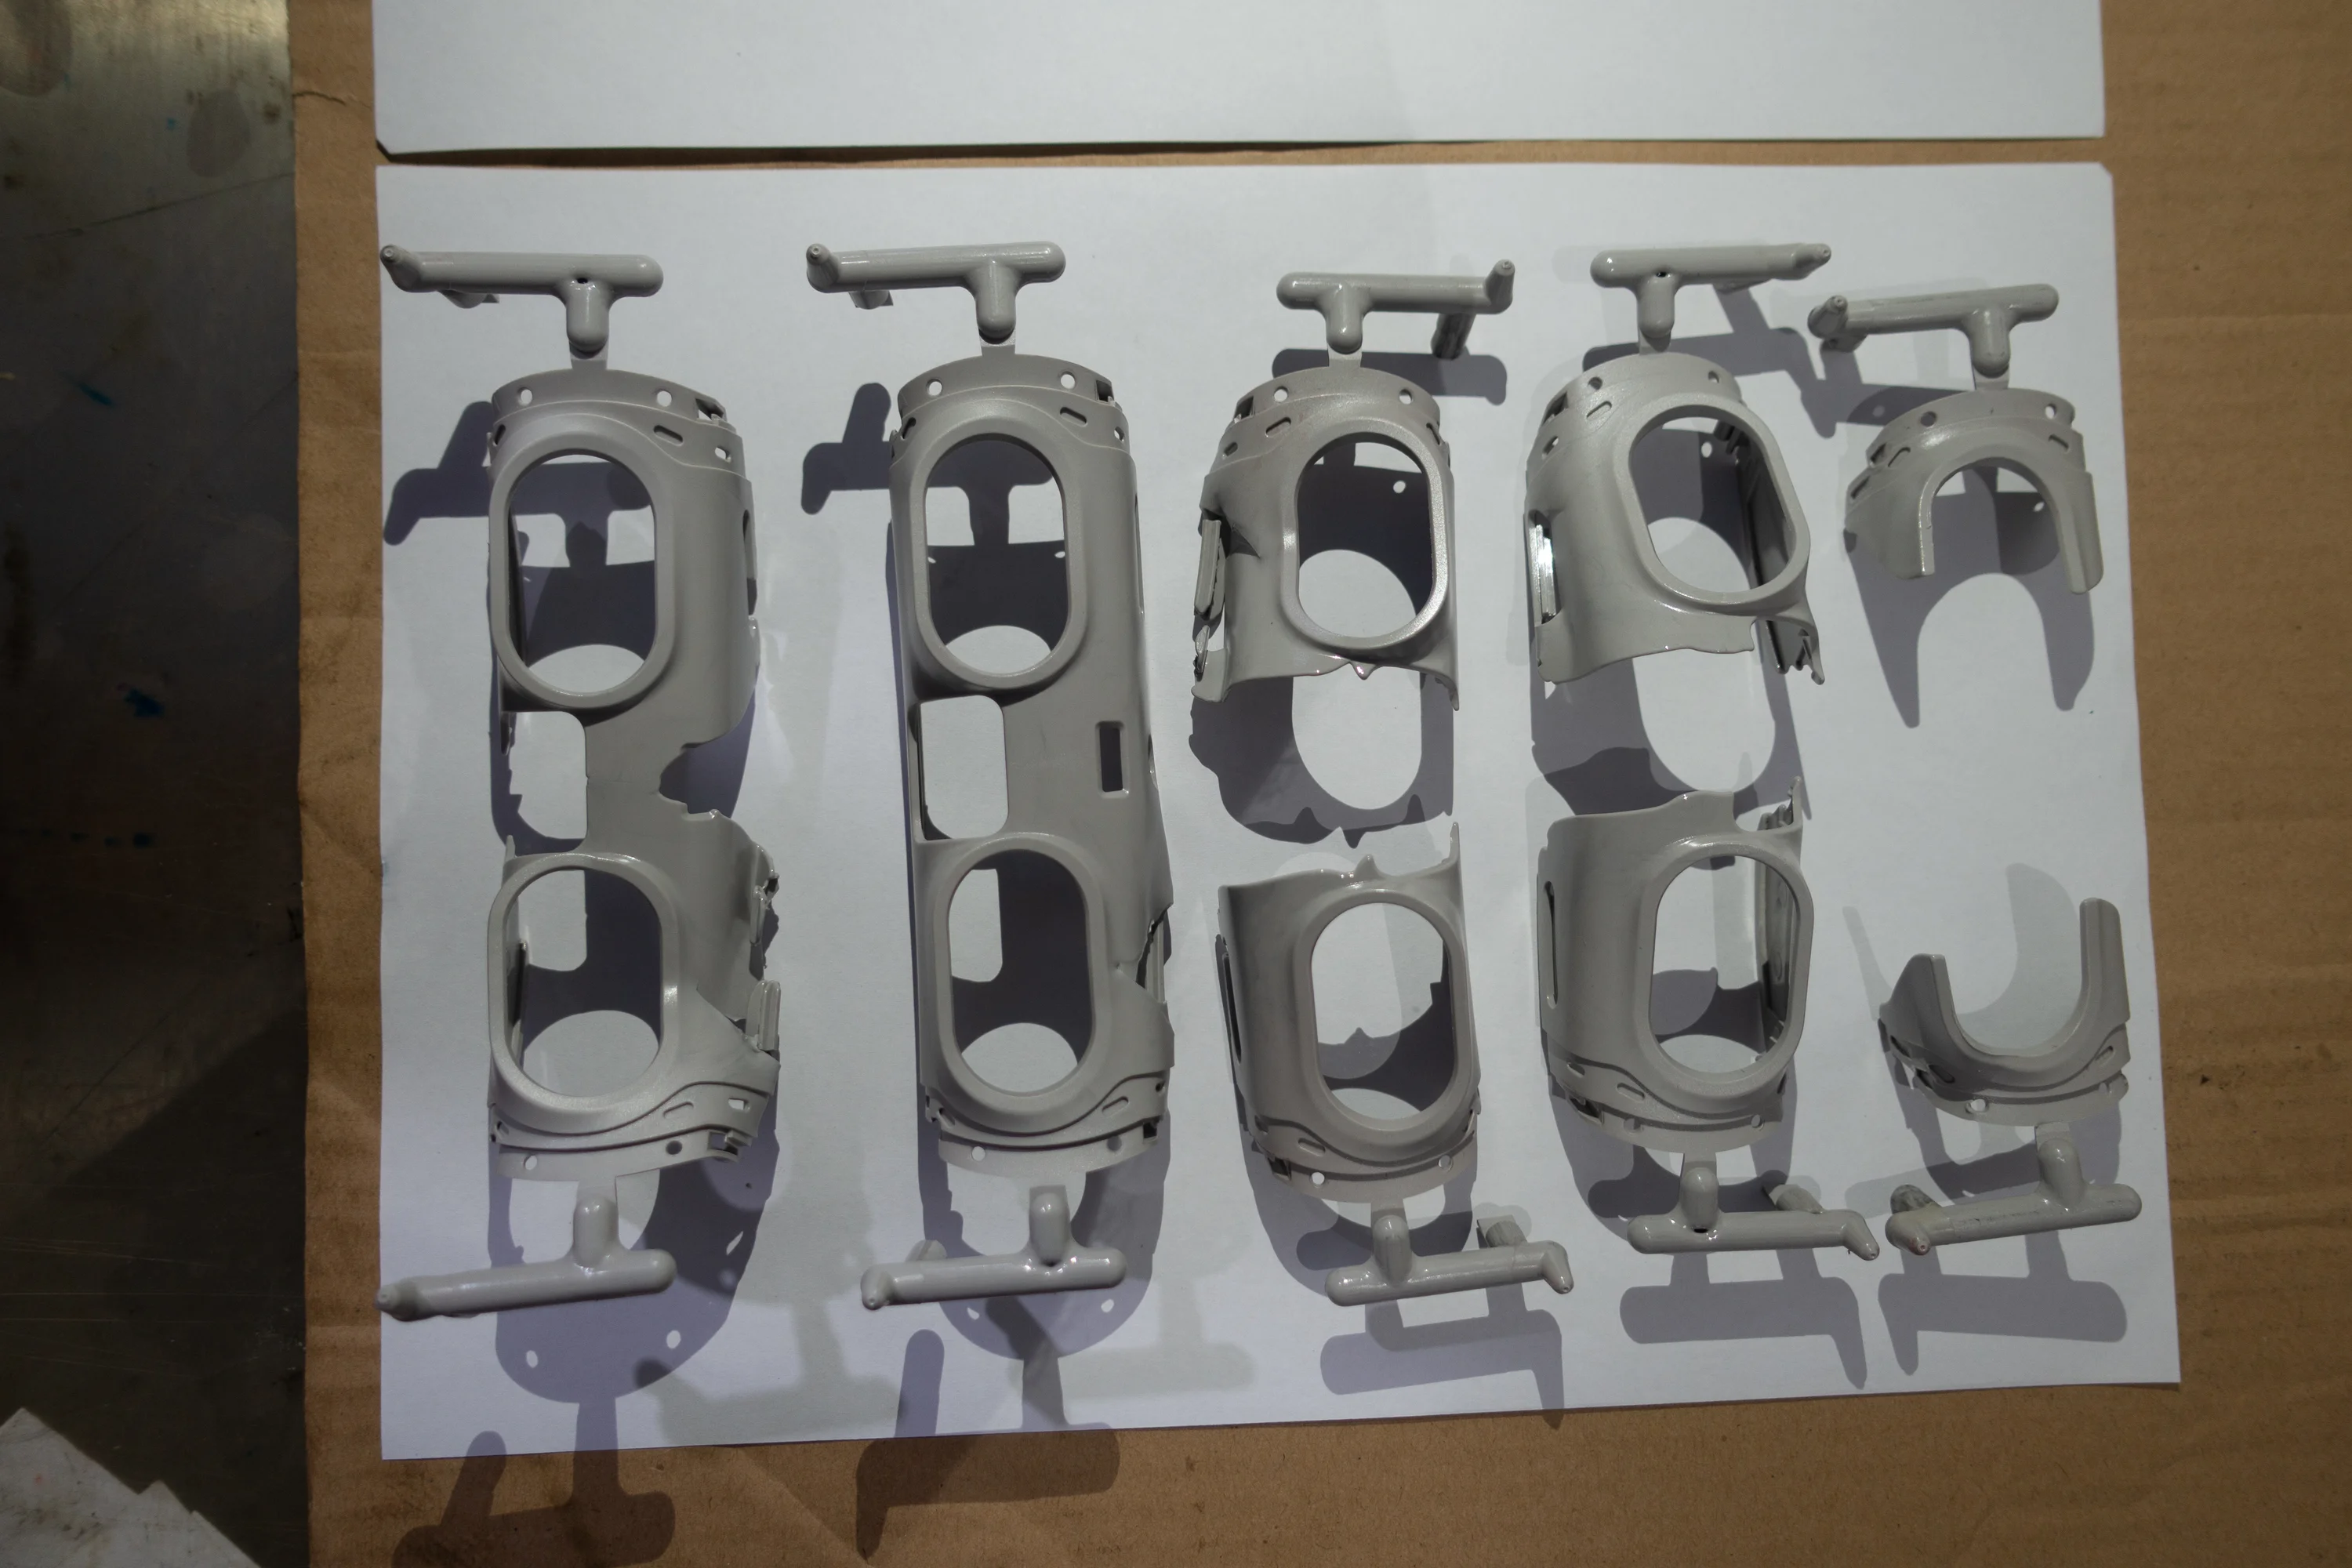
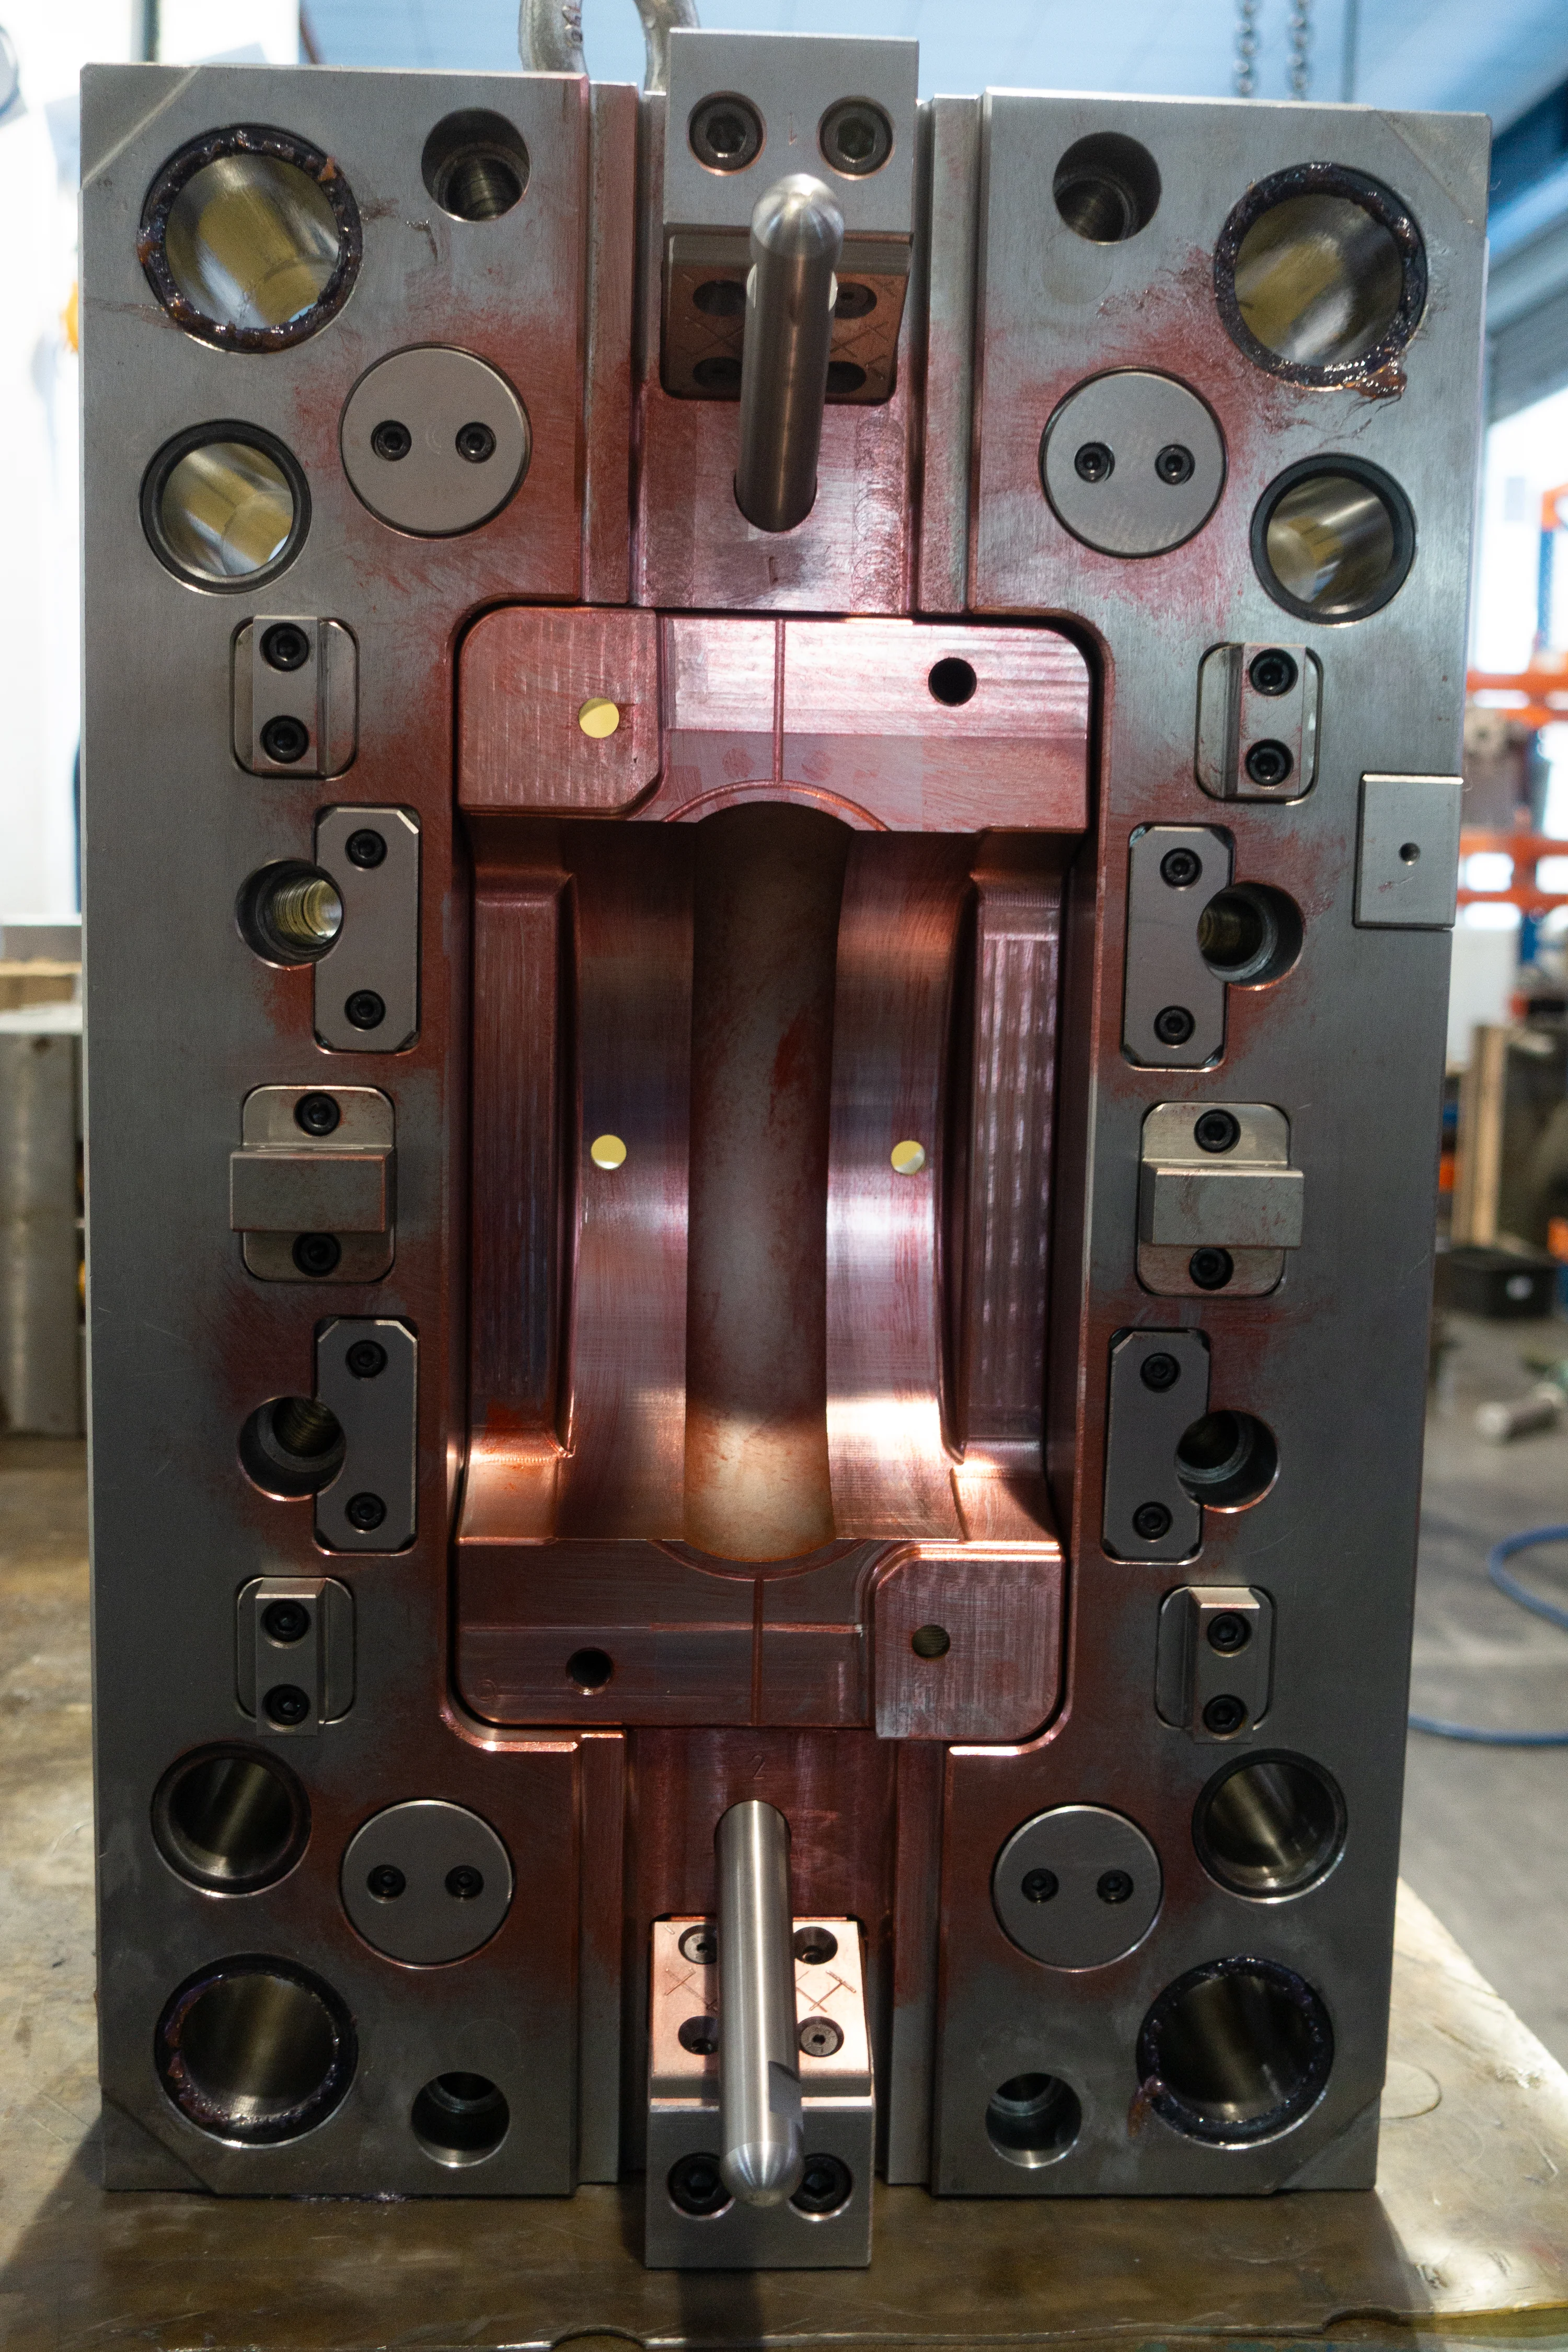
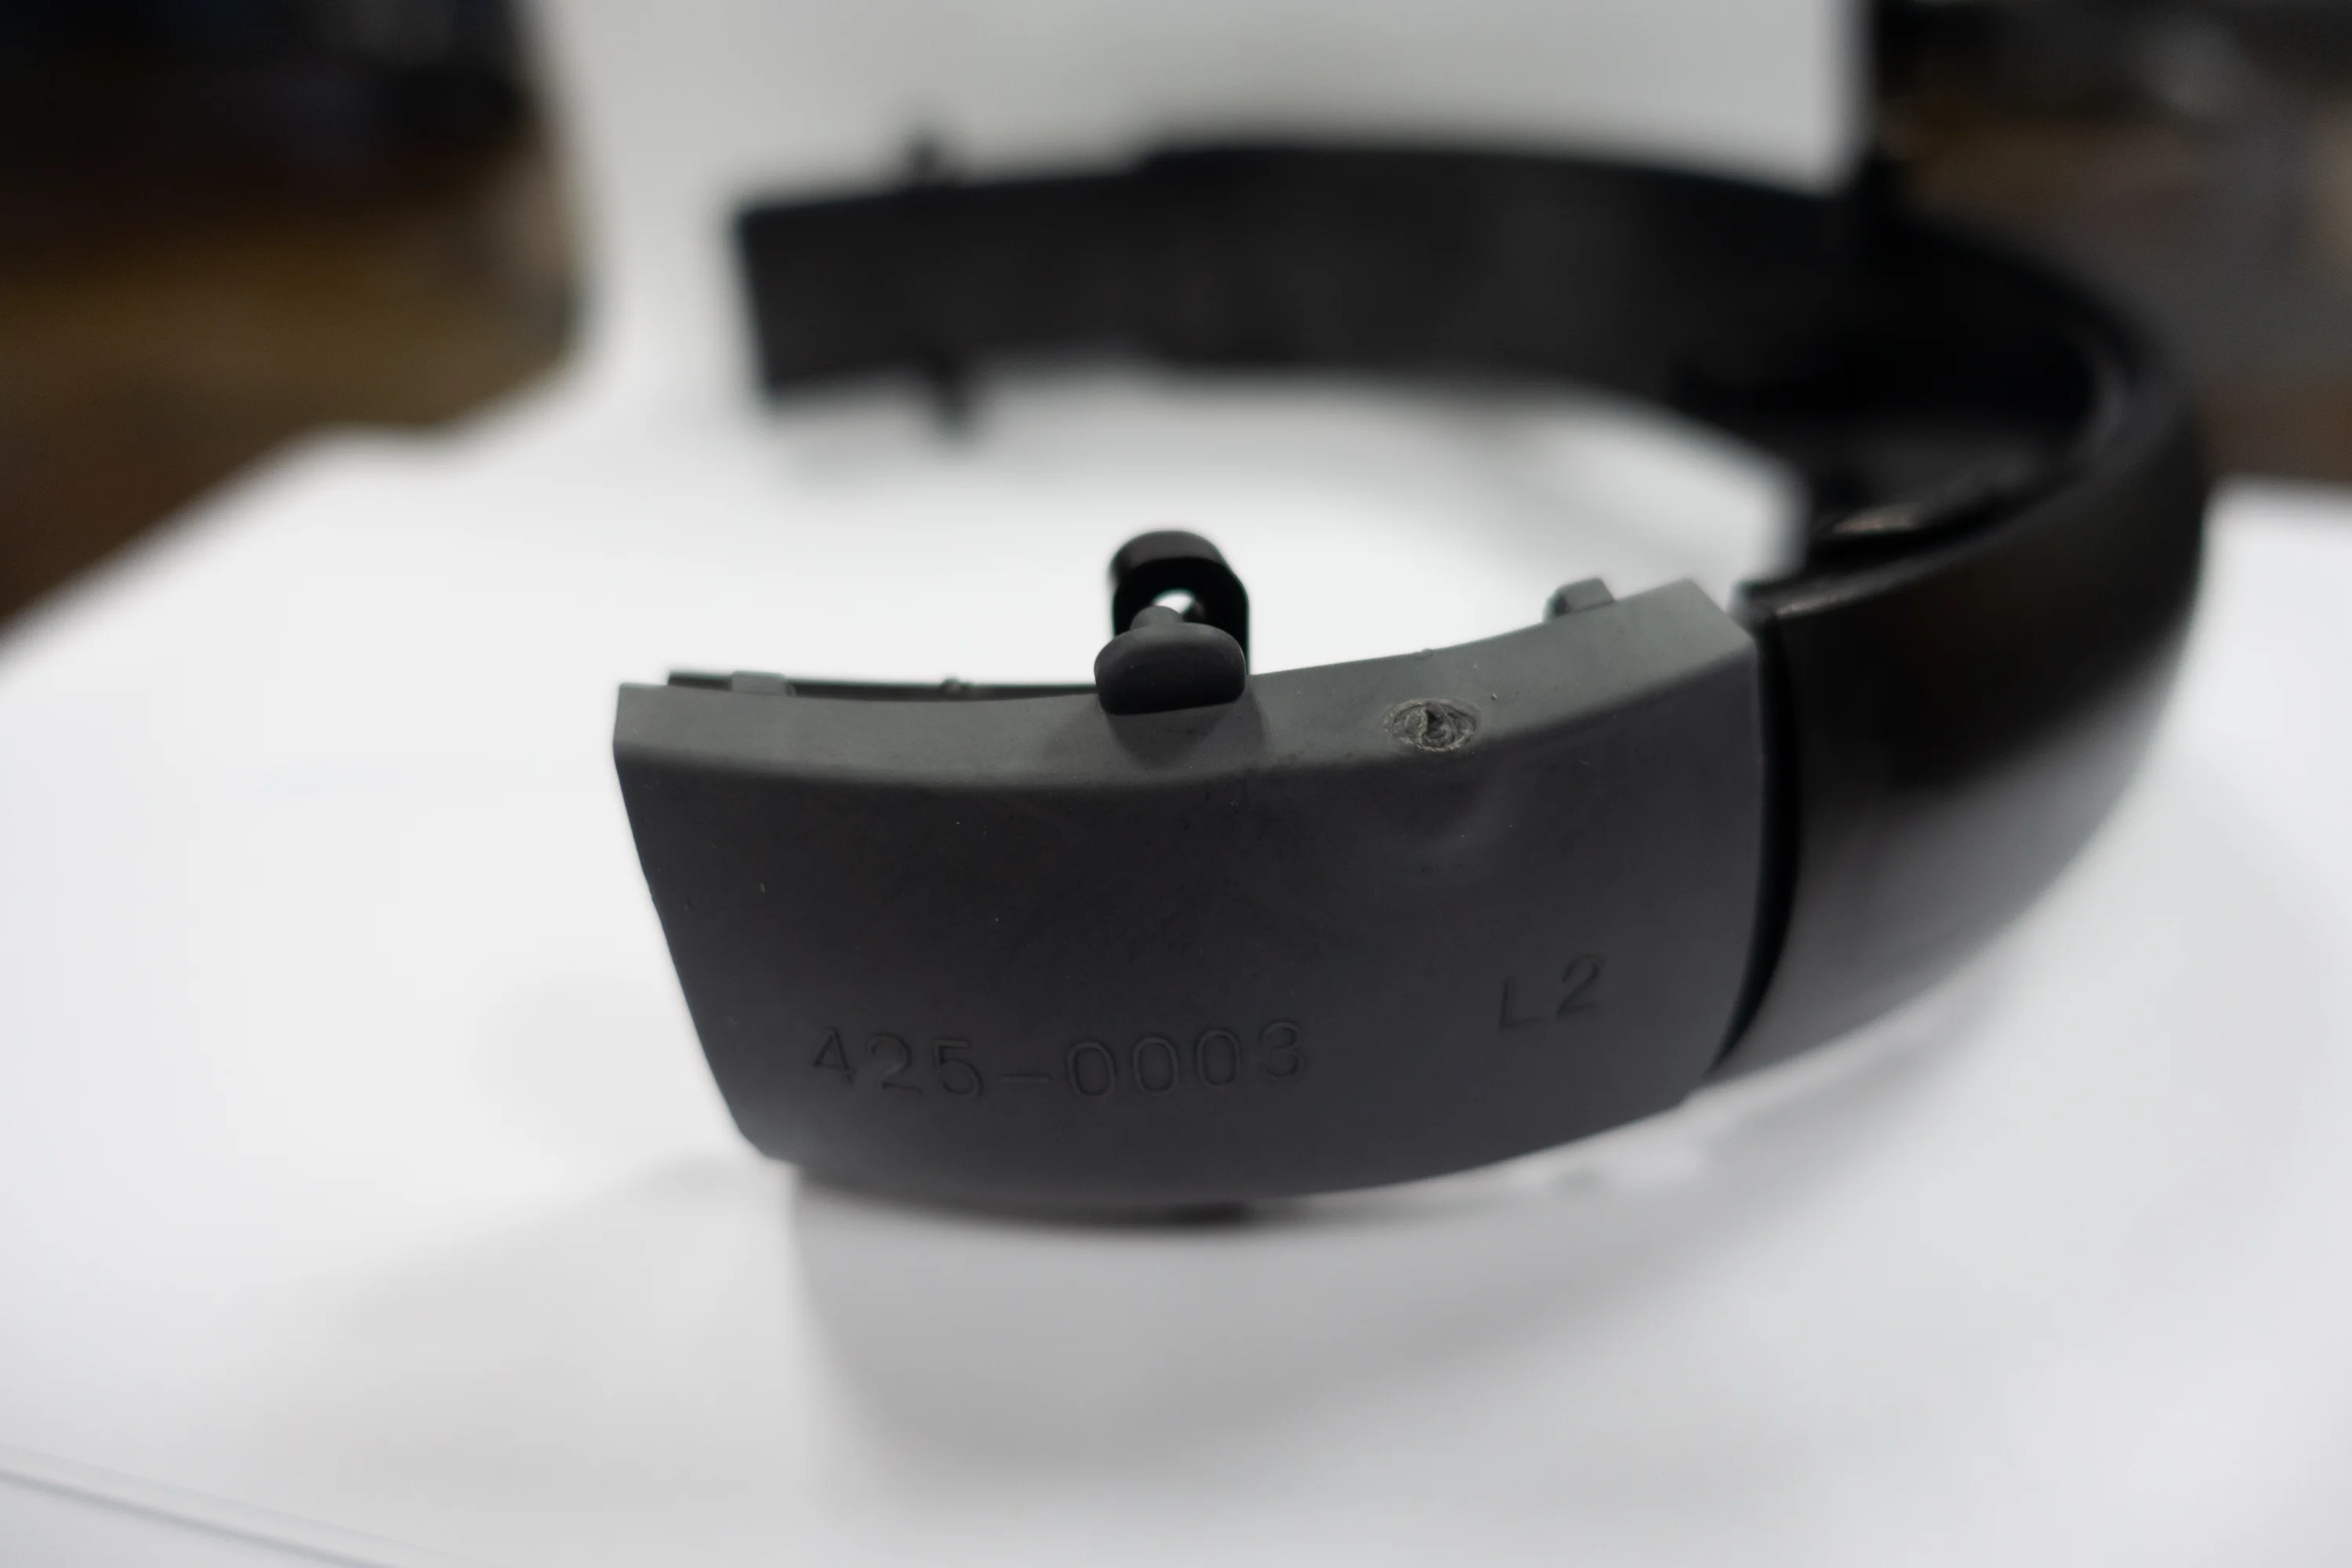
Of the roughly 40 tools I was responsible for on Glyph, the outer-headband tool was the trickiest. The part, 425-0003, was a sweeping arch nearly 200 mm across, molded in SABIC EXL1414 impact-modified polycarbonate.
Moving to a hot-runner setup was a big part of getting the outer-headband molding to work. I ended up tuning the process parameters to produce the right as-molded part weight. That gave us parts that could eject and then cool into the right shape and size, repeatably. This kind of process tuning is familiar work in plastic molding. What made the headband difficult was how sensitive the whole part and tooling system was.
 From the workbench
Recovering the outer-headband molding process
Mold flow, knit-line cracks, tool actions and ejection trials explain why getting an intact part was only the beginning.
Explore investigation +Close investigation −
Recovering the outer-headband molding process
Mold flow, knit-line cracks, tool actions and ejection trials explain why getting an intact part was only the beginning.
Explore investigation +Close investigation −The arch also carried small tabs, clips and locating features. Fifteen M1.6 brass inserts were installed ultrasonically in three different setups. The CMF specification called for four different molding finishes across its surfaces, including SPI-A1-polished areas where gates and parting lines were prohibited.
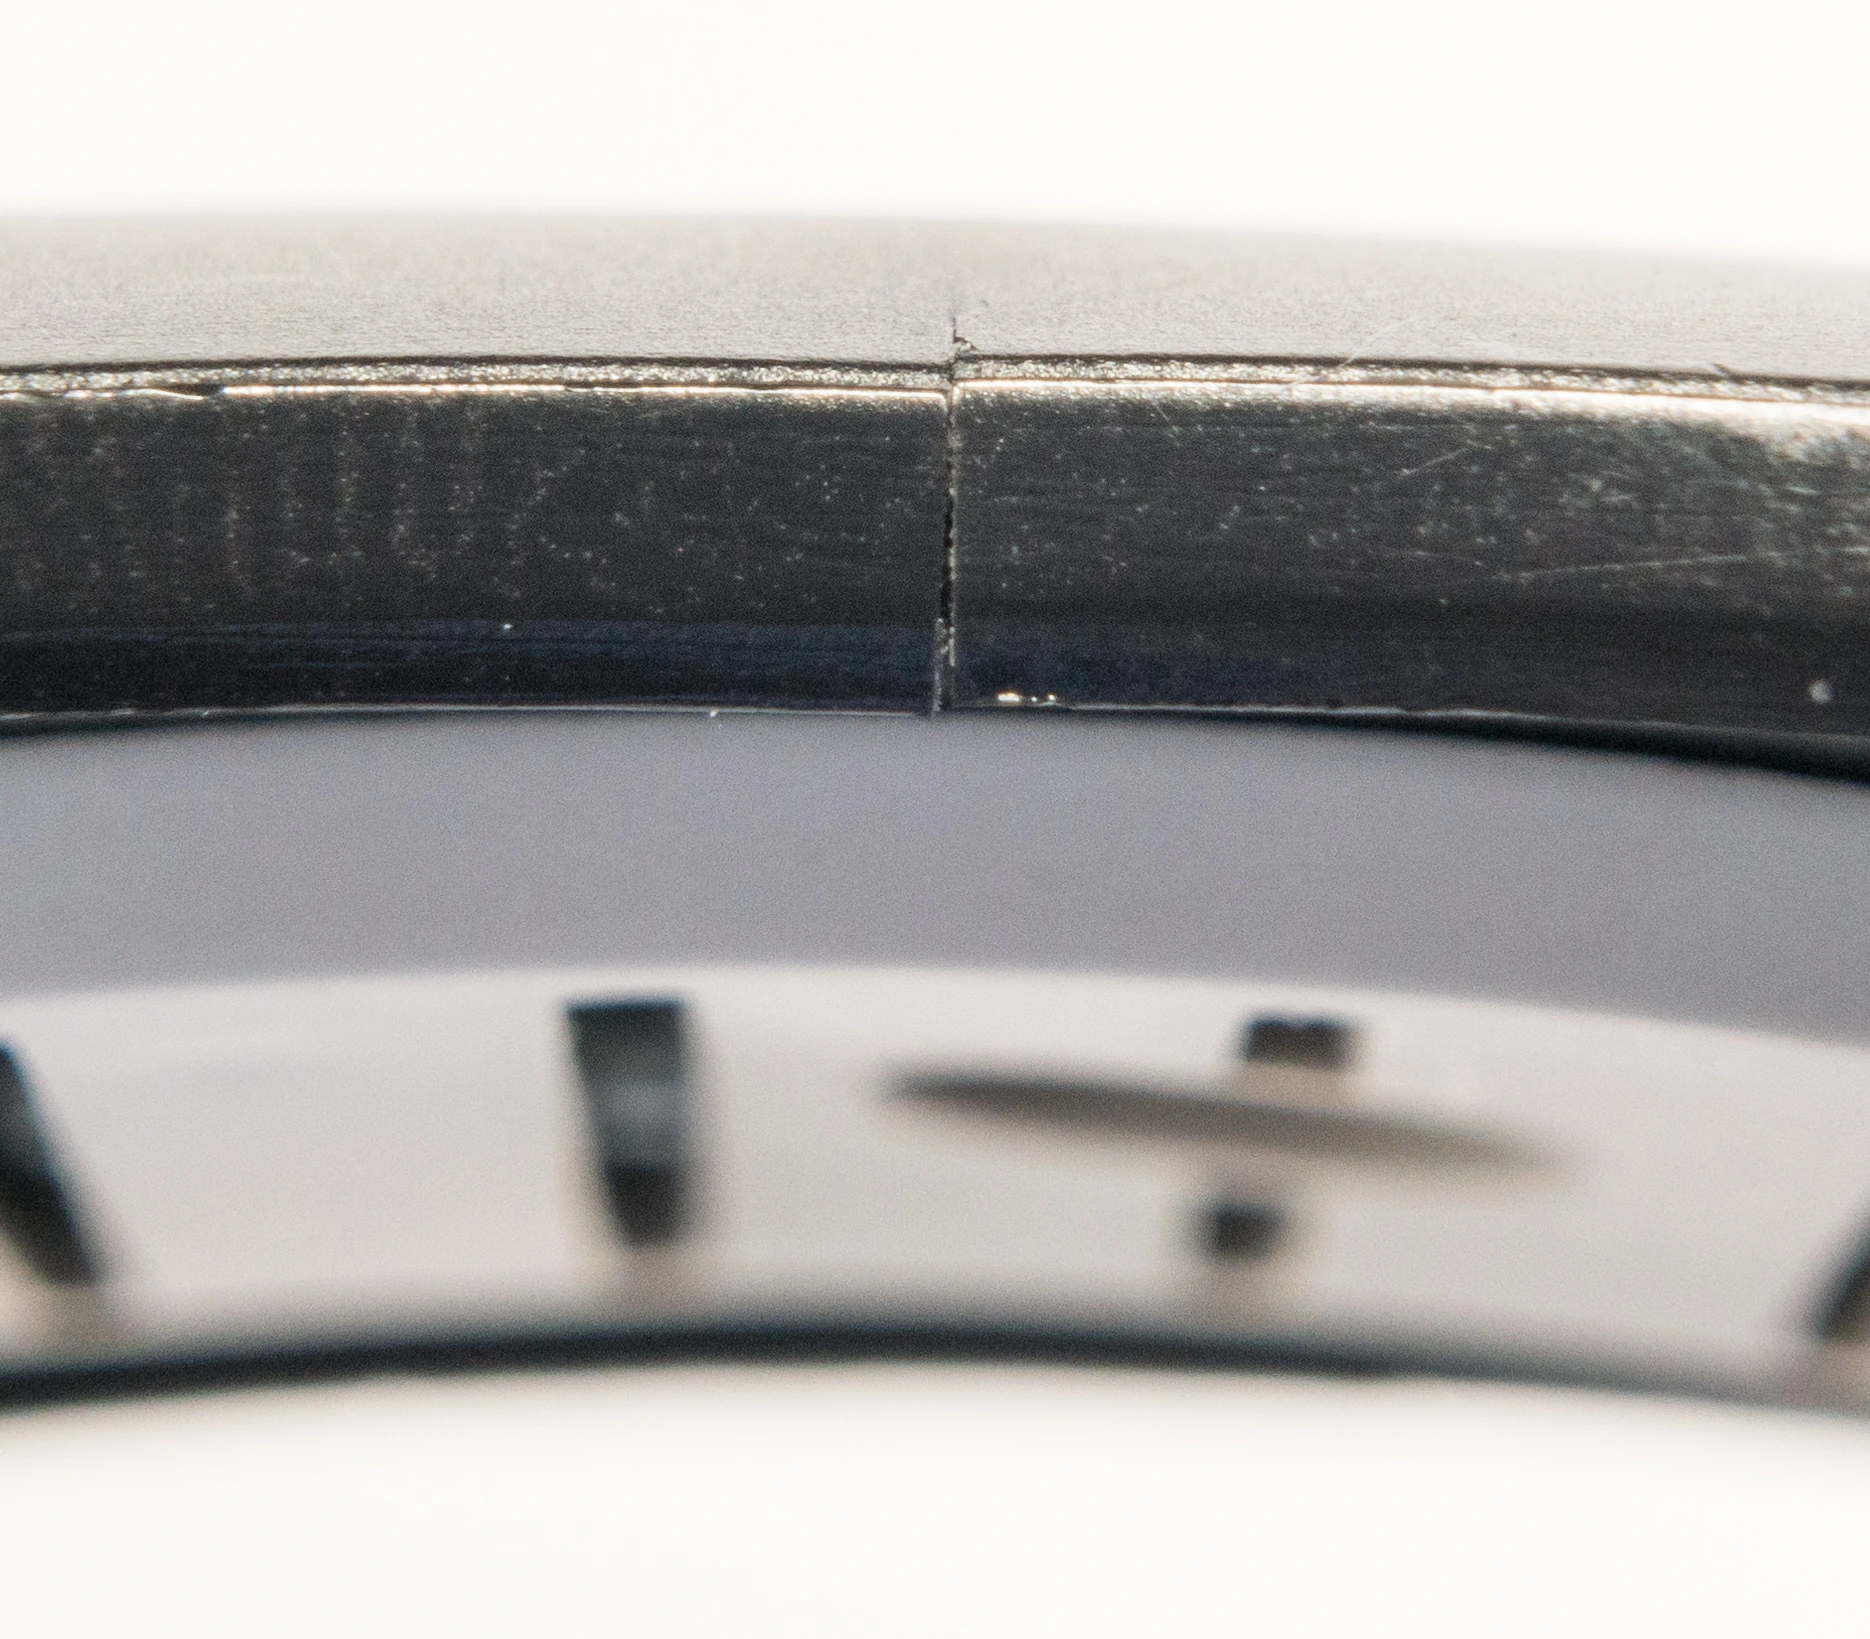
Moldflow analysis
Mold-flow simulations were not always accurate, but in this case the early trials developed structural knit lines precisely where the model predicted them. The headbands cracked under normal flexing, right at those knit lines. Tuning the molding parameters eliminated the structural problems.
Knit-line cracking
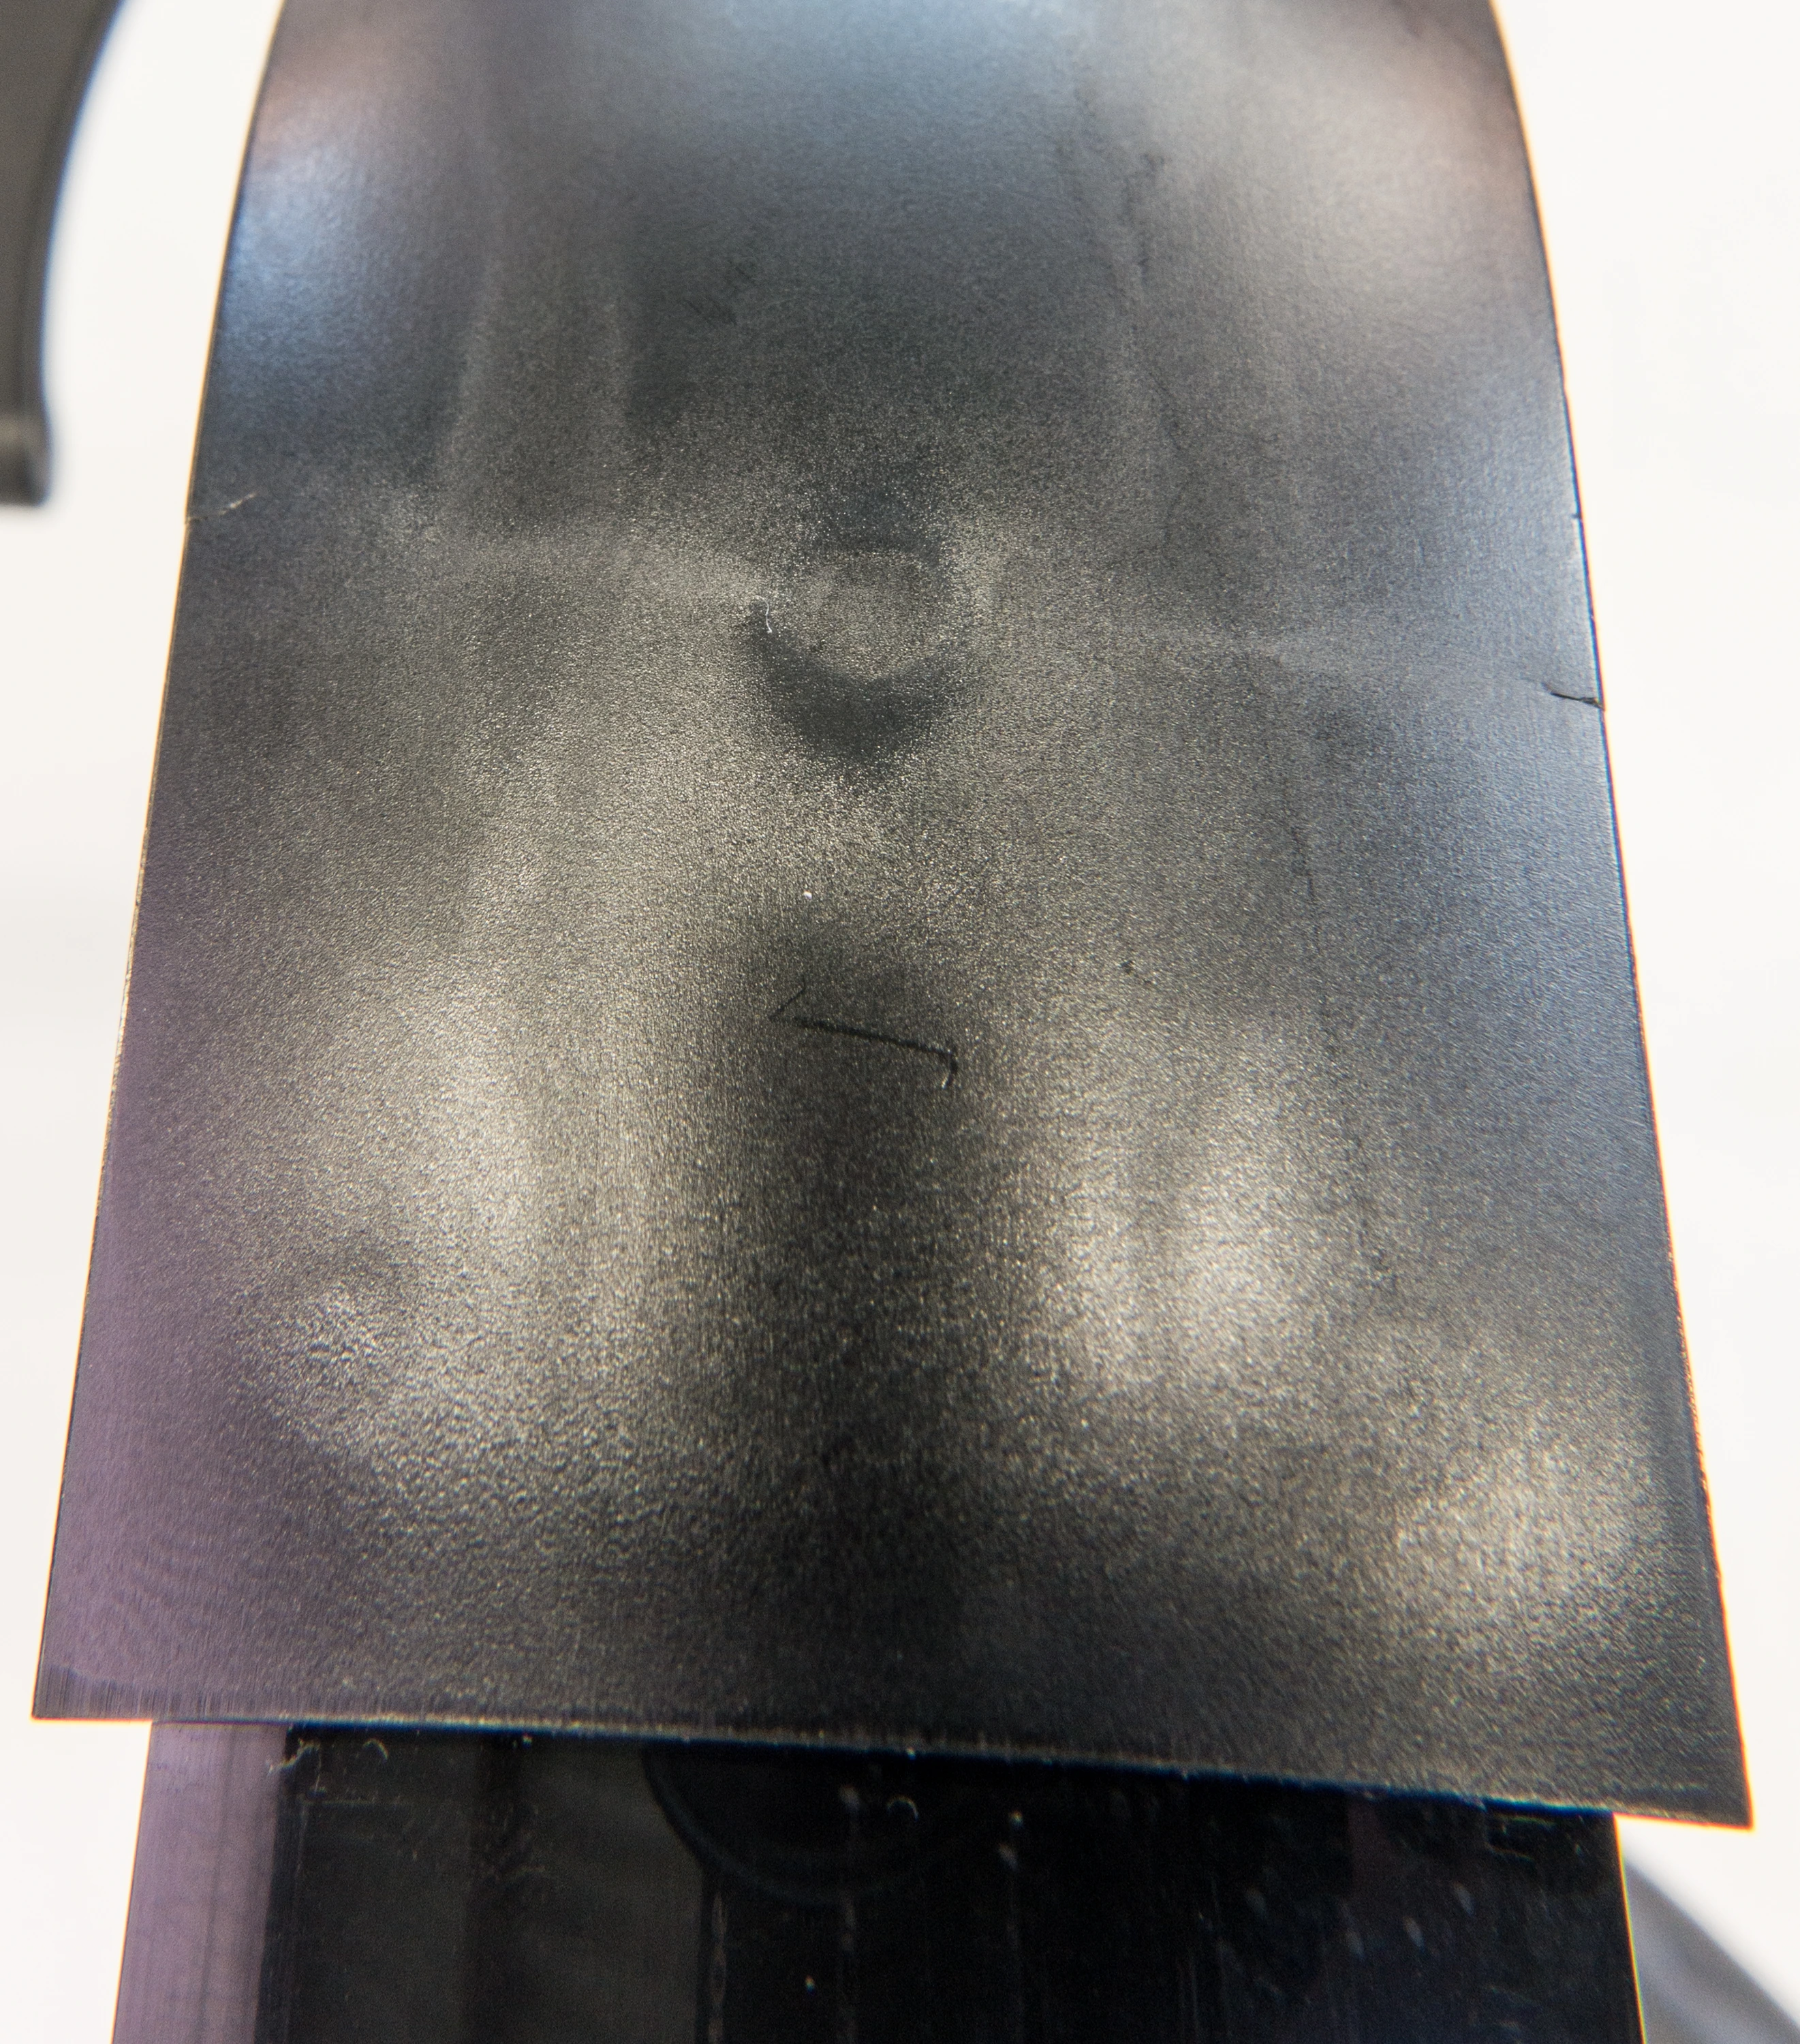
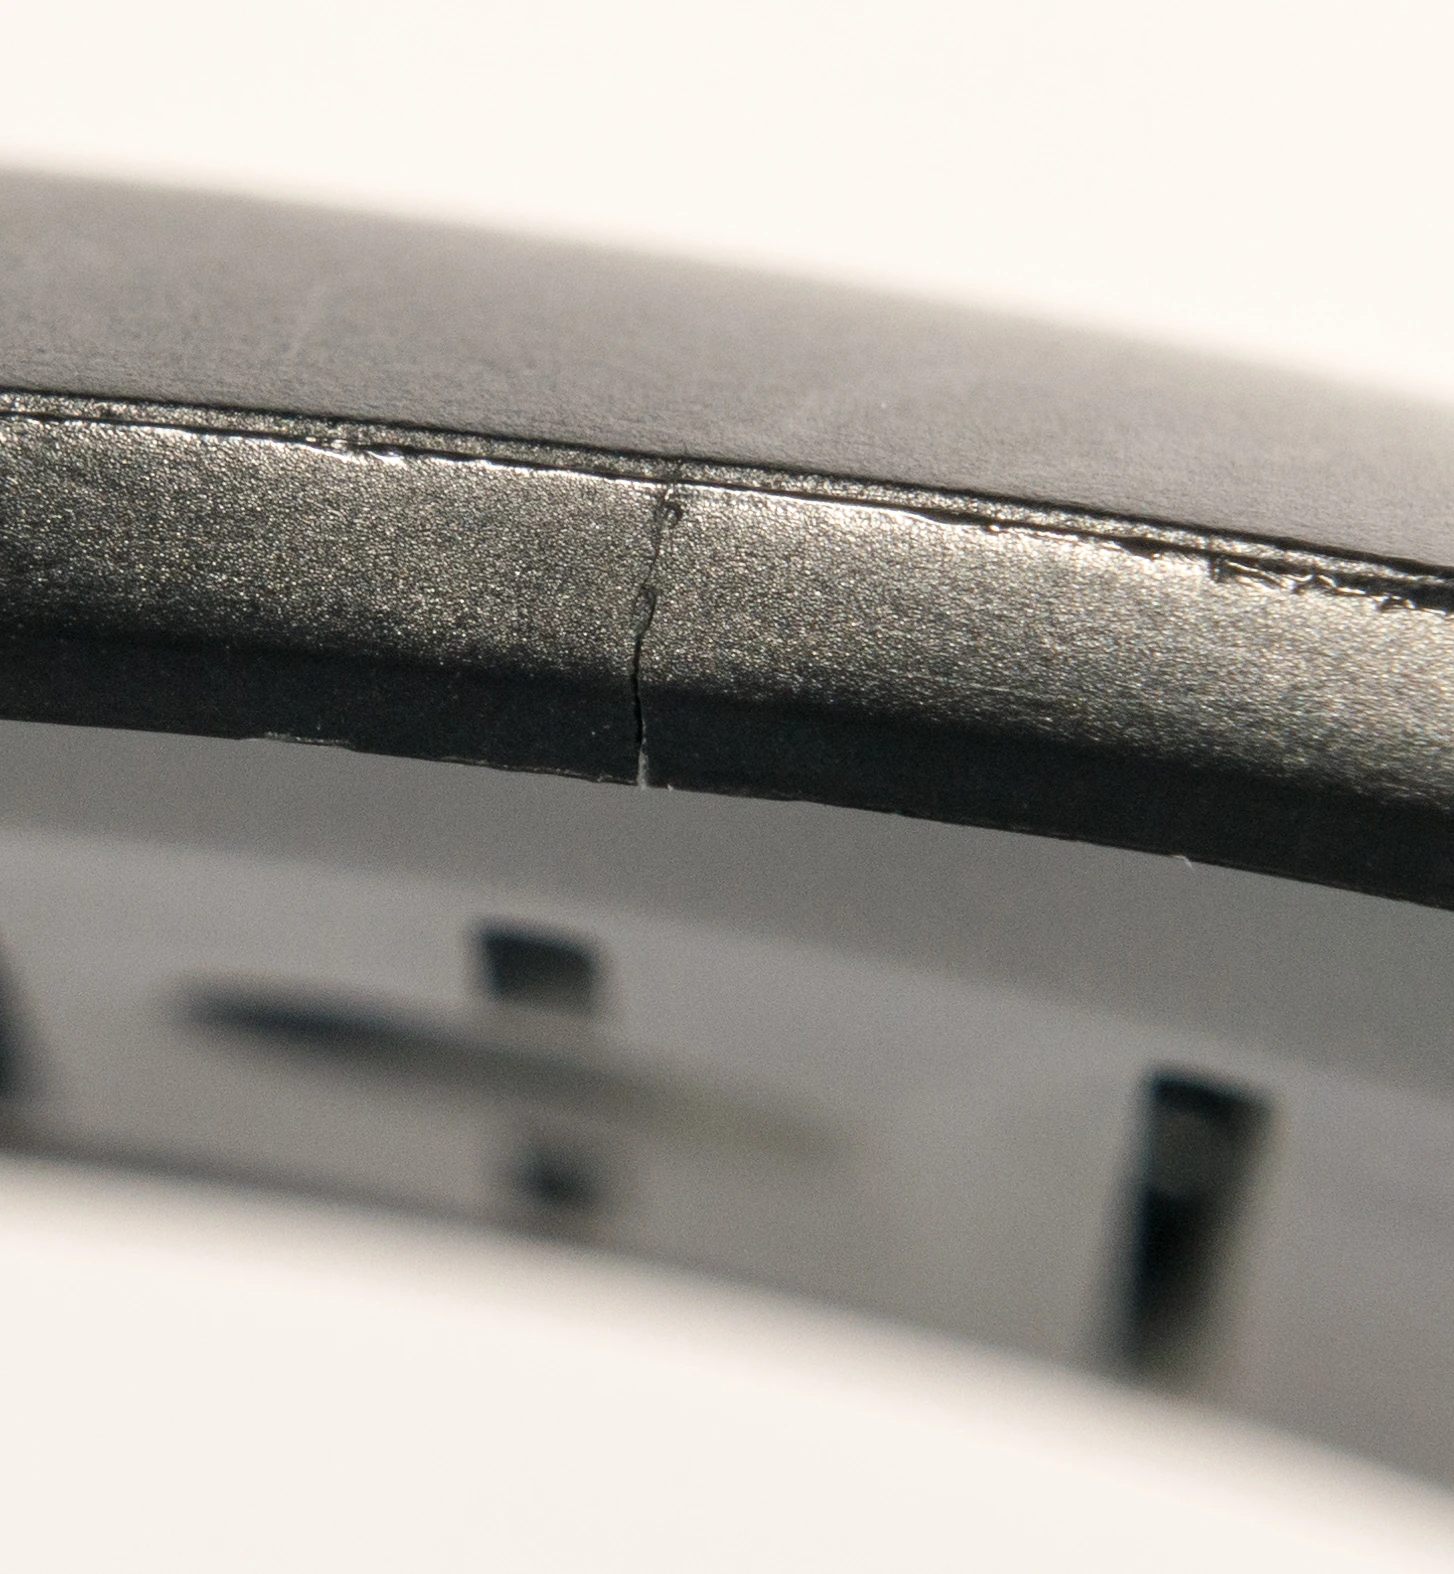
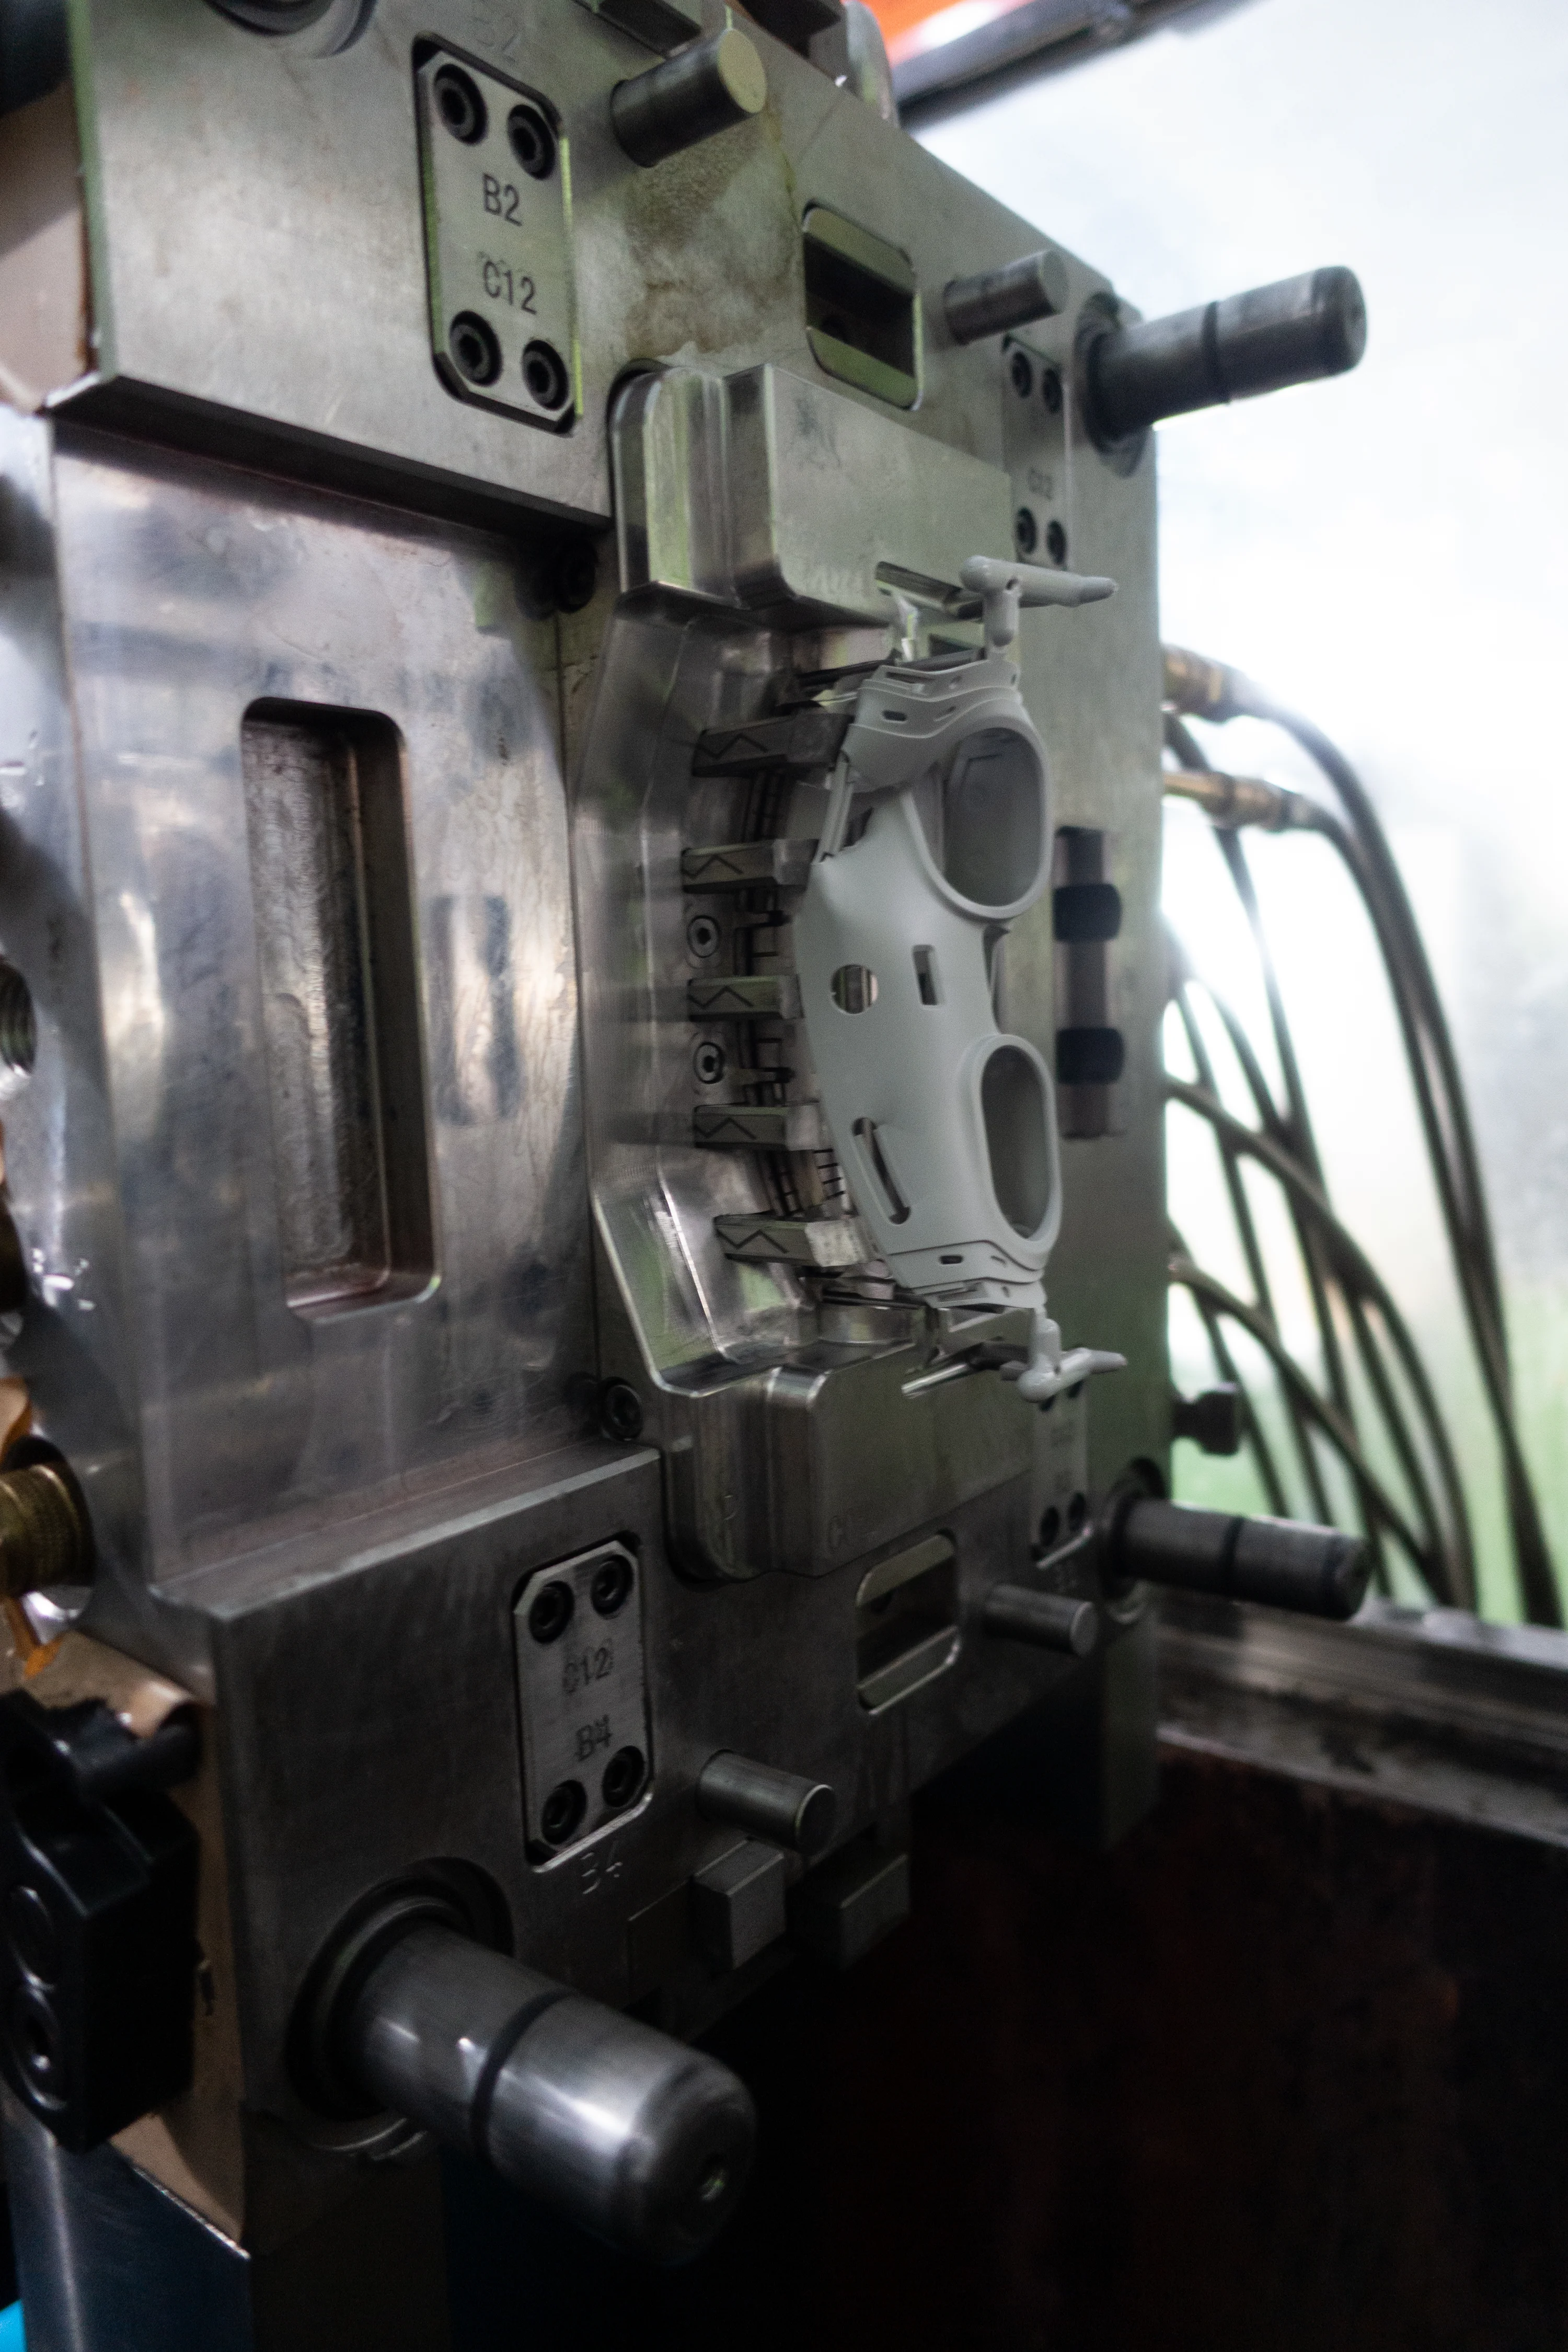
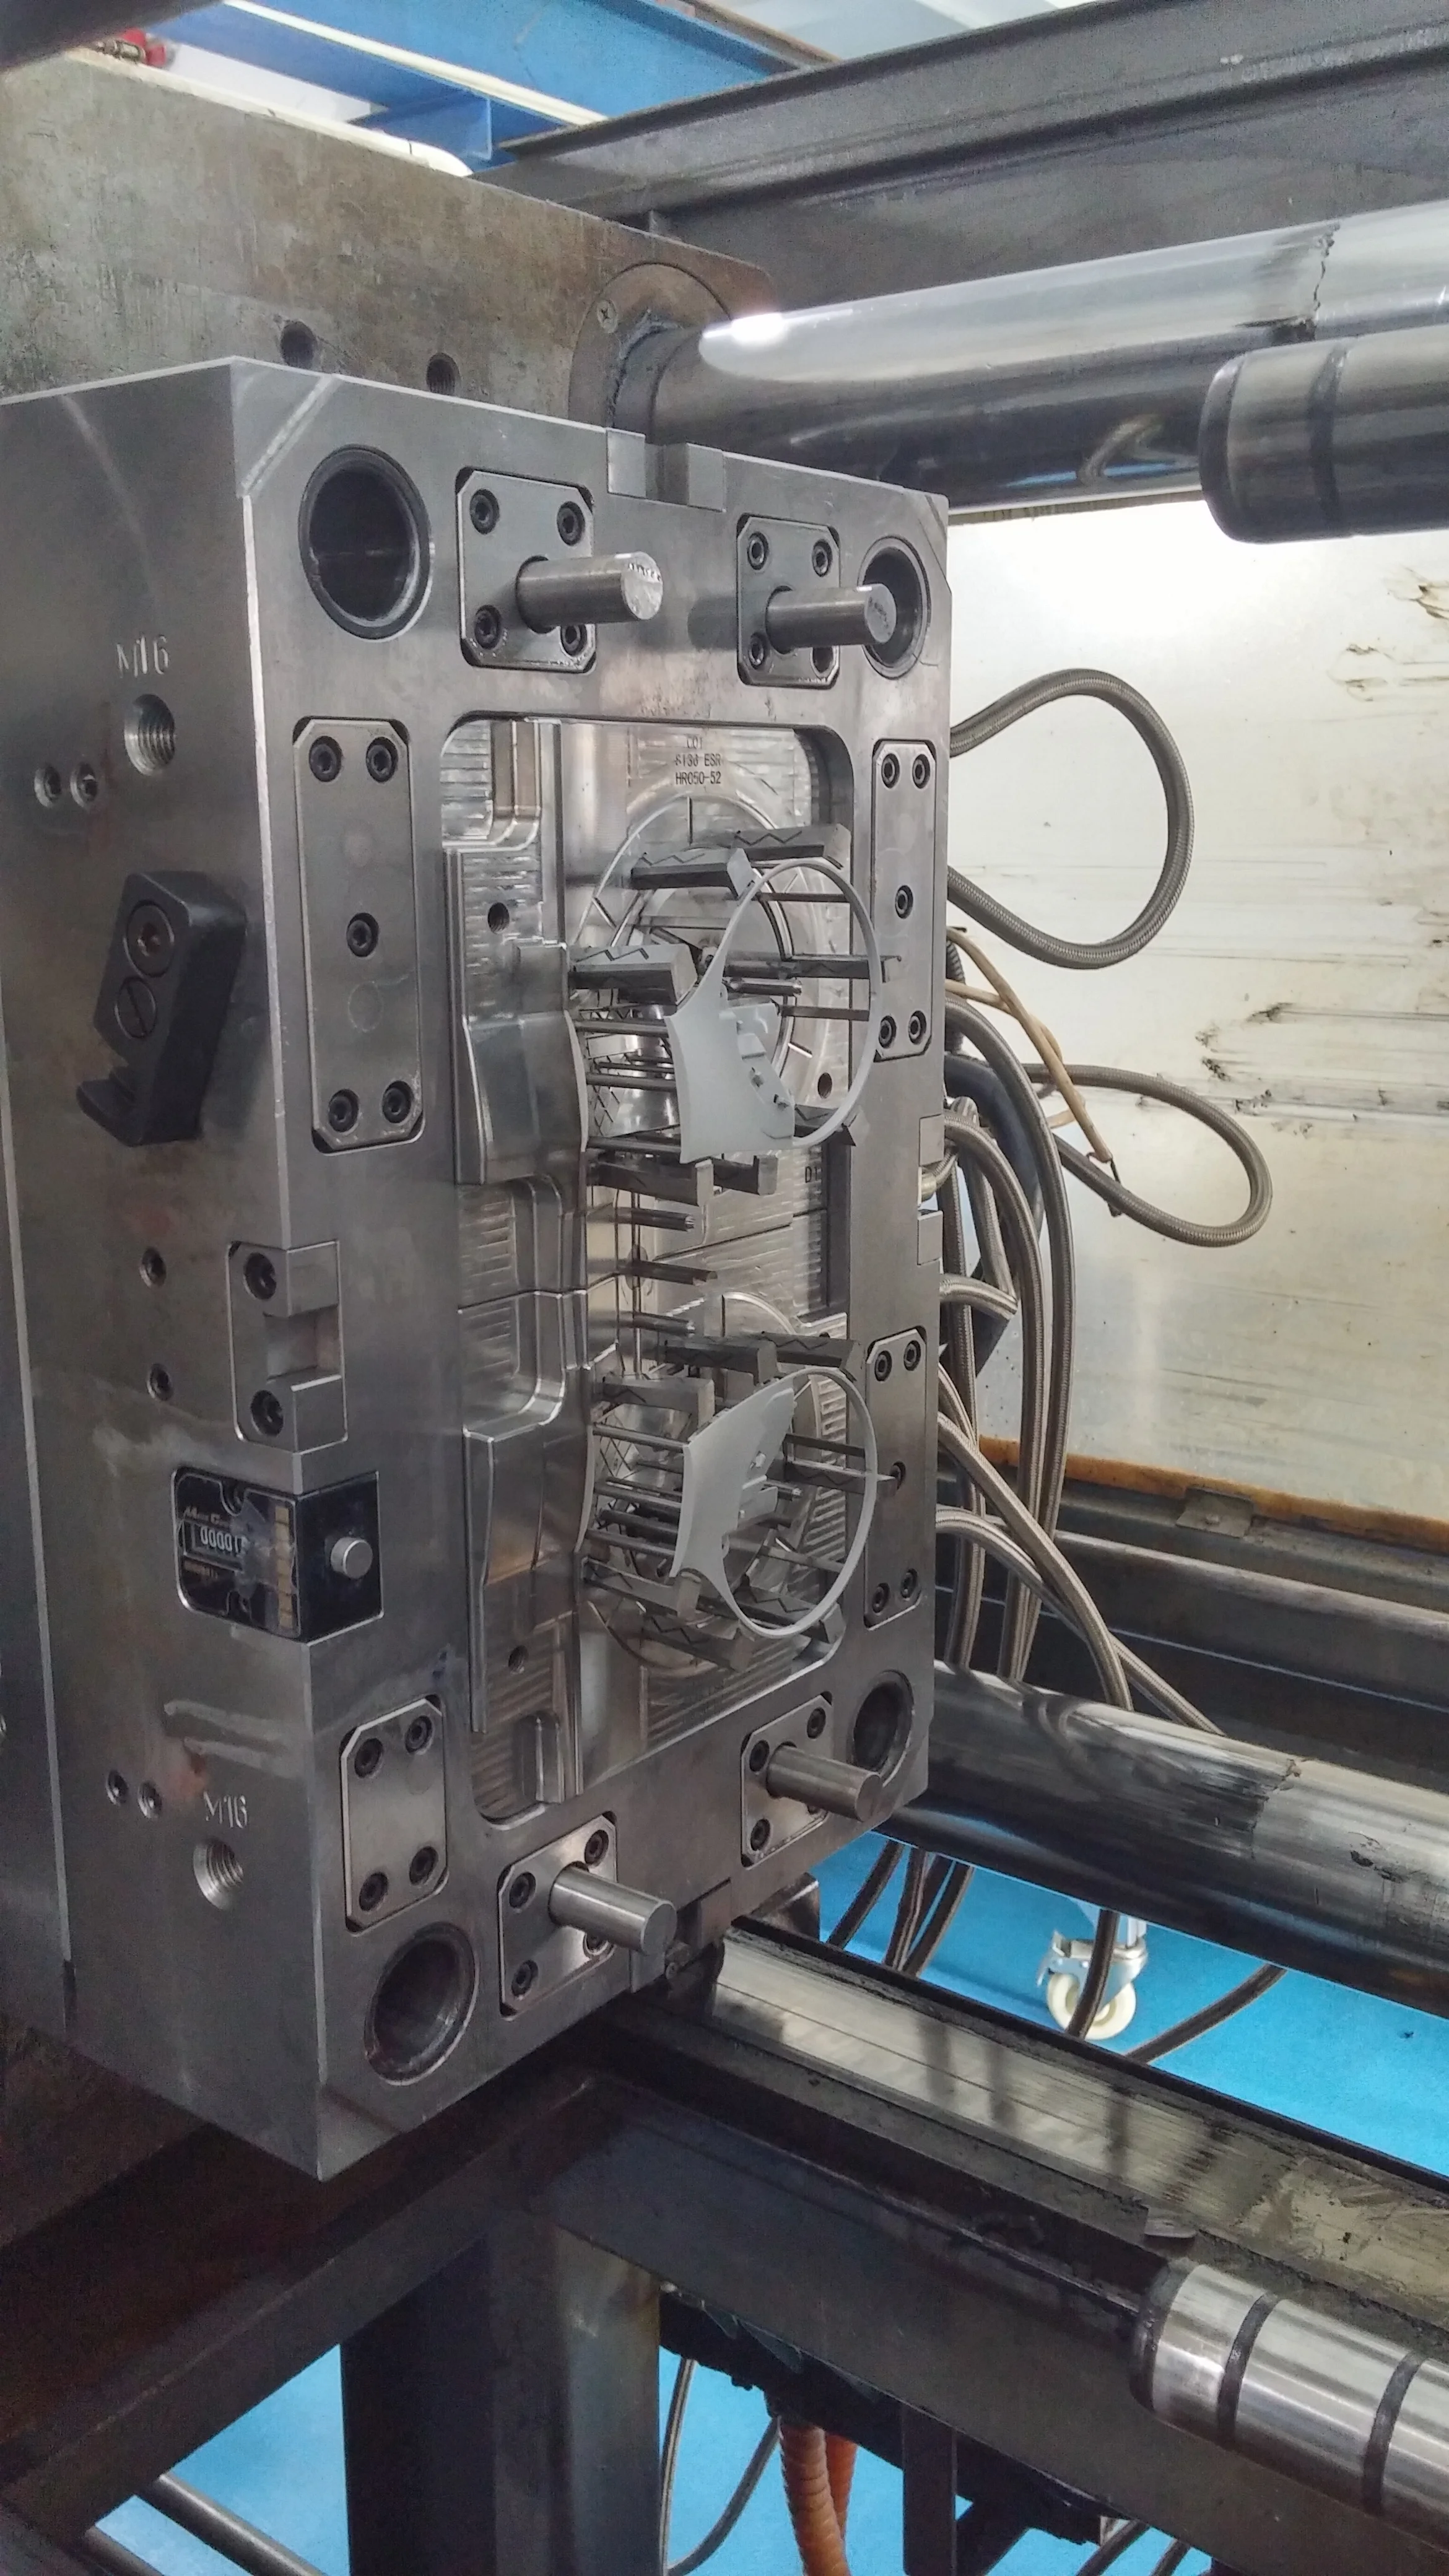
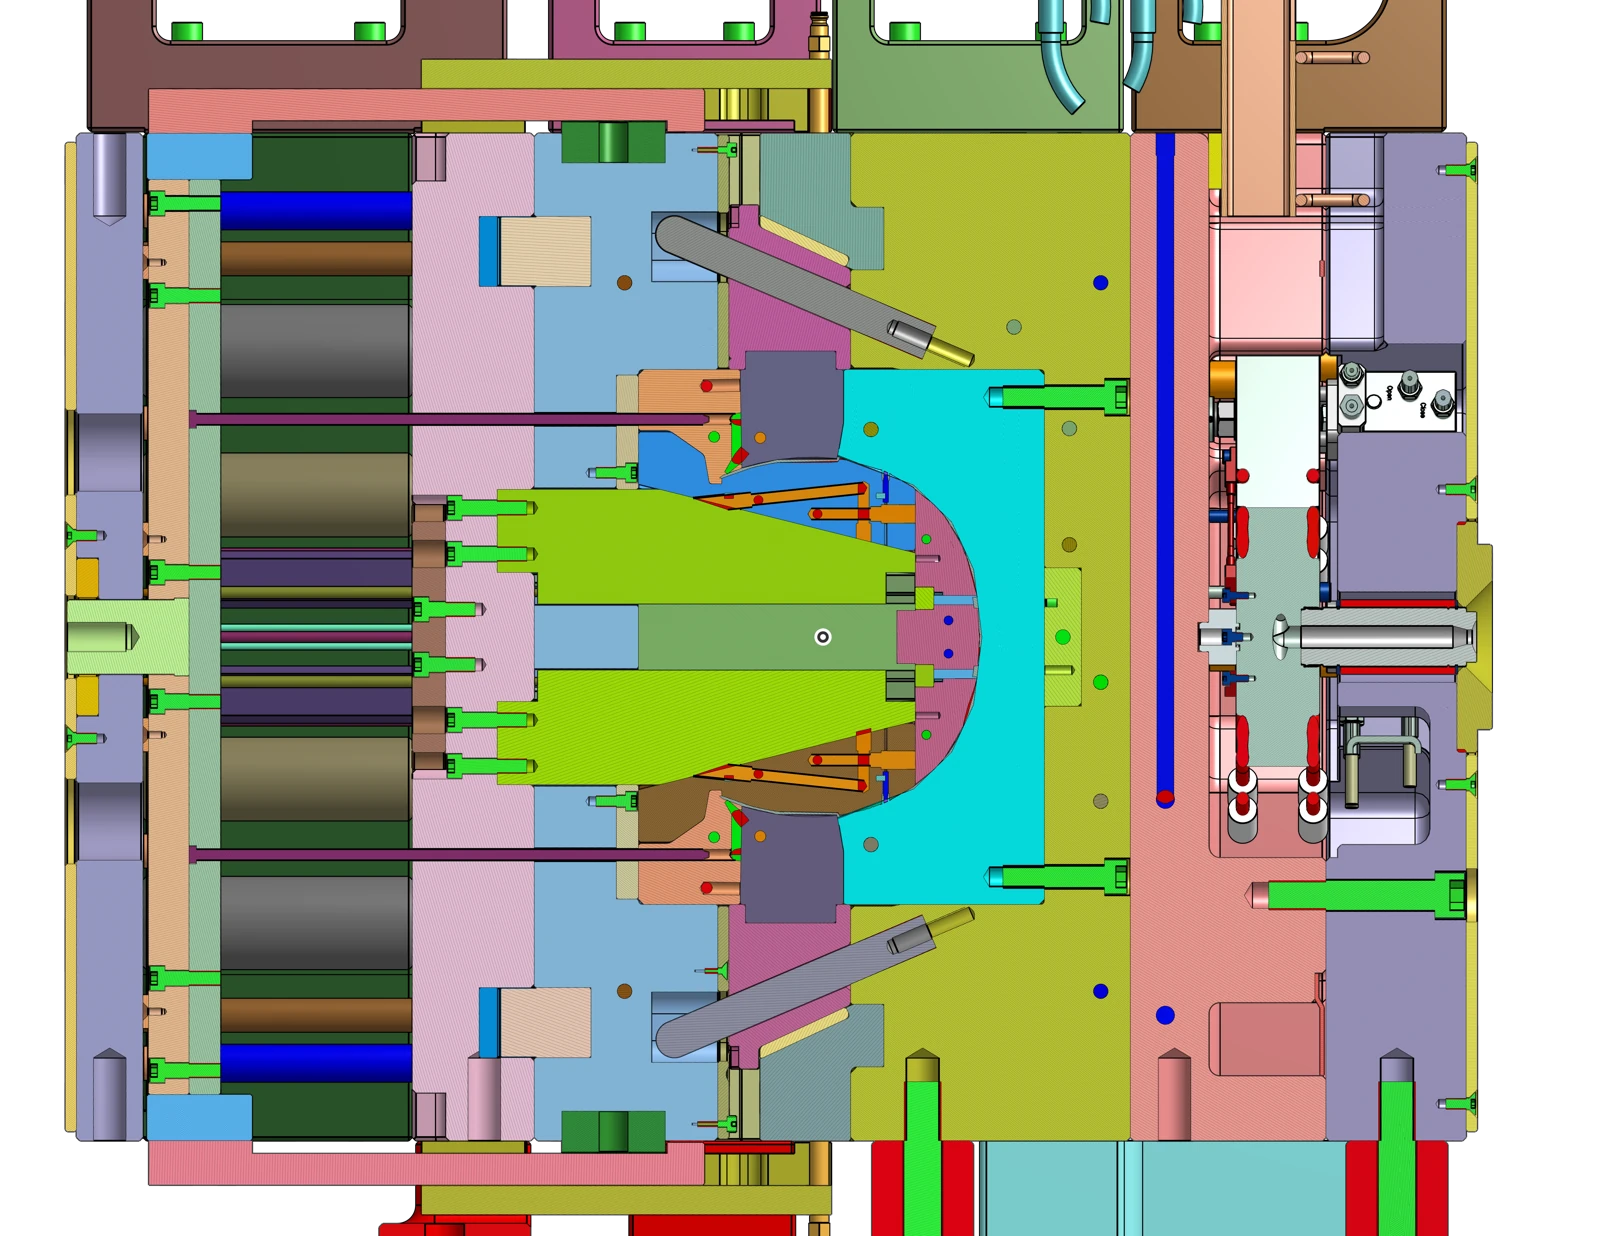
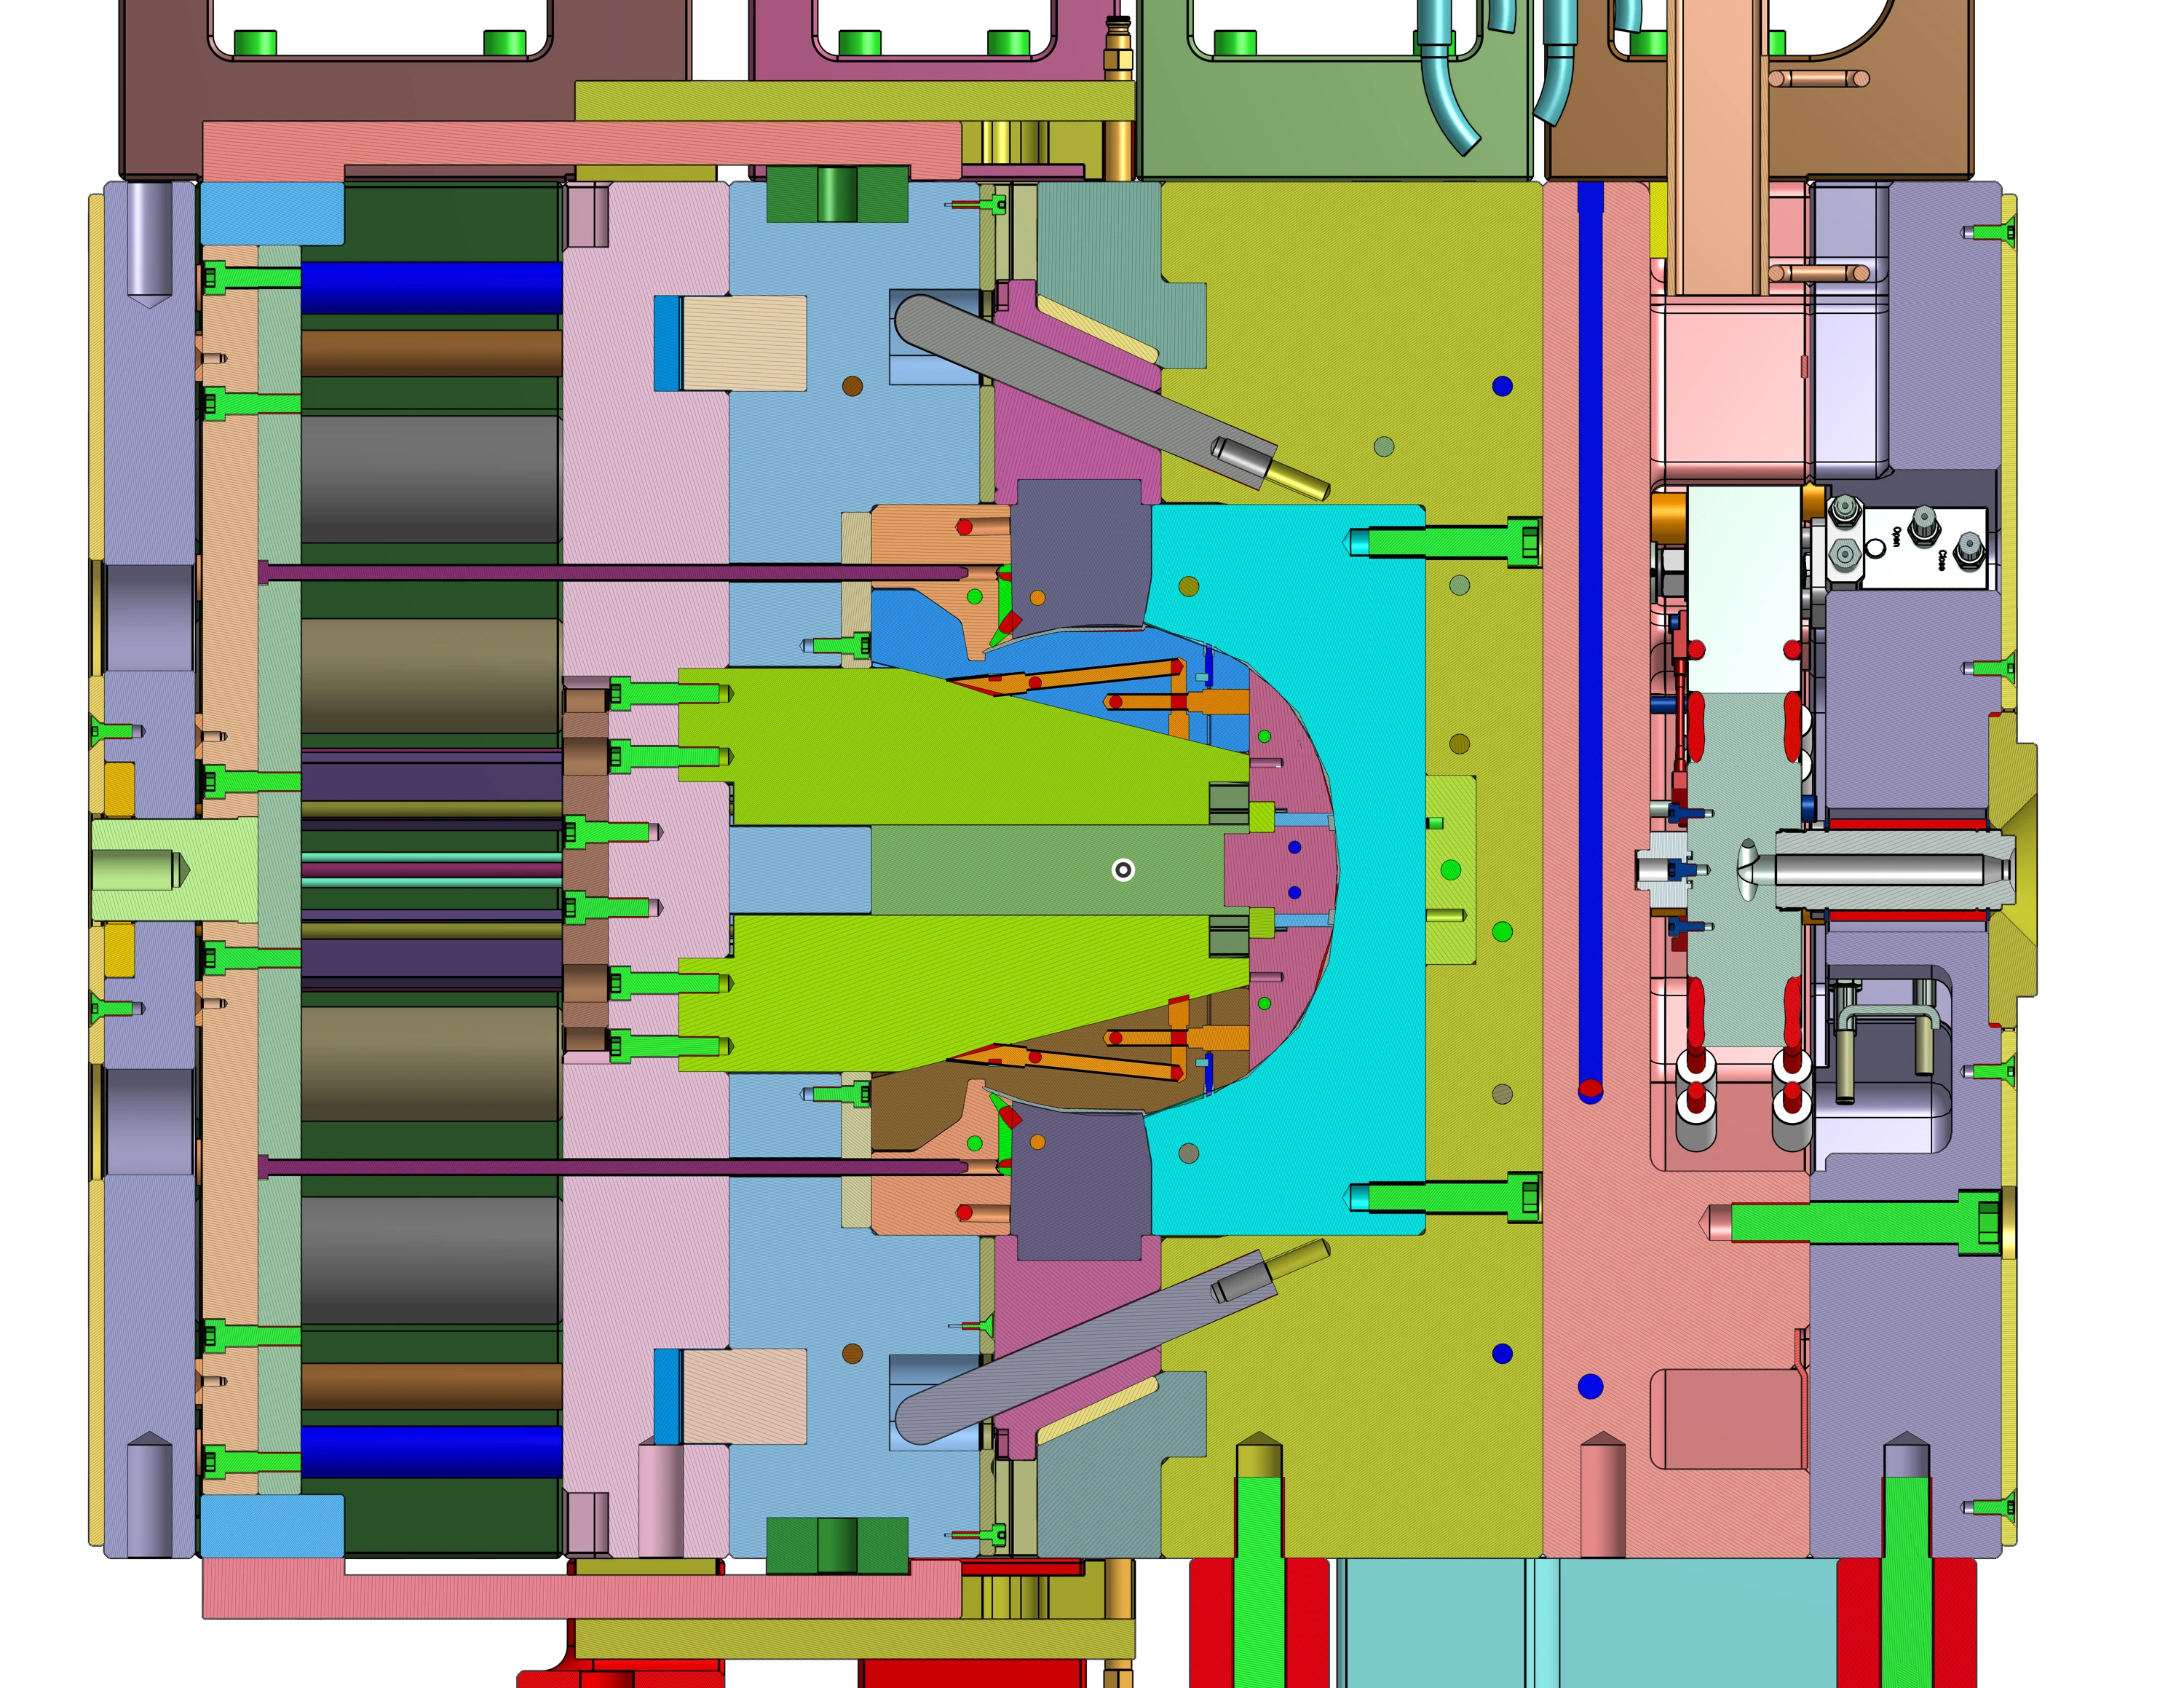
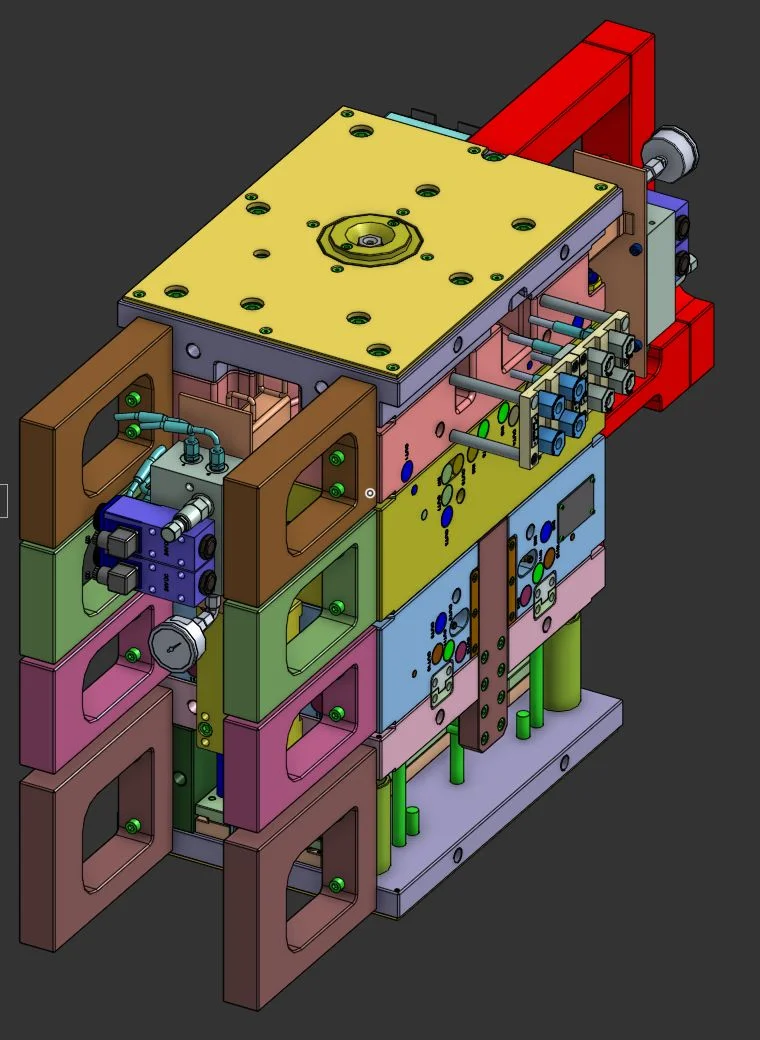
The part geometry, internal features, ejection method and practical tooling constraints all forced compromises on one another. Clearing the undercuts required a collapsing internal core and opposing slides on each side. When the mechanism worked correctly, the part cleared the tool without needing to deform. Getting the tool actions, ejection and cooling to work repeatably was difficult.
Inside the outer-headband mold
In one failure mode, ejection pressure against the sticking part broke it. Getting a part out intact was not enough either: we also had trials with correct ejection while the part was still dimensionally unstable.
Ejection failure and clearance
Hi-P pushed for post-molding cooling fixtures. I pushed back hard: holding individual parts in fixtures while they cooled was not a viable production route. I had to define and control the molding process so the part could leave the tool in a controlled condition and cool into the shape and dimensions we needed.
Getting complete process records was a recurring struggle. I sent the molder a template for the relevant parameters and a trial progression log so we could run a design of experiments. They kept running trials without that visibility, then bringing back parts and pushing for approval. I made several trips and spent time at the molder to get the process information we needed.
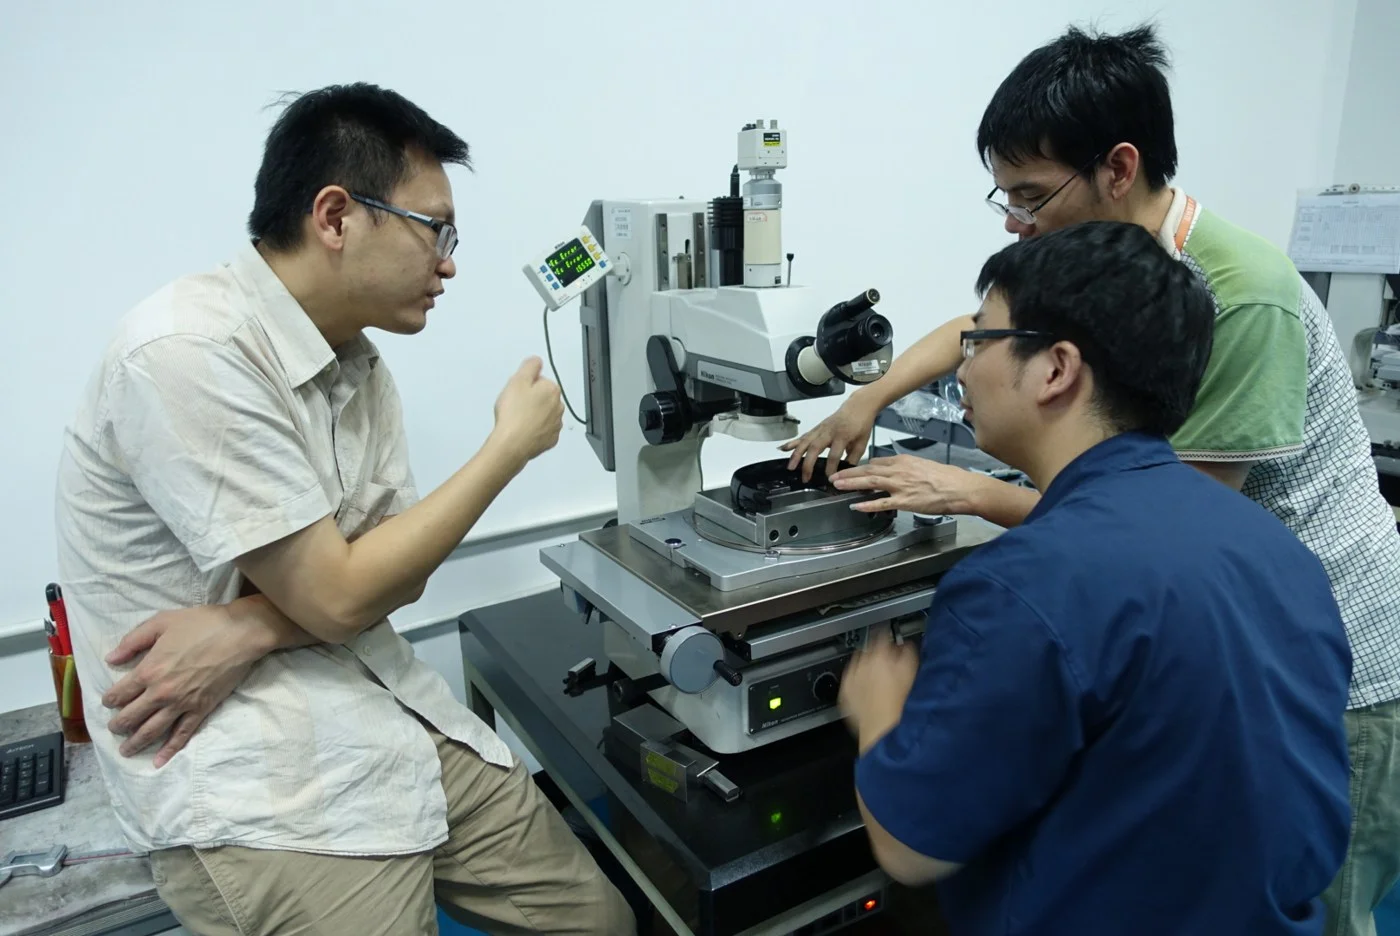
How we held the part for inspection mattered, as did what happened when it met the surrounding parts. Hi-P, the molder, flagged distortion, difficulty establishing a measurement datum and flash at local features. Working through those findings meant deciding what needed a better measurement, what needed an assembly check and what needed a change to the part or tool.
Our August 26, 2015 engineering review listed 16 discrepancies. The overall span measured 197.06 mm against a nominal 196.31 mm. The inspection sheet flagged it against the drawing tolerance; the engineering review accepted it as a reference dimension. That disposition applied to that dimension, while the other findings still needed their own decisions.
A local feature that might have warped needed to be measured in a fixture. At a mating interface, the review called for checking that assembly did not deform the parts. At the screw-capture ledge, the problem was more specific: the screw was bottoming out. The ledge measured 1.133–1.140 mm, and the review called for raising it to at least 1.15 mm.
Inspecting the molded part
The outer headband continued to change after shipping began. Its drawing package reached revision 25 in May 2016. The later revision history records detent and paint-thickness changes, a boss-counterbore change, and revisions to the artwork and its placement. The finish drawings mapped soft-touch black paint and black UV hard coat to different regions, with explicit masking and overspray limits. Fit, finish and appearance kept meeting in this same part.
Keeping the wider build moving
I delegated as much of the drawing and documentation work as I could. Leonard Pang and others helped with drawings and revisions. That let me protect time for troubleshooting, supplier work and the decisions needed across the mechanical BOM.
That work extended across the BOM: spring indexing, gimbal holes and pins, sliding and bearing surfaces, snaps, screw features, texture and finish. We had to distinguish a drawing or measurement problem from a tooling or processing problem, agree on the correction and check the next parts. Chris, Misha, the supplier engineers and I worked through those reviews together.
The first question with a fix was how much validation it would take. Then came what the supply chain and fabrication could support. I coordinated on the fly, trying to make the best use of time and money. I worked for Chris Westra and Allan Evans, who approved major expenditures. Those practical limits shaped how much we could change, and when.
I've always been an avid photographer, and I use photography to communicate technical work. At Avegant, photographing parts, assemblies and the work around them was part of pursuing good parts at volume and acceptable yield.
Building up the headband
Outer band, springs, main harness and precisely placed die-cut PSA patches.
Designing the assembly and inspection fixtures
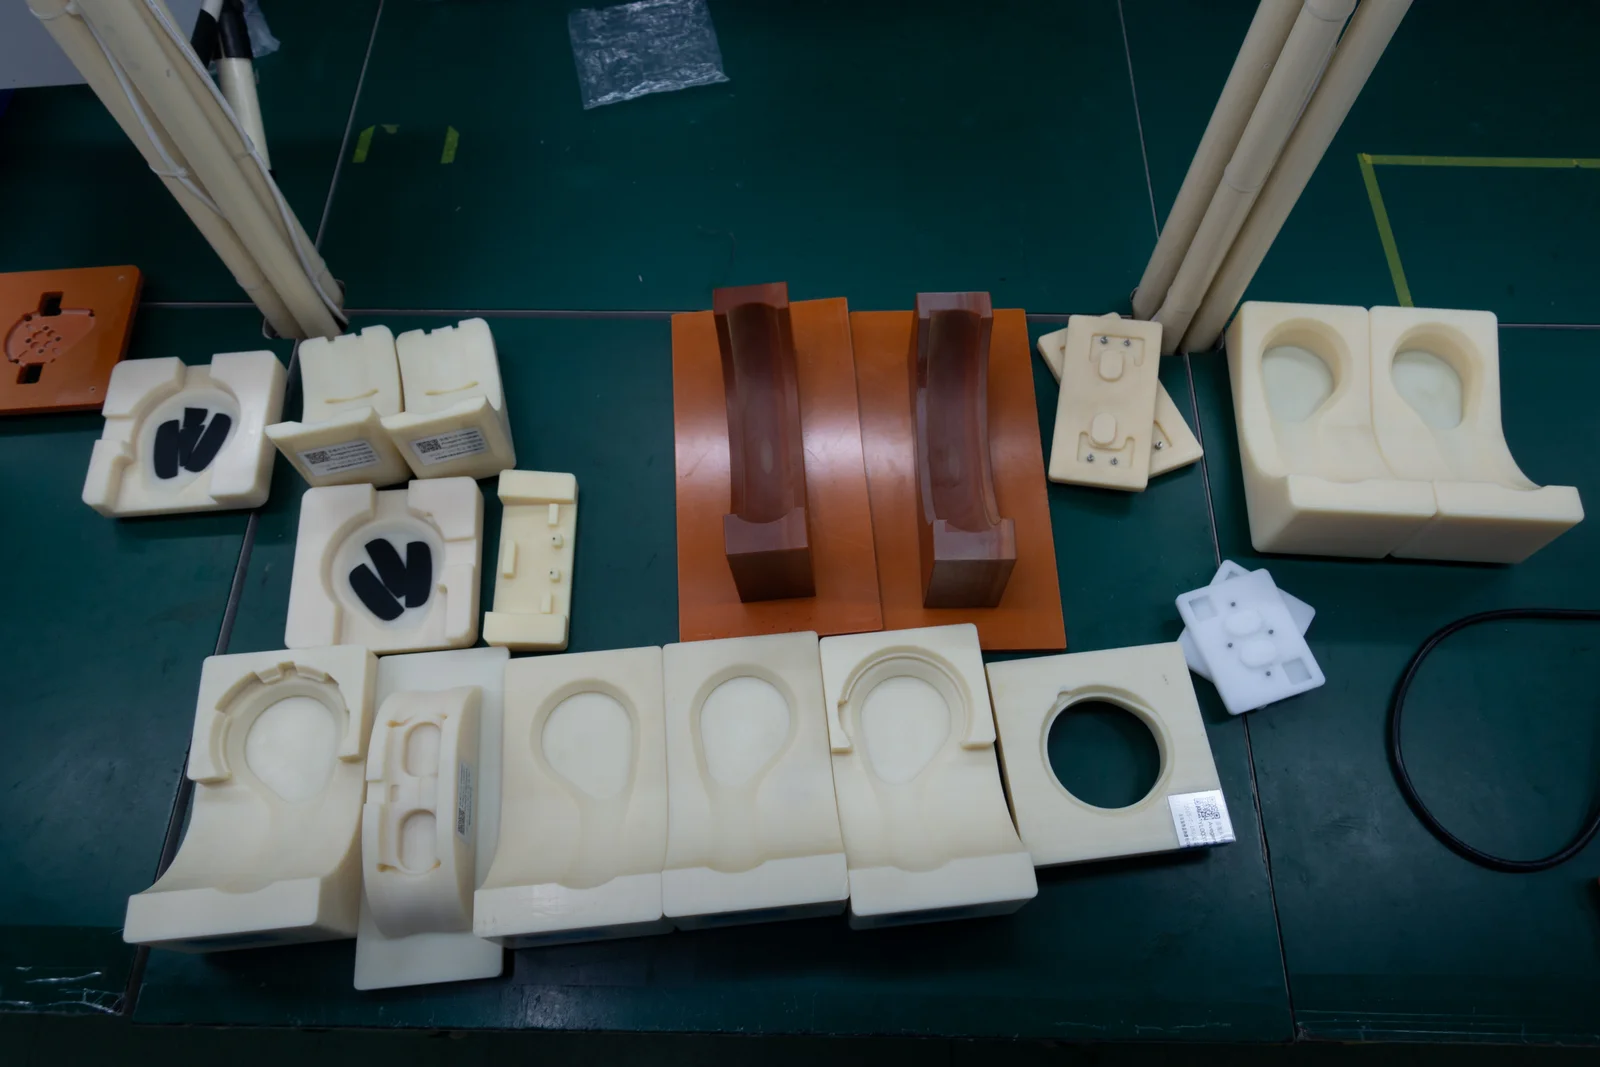
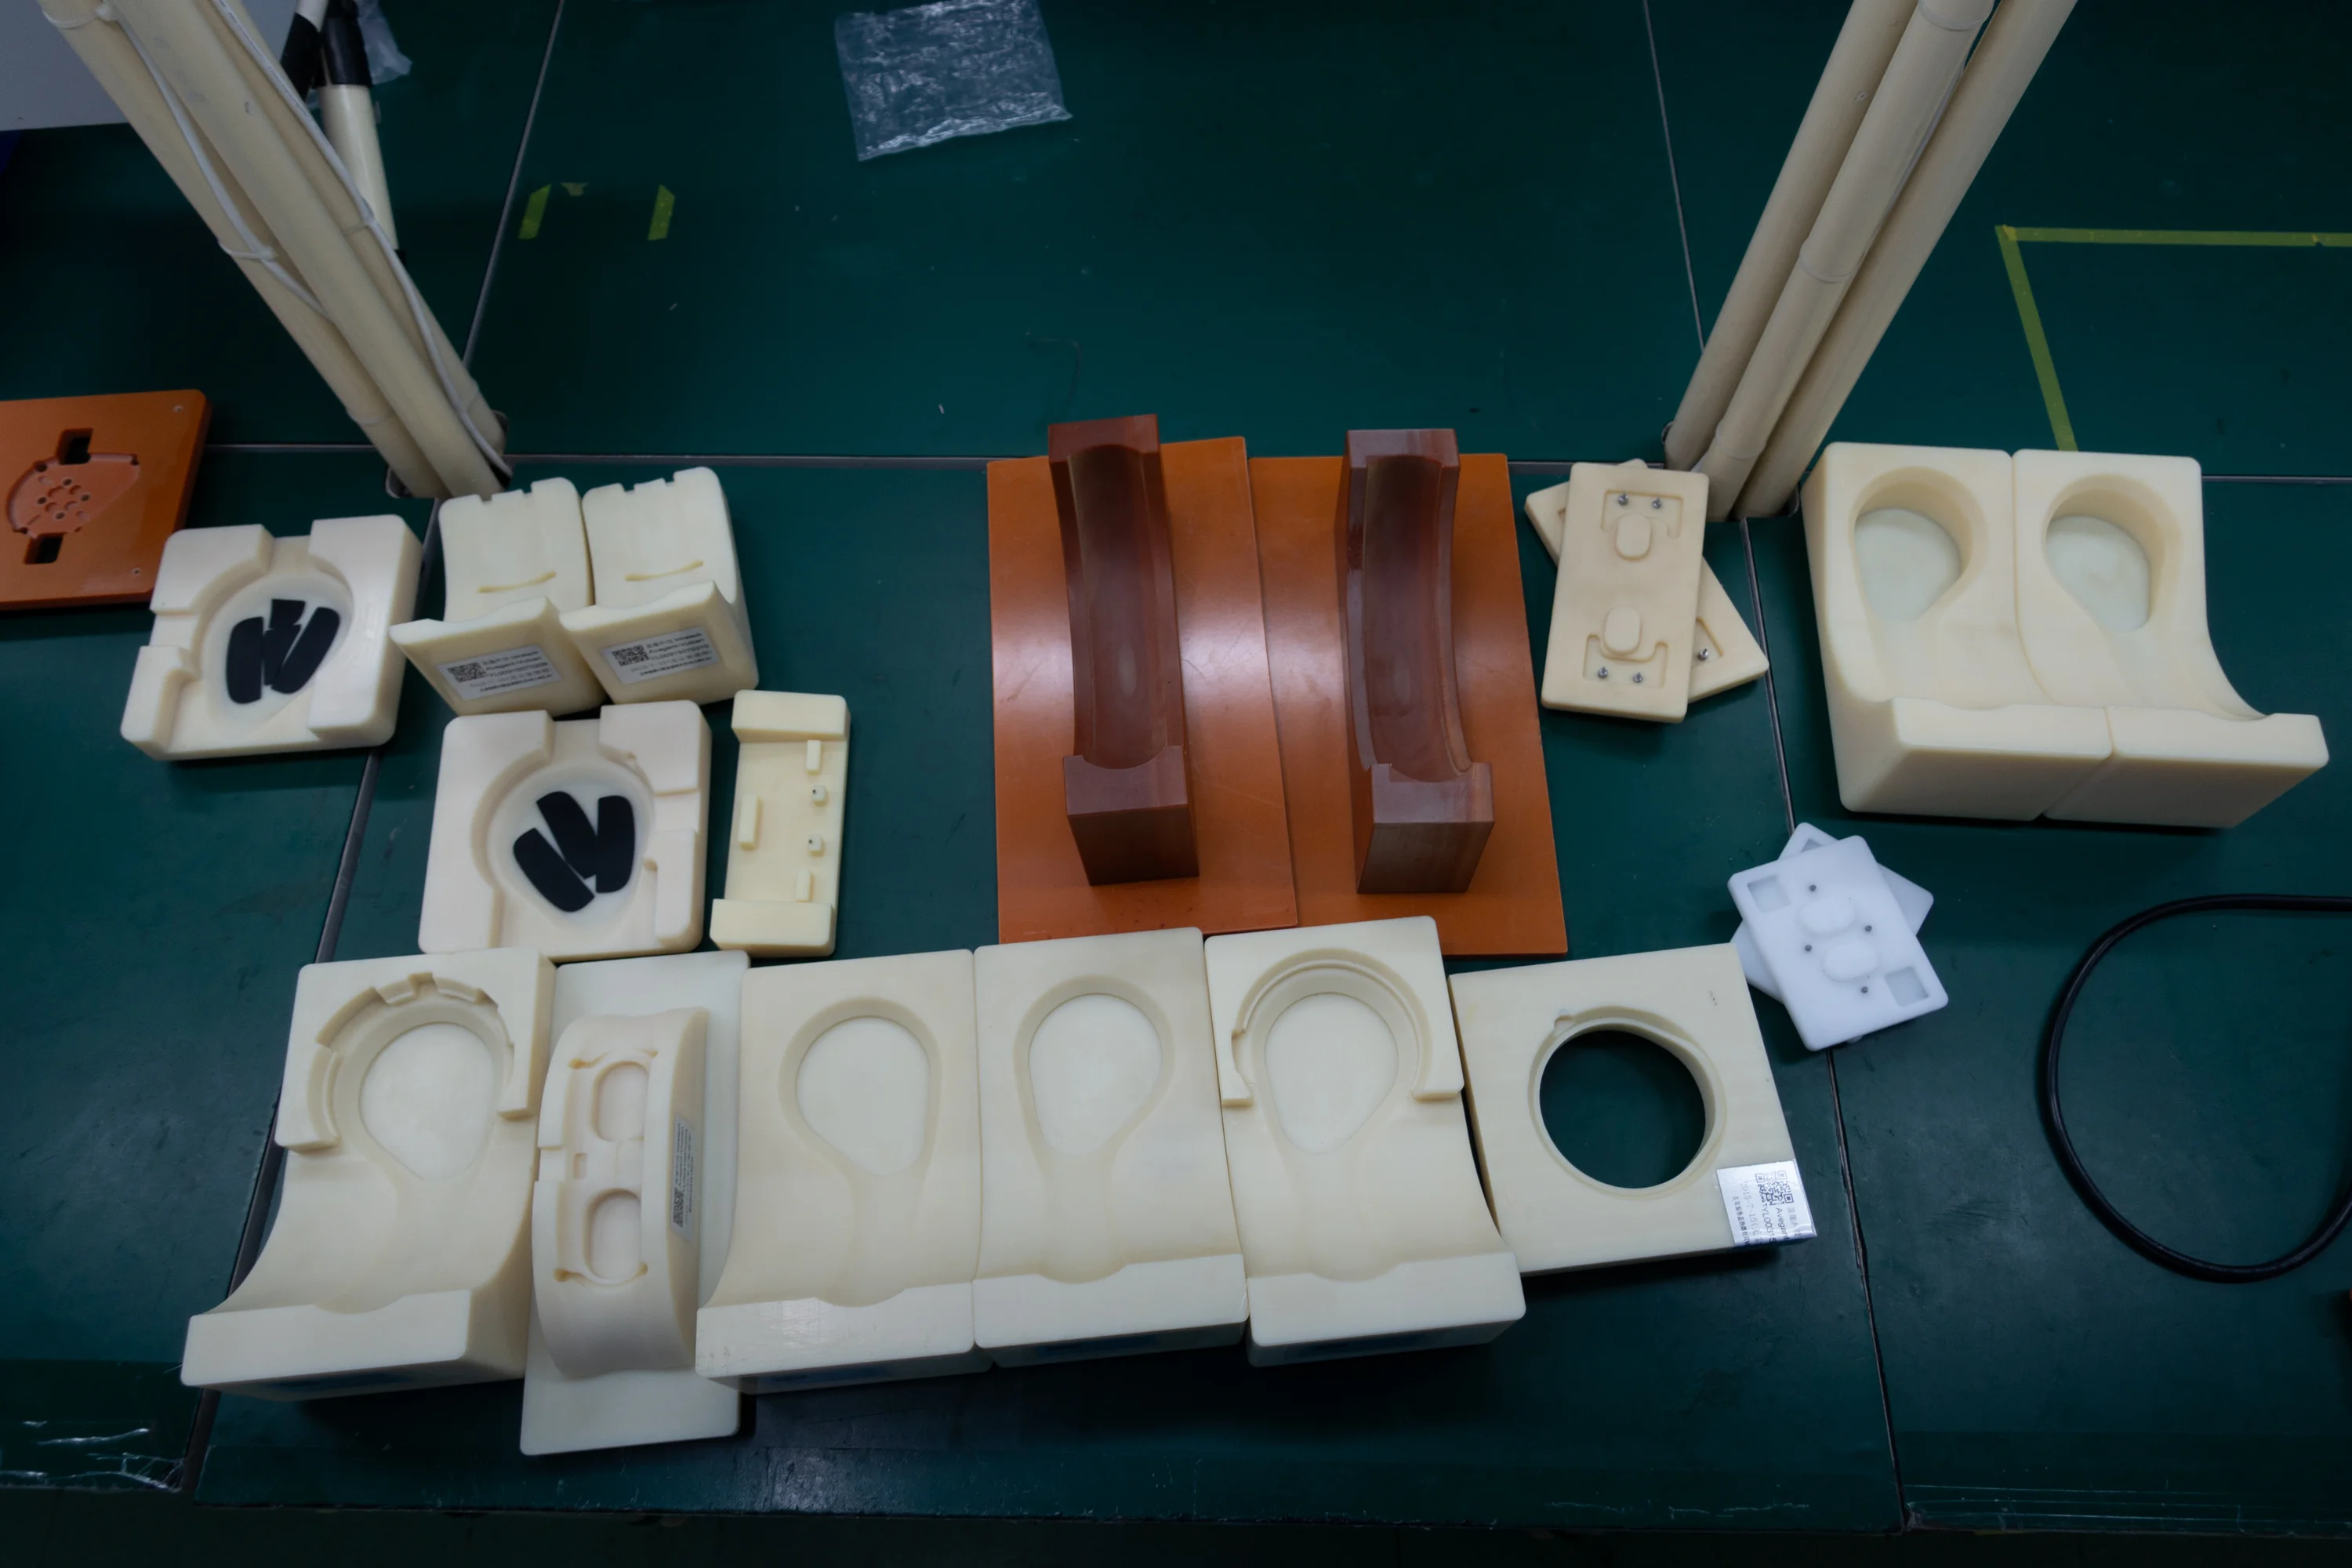
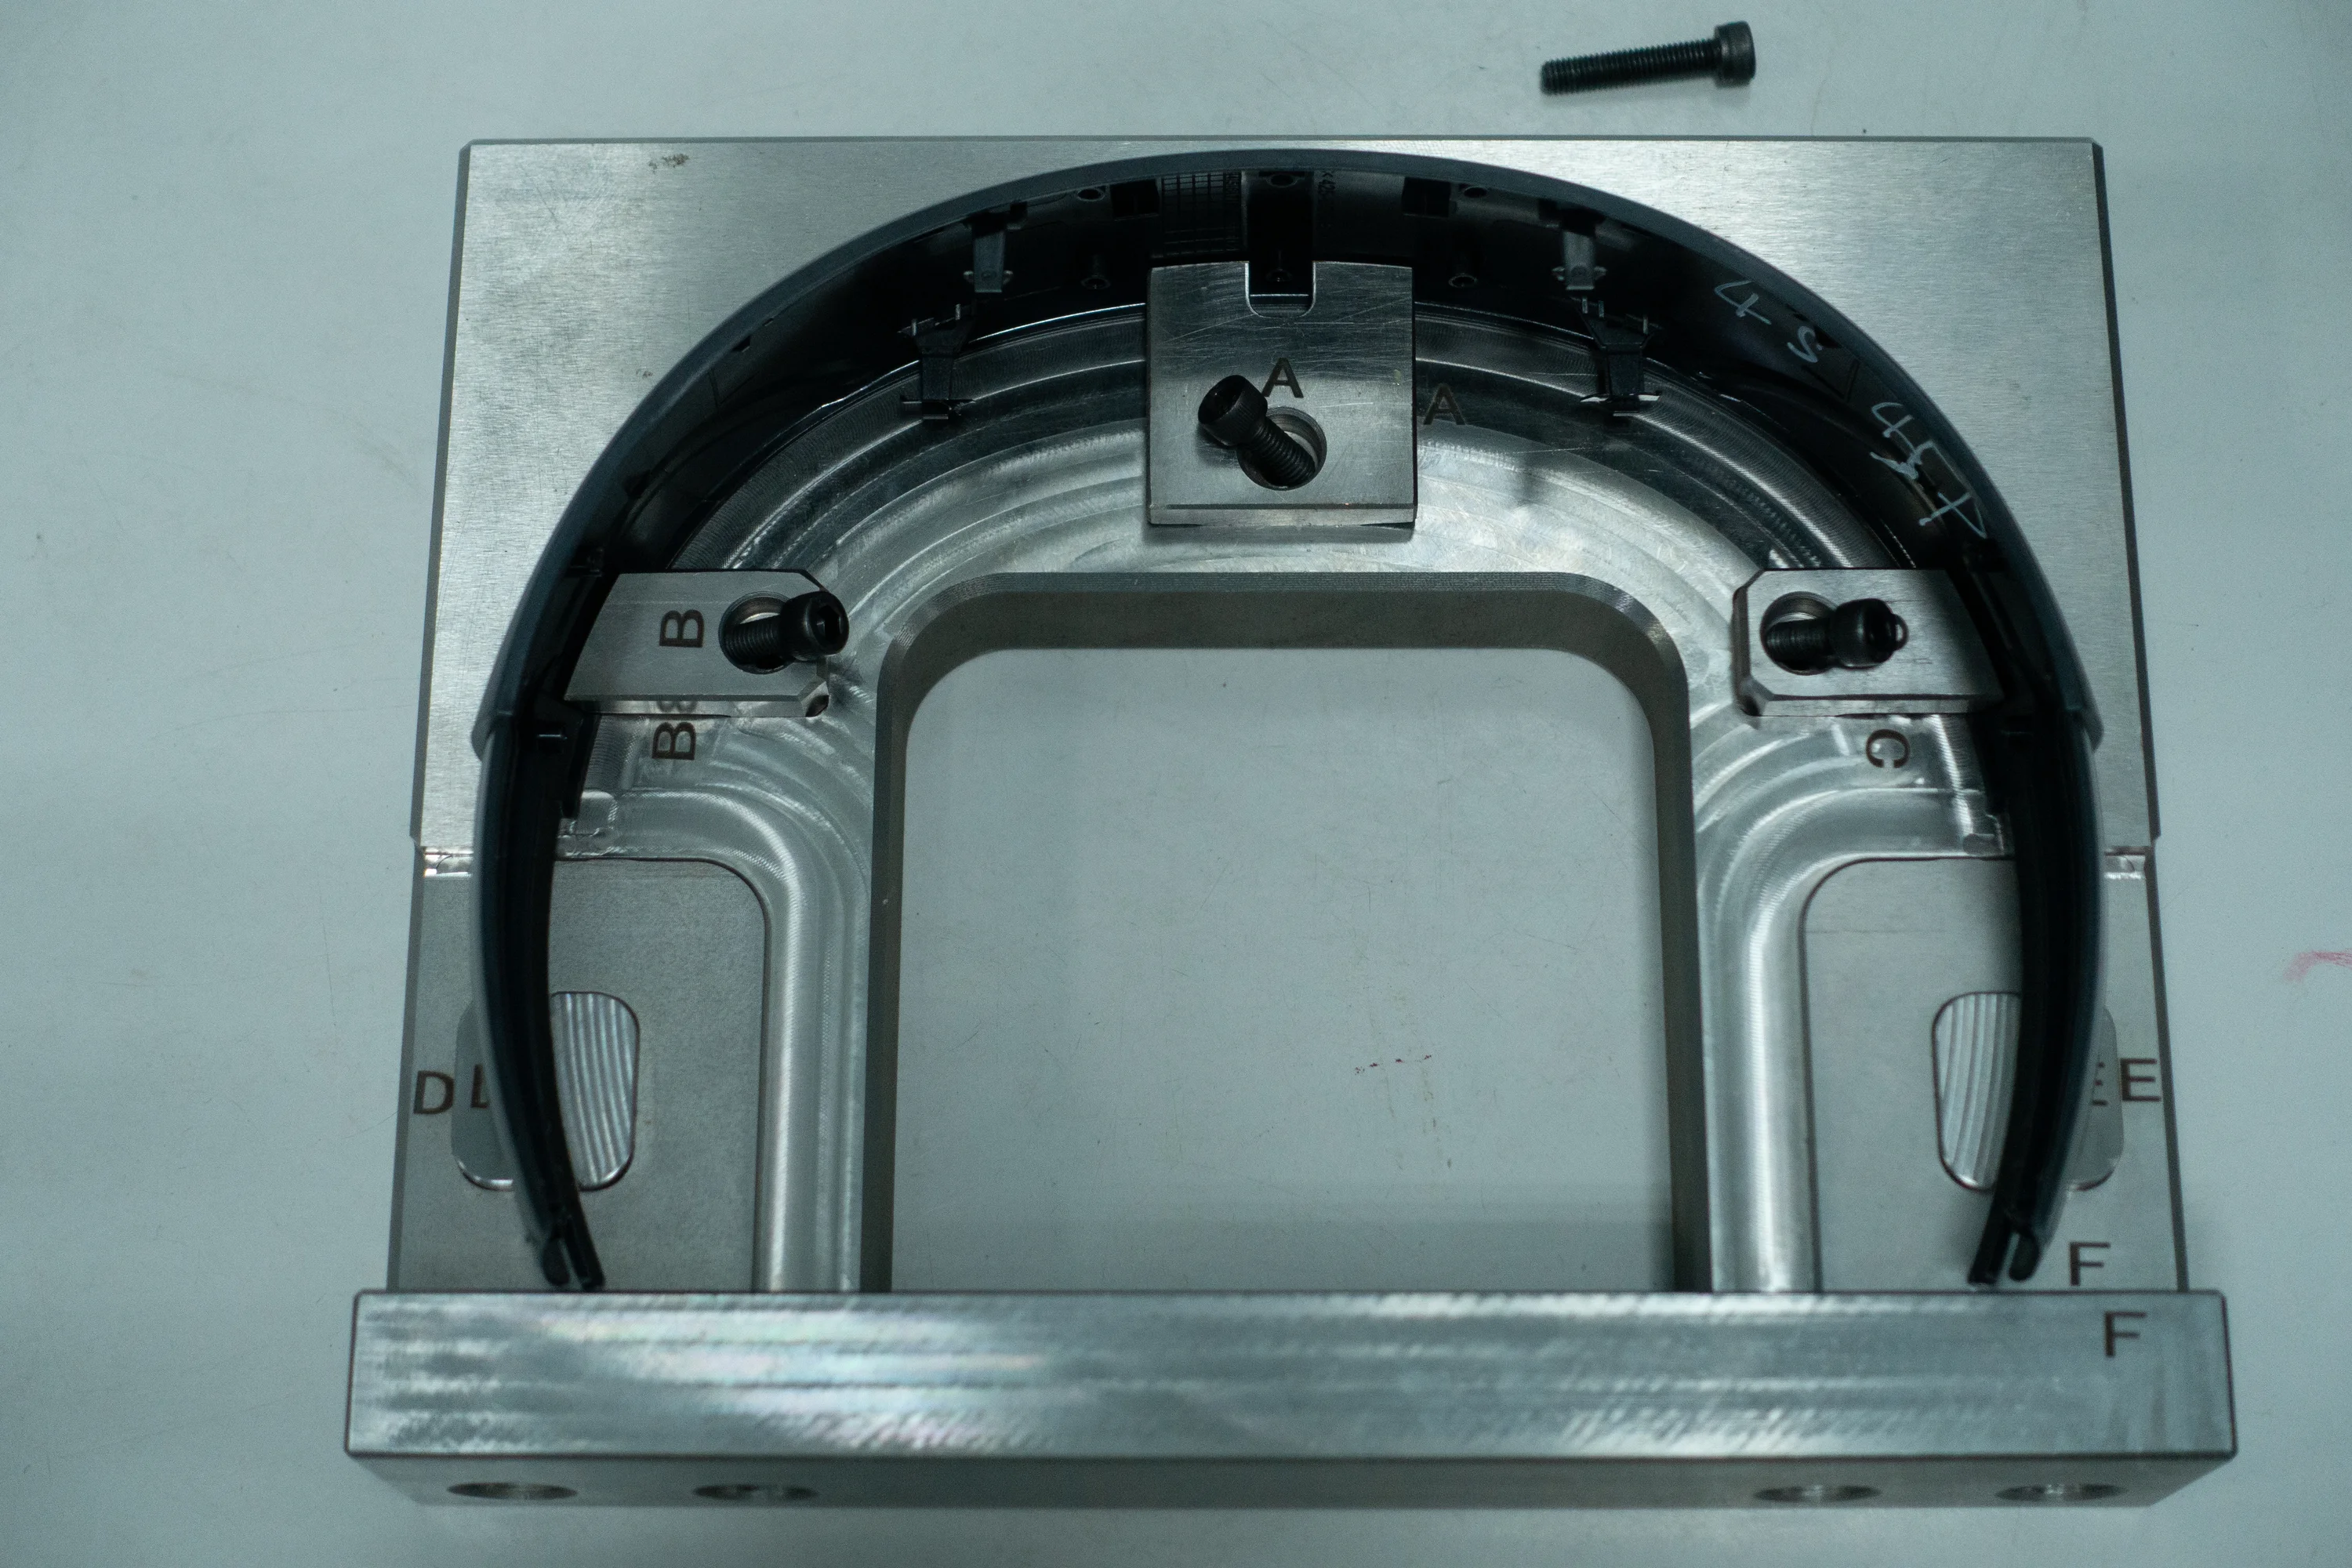
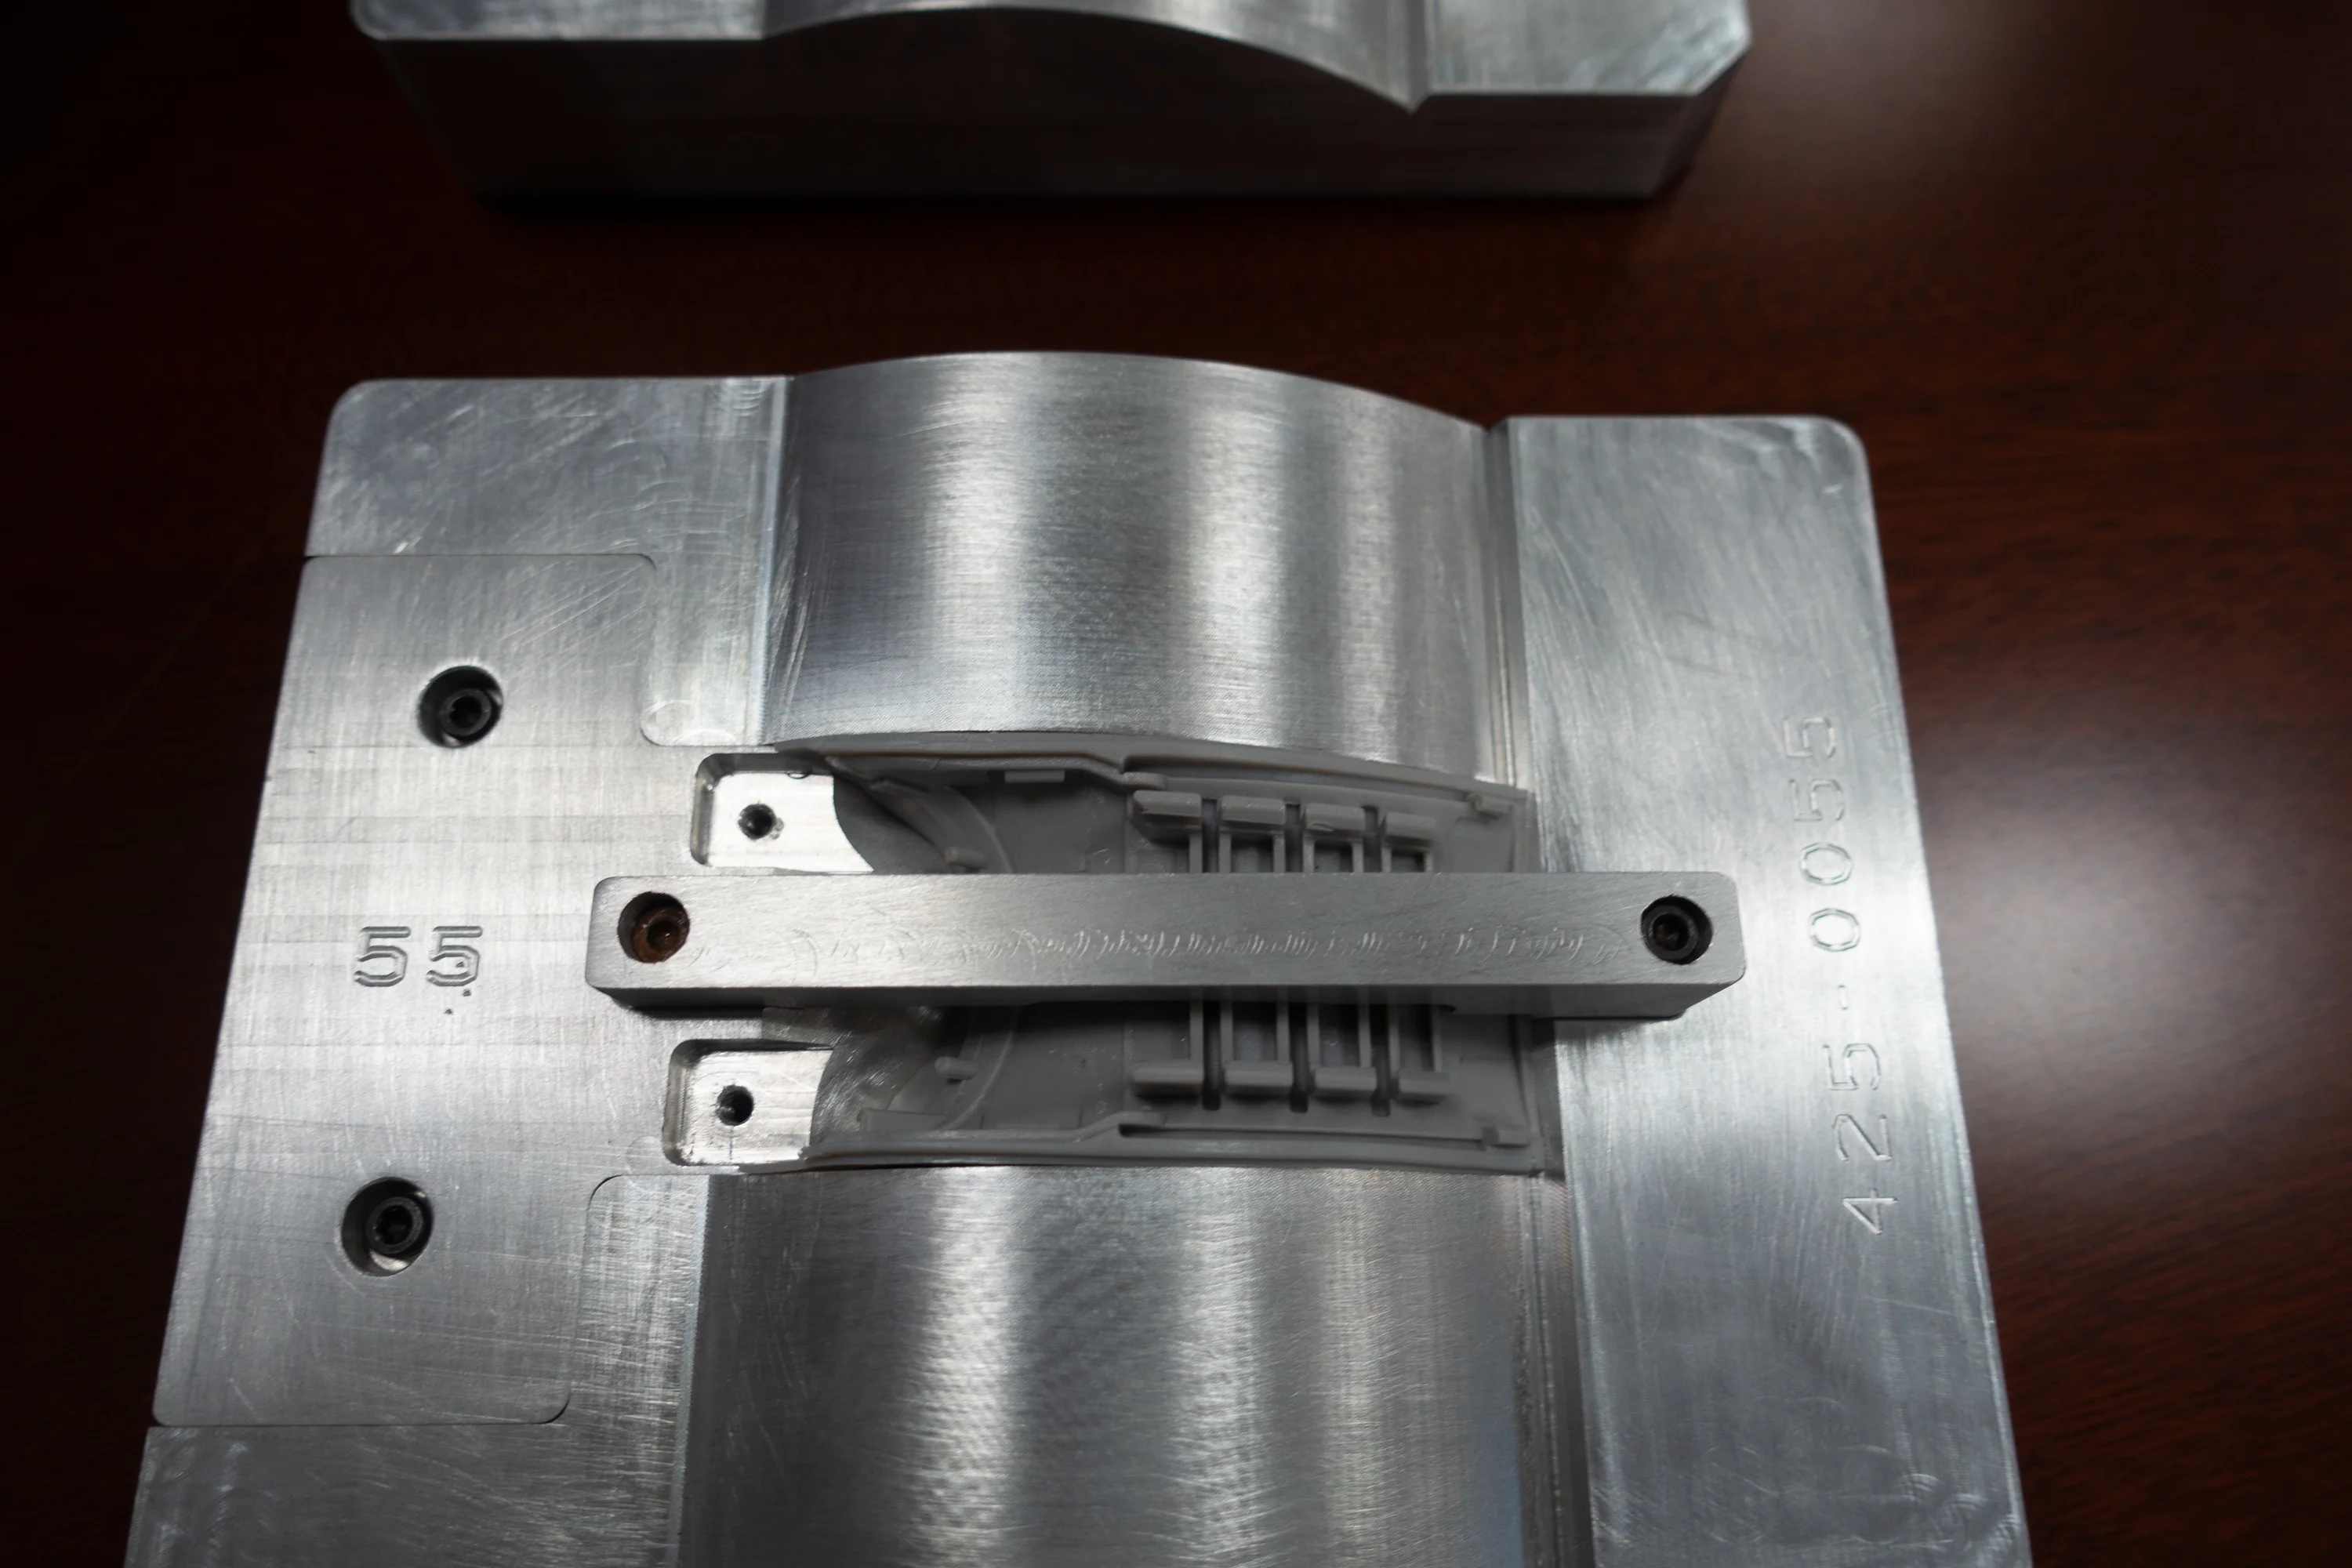
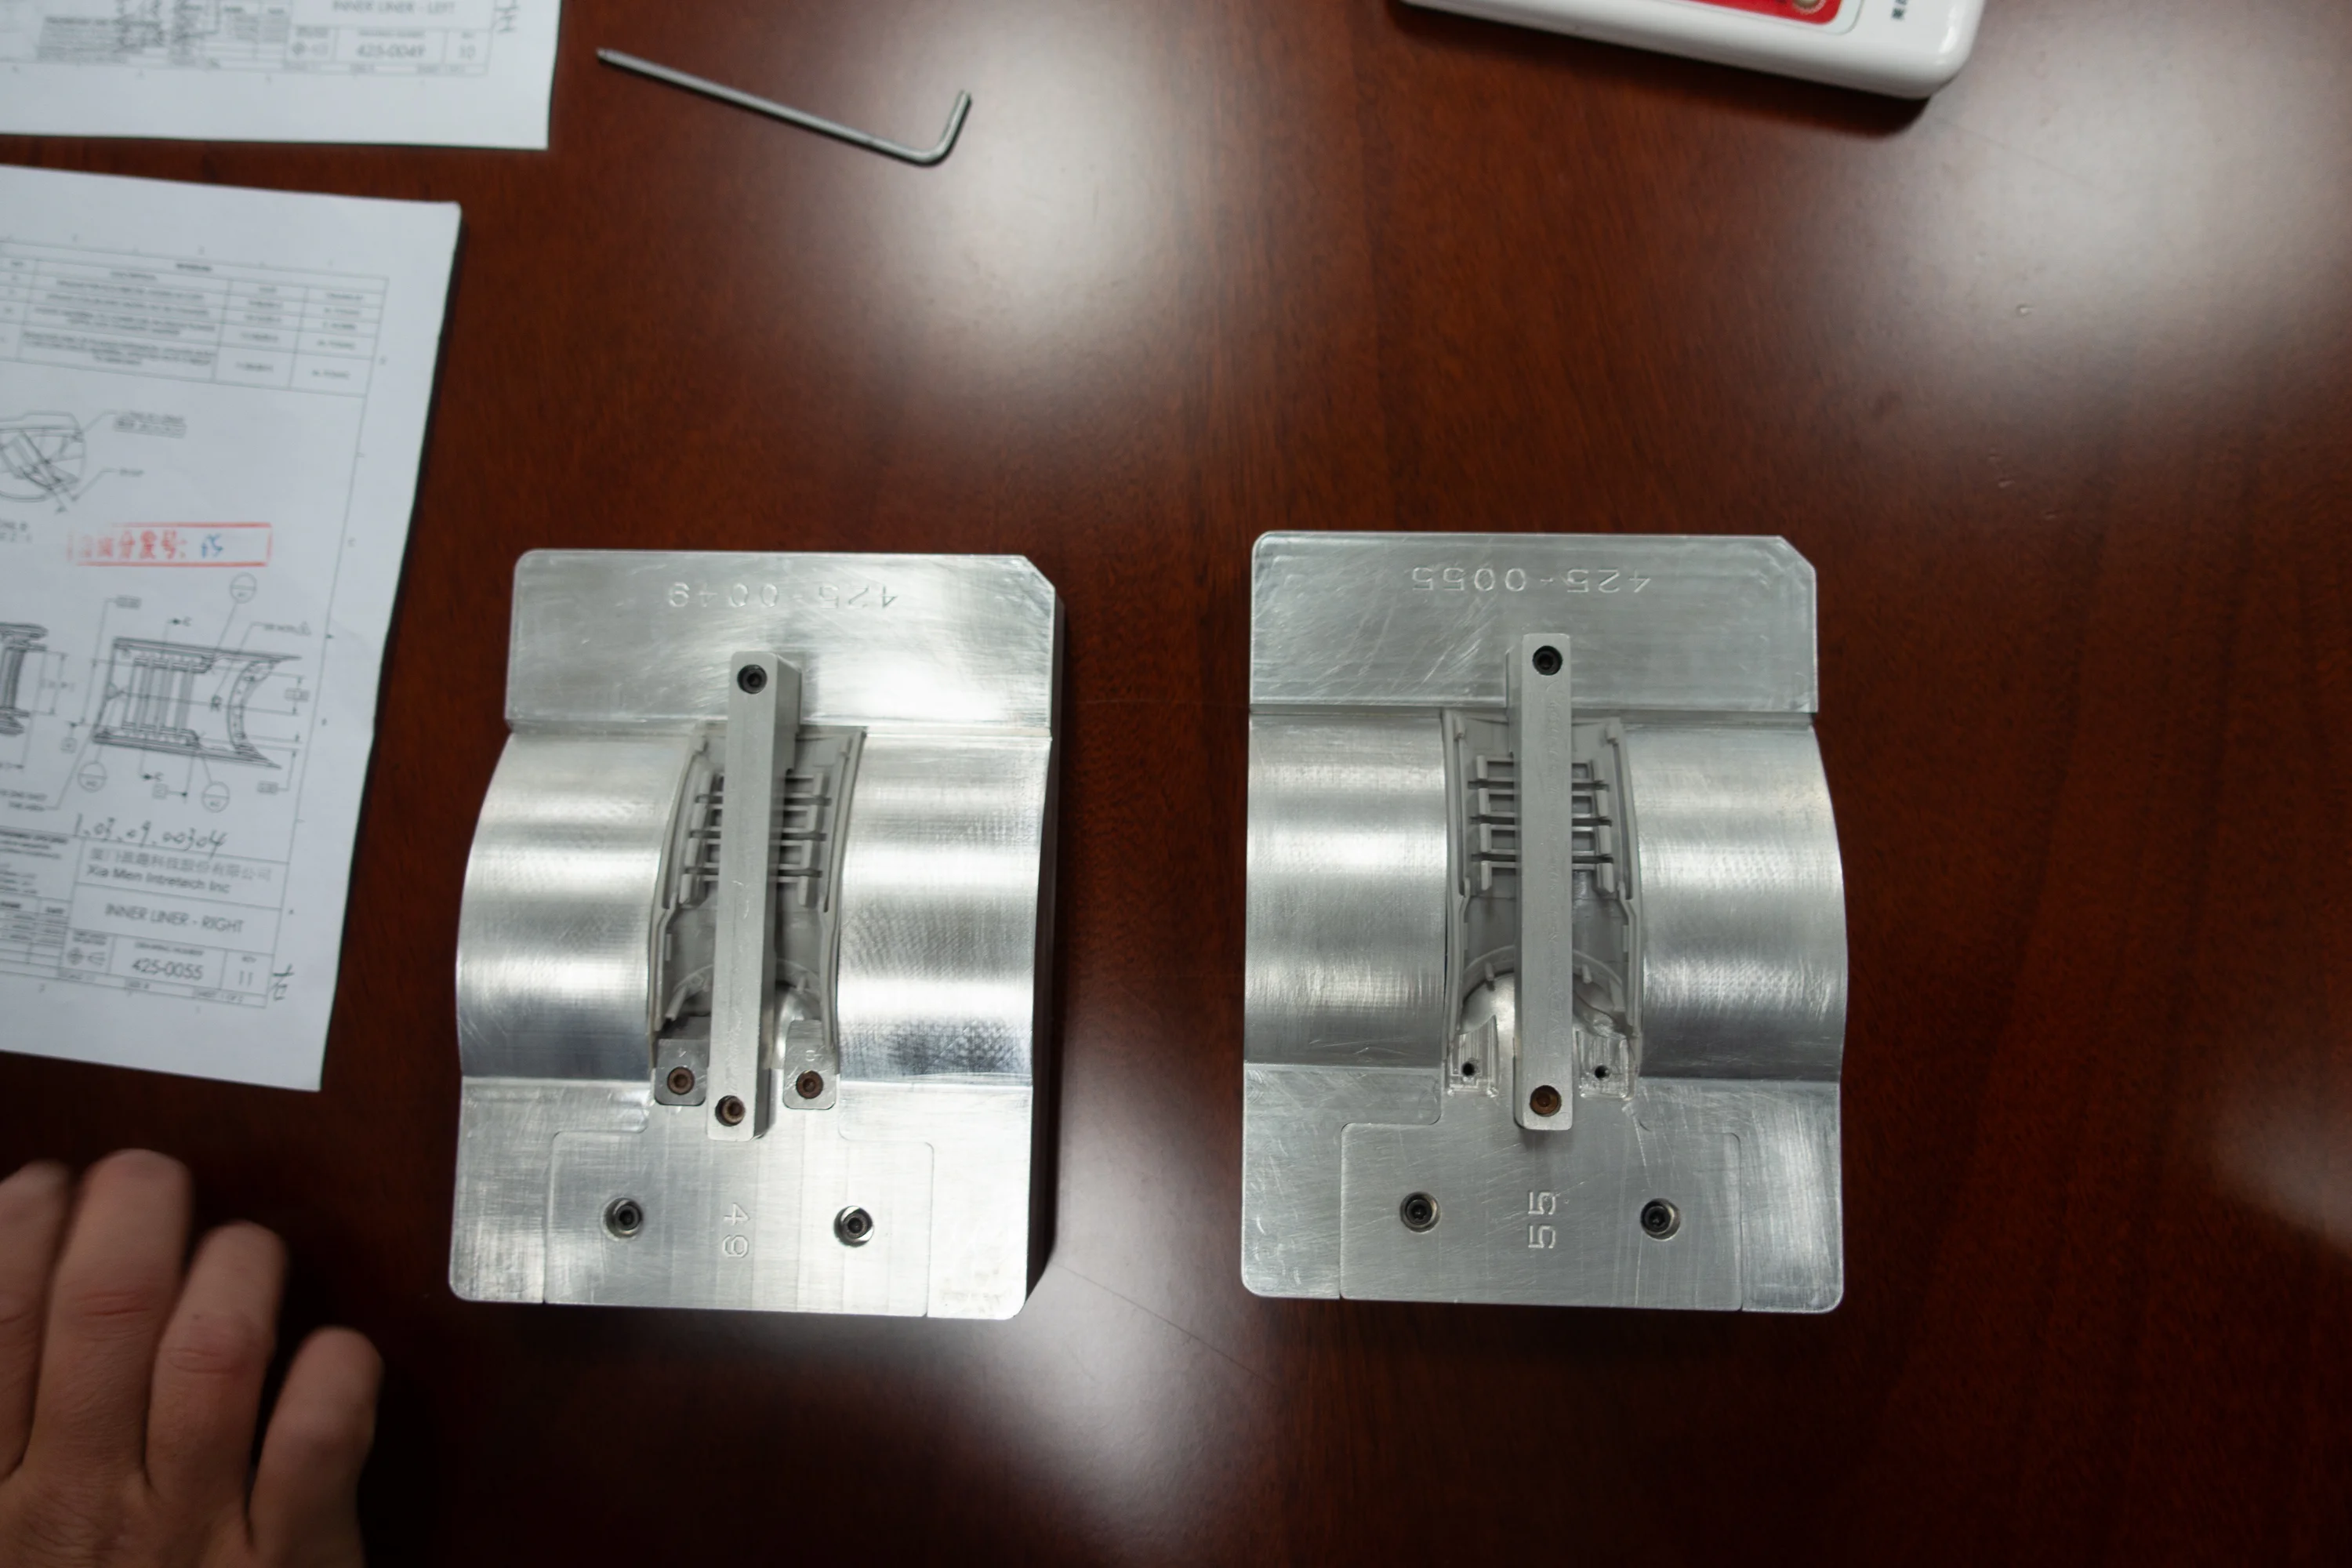
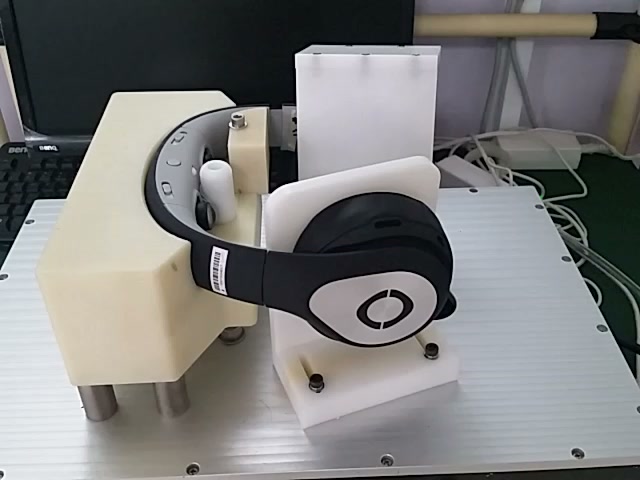
I designed all of the assembly fixtures, along with inspection fixtures for parts such as the outer headband and inner liners. The geometry we were asking suppliers to hold had to be reflected in how we supported and located the parts for inspection.
The outer-headband fixture followed the long arch and located it at labeled positions. The liner fixture supported the smaller, ribbed part in a shaped nest.
I wrote individual inspection procedures and acceptance/rejection criteria for critical parts, including the headband and liners, arm inners, ear covers, bezel rings, shutters, button plates and backers, ear pads, bushings and faceplate. I also created the master gap specification (795-0002), defining target and allowable gaps at the assembled interfaces. The fixtures, procedures and gap plan connected the part drawings to how we would inspect parts and judge the assembled product.
 From the workbench
Locating, assembling and inspecting the parts
Inspection nests and ultrasonic-insertion setups connect the part geometry to the work on the line.
Explore investigation +Close investigation −
Locating, assembling and inspecting the parts
Inspection nests and ultrasonic-insertion setups connect the part geometry to the work on the line.
Explore investigation +Close investigation −Fixtures for assembly and inspection
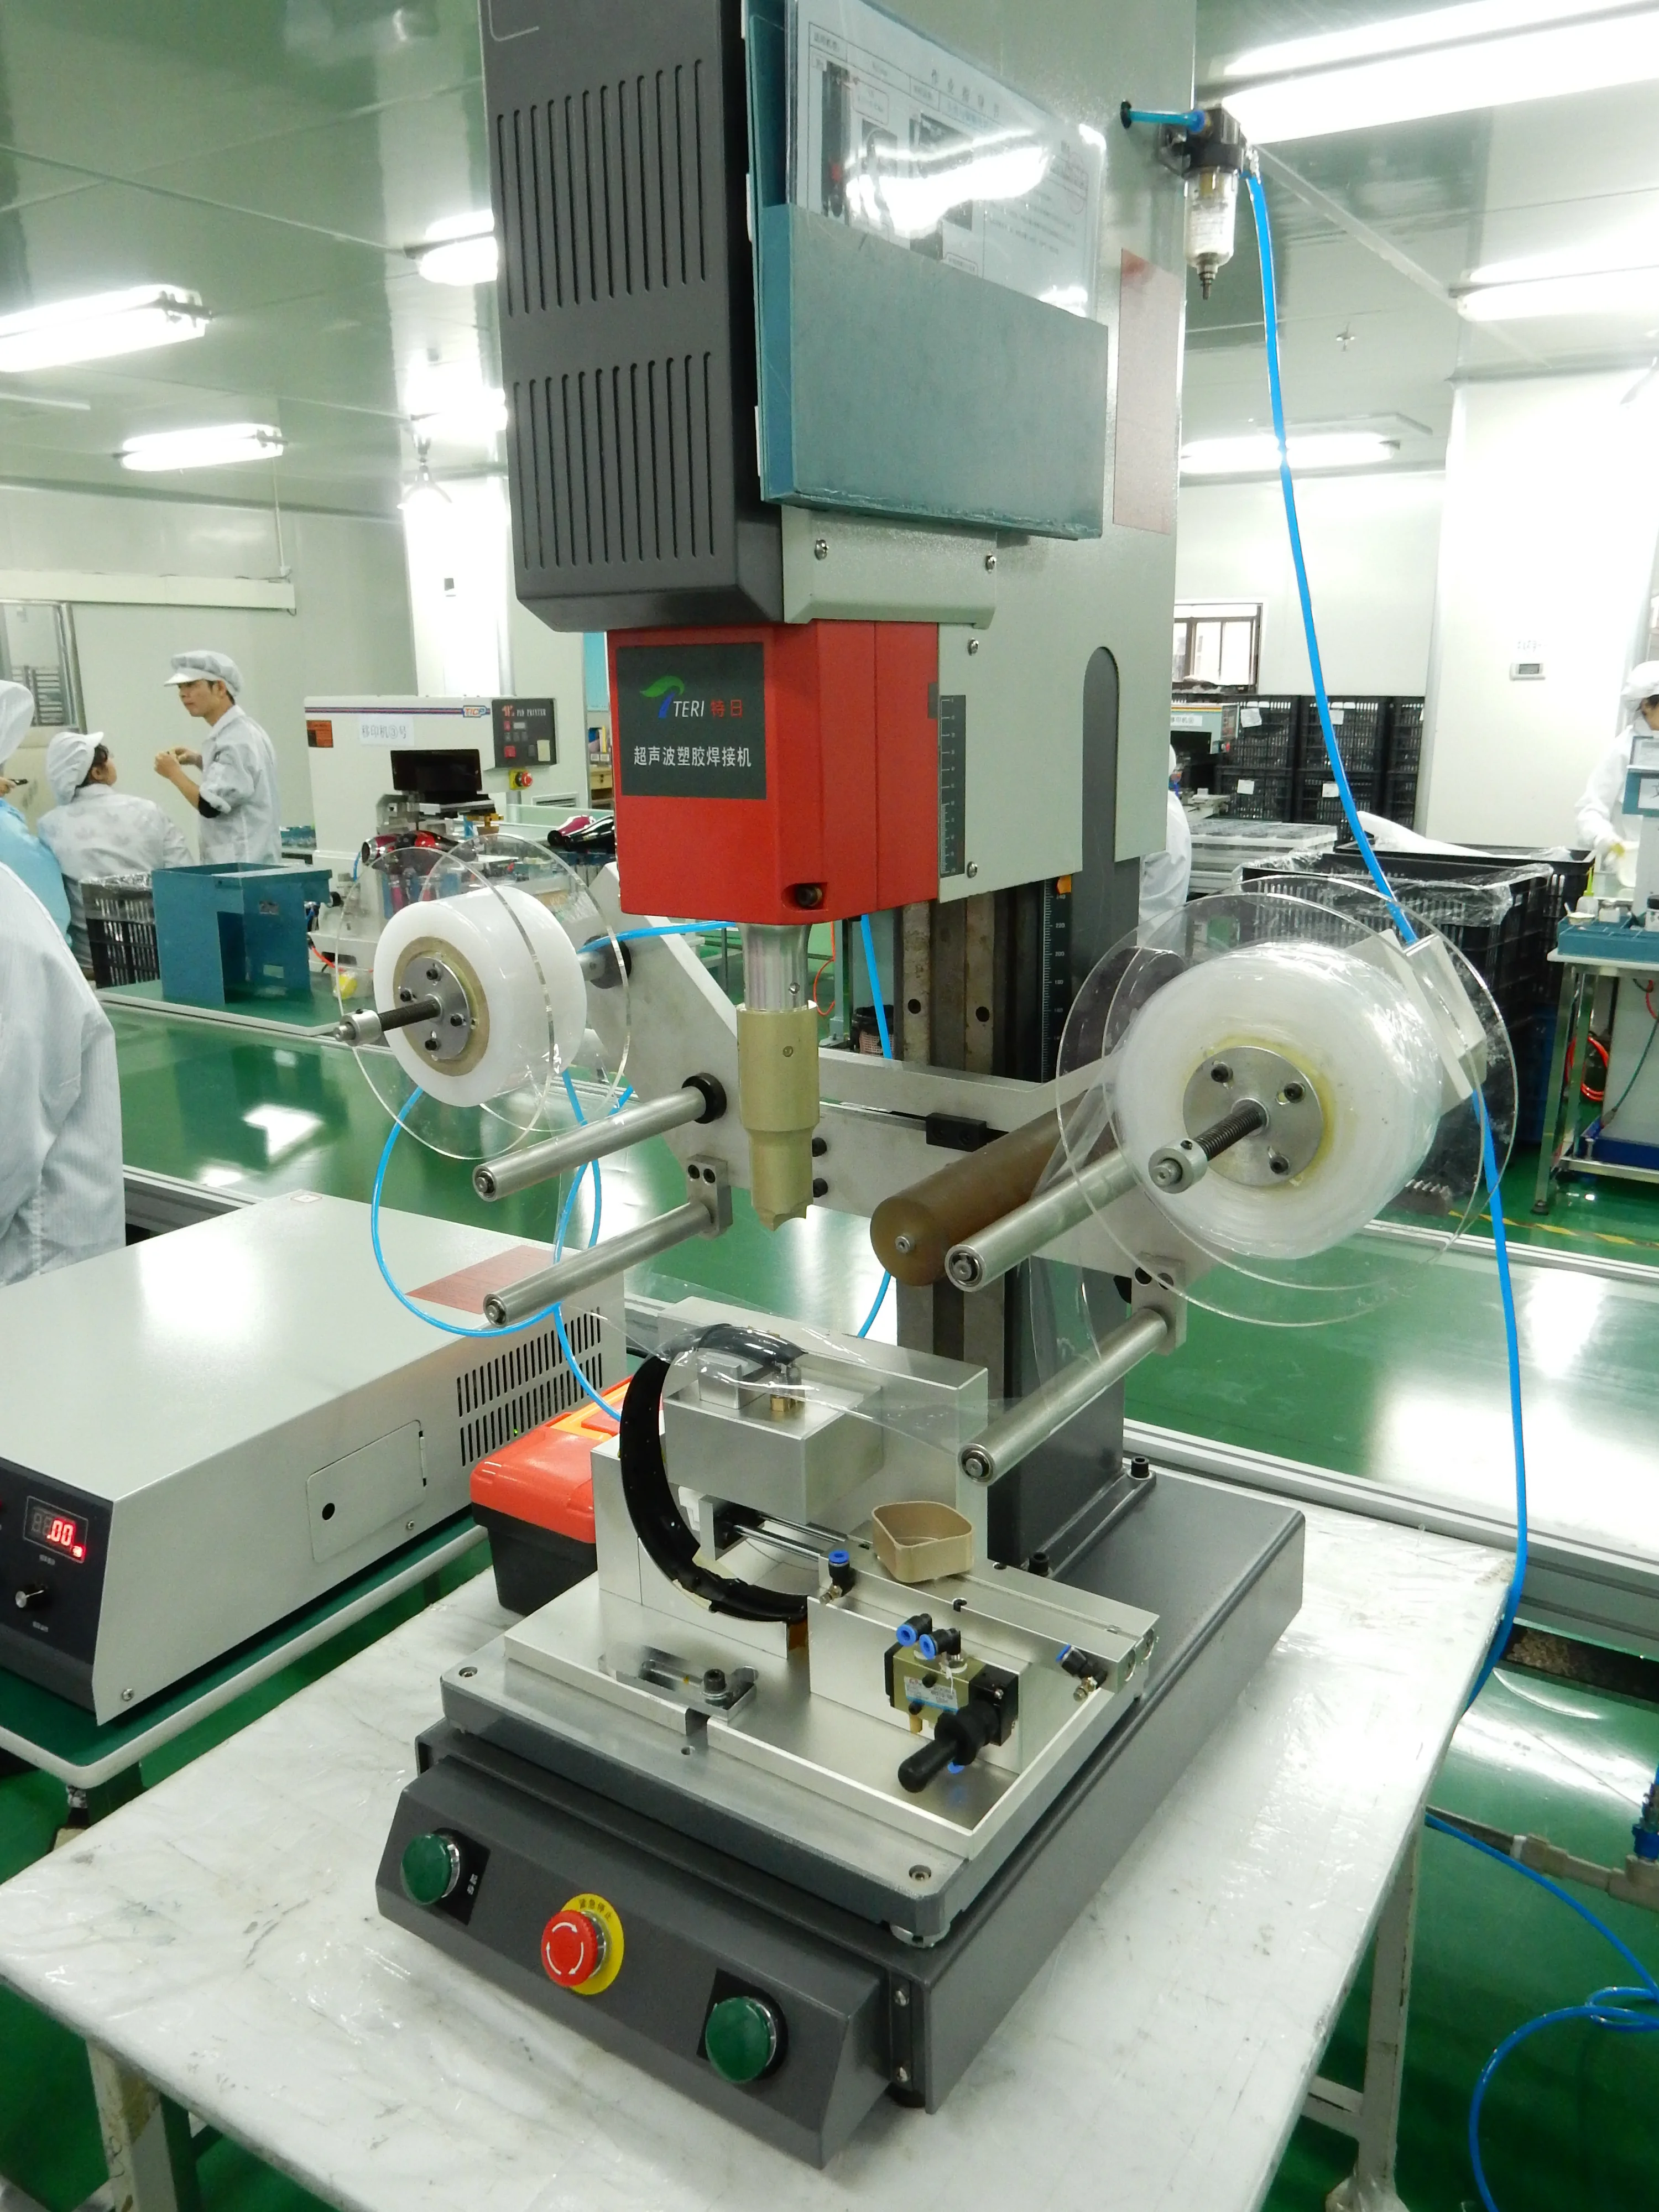
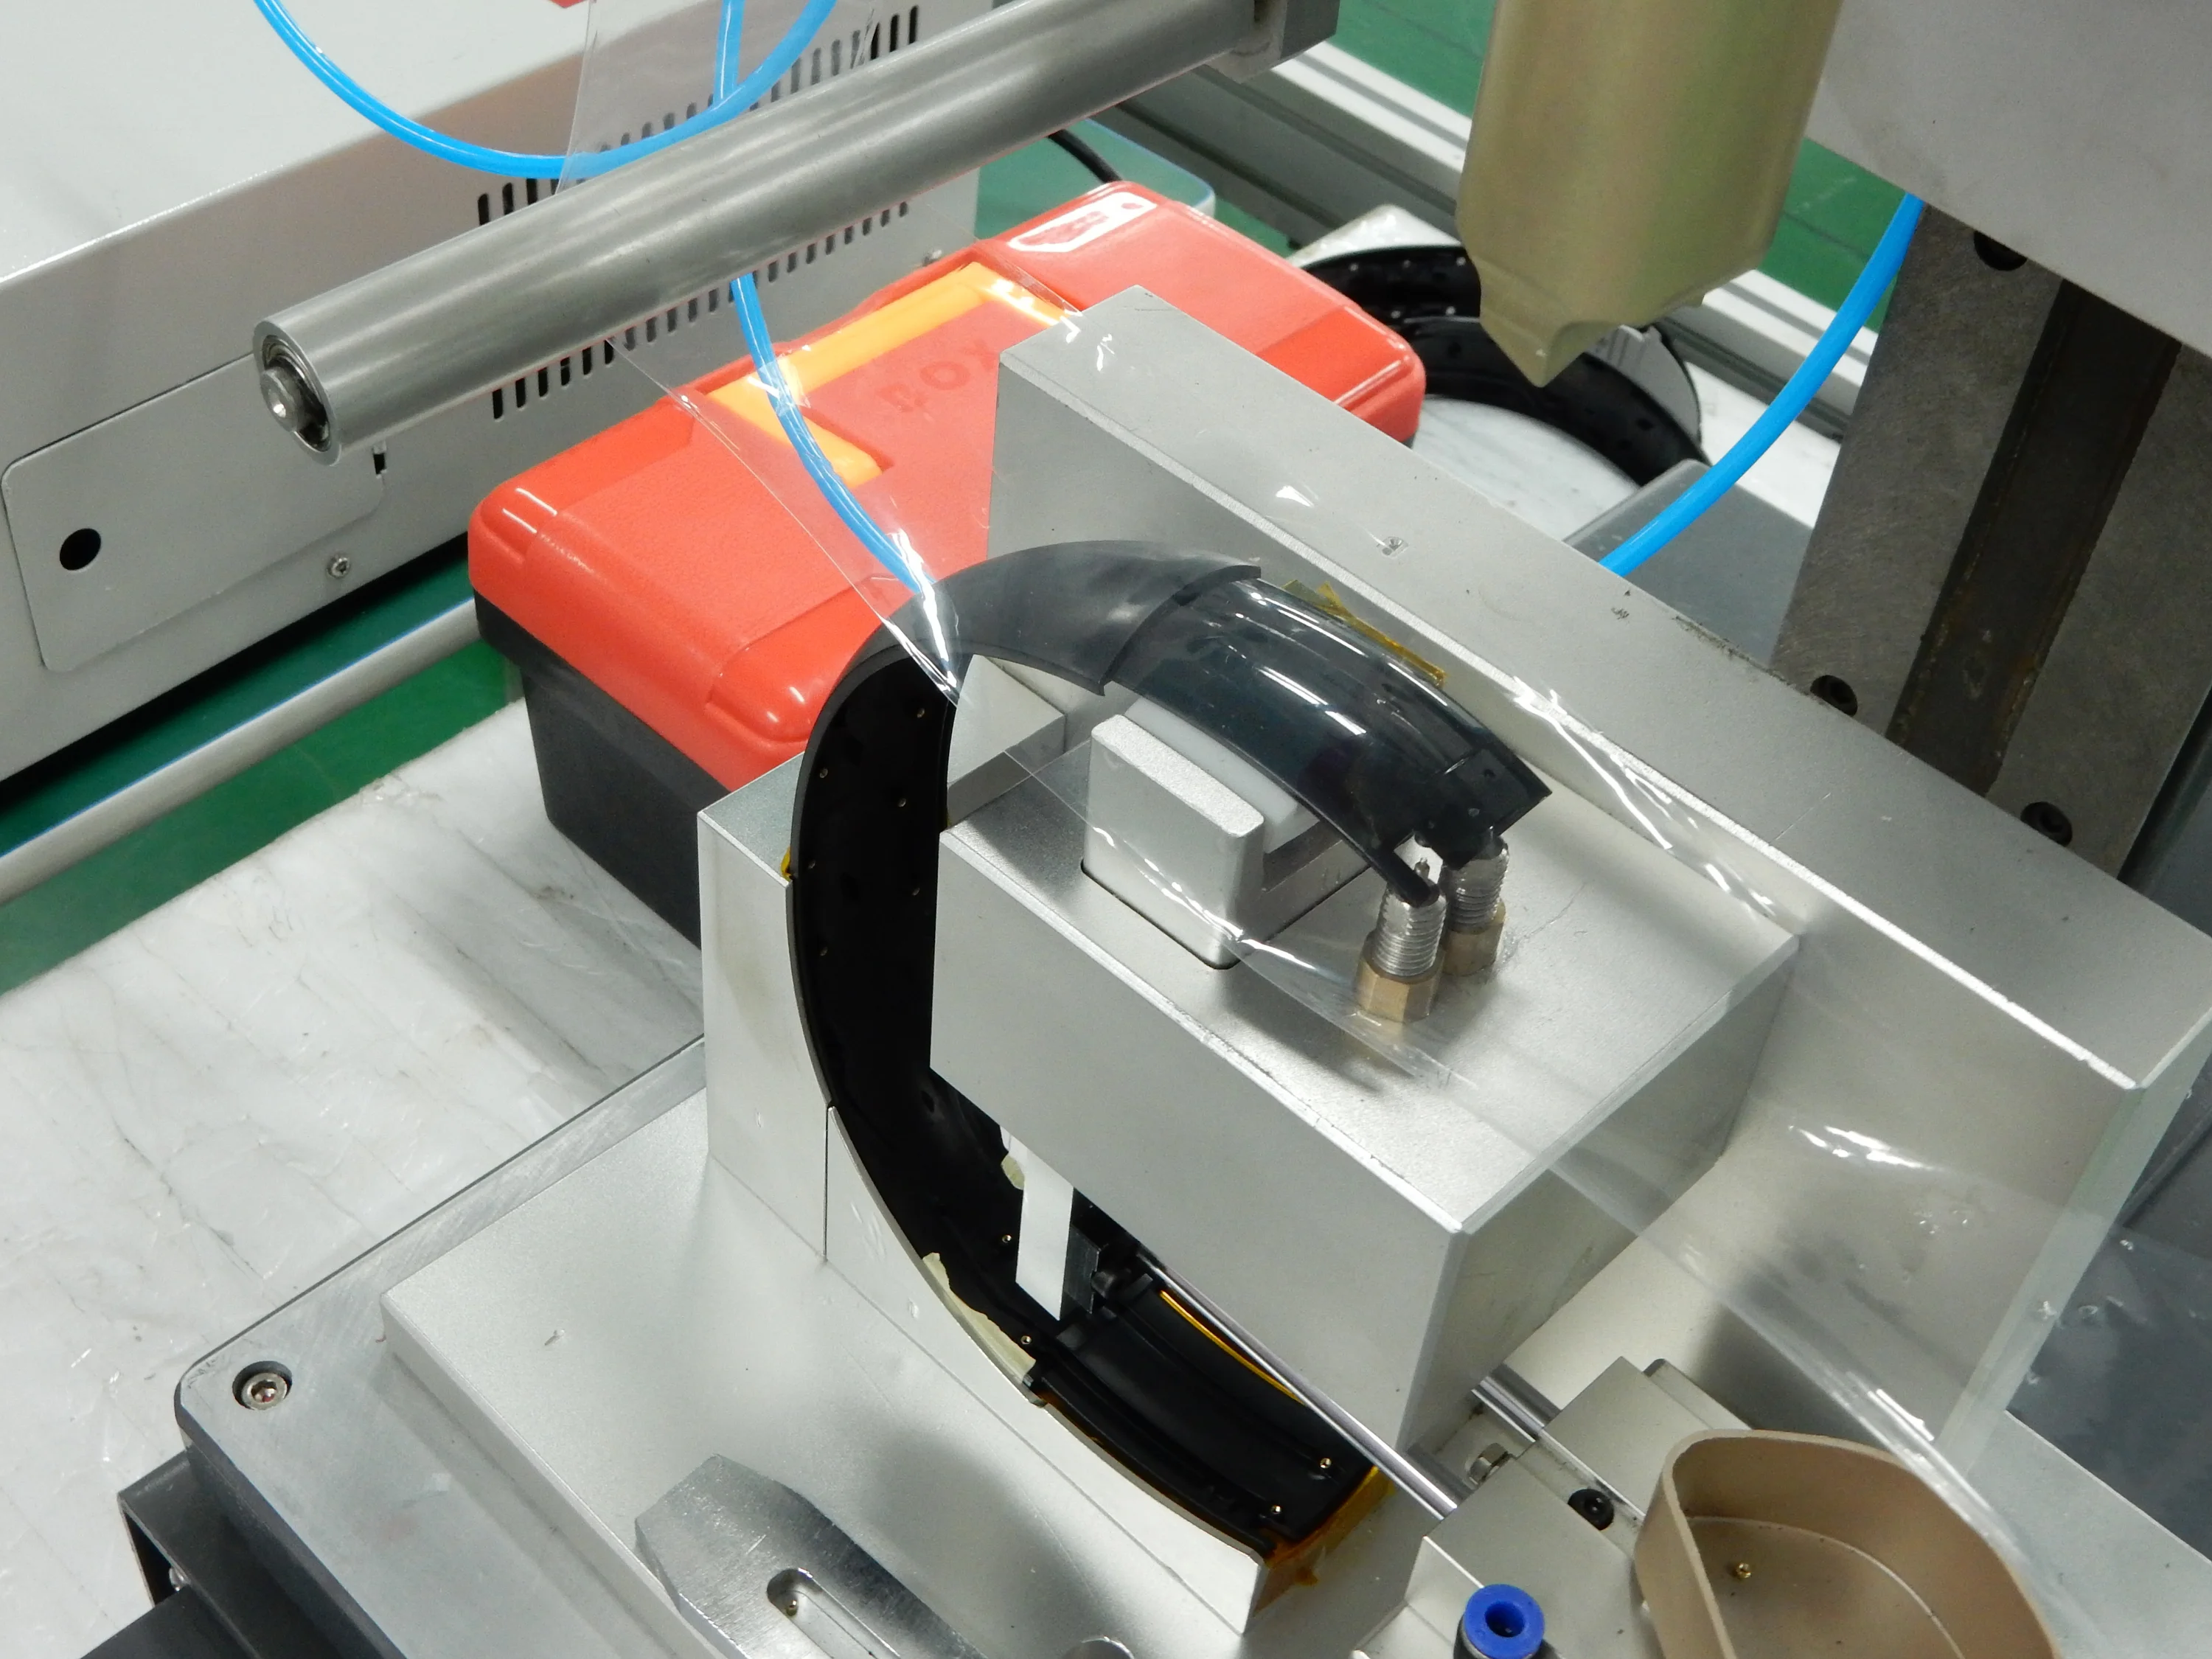
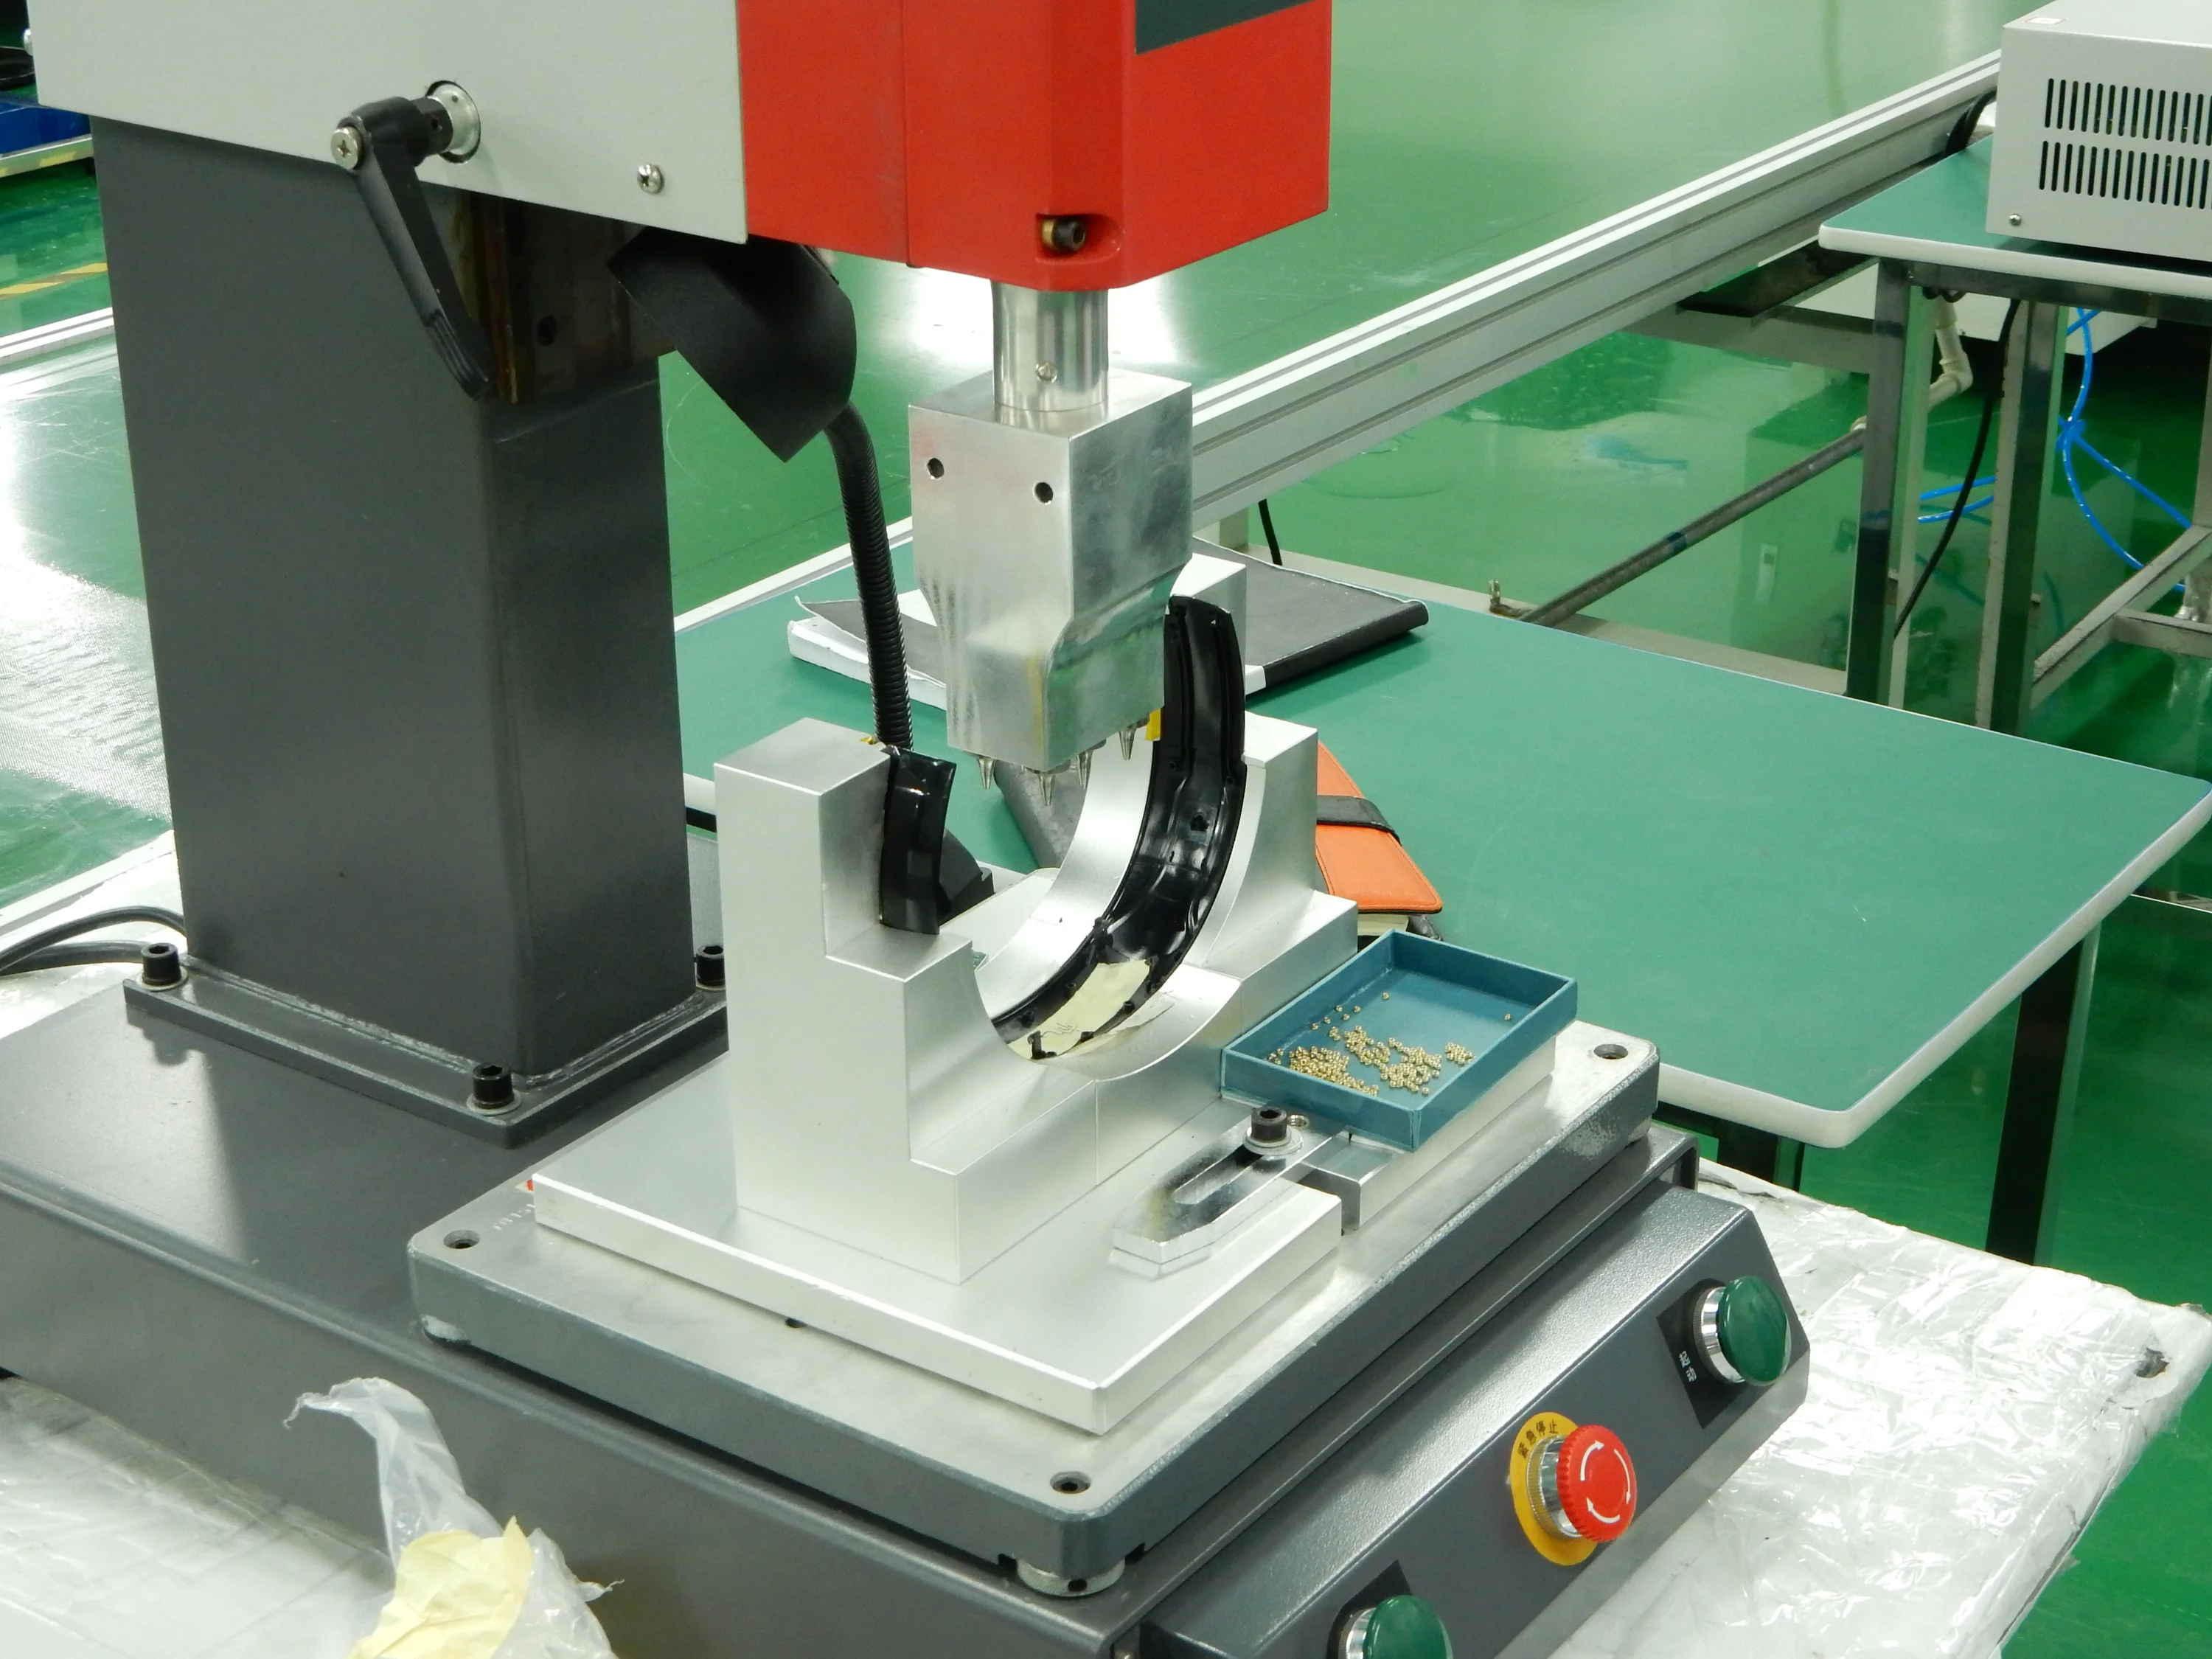
Installing the threaded inserts
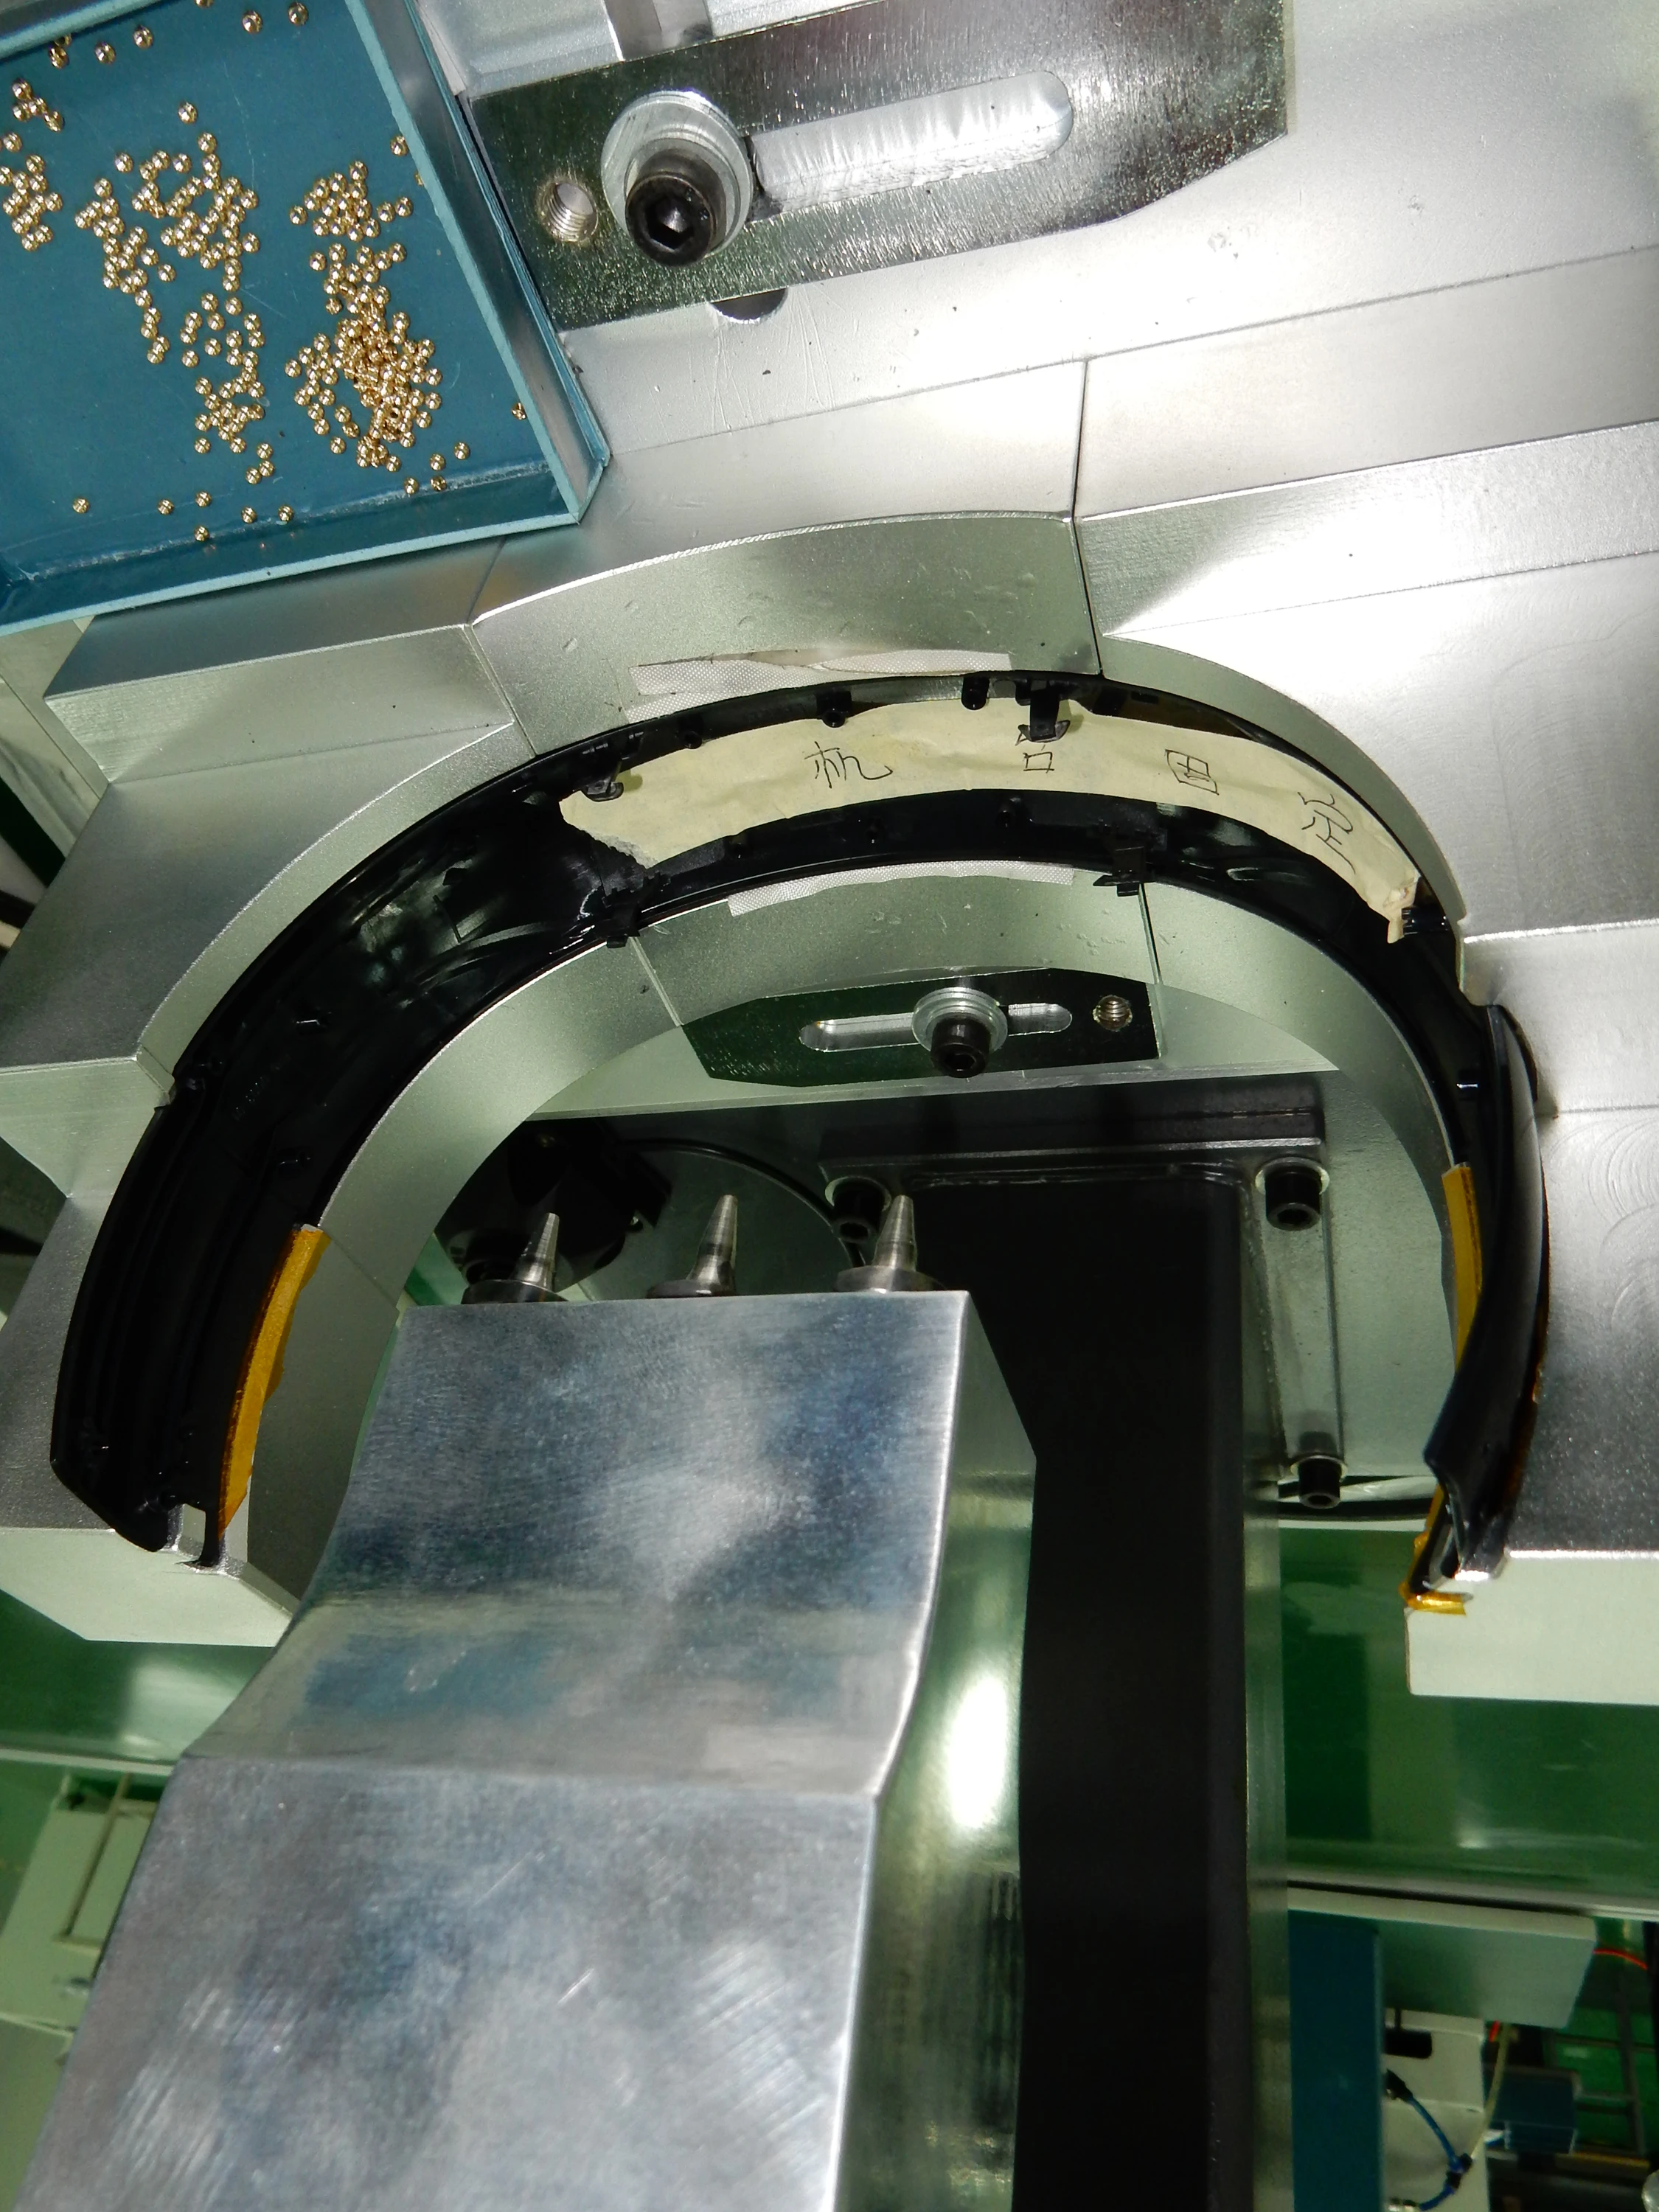
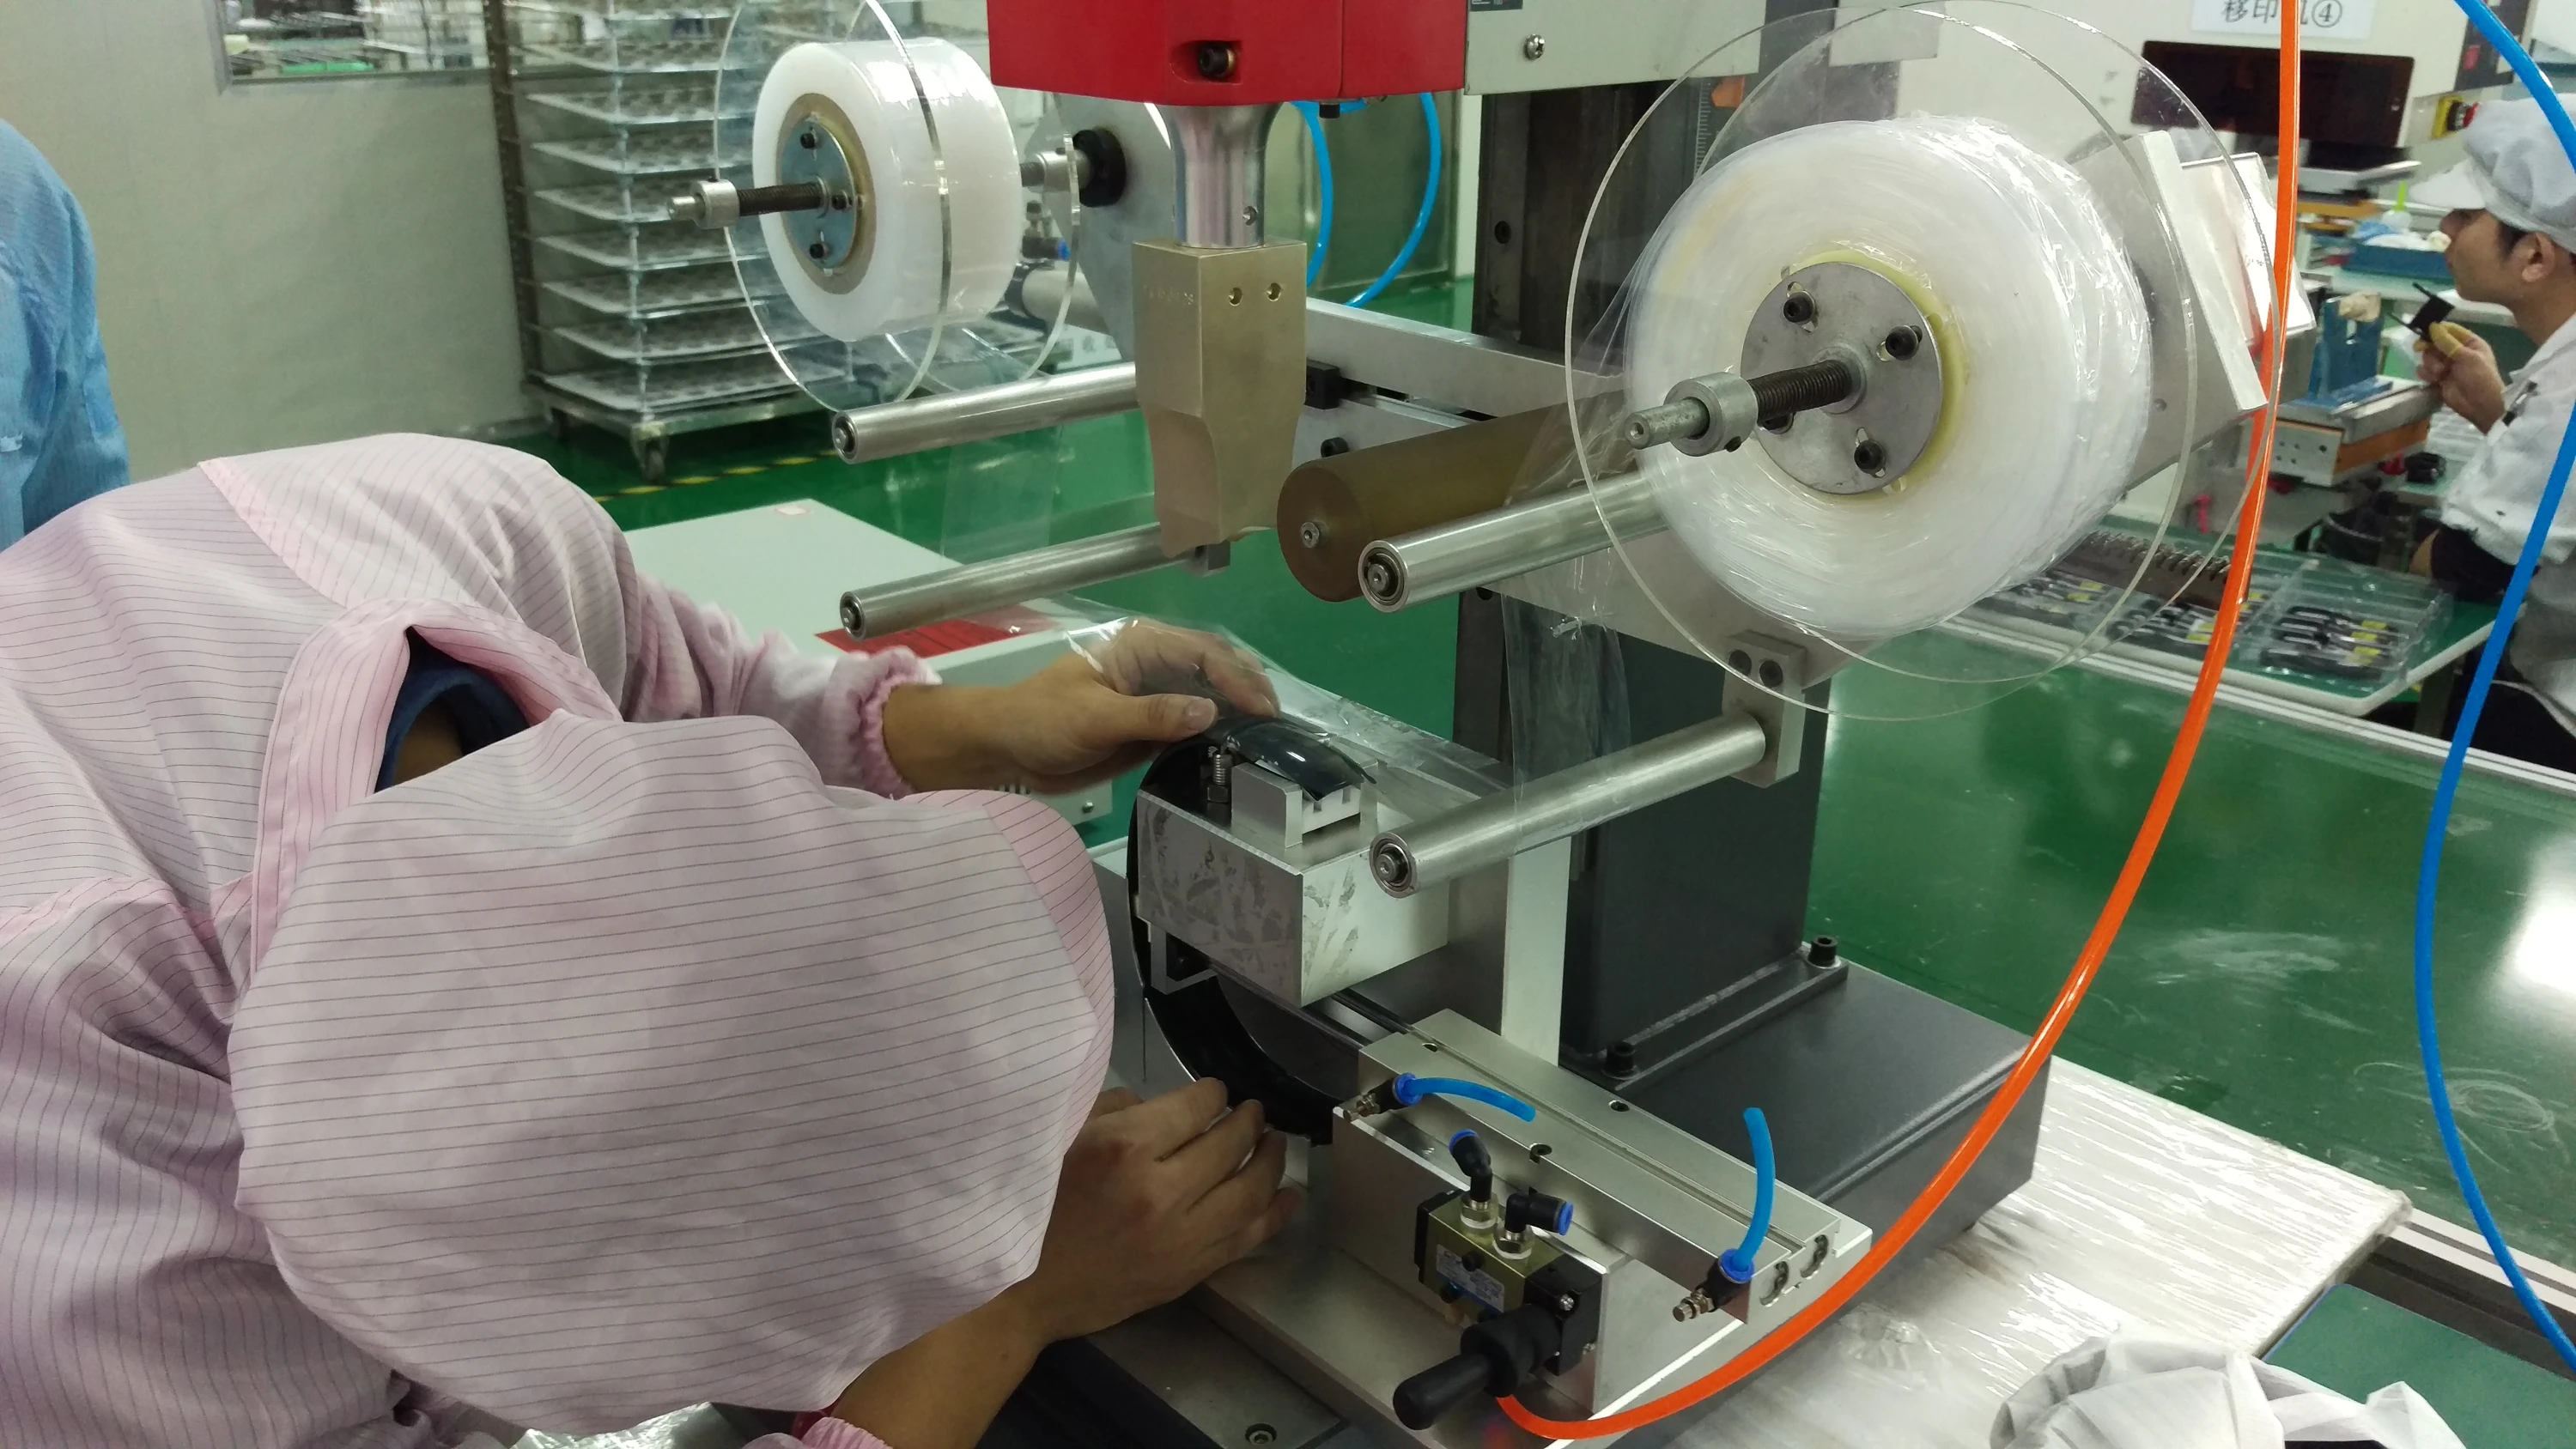
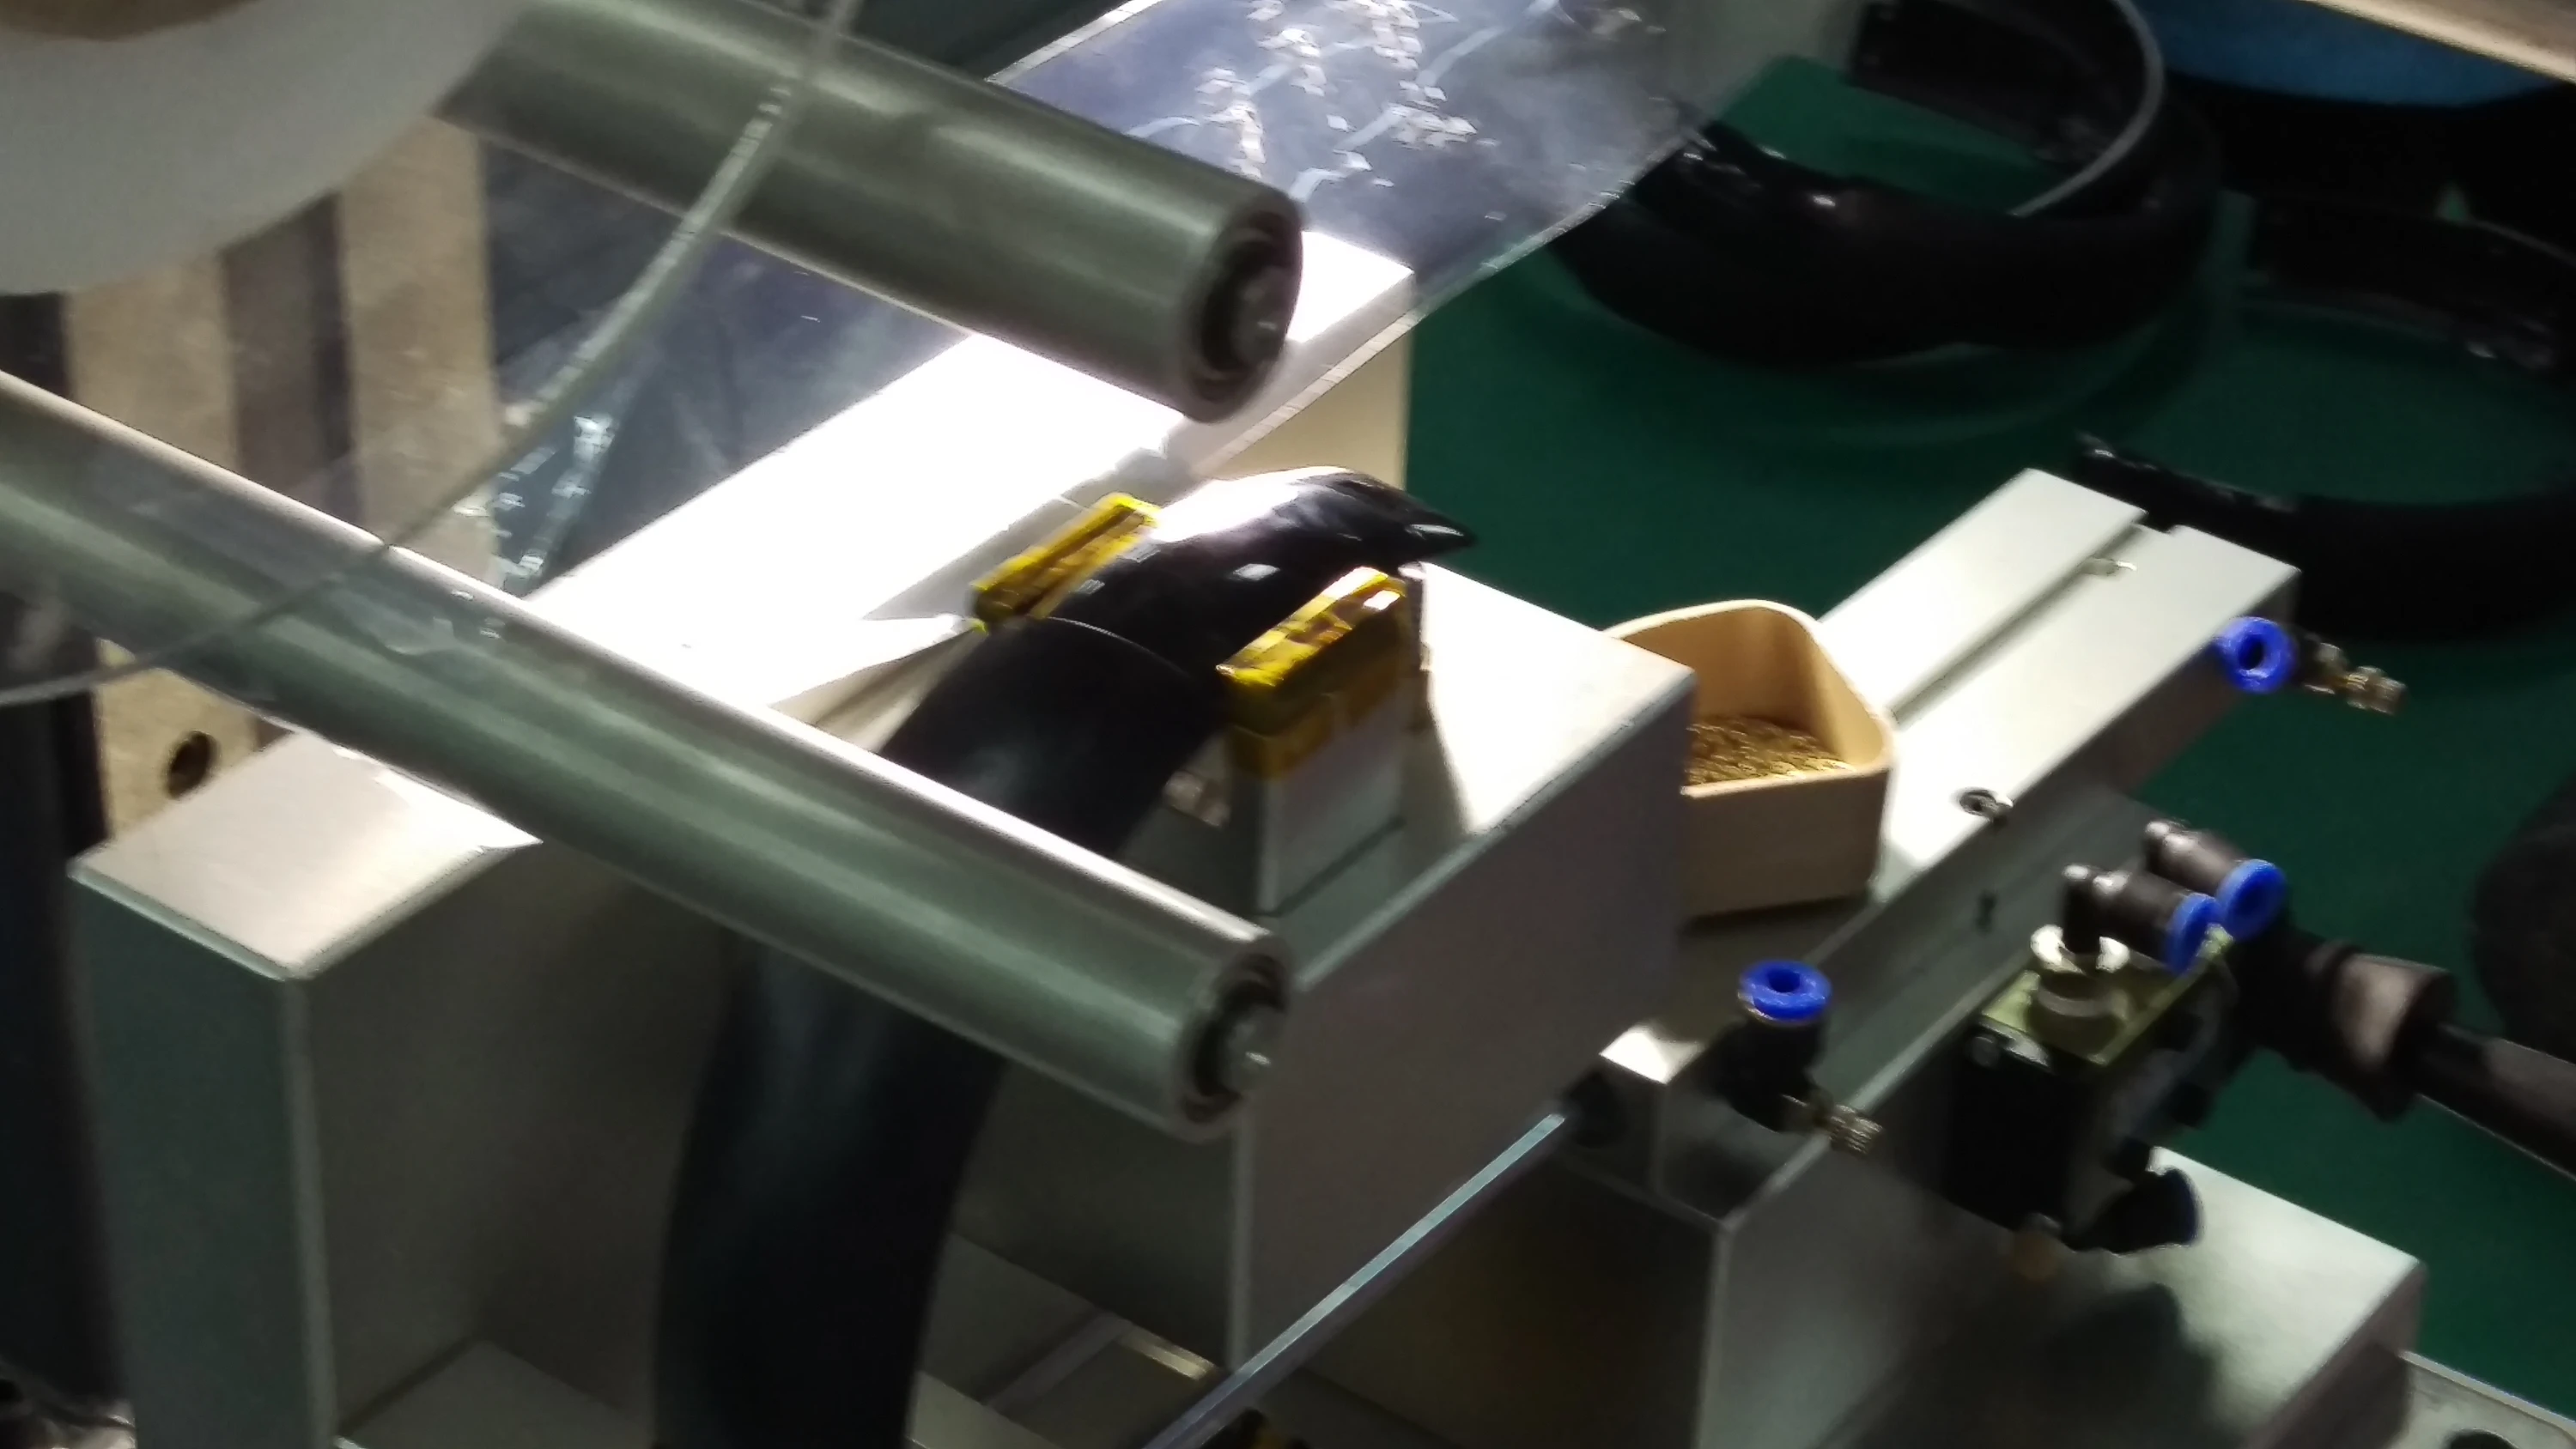
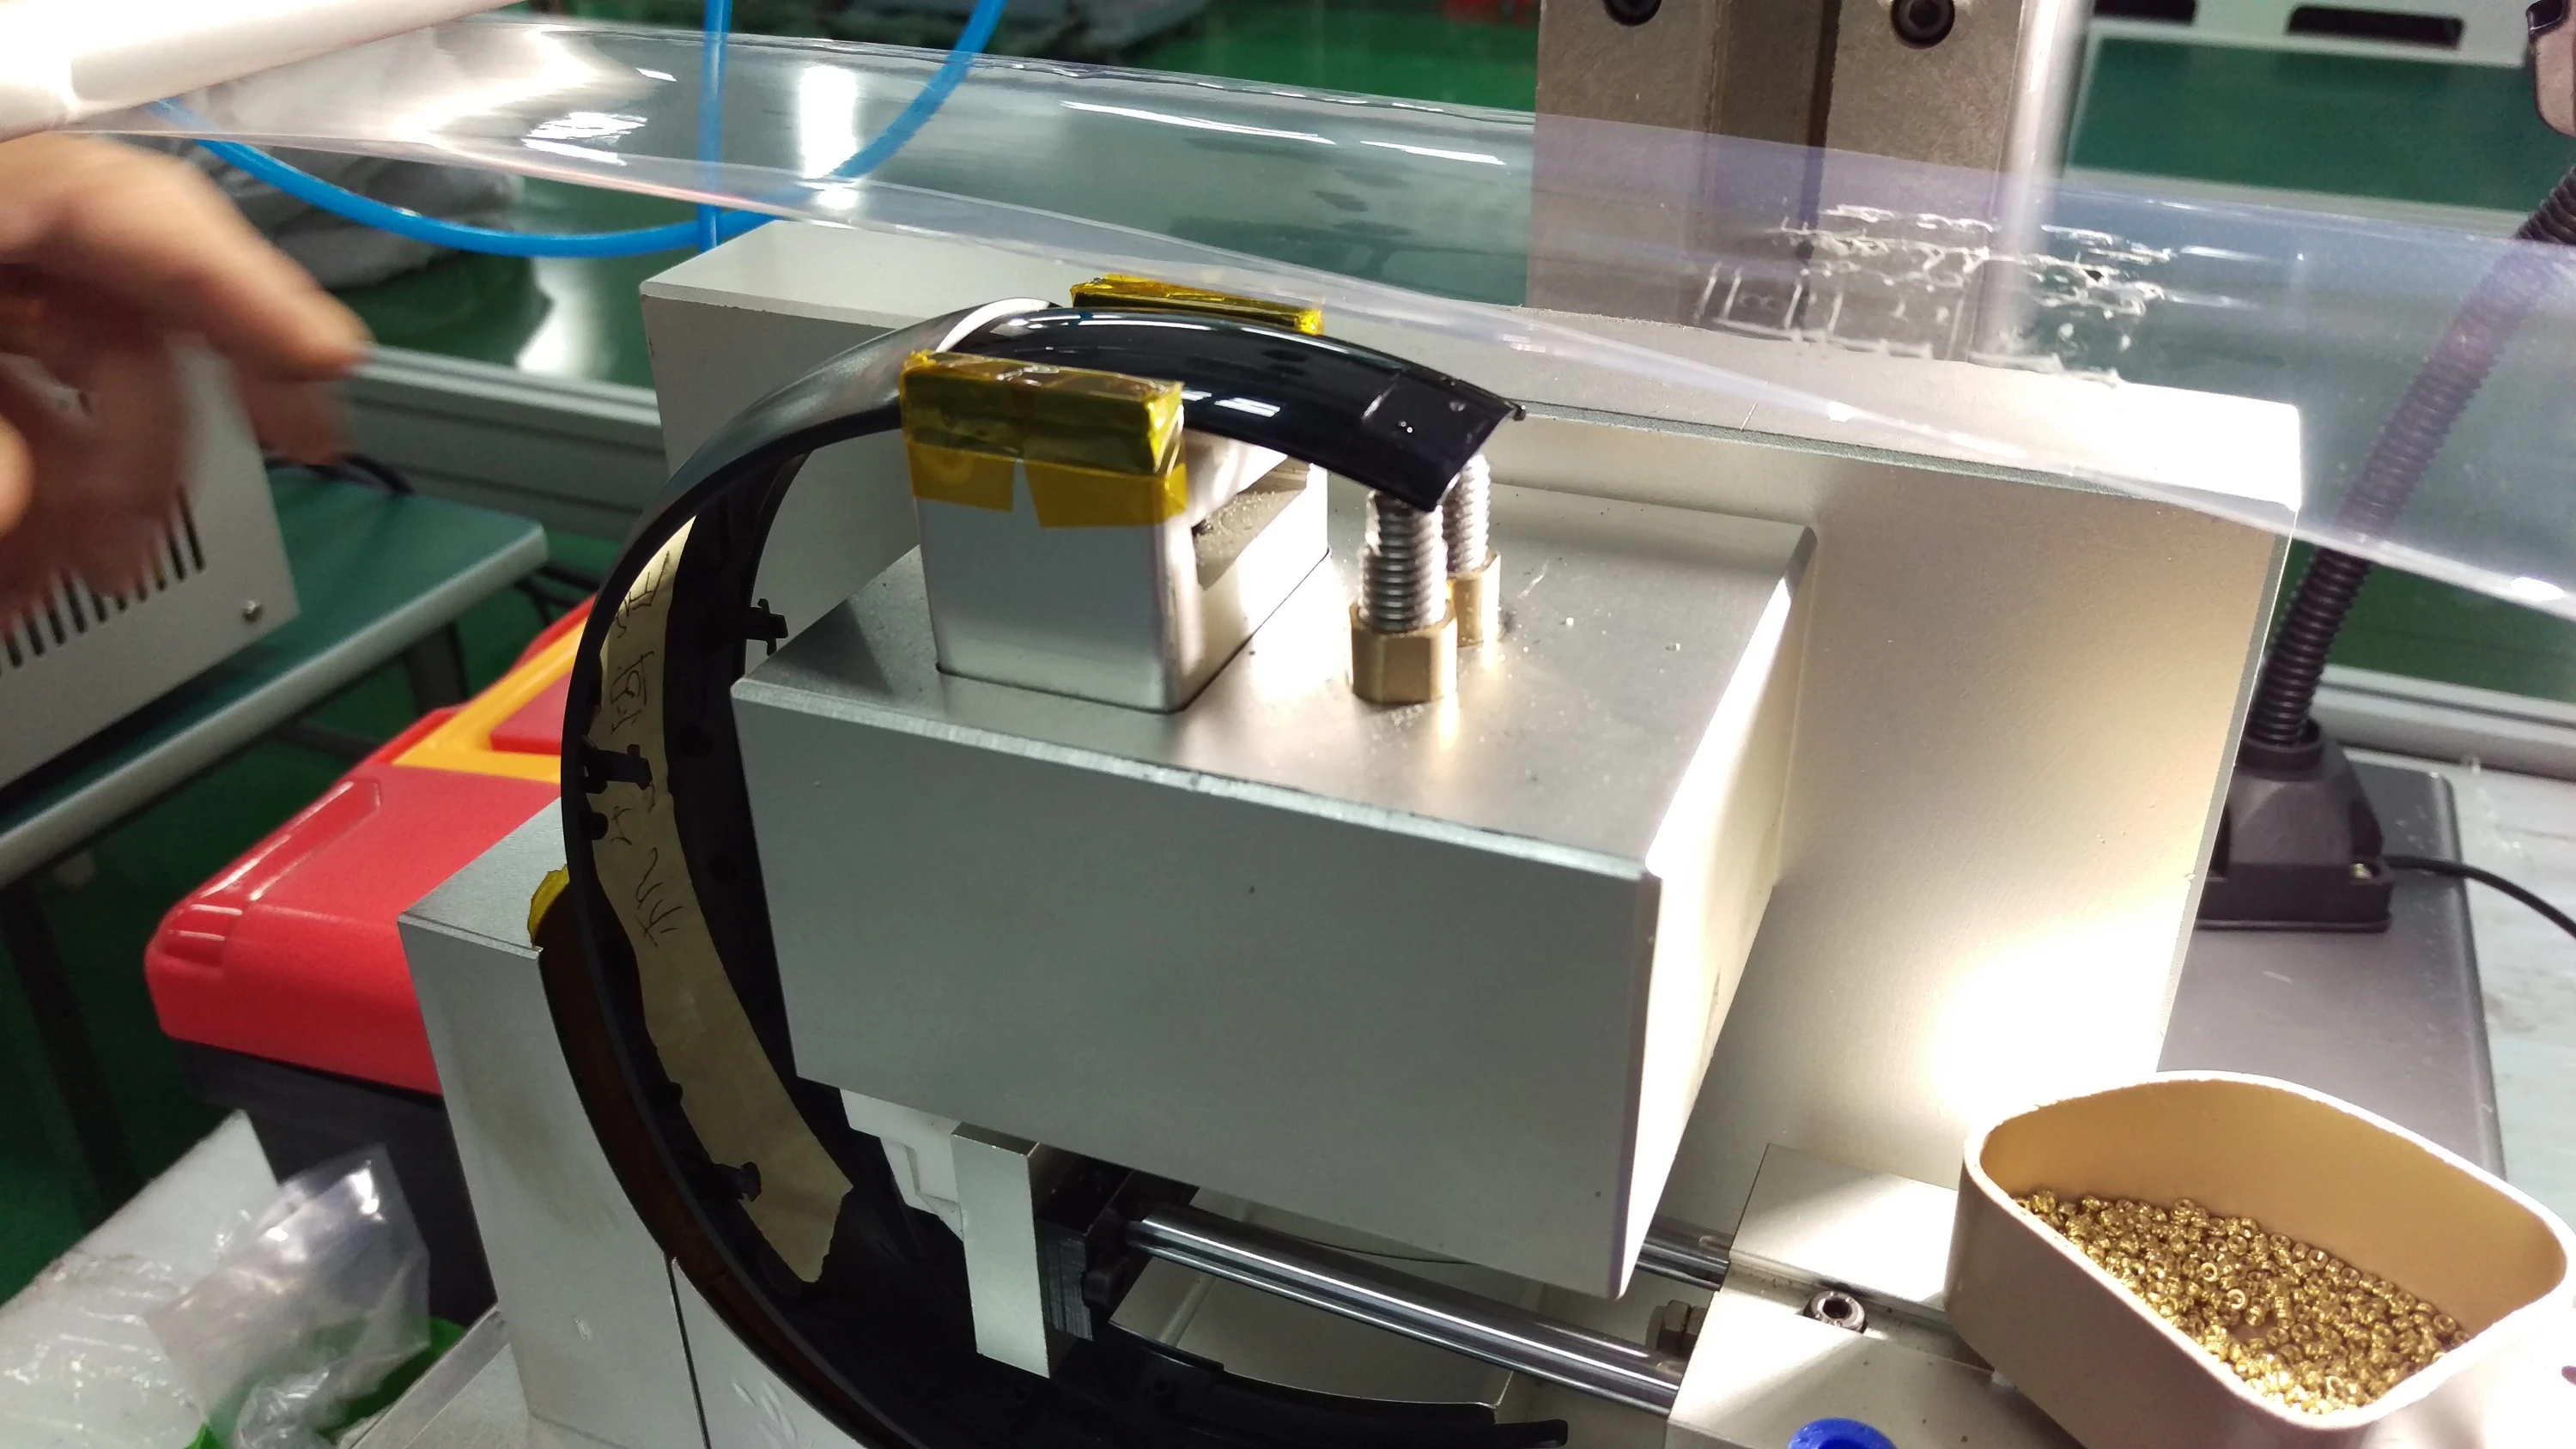
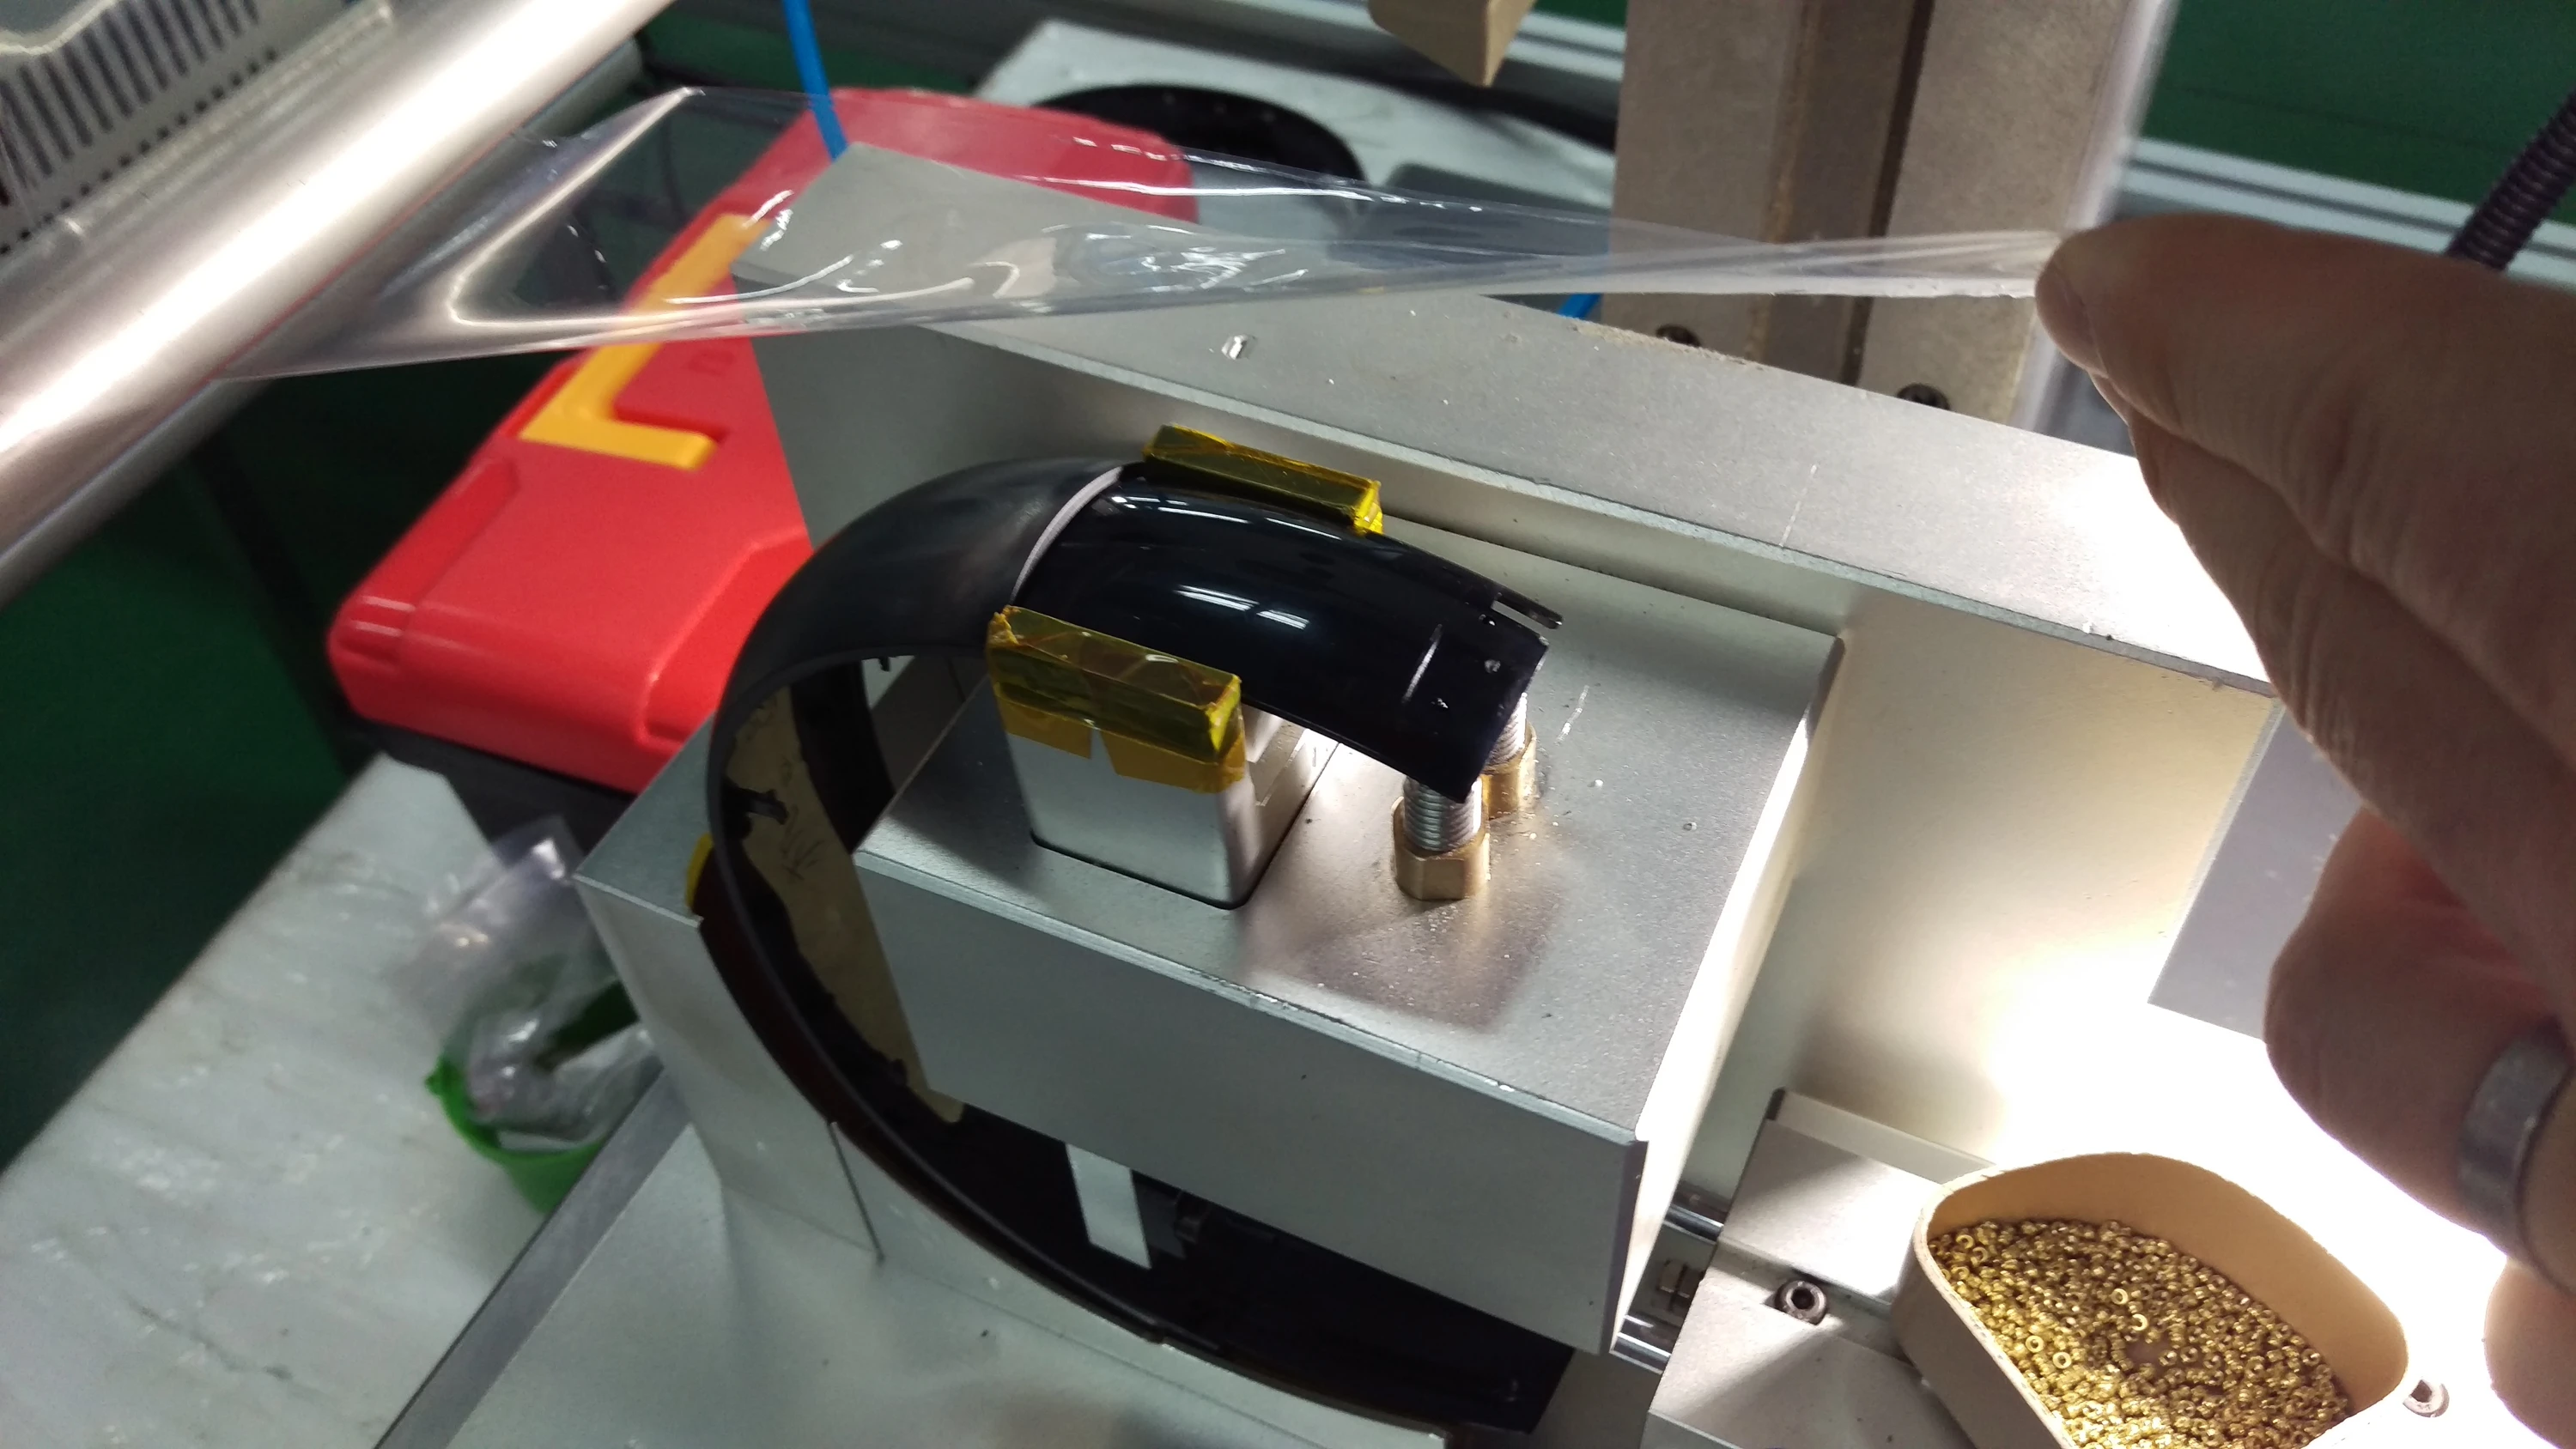
The outer headband required three ultrasonic insertion setups, each with custom fixturing and supports.
Defining and running qualification
I designed and managed the reliability testing program across Glyph. I worked with Intretech on how we would qualify the product and validate changes. The work covered the assembled headset's moving interfaces, environmental exposure, drops, buttons and connectors, as well as the durability of coatings, printing and packaging. It involved test samples and fixtures, operating conditions, inspections during testing and functional checks afterward.
The testing program at a glance
The spring study was one part of this larger effort: its April compilation records 950 measurements across 19 assemblies. It covered three spring groups, ten head widths from 100 to 190 mm, and telescope extensions from 0 to 40 mm. The interactive chart later in the story opens one of those five settings: 190 measurements at 20 mm extension.
We planned the September reliability allocation around a pool of 20 units, assigning samples across the different tests. As the design and process changed, specific fixes needed their own validation. In April 2016, after initial shipping had begun, I had cable-abrasion fixes in validation on 20 units for headband lifecycle testing and another 10 for drop testing. Short-term chassis machining, cable rework and a revised routing scheme were being evaluated alongside longer-term tooling and harness changes.
By April, the six-variant cable comparison was complete and we had rejected the splint approach. Testing was helping us decide what to change in the product already being built.
Manual harness cycle testing
 From the workbench
Testing the parts, the assembly and the process
Map the test programs, watch the lifecycle fixtures and follow a cable failure into a validation plan.
Explore investigation +Close investigation −
Testing the parts, the assembly and the process
Map the test programs, watch the lifecycle fixtures and follow a cable failure into a validation plan.
Explore investigation +Close investigation −A map of the testing program
The test configuration mattered as much as the method. A bare spring, a cable installed in the headset and a powered finished unit answered different questions. I had to connect the result to the parts, assembly condition and change we were evaluating.
| Program and level | Configuration and method | What we checked or learned |
|---|---|---|
| Mechanism life · assembled headset | Repeated headband opening, telescoping, eyepiece release/lock, gimbal and switch operation | Force, return, retention, cable wear and function at intervals; the March report attributed one eyepiece-lock failure to an overly tight screw. |
| Environmental · finished units | Operating and non-operating temperature/humidity, including 96-hour exposures in the March program | Appearance and operation after exposure; the results included display and audio problems requiring diagnosis. |
| Vibration and drops · assembled product | Vibration testing and separate drop-test allocations; revised cable assemblies needed their own validation | Retention and function; vibration exposed a loose lock spring. A planned drop allocation remained distinct from a completed result. |
| Interfaces · parts and assemblies | Connector insertion and directional loading; button force/travel; gap measurements before and after temperature/humidity shipment | Free play, intermittent display, actuation feel and changes at mating surfaces. |
| Fit · springs, liners and complete headsets | Spring metrology, clamp-force comparisons at different widths/extensions, earpad variants and wearer trials | Part variation, assembled force, retention and comfort; Jill helped with the spring-and-liner assembly and testing. |
| Cosmetics · materials and finishes | A 16-method specification system with material-specific applicability; solvent, stain, UV, hardness, adhesion and abrasion testing | Coating and printing condition, finish durability and appearance. The specification methods and populated result sheets served different purposes. |
| Accelerated stress and screening | HALT/HASS alongside subsystem and system reliability work | Part of the wider set of experiments and testing programs I designed and managed. |
| Production changes · revised assemblies | Targeted cycling, drops, functional checks and teardown after rework | Whether a proposed change addressed the failure in the assembled product; the cable example below shows how we set up that validation. |
The map brings together the reliability plans, March production-test results, interface studies and cosmetic specifications. HALT/HASS was also part of the program I designed and managed.
Exercising the assembly
The fixtures had to reproduce the movement we cared about: opening the headband, extending and returning the arms, and moving the earcup interfaces. Travel, speed, applied force and the position of the stops all mattered. In September 2015, I requested an adjustment to the headband-life fixture so it could exercise the assembly at full extension.
These three short clips show a few of the fixtures exercising Glyph. They make the motion visible; the measurements, inspections and functional checks tell us what happened to the product.
Exercising the moving interfaces
For the headband, we specified 3,000 cycles, checking every 500 and measuring the opening force before and after. The telescoping arms also had a 3,000-cycle procedure. I was revising Frank Jiang's earlier reliability plan and seeking input from Jansen and Geoff on the methods and missing conditions.
Checking function while the interface moved
The micro-HDMI investigation shows why a functional check at rest was only part of the test. In August 2015, the connector was repeatedly inserted, removed and loaded in four directions, with dimensional and free-play measurements before and after. The display could look normal at a checkpoint, then briefly turn green or black during the separate wiggle check before recovering. Those observations made the behavior under movement visible alongside the changes in the physical interface.
A September button reference study paired a position map with repeated force and travel measurements, recorded curves and photographs of the tester. It mapped seven button positions on four labeled samples, with ten repeats of each measurement. The report also recorded a hand-feel complaint: the measured response and the feel of the interface were separate parts of the evaluation.
Reading the test response
A September test-command workbook put Intretech's replies beside Avegant's feedback. The status-command definition allowed an OK response while still reporting a nonzero error code. The audio feedback clarified another apparent fault: without video, audio was supposed to be muted. Interpreting the result meant checking what the command reported and the operating state it assumed. An OK response alone did not mean the product had passed its tests.
From cable failure to a validation plan
The cable work joined a symptom, a physical investigation and a test of the proposed changes:
- Expose the failure. Repeated movement could kink the cable inward or outward. Protective tape could also curl at its edges and make the arm harder to telescope. A change that resisted buckling still had to fit and move through the confined route.
- Change the assembly. The January cable study records removing damaged wrap and replacing it with new tape. We also compared stiffness and wrap concepts, then evaluated cable changes alongside chassis machining, protective tape, PSA placement and routing. The surrounding parts were part of the fix.
- Exercise and inspect the revised units. The March validation plan allocated 20 production-level assemblies to headband life and another 10 to drops. The life procedure called for 3,000 cycles, with audio/video checks every 500. The cable study also called for functional evaluation before teardown and internal inspection.
The April updates still had cable-abrasion changes in validation. They recorded the splint approach as rejected while alternative harness work continued. That was the decision reached at this stage, with further work still underway. The cable investigation follows the routing, photographs and separate cycle-test groups in detail.
Keeping track of the test units
The September reliability allocation used a shared pool of 20 units. That was a separate allocation from the later cable-fix validation. Reusing assemblies across methods made sample configuration and test order part of the engineering work.
I coordinated reuse of test units across those investigations: clear housings made cable routing visible, and units could go on to salt spray, humidity and UV testing. A unit could contribute to several investigations, with each test answering a different question.
Qualification continued through the ramp. I had to coordinate the parts and sample configurations, the supplier changes and the testing needed to put a change into production, while backer deliveries were still underway. Comfort brought us back to people wearing the assemblies we were making.
Making Glyph wearable
Taking the load off the nose
I couldn't wear Glyph for more than a few minutes without pain. We kept hearing that people's ears hurt, and the silicone nosepads left deep, angry marks on many test subjects that took a long time to disappear.
Radius Product Development supported the headstrap work.
The headstrap was a late addition. I proposed it, got it approved, tested it and brought it into production relatively quickly. Radius developed support concepts and mockups during that work. I added receiver features to the earcans for quick-release buckles, so the strap could be removed and Glyph could still be used without it.
With the strap attached to both earcans and adjusted over the crown, it took almost all the load off the nosepiece. The nosepiece then mainly located the unit, while the top of the head carried the weight. The strap also added another contact that helped keep the display in place.
It was a hold-your-nose solution. The strap was big and bulky, caught in people's hair and was tricky to adjust correctly the first time. It basically turned the headphones into a hat. We accepted it reluctantly, late in a long and frustrating engineering effort under pressure to deliver the overdue Kickstarter product. Once people got the hang of it, though, it became essential for longer use. It was the comfort fix I felt had the most impact.
Keeping it optional left another constraint in place: the earcups still had to grip hard enough to hold Glyph without the strap. I reduced the clamp as far as I could while preserving that use. Even then, it was too much for me to wear comfortably for long, with or without the strap. Taking weight off the nose made a substantial difference; the ear pressure remained.
Tuning the pivot feel
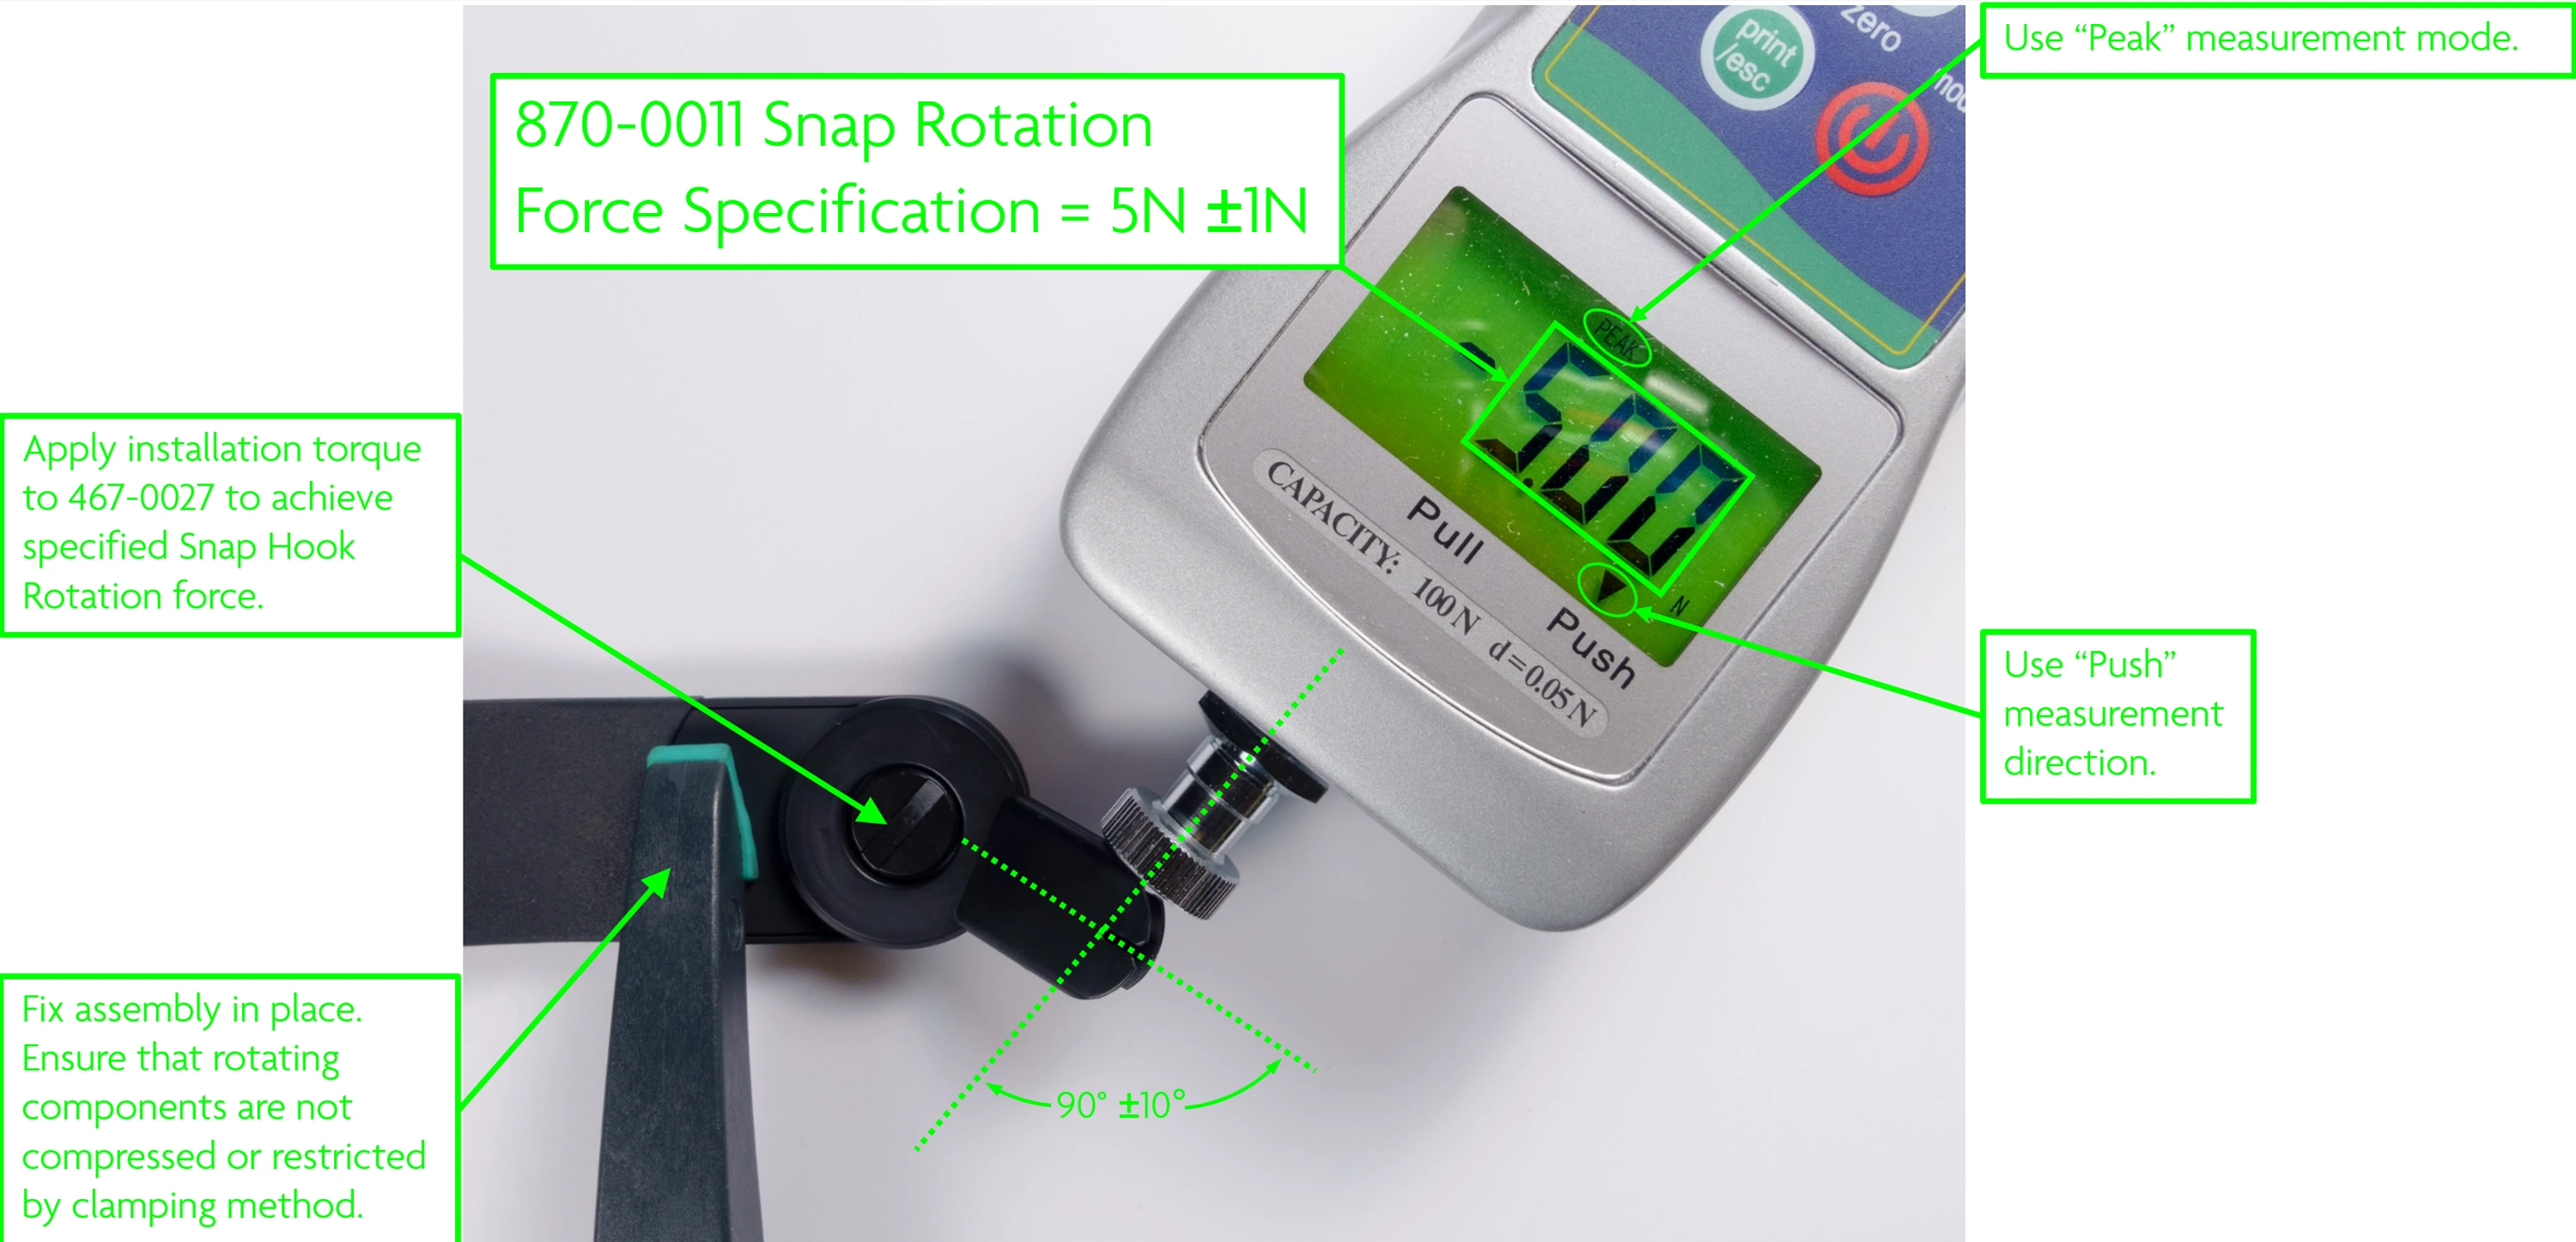
I also specified a damping grease for the headstrap pivot to get the feel and resistance right. I wanted something like the controlled movement of an expensive volume knob. Pivot torque testing was part of that work.
Measuring the pivot force
Measuring the assembled clamp force
Clamp force changed with both head width and telescope position. We measured the assembled headset across those settings while comparing spring and liner configurations. Jill helped with assembly and testing during the spring-and-liner work. At 150 mm width and 20 mm extension, the recorded 1.6, 1.4 and 1.2 mm spring groups averaged 11.7, 11.0 and 9.6 N. The curves show why a single force number could not describe the fit.
 From the workbench
Spring response, test coverage and part variation
Explore the assembly force curves and measurement coverage, then compare them with spring dimensional checks.
Explore investigation +Close investigation −
Spring response, test coverage and part variation
Explore the assembly force curves and measurement coverage, then compare them with spring dimensional checks.
Explore investigation +Close investigation −Spring assemblies: response and test coverage
20 mm telescope extension · 75A liners · 19 assemblies
Assembly response
Heavy lines show group means; fine lines show each assembly. Move across the measured widths to compare the responses.
Separate groups of assembled headsets. These curves show assembly response, not wearer comfort or an isolated causal effect of spring diameter.
Test coverage
19 assemblies × 10 widths = 190 measurements
Each filled cell is one recorded force measurement. Rows follow individual assemblies across the same ten widths.
| Assembly | 100 | 110 | 120 | 130 | 140 | 150 | 160 | 170 | 180 | 190 |
|---|---|---|---|---|---|---|---|---|---|---|
| 1.6 mm · 01 | 5.4 N● | 6.35 N● | 7.3 N● | 8.65 N● | 10.6 N● | 12.5 N● | 14.4 N● | 16.8 N● | 18.6 N● | 20.3 N● |
| 1.6 mm · 02 | 5.2 N● | 6.35 N● | 7.75 N● | 9.3 N● | 11.25 N● | 12.85 N● | 15.1 N● | 16.95 N● | 18.8 N● | 20.8 N● |
| 1.6 mm · 03 | 5.05 N● | 6.35 N● | 7.45 N● | 8.85 N● | 10.75 N● | 12.7 N● | 14.5 N● | 17.3 N● | 19.1 N● | 20.9 N● |
| 1.6 mm · 04 | 5.3 N● | 6.5 N● | 7.7 N● | 9 N● | 10.85 N● | 12.75 N● | 14.65 N● | 17 N● | 18.8 N● | 20.9 N● |
| 1.6 mm · 05 | 3.9 N● | 5.2 N● | 6.35 N● | 7.6 N● | 9.6 N● | 11.5 N● | 13.3 N● | 15.35 N● | 16.9 N● | 18.8 N● |
| 1.6 mm · 06 | 5.05 N● | 6.1 N● | 6.9 N● | 8.5 N● | 10.2 N● | 11.85 N● | 14 N● | 16.55 N● | 18.6 N● | 19.75 N● |
| 1.6 mm · 07 | 3.6 N● | 4.65 N● | 5.7 N● | 6.9 N● | 8.3 N● | 10.05 N● | 12.1 N● | 14.3 N● | 16.2 N● | 17.8 N● |
| 1.6 mm · 08 | 4.2 N● | 5.2 N● | 6.1 N● | 7.25 N● | 8.6 N● | 10.15 N● | 12 N● | 13.7 N● | 15.35 N● | 17 N● |
| 1.6 mm · 09 | 4.35 N● | 5.45 N● | 6.3 N● | 7.5 N● | 8.9 N● | 10.55 N● | 12.5 N● | 14.4 N● | 16 N● | 18 N● |
| 1.4 mm · 01 | 3.9 N● | 4.7 N● | 5.75 N● | 6.9 N● | 8.5 N● | 10.3 N● | 12.4 N● | 14.4 N● | 16.9 N● | 18.8 N● |
| 1.4 mm · 02 | 4.15 N● | 5.2 N● | 6.35 N● | 7.85 N● | 9.5 N● | 11.2 N● | 13.15 N● | 15.5 N● | 17.4 N● | 18.6 N● |
| 1.4 mm · 03 | 3.55 N● | 4.8 N● | 5.9 N● | 7.3 N● | 9.1 N● | 10.95 N● | 12.75 N● | 14.7 N● | 16.85 N● | 18.75 N● |
| 1.4 mm · 04 | 4.3 N● | 5.55 N● | 6.55 N● | 7.75 N● | 9.35 N● | 11.1 N● | 12.8 N● | 15.1 N● | 17.4 N● | 19 N● |
| 1.4 mm · 05 | 4.35 N● | 5.55 N● | 6.6 N● | 7.8 N● | 9.5 N● | 11 N● | 12.8 N● | 15.35 N● | 17.4 N● | 19.05 N● |
| 1.4 mm · 06 | 4.3 N● | 5.55 N● | 6.65 N● | 8.05 N● | 9.55 N● | 11.4 N● | 13.25 N● | 15.4 N● | 17.5 N● | 19.45 N● |
| 1.2 mm · 01 | 3.55 N● | 4.65 N● | 5.65 N● | 6.75 N● | 8.3 N● | 9.9 N● | 11.45 N● | 13.3 N● | 15.3 N● | 17.2 N● |
| 1.2 mm · 02 | 4.15 N● | 5.05 N● | 6.05 N● | 6.95 N● | 8.4 N● | 10 N● | 11.85 N● | 13.7 N● | 15.7 N● | 17.5 N● |
| 1.2 mm · 03 | 3.5 N● | 4.25 N● | 5.4 N● | 6.45 N● | 7.7 N● | 9.45 N● | 10.75 N● | 12.45 N● | 14.4 N● | 16.2 N● |
| 1.2 mm · 04 | 3.65 N● | 4.4 N● | 5.25 N● | 6.25 N● | 7.7 N● | 9.05 N● | 10.7 N● | 12.5 N● | 14.3 N● | 16.15 N● |
Widths in millimeters. Assembly numbers identify rows within this view. This is one documented test condition from the April 2016 compilation, not a count of the entire test program.
Inspect all 190 measurements and group means
| Spring / assembly | 100 mm | 110 mm | 120 mm | 130 mm | 140 mm | 150 mm | 160 mm | 170 mm | 180 mm | 190 mm |
|---|---|---|---|---|---|---|---|---|---|---|
| 1.6 mm · 1 | 5.40 | 6.35 | 7.30 | 8.65 | 10.60 | 12.50 | 14.40 | 16.80 | 18.60 | 20.30 |
| 1.6 mm · 2 | 5.20 | 6.35 | 7.75 | 9.30 | 11.25 | 12.85 | 15.10 | 16.95 | 18.80 | 20.80 |
| 1.6 mm · 3 | 5.05 | 6.35 | 7.45 | 8.85 | 10.75 | 12.70 | 14.50 | 17.30 | 19.10 | 20.90 |
| 1.6 mm · 4 | 5.30 | 6.50 | 7.70 | 9.00 | 10.85 | 12.75 | 14.65 | 17.00 | 18.80 | 20.90 |
| 1.6 mm · 5 | 3.90 | 5.20 | 6.35 | 7.60 | 9.60 | 11.50 | 13.30 | 15.35 | 16.90 | 18.80 |
| 1.6 mm · 6 | 5.05 | 6.10 | 6.90 | 8.50 | 10.20 | 11.85 | 14.00 | 16.55 | 18.60 | 19.75 |
| 1.6 mm · 7 | 3.60 | 4.65 | 5.70 | 6.90 | 8.30 | 10.05 | 12.10 | 14.30 | 16.20 | 17.80 |
| 1.6 mm · 8 | 4.20 | 5.20 | 6.10 | 7.25 | 8.60 | 10.15 | 12.00 | 13.70 | 15.35 | 17.00 |
| 1.6 mm · 9 | 4.35 | 5.45 | 6.30 | 7.50 | 8.90 | 10.55 | 12.50 | 14.40 | 16.00 | 18.00 |
| 1.6 mm mean | 4.67 | 5.79 | 6.84 | 8.17 | 9.89 | 11.66 | 13.62 | 15.82 | 17.59 | 19.36 |
| 1.4 mm · 1 | 3.90 | 4.70 | 5.75 | 6.90 | 8.50 | 10.30 | 12.40 | 14.40 | 16.90 | 18.80 |
| 1.4 mm · 2 | 4.15 | 5.20 | 6.35 | 7.85 | 9.50 | 11.20 | 13.15 | 15.50 | 17.40 | 18.60 |
| 1.4 mm · 3 | 3.55 | 4.80 | 5.90 | 7.30 | 9.10 | 10.95 | 12.75 | 14.70 | 16.85 | 18.75 |
| 1.4 mm · 4 | 4.30 | 5.55 | 6.55 | 7.75 | 9.35 | 11.10 | 12.80 | 15.10 | 17.40 | 19.00 |
| 1.4 mm · 5 | 4.35 | 5.55 | 6.60 | 7.80 | 9.50 | 11.00 | 12.80 | 15.35 | 17.40 | 19.05 |
| 1.4 mm · 6 | 4.30 | 5.55 | 6.65 | 8.05 | 9.55 | 11.40 | 13.25 | 15.40 | 17.50 | 19.45 |
| 1.4 mm mean | 4.09 | 5.23 | 6.30 | 7.61 | 9.25 | 10.99 | 12.86 | 15.08 | 17.24 | 18.94 |
| 1.2 mm · 1 | 3.55 | 4.65 | 5.65 | 6.75 | 8.30 | 9.90 | 11.45 | 13.30 | 15.30 | 17.20 |
| 1.2 mm · 2 | 4.15 | 5.05 | 6.05 | 6.95 | 8.40 | 10.00 | 11.85 | 13.70 | 15.70 | 17.50 |
| 1.2 mm · 3 | 3.50 | 4.25 | 5.40 | 6.45 | 7.70 | 9.45 | 10.75 | 12.45 | 14.40 | 16.20 |
| 1.2 mm · 4 | 3.65 | 4.40 | 5.25 | 6.25 | 7.70 | 9.05 | 10.70 | 12.50 | 14.30 | 16.15 |
| 1.2 mm mean | 3.71 | 4.59 | 5.59 | 6.60 | 8.03 | 9.60 | 11.19 | 12.99 | 14.93 | 16.76 |
Checking the parts behind the force curves
The springs needed their own dimensional checks. In May 2016, an inspection compared ten 1.4 mm headband springs from each of two supplier lots. On one 148.30 ± 2.00 mm feature, the recorded means were 145.605 mm and 145.766 mm; five of ten parts in the first lot and eight of ten in the second were outside the drawing limits. The second lot had less scatter, but its tighter grouping was still offset from the required dimension. Consistency and conformance were different questions.
Those part measurements complemented the assembled-headset tests. A spring drawing, an inspection result and a force curve each described a different part of the problem: the shape we requested, the parts we received and what the complete assembly did.
Developing the earpads
The earpads were a development effort in their own right, balancing contact pressure, comfort, traction and appearance.
I tore down numerous headphones, obtained vendor samples and bought replacement earpads for a wide range of models. These gave me a broad set of constructions to examine while designing and prototyping Glyph's pads. My favorite Bose earpads were a reference for the foam type and combination.
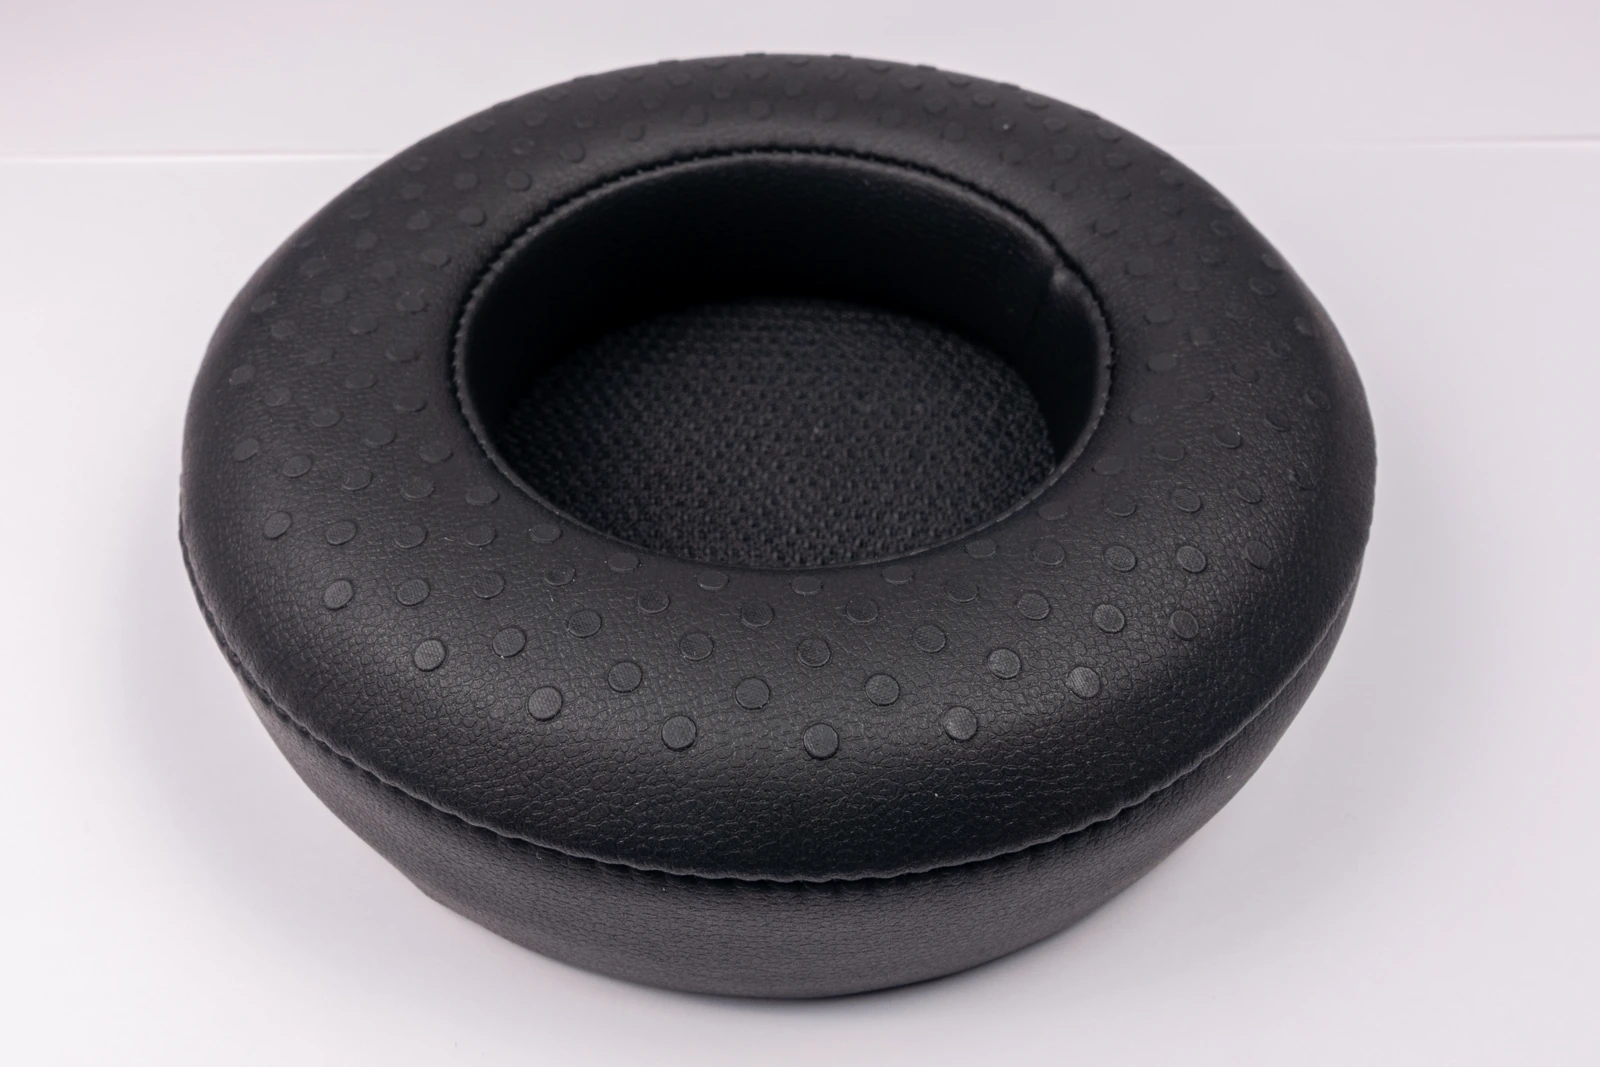
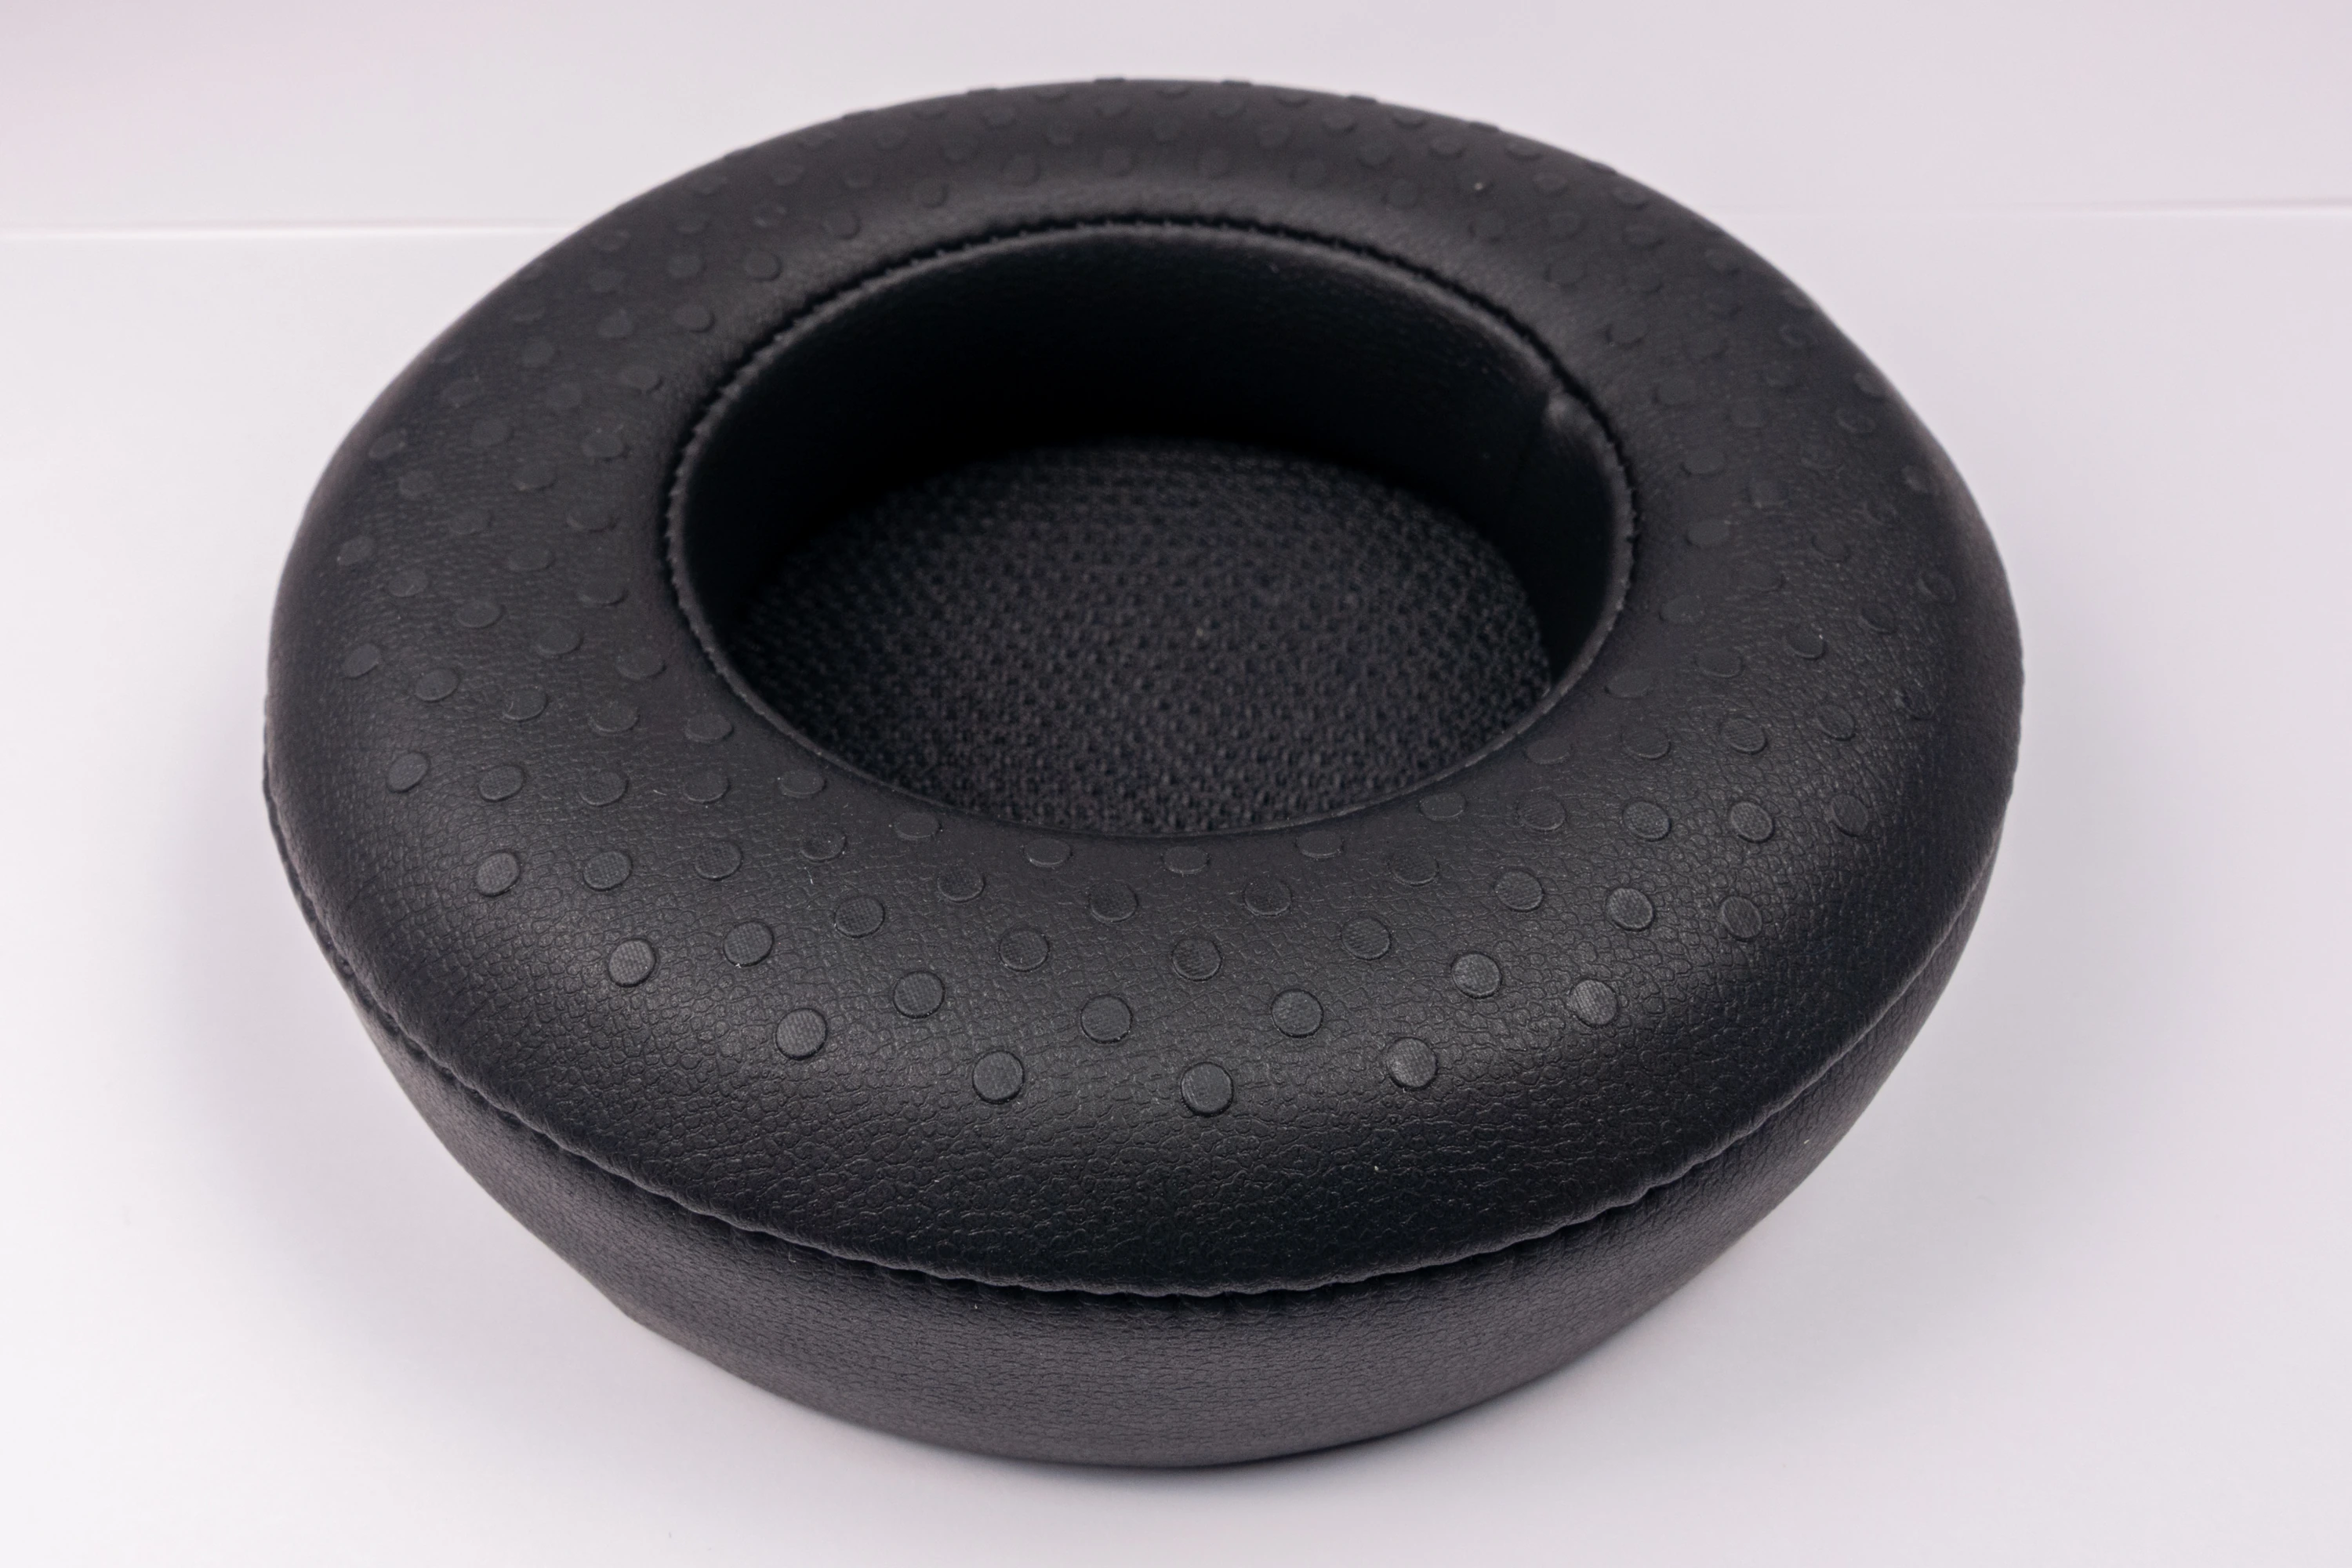
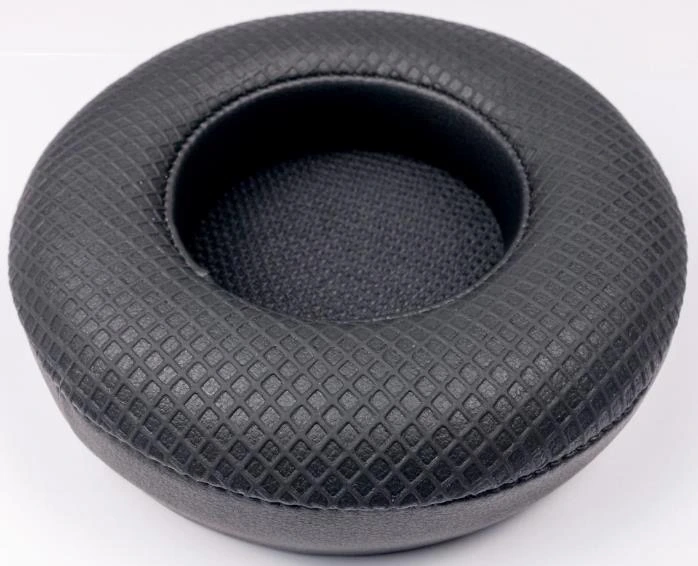
I built up a group of Glyphs with the different earpad variants and had colleagues try them and provide comments. Nearly everyone liked the dots and the low-pressure foam, and I used that feedback to make the selection. We chose the normal dotted surface, shown in the finished earpad photograph, rather than the gel dots or silicone netting.
 From the workbench
Earpad materials, grip and prototypes
Compare seven surface variants, the bench retention results and the samples behind the selected dotted pad.
Explore investigation +Close investigation −
Earpad materials, grip and prototypes
Compare seven surface variants, the bench retention results and the samples behind the selected dotted pad.
Explore investigation +Close investigation −We also compared how pad surfaces gripped an adjustable acrylic fixture. At a 132 mm span, we added weight to a hanging bag until the headset slipped. The seven variants behaved very differently; four examples show the range:
| Pad surface | Recorded hanging mass at slip |
|---|---|
| Normal Vulcan dots | 656.9 g |
| Silicone netting | 1,081.74 g |
| Gel dots | 1,000.04 g |
| Suede | 35.98 g |
The suede result included the impact of the first bearing landing in the bag. At a wider 155 mm setting, the normal dotted pads held beyond 1,637.3 g before we ran out of weights. The fixture gave us a comparison under a common setup, but acrylic could produce more contact and suction than a person's head. These were bench retention measurements; acoustic seal and comfort still depended on people wearing the product.
Earpad constructions and material trials
The selected pad, sample photographs and contemporary surface renders.
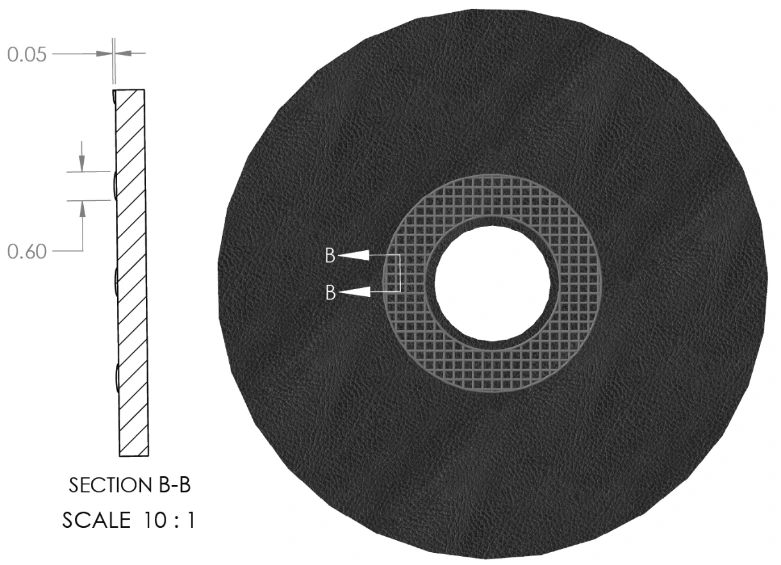
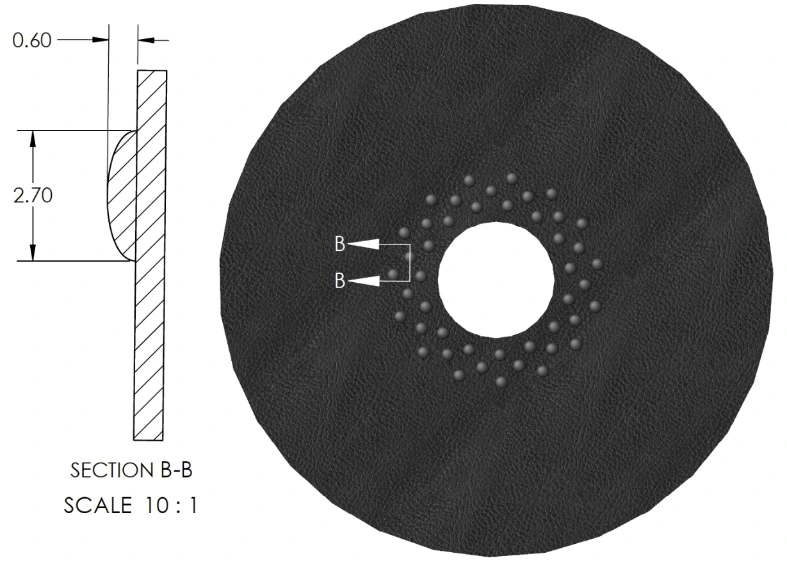
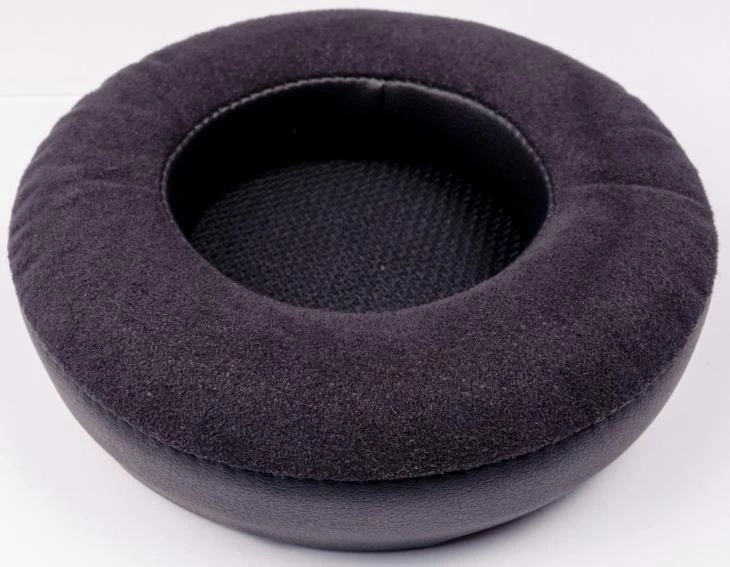
The inner liner and its fixed constraints
The inner liners were among the most difficult parts I worked on. These two-shot molded parts had to move within largely fixed interfaces: the surrounding parts, travel and extension distance left little room to change the design.
During flex or twist, the liner and its mating flange did not deform together. A small gap would open at the edge, like a coin purse: the dreaded pucker. I tried incremental changes, but we had to live with some puckering and deformation. The product shipped with those compromises still in place.
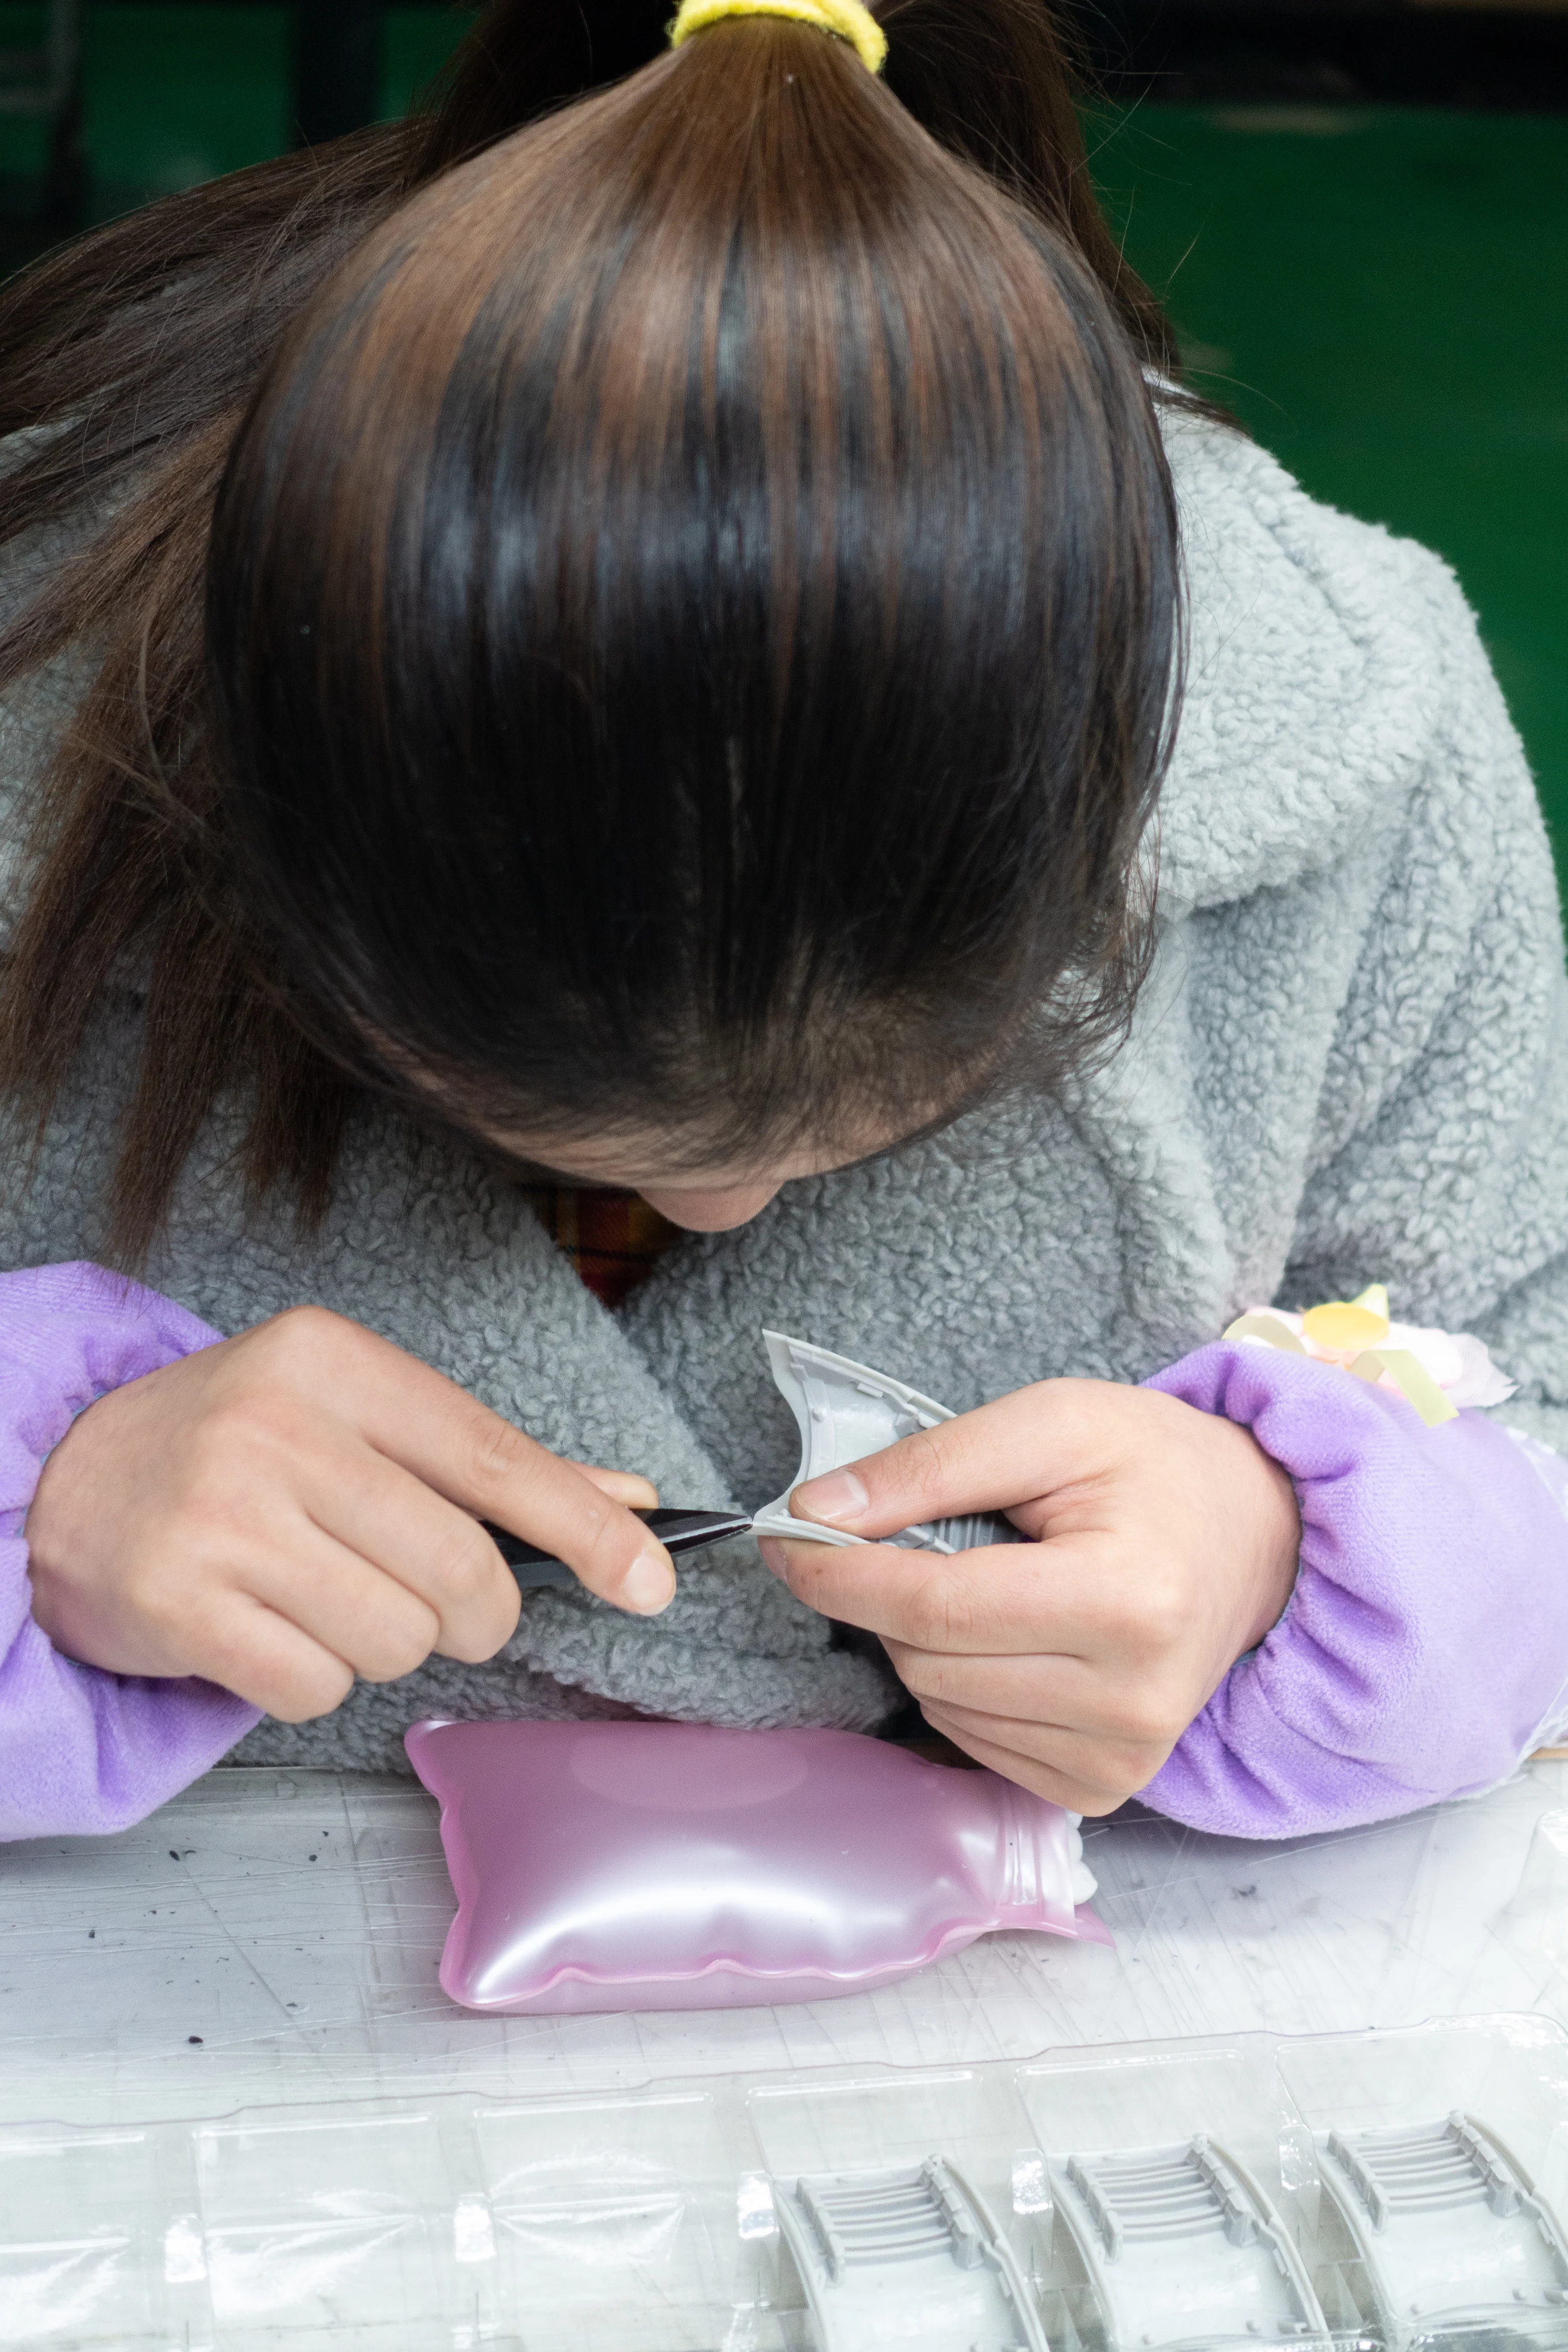
Trimming presented a separate production problem. The fixture technique was difficult to reproduce, so we ended up trimming the liners by hand. One operator had mastered the job, and she was the only person who did it.
From the workbench Working within the liner's limits
Inspect the moving interface, then follow the trimming trials to the operator and physical workmanship standards.
Explore investigation +Close investigation −
Working within the liner's limits
Inspect the moving interface, then follow the trimming trials to the operator and physical workmanship standards.
Explore investigation +Close investigation −Two parts moving differently
The tooling itself was straightforward enough. The harder problem was getting the part to satisfy its functions and interfaces throughout the assembly's movement. Apart from subtle, steel-safe changes, the surrounding parts were off-limits.
I was trying to connect the failures I saw during cycle testing and use with how the materials deformed together. I made incremental changes during tool fabrication and trials, but that region never worked correctly through every aspect and axis of its travel.
The liner interface
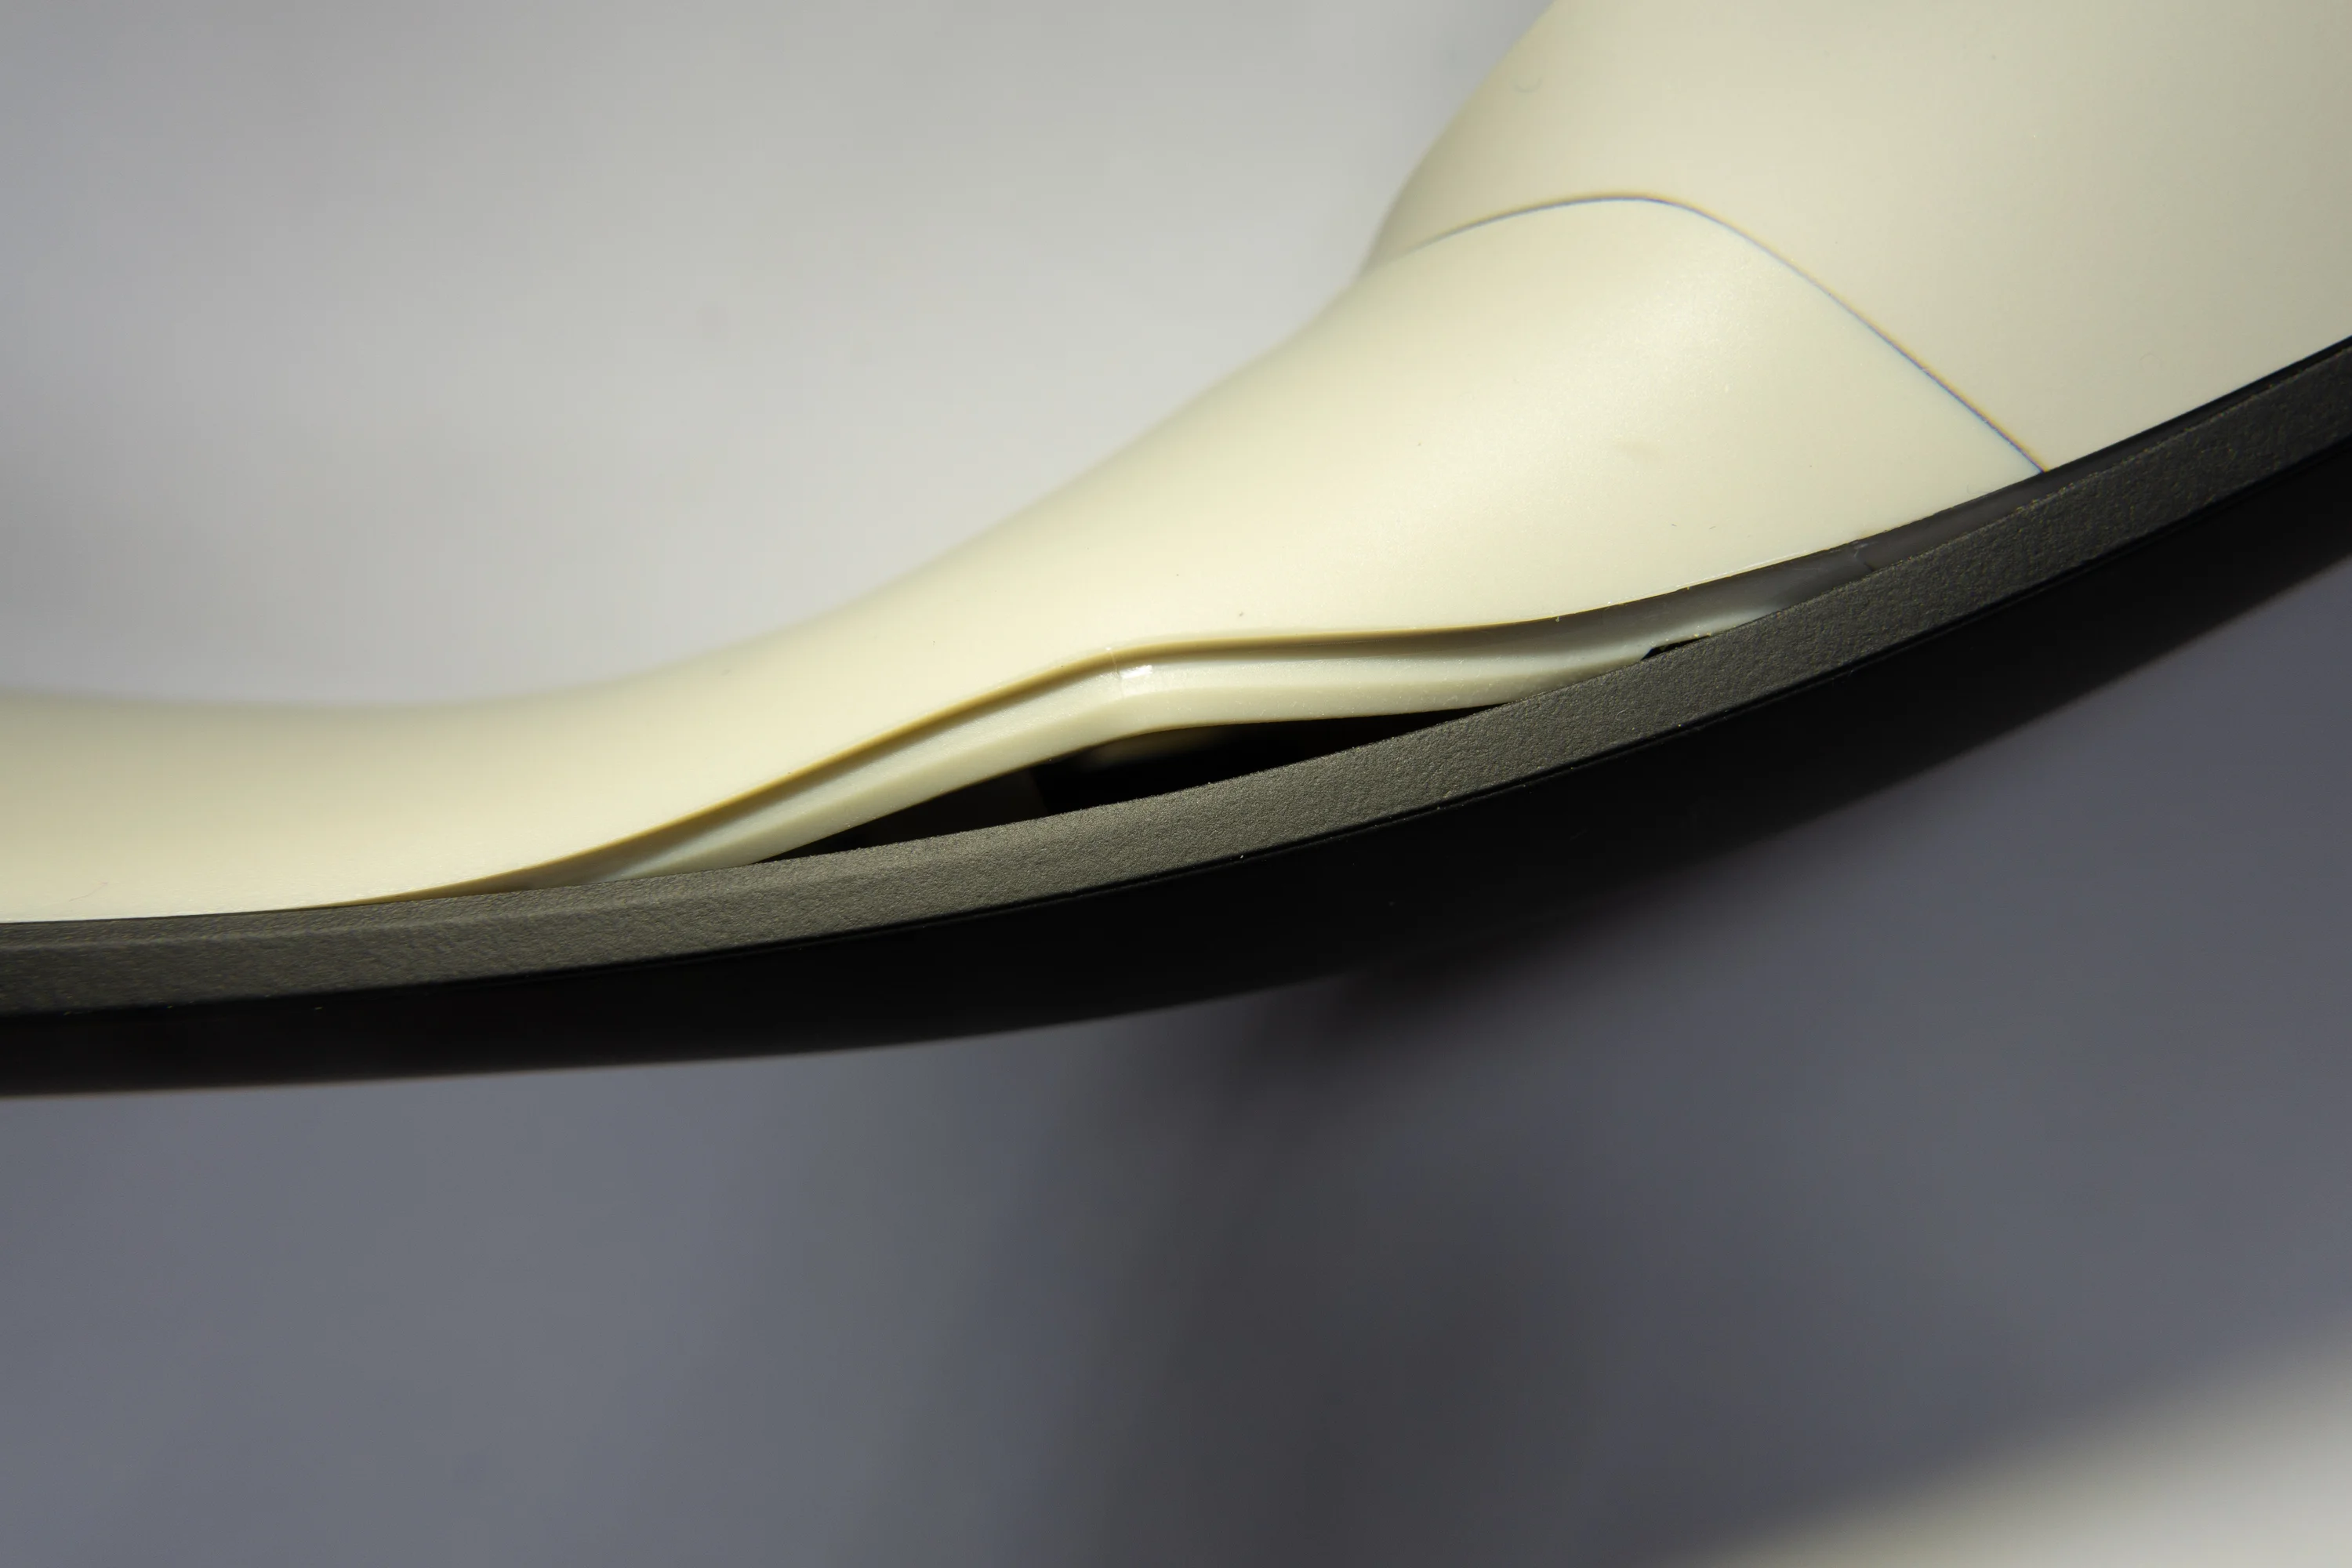
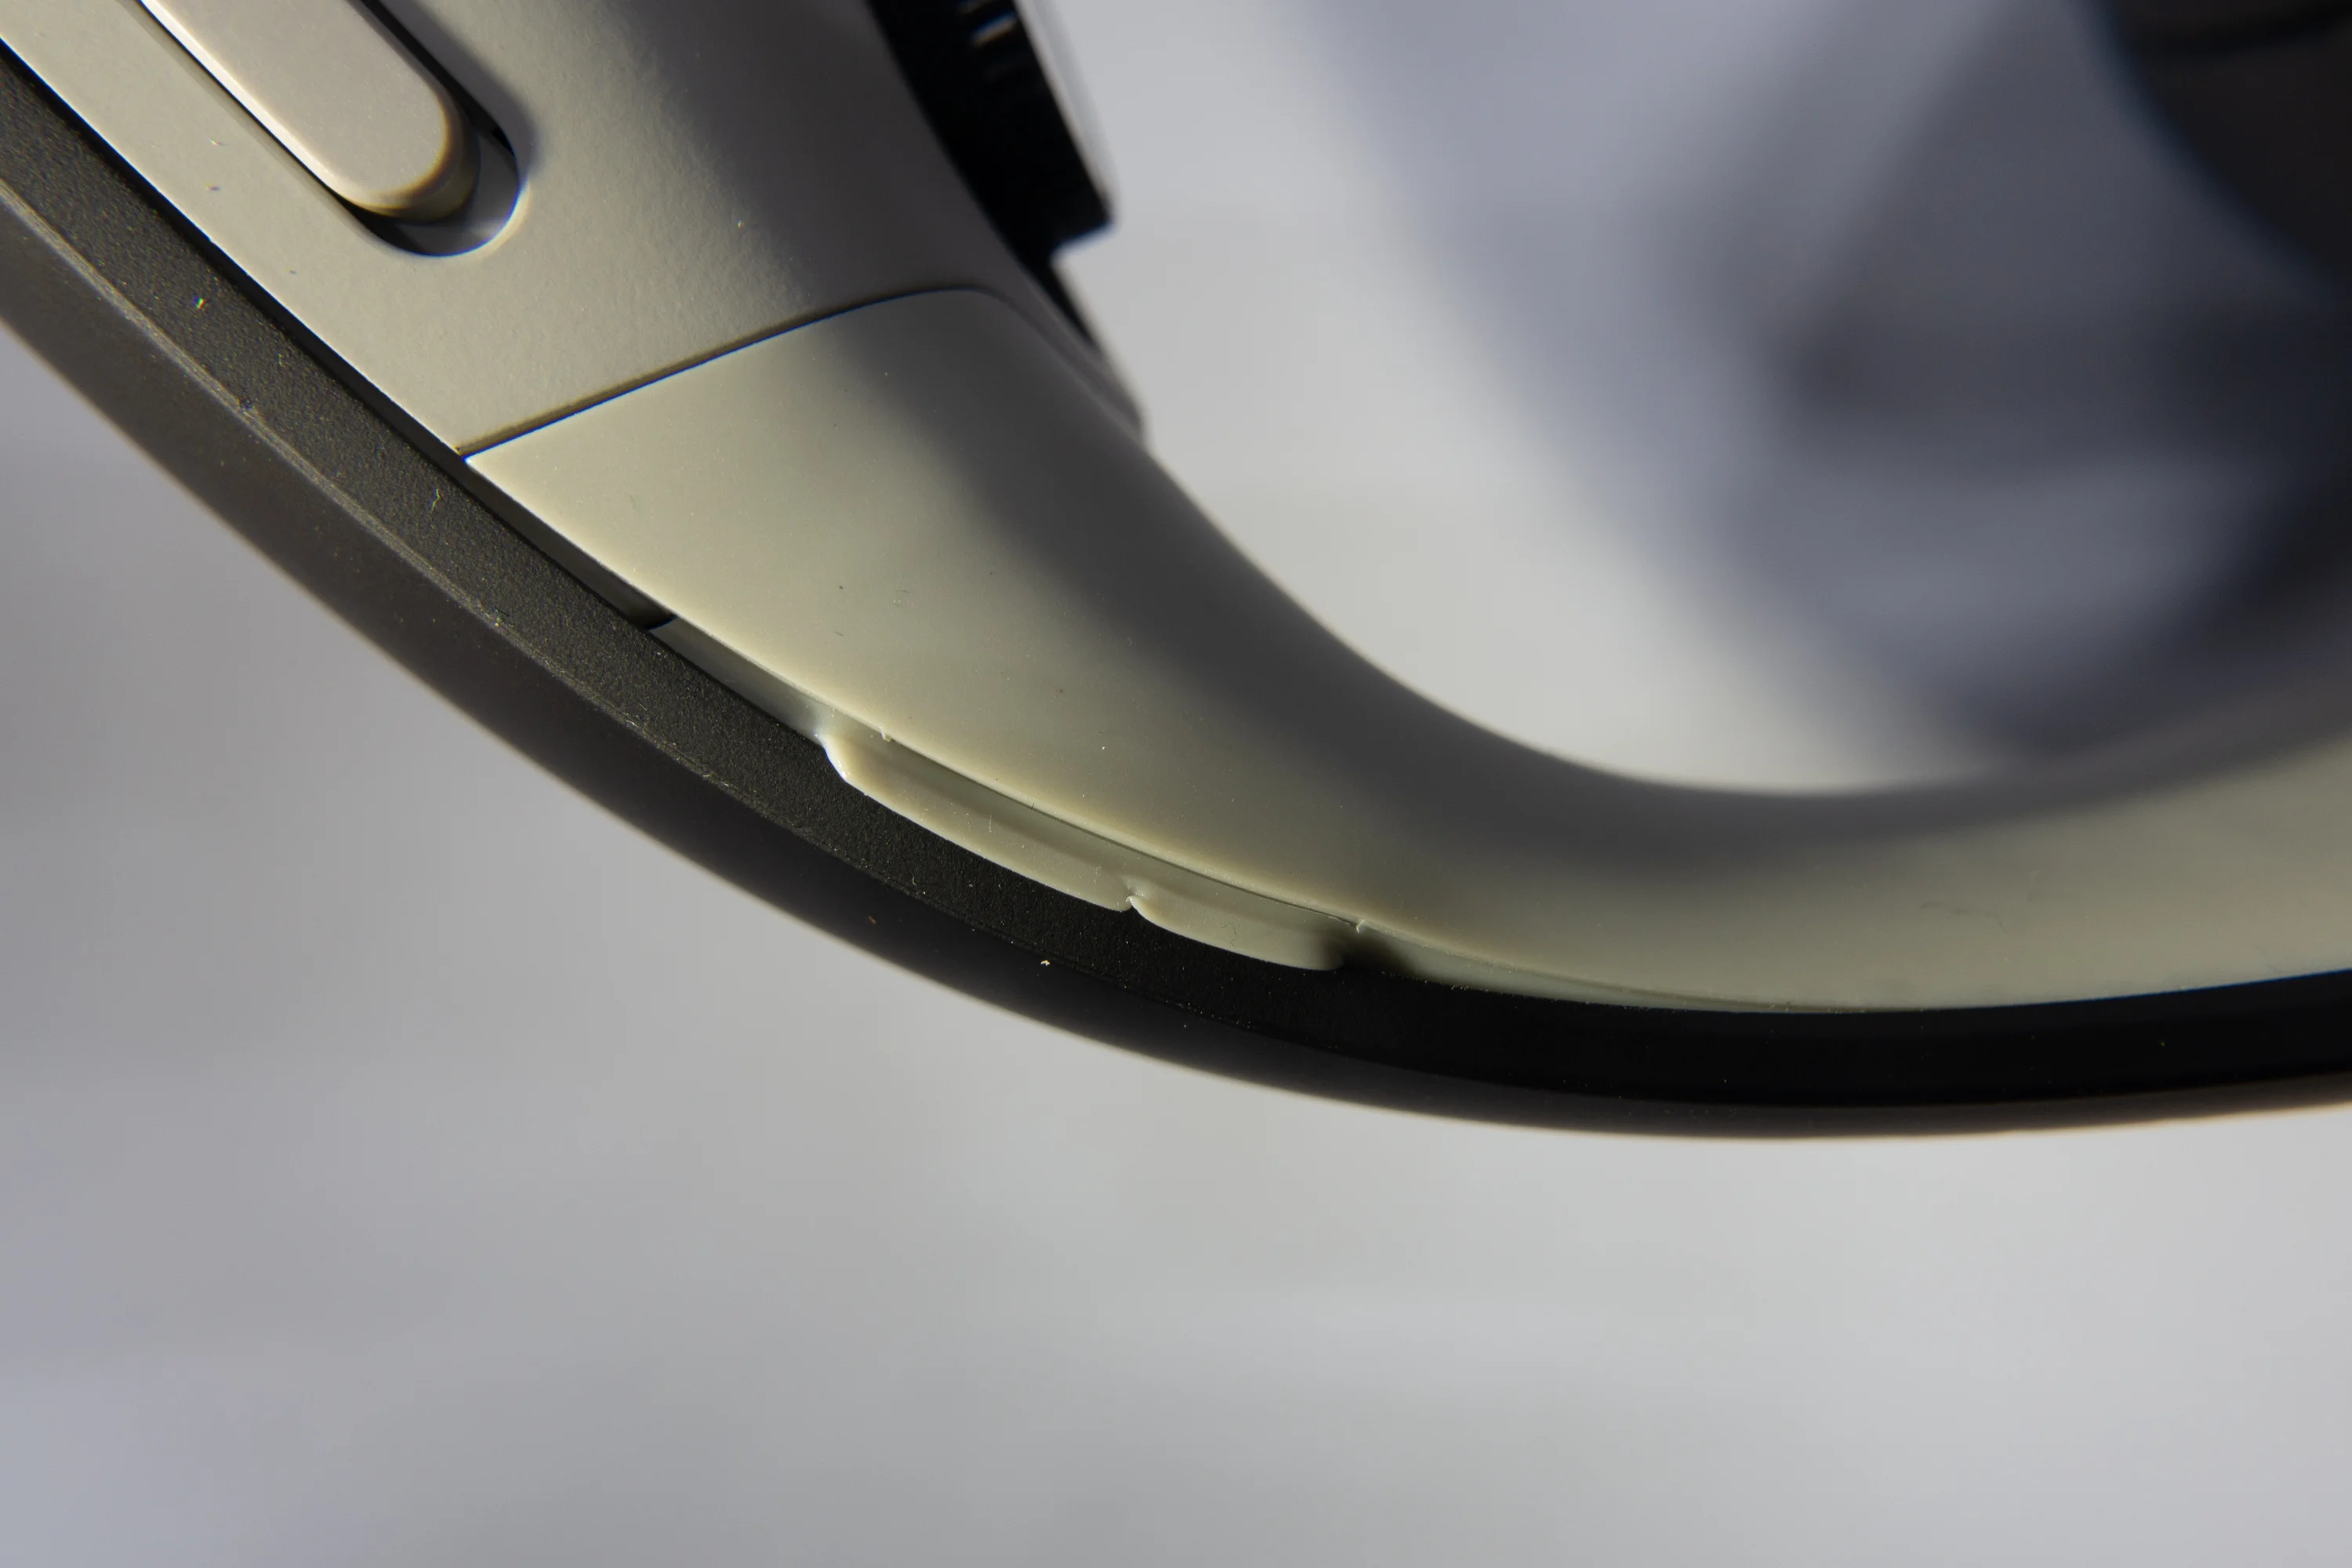
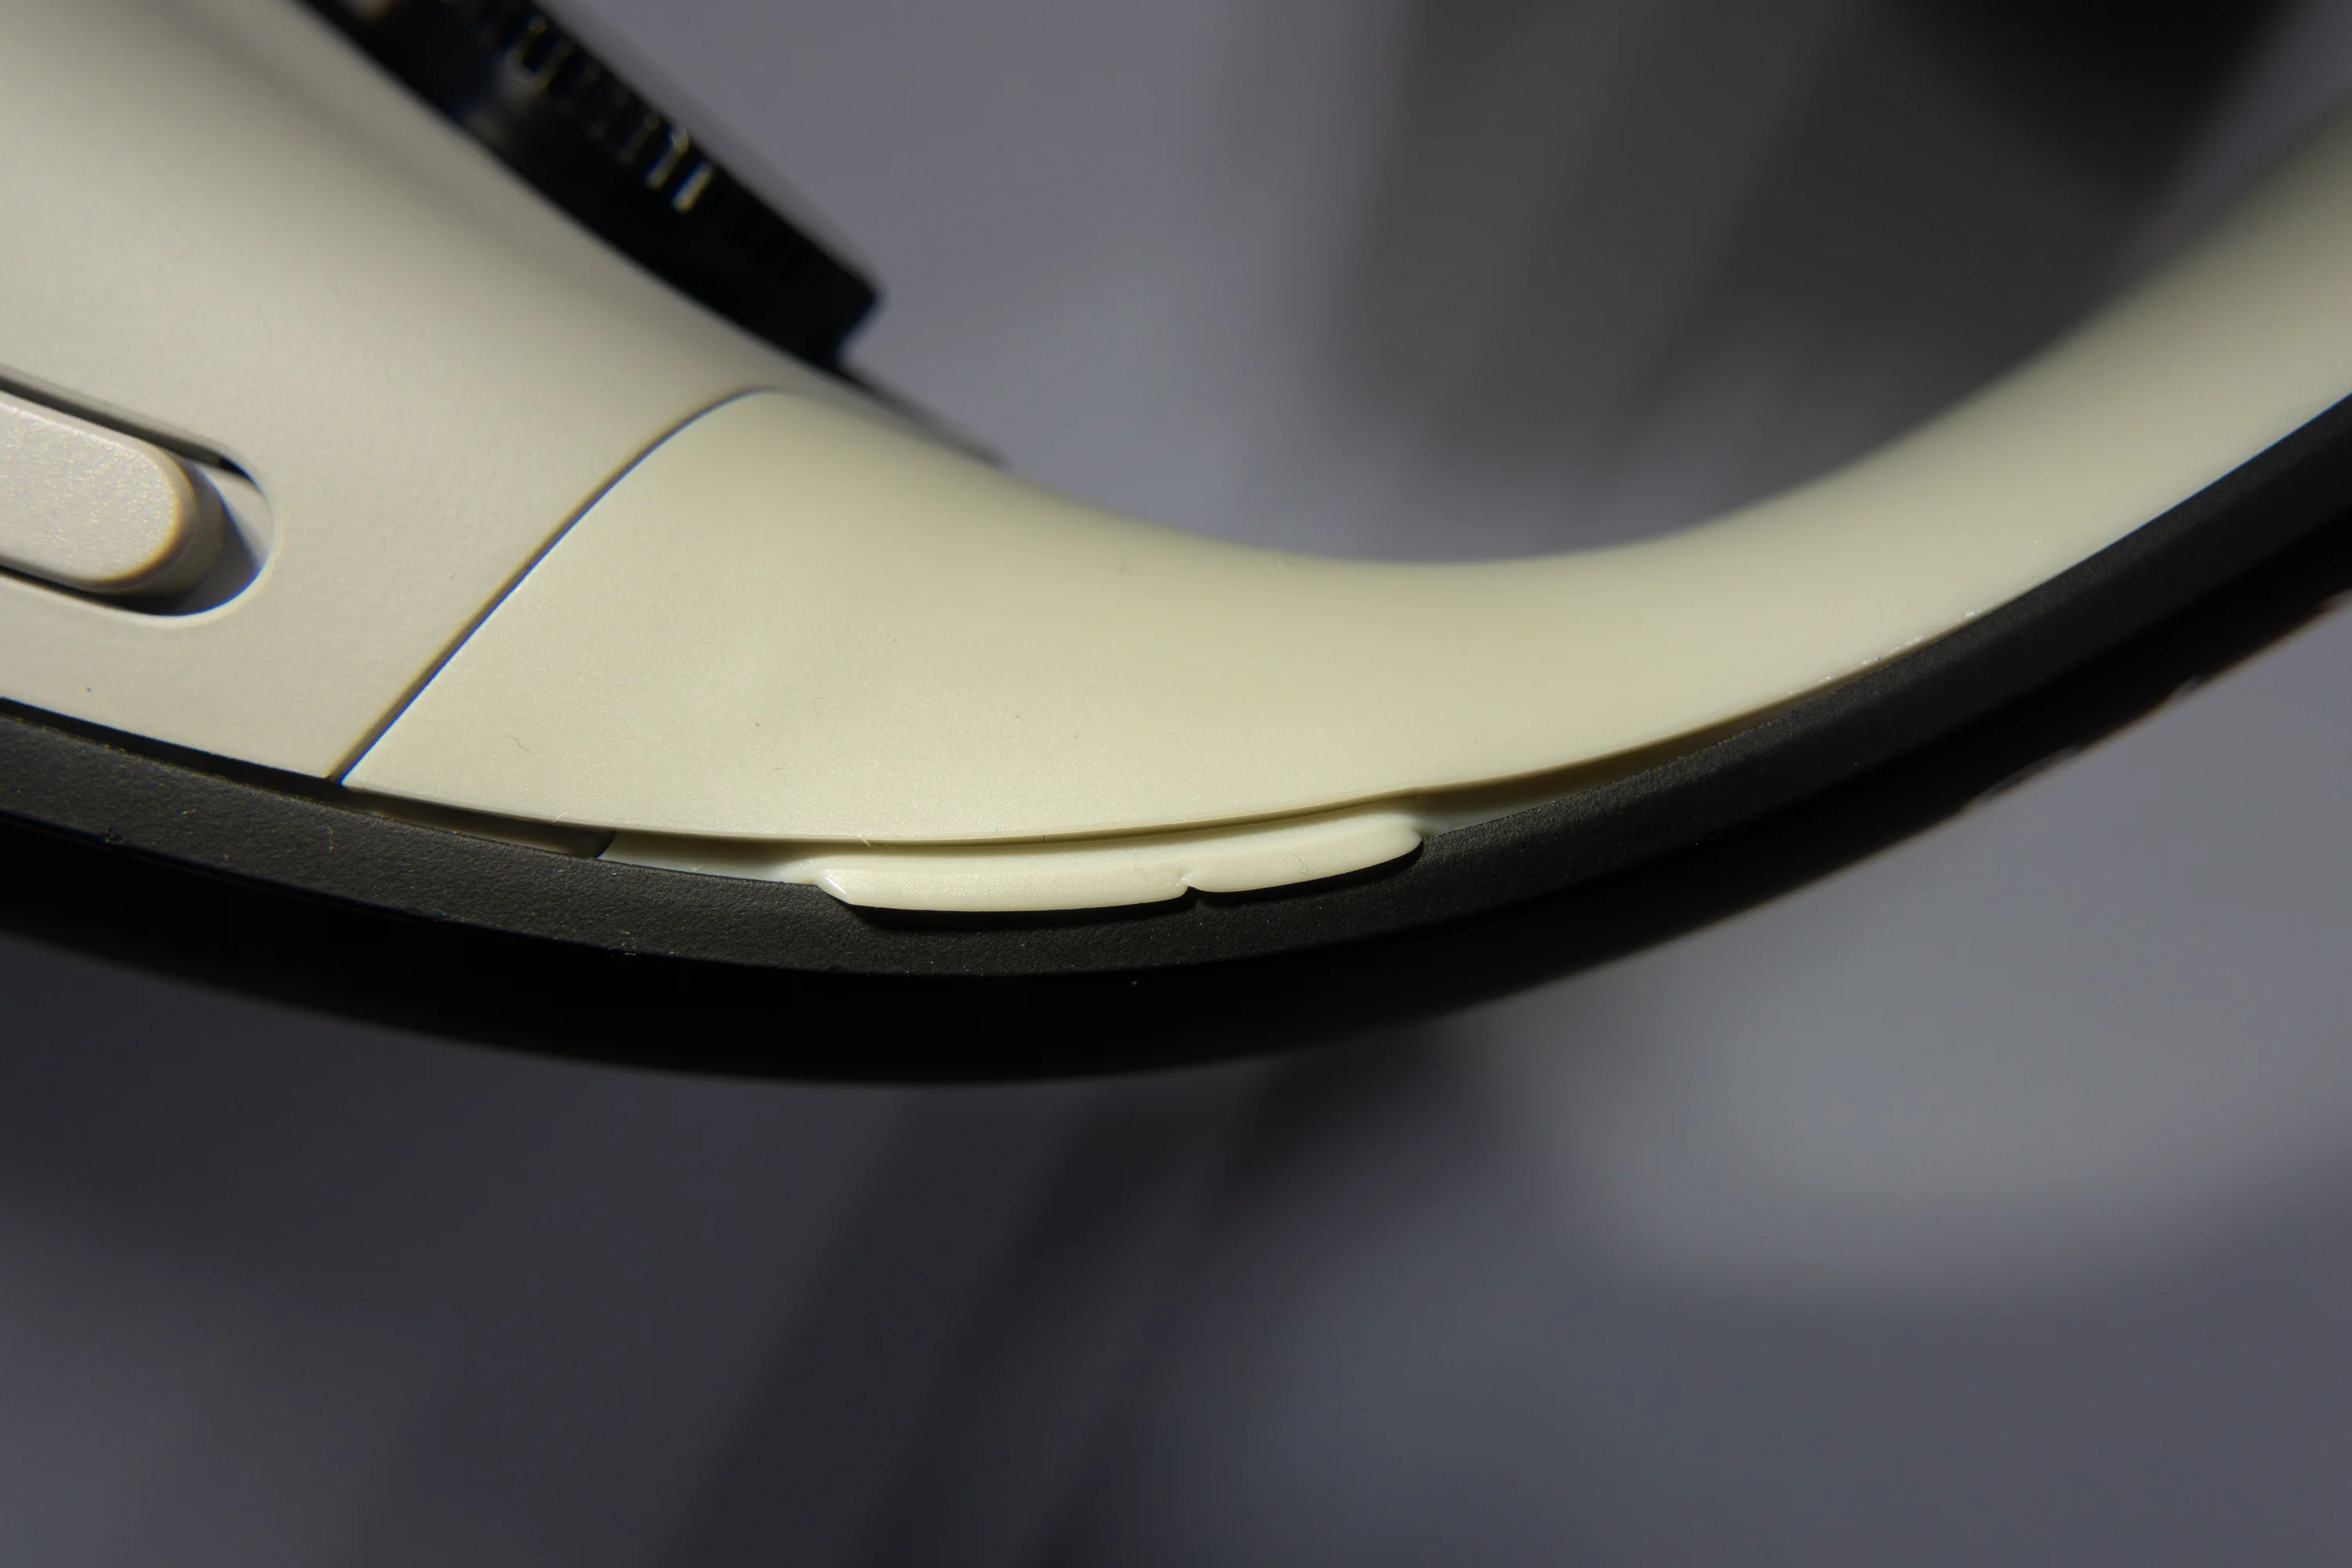
A longer production run at higher volume might have supported further development. I wasn't prepared to call the problem impossible, but I didn't believe that liner, as it stood, could satisfy every constraint.
Trimming the liners
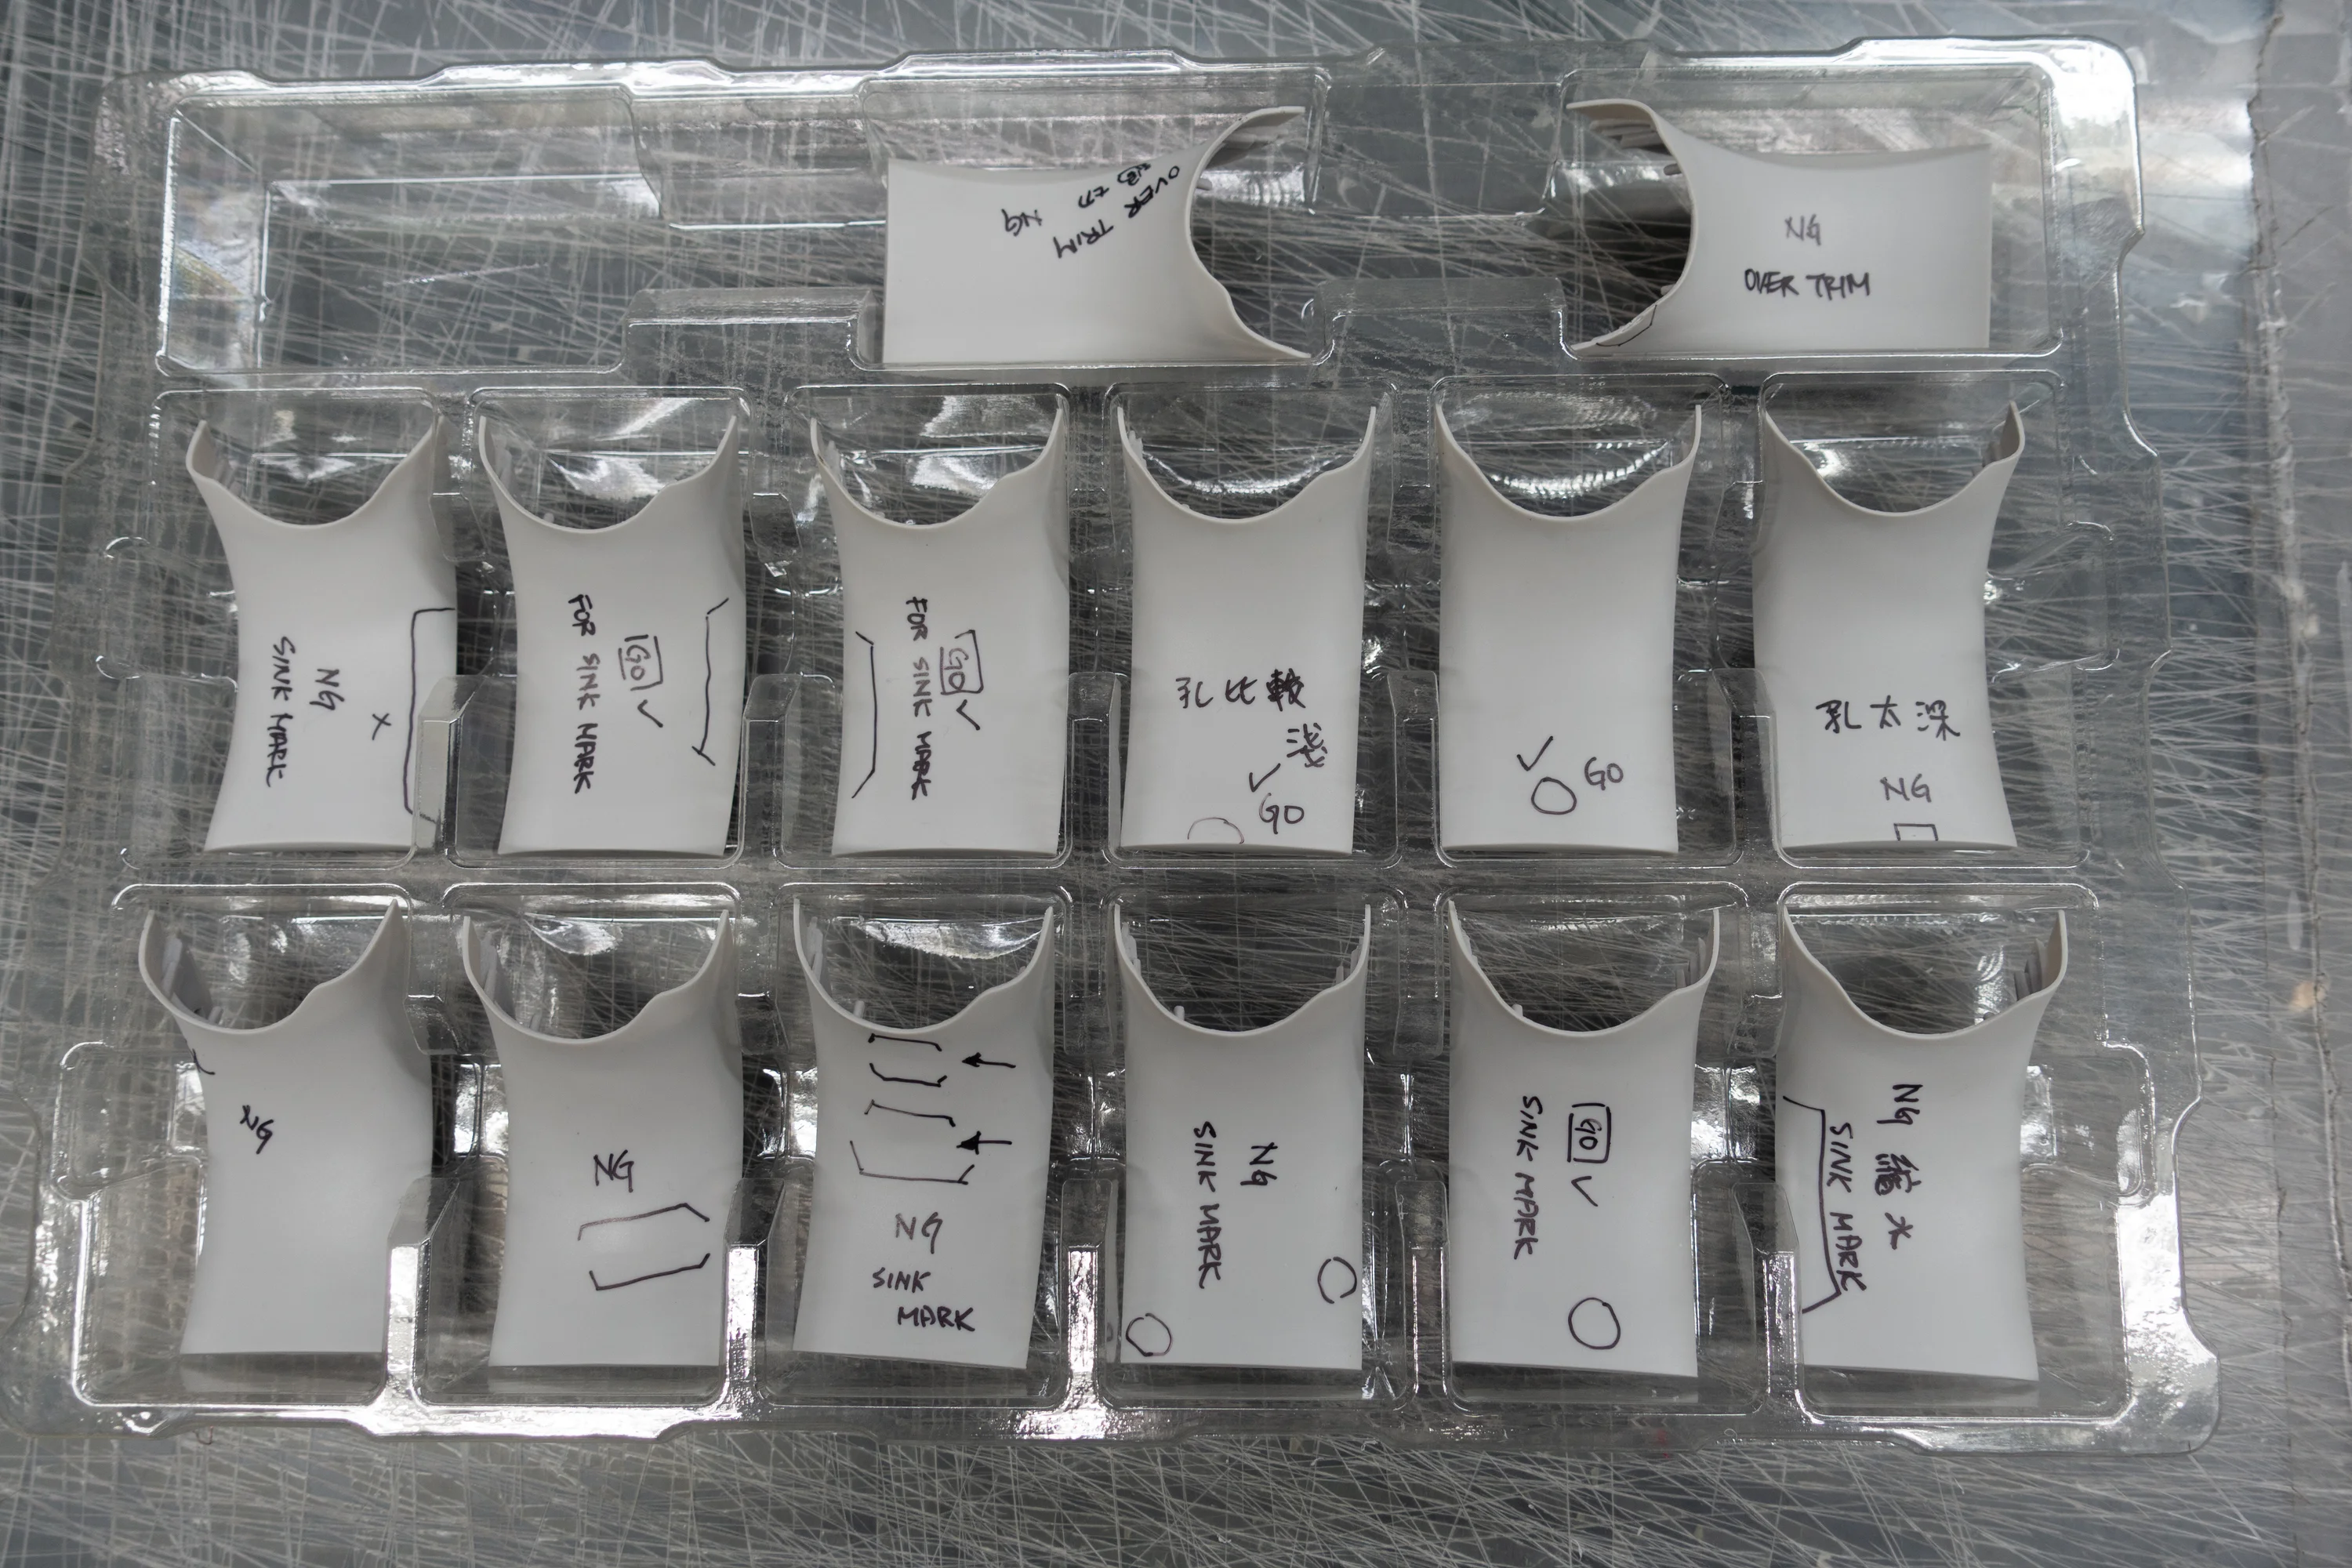
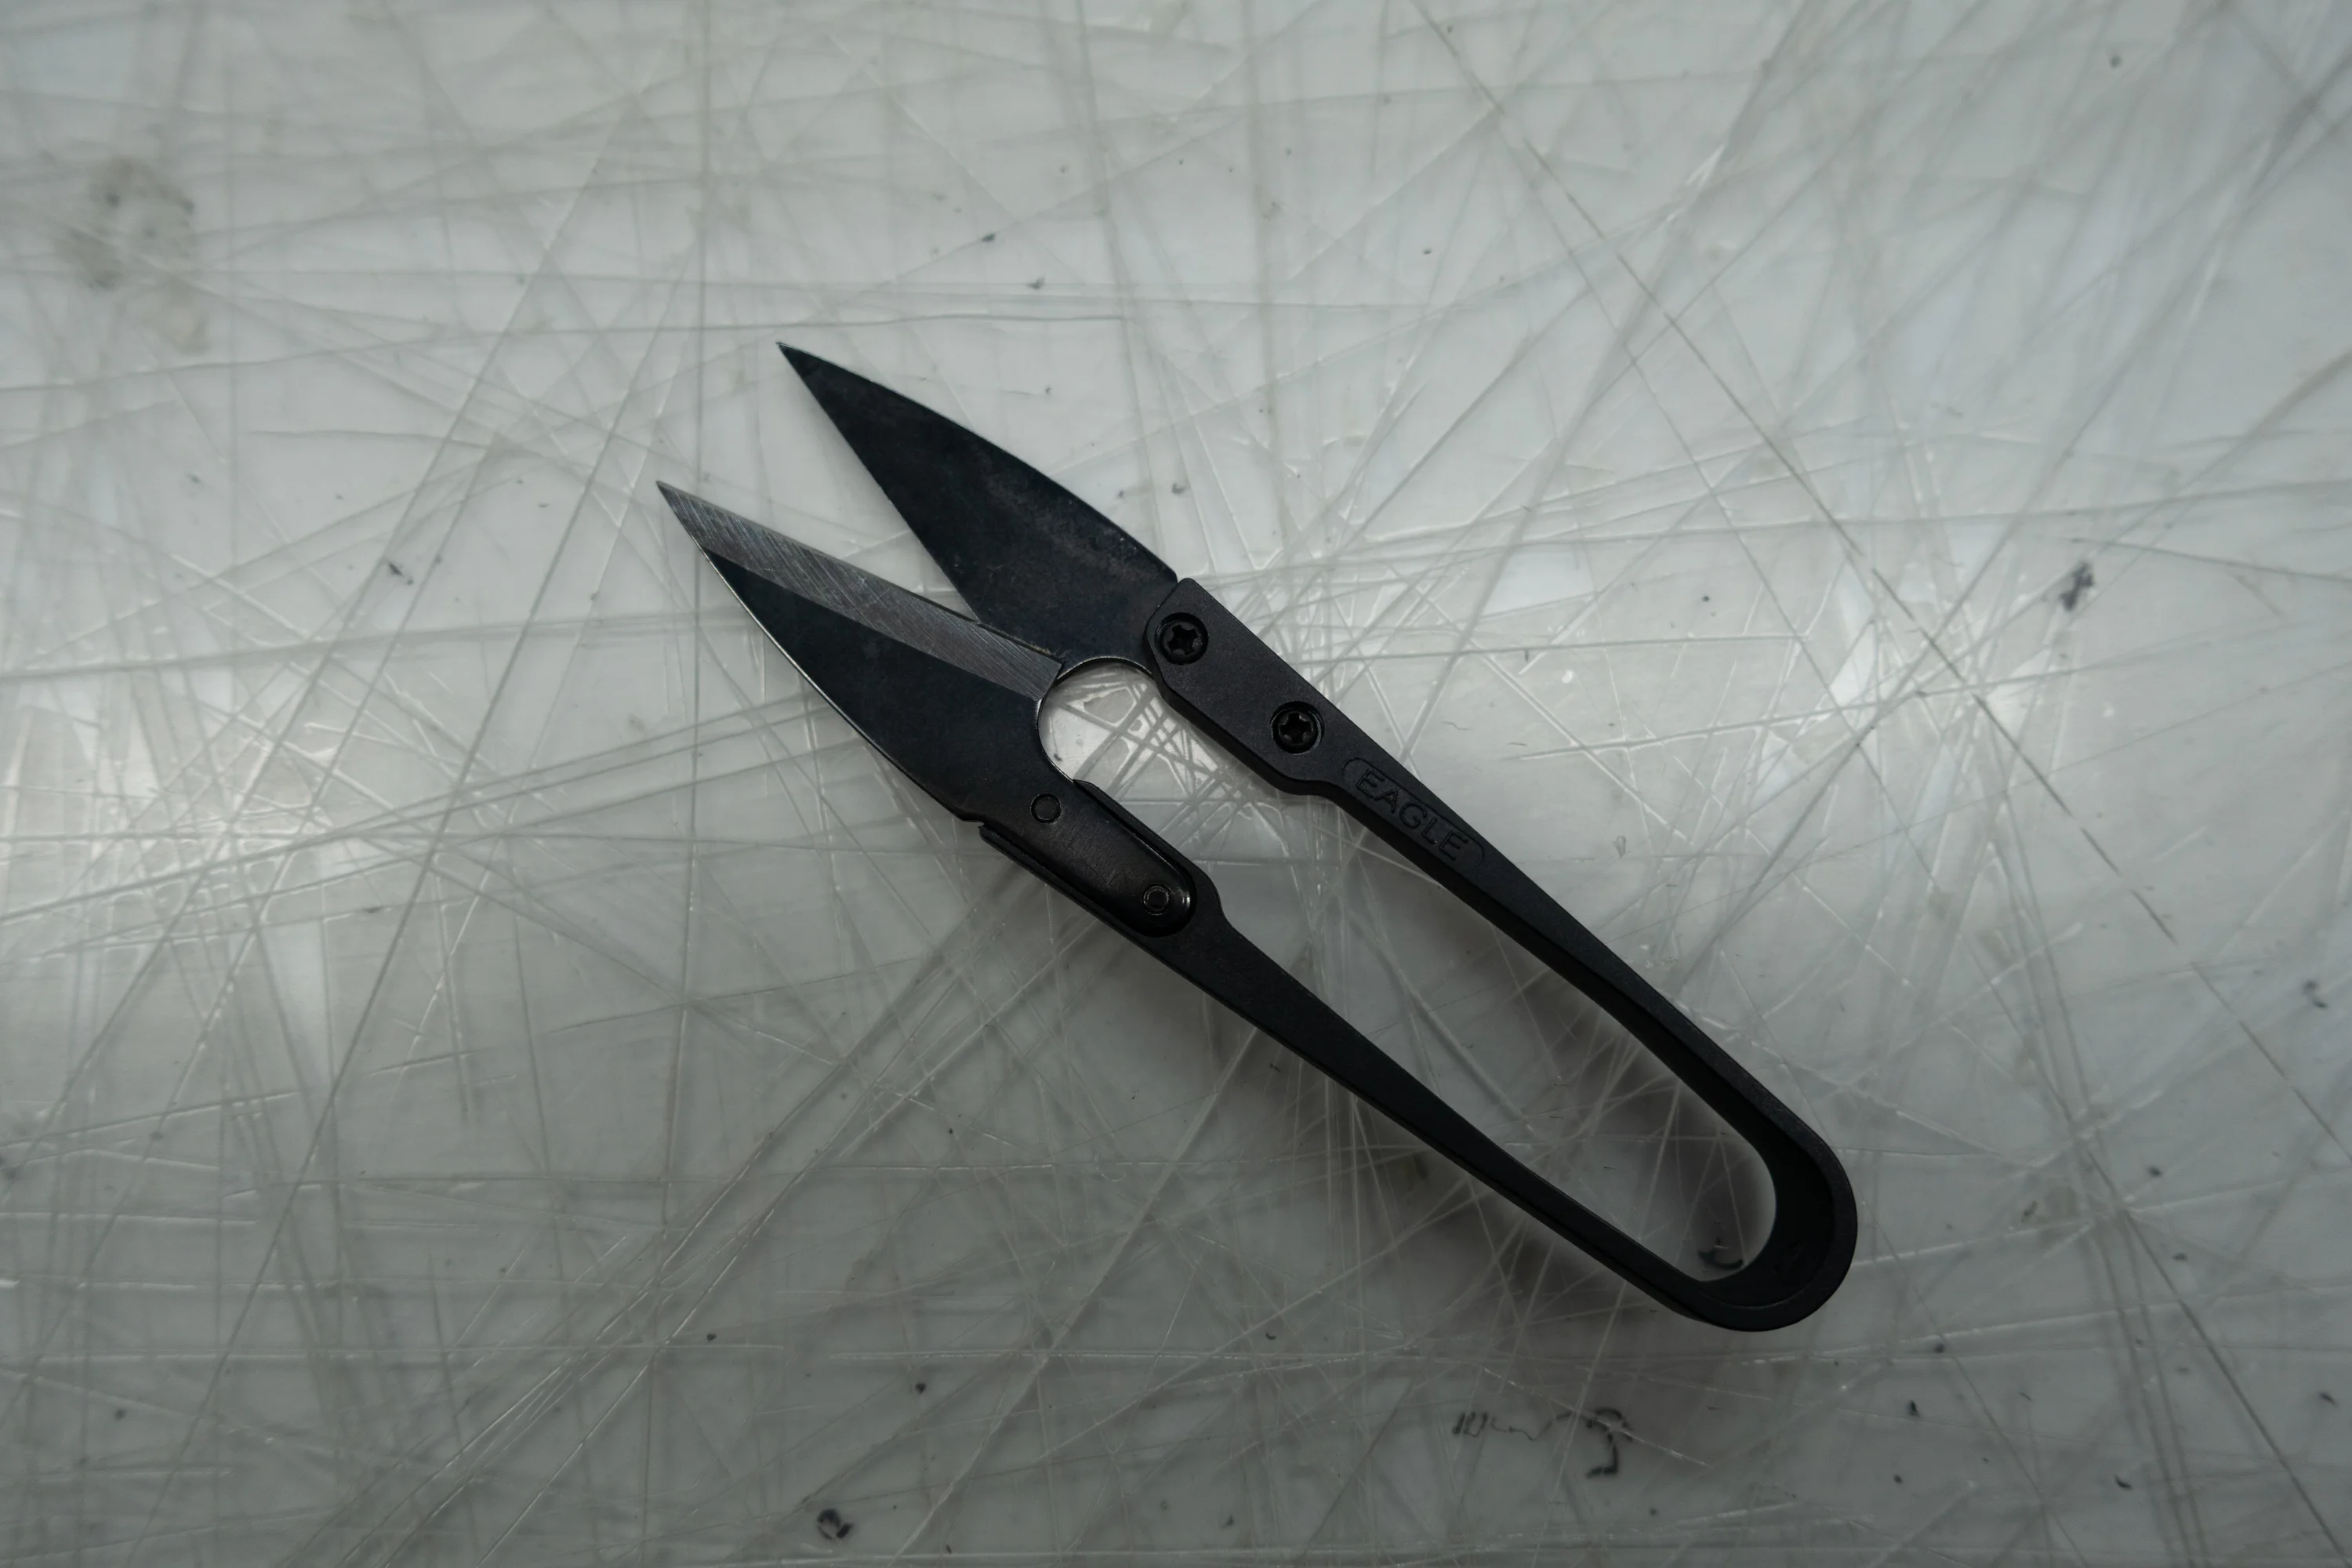
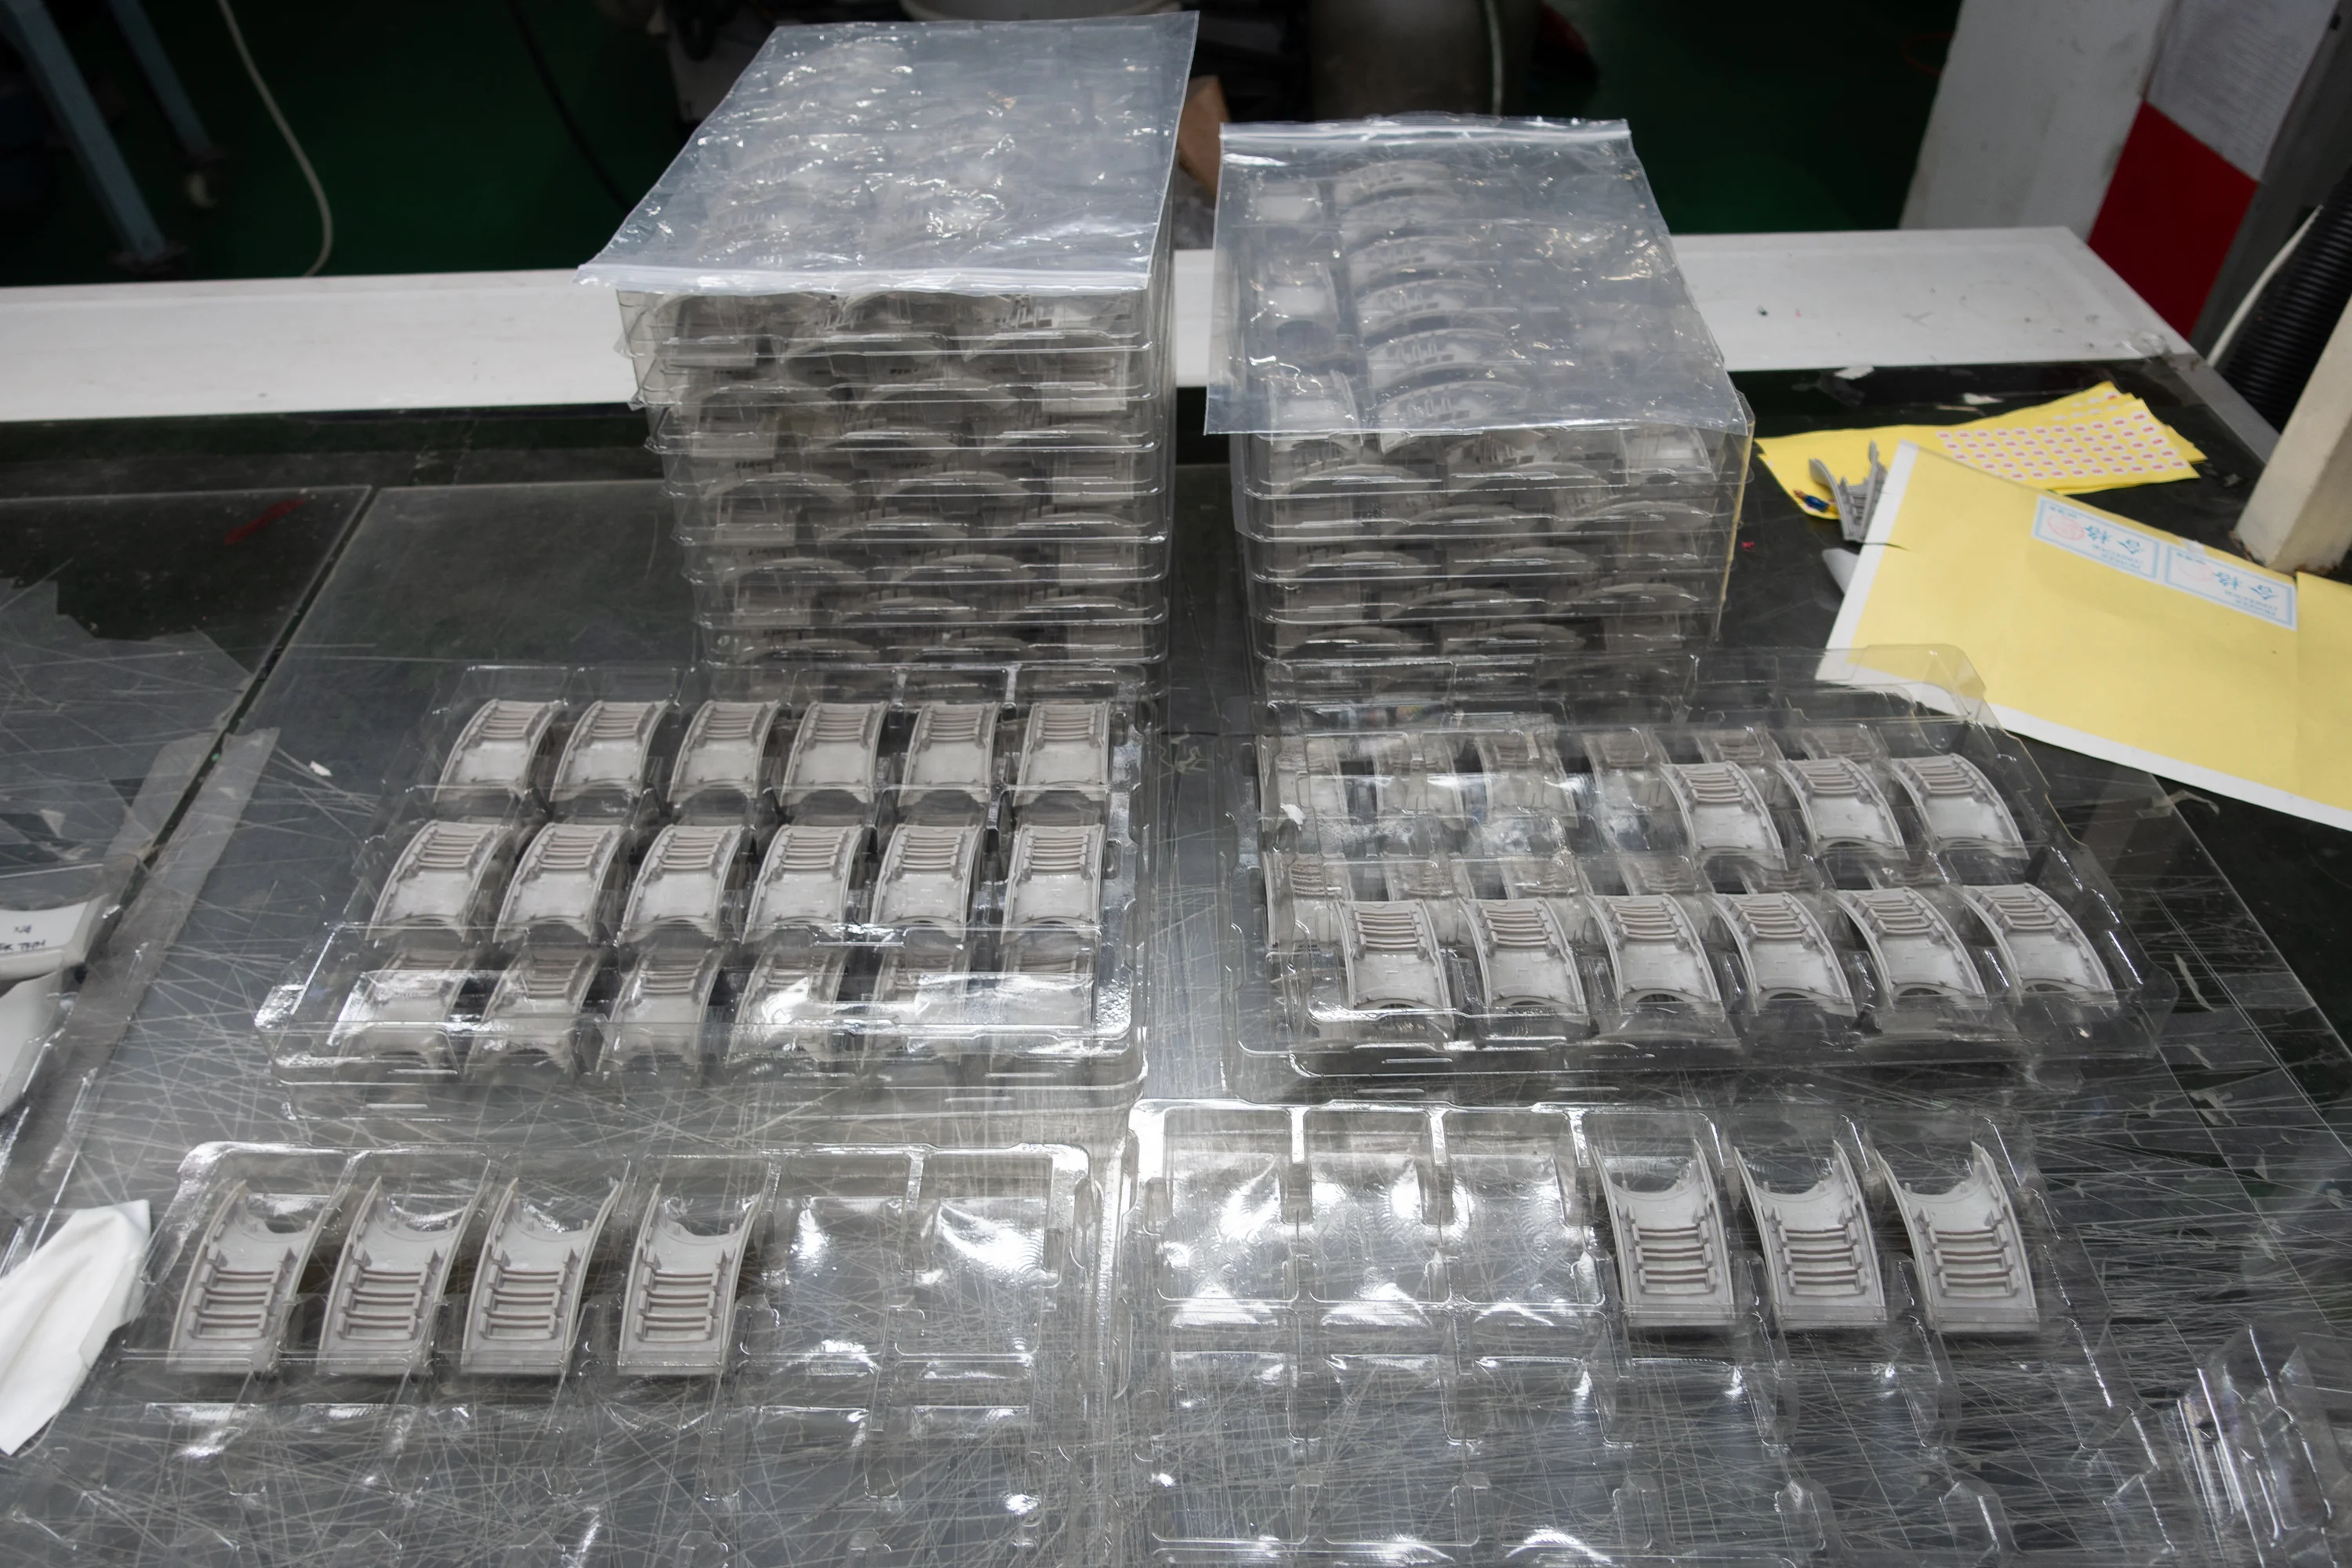
We worked on a trimming fixture in parallel. The first two photographs show the attempted setup; the following views show the operator who ultimately did the work by hand, her physical reference samples, tool and workstation.
I chose and documented the physical defect samples for the trim technician, describing and quantifying the defects in specifications and technical communications. Those master samples put the workmanship standard beside the person doing the job.
Trimming and the workmanship standard
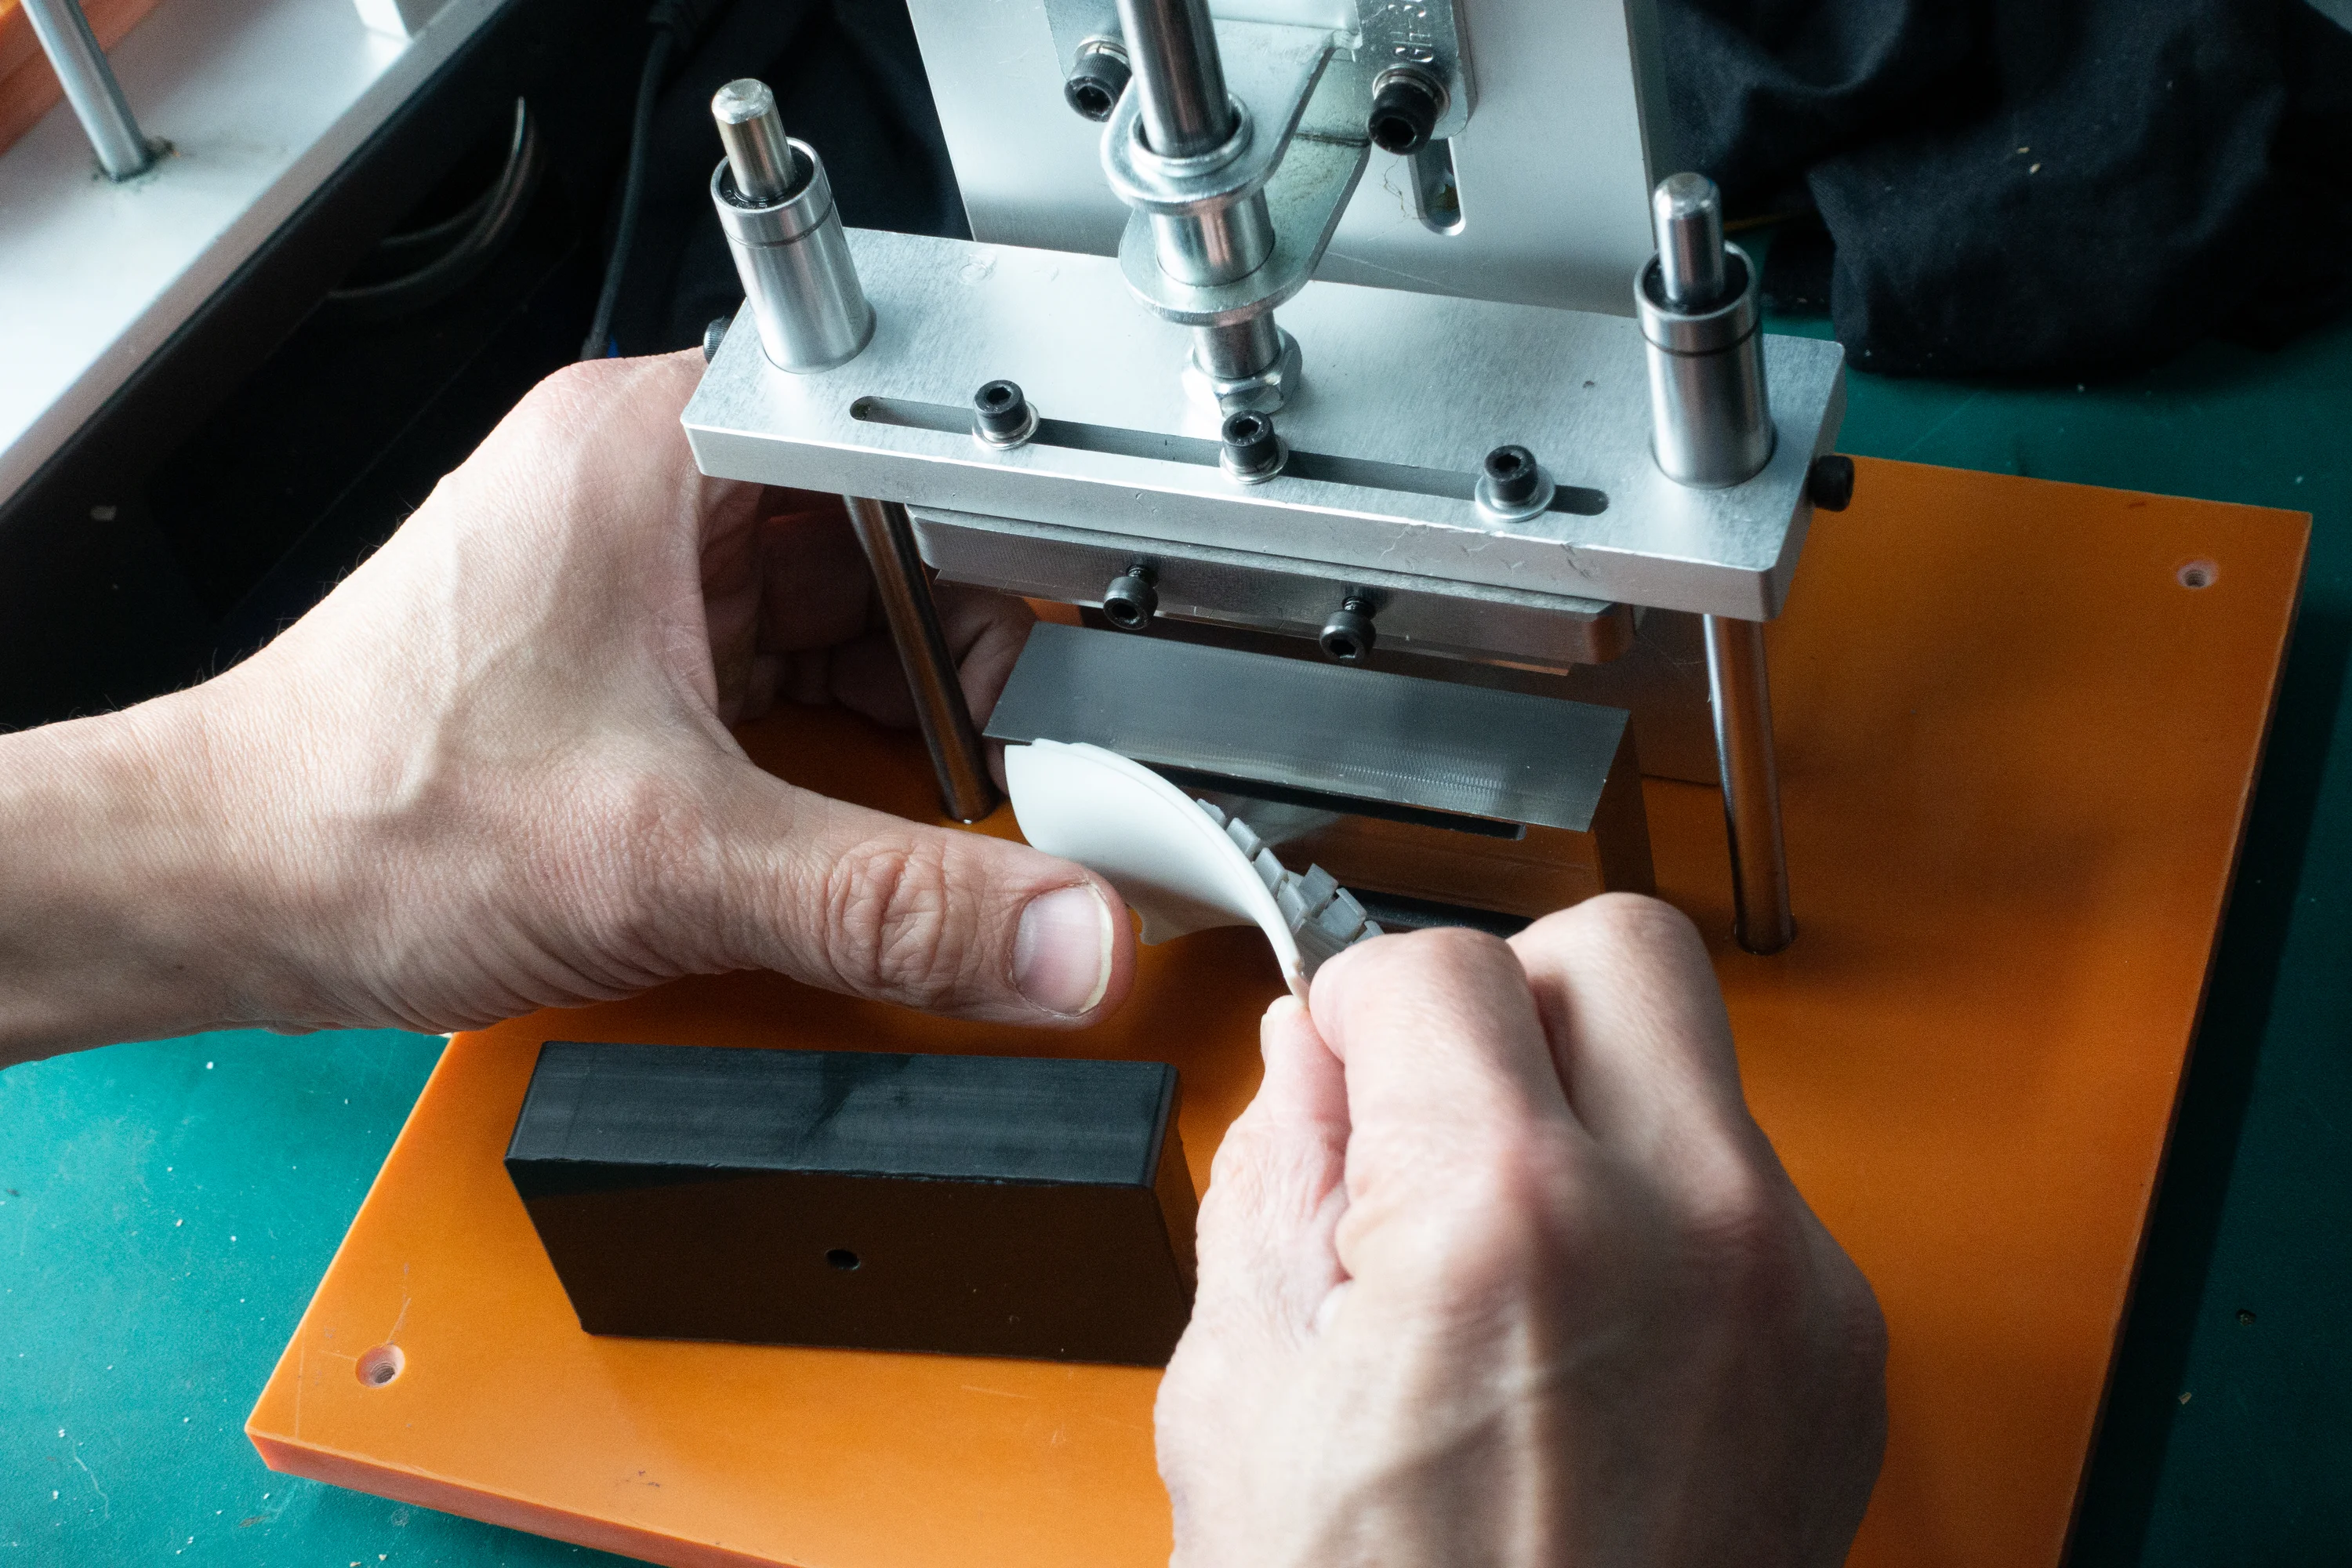
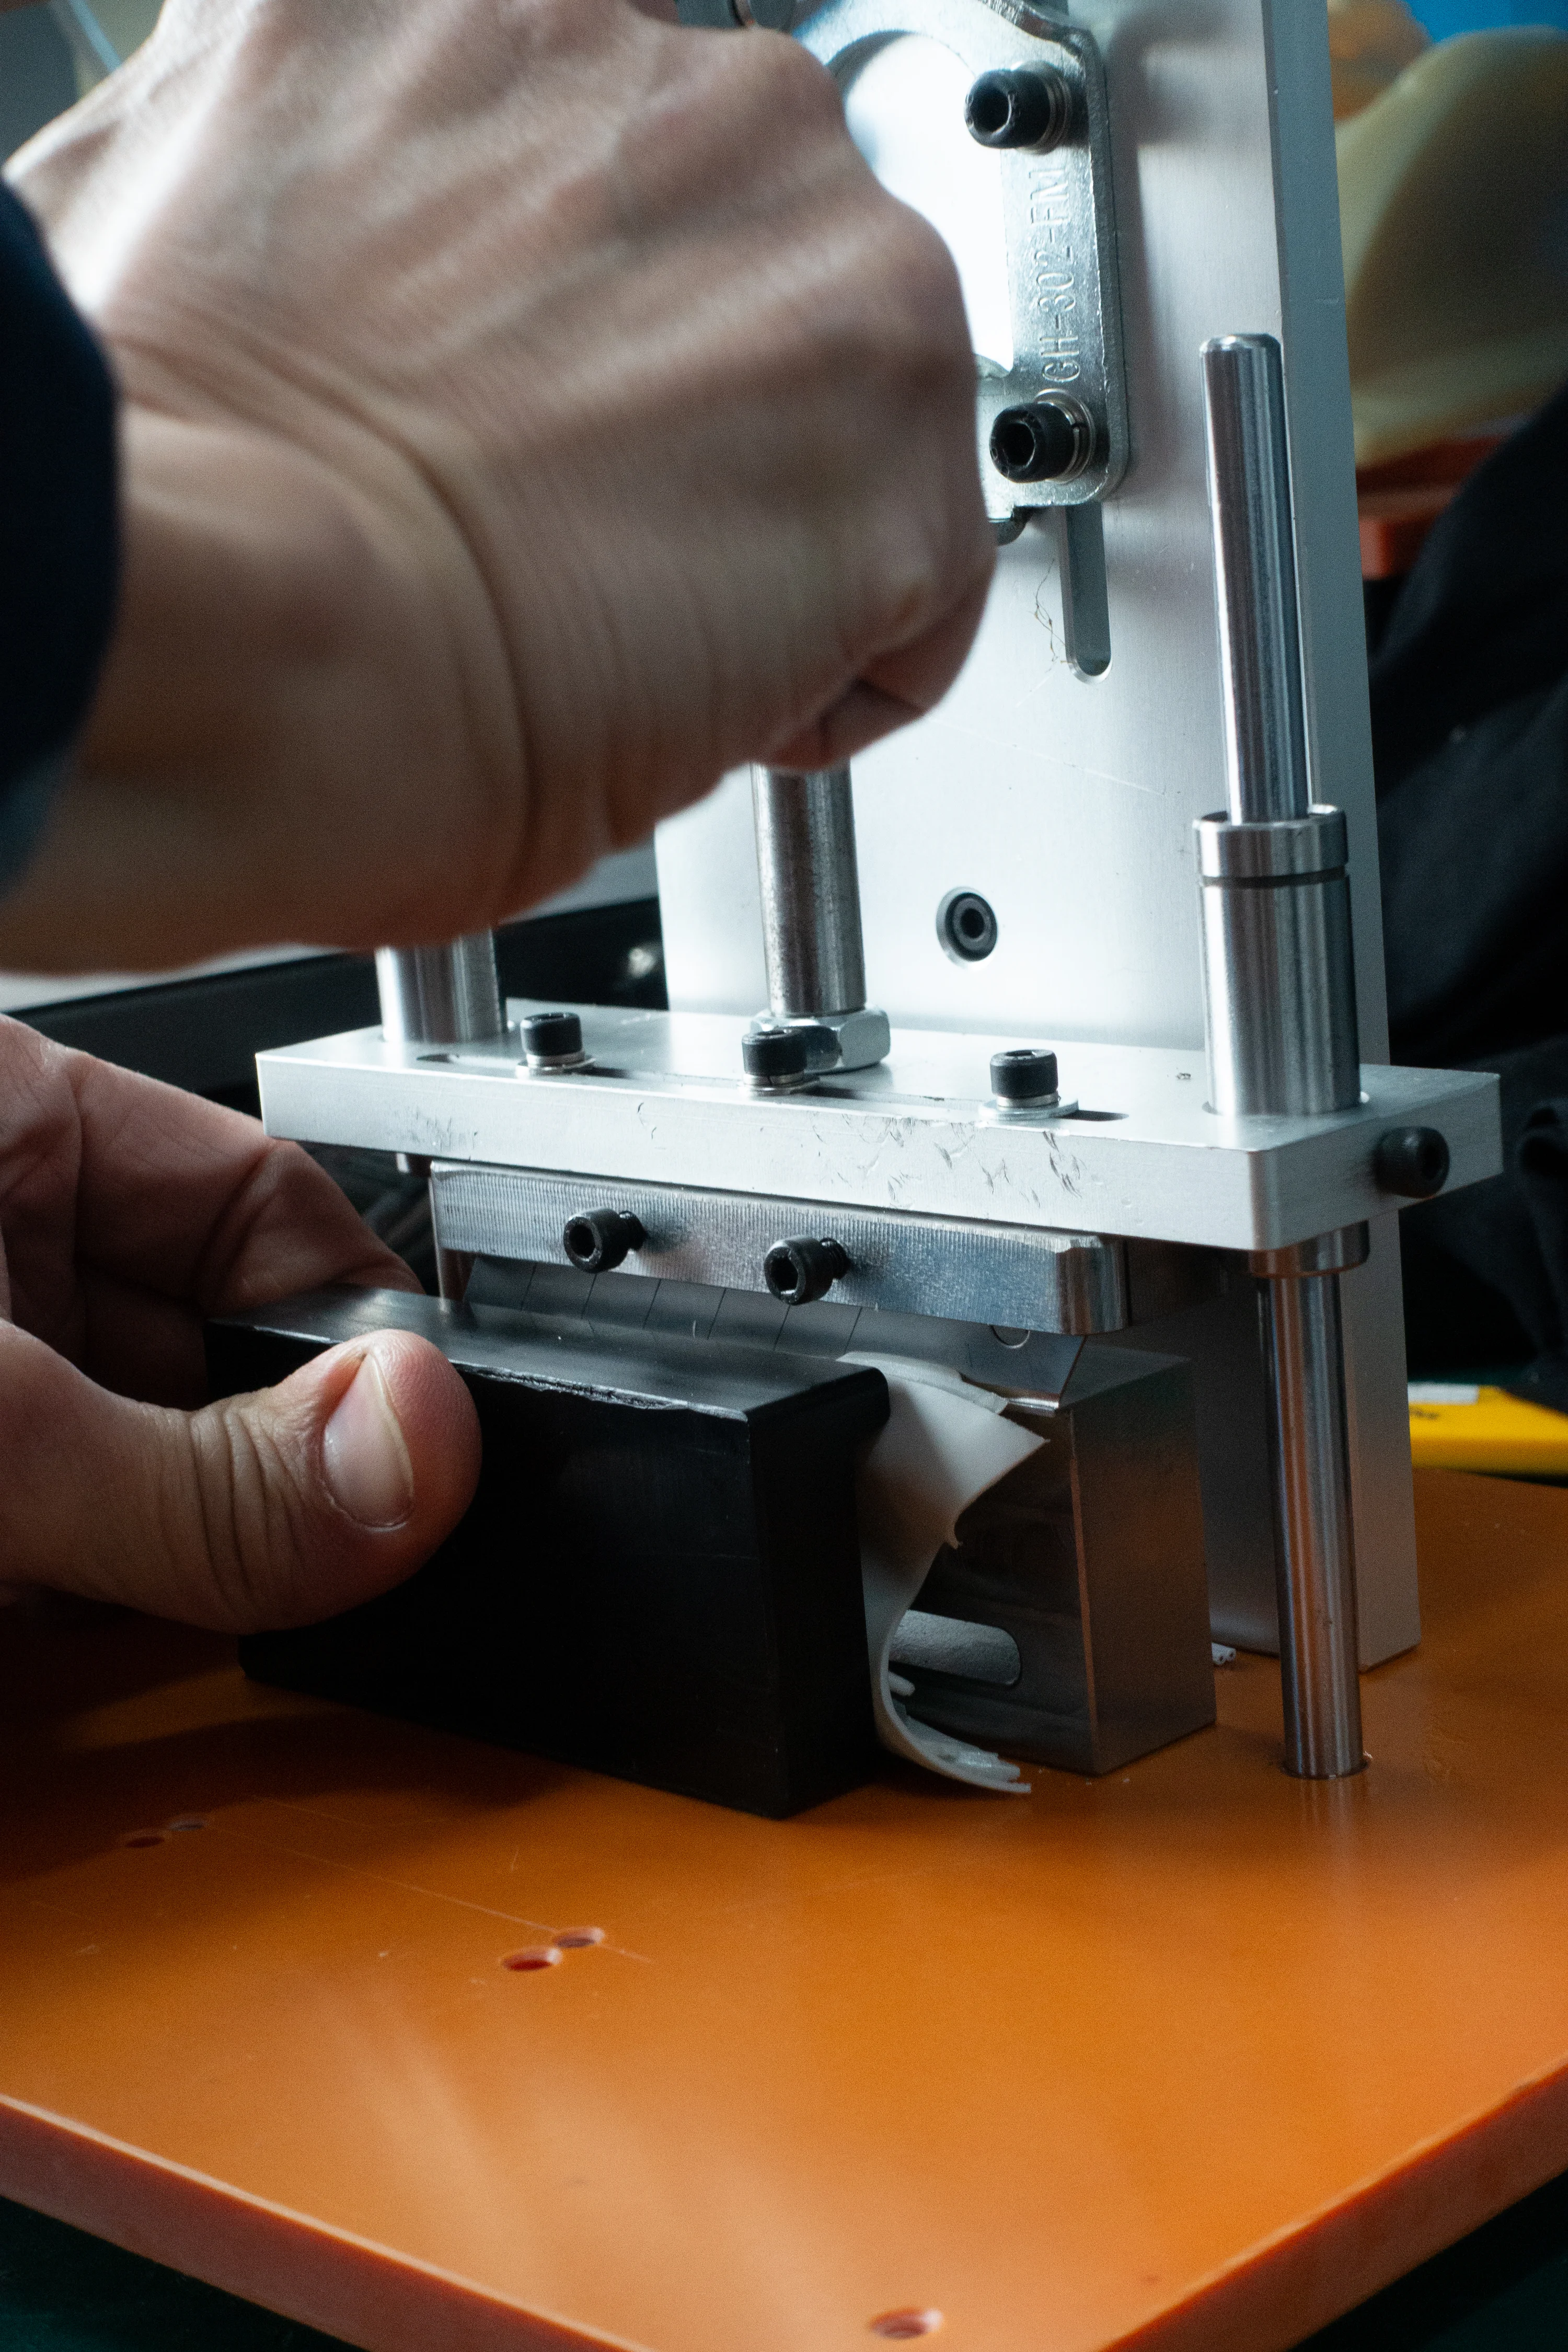
Movement, reliability and dust
Cable routing through a moving assembly
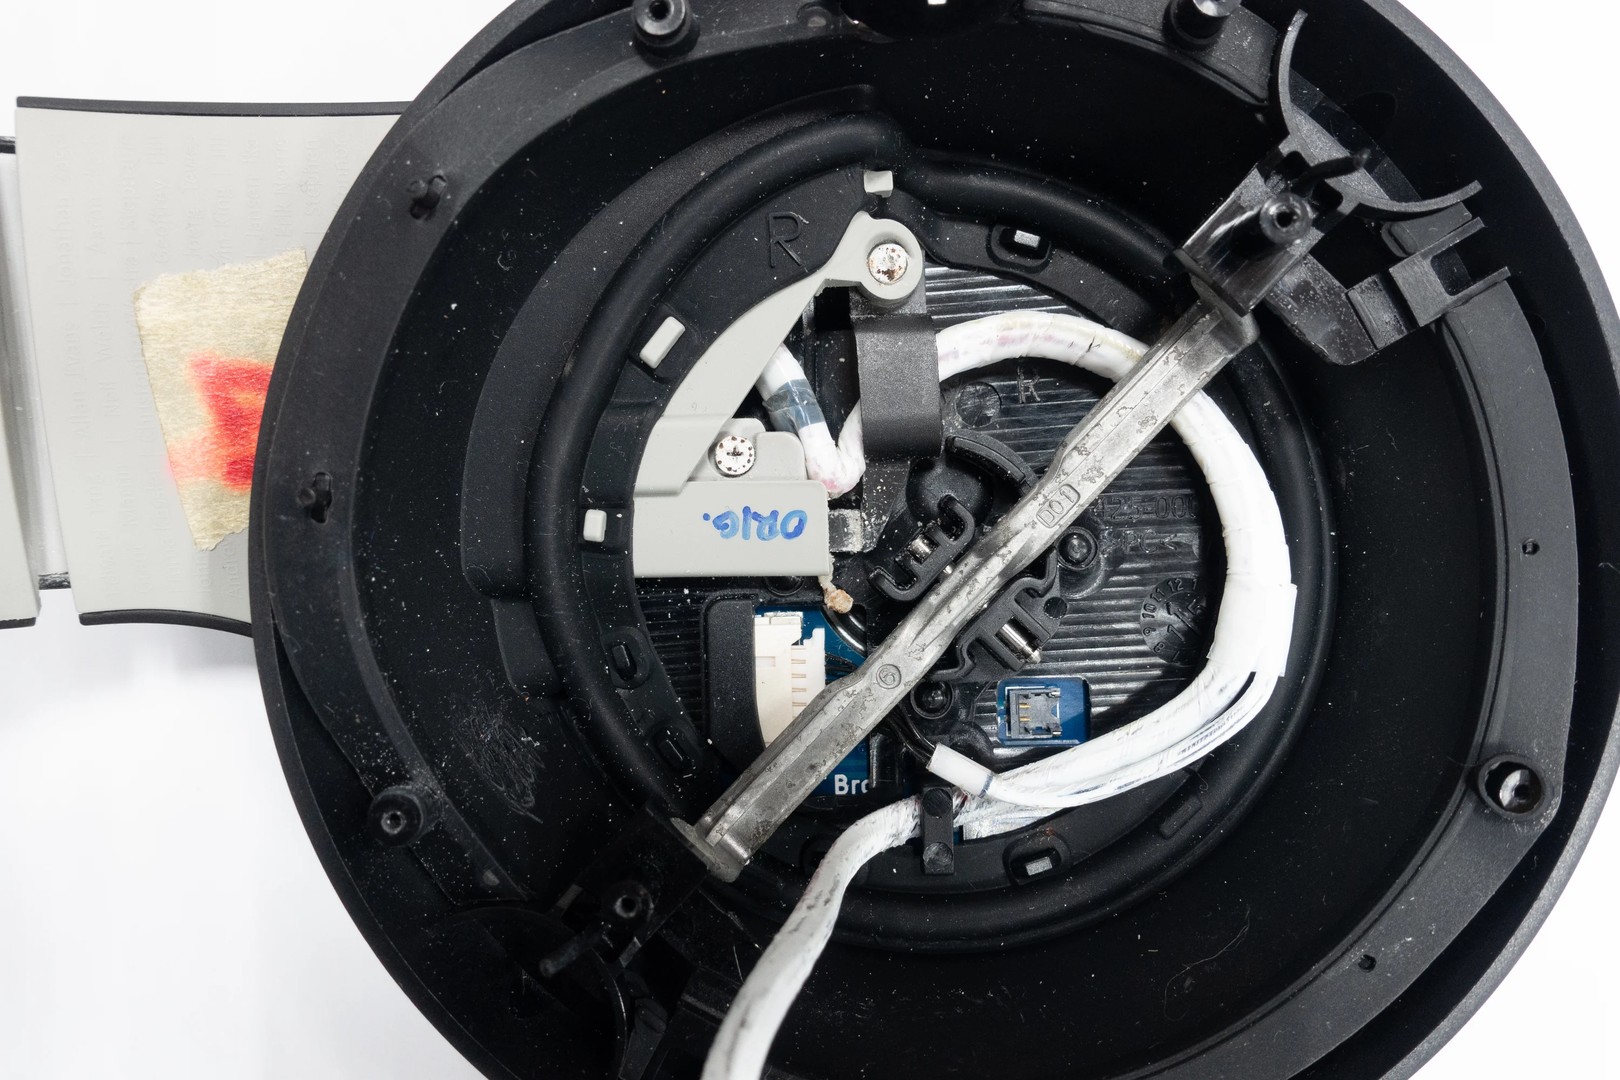
The cable could work initially, then develop a kink after repeated cycling and bind soon afterward. Adding stiffness could help it resist buckling, but the bundle still had to fit and move through a confined path. Protective tape could curl at its edges and increase the effort needed to telescope the arm. Local stiffness, bundle size, friction and routing had to work together.
I spent a great deal of time working through those combinations: splints, different jackets and wires, changes to the looming specifications. Careful design of experiments, lots of changes and lots of cycles.
 From the workbench
Following the cable through repeated motion
Trace the service loop and inspect cable variants as kinks, abrasion and return problems emerge.
Explore investigation +Close investigation −
Following the cable through repeated motion
Trace the service loop and inspect cable variants as kinks, abrasion and return problems emerge.
Explore investigation +Close investigation −The slack for telescoping extension lived inside the earcan, wound around the center as a service loop. Adjacent features guided and housed it as it expanded and contracted. The pass-throughs at each end of the telescoping sections mattered too. The pivot arm could bind the cable against the housing in several positions, and long, curved surfaces sliding past one another offered more places to snag. Fixing points, routing and variation in the cable and its covering all affected how it behaved.
Kinking and abrasion across cable variants
Different tested cable variants, showing kinking and abrasion.
Cycle testing exposed kinking and abrasion across multiple harness variants. The photographs record the different ways the cables were damaged as the earcans were extended and retracted.
The comparative cable builds used identified assemblies and staged inspections. The protocol called for opening the units, photographing the cable in its collapsed position and reassembling them between checkpoints. That let us examine how a construction changed as it accumulated cycles, as well as whether the arm still returned.
An idea also had to survive fabrication and assembly. Fujikura withdrew one PET-film stiffening proposal because the film peeled open before or during the spiral-wrapping operation. Other discussions compared sidewalls, splints, wrap widths and wrap direction. A promising cross-section was only one part of making a workable harness.
Two five-unit groups tested in March 2016 give a sense of the range of behavior. In T6, two units could not return at 250 cycles. The separate T5 group recorded OK wear and kink checks through 3,000 cycles.
With the splint approach rejected, we were working on three fronts:
| Workstream | What we were changing |
|---|---|
| Existing production assemblies | Chassis machining, cable rework, protective tape and routing |
| Production tooling and harness design | Changes intended to replace repeated secondary operations and rework |
| Alternative cable construction | Amphenol tube/sleeve concepts and samples, while Fujikura sustaining work continued |
Mechanical ECOs for the surrounding parts were released while the alternative cable samples remained a separate development effort. The practical task was to keep improving the assembly in production while evaluating what should replace it.
The work carried into production through careful harness assembly, inspection and system assembly. During the short production run, I instituted a mid-build "break-in" cycling station to test and validate the process and support ongoing improvement. I specified cycling 20% of units; in practice, we only did one in ten. No kink meant pass and continue through assembly.
Electrical checks and physical condition
Electrical continuity did not tell the whole story. Of 17 cables returned from the production line for supplier analysis, 11 passed the electrical retest, five had open or short circuits, and one connector was too damaged to test. Some of the electrically passing cables still showed visible jacket or connector damage. Inspecting the physical condition answered a different question from checking whether the wires still conducted.
The work extended into retention, strain relief, adhesive placement and assembly instructions. We were working on the harness and the parts around it at the same time: modifying routing and wrap, protecting contact points and changing the chassis where it could damage the cable. Those changes needed to work together in the assembled product.
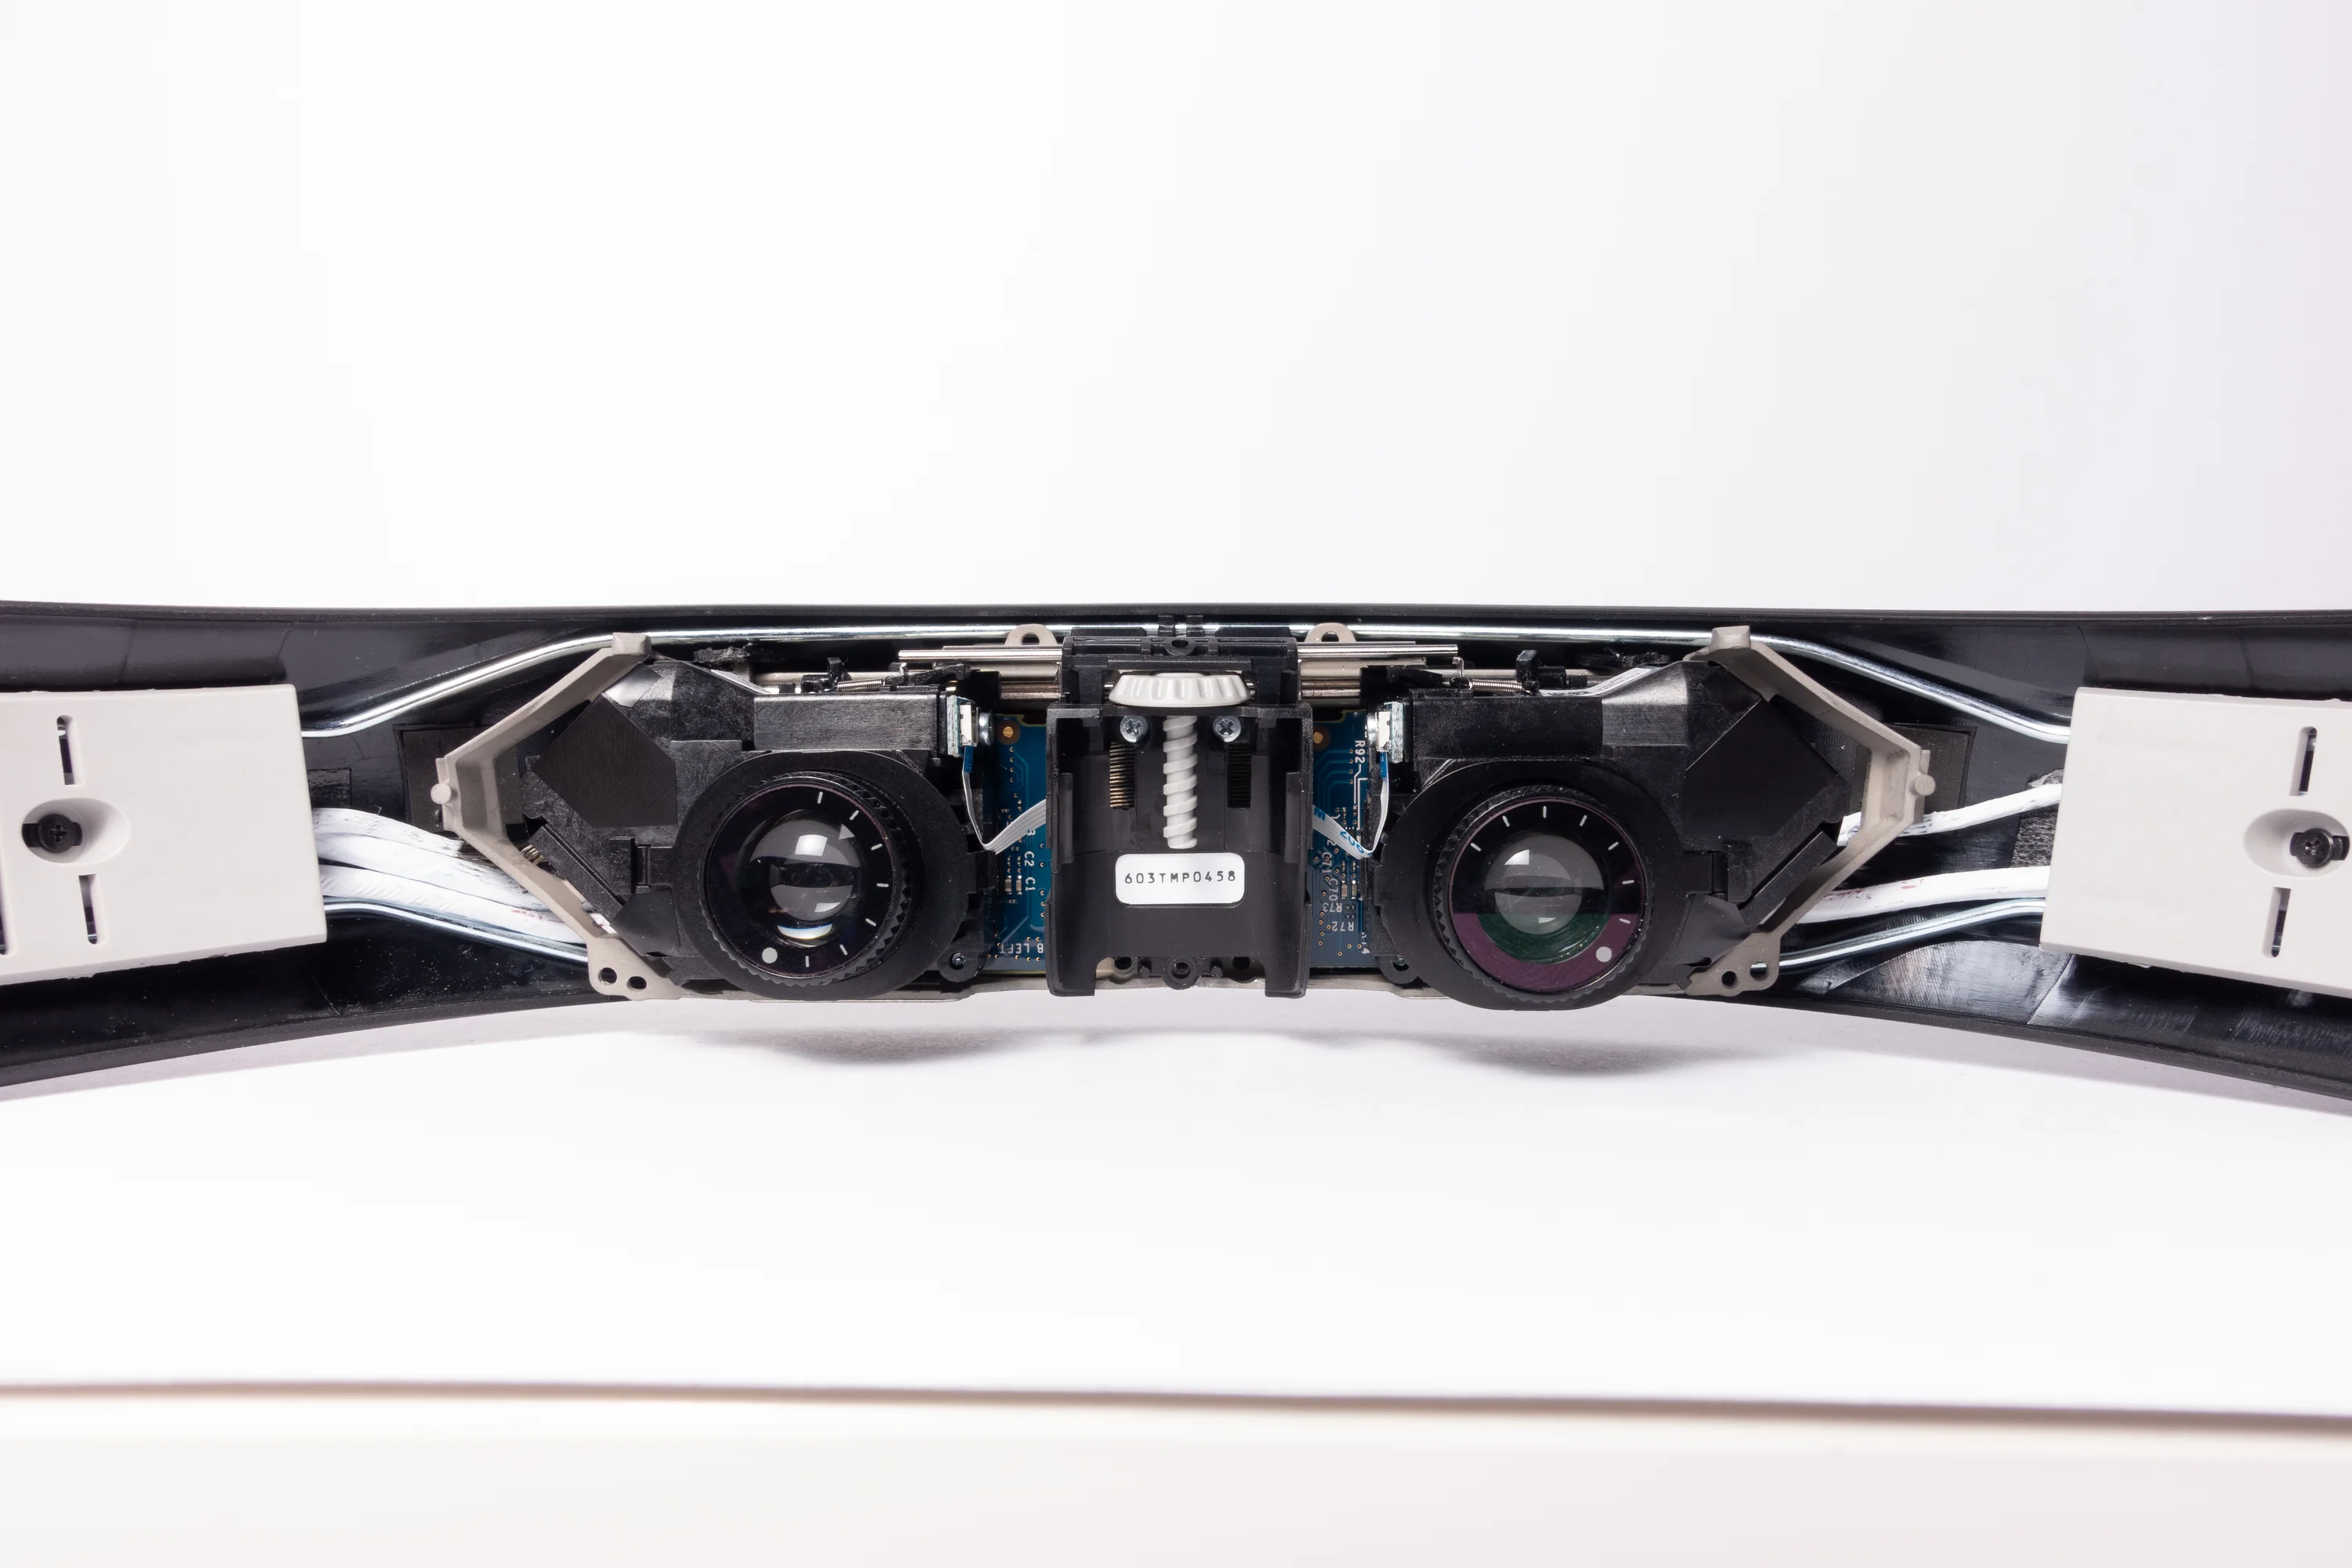
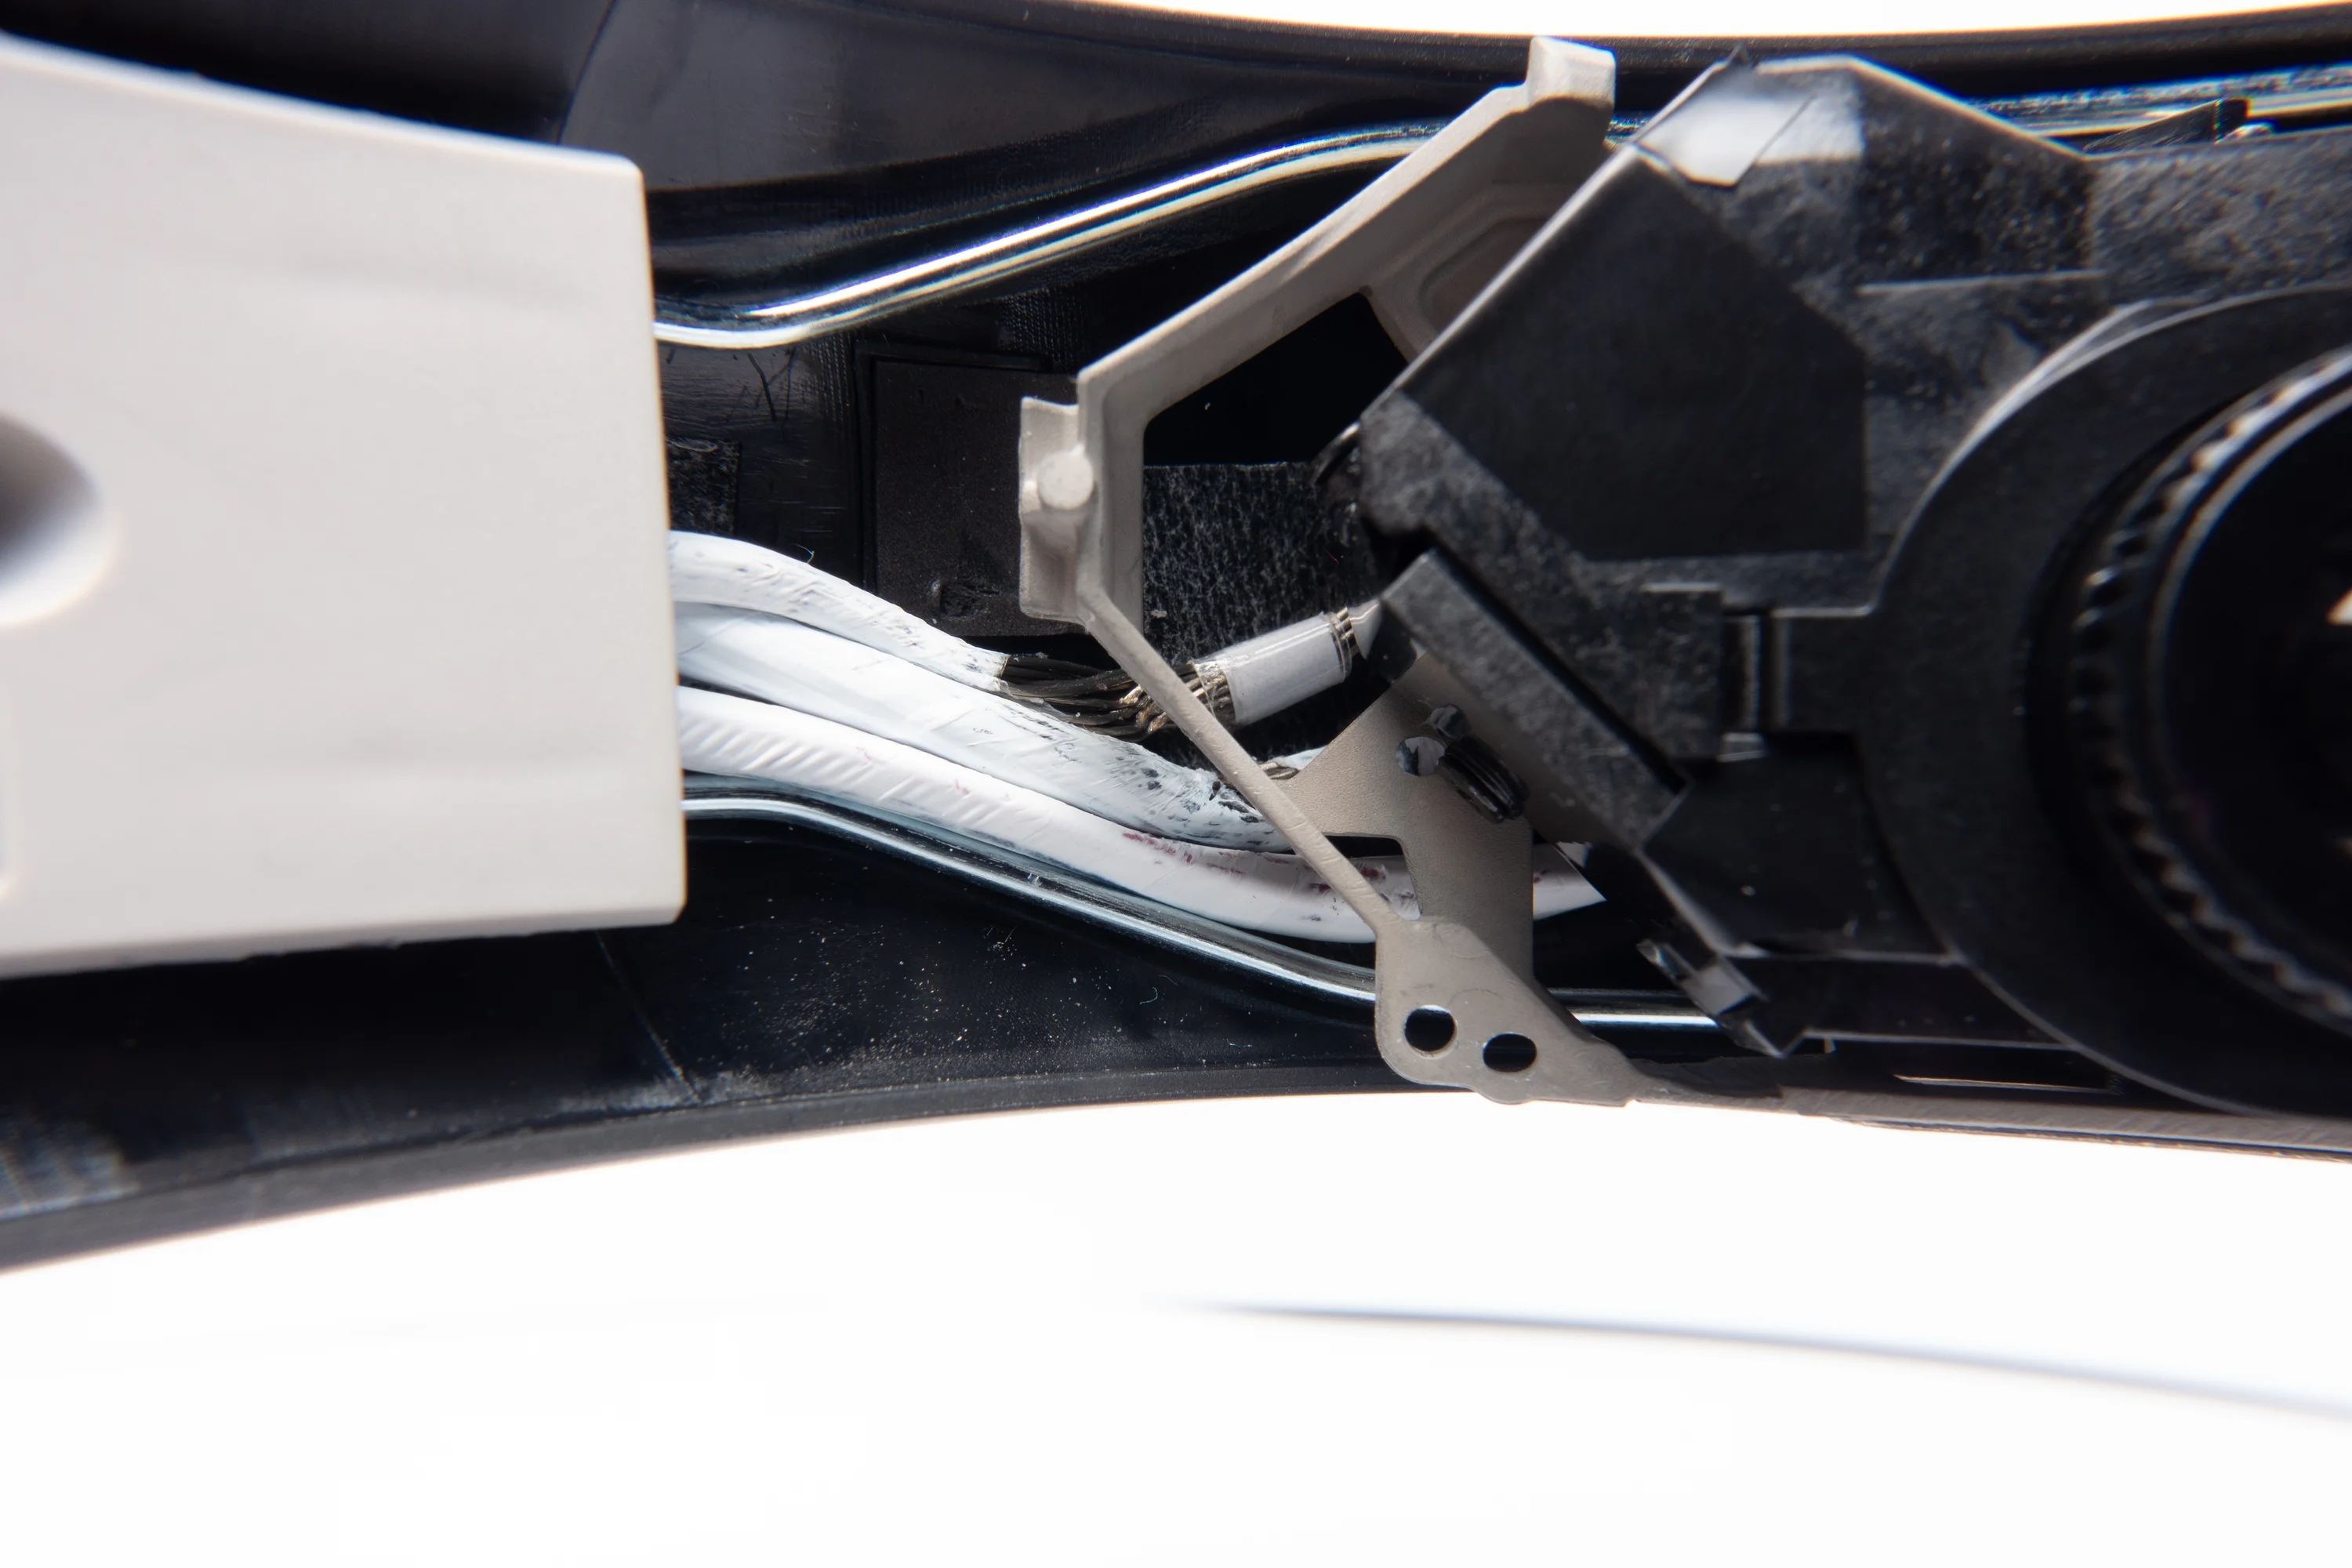
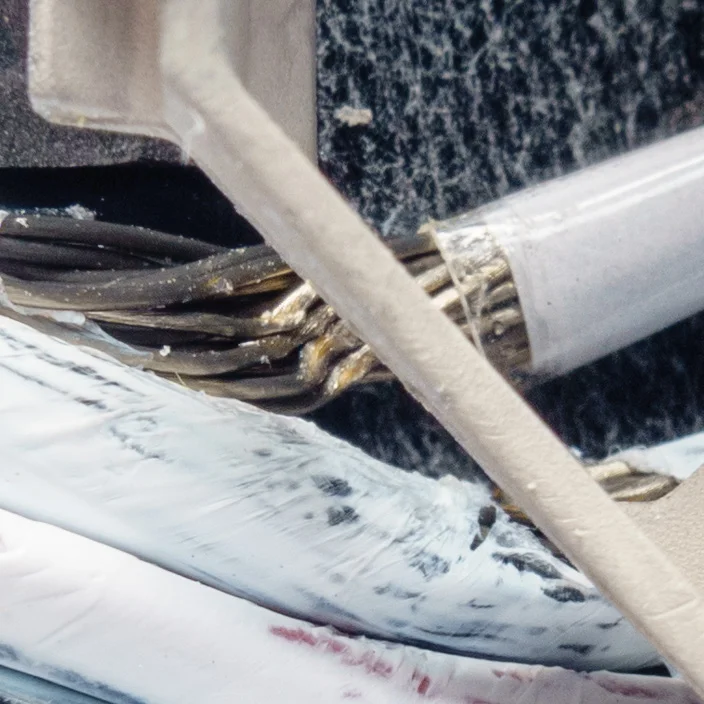
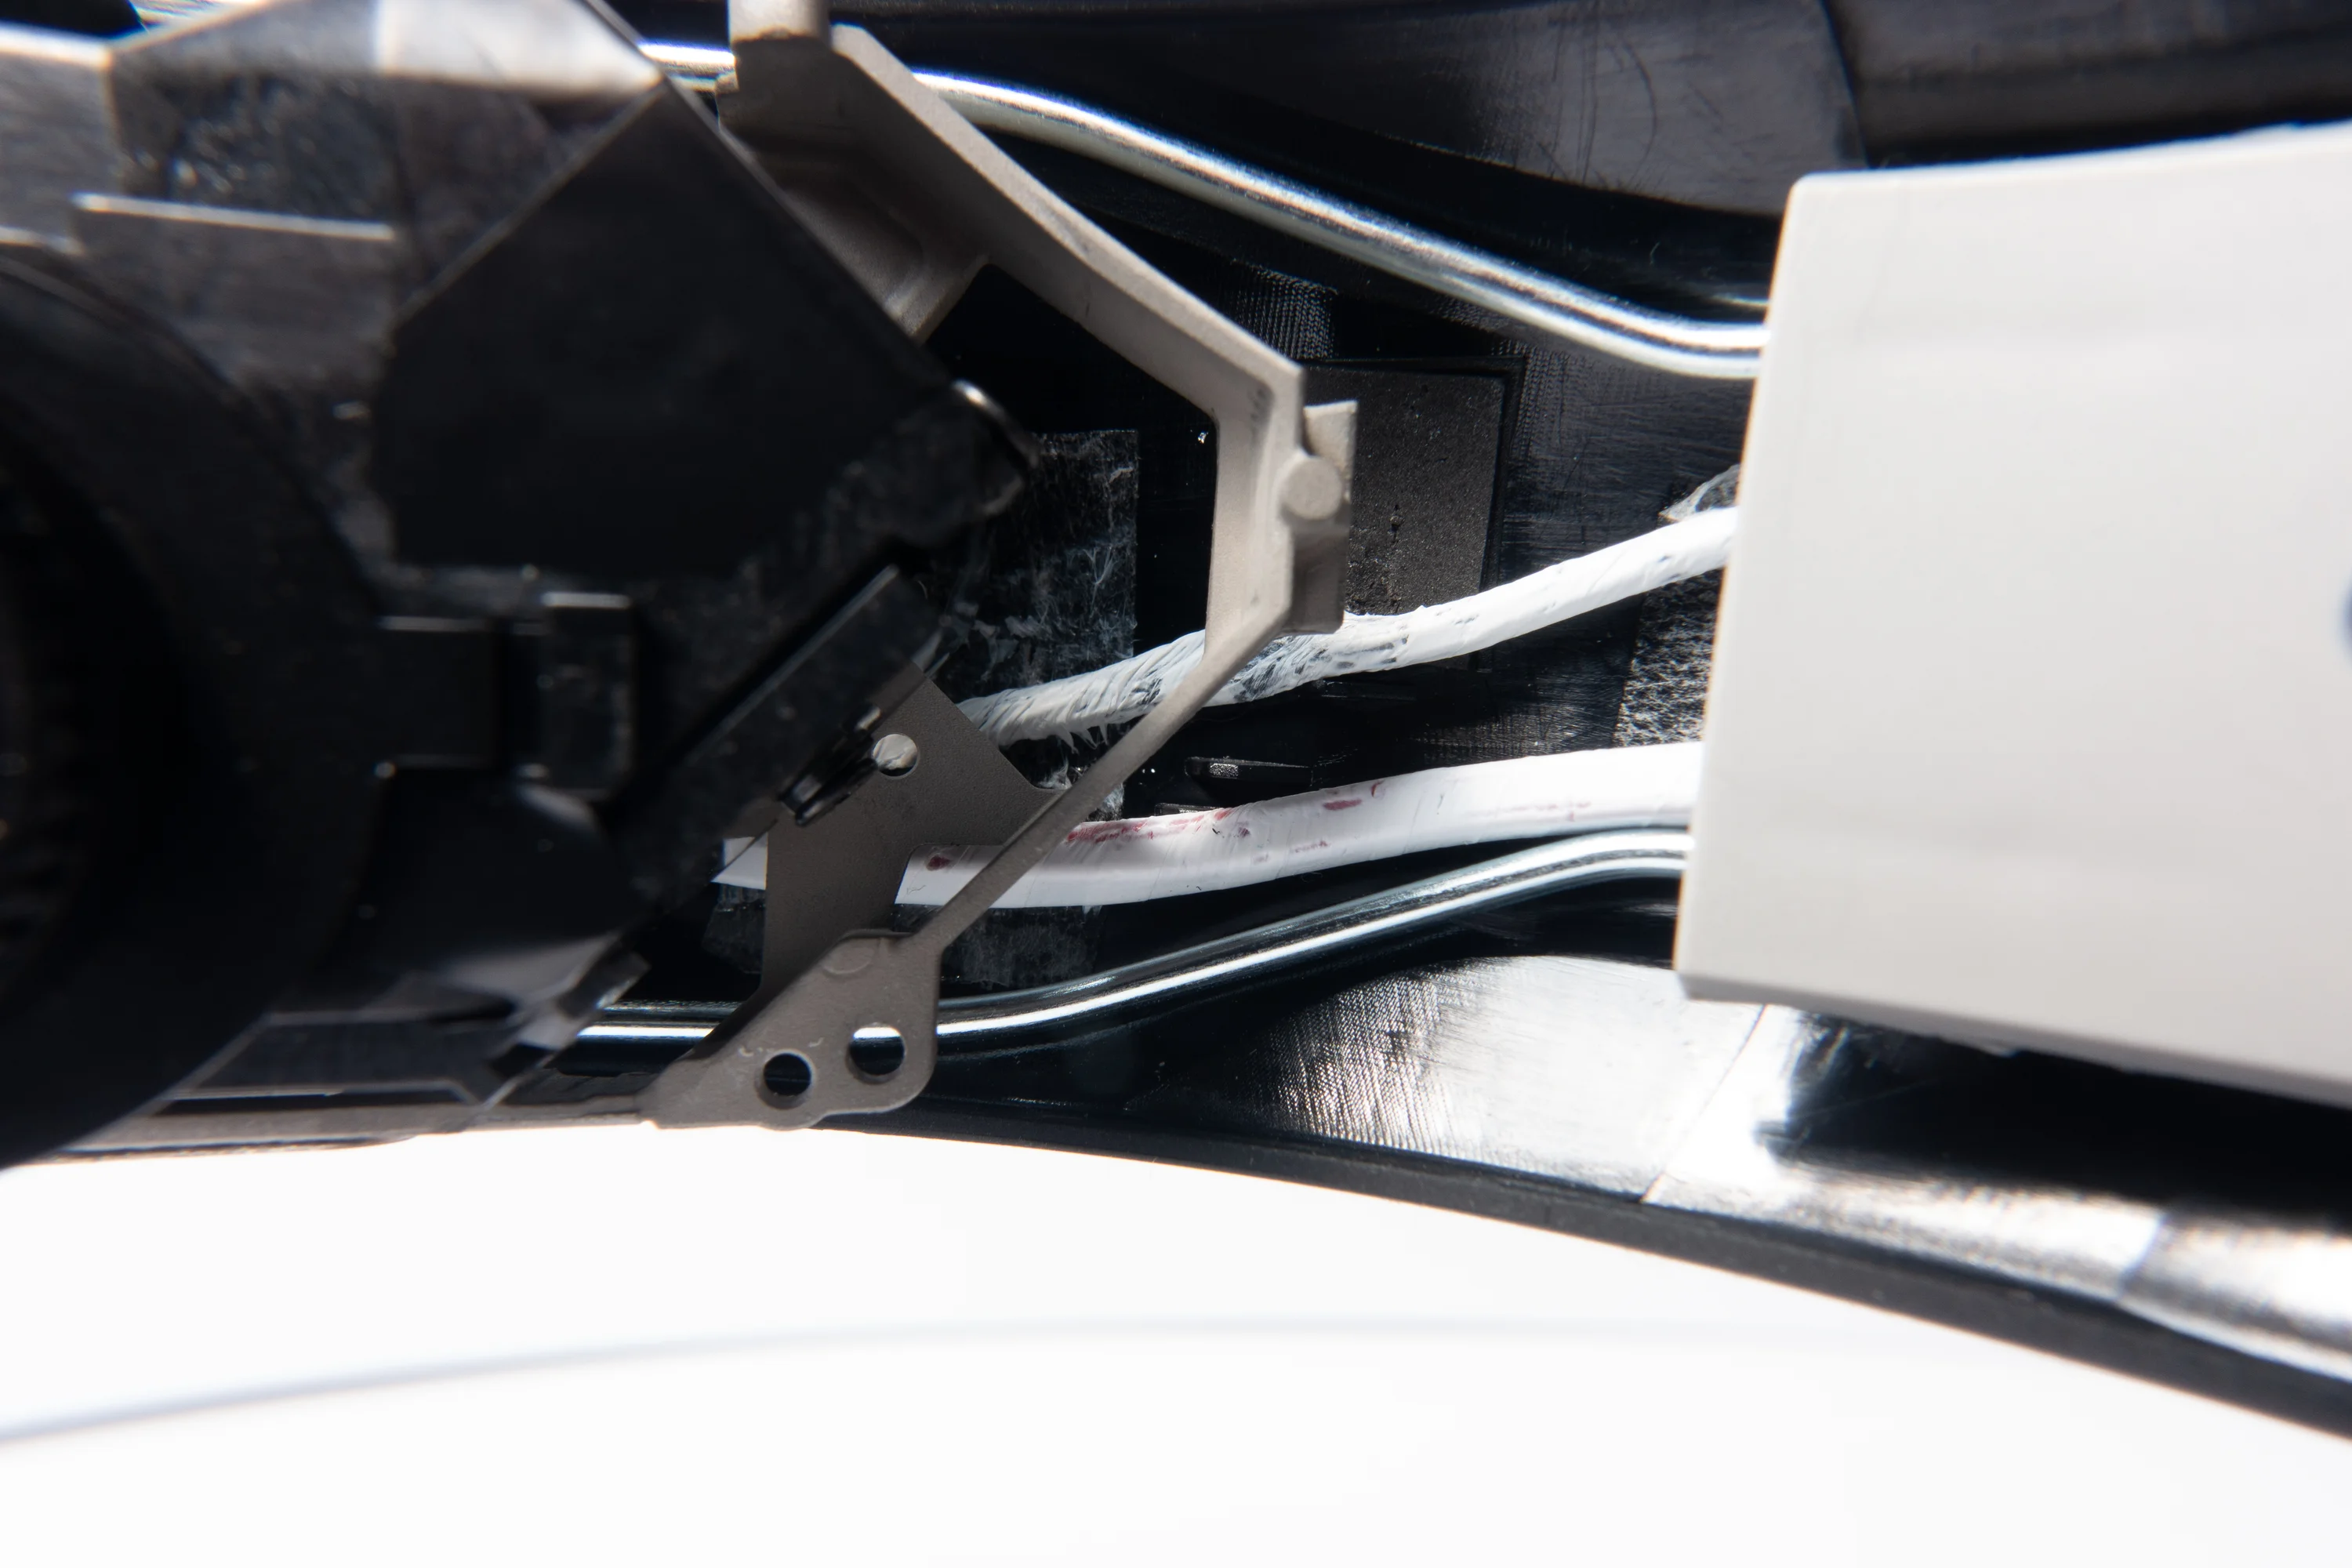
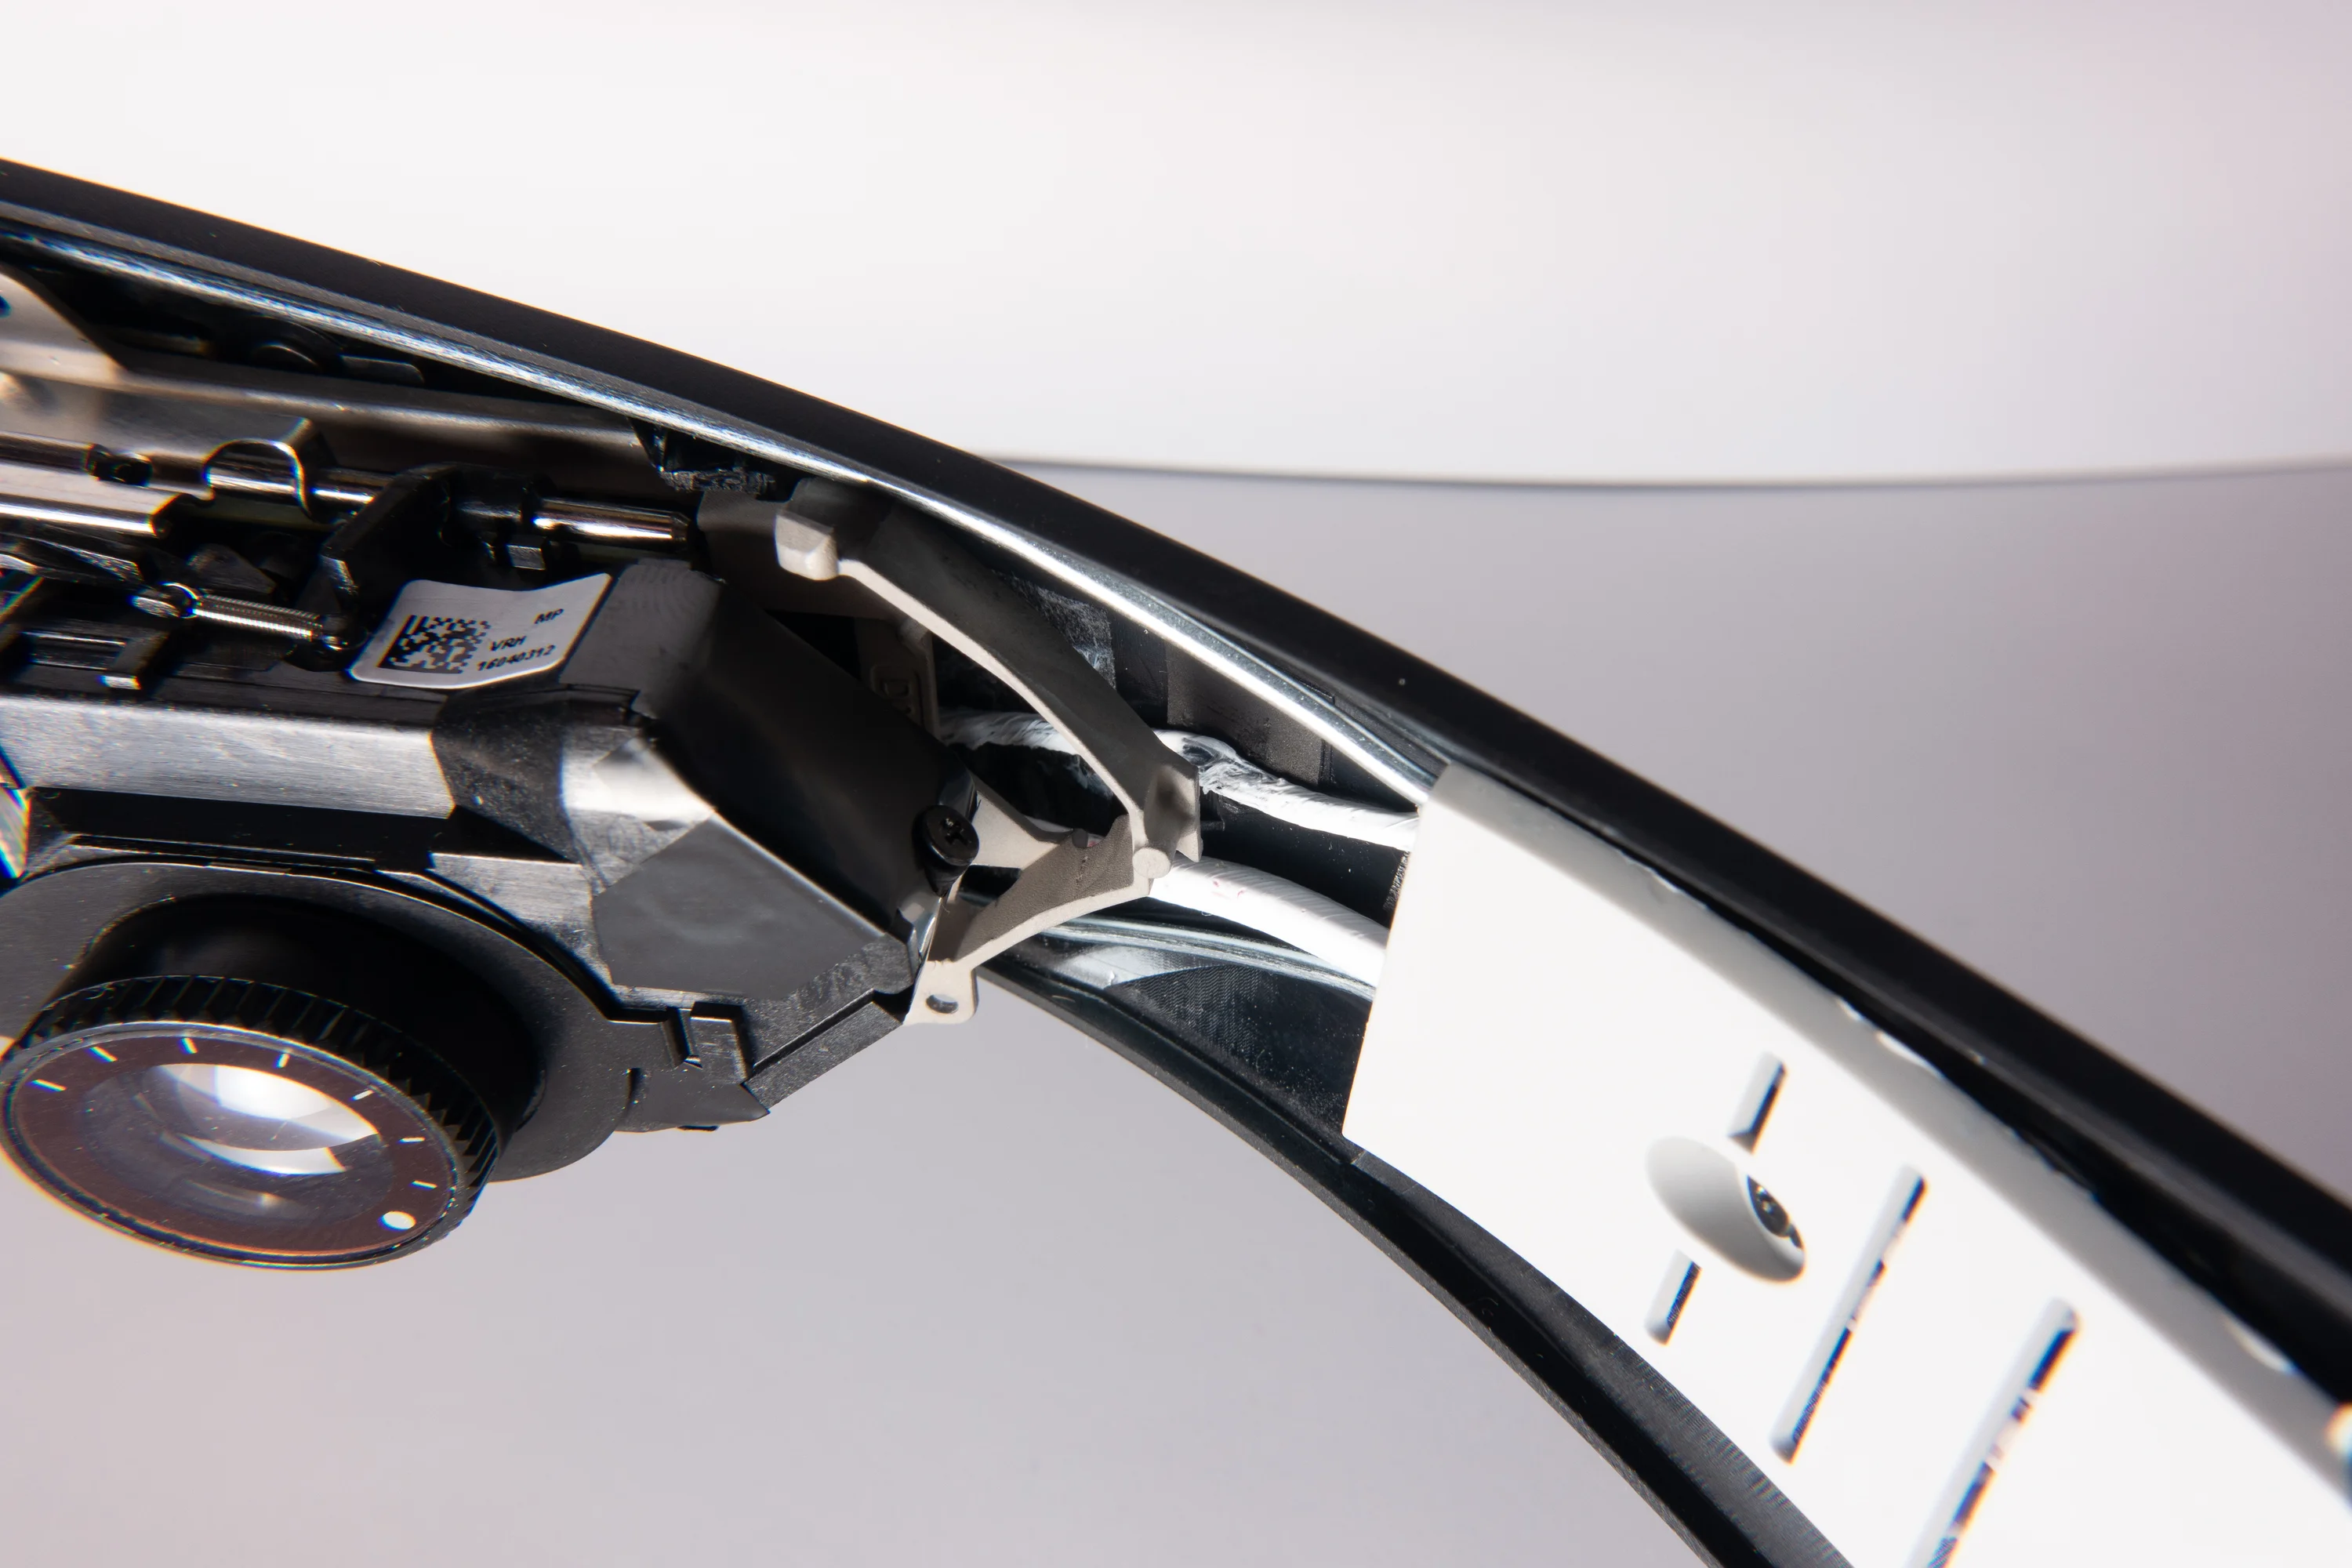
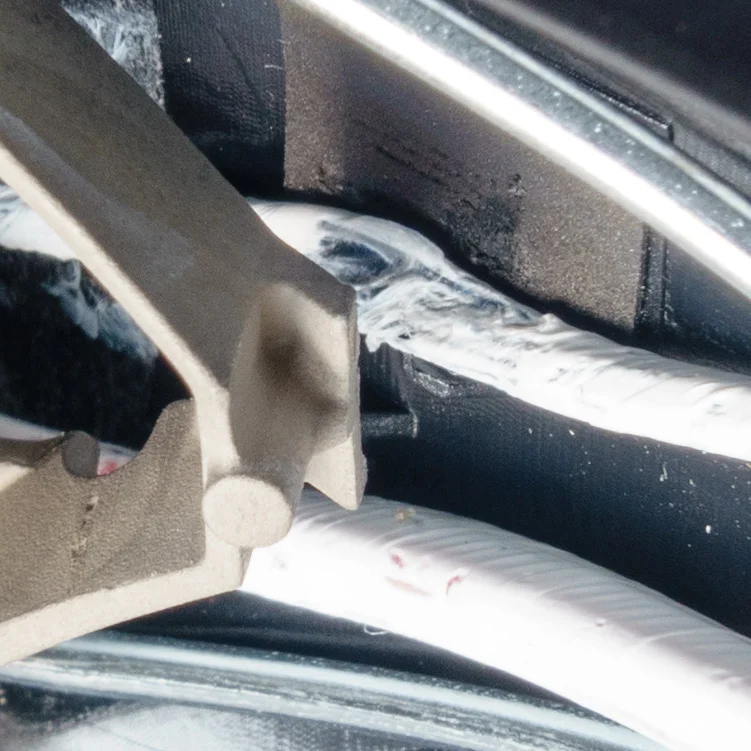
Pinching at the optical chassis
Some cable damage came from mechanical pinching and impingement during normal use, or was present straight out of assembly. I spent a great deal of time specifying secondary operations and trimming of the optics chassis, and documenting acceptable surface conditions and zones after injection molding.
Pinching at the optical chassis
Pinching and impingement during normal use or straight out of assembly. My work included chassis trimming, secondary operations and specifications for acceptable surface conditions and zones.
Dust after assembly
With a disassembled Glyph, you could feel the air move as you extended and retracted the arms. Extension left more internal volume; retraction left less. Cycle it quickly and it pumped air through the gaps, carrying ambient dust toward the optics.
That meant a clean optical subassembly could become contaminated inside a nearly finished product. The optics-module assembly had its own dust problems. Cleanroom conditions and procedures largely brought that source under control, and every optical subassembly was inspected, with affected assemblies sent for rework or scrap. Some particles also came from materials inside the product. Around the folding mirrors, blackout-tape trimmings were a source of particles. The team's change to painted mirror edges made cleaning and rework easier.
I tightened the fits and tolerances between the stationary headband parts and the sliding earcan parts to reduce the gaps. I also added Kapton tape around the optical module to reduce the openings for particles. We never completely eliminated the pumping.
I changed the test order as well. Final optical checks moved into the final clean-area functional tests, after all the other physical functional tests. The optical inspection then checked the condition left by the operations that could contaminate the unit.
Diagnosing returned units
Diagnosing and mitigating field failures took a substantial amount of my time. A dead headset, a dark display or missing audio was a starting symptom. The investigation could take us through the mechanical assembly, cables, electronics and optics before we understood what needed to change.
Reproducing the reported problem
One returned unit was reported to have no left-channel audio and static. The March 2016 bench report found audio working in both analog and HDMI modes, but reproduced the static. Its recommendation was to check the twist and wrapping of the cable bundles entering the input board. The reproduced problem was narrower than the original complaint, and it led back to a physical detail of the assembly.
Production board analysis showed why similar display symptoms could require different fixes. In November 2015, the team restored a striped-display board by cleaning an oxidized DMD connector pad. Other boards worked after shorted components were replaced. In one repair, a 33-ohm resistor had been replaced with 180 kilohms; correcting it brought the board back. These were specific diagnoses and repairs, rather than one explanation for every nonworking display.
My mechanical work overlapped those electrical investigations. In April, cable wear at the chassis was suspected in two MCU shorts, and I was responsible for the mechanical response. That work fed into the clearance, protection and routing changes described above. Cycling, electrical checks and teardown each told us something different about the resulting assembly.
What the return records captured
A return-analysis log covering December 19, 2016 through January 12, 2017, during my final weeks at Avegant, gives a useful snapshot of the range of findings. It contains 292 observations across 290 recorded serial numbers: 220 observations marked failed and 72 marked passed. Two serials occur in both groups. The failed observations break down by their recorded primary code:
| Recorded finding | Observations |
|---|---|
| Particles | 131 |
| Detached eyecan | 19 |
| Collapsed lens | 18 |
| Power | 13 |
| Boot | 7 |
| Other primary codes | 32 |
These are observations in one return-analysis log, not a failure rate for all shipped Glyphs. A unit could have more than one symptom, so its primary code was only part of the diagnostic picture. The mix shows why the work extended beyond whether a unit switched on: optical contamination, physical retention and electrical behavior all needed attention.
Factory corrective actions
A separate factory report records a revised mirror carrier entering production and a requirement to hold products in the QC room for seven days before first-article inspection and shipment. It also records supplier corrective-action follow-up for PCB via deviations and confirmation that a new shutter mold could meet its 90–93 degree bend-angle requirement.
Finish, graphics and personalization
Getting the appearance into production
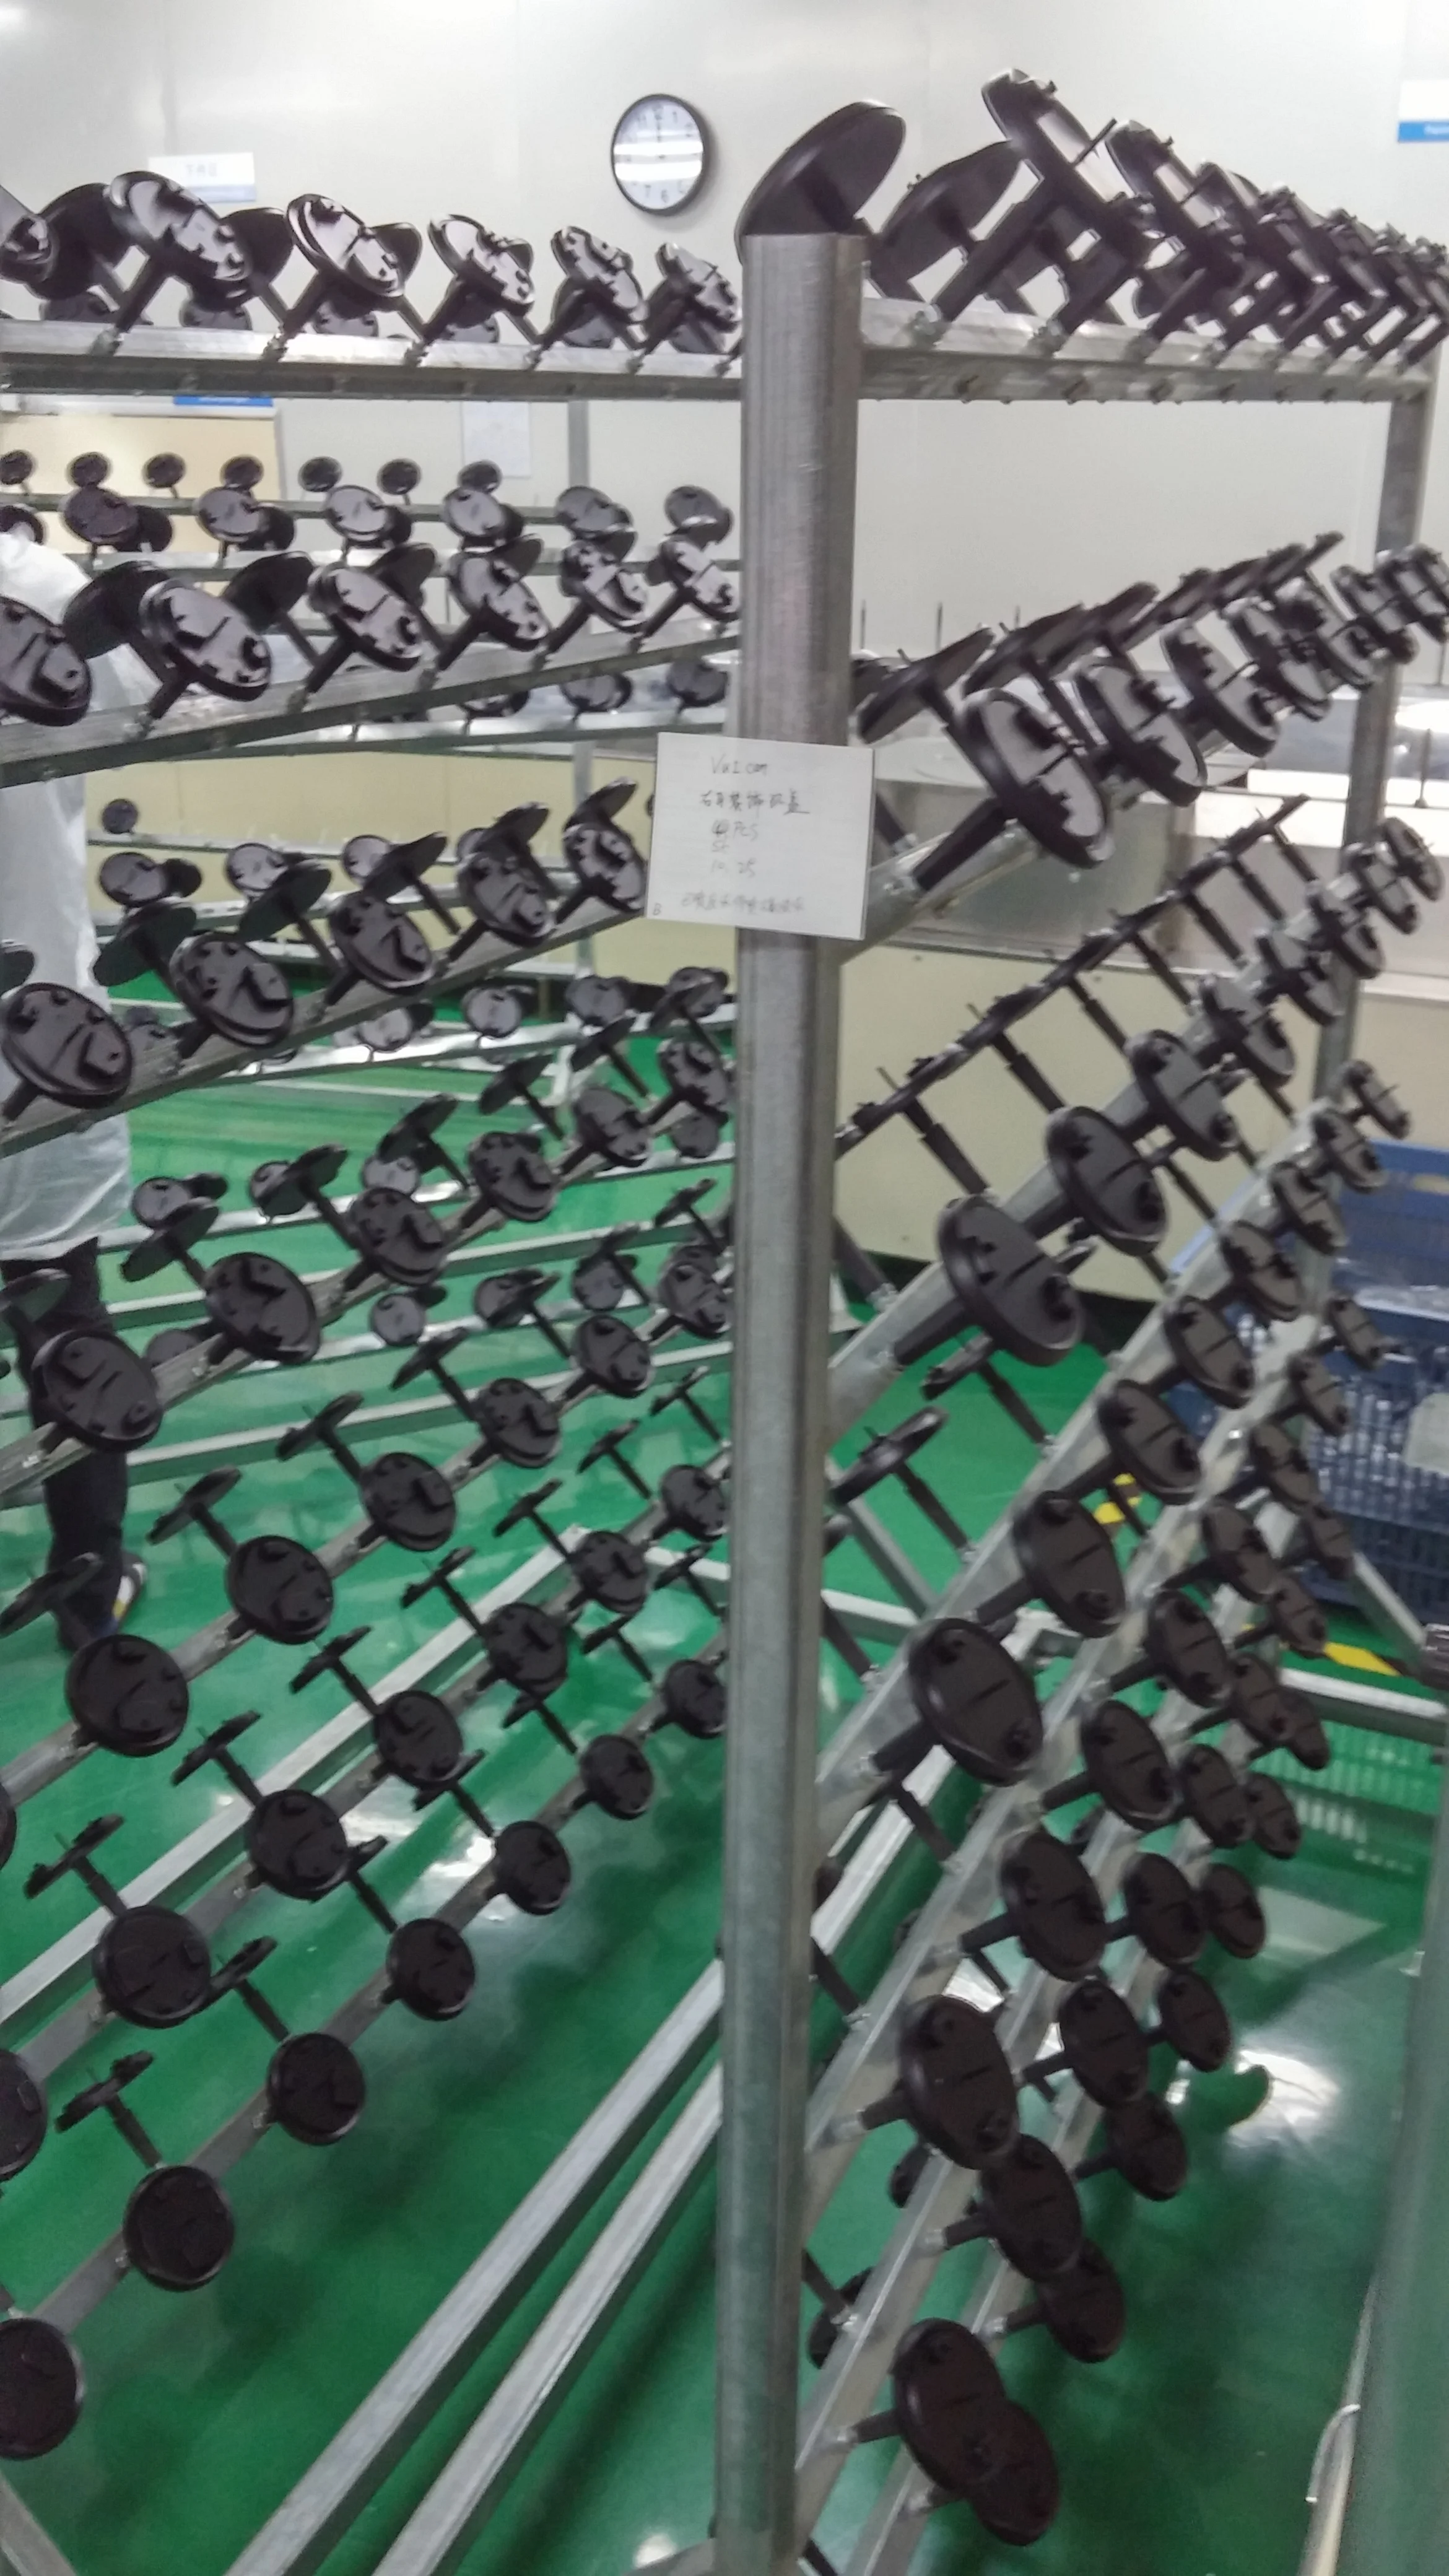
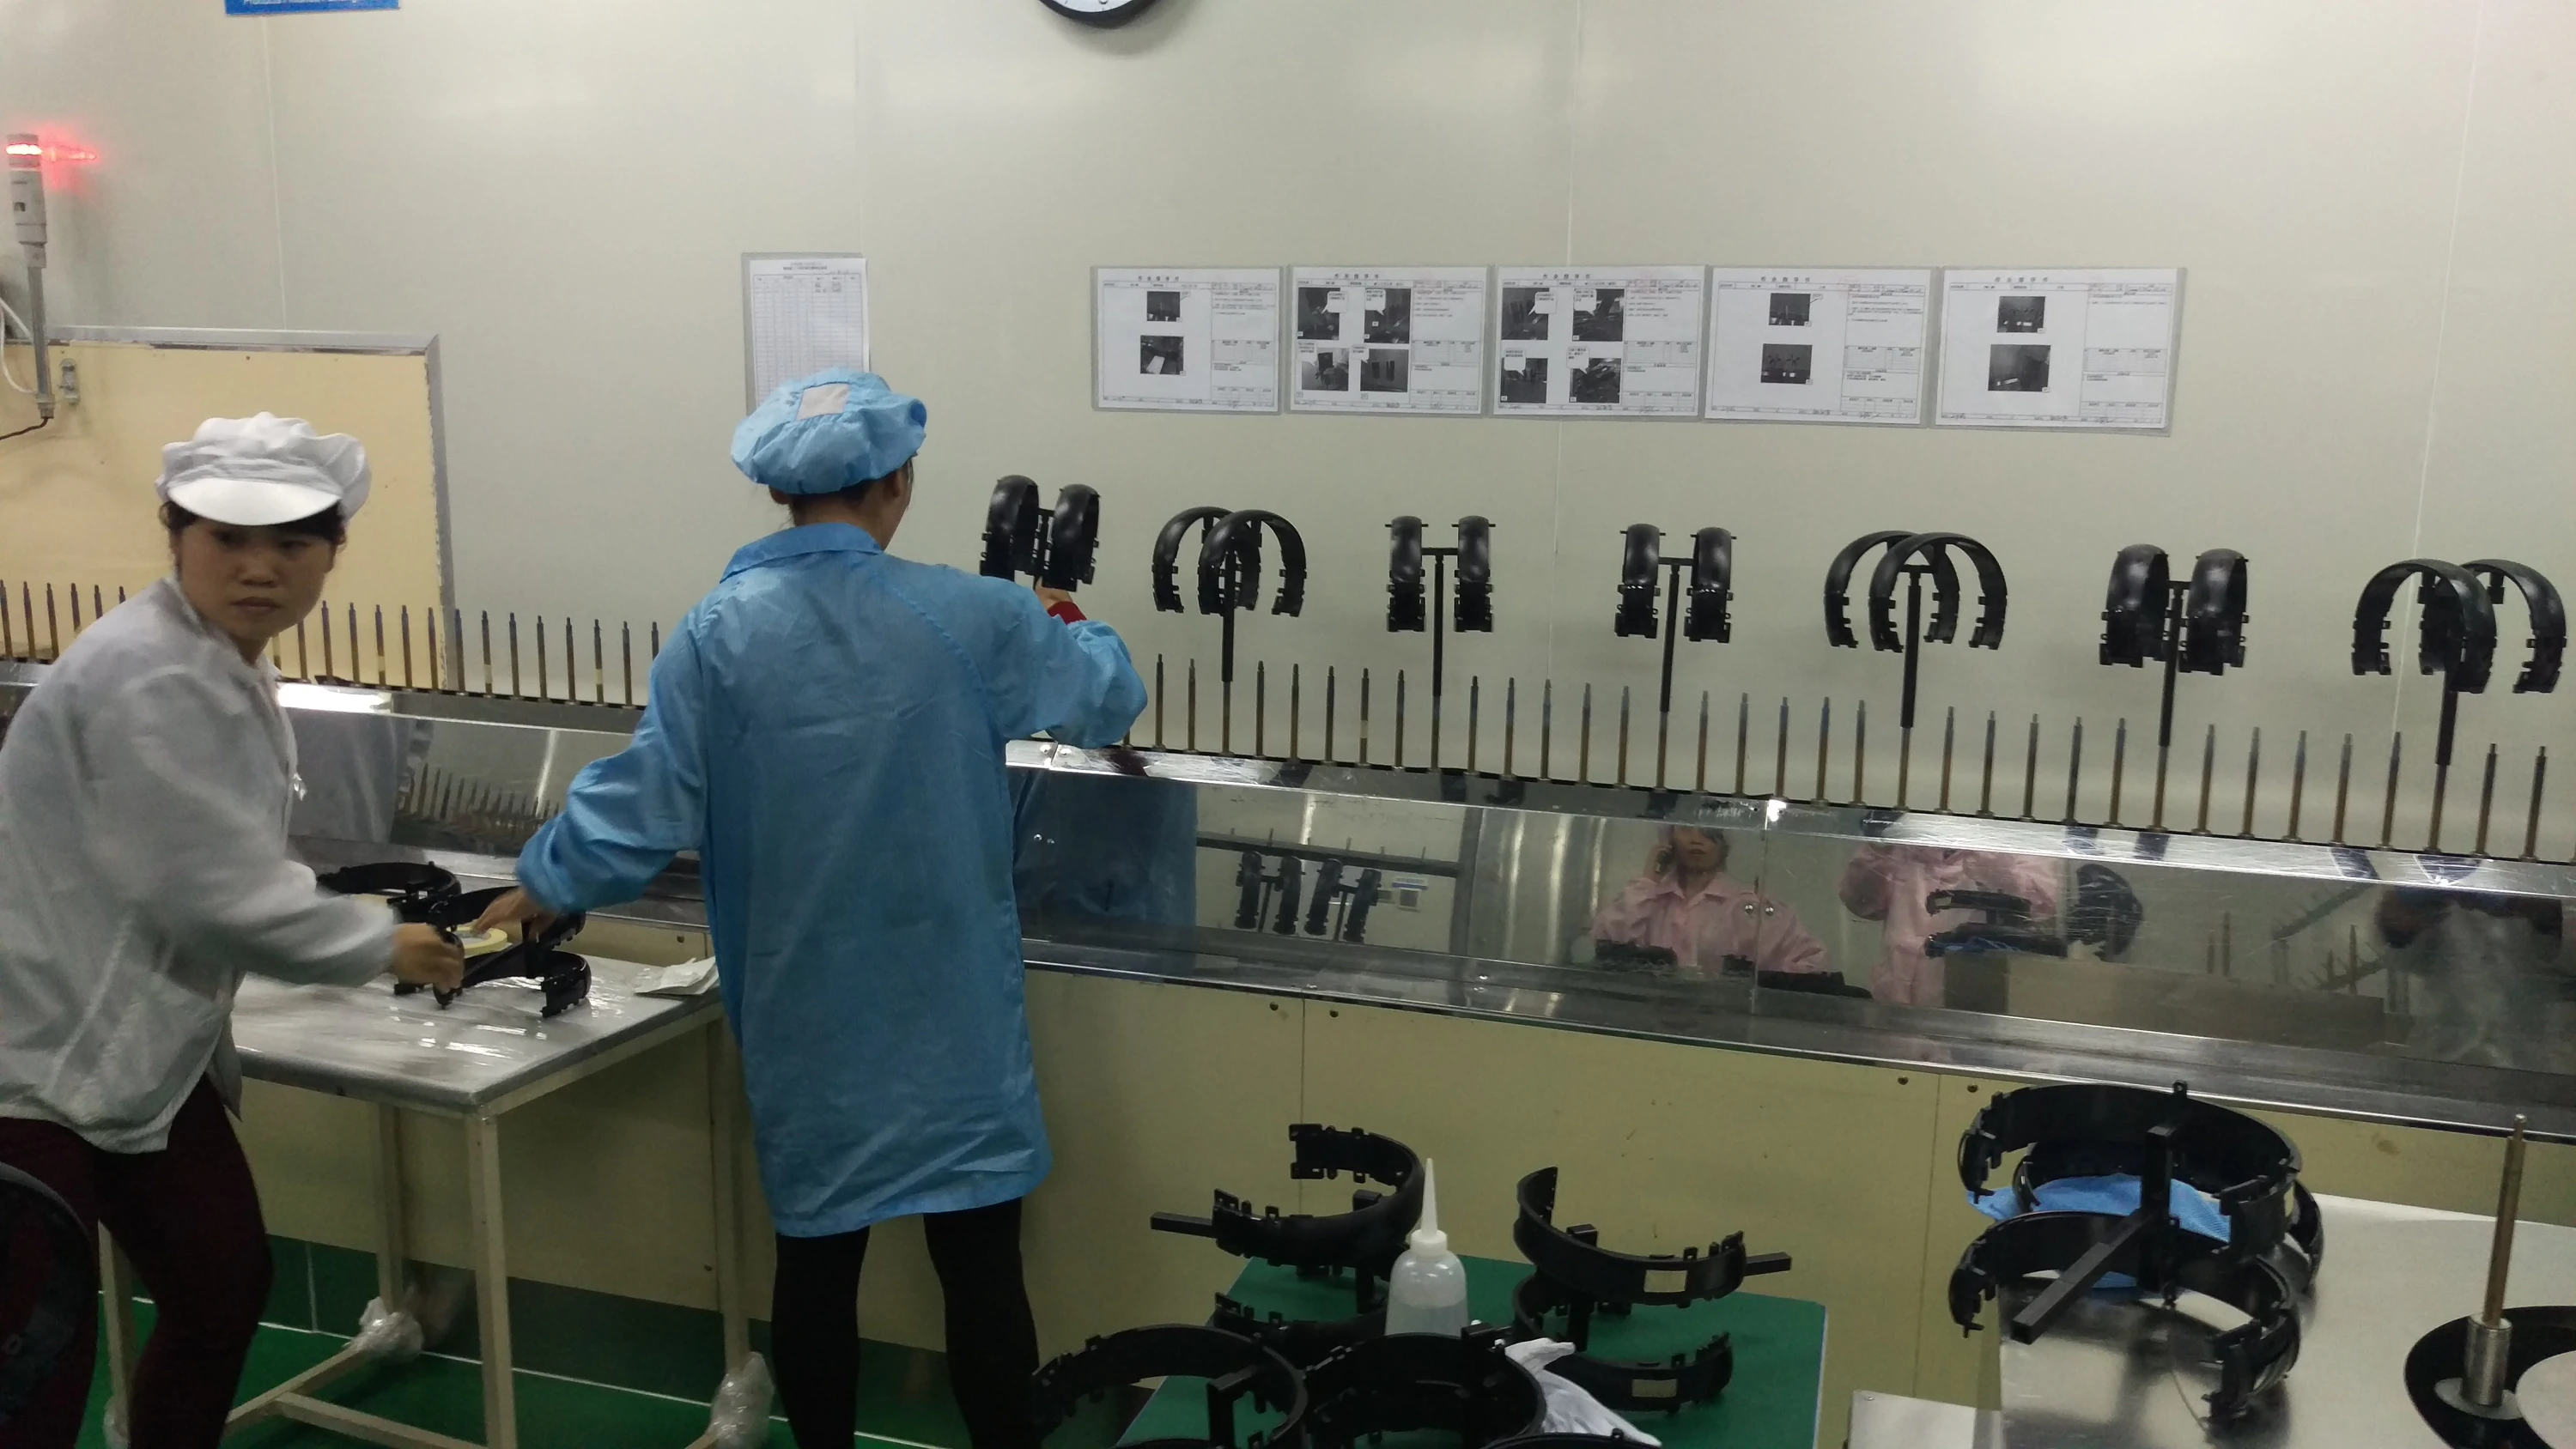
I created Glyph's master color plan (795-0001) and graphic plan (795-1000). These defined the color, material, finish and graphics requirements across the mechanical BOM, linking the parts to material and coating specifications, color-chip references and inspection procedures. Glyph's look was already established; carrying it across different parts, materials and coatings took judgment.
The specifications I created were a necessary line of defense across the vendors in our distributed supply chain. CMF, graphics, gap and individual-part specifications worked together, and the part drawings referenced the cosmetic specification. They gave me a defined requirement to return to when discussing a part, an interface or a finish with its supplier.
I used measurements wherever possible, and always my own eye. Perfect color matching across all those adjacent surfaces wasn't realistic. The CMF and graphics plan helped me navigate the compromises and define acceptable bands for production cosmetics.
 From the workbench
Carrying the finish across suppliers
Follow the specification links, molded masks and finishing line, then inspect a difficult color match.
Explore investigation +Close investigation −
Carrying the finish across suppliers
Follow the specification links, molded masks and finishing line, then inspect a difficult color match.
Explore investigation +Close investigation −Connecting the specifications
The documents addressed different parts of the same product:
- CMF: material, coating and finish requirements, with color-chip references for the parts.
- Graphics: artwork and its application, linked to the part, process, material, color and inspection procedure.
- Gap: target and allowable gaps at assembled interfaces.
- Individual-part specifications: inspection procedures and acceptance/rejection criteria for critical parts, including the headband, liners, ear covers, shutters and faceplate.
- Cosmetic specification: the common requirements referenced by part drawings. Individual part-level specifications could supersede the general requirements.
That connected appearance to the part and the assembly. The inspection fixtures and gap plan described earlier supported the same work: defining what we were asking suppliers to make and how we would judge what arrived.
Making the masks fit the parts
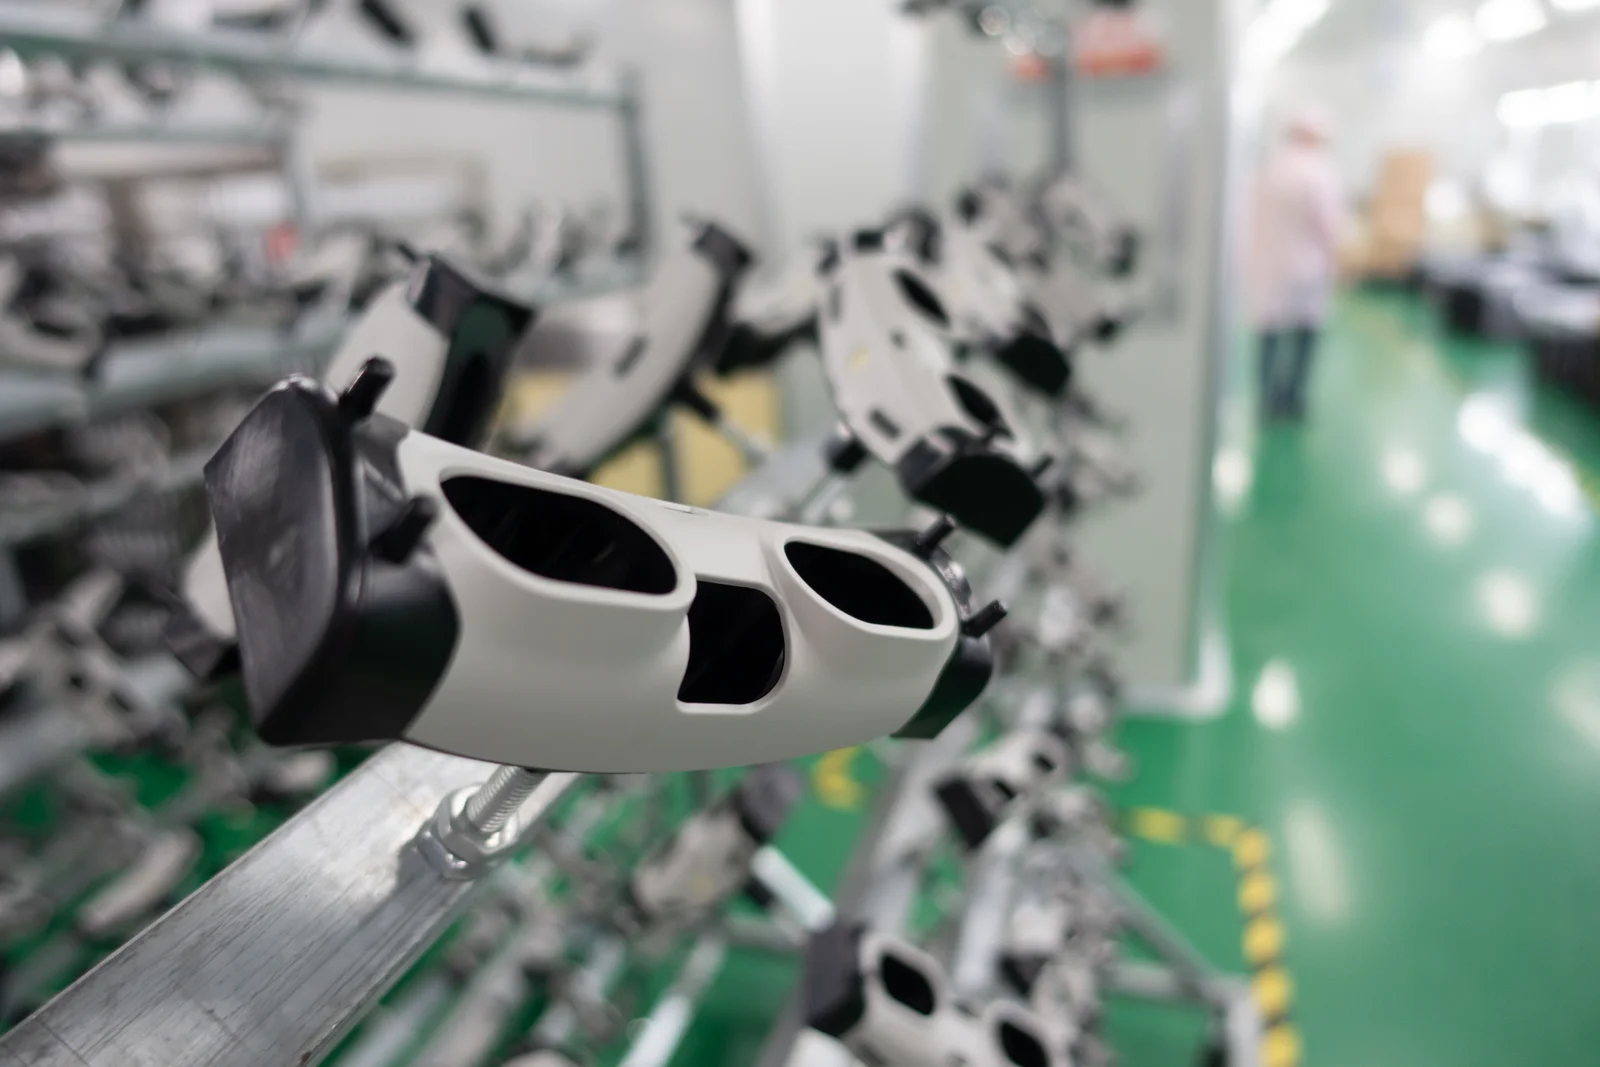
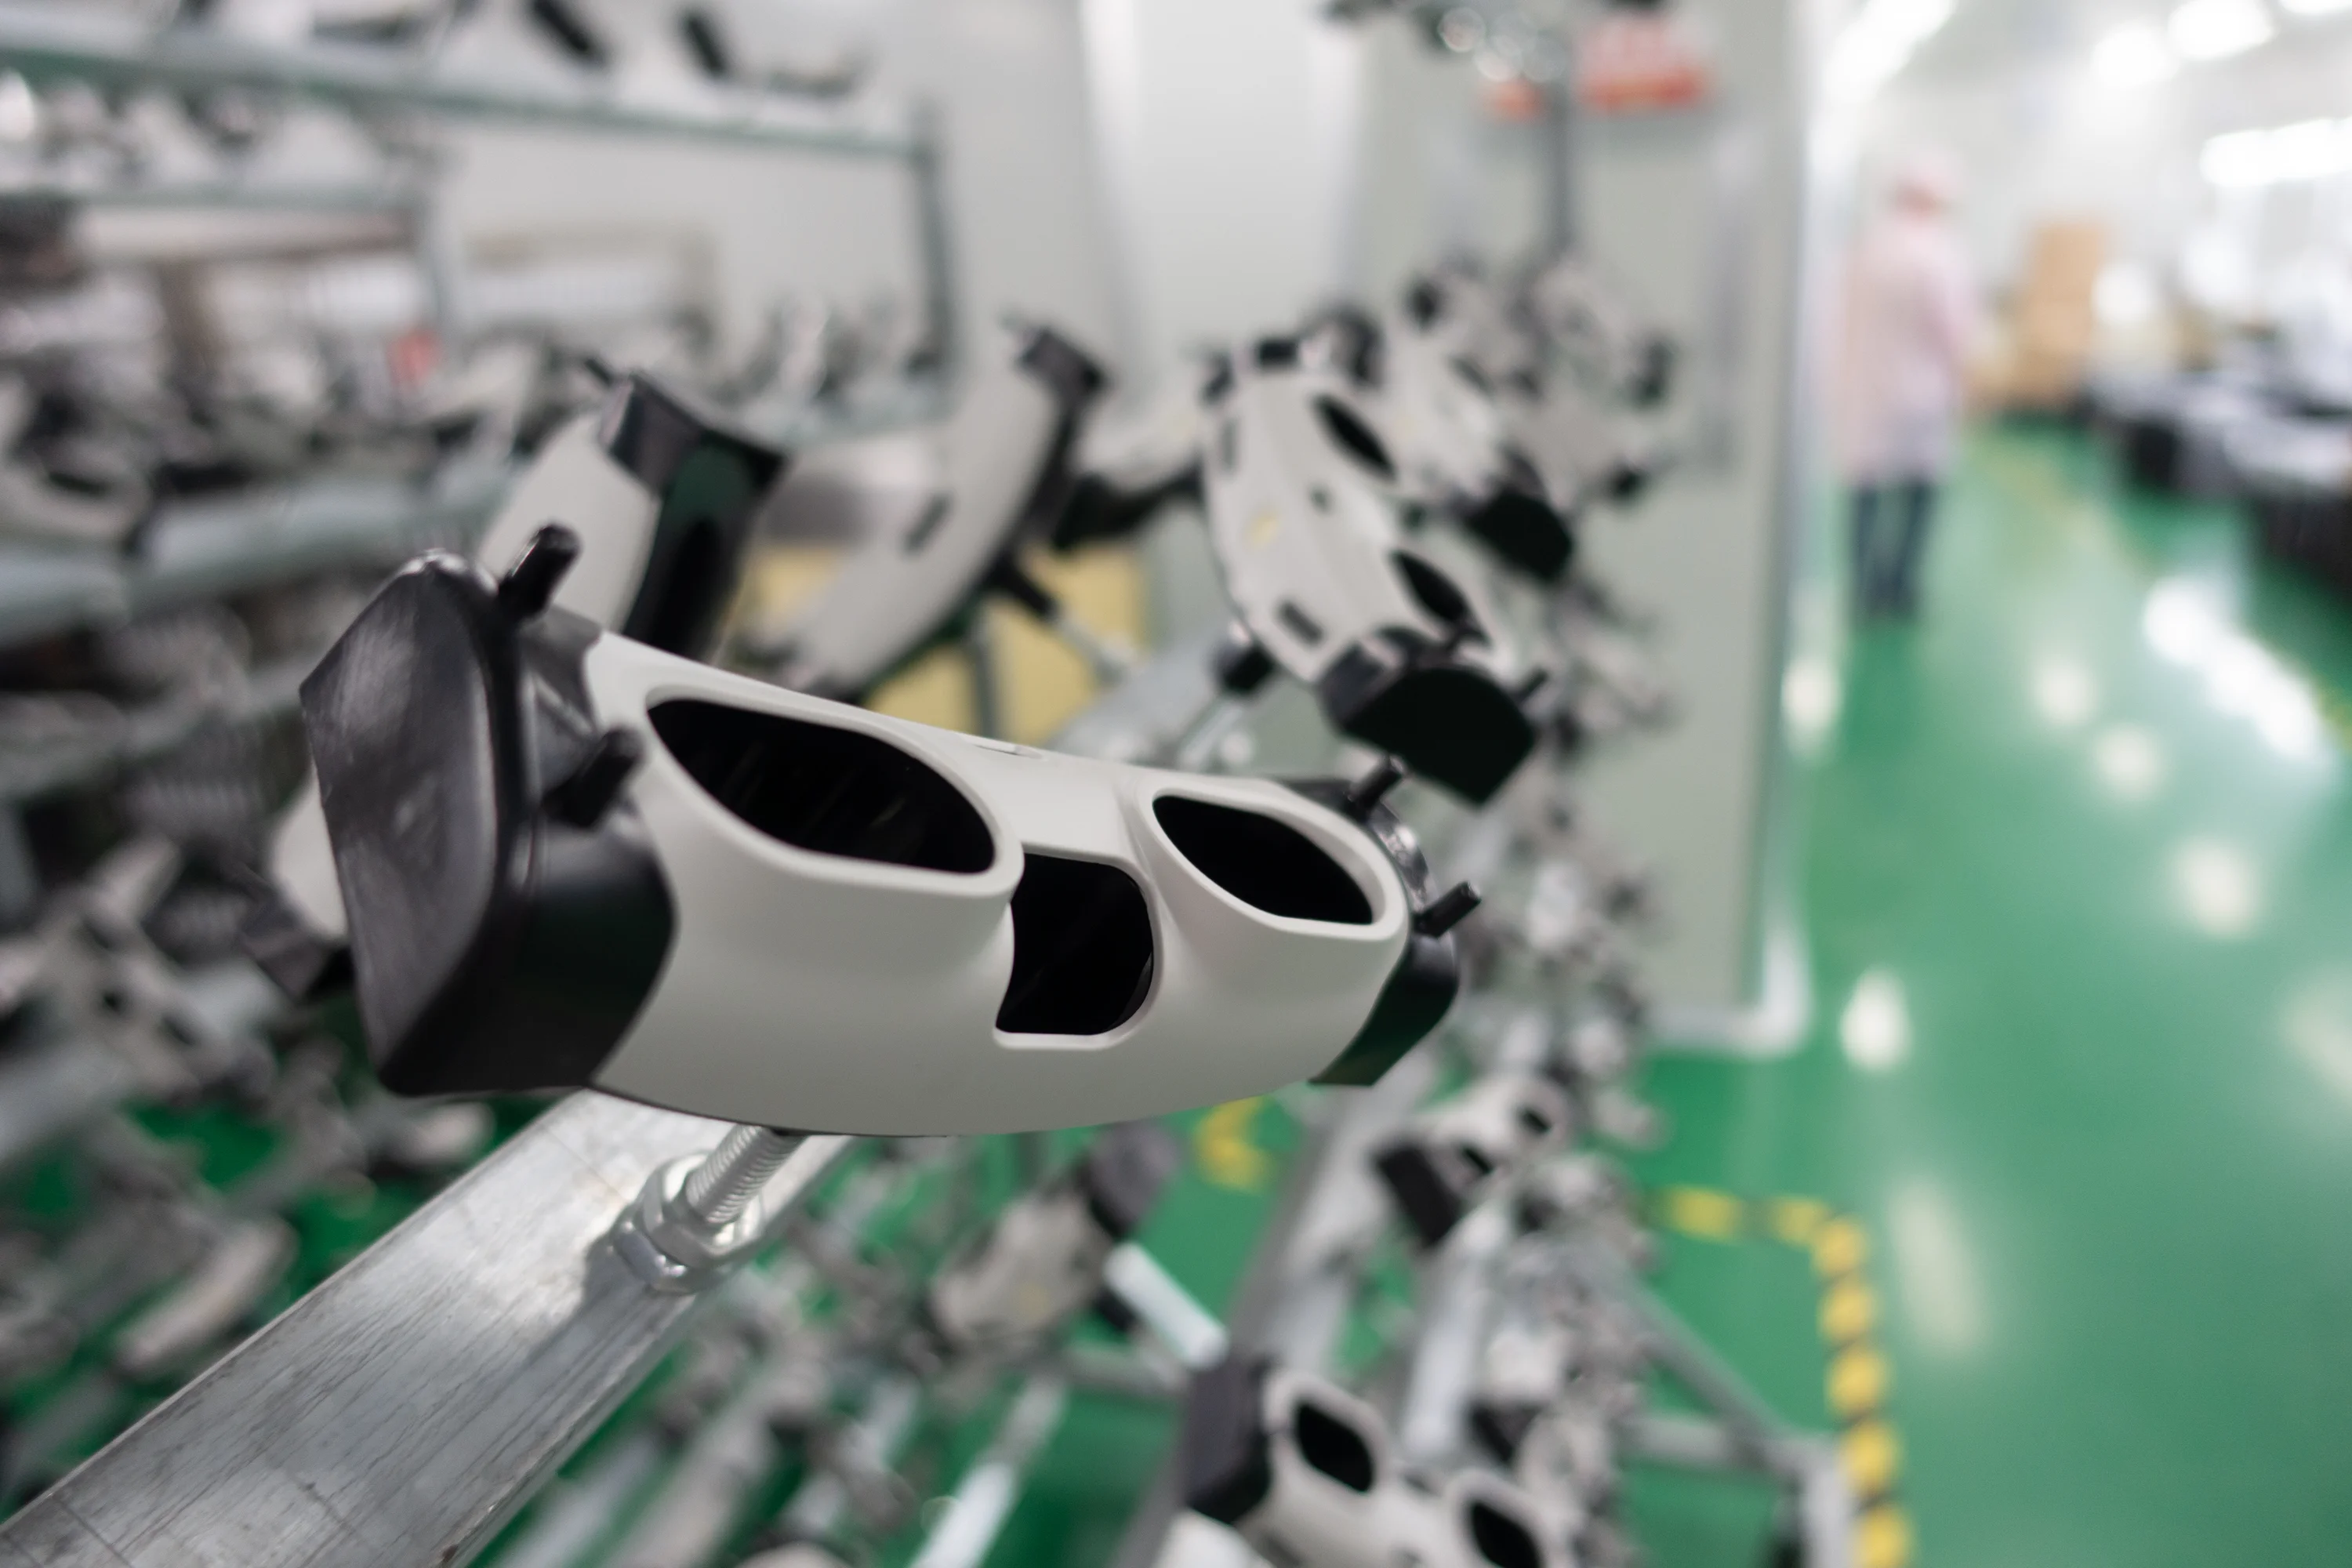
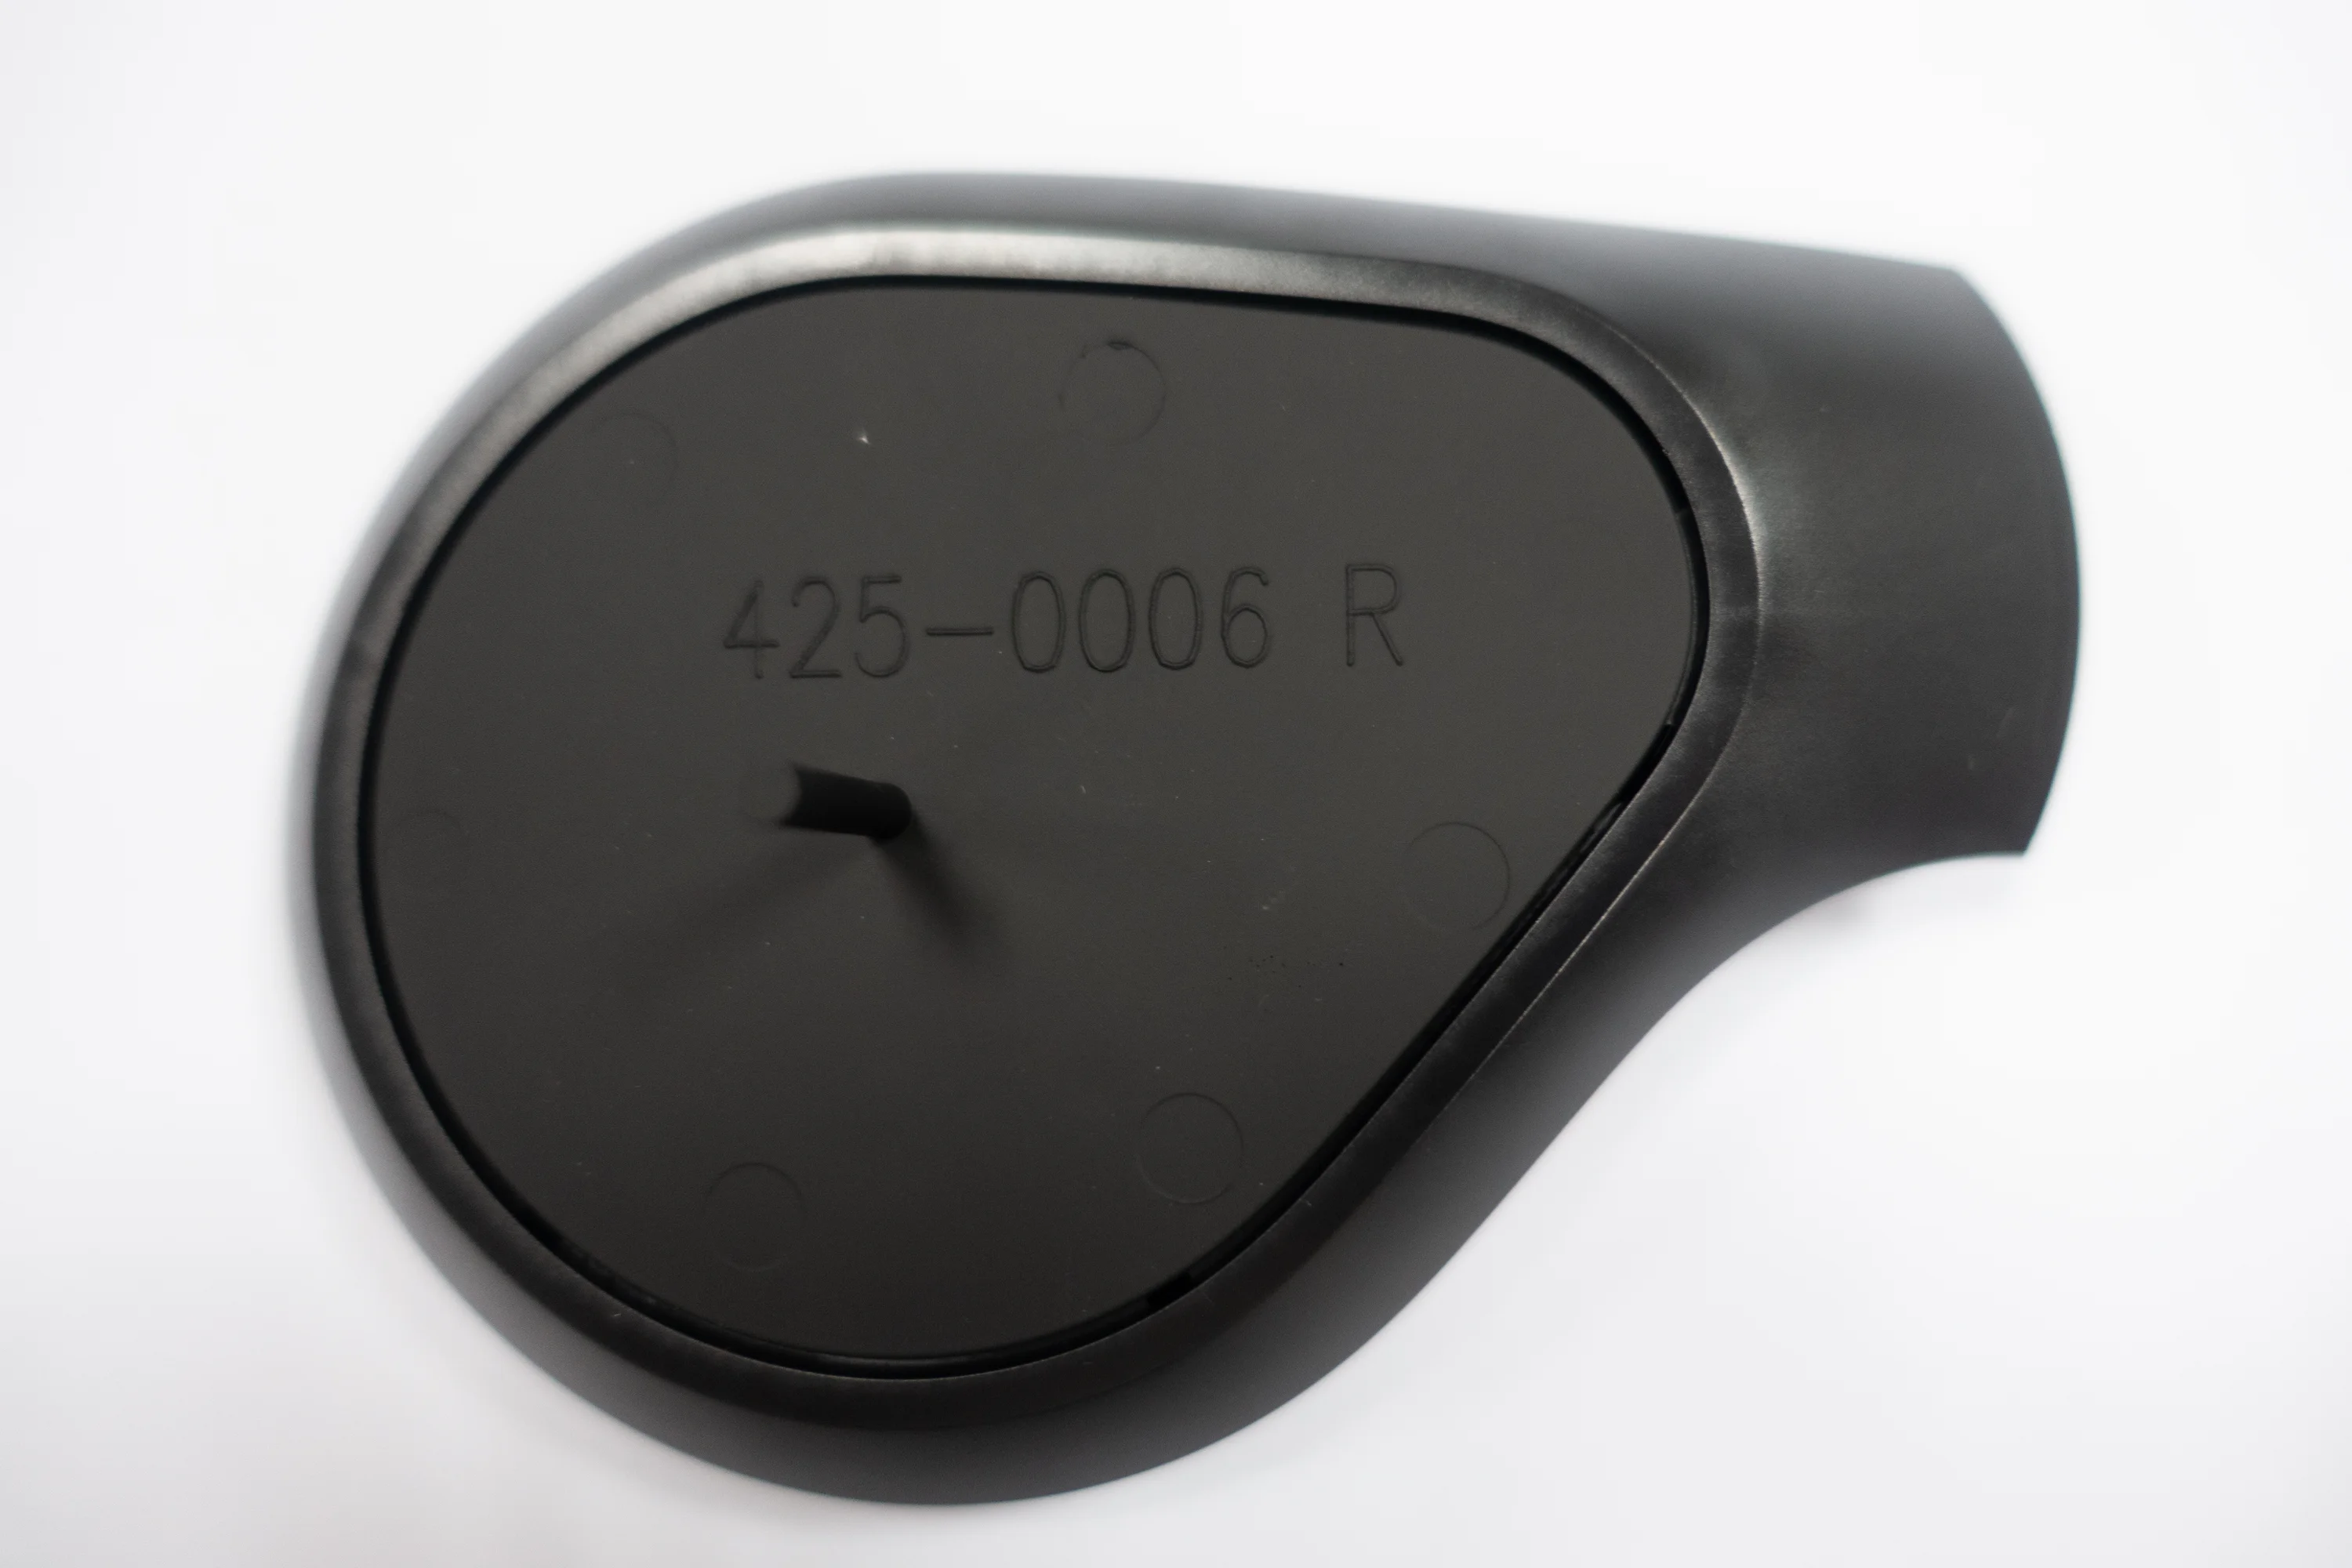
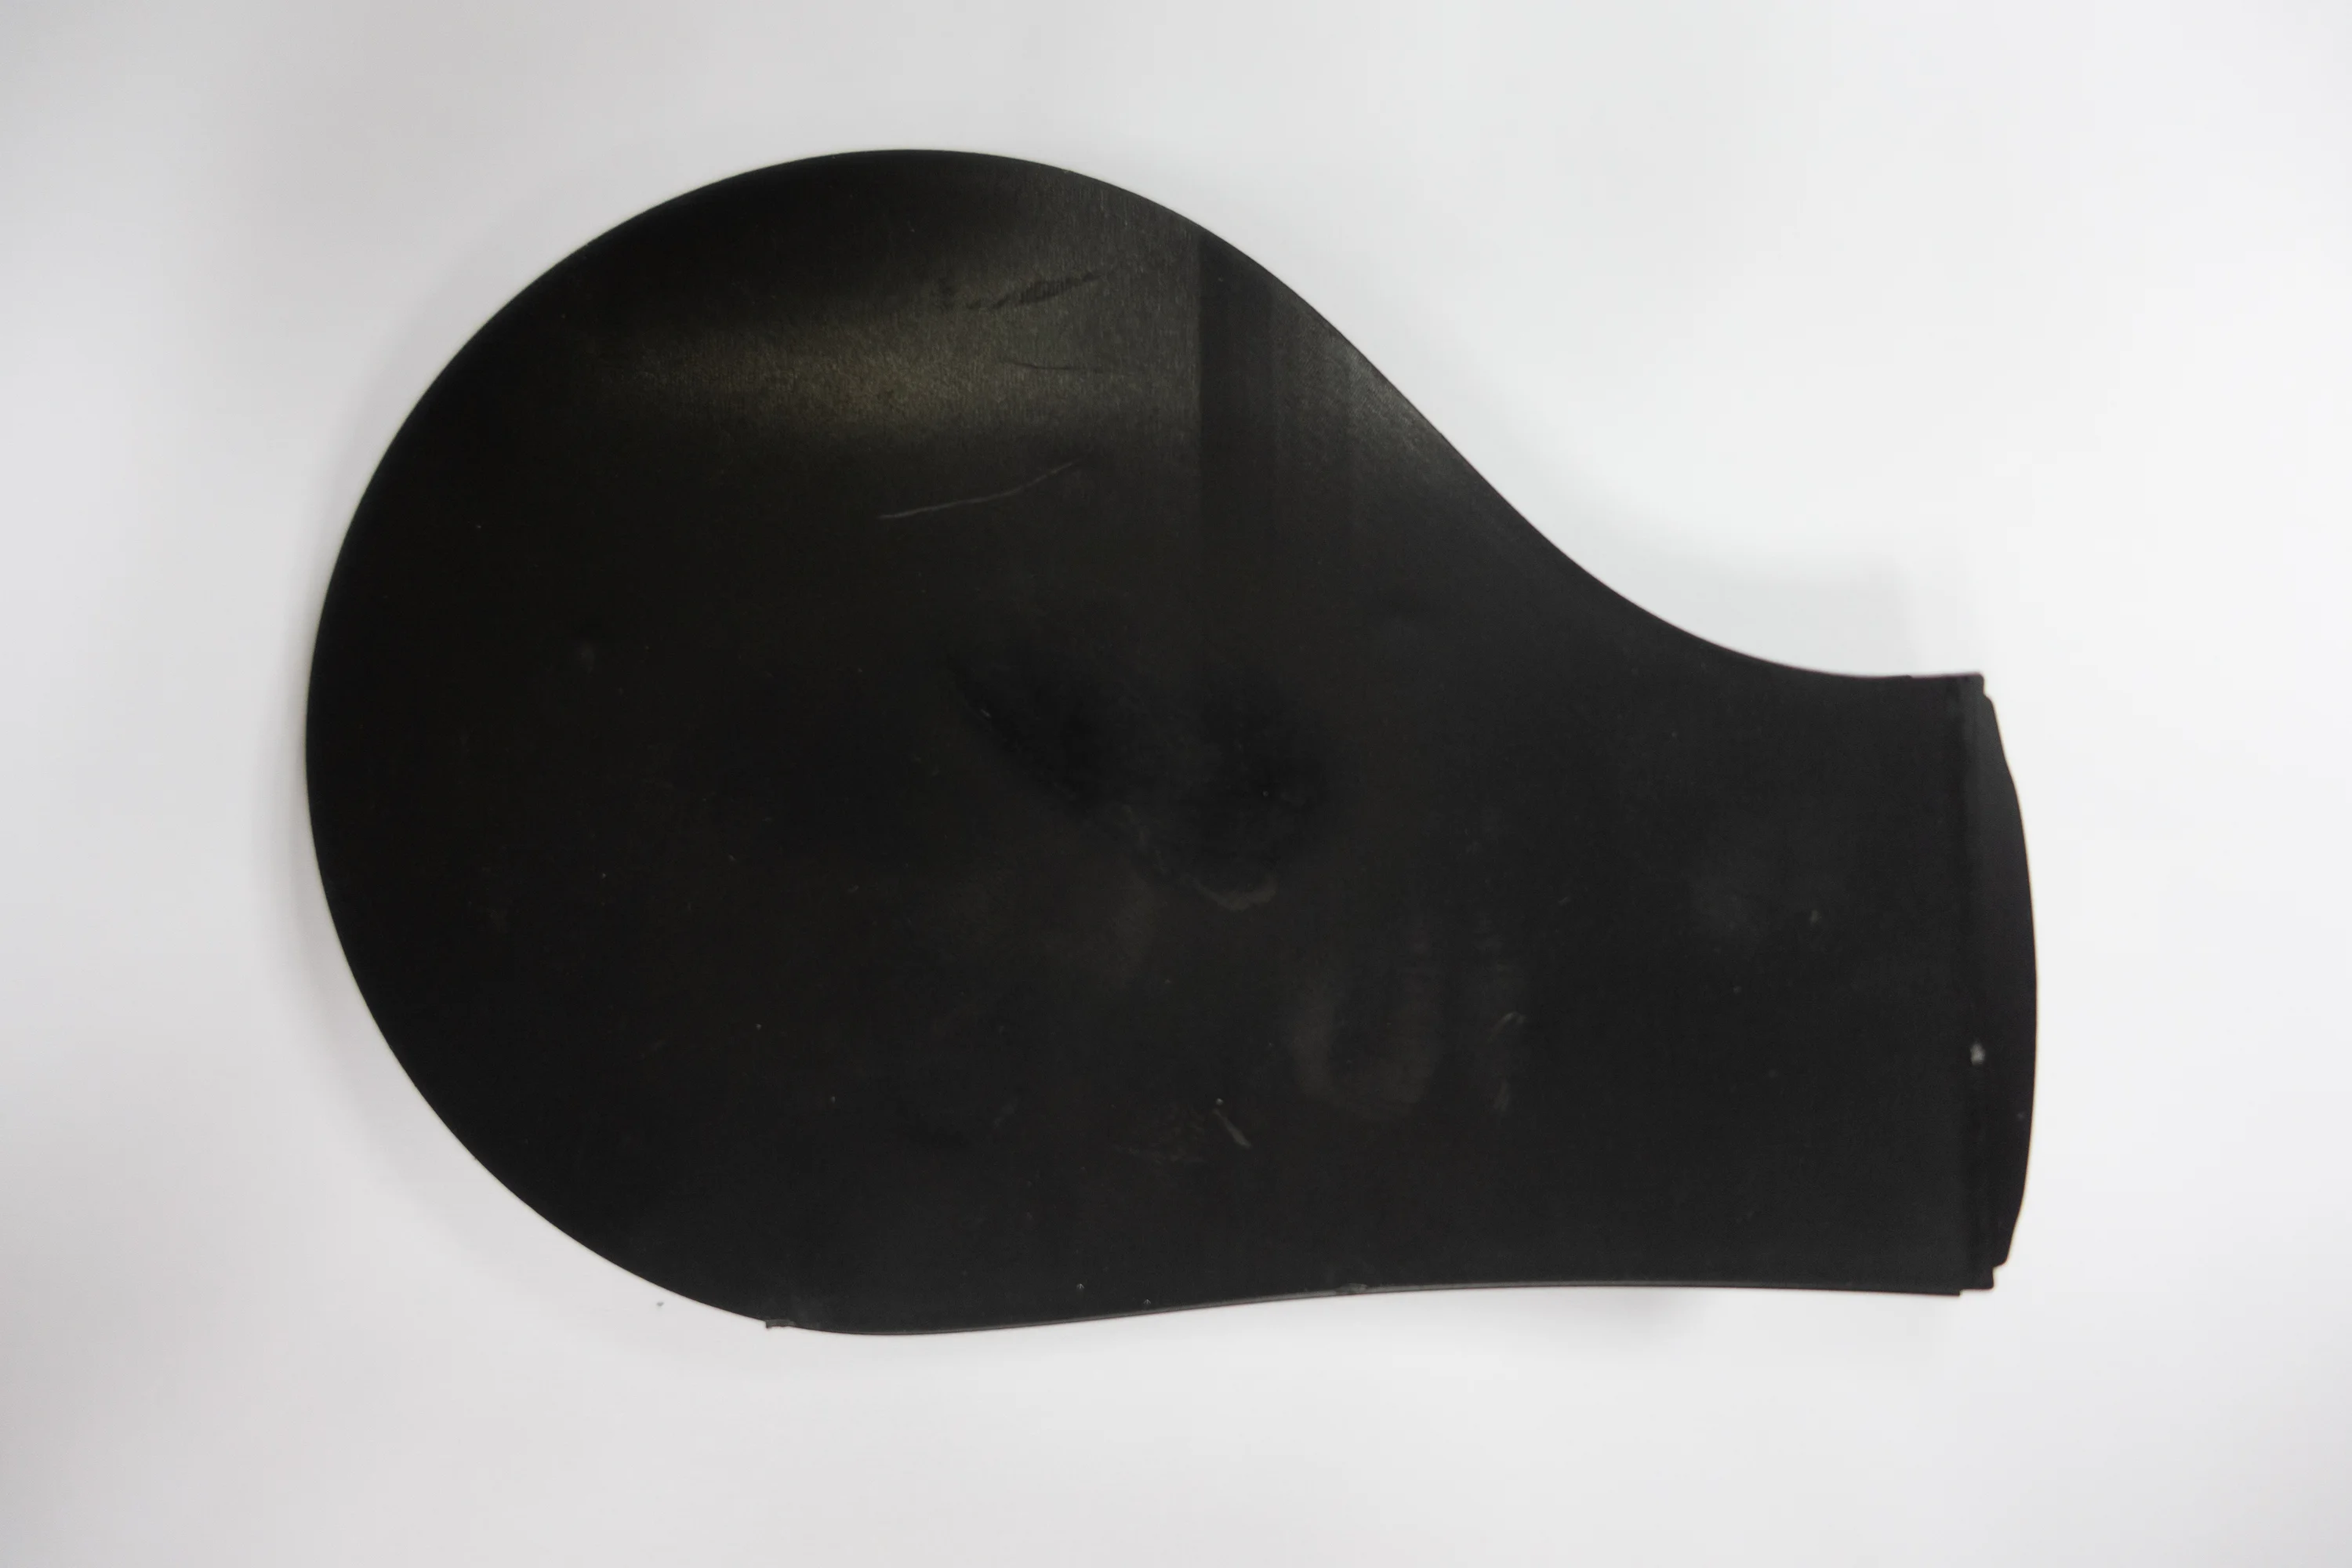
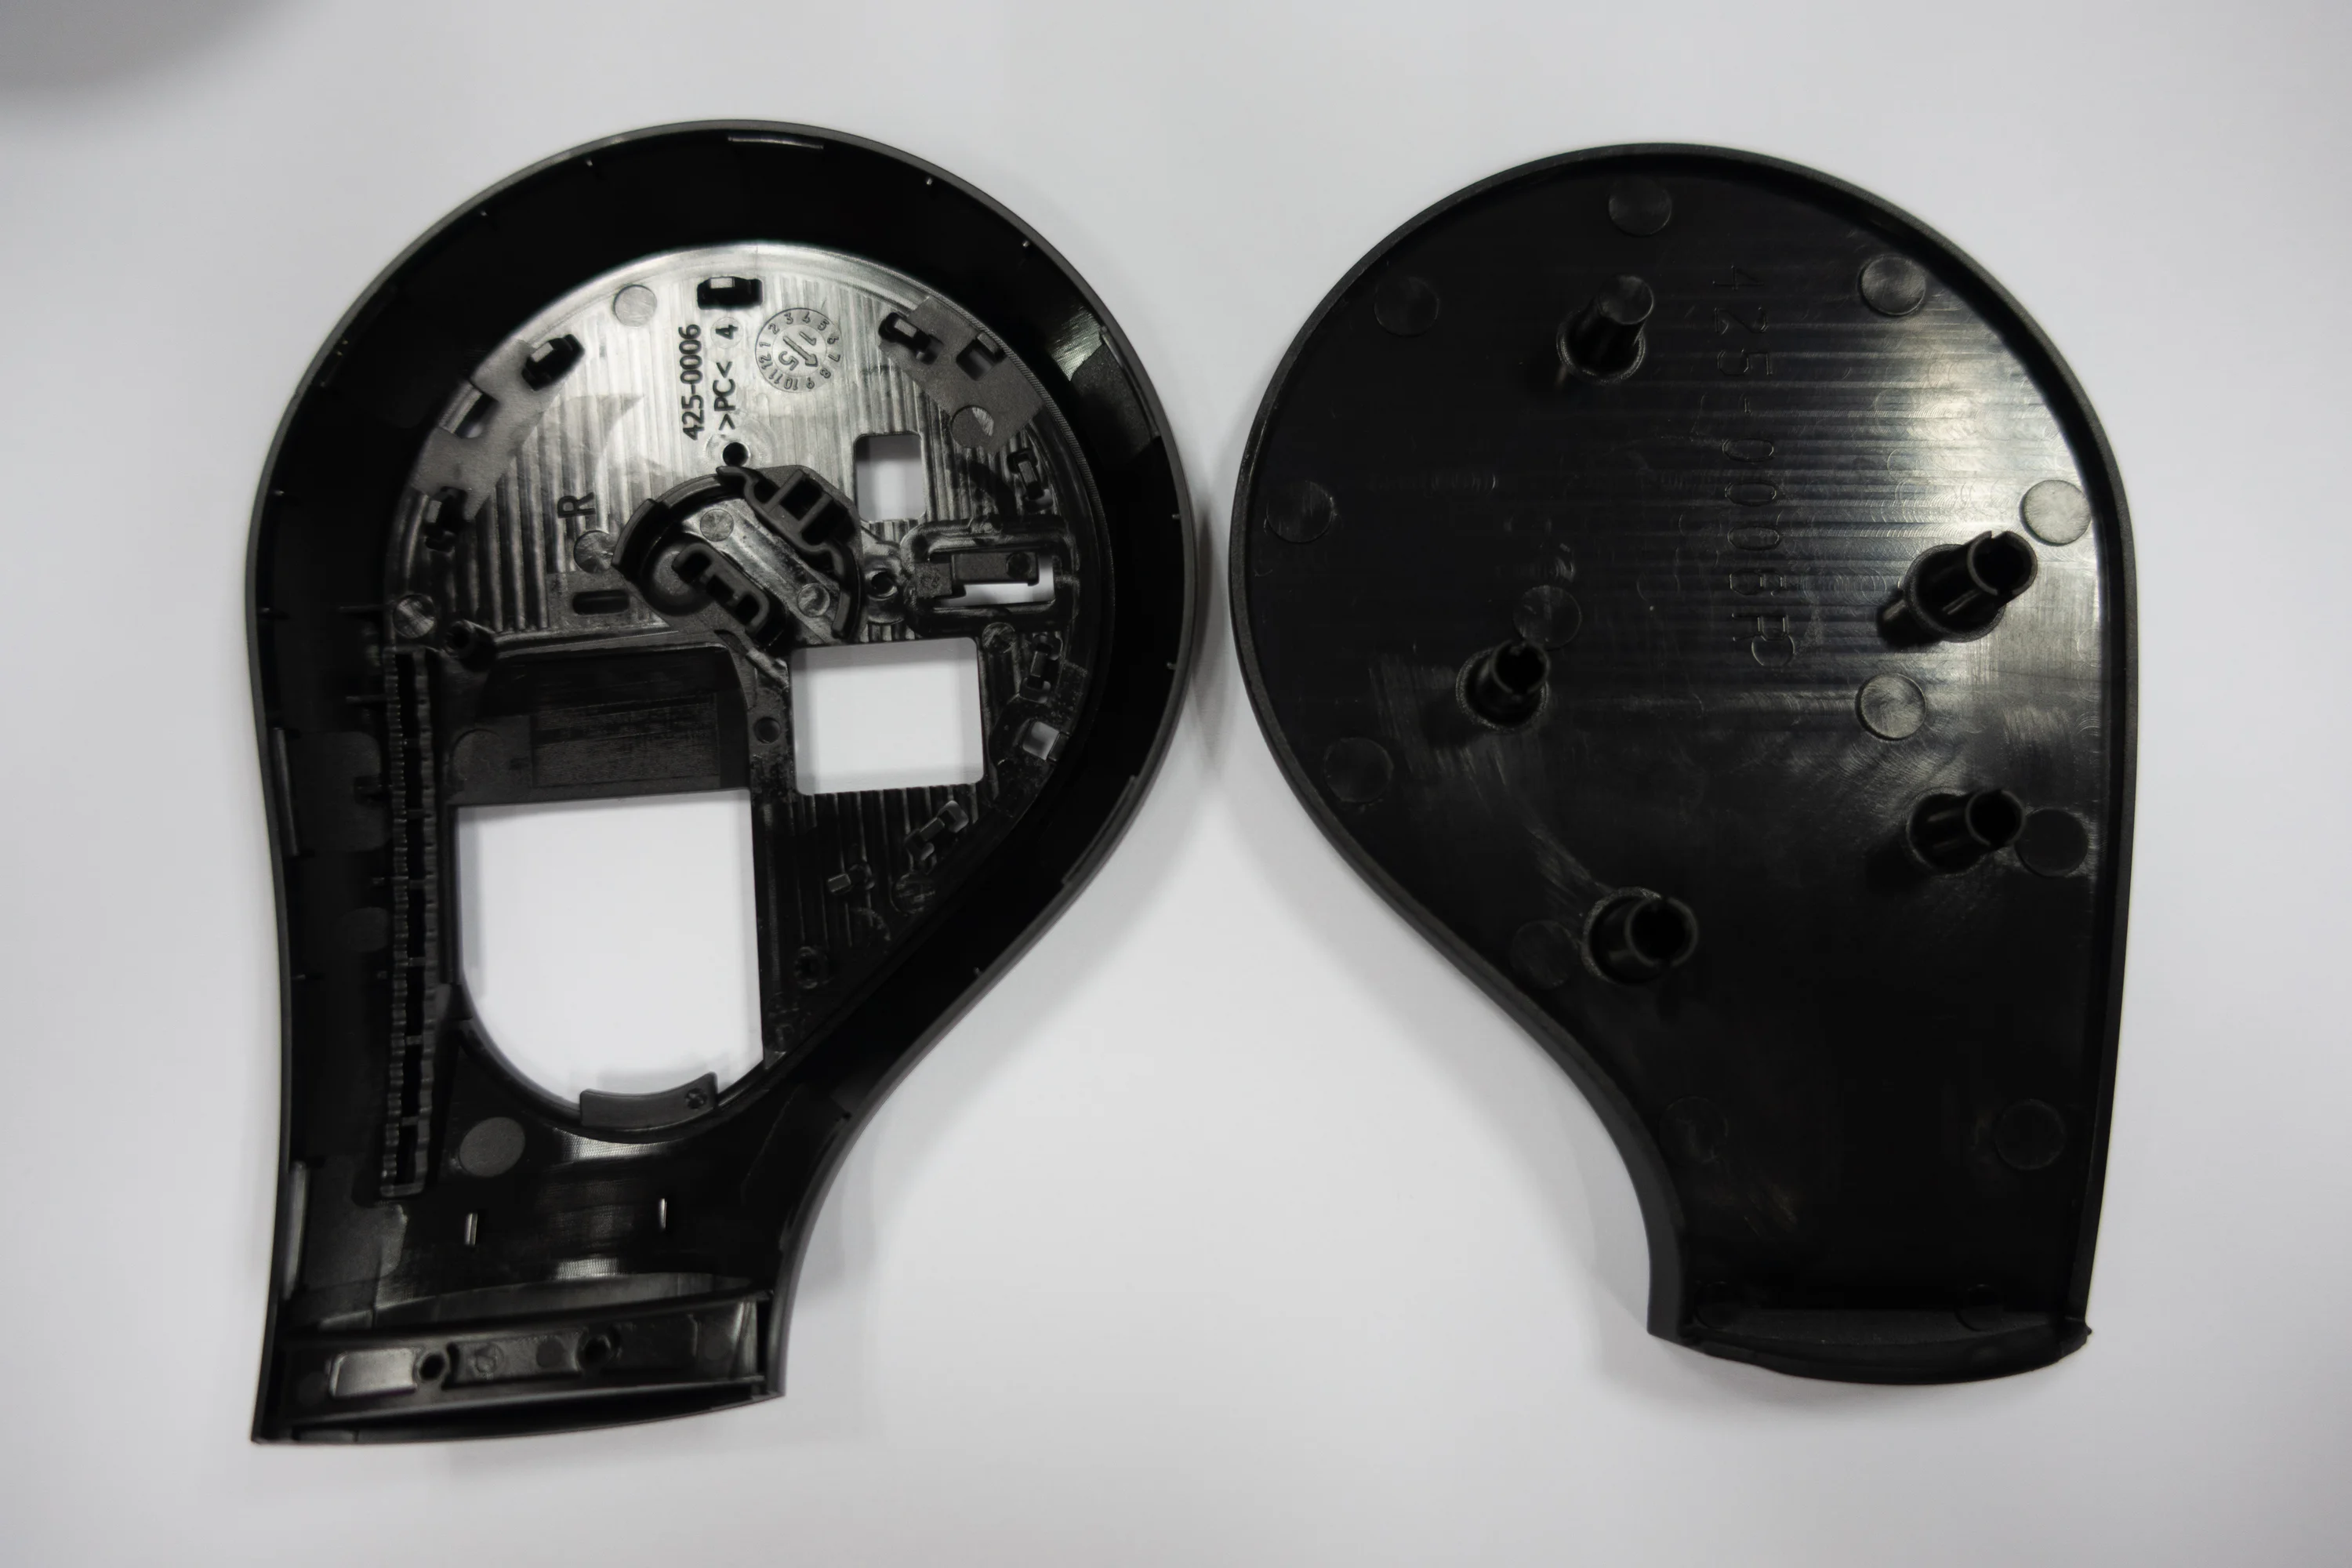
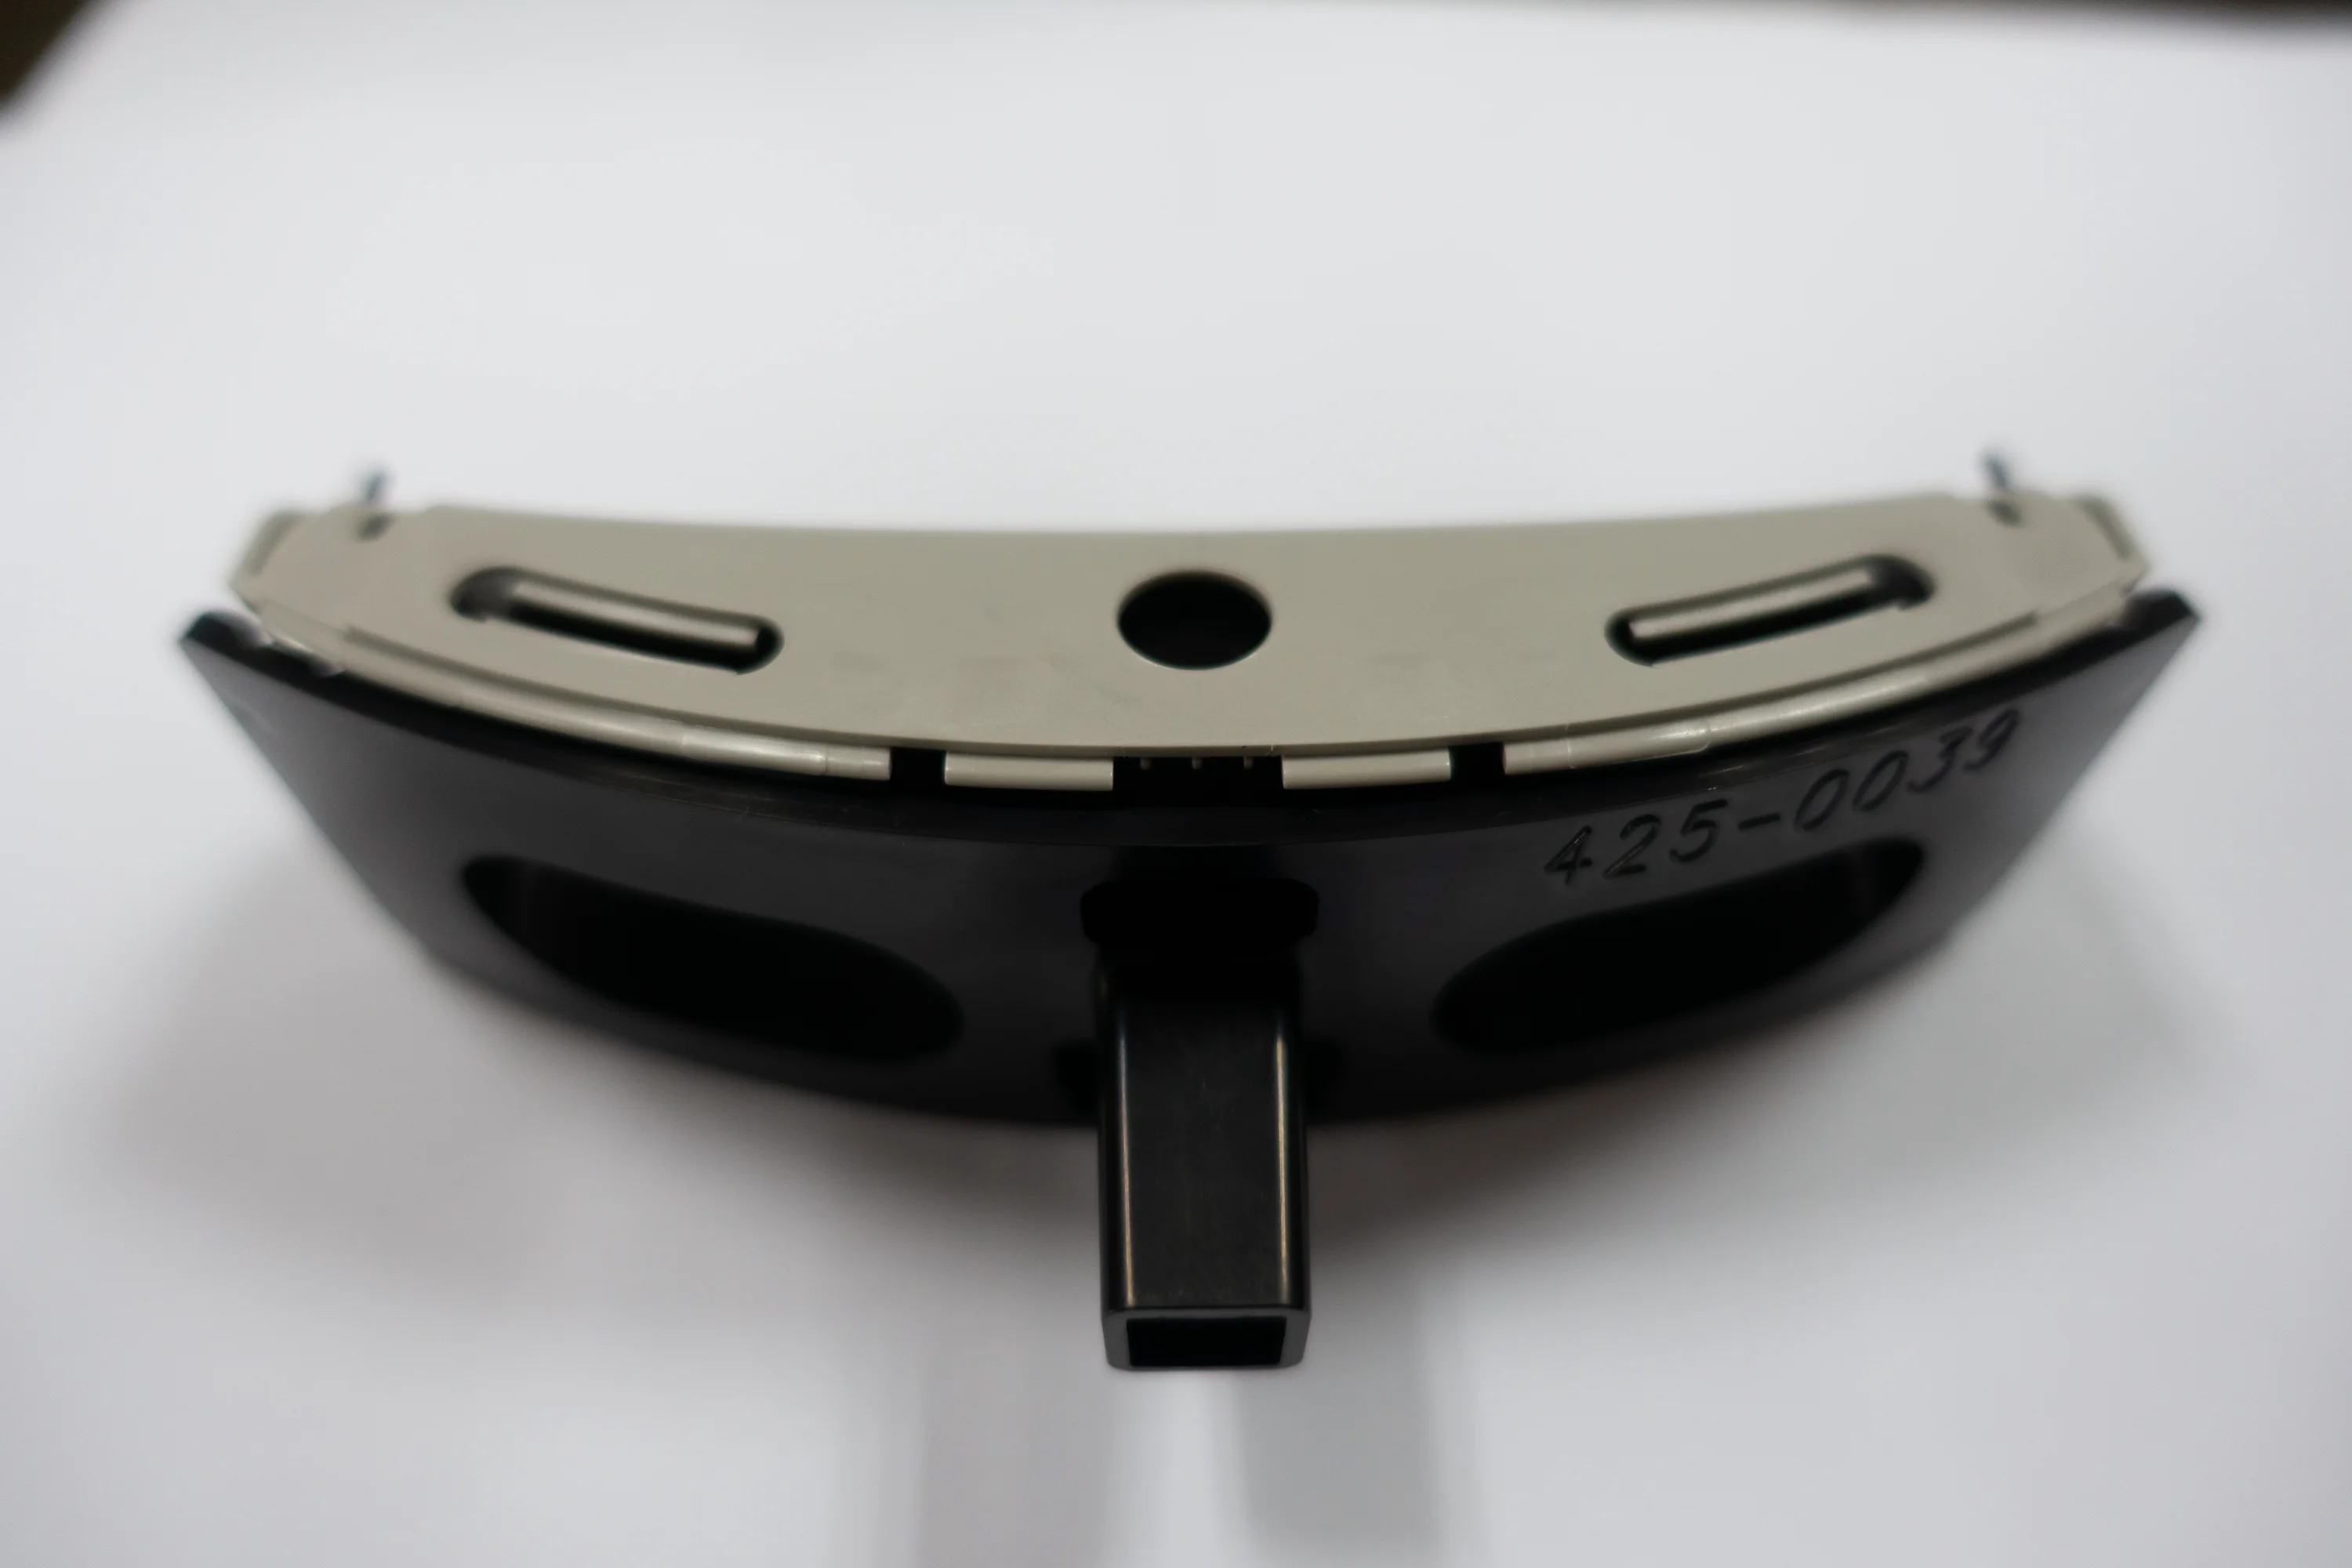
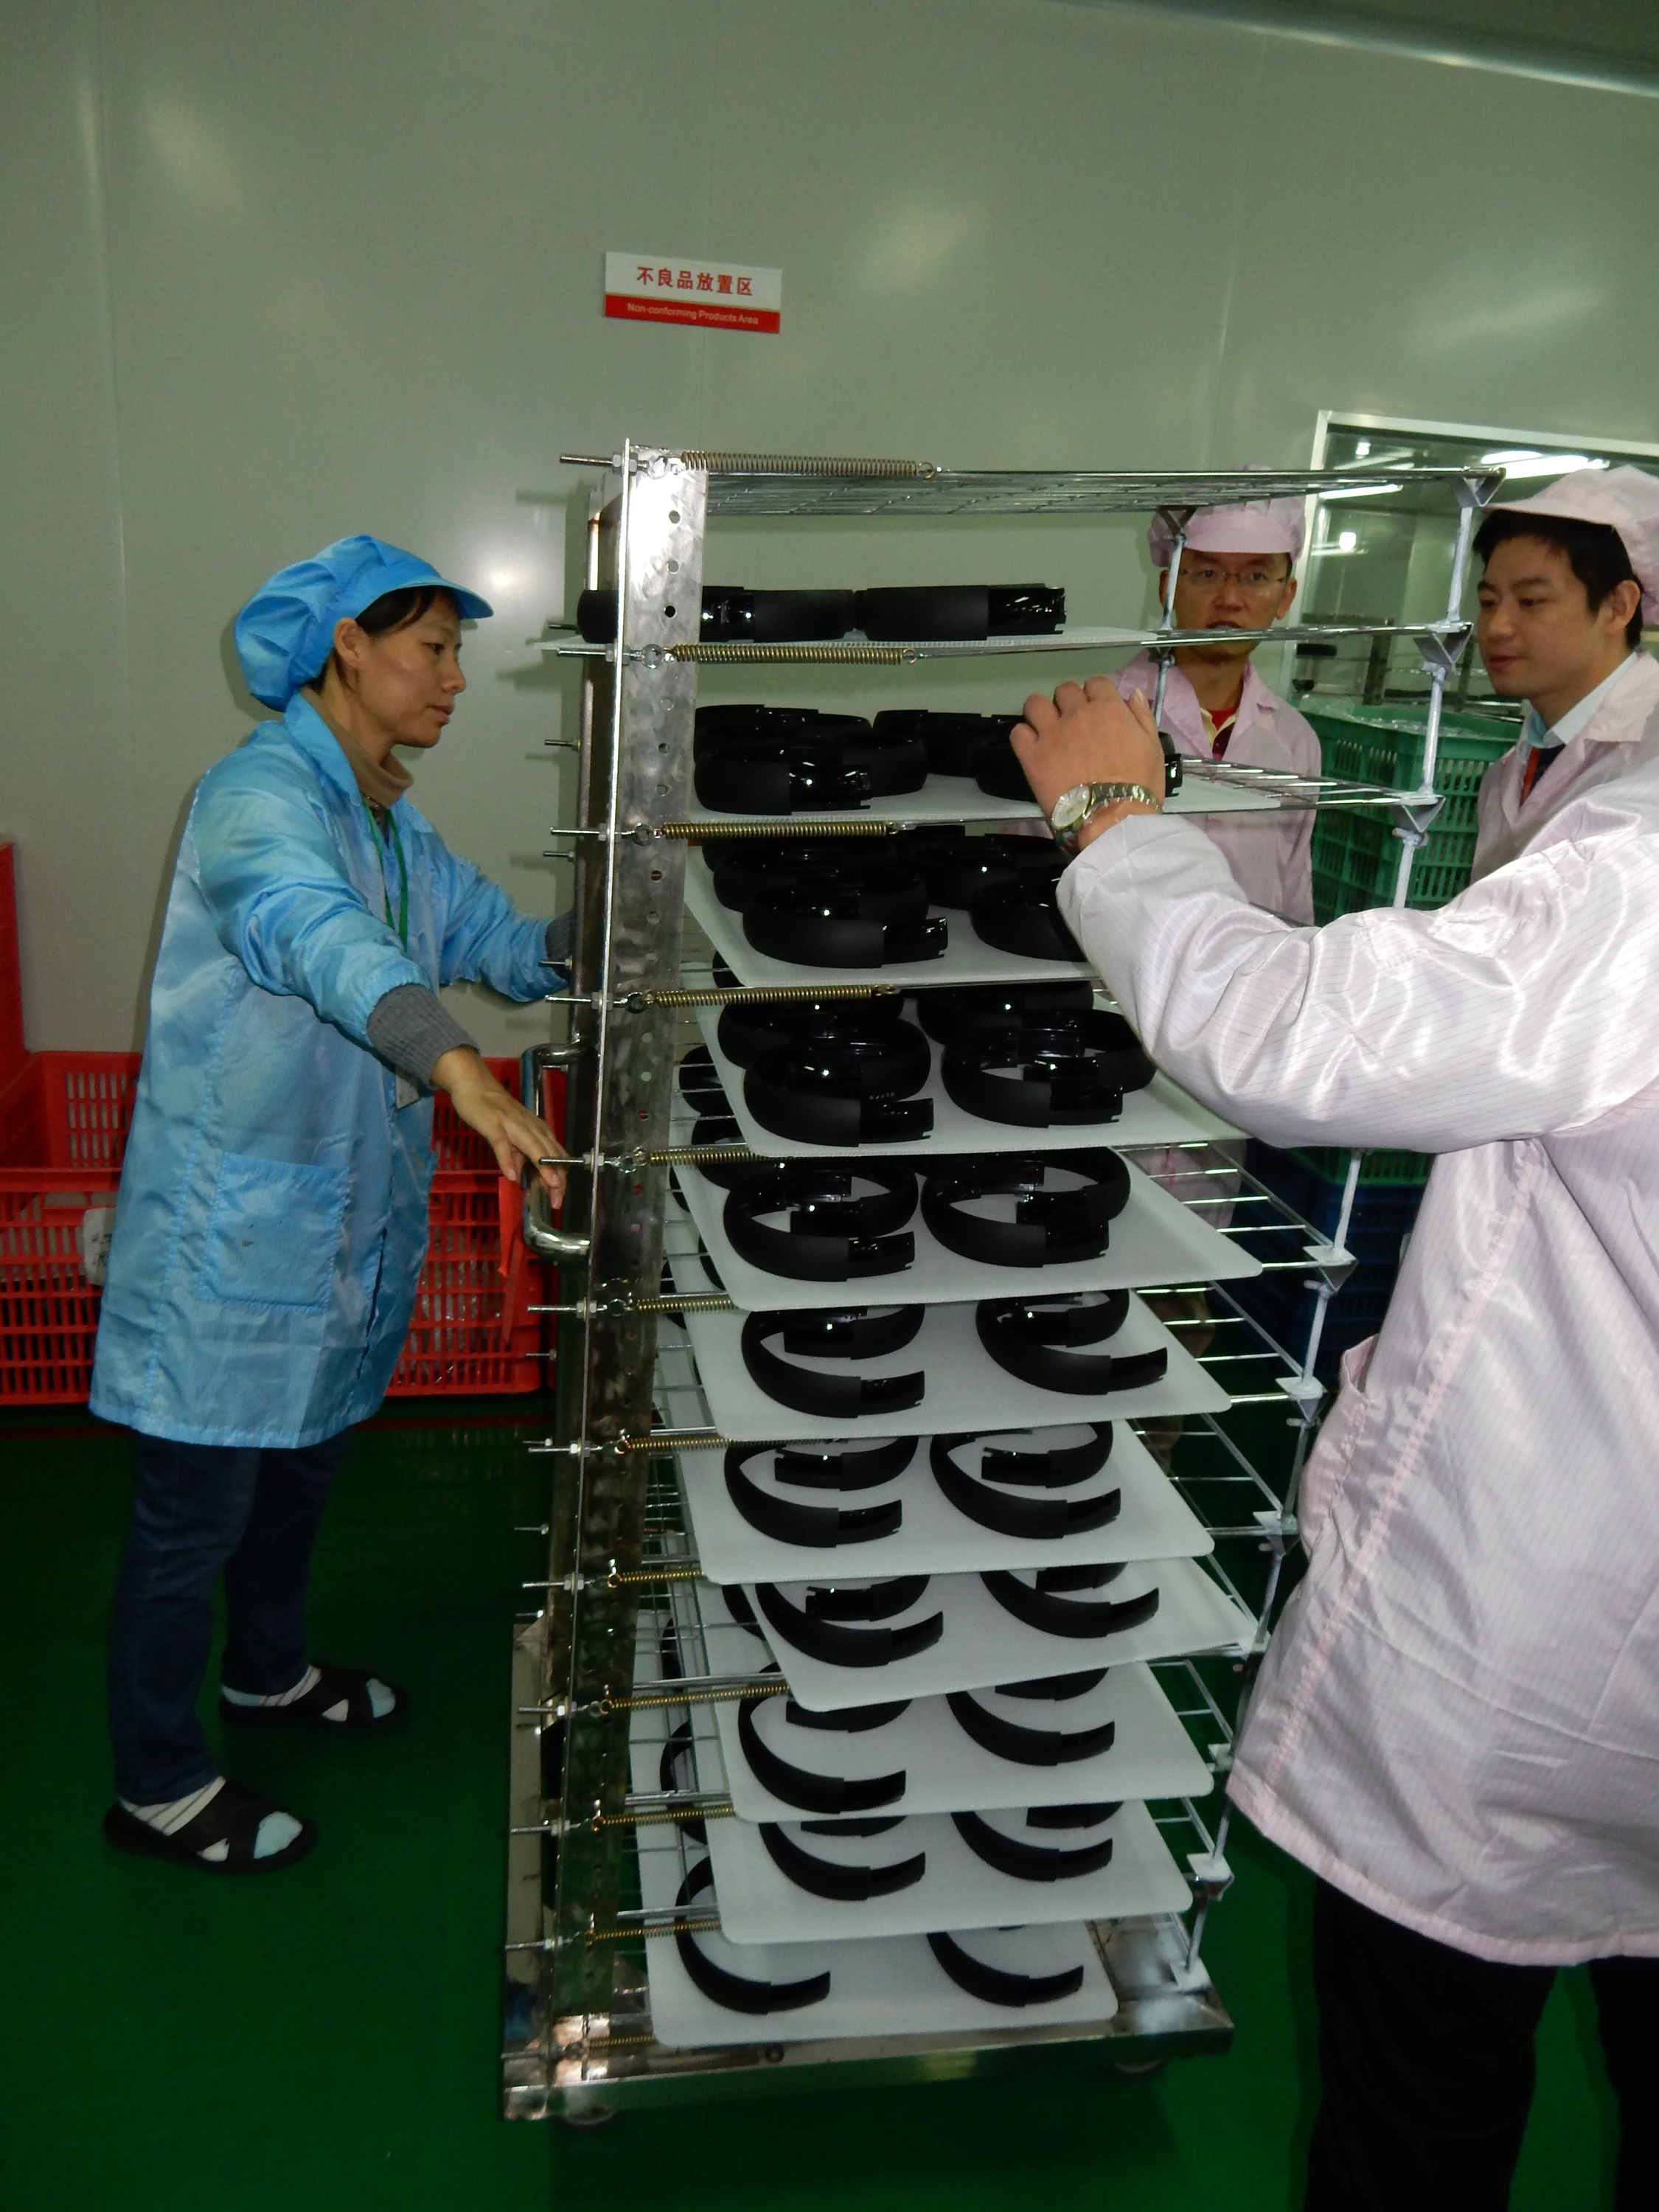
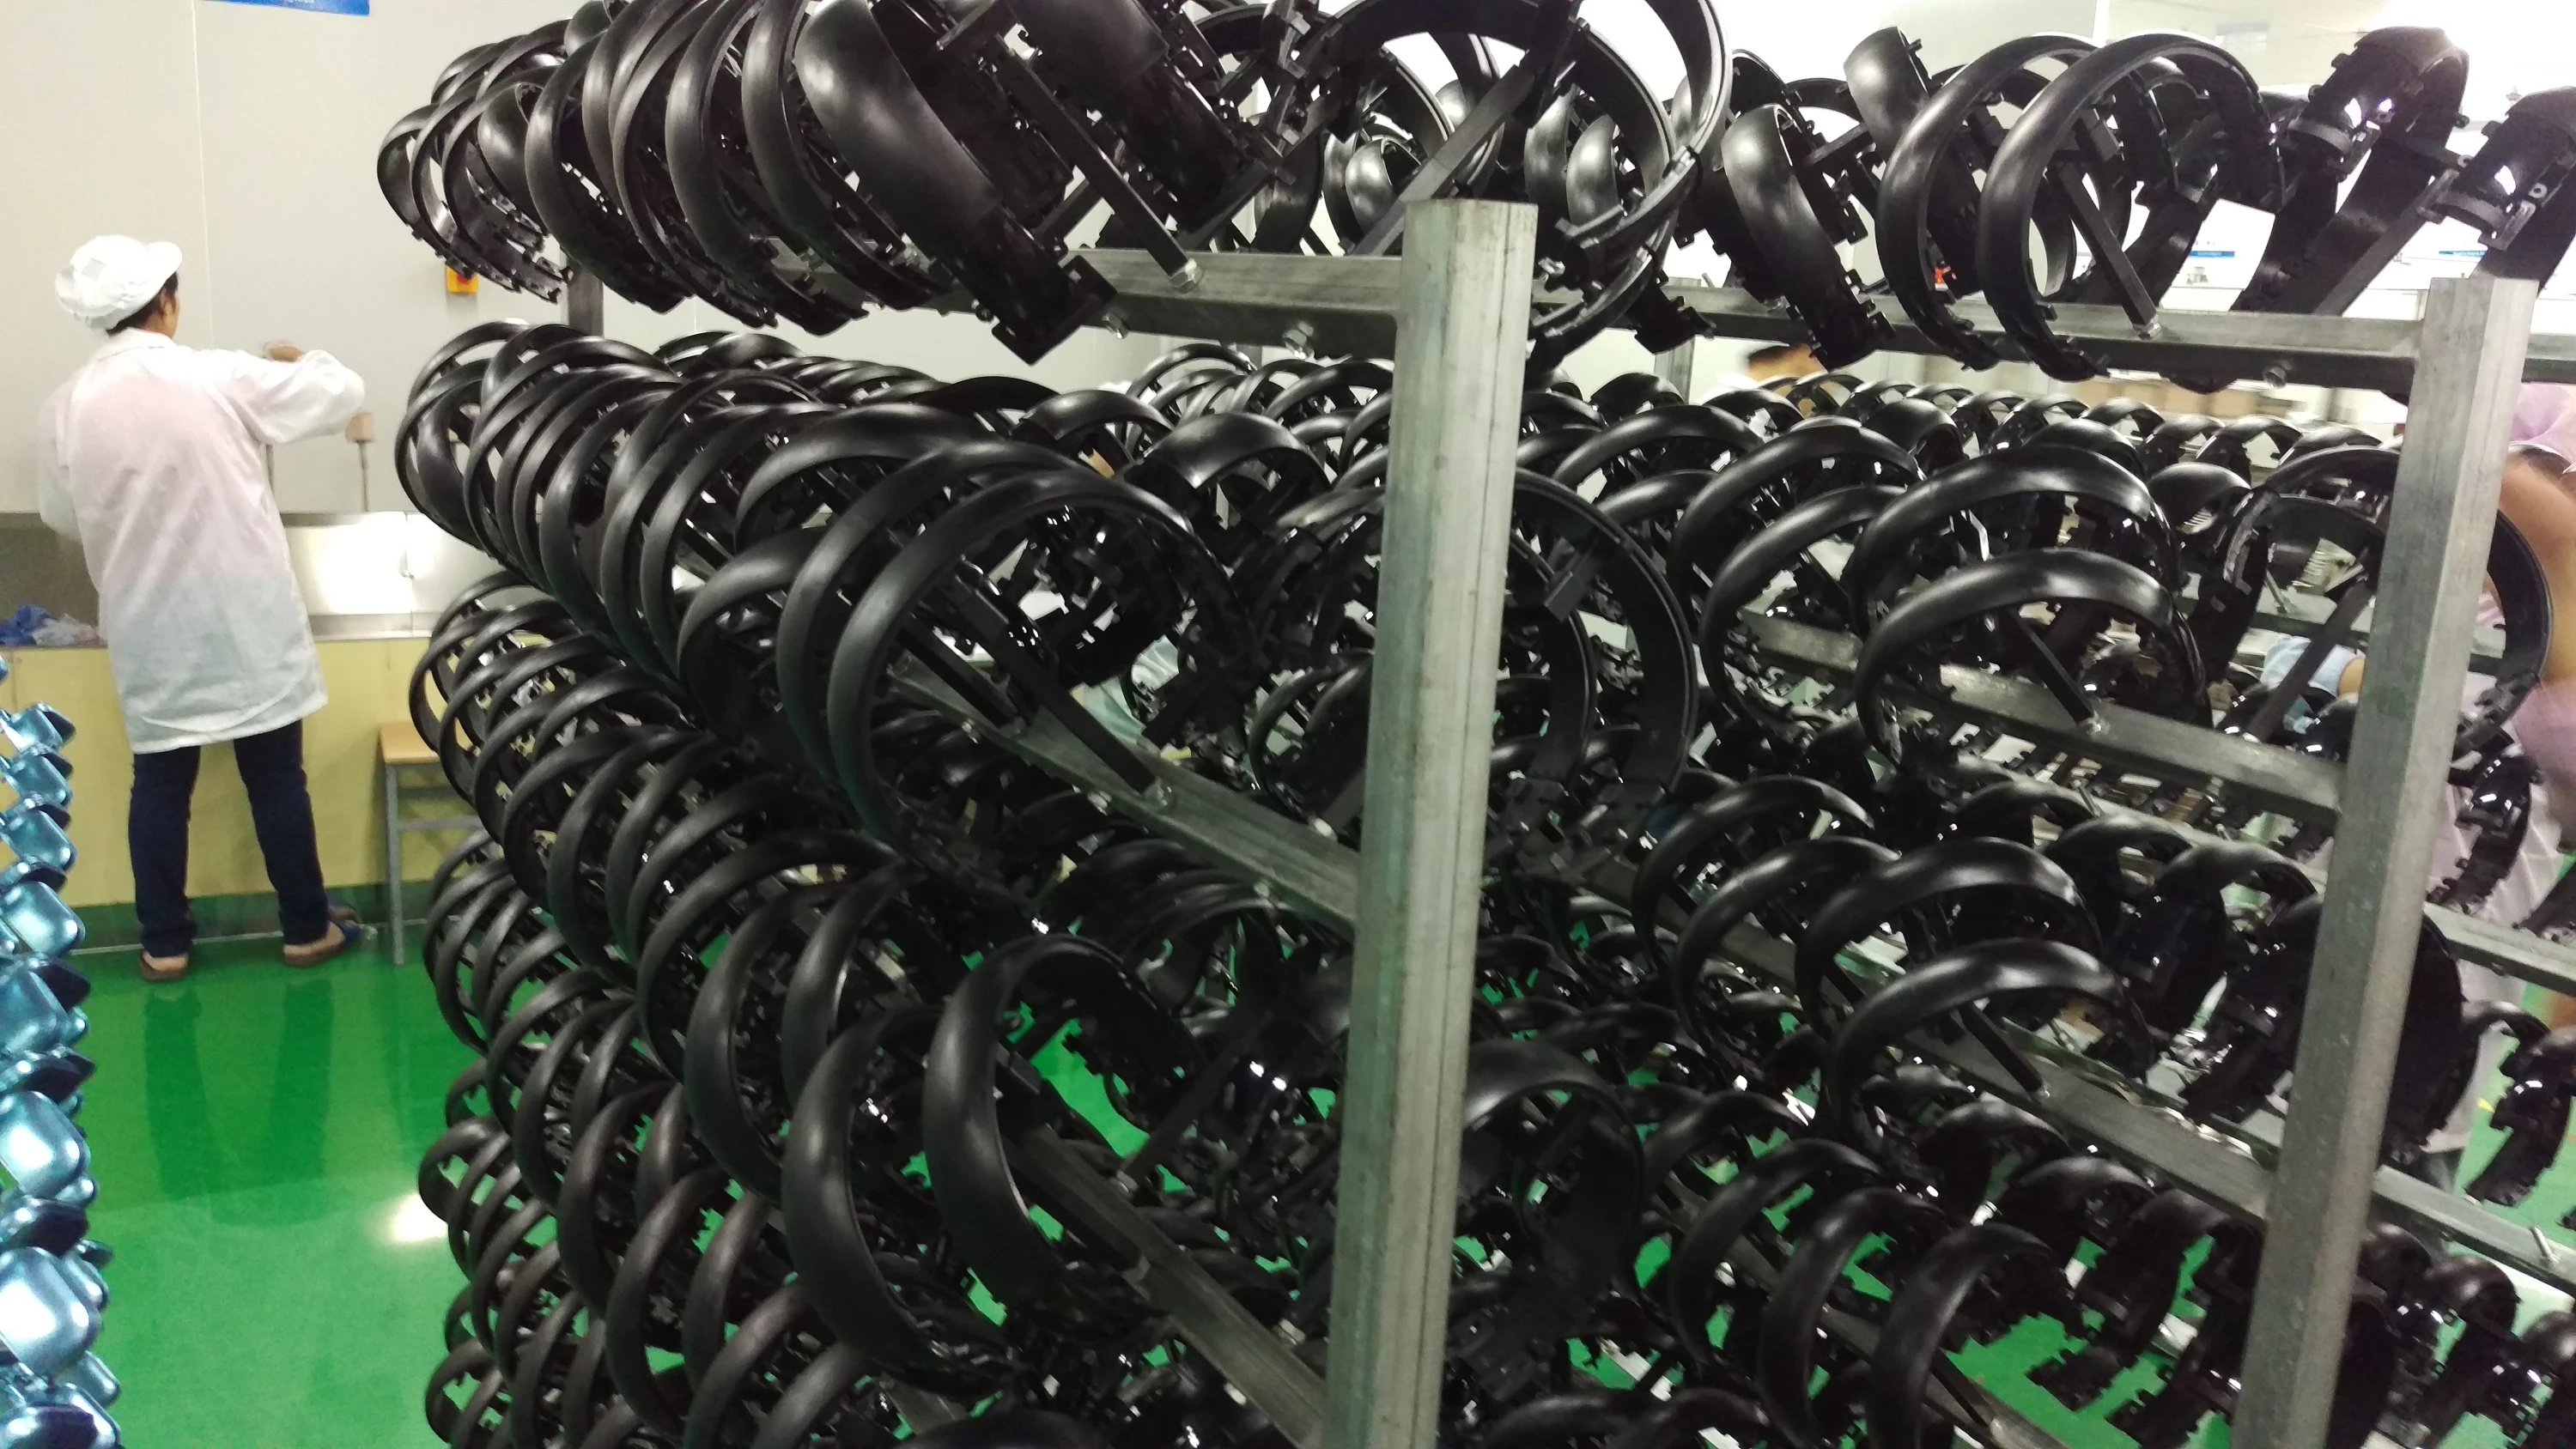
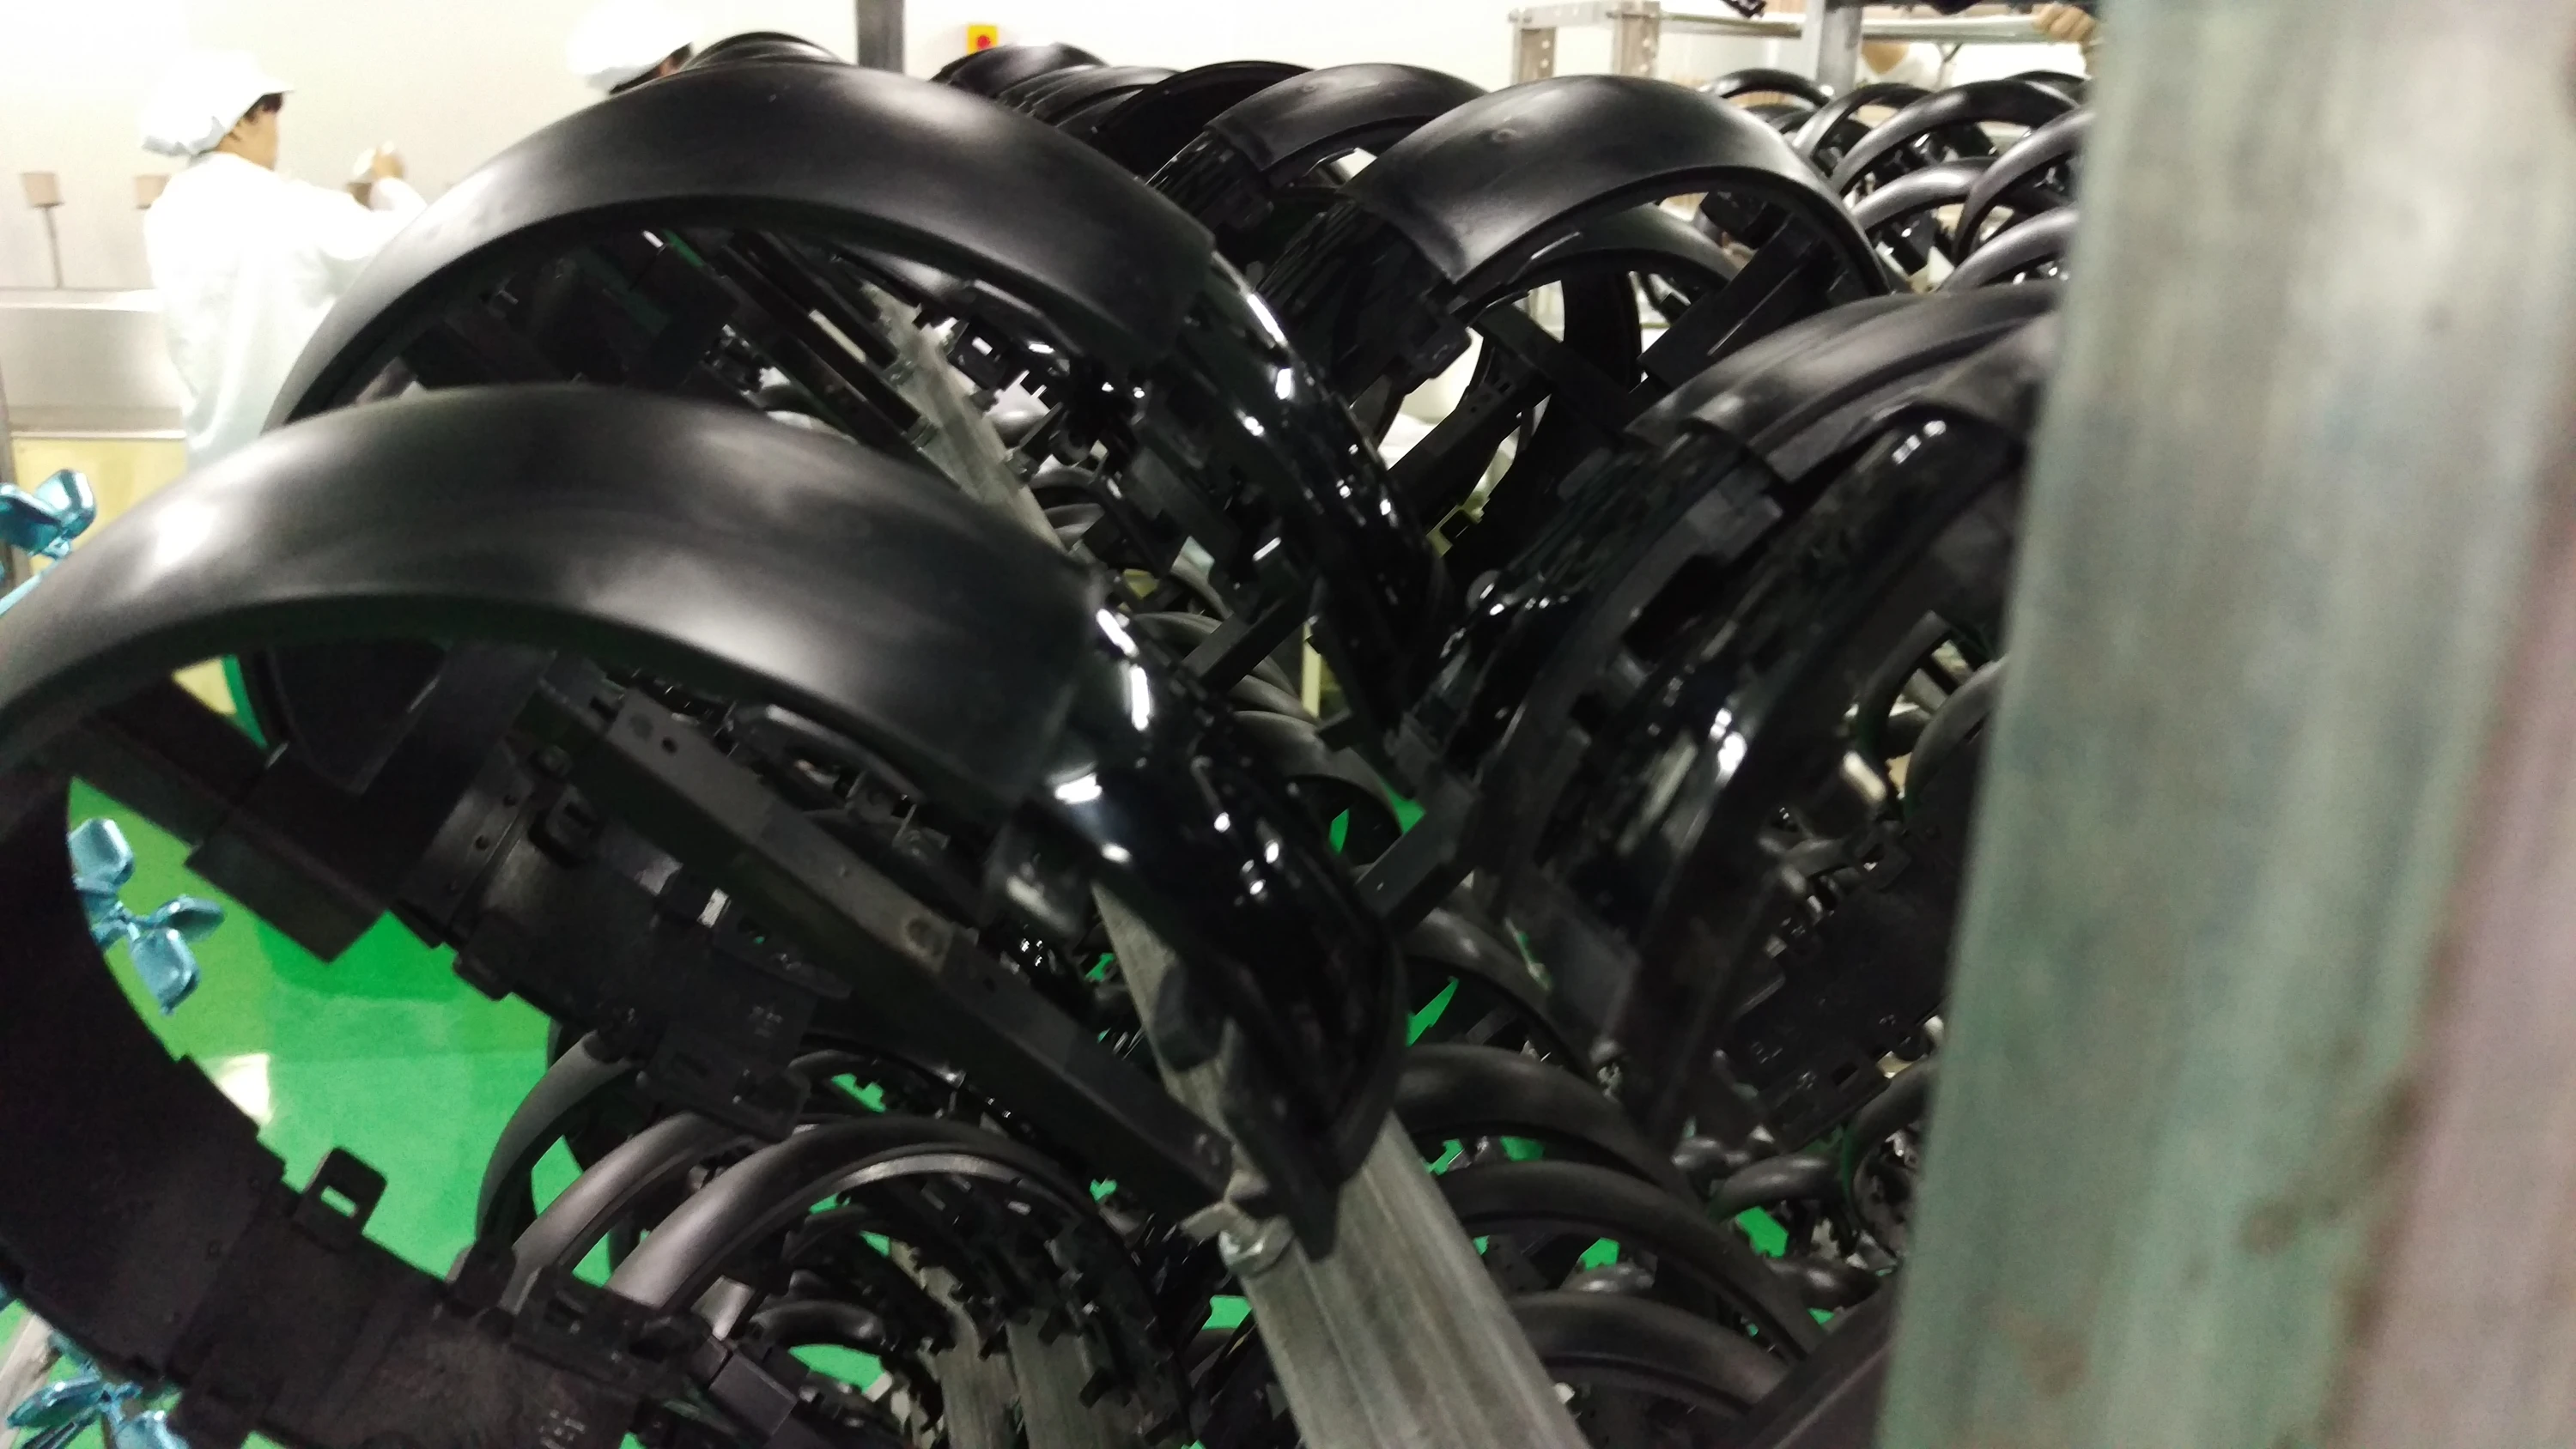
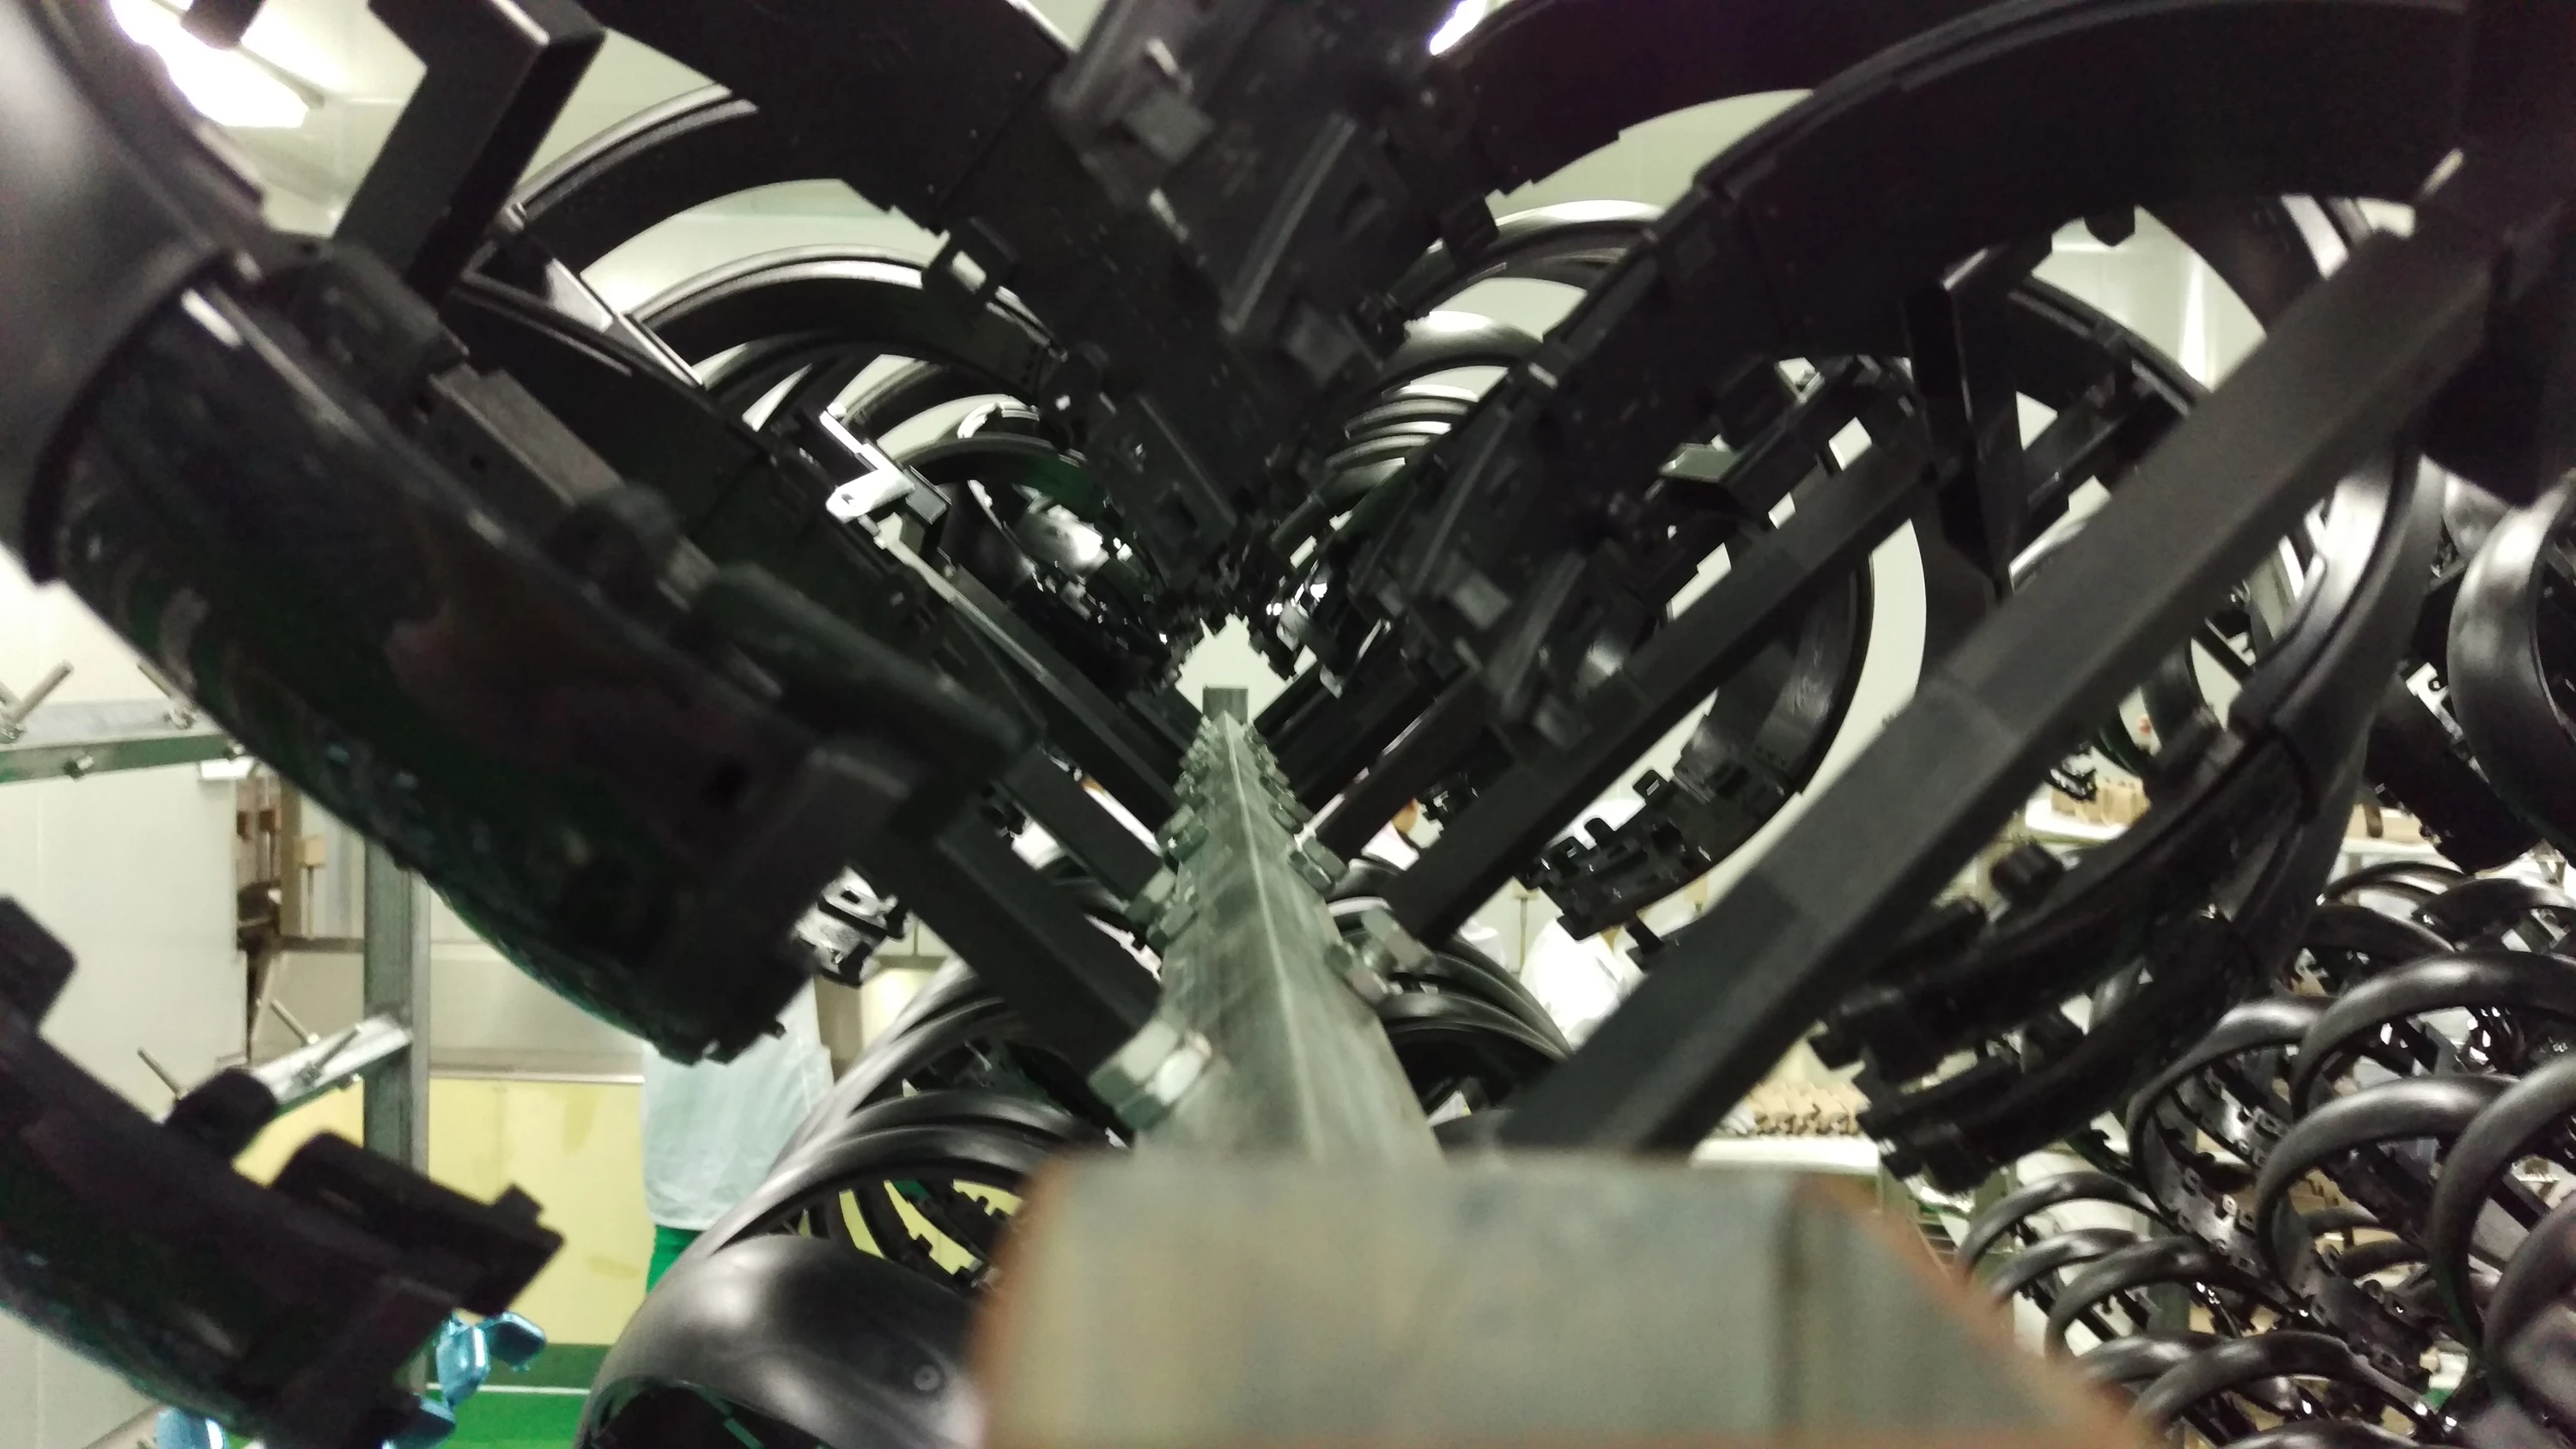
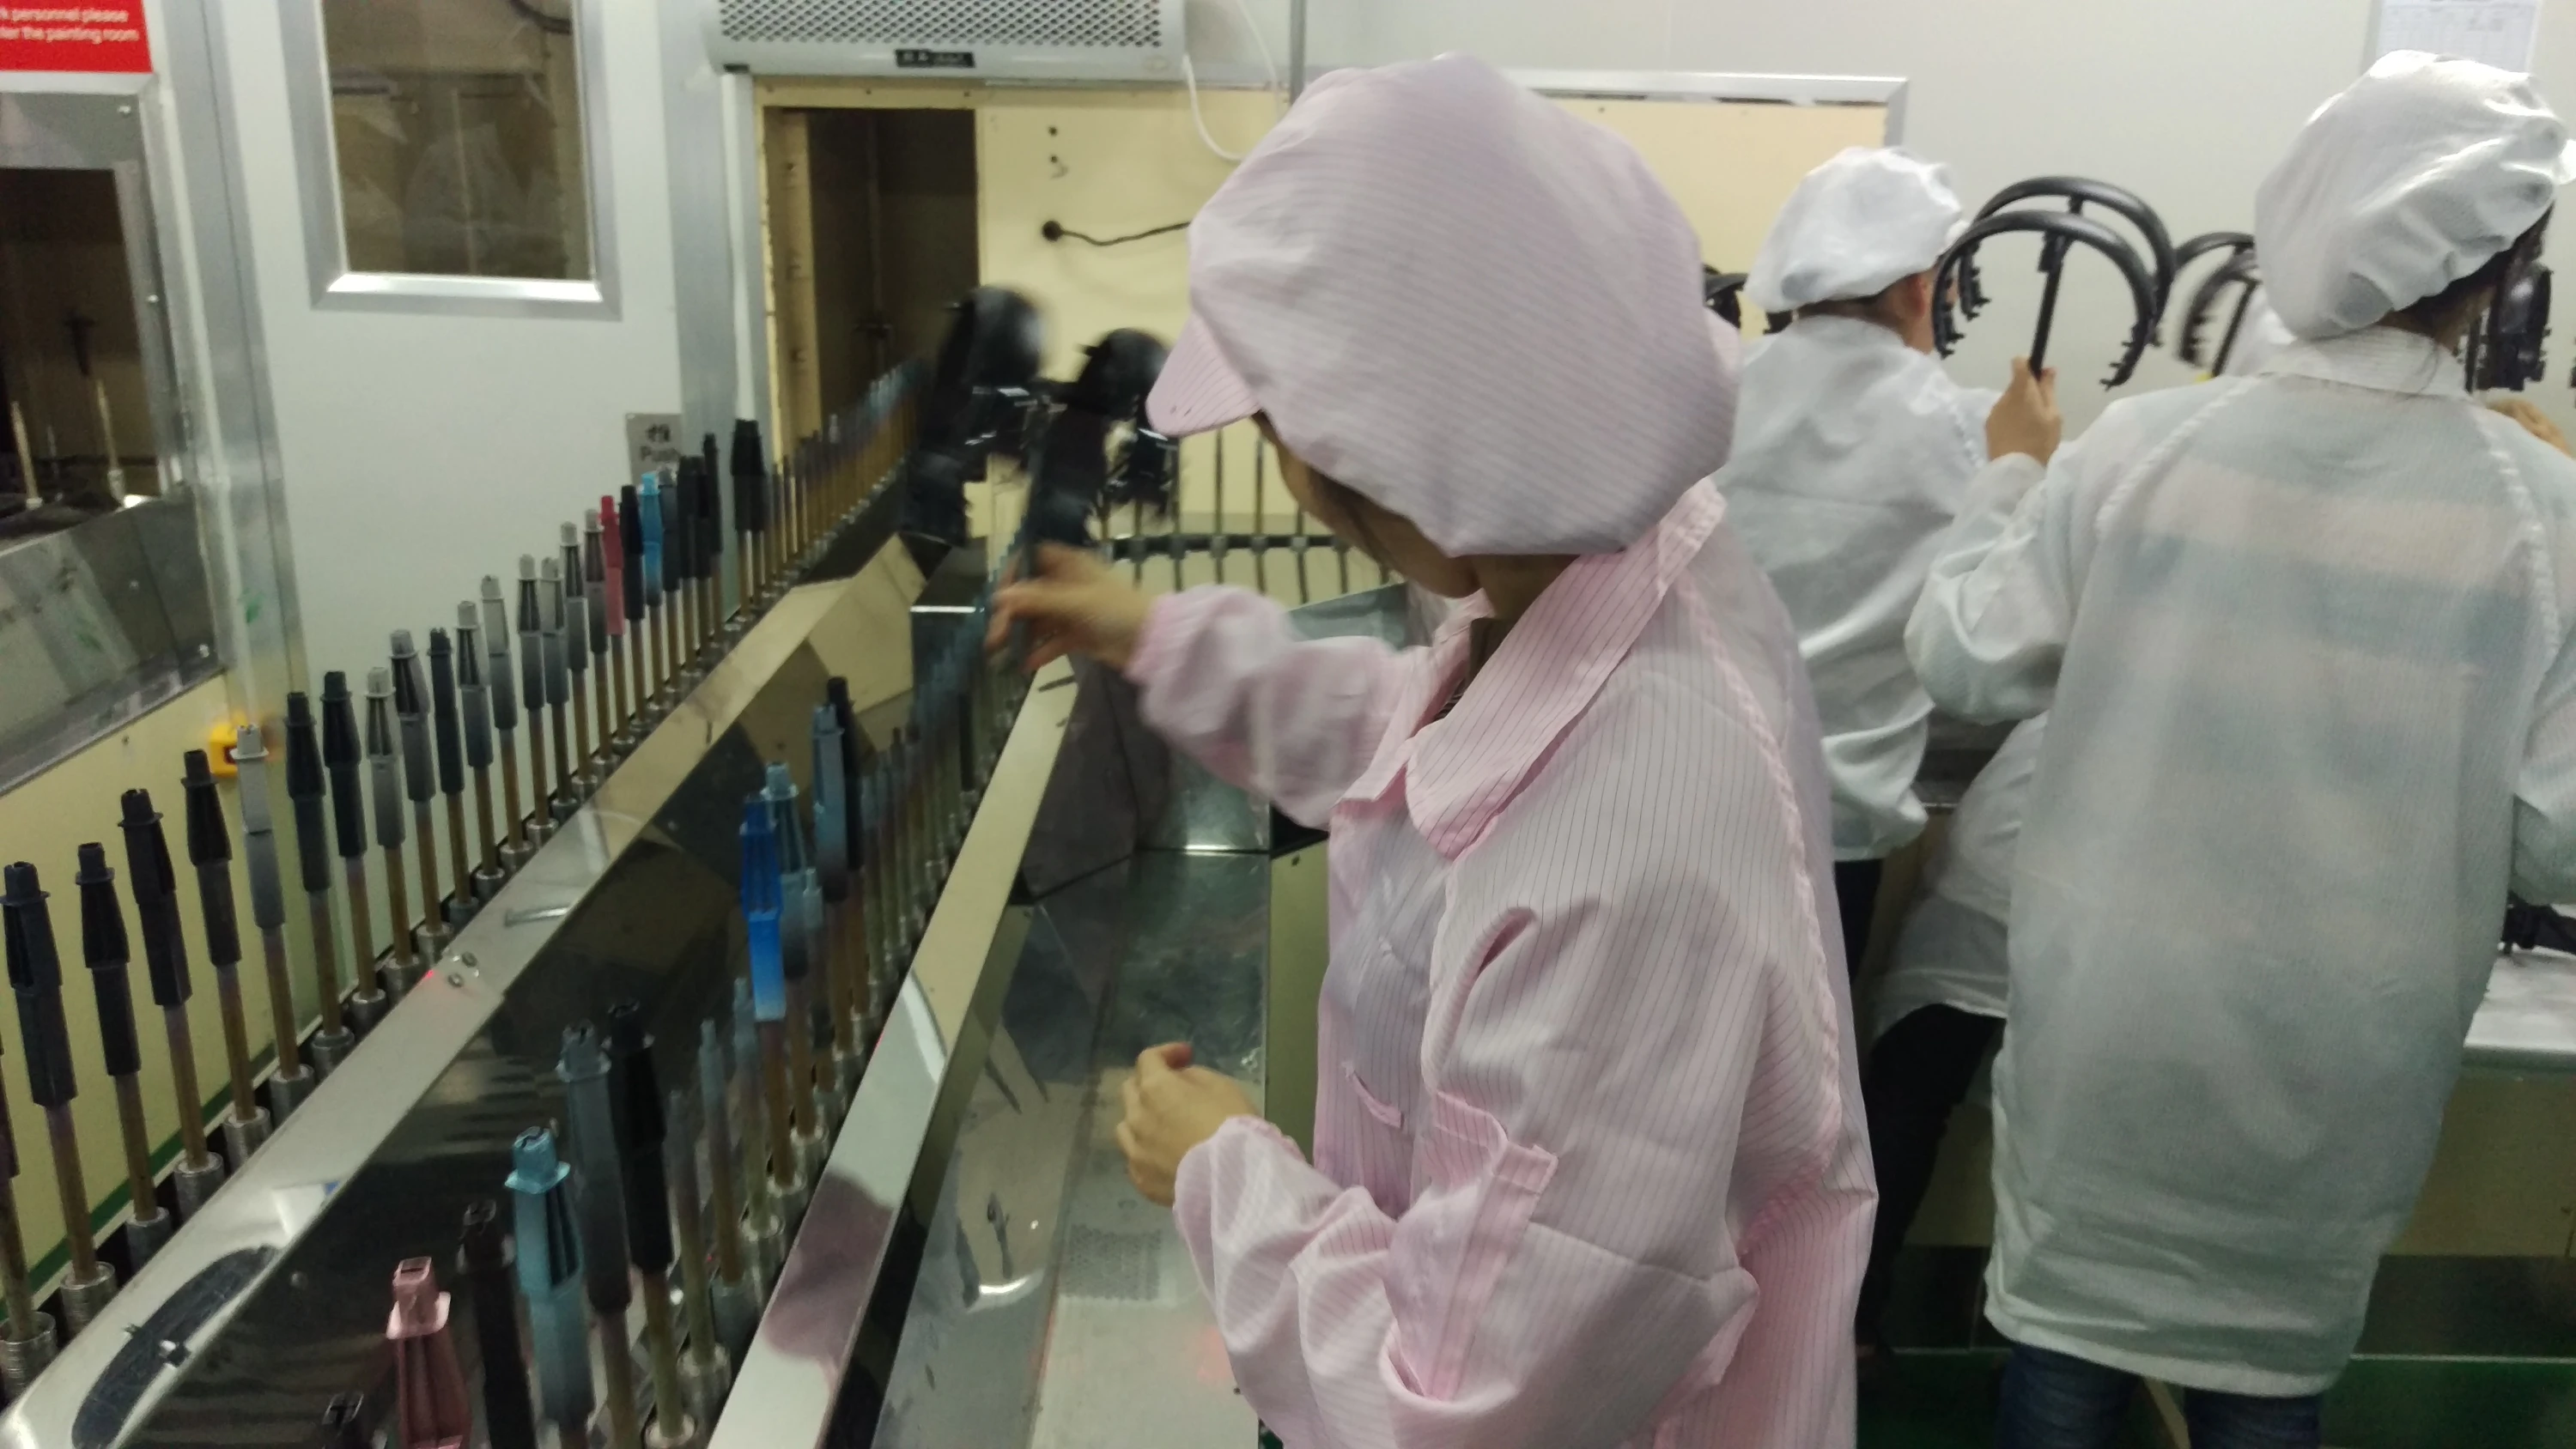
I designed the paint and coating masking tooling too, including reusable and disposable injection-molded masks. These parts interdigitated with the production parts: their geometry covered the sections that needed protection while leaving the specified finish regions exposed.
Molded masks for paint and coating
Interdigitating tooling defined which regions were protected and which were exposed to paint or coating.
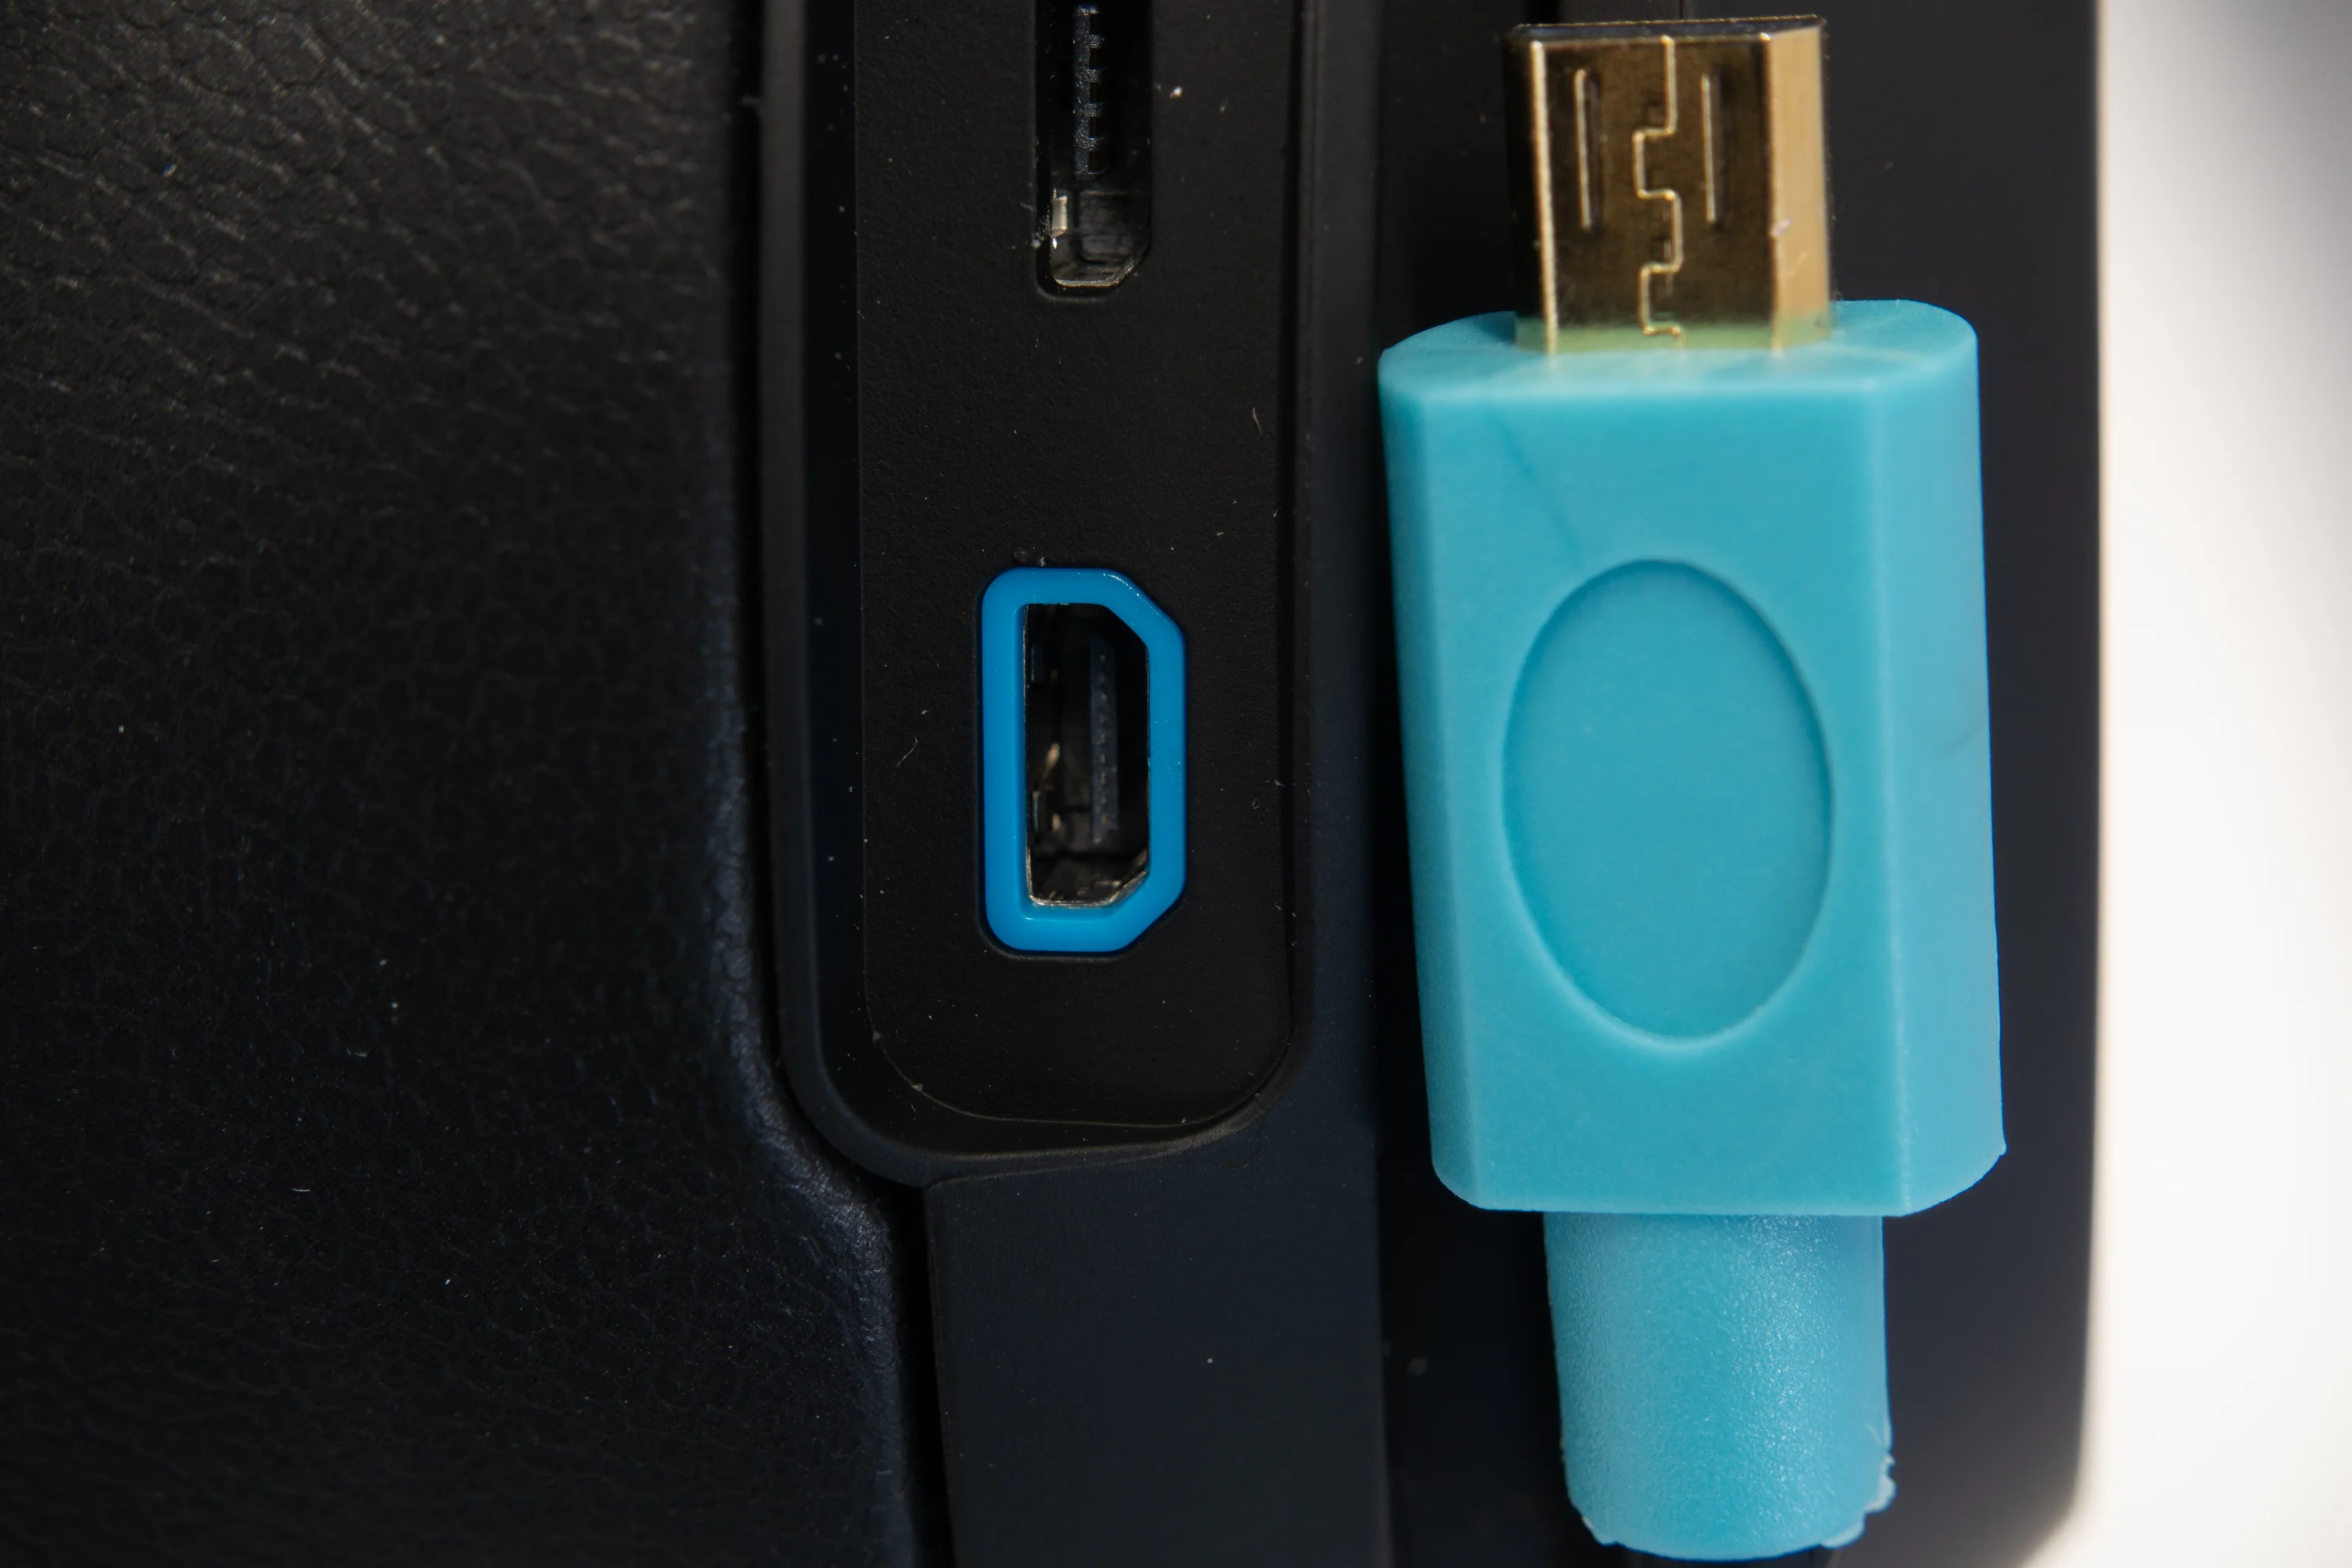
Judging the color match
The two blues below were intended to match. Holding the suppliers to that match took rigorous CMF documentation. The photograph shows why an individual part's color had to be considered alongside the neighboring parts and finishes.
Holding the color match
Customer artwork and employee units
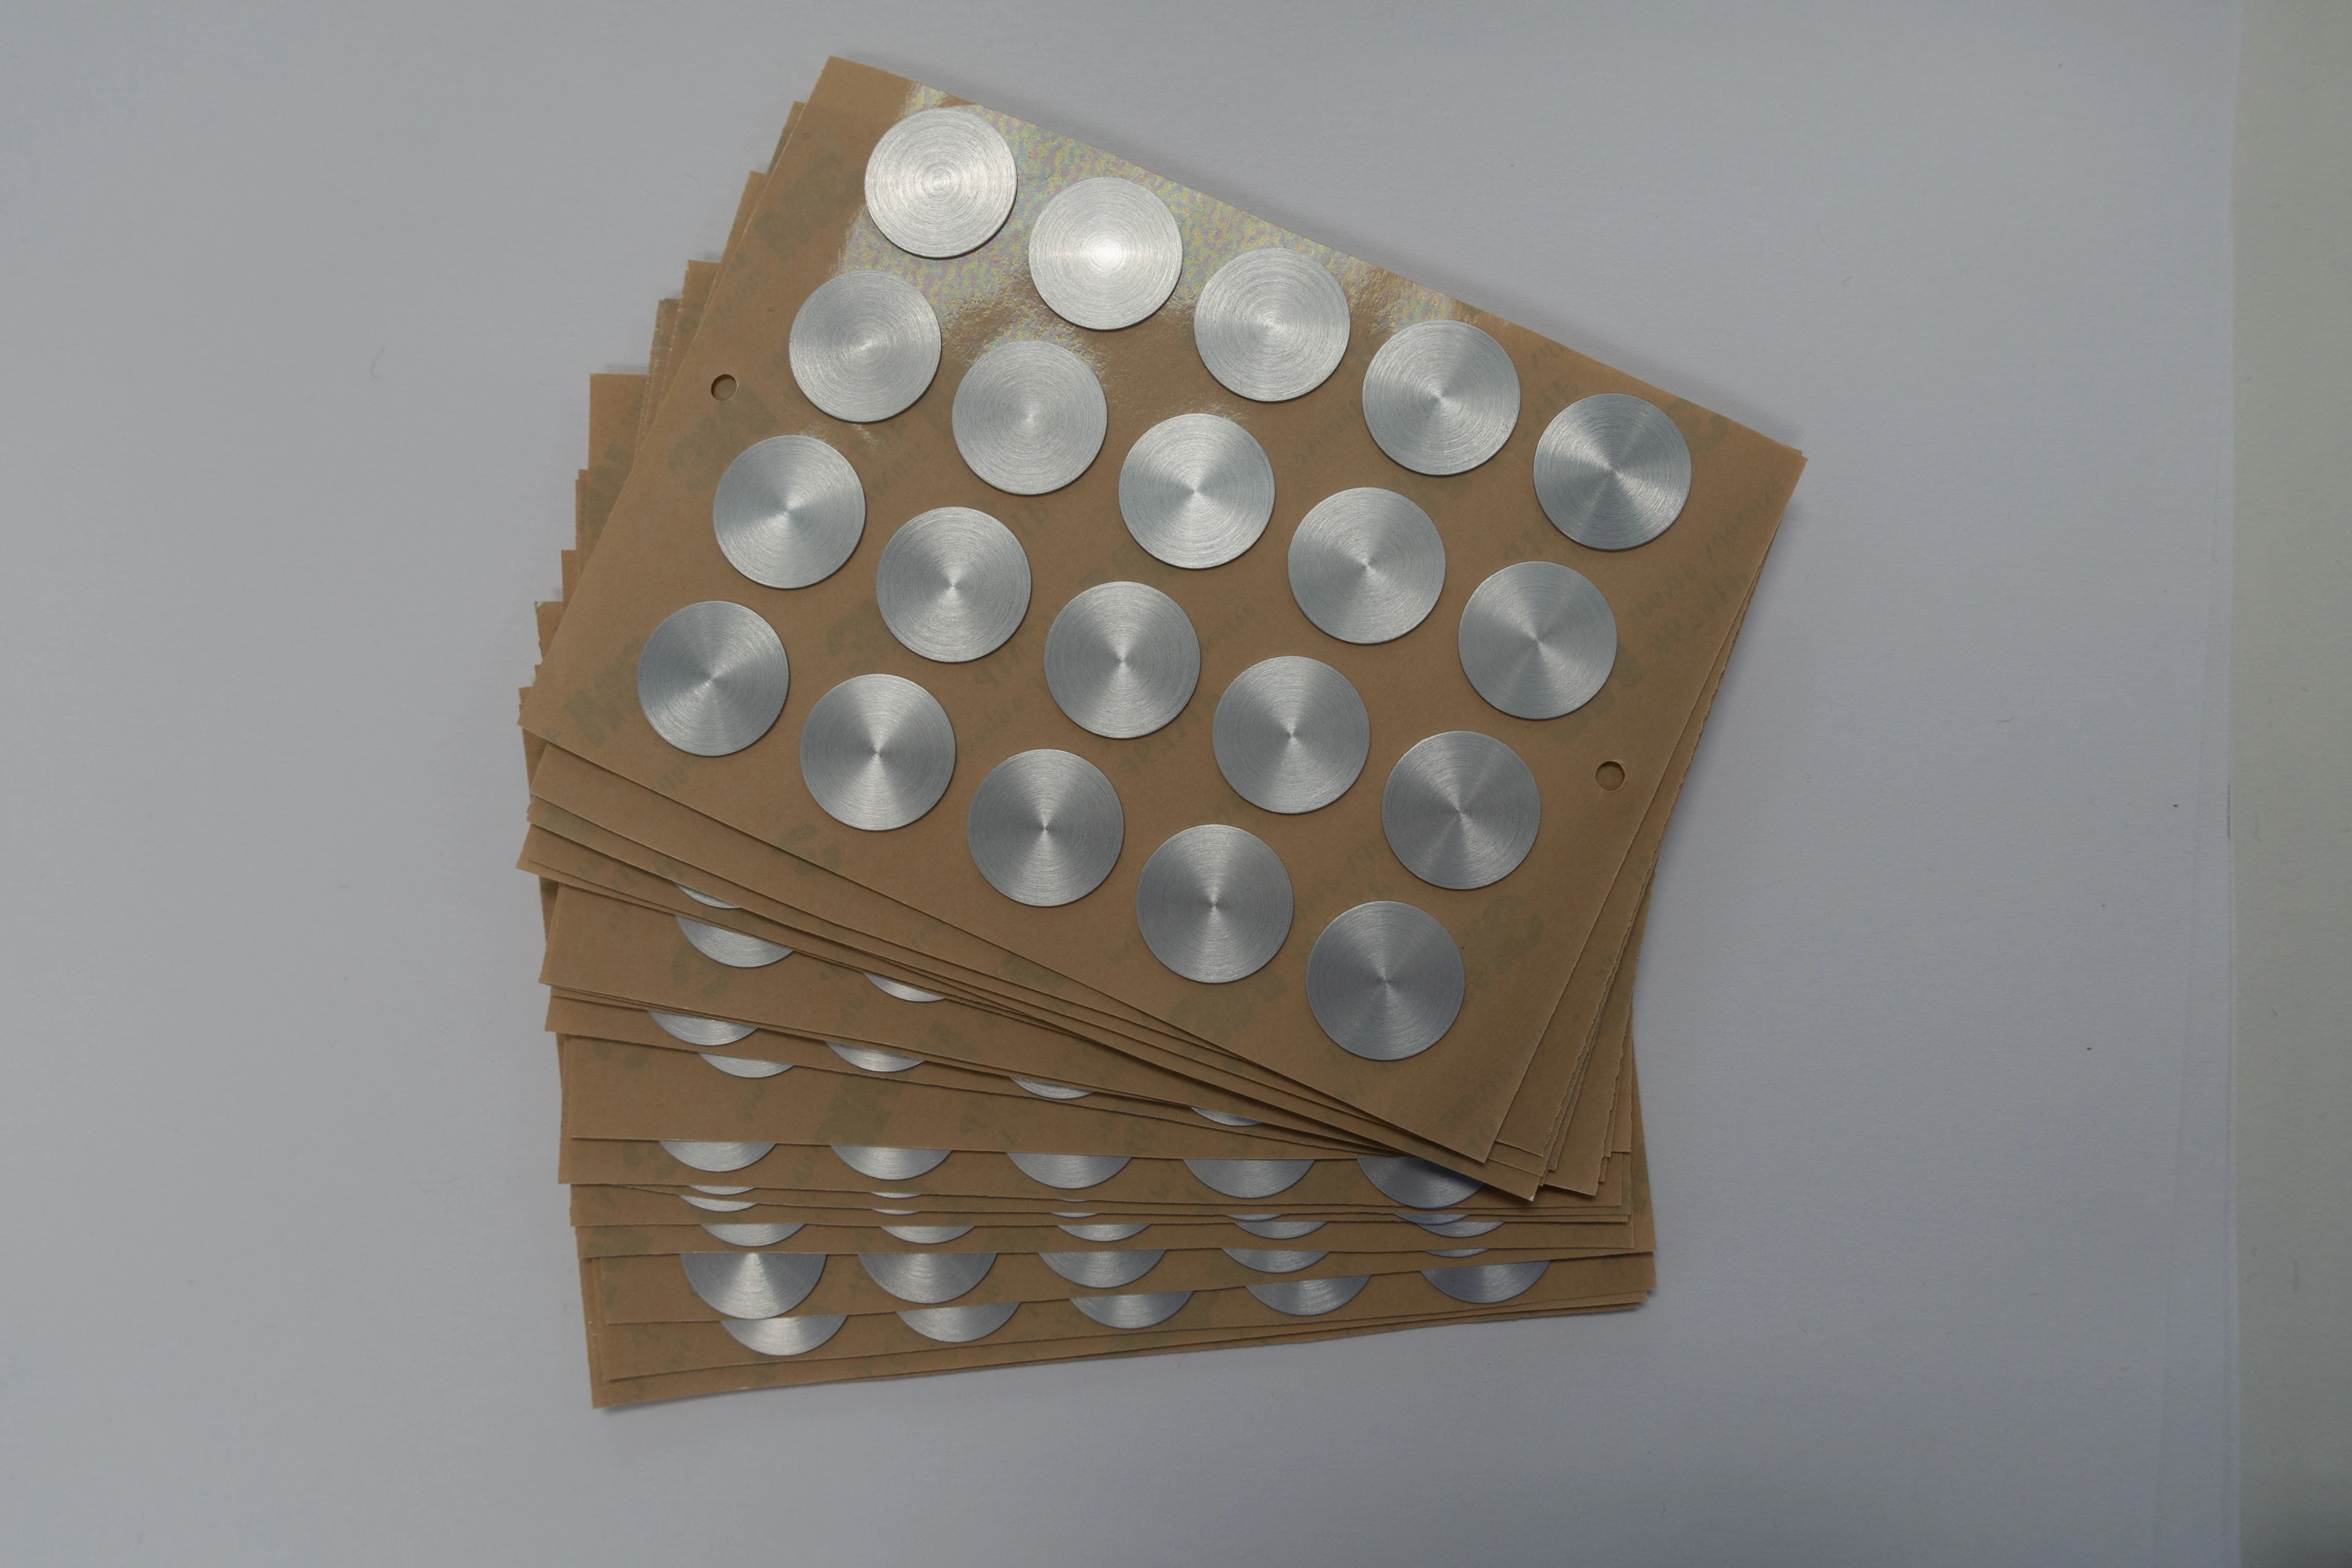
My work also included customized aluminum discs for customer-supplied artwork.
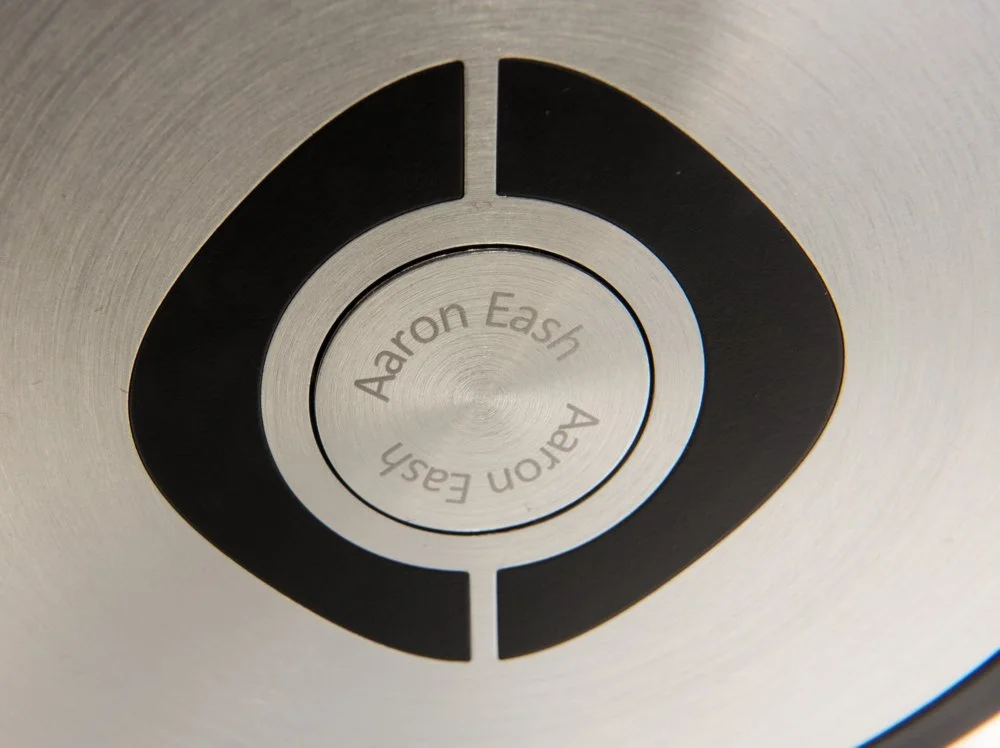
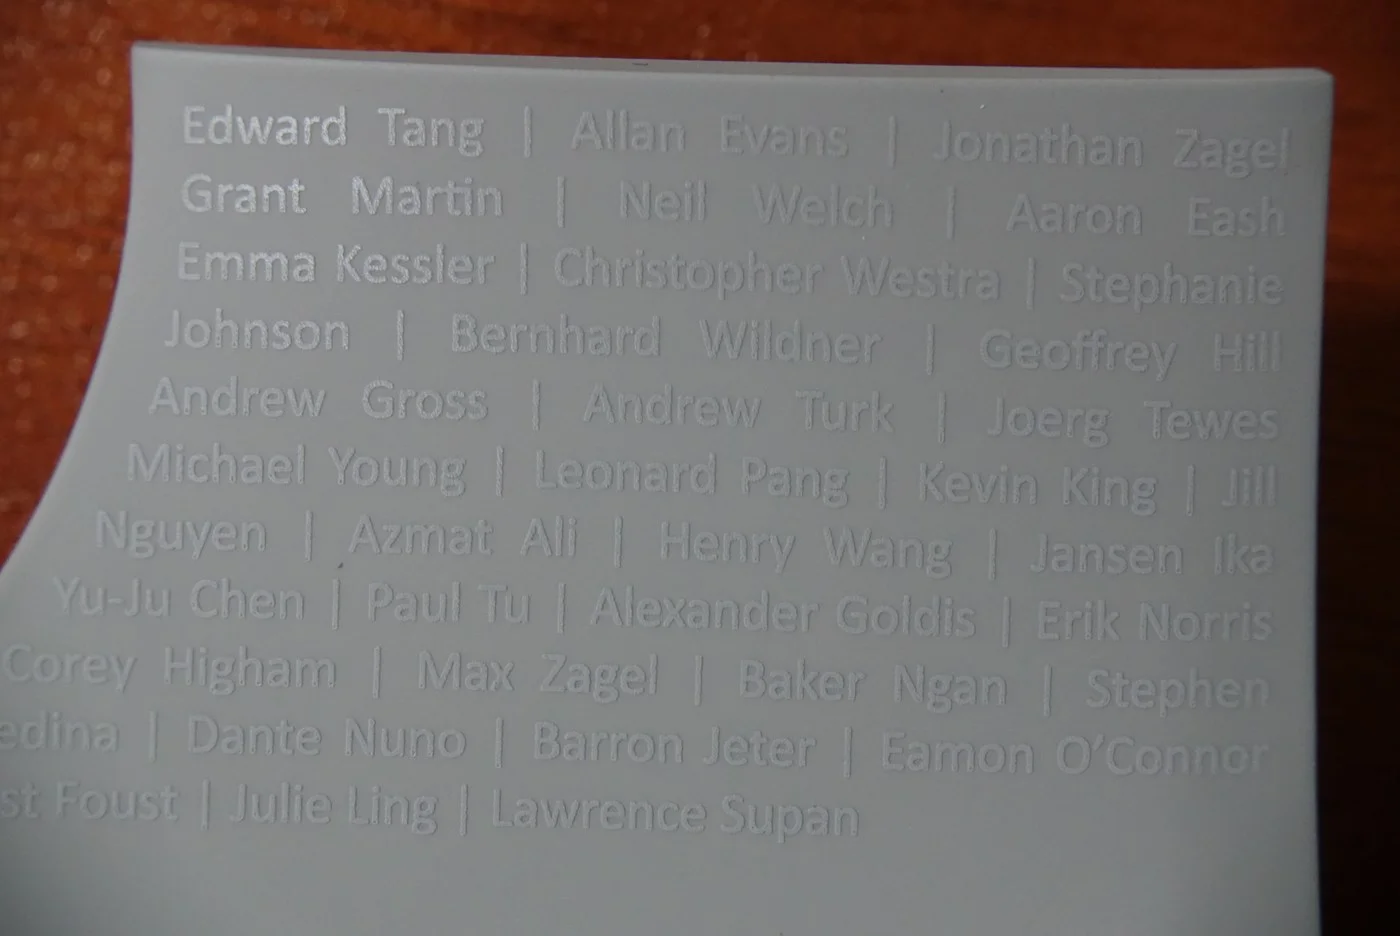
For the employee commemorative units, each person chose artwork for the small aluminum center disc. I delivered the artwork to the vendor and coordinated getting the personalized parts made. I also designed the team-name artwork and arranged for it to be pad-printed on the right inner ear-cover bushing of those same units.
Personalizing the ear covers
Employee units
Shipping while the ramp continued
Finished units ready for handling
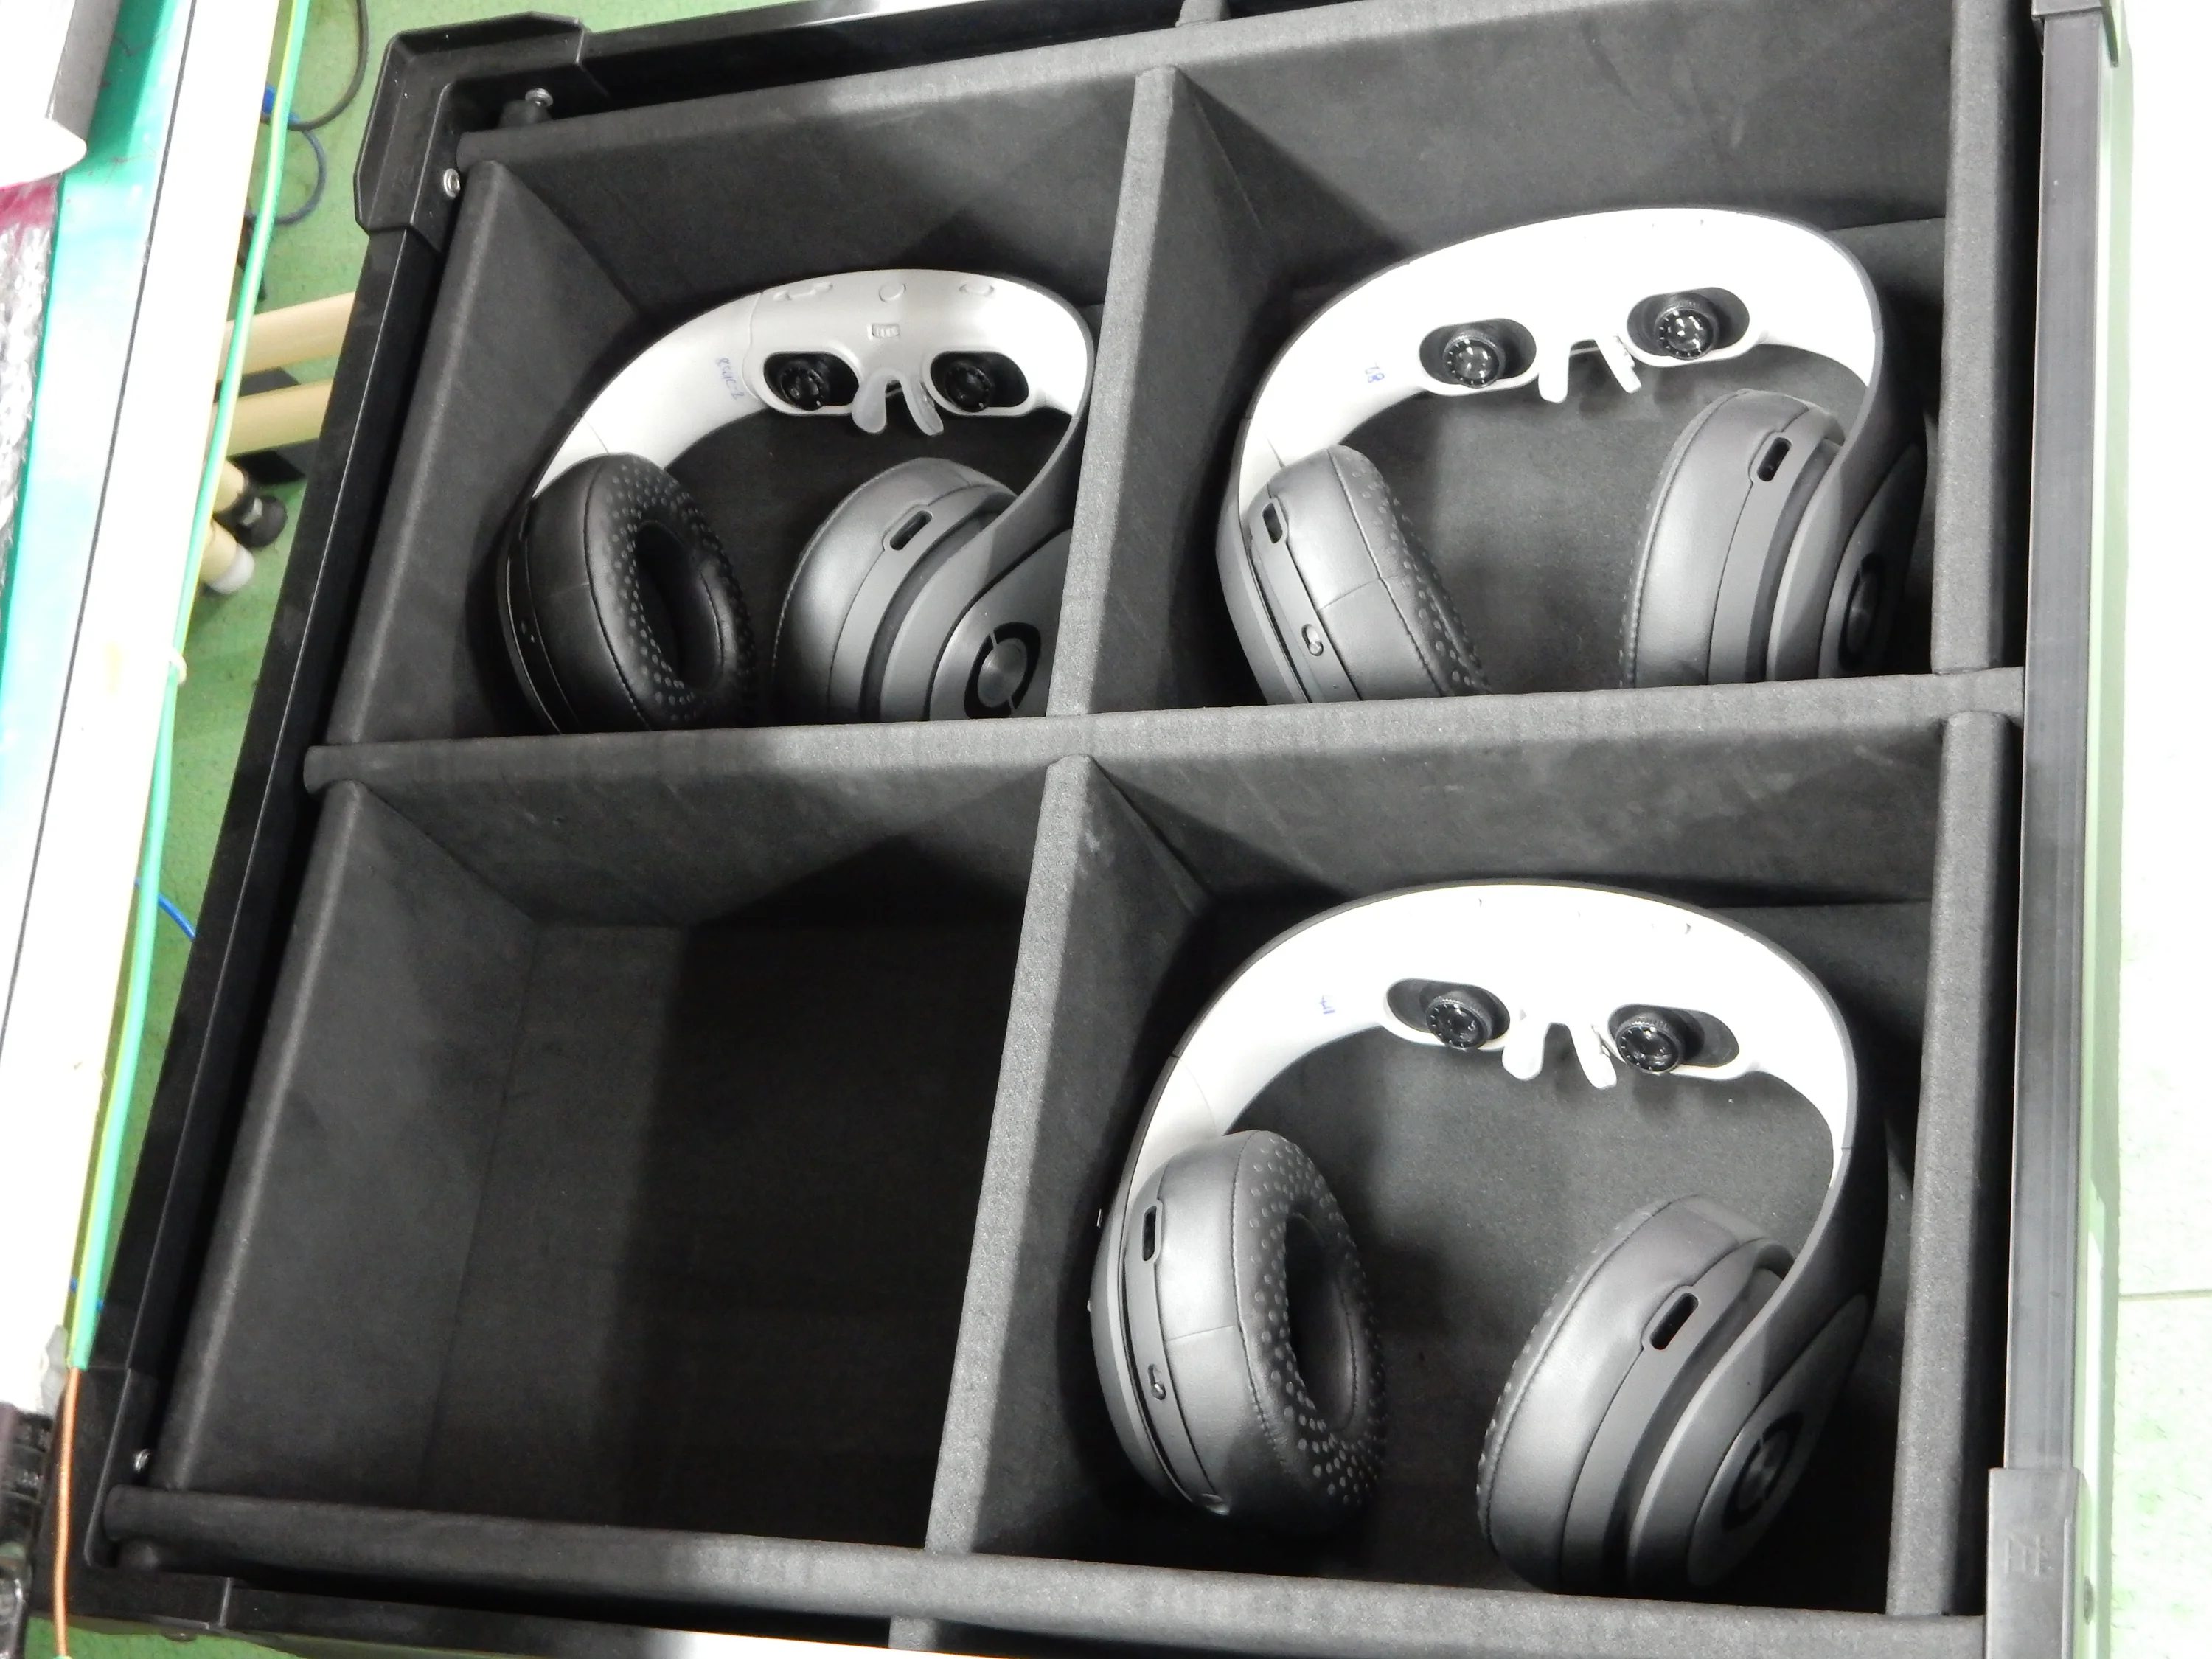
On January 28, 2016, Avegant announced that shipping was beginning. By February 3, the company had sent more than 200 tracking numbers, with yields improving and the line still below full rate. On March 3, it reported about 1,000 units shipped.
Through that spring, I kept working on the mechanical problems that came with the ramp. In April, cable-abrasion changes were still in validation, and I was working on clamp force, liner tooling and another cable supplier. The Amphenol work included defining the validation needed for its samples and coordinating that work with Intretech.
Delivery depended on work across the company too. CE certification held up international orders, and engraving added another step to fulfilling customized orders. On June 2, Avegant reported the Kickstarter units fully deployed.
Kickstarter fulfillment was a shipping milestone, not the end of the engineering work. The August clamp-force comparison still separated liner material, paint state and spring diameter. By December and January, the return-analysis work described above was feeding another set of findings back into the product. Testing, production support and field diagnosis continued through my final months at Avegant.
Leaving Avegant
I worked at Avegant from July 20, 2015 to January 27, 2017. When I left, Chris Westra shook my hand as I was walking out the door and said, "Thanks for fixing all of my problems!" Coming from Chris, that was high praise. It meant a lot to me.