320-Slot Carousel
Making all 320 positions work
The carousel in Kaleidescape’s M700 and DV700 disc vaults had to do more than hold 320 discs. Each position had to present a disc consistently to a kicker, accept it from the pinch rollers, and remain readable by the inventory sensor. A large molded part connected all those interfaces. Small differences in a slot, a rib, a tooling insert or the disc itself could become a handling problem.
My work moved between that functional geometry and the realities of the tooling: defining changes, investigating samples, coordinating supplier follow-through, and turning observations into drawing controls and inspection procedures. Function Engineering developed the early breadboards; Loyd May contributed tooling, rib, radius, cooling and venting work; Nathan Forster later tested changes in the complete handling system.
Establish the path before committing it to steel
The early record shows several capacity alternatives being worked through together. Function’s May 2010 sizing study compared disc spacing and 250-, 300-, 350- and 400-disc envelopes. A June 4 note identifies 300 discs as the plan of record entering breadboard development, and the end-of-phase report describes a 300-disc molded platter. Yet a June 16 concept still has 250 slots, and the June requirements retain older 250-disc language alongside a target of at least 300. By August, Function was evaluating a 320-disc system. These are overlapping studies, not a clean sequence of capacity increases. The exact decision fixing 320 remains unresolved.
The June architecture already connects the carousel to the rest of the machine: perimeter belt drive, paired idlers, a home flag, encoder teeth for individual slots, a central support and three support rollers. It also leaves questions about obstruction sensing, foreign objects, smaller discs and maximum disc thickness. Those are design commitments and open questions in the phase report, not a claim that the resulting product had passed them all.
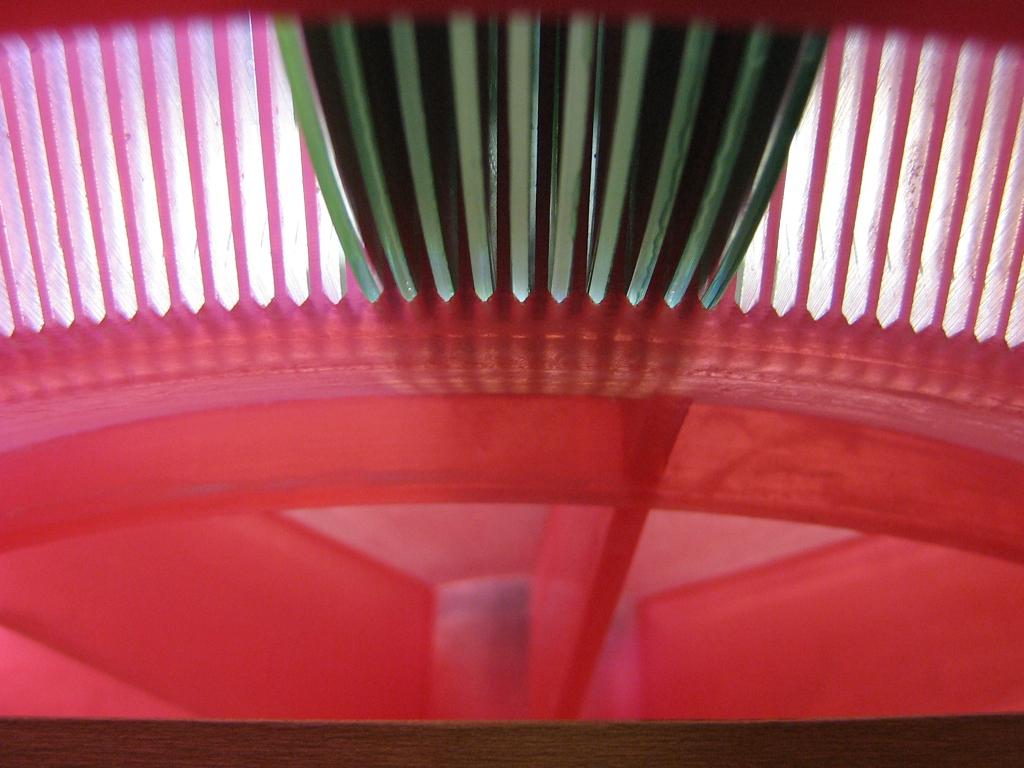
The breadboards were built to test the interfaces. Four disc-slot geometries were compared, with a full SLA carousel and separate kicker and pinch-roller mechanisms. Function found that a V-groove was necessary to constrain the disc and align it with the kicker. It also investigated alignment sensitivity and the timing of moving a disc through the mechanism. Full-system position confirmation and life testing remained further work.
The carousel’s perimeter was another interface, functioning as a large timing pulley. The breadboard report discusses belt engagement over a long wrap and an integral number of motor steps per slot. Those choices made the shape a coordinated mechanism rather than an isolated molded tray.
Prototype disc constraint
Getting material through the geometry
Before molding trials, the archive contains several gating studies. Yudo compared 26-, 18- and 12-drop layouts, then produced a separate eight-drop study. Other Moldflow reports explored different model and resin conditions. They map potential fill, weld-line and trapped-air behavior, but their differing assumptions prevent a simple claim that one layout or material conclusively won. Commercial records likewise move from six-drop alternatives in September to an eight-drop quote in November. Those quotations establish proposed configurations; they are not a record of every drop actually installed.
The tool-build reports add an intermediate stage between those studies and the first samples. Successive December schedule columns report 62, 75 and 90 percent actual progress. They show the mold moving through construction, with future dates and incomplete work still visible. The final January target is not a completion receipt. Packaging was being considered before the trials too: a January brief emphasizes preserving flatness and protecting the encoder teeth, distinguishing temporary sample shipping from the future production pack.
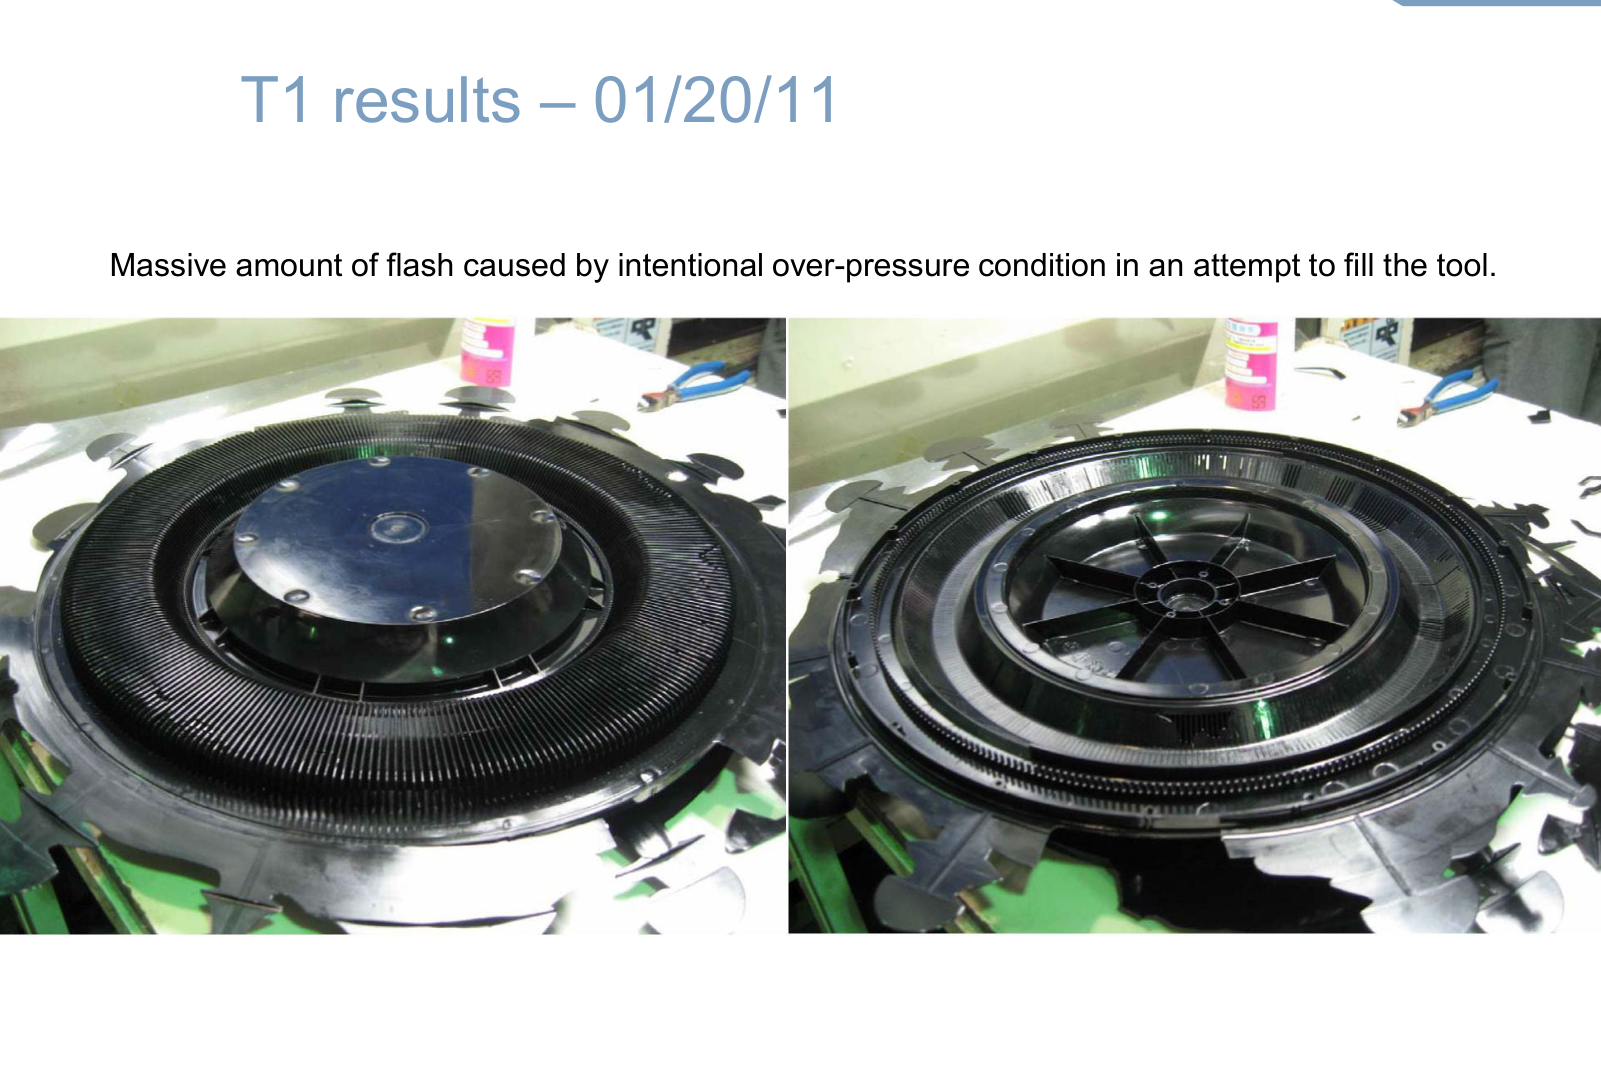
The first trials exposed the difficulty of filling and releasing the part. T1 photographs show flash and ribs broken in the tool. At T2, the team could balance flow in the center, but filling the inner ring and then the ribs and outer hub remained difficult. Meeting notes describe a narrow operating window, unequal tool temperatures and plastic stuck in the cavity. Cooling distribution, vent locations, polish, ejection and resin choice were all being questioned.
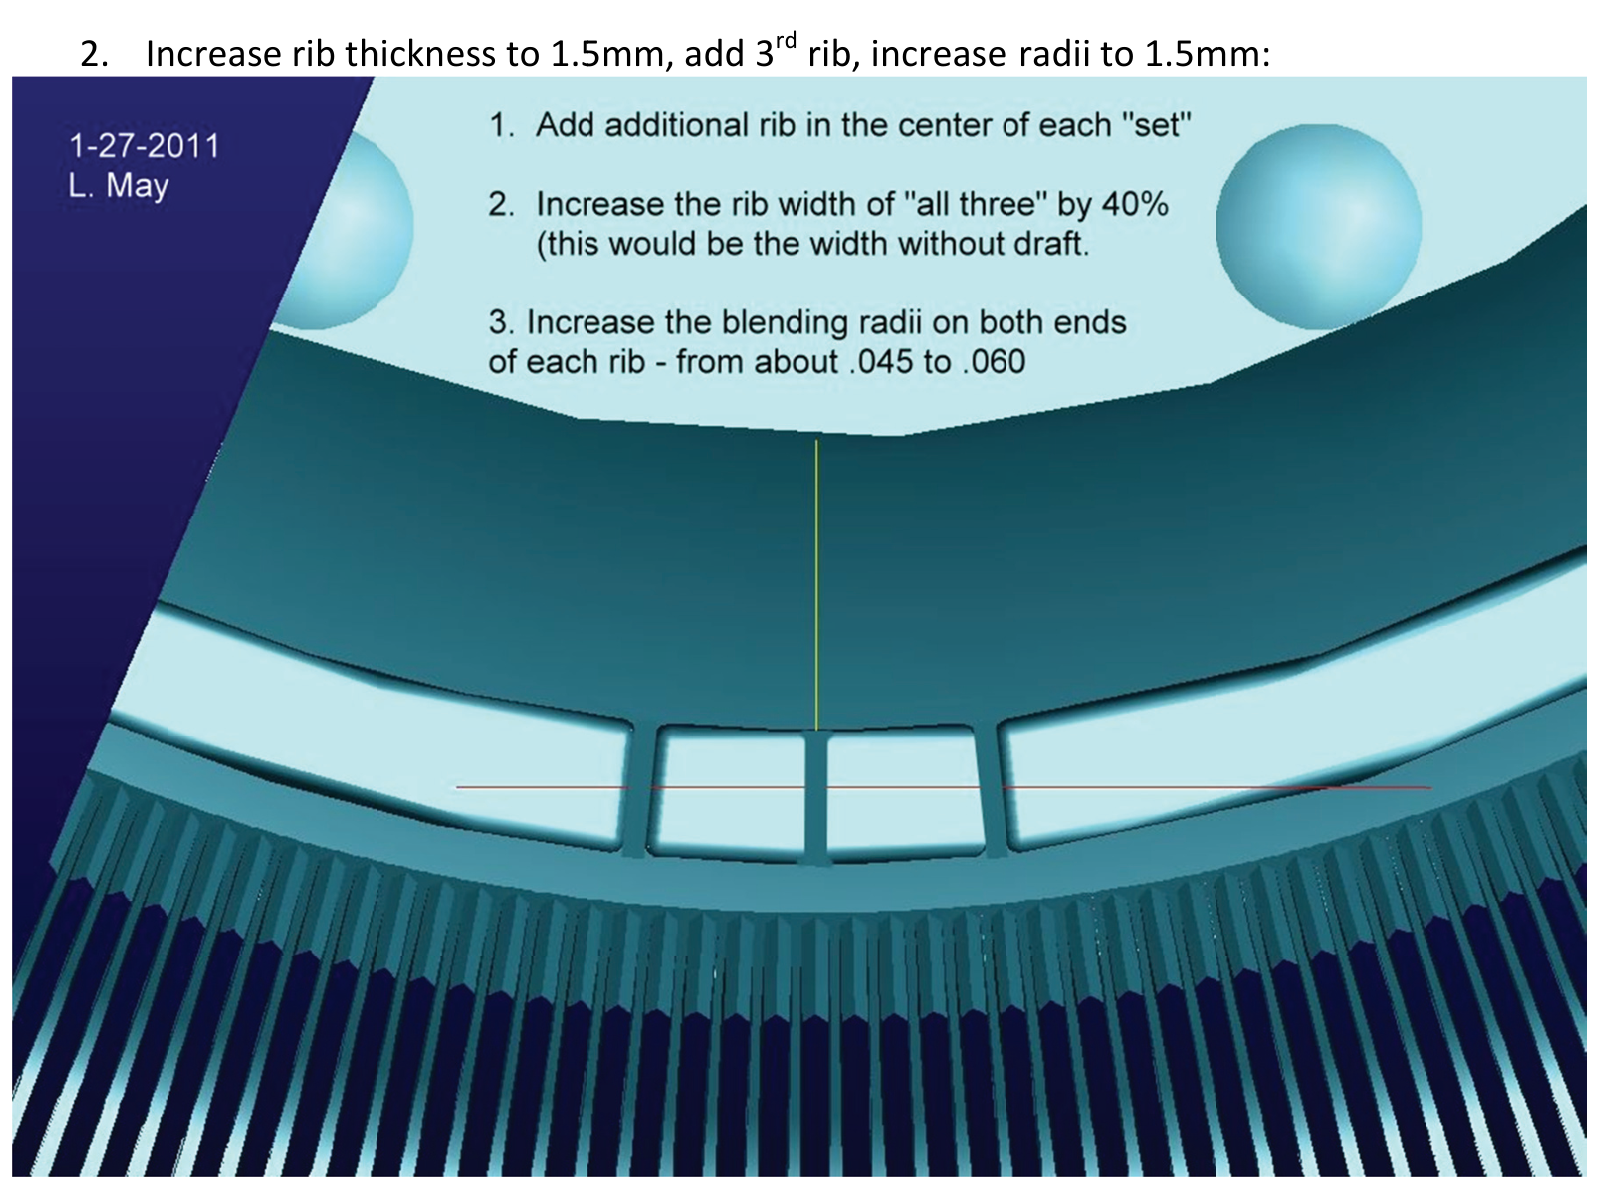
The response was incremental. The T4 plan prioritized ribs, radii, cooling, vents, polishing and gate changes. More invasive alternatives, including additional cavity ejectors, undercuts and vacuum venting, remained available after sampling the first changes. The February update records an approved internal purchase request for the rib/radius work. By the March 17 report, Function labels a sample photograph with implemented ribs, while still documenting air traps and short shots. Getting a part to fill was progress; it did not settle dimensional or functional acceptance.
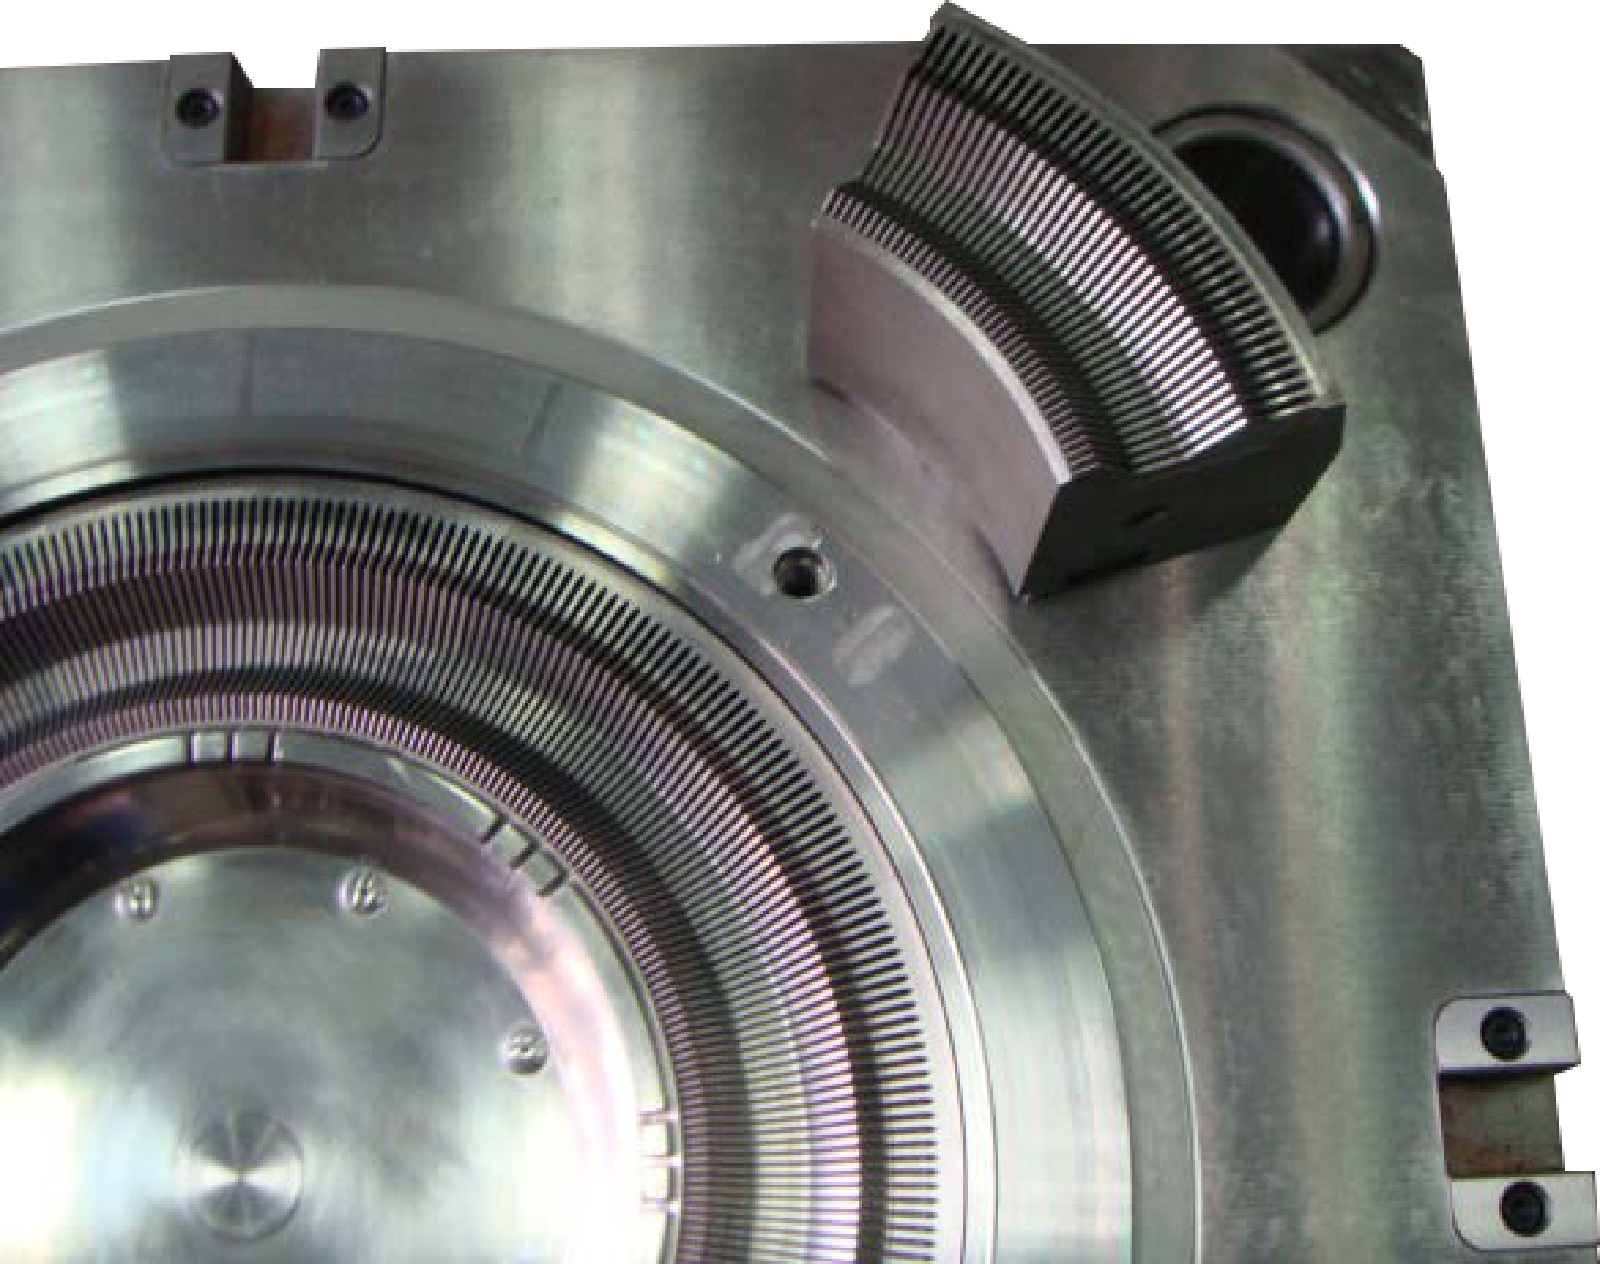
Carousel mold section
T1 molding trial
Rib and radius changes
Know what is actually in the tool
In May, the issue was partly one of configuration. Loyd asked Alan Wu to identify the vent land geometry actually present in the tool and reconcile it with earlier sketches and the current drawing. His memo refers to my earlier question about land depth and vent width. He also asked for numbered hot-runner wiring so later operators could connect the correct controls to the correct drops. A proposed modification was not useful unless the team knew what had actually been cut and connected.
In June, Loyd reported that enlarging the core-side vents had not markedly improved trapped air. He recommended adding release channels to 45 ejector pins. The later drawing history records ejector-pin vent changes, but that is evidence of drawing intent; the memo and revision entry do not by themselves prove exactly when the hardware changed or what improvement followed.
Photographs from June also show another problem becoming visible: the geometry was not identical around the carousel. Loyd marked changes in rib height and profile where cavity inserts met. That observation connects the tooling investigation to the local slot problems found during handling checks. It should not be stretched into a quantified causal result without reconciling the sample and measurements.
The later supplier trial review makes the tradeoff explicit. Better filling of the V-cut required higher clamping pressure, but the supplier reported that this also pulled or distorted slot ribs. Trapped gas, short fill and ejection whitening prompted competing suggestions about pressure and root radius. This undated report, delivered in an October-labelled folder, helps explain why a fuller-looking part was not automatically a better functional part. It does not establish the exact trial date or the outcome of the proposed later production run.
Inspect the function at every position
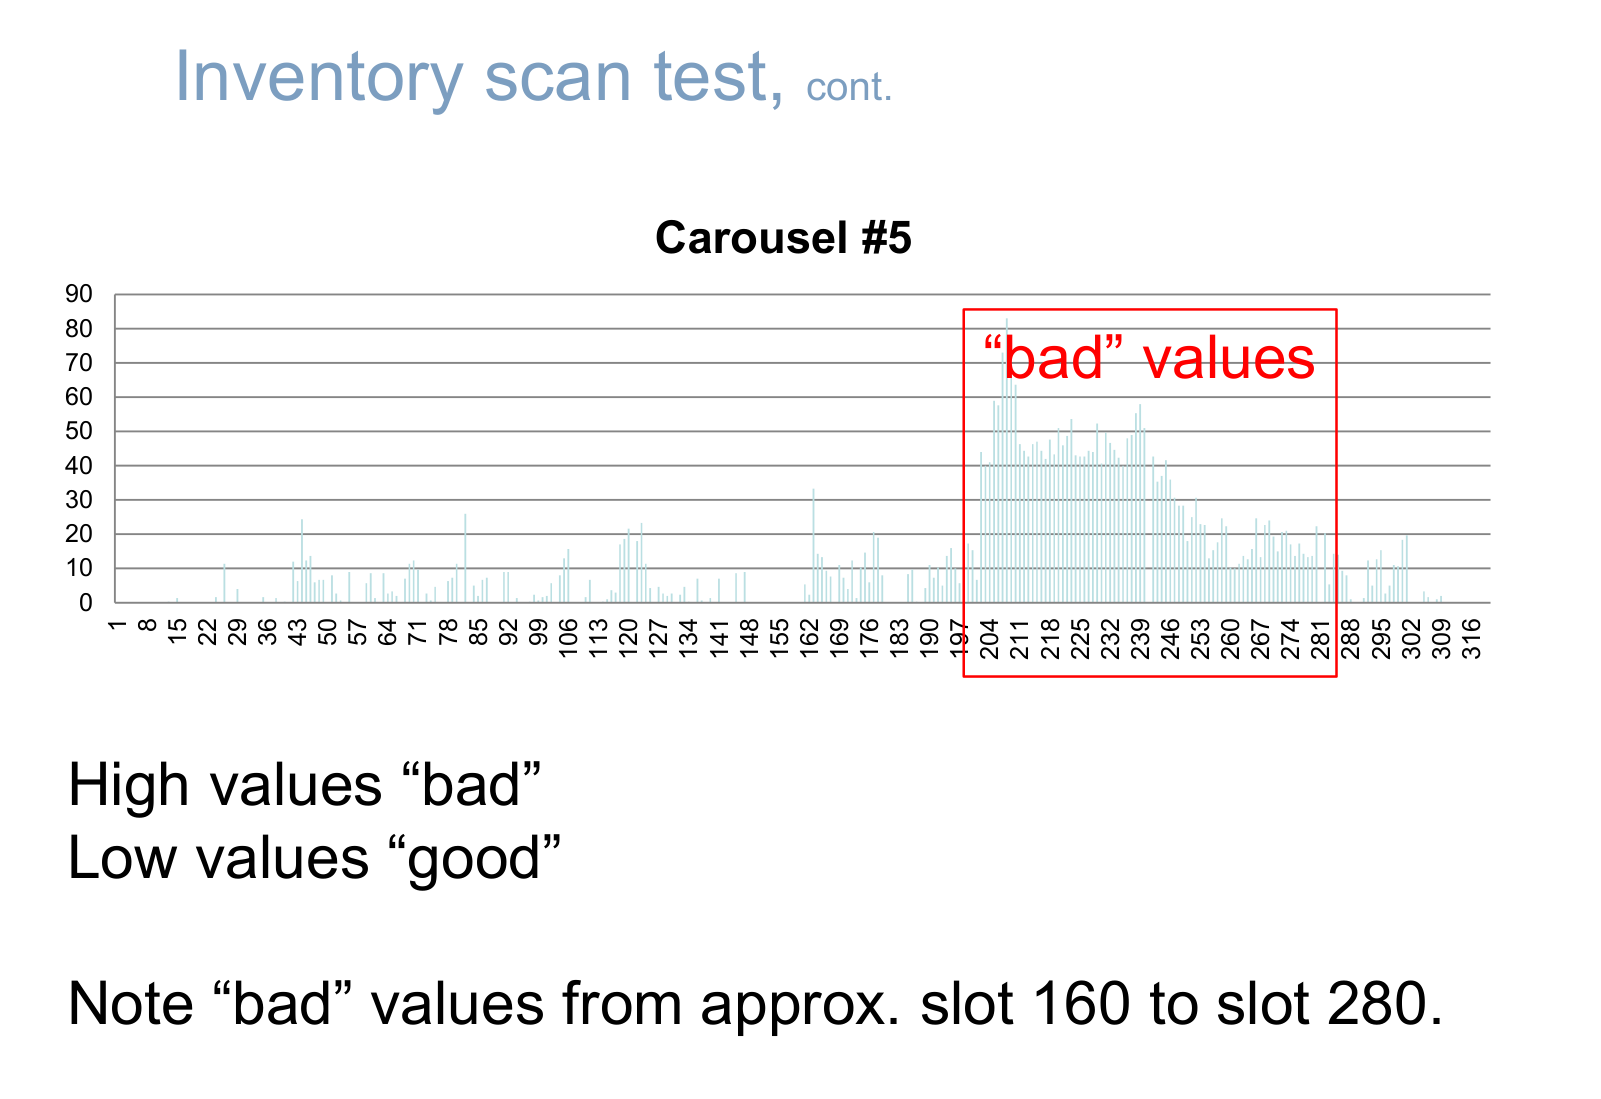
A pilot disc did not seat correctly at slot 205. The investigation compared the narrow local slot and its ribs with other positions and with a disc whose edge was thicker than its nominal body. Later inventory scans showed repeated problem regions around the carousel. The working hypothesis included differences between tooling sections and the electrode setups used to make them; the source proposed that cause rather than proving it.
The controls became more specific. Temporary instructions distinguished removable flash from physical damage that required rejection. The slot procedure called for three inspection discs in all 320 positions, letting each settle under its own weight and checking alignment. Separate instructions controlled the height of the ejector-pin pads. These were functional checks directed at the actual handling interface. The procedures describe what to do; they do not prove that every manufactured part received the checks.
The photographs made those local conditions traceable. A November report explicitly separated raw, unreworked samples and marked inspection locations around a part before showing the slot edges in close-up. The numbered locations were a way to return to the same geometry. They were not a count of defective parts or a measure of production yield.
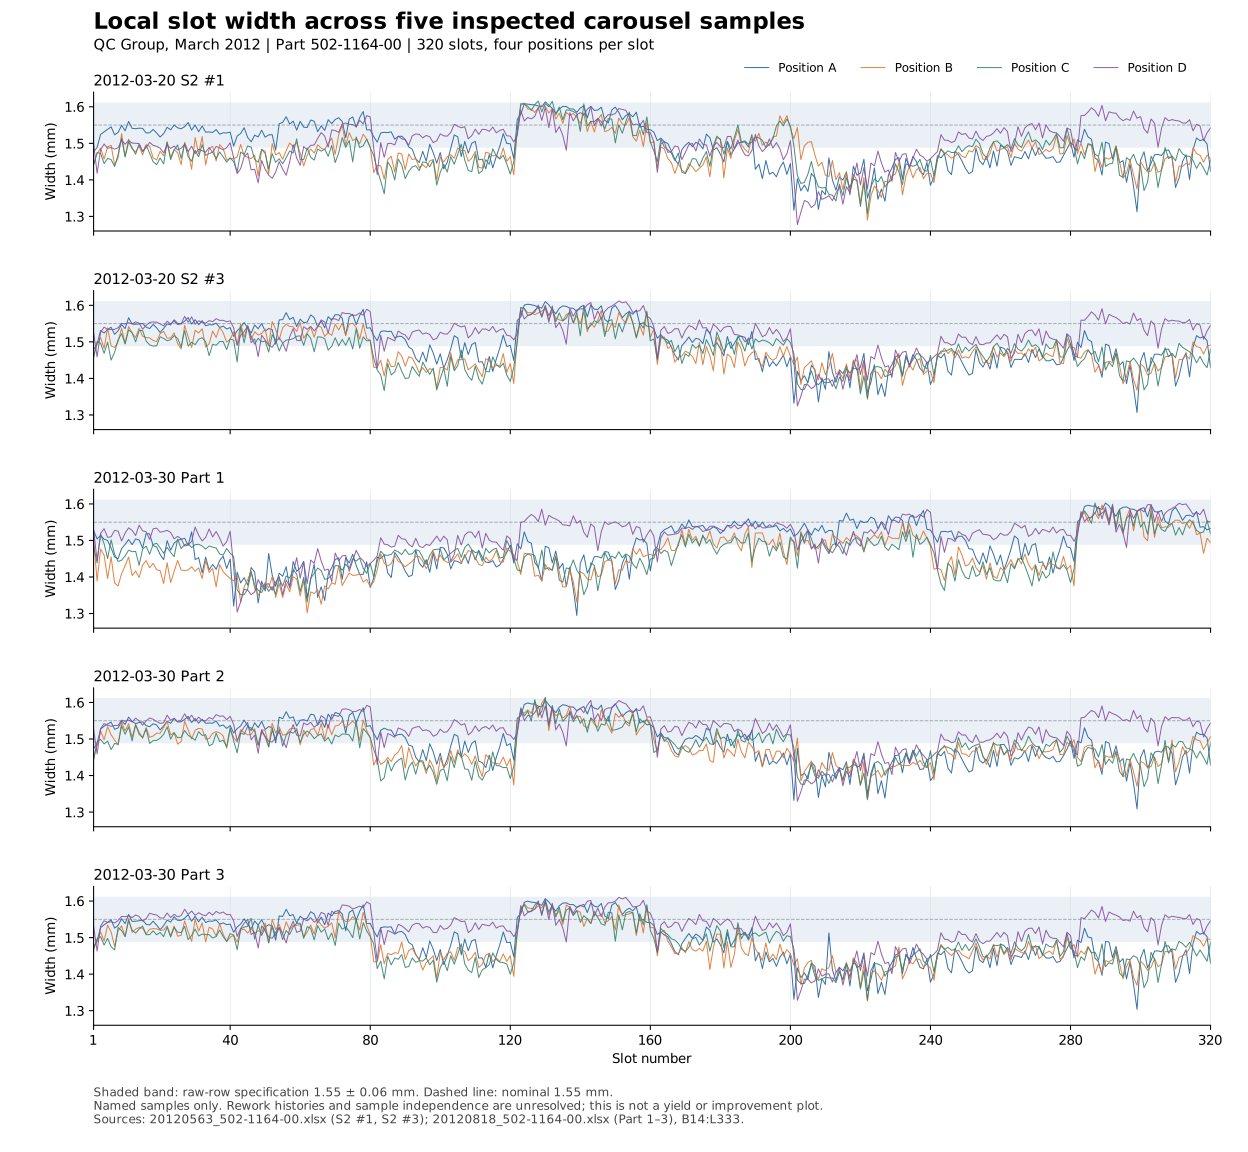
Metrology adds evidence at two different scales. QC Group’s August 2011 laser-scan report compares the overall part with CAD. Its March 2012 native workbooks go position by position: two named samples on March 20 and three on March 30, each with all 320 slots measured at four source-labelled positions. The 6,400 raw readings show how width varies around a carousel and within a slot. Several profiles contain broad narrow regions and abrupt changes, making the local nature of the problem visible.
The figure plots those readings against the limits carried on the measurement rows, 1.55 ± 0.06 mm. It deliberately preserves the sample identities and dates. We have not established whether those samples share a molding lot, treatment or rework history, so the two dates cannot be presented as a controlled before-and-after improvement. Nor do selected inspection samples provide a production-yield or capability result. The workbook matters: its March 30 PDF shows only Part 1, while the native file also holds Parts 2 and 3.
By February 2012, the review called for replacement of four tool sectors, with another conditional on the slot-120 problem, and for samples to be inspected and reworked against the gauge procedure. REV 12 records the gauge thickness change from 1.2 to 1.4 mm. Tool-steel views then clarified a dimension and its polishing allowance; tool-versus-part tables and the slot-120 RFQ examined whether to replace a section or repair it. The repair request considered adding steel and reburning, and asked for alternatives, cost and lead time. The archive preserves those requests without giving every proposed repair an invented completion.
A slot-by-slot comparison placed the tool measurements beside molded-part readings. All 320 values in its tool column trace to the eight gate reports. The comparison kept tooling geometry and part measurements distinct while focusing the review on particular sectors and slots.
Local slot measurement
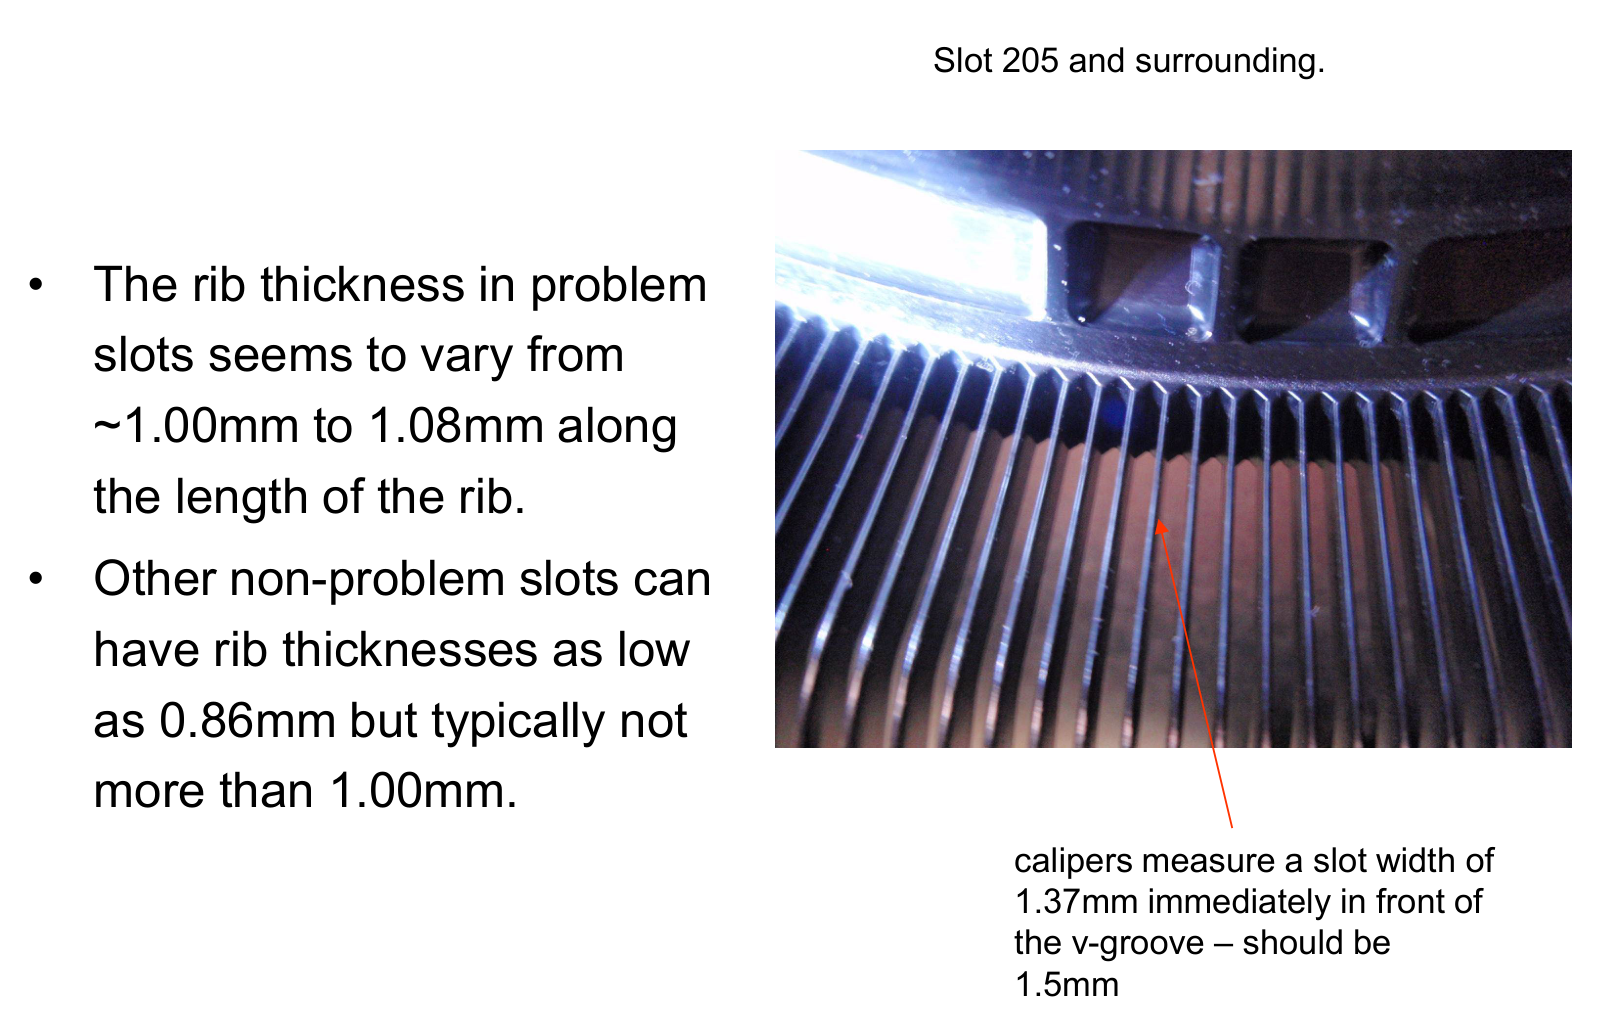
Optical inventory scan
Local slot width across five inspected samples
QC Group, March 2012: five named samples, 320 slots and four reported measurement positions per slot. Values are read from the raw workbook cells. The shaded band is the row specification, 1.55 ± 0.06 mm. Sample independence and rework histories are unresolved; this is not a yield or improvement comparison.
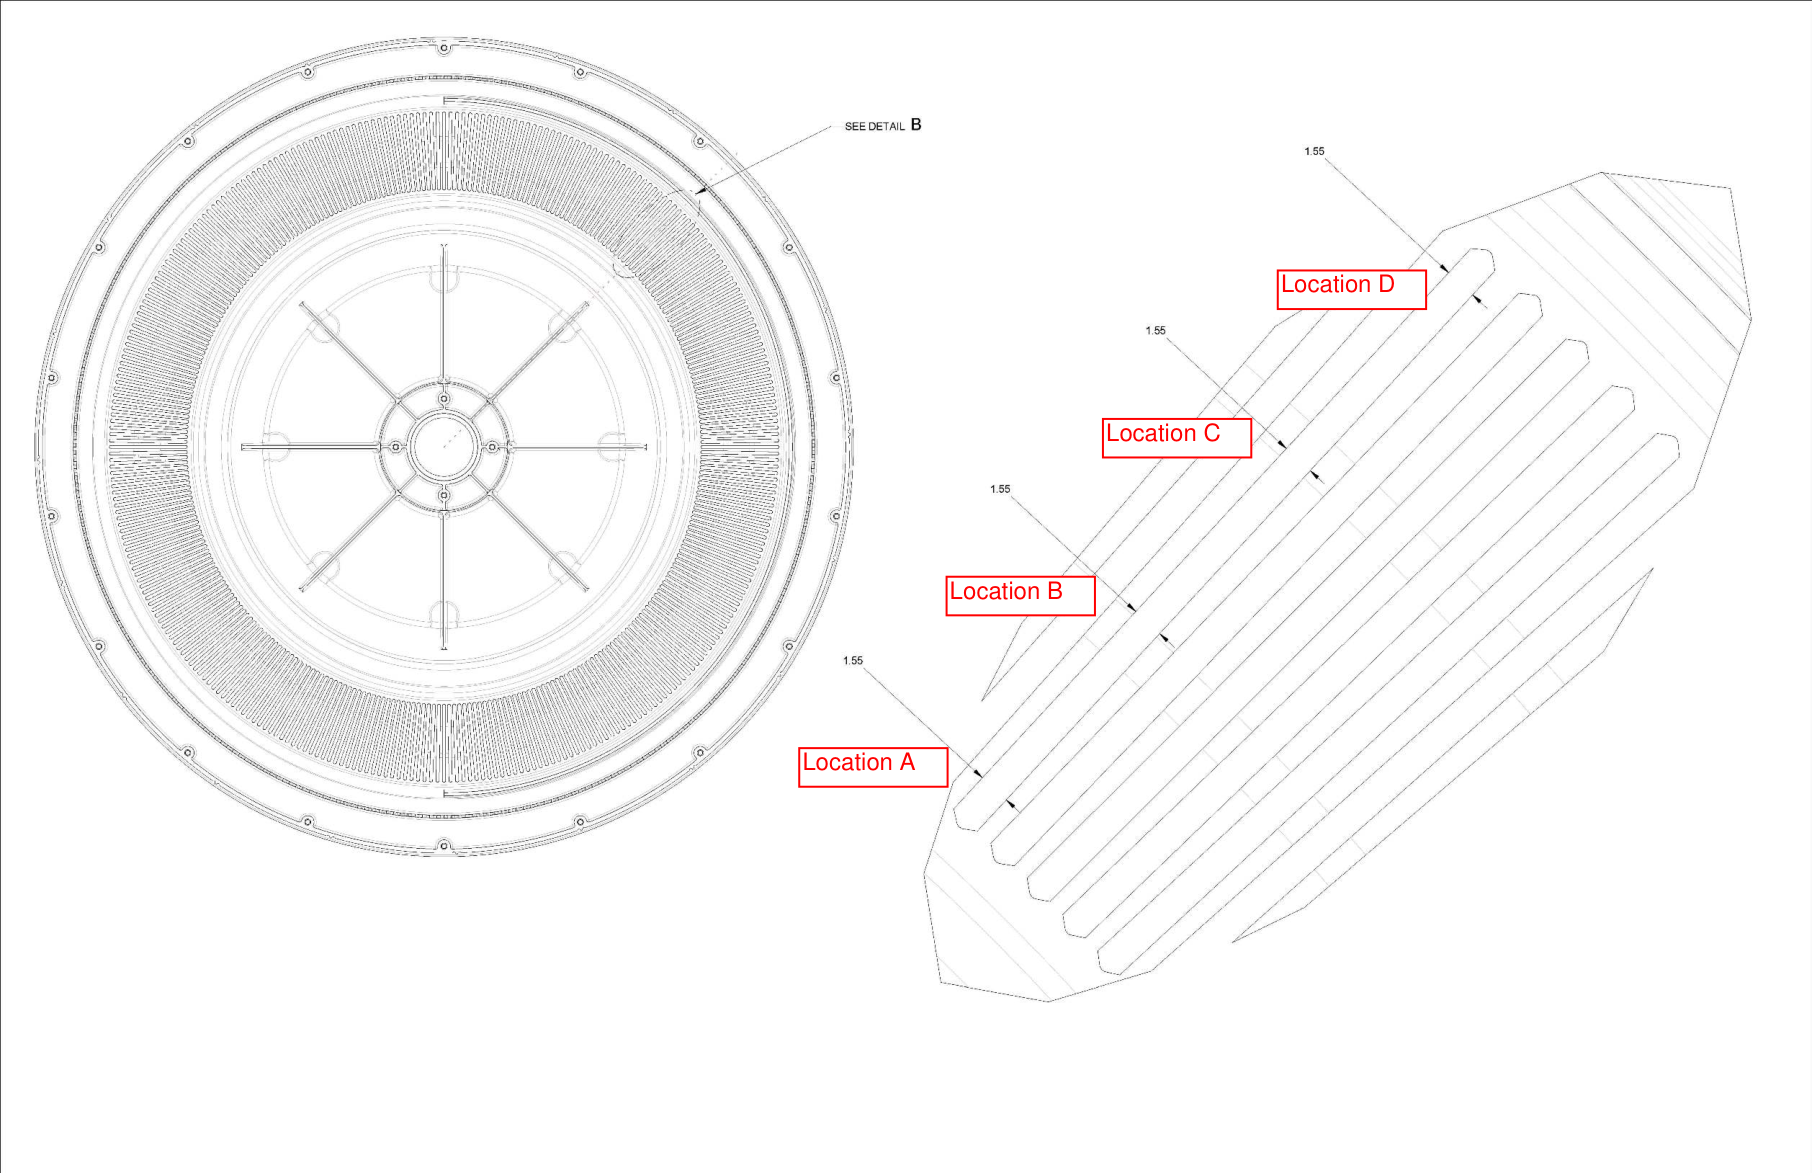
Four inspection locations
The inspection-location drawing labels four positions, A through D, along a slot. The QC workbooks report those same four location labels for each of the 320 slots. Matching labels establish the drawing-to-workbook context; they do not independently verify the physical probing setup.
A redesign had to preserve the interfaces
The 2012 new-tool discussion was broader than correcting one slot. Yomura proposed new gate positions and a 32-section rib layout. In the May response, I worked through the implications for kicker clearance, roller-track keepouts, recessed slot numbers and the metal retaining ring. A preliminary peripheral-piece concept was considered alongside a proposed snap-in arrangement. Those pieces were not the eight sectors of the original mold.
The follow-through shows why the geometry remained a negotiation. In June, Yomura warned that a curved design could improve flow while reducing stiffness, and that thicker plastic could weaken the remaining mold steel. It proposed moving ribs to the core side and kept an extra rib conditional on the actual trial. The supplier also preferred embossed IDs over the requested recesses. July comments revisited the IDs, a proposed surrounding step and the balance between root radius, strength and sink. These are unresolved design choices in the record, not a finished new tool.
The June 26 revision of the new-carousel drawing was released for prototype and final tooling review. It marked keepout areas on the upper and lower roller surfaces and retained a zero-flash requirement in all 320 disc slots.
By July 11, a 502-1189 SLA prototype review was correcting the direction of the home ring. That gives the redesign a concrete prototype stage in the record. It does not establish that this design, or the separately quoted 2015 replacement tool, reached production.
Continue at the system and production-support level
Later work returned to the whole disc path. February 2014 bench reports documented repeated loading through slot 320, scratches and observations around the roller frame, alignment features and motor wiring restraint. Returned roller assemblies were also tested in a common carrier under stated conditions. Failure to reproduce their original complaints in that setup did not clear every returned unit or validate all 320 positions. A later RMA summary explicitly separated the customer’s complaint from a theory, reproduced finding or unresolved case.
Further tests preserved failures as well as non-reproductions. A rear-path run with the cone fitted reported no transfer trouble and still recorded disc scratching. In March, one donor front-roller assembly immediately rejected the attempted disc. Another assembly, left unidentified in its report, failed to accept a disc; its report records repeated startup motion and an obstruction warning on restart. These observations kept attention on the interfaces around the carousel; they did not establish the molded carousel as the cause of every handling fault.
In April, Nathan reported tests of revised guides, bearing blocks and spring loads. He observed permanent set in the triple-force spring and reported four run-in cycles with double-force springs, including dirty rollers and a unit that reproduced a rib hit. My follow-up separated the near-term guide, bearing and spring changes from broader alternatives and from bushings or gears that still needed tests. These are bounded observations and implementation plans, not a fleet-reliability result.
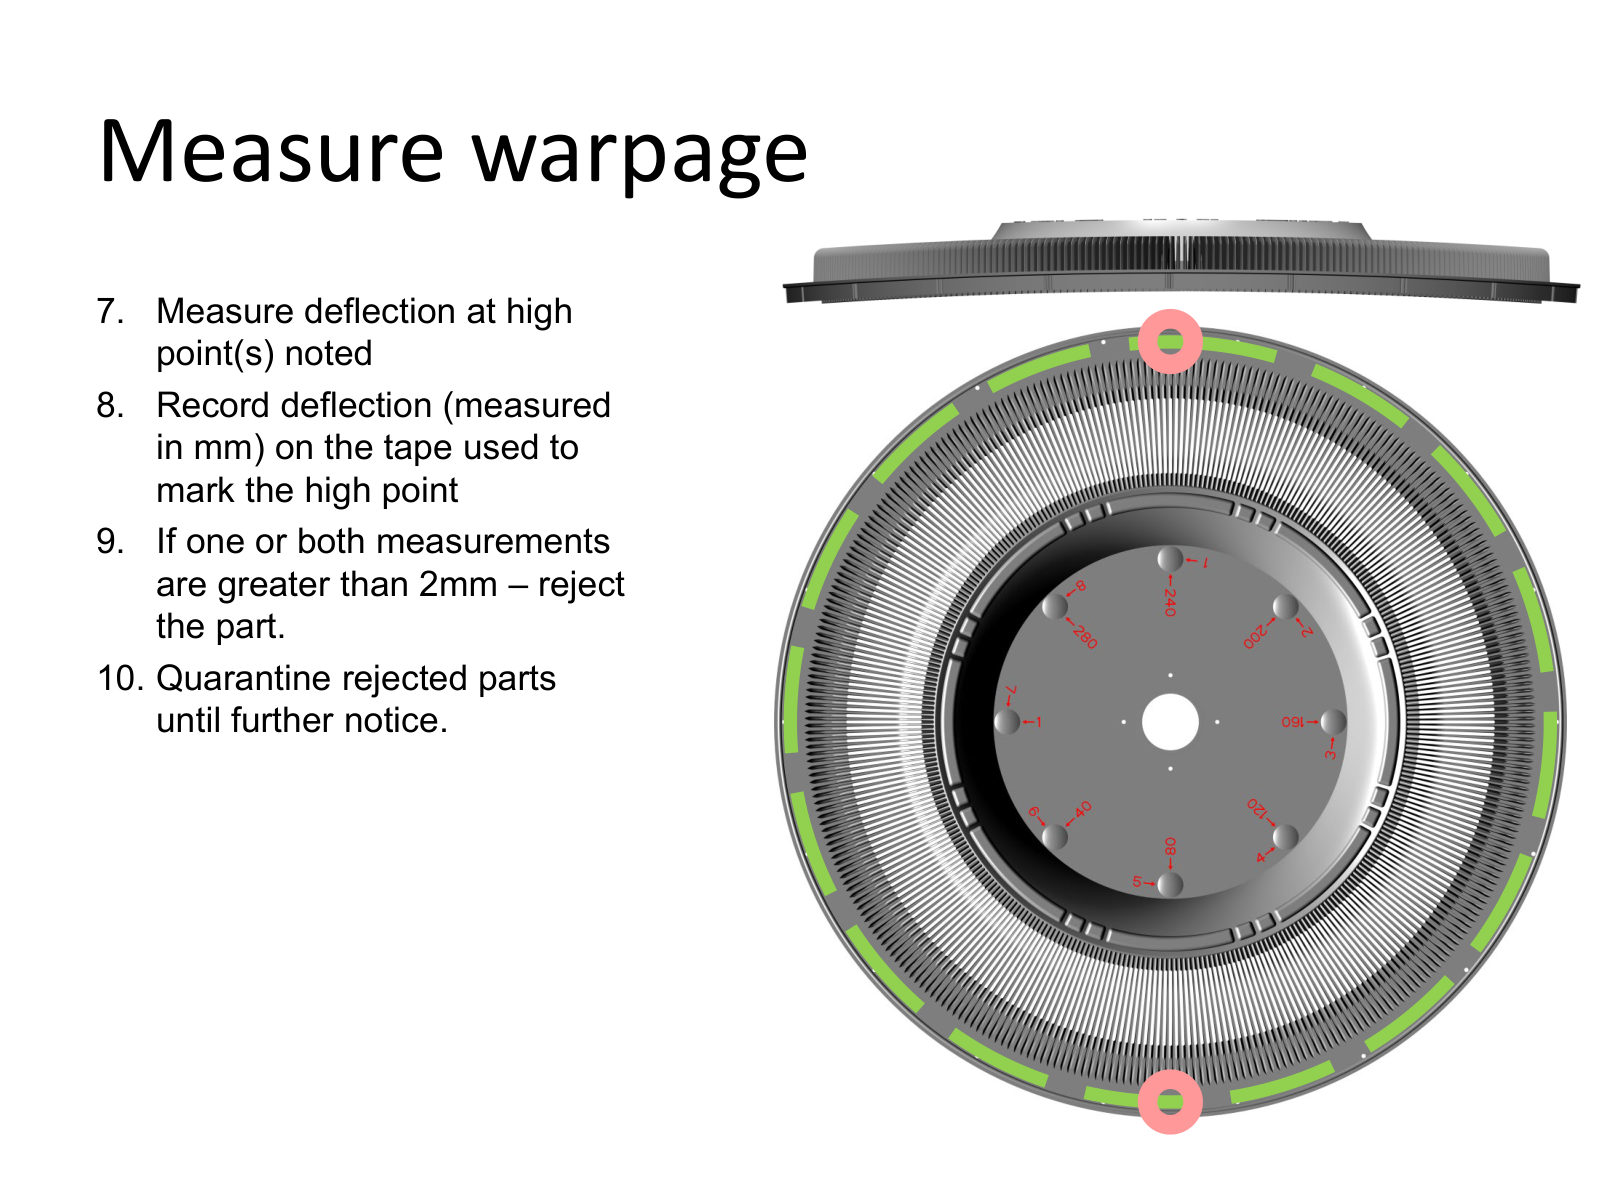
The carousel itself also needed production controls. Warpage inspection and packaging instructions were revised; rejected parts were dispositioned through a later scrap chain. The records do not prove that packaging caused the field problems or that the revised packaging eliminated them.
The supported replacement-tool endpoint is still a January 2015 quotation followed by internal review. Many changes reached production, but the exact combination and final replacement-tool outcome remain unresolved.
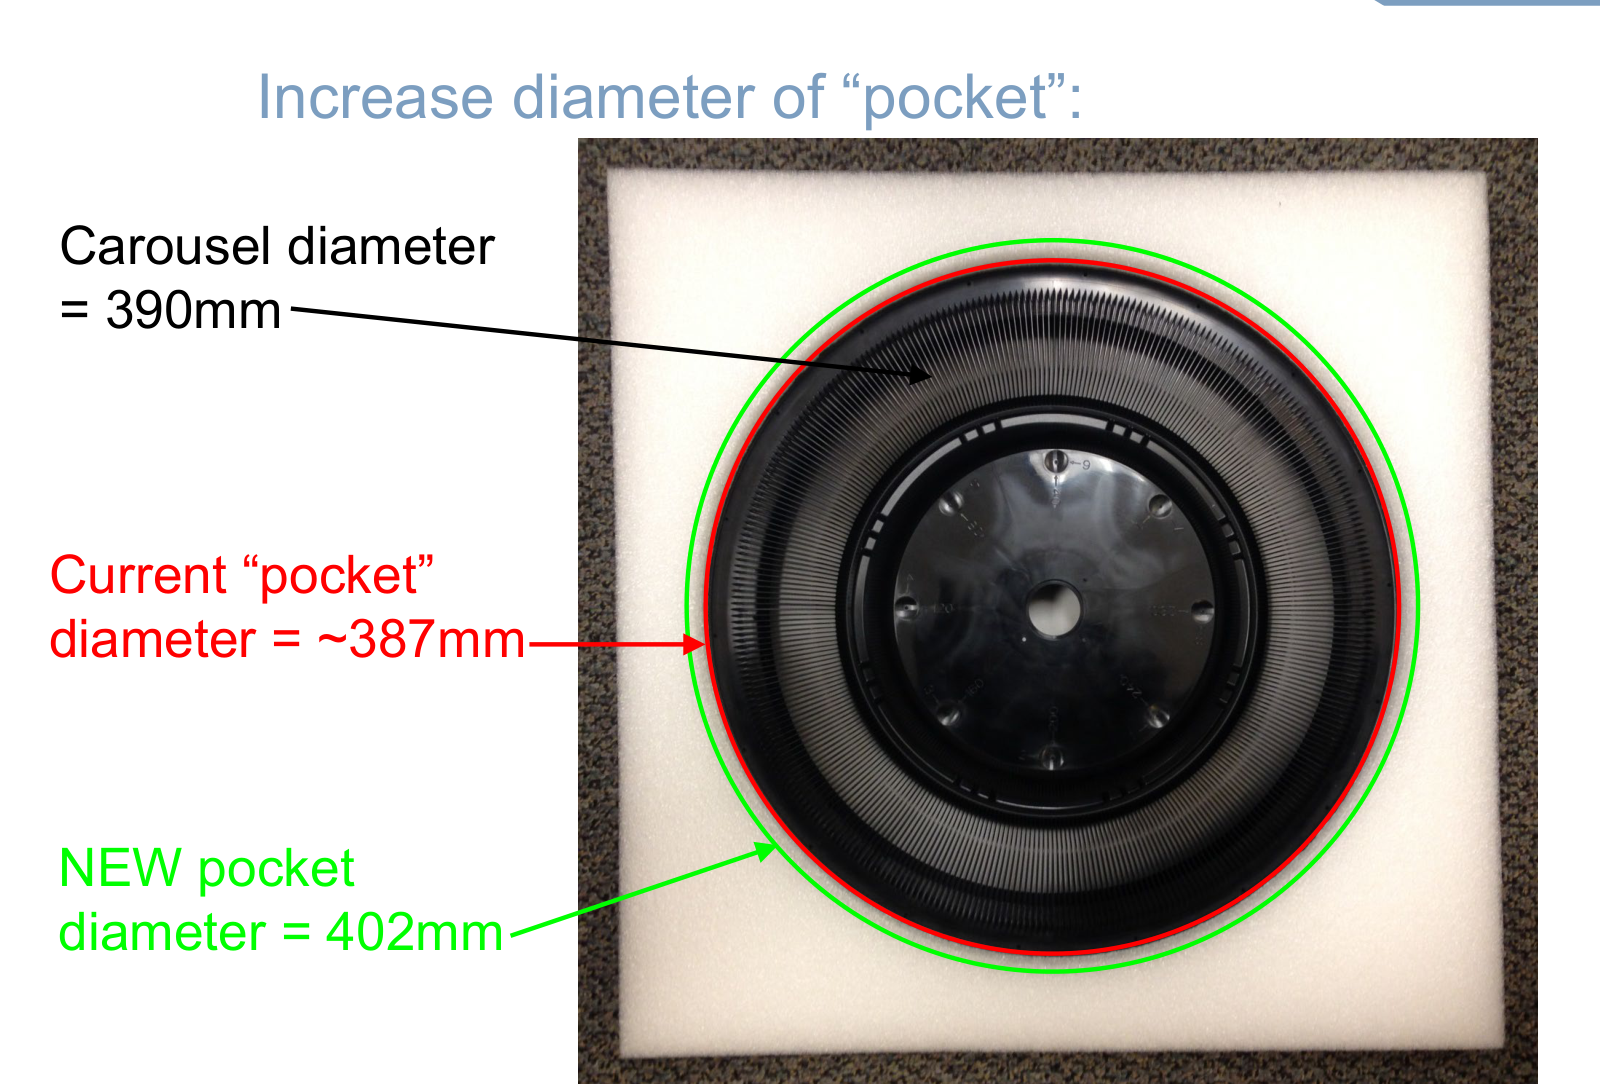
Packaging clearance
Warpage inspection
Development chronology - working selection
-
Capacity alternatives fitted to the enclosure
Function compares disc-spacing assumptions and 250/300/350/400-disc envelopes. The assumed 1.4 mm spacing is a sizing input, not a measured Vesta slot result.
Function Engineering.
Read this phase ↓ -
300-disc plan enters breadboard development
D. Northway notes 300 discs as the plan of record in the sizing deck. The end-of-phase report proposes a 300-disc molded platter with belt drive, idlers, home flag, per-slot encoder teeth, central support and three support rollers. Foreign objects, 80 mm discs, obstruction sensing and thickness assumptions remain open. The later June 16 250-disc concept shows overlapping alternatives, not a simple linear capacity increase.
Function Engineering; D. Northway.
Read this phase ↓ -
A 250-slot concept
Function records a 250-slot HIPS concept after the June 4 report described a 300-disc plan. This demonstrates overlapping alternatives, not an unambiguous linear 250-to-300-to-320 sequence. The final 320-capacity decision remains unresolved.
Function Engineering.
Read this phase ↓ -
Capacity and handling requirements
Requirements Rev 4 targets at least 300 discs while retaining 250-or-more background wording. Pinch rollers, kickers and carousel are one coordinated handling system; reliability, serviceability and content protection are requirements, not demonstrated results.
Kaleidescape; Function Engineering.
Read this phase ↓ -
Breadboards establish the handling approach
Function reports four slot-geometry breadboards and a full SLA carousel. V-grooves constrain discs and align them with the kicker; alignment sensitivity and transport timing were investigated. Complete-system control/position confirmation and life testing remain next steps.
Function Engineering.
Read this phase ↓ -
Multiple hot-runner layouts simulated
Yudo compares 26-, 18- and 12-drop layouts for PH-879 PS. Predictions concern filling, weld lines, injection pressure and clamp force; they are not measured trial performance.
Yudo.
Read this phase ↓ -
Eight-drop molding study
Yudo models an eight-drop layout in a separately dated PH-879 report. The report shows localized short-shot and weld-line predictions; no controlled solver-to-solver performance conclusion is proposed.
Yudo.
Read this phase ↓ -
Tool progress reported at 90 percent
The seventh report shows 90 percent actual progress at December 27. January 6, 2011 appears as a future schedule column with no actual total; do not turn it into a tool-completion date.
Function Engineering.
Read this phase ↓ -
T1 fills at the cost of flash and broken ribs
Function photographs overshot parts and broken fins; later summary reports intentional over-pressure to fill the tool. Brittle appearance does not settle resin-versus-processing causality.
Function Engineering; ChunKing.
Read this phase ↓ -
T2 exposes the fill-path problem
Meeting notes and trial reports describe balancing the center before filling the inner-ring/rib/outer-hub region, a narrow process window, unequal tool temperatures and material trapped in the cavity. The team explores ejection, flow leaders, venting and alternative resins.
Loyd May; Joel Jensen; Thomas Chen; Ze Shen Wong; Erik Norris; Zao Tech.
Read this phase ↓ -
Ribs and radii revised; T3 samples produced
Loyd diagrams additional ribs and larger blending radii. Separately, T3 at Sheng Ming yields 46 ABS and 46 HIPS samples; pin-punch/knit-line defects remain and further dimensional inspection is requested. Neither event alone proves approved production.
Loyd May; Sheng Ming; Alan Wu; Erik Norris.
Read this phase ↓ -
Tooling quote advances to internal PO approval
Updated T4 plan reports the Jan 29 quote and an approved internal PO request for the rib/radius changes. It also documents undersize diameter, dish, flash, incomplete V-grooves and voids.
Erik Norris; Alan Wu.
Read this phase ↓ -
T4 includes implemented ribs but persistent local defects
Function labels one photograph Implemented Ribs. Short shots and air-trap marks remain; the later summary reports consistent fill but undersize diameter. A proposal to widen vents to 20 mm follows.
Function Engineering; Sheng Ming.
Read this phase ↓ -
Actual tool configuration challenged
Loyd asks Alan to identify vent-land geometry at all 16 locations and reconcile it with earlier sketches and the latest drawing. He also asks for numbered hot-runner wiring to prevent connection errors.
Loyd May; Alan Wu; Erik Norris.
Read this phase ↓ -
A disc does not seat at slot 205
Later November report dates this observation to June. Local slot/rib geometry and a thick disc edge explain why overall diameter alone is insufficient. Preserve observed dimensions and avoid treating 0.86 mm comparison as a universal nominal spec.
Read this phase ↓ -
Venting the ejector pins proposed
After larger core vents failed to markedly improve trapped air, Loyd recommends added release channels on 45 ejector pins. Diagram divides them into 21 10 mm and 24 6 mm pins. This establishes the proposal and mechanism, not its success.
Loyd May.
Read this phase ↓ -
Physical samples reveal sector transitions
Loyd annotates local sample readings and differences in rib height/profile where cavity inserts meet. The same date appears in REV 9 drawing history for drawing updates, venting ejector pins and ramp-wall thickening. The two records establish observation and drawing intent separately.
Loyd May; Erik Norris.
Read this phase ↓ -
Laser-scan comparison documented
QC Group issues a precision laser scan and 2D report for 502-1164-00. Whole-part color comparison and hub/sector views establish a metrology strand before the later all-slot CMM tables. The scan and slot-width measurements are different measurement products.
QC Group; Steve Traynor.
Read this phase ↓ -
Slot scan exposes regional variation
Five-carousel inventory scans and local measurements focus investigation on repeated narrow-slot regions. Different EDM electrode setups are a proposed cause; section replacement or reburning are suggested fixes.
Read this phase ↓ -
All-slot inspection procedure defined
Procedure calls for cycling three inspection discs through all 320 slots, letting each settle under its own weight, and reworking obstructions until alignment meets the illustrated condition. This establishes the procedure, not its execution on every manufactured part.
Erik Norris.
Read this phase ↓ -
Replacement sectors and stronger inspection requested
Great Mold is asked for replacement of four sectors, with another conditional on slot 120. Yomura is asked to inspect/rework samples against the revised gauge procedure.
Erik Norris; Great Mold; Yomura.
Read this phase ↓ -
Two full slot-width profiles measured
QC Group work order 20120563 records samples S2 #1 and S2 #3, each with 320 slots measured at source positions A-D. Raw G14:J333 contains 2,560 values. Regional narrow-slot patterns can be plotted with the source limits; this is neither production yield nor a cause diagnosis.
QC Group; Steven DeVowe.
Read this phase ↓ -
Three additional sample profiles preserved in workbook
QC Group work order 20120818 contains Part 1, Part 2 and Part 3, each with 320 slots at A-D. Its PDF exports only Part 1. Together with March 20, the native sheets provide 6,400 raw values. Sample lineage and rework history are not established, so dates are not a before/after improvement experiment.
QC Group; Steven DeVowe.
Read this phase ↓ -
Slot 120 repair alternatives requested
RFQ contrasts replacement using an existing spare with repair of the existing insert, including adding steel and reburning. It asks for cost/lead time and other options.
Erik Norris; Great Mold.
Read this phase ↓ -
New-tool architecture proposed
Yomura schema describes new gate positions and 32 even rib sections with modified ribs and roller-track geometry. These are proposed changes, not a released replacement tool.
Yomura.
Read this phase ↓ -
Redesign reconciled with mechanism interfaces
Erik responds to new gate/rib recommendations while protecting kicker clearance and roller tracks, requests recessed numbers, and explores eliminating the metal ring with a snap-in concept.
Erik Norris; Yomura.
Read this phase ↓ -
New-tool DFM exposes a flow and strength tradeoff
Yomura warns that curved geometry can improve flow while weakening the part and tool. It compares old and proposed rib widths while retaining the requested 1.55 mm slot, proposes core-side ribs and makes an extra rib conditional on actual trials. Embossed IDs conflict with the earlier recessed-ID preference.
Yomura.
Read this phase ↓ -
SLA home-ring orientation corrected
A 502-1189 proto1 review contrasts incorrect and corrected home-ring direction on an SLA prototype. This advances the redesign record to prototype review, without proving later production.
Erik Norris.
Read this phase ↓ -
Disc-path baseline records scratch and alignment observations
A known-good carrier receives repeated scripted loading through slot 320. The report documents disc scratching and observations at the roller frame, alignment features and motor cable restraint. One position and one carrier do not qualify all carousel slots or the product fleet.
Read this phase ↓ -
Packaging and inspection revised
Reviewed records describe protective packaging and revised warpage checks. Neither proves packaging qualification or elimination of field failures.
Read this phase ↓ -
Guides, bearings and spring loads tested
Nathan reports four run-in cycles, including dirty rollers and a reproducible rib-hit unit. Triple-force springs take permanent set; double-force springs pass the reported runs. This is bounded system testing, not fleet qualification.
Nathan Forster; Erik Norris.
Read this phase ↓ -
Replacement tool quoted
Reviewed native attachment identifies 502-1164-00 and Vesta 320 slots. Quotation establishes a commercial proposal, not completed replacement tooling.
Yomura.
Read this phase ↓ -
Quotation remains under internal review
Mark McKenzie replies that the quotation will be discussed internally. No later manufacturing/fleet endpoint is established.
Mark McKenzie.
Read this phase ↓